 IN
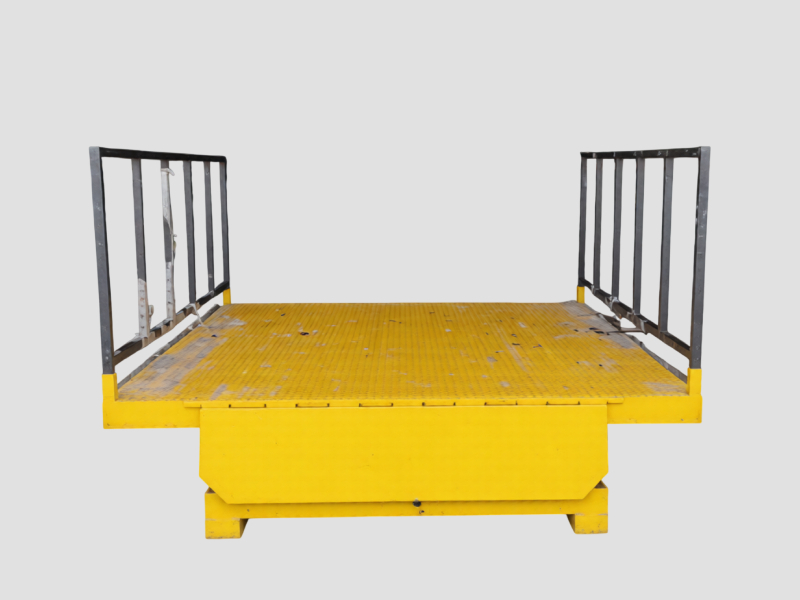
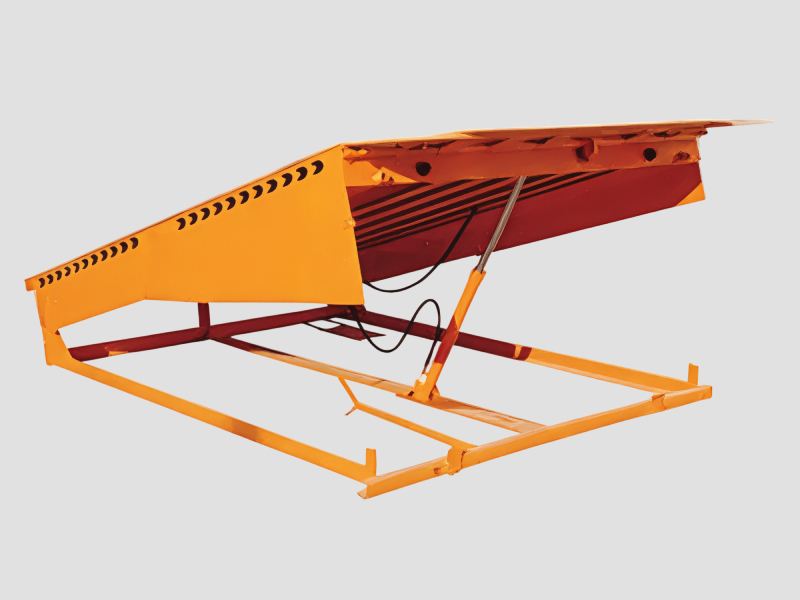
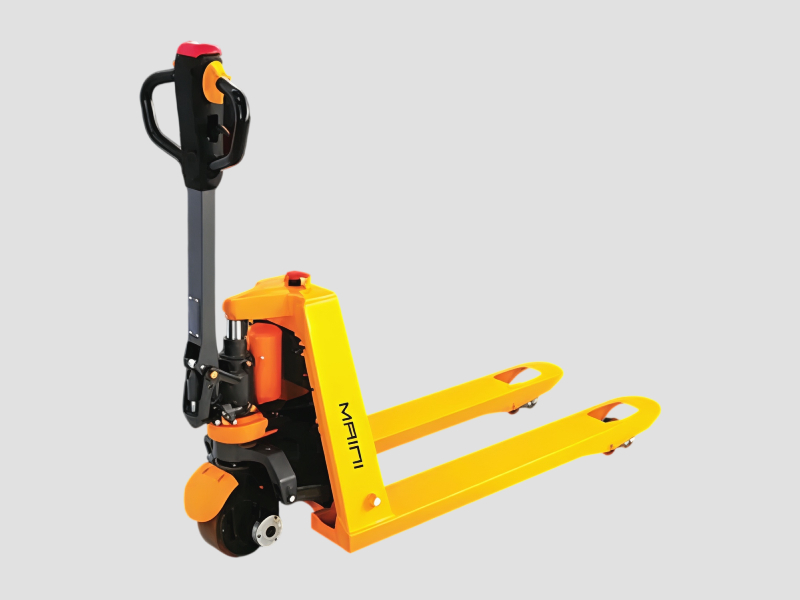
Conveyors & Material Handling Systems
2608 products available
𝗪𝗵𝗮𝘁 𝗮𝗿𝗲 𝗖𝗼𝗻𝘃𝗲𝘆𝗼𝗿𝘀 & 𝗠𝗮𝘁𝗲𝗿𝗶𝗮𝗹 𝗛𝗮𝗻𝗱𝗹𝗶𝗻𝗴 𝗦𝘆𝘀𝘁𝗲𝗺𝘀?
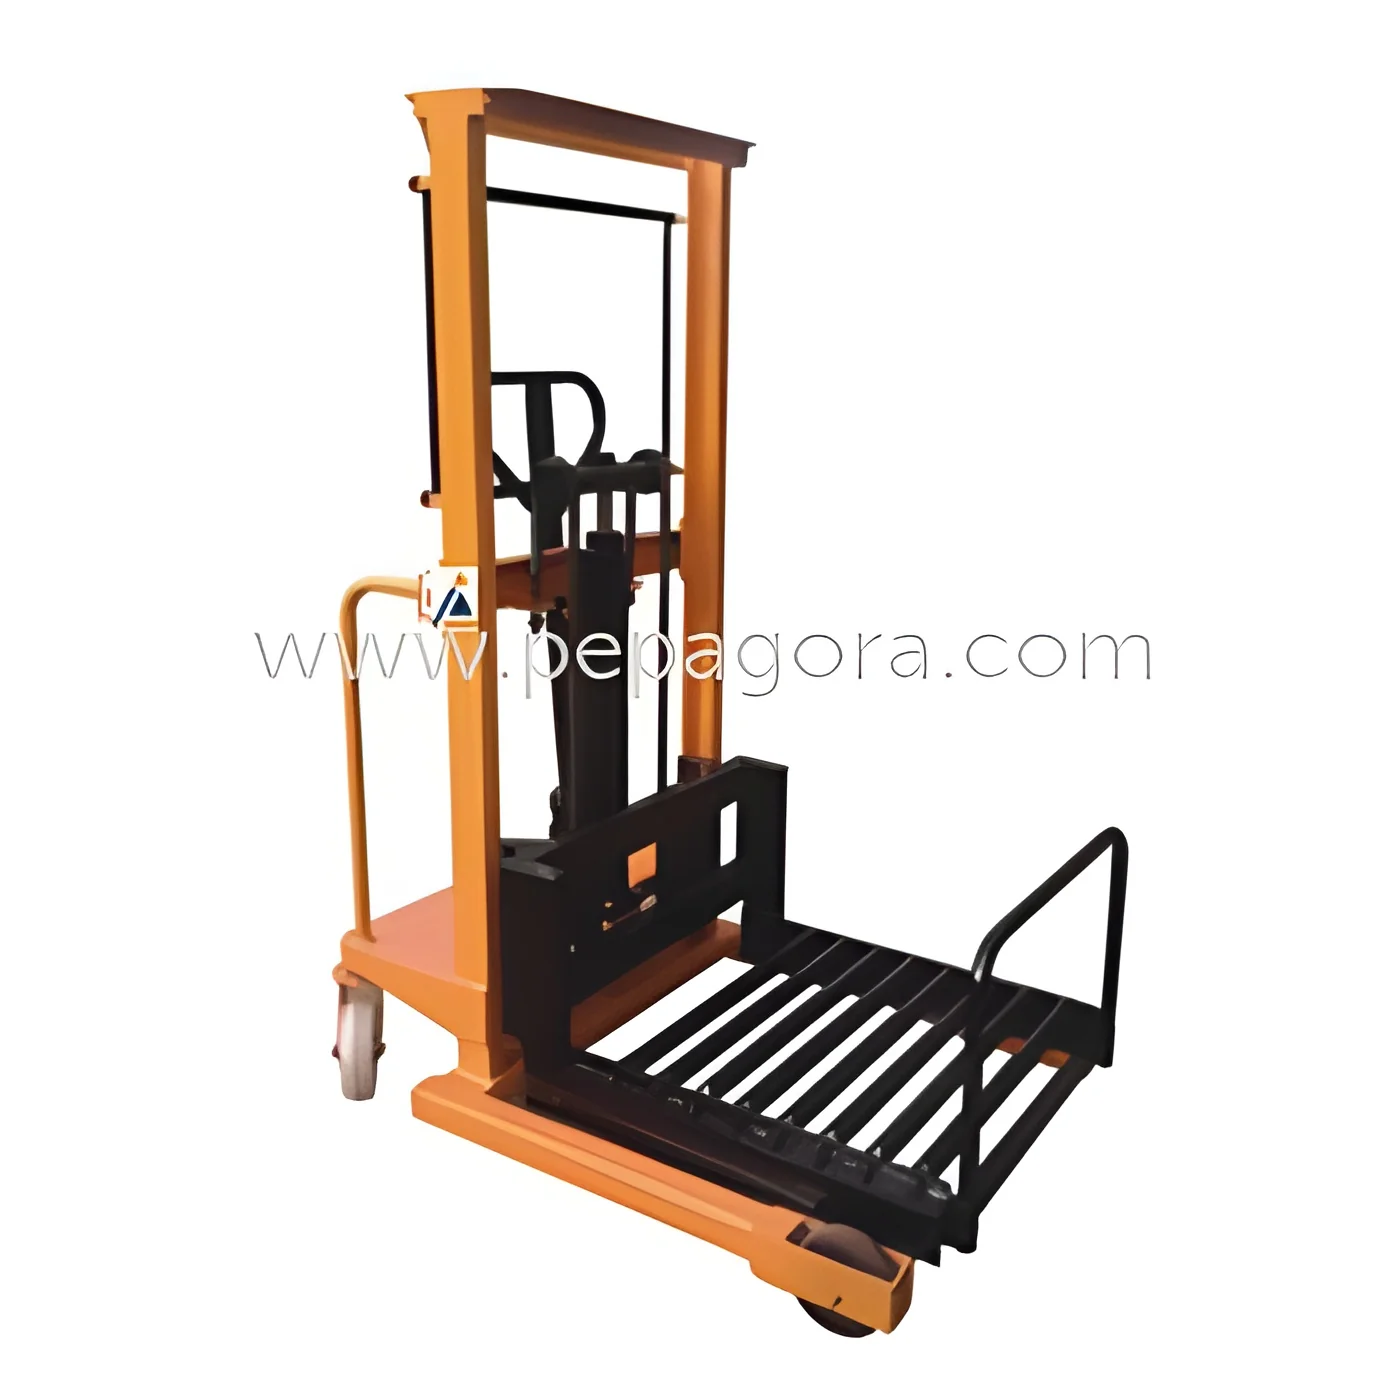
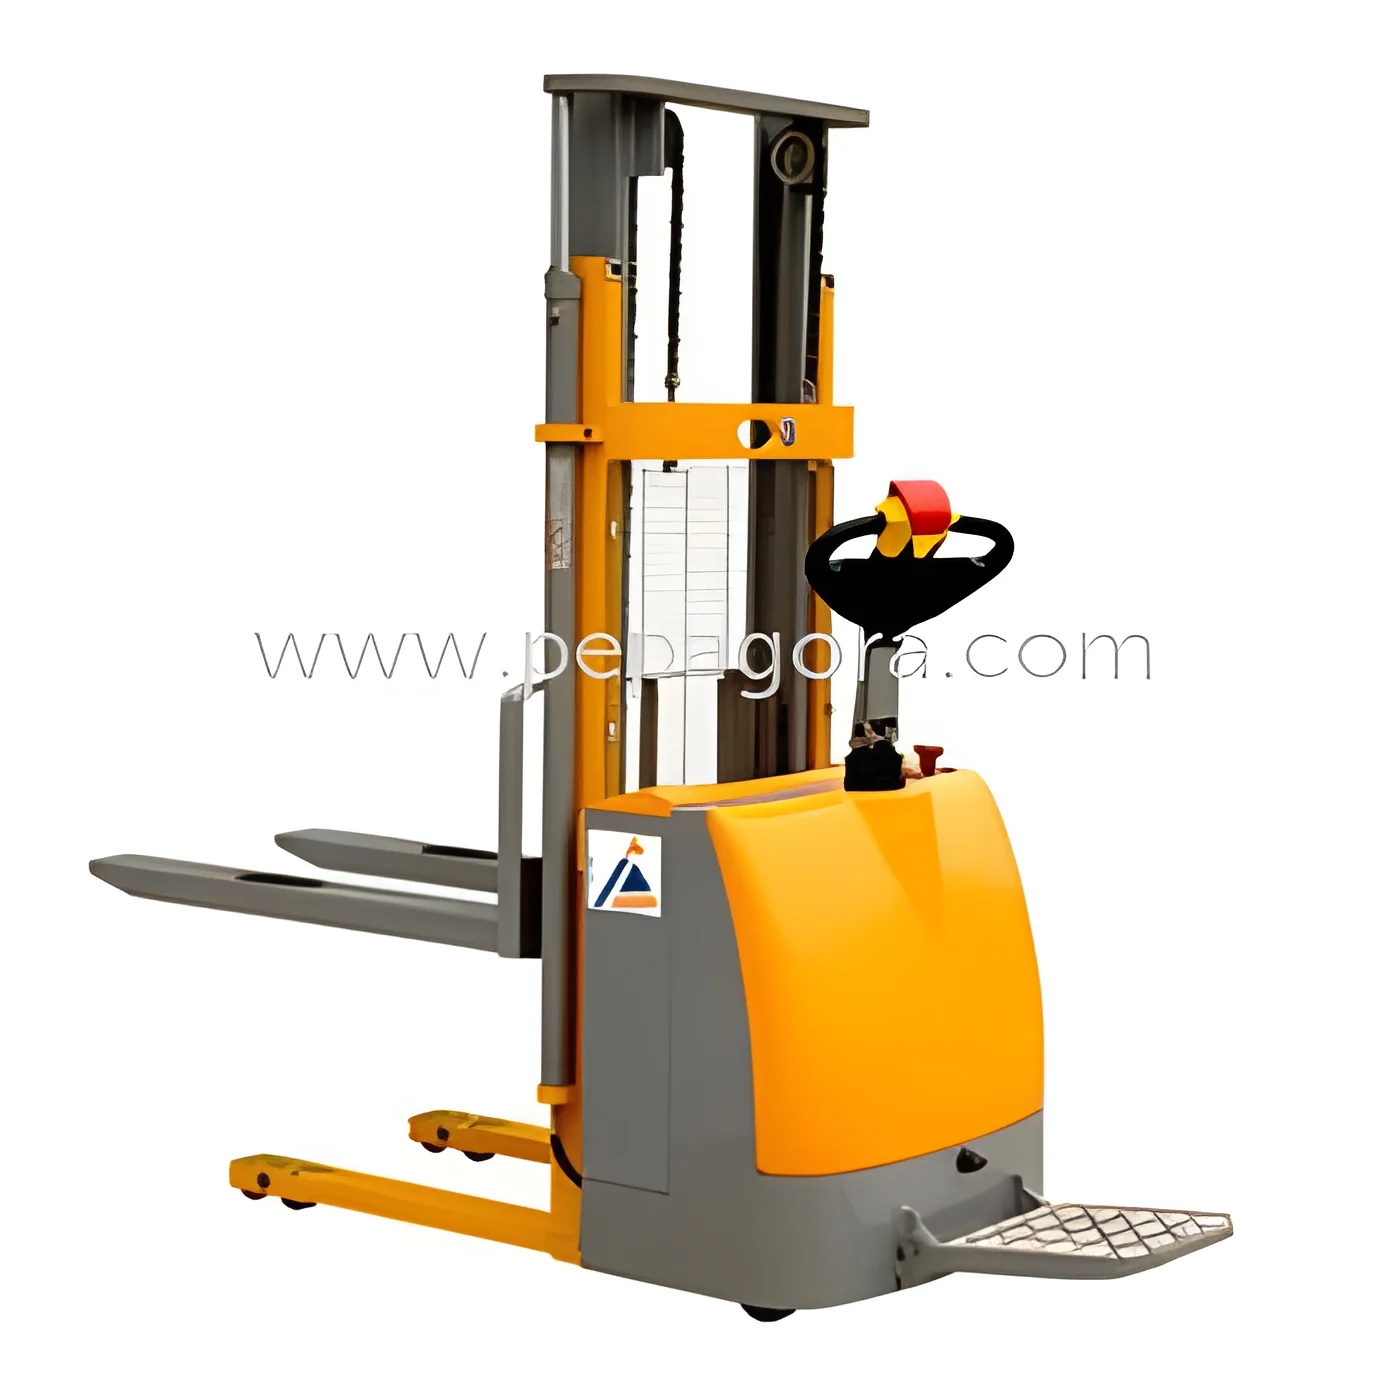
Conveyors and material handling systems are essential tools in modern manufacturing and logistics operations. These systems are designed to transport materials, products, and goods efficiently from one location to another within a facility. They can include various types of equipment such as belt conveyors, roller conveyors, and automated guided vehicles. Their primary function is to enhance productivity by minimizing manual handling and streamlining workflows.
These systems find applications in numerous sectors, including manufacturing, warehousing, distribution, and packaging. They are crucial for moving raw materials, assembly parts, and finished products throughout the supply chain. In industries like automotive, food and beverage, and pharmaceuticals, conveyors help ensure that operations run smoothly and efficiently, ultimately leading to reduced labor costs and improved safety.
The relevance of conveyors and material handling systems in today’s market cannot be overstated. As businesses continue to seek ways to improve efficiency and cut costs, the demand for advanced material handling solutions is on the rise. With the growth of e-commerce and increased focus on automation, the market for these systems is expected to expand significantly in the coming years, highlighting their importance in industrial operations.
𝗞𝗲𝘆 𝗙𝗲𝗮𝘁𝘂𝗿𝗲𝘀 𝗮𝗻𝗱 𝗦𝗽𝗲𝗰𝗶𝗳𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀
When selecting conveyors and material handling systems, it is essential to understand their key features and specifications. These specifications will help determine the right solution for specific business needs.
Key specifications include:
1. Material Construction
- Common materials include steel, aluminum, and plastic.
- Each material offers different durability and weight capacities.
2. Load Capacity
- Systems can handle loads ranging from a few pounds to several tons.
- Load capacity must match the operational requirements.
3. Speed
- Conveyor speeds typically range from 10 to 100 feet per minute.
- Speed selection depends on throughput needs.
4. Width and Height
- Conveyor widths can vary from 12 inches to over 60 inches.
- Height adjustments are crucial for integration with existing systems.
5. Drive Type
- Options include electric motors, hydraulic drives, or manual systems.
- The choice affects maintenance and operational efficiency.
6. Control Options
- Systems may feature manual controls, PLCs, or remote operation.
- Control type impacts automation levels and user interface.
7. Customization Options
- Many systems can be tailored to specific layouts and processes.
- Custom features may include specialized belts, sensors, and safety devices.
8. Compliance Standards
- Ensure systems meet industry standards such as CE certification.
- Compliance is vital for safety and regulatory adherence.
In summary, understanding these specifications is crucial for businesses looking to optimize their material handling processes.
𝗖𝗼𝗺𝗺𝗼𝗻 𝗔𝗽𝗽𝗹𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀 𝗮𝗻𝗱 𝗨𝘀𝗲 𝗖𝗮𝘀𝗲𝘀
Conveyors and material handling systems serve various industries with tailored applications.
1. Manufacturing: In manufacturing, conveyors are used to transport raw materials and components throughout the production line, enhancing assembly efficiency and reducing manual handling.
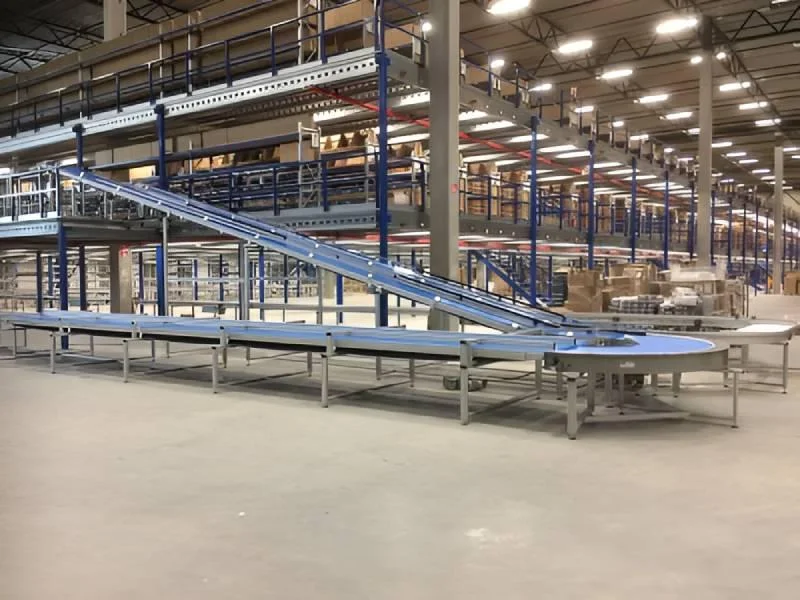
2. Warehousing: In warehousing, these systems facilitate the movement of goods from receiving areas to storage and picking locations, streamlining inventory management.
3. Food and Beverage: In the food industry, conveyors transport products through processing and packaging lines while adhering to strict hygiene and safety standards.
4. Pharmaceuticals: In pharmaceuticals, conveyors help maintain product integrity by minimizing handling during the packaging and distribution processes.
5. Automotive: In the automotive sector, conveyors are crucial for moving parts along assembly lines, ensuring timely production rates.
6. Retail: In retail distribution centers, conveyors assist in sorting and transporting products for order fulfillment, improving overall efficiency.
7. Construction: In construction, material handling systems move heavy materials like concrete and aggregates, reducing labor costs and improving safety.
𝗣𝗿𝗼𝗱𝘂𝗰𝘁 𝗩𝗮𝗿𝗶𝗮𝗻𝘁𝘀 𝗮𝗻𝗱 𝗦𝘂𝗯𝗰𝗮𝘁𝗲𝗴𝗼𝗿𝗶𝗲𝘀
Conveyors and material handling systems come in various forms to meet diverse operational needs.
Belt Conveyors
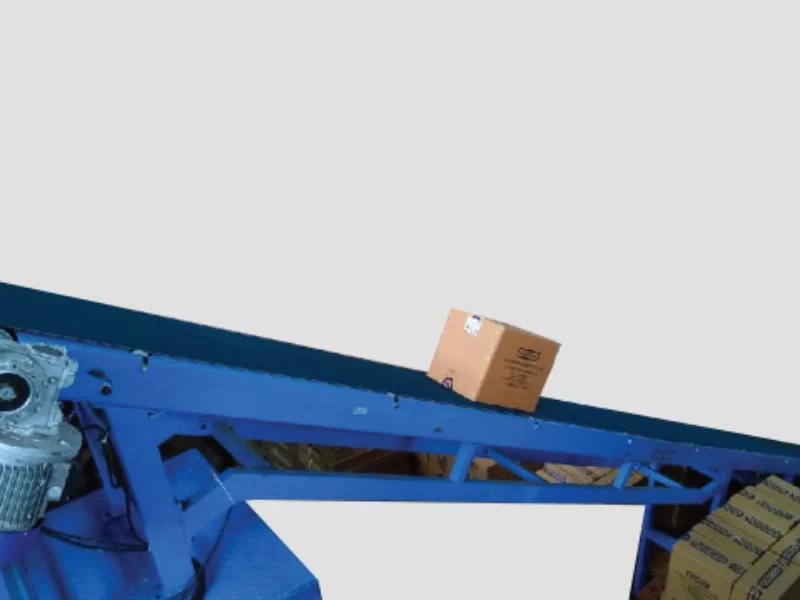
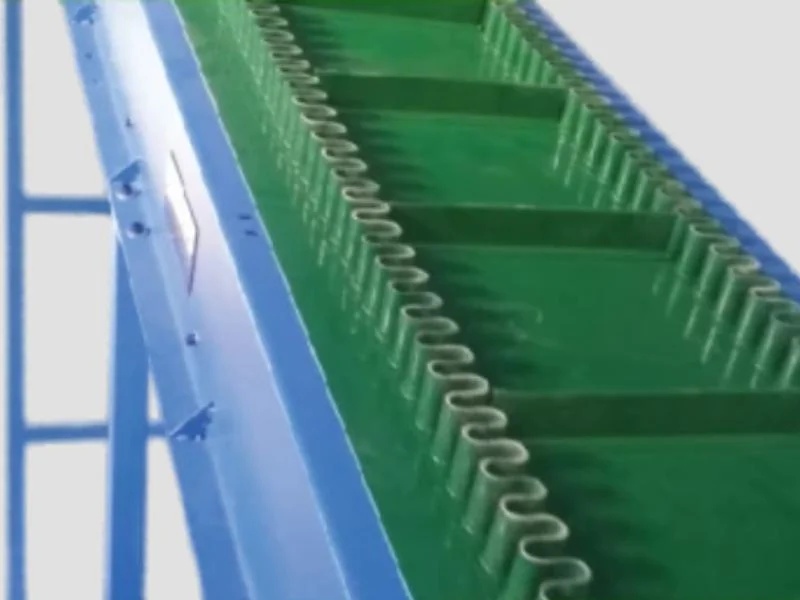
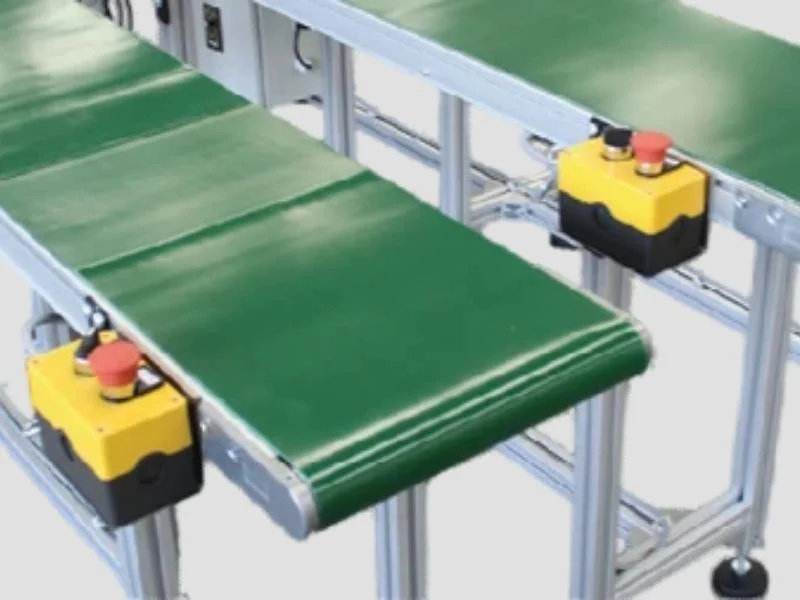
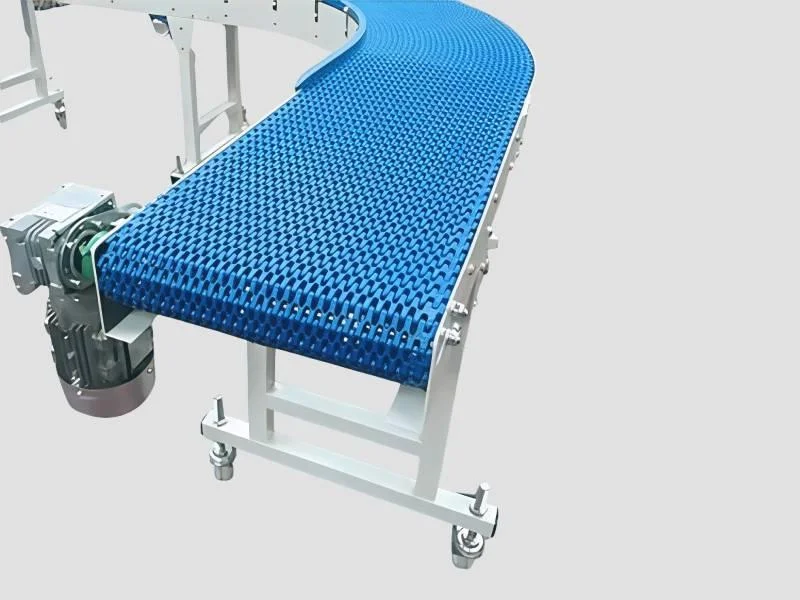
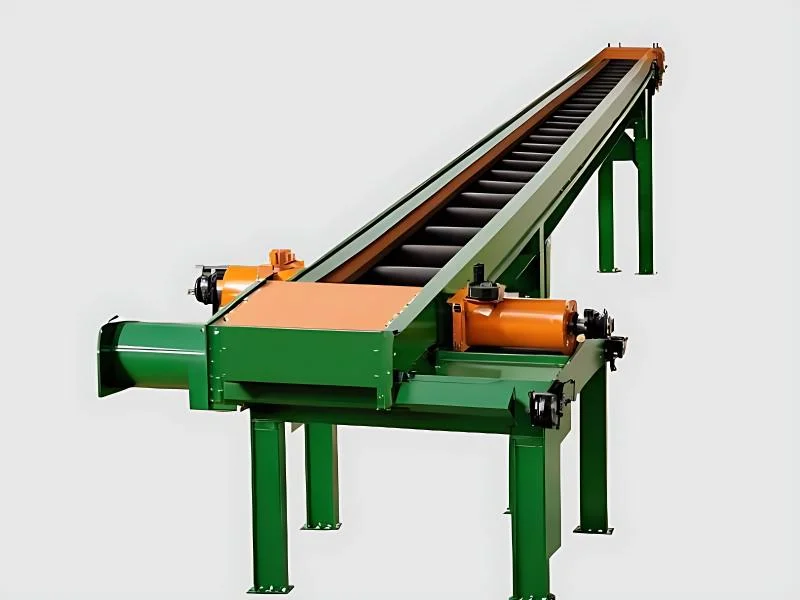
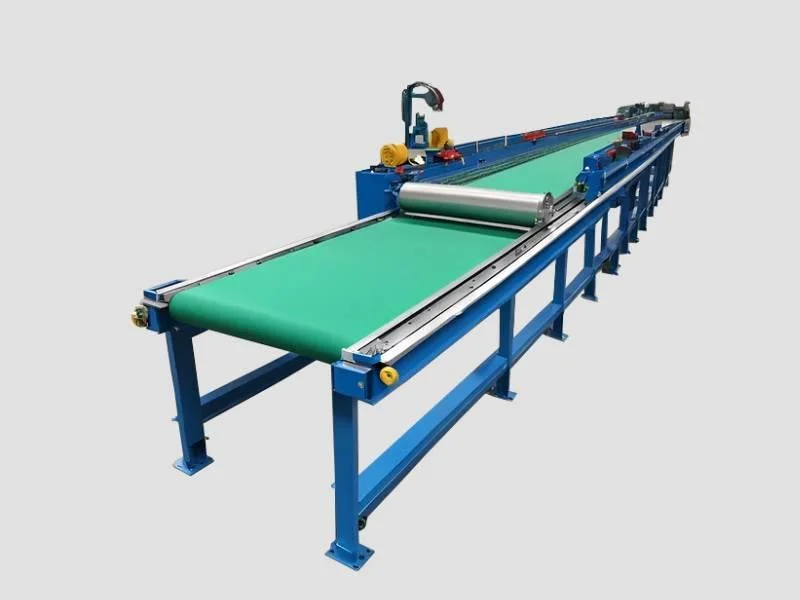
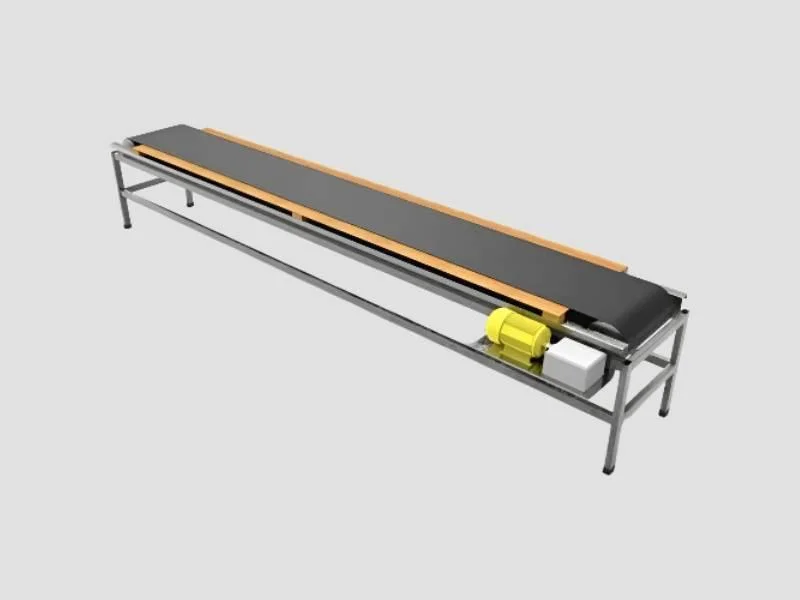
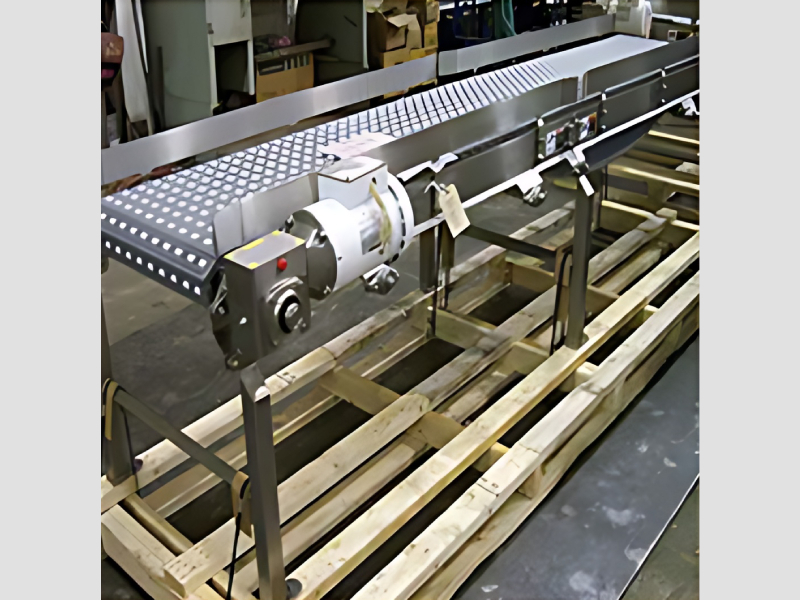
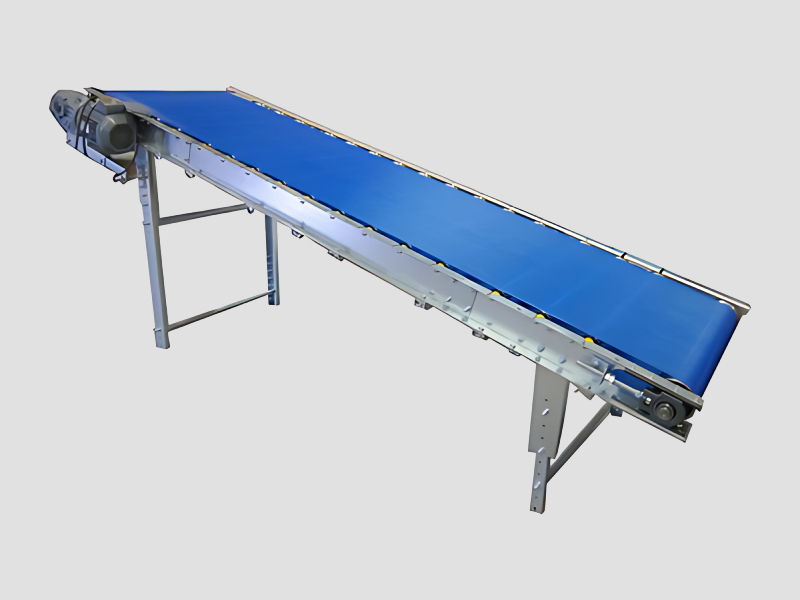
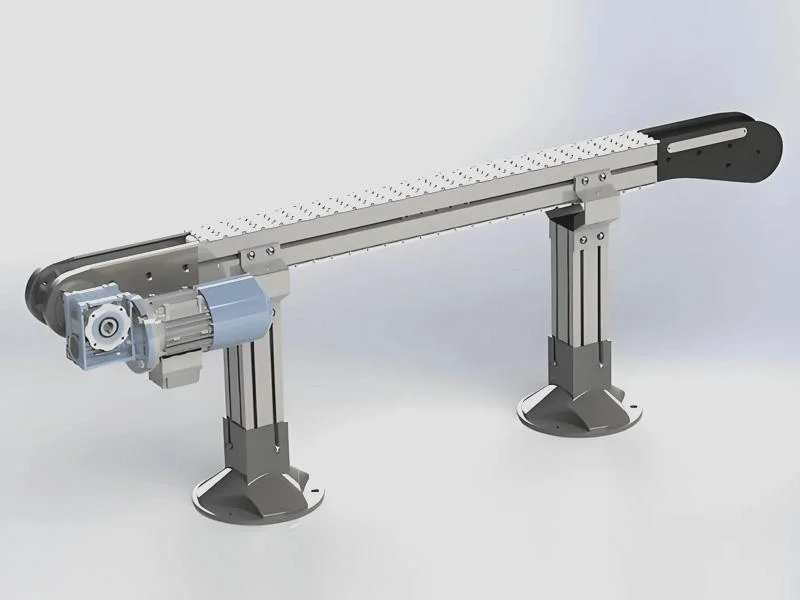
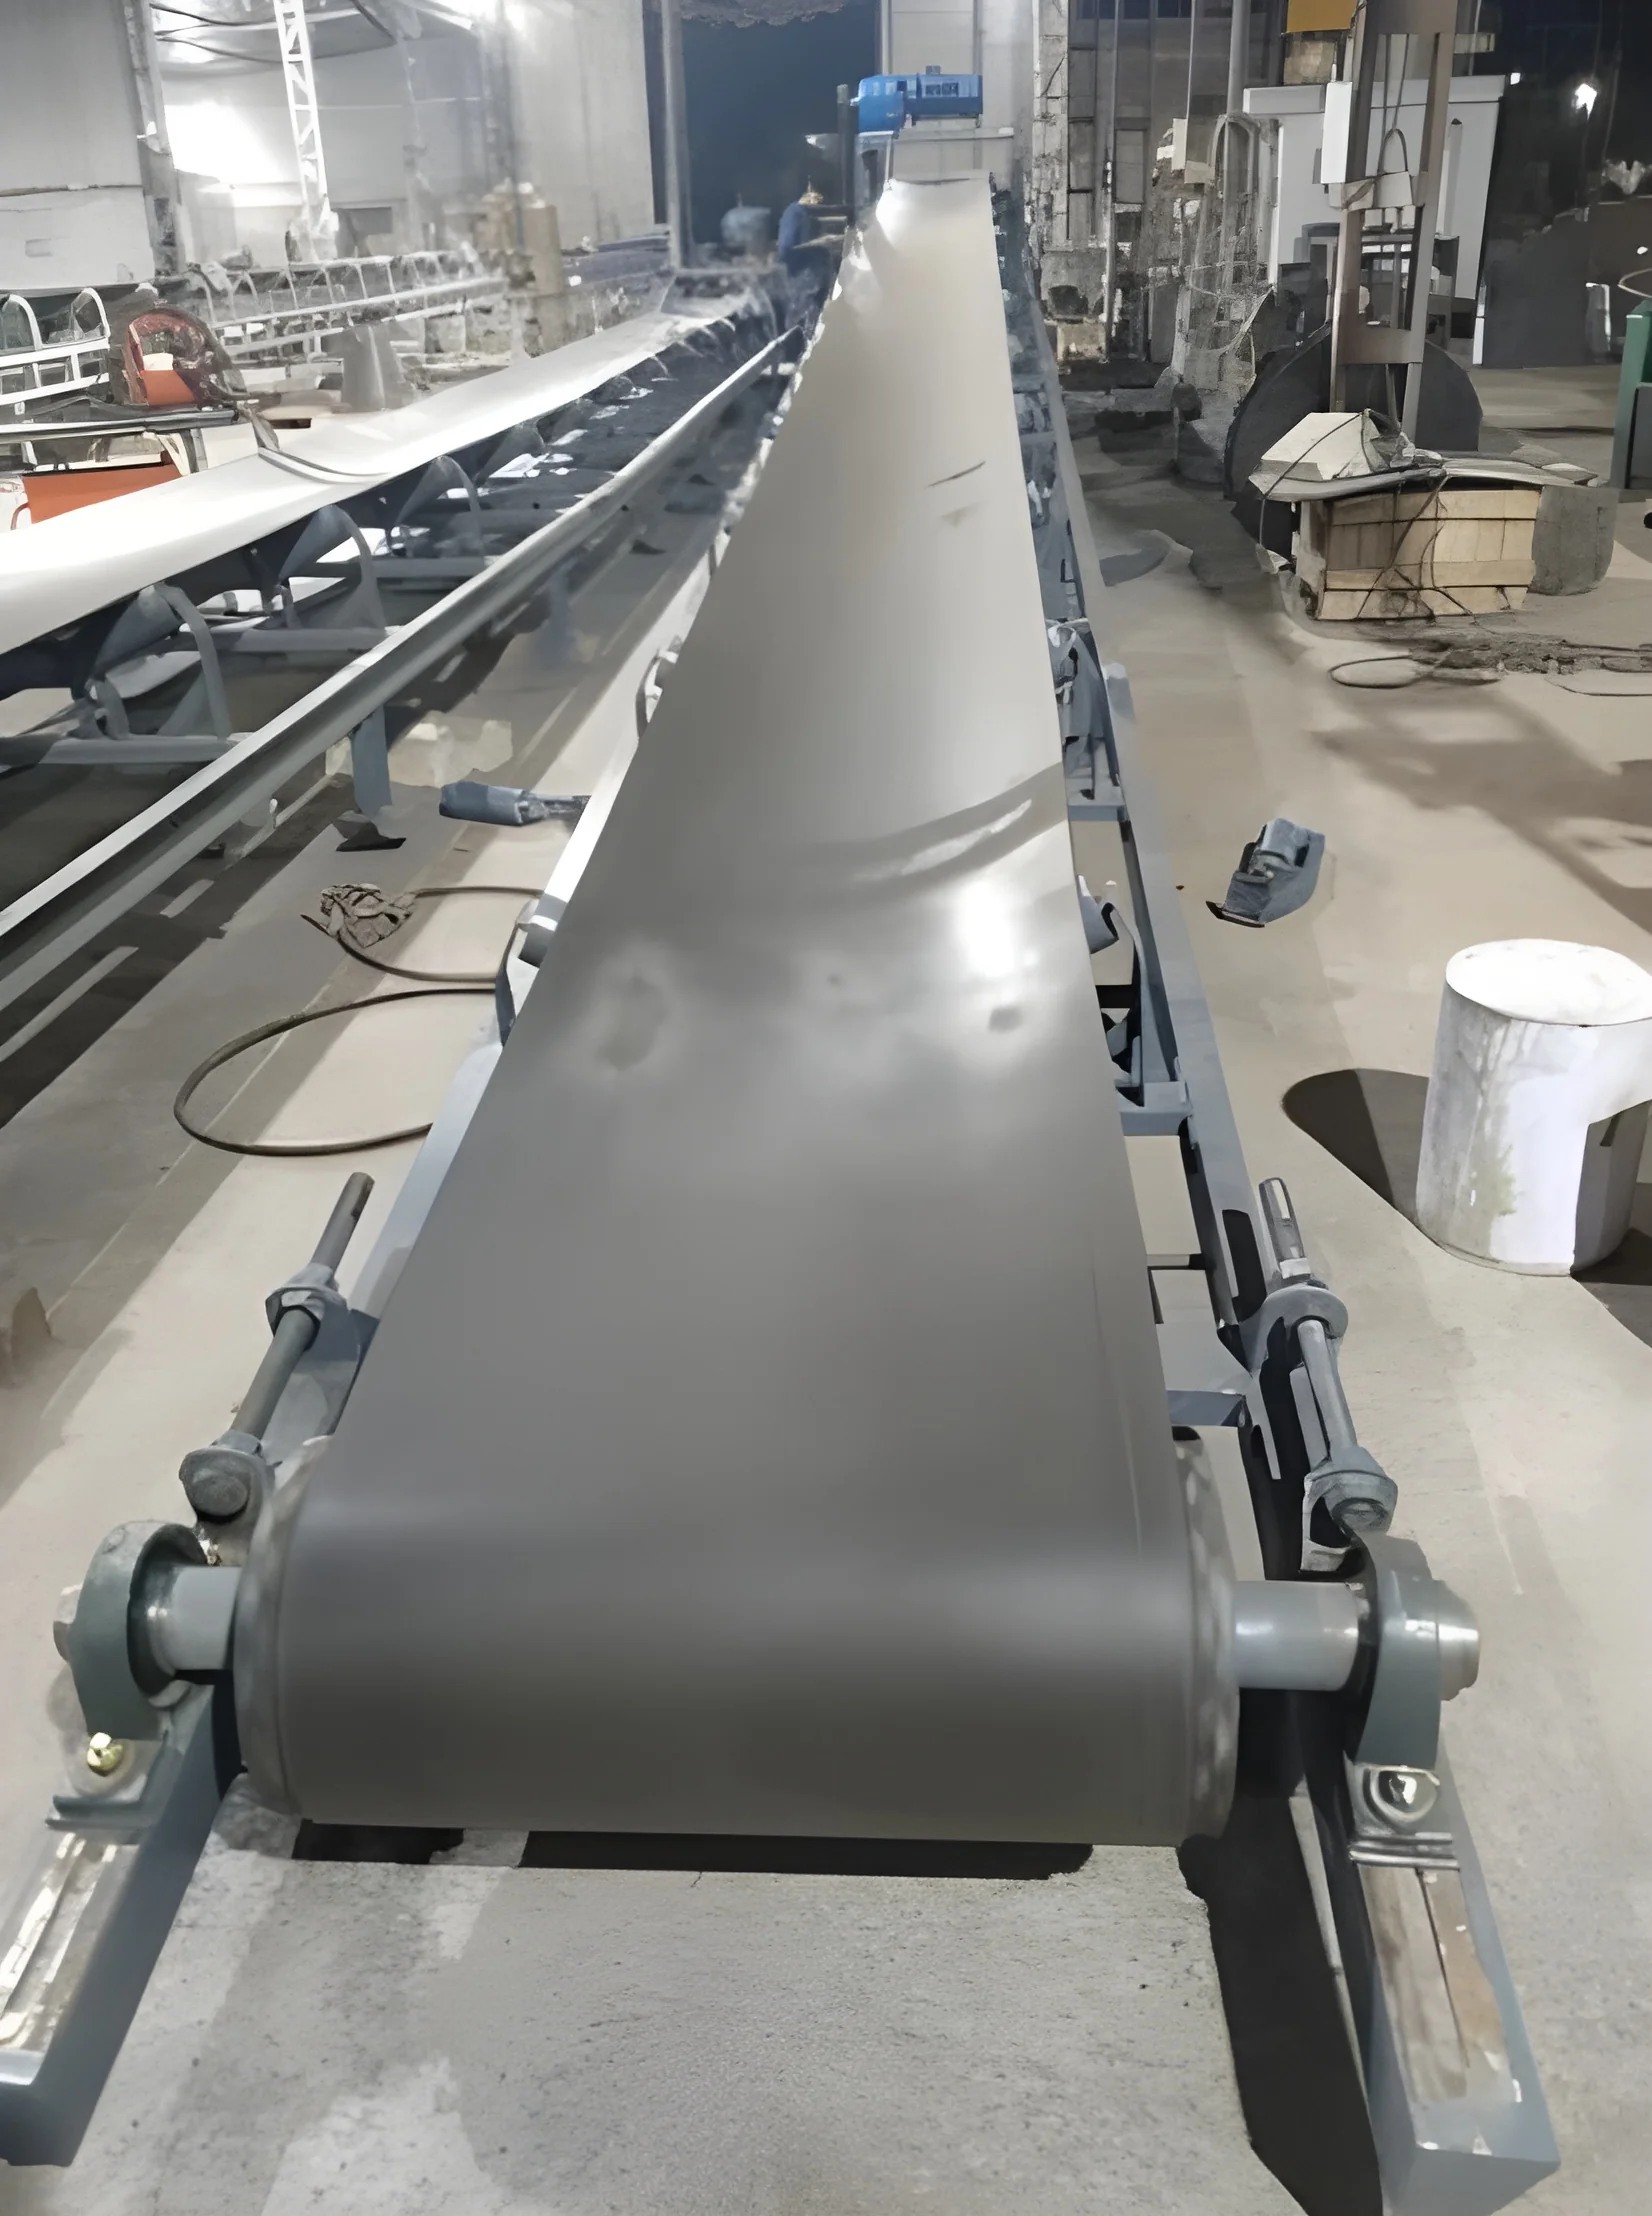
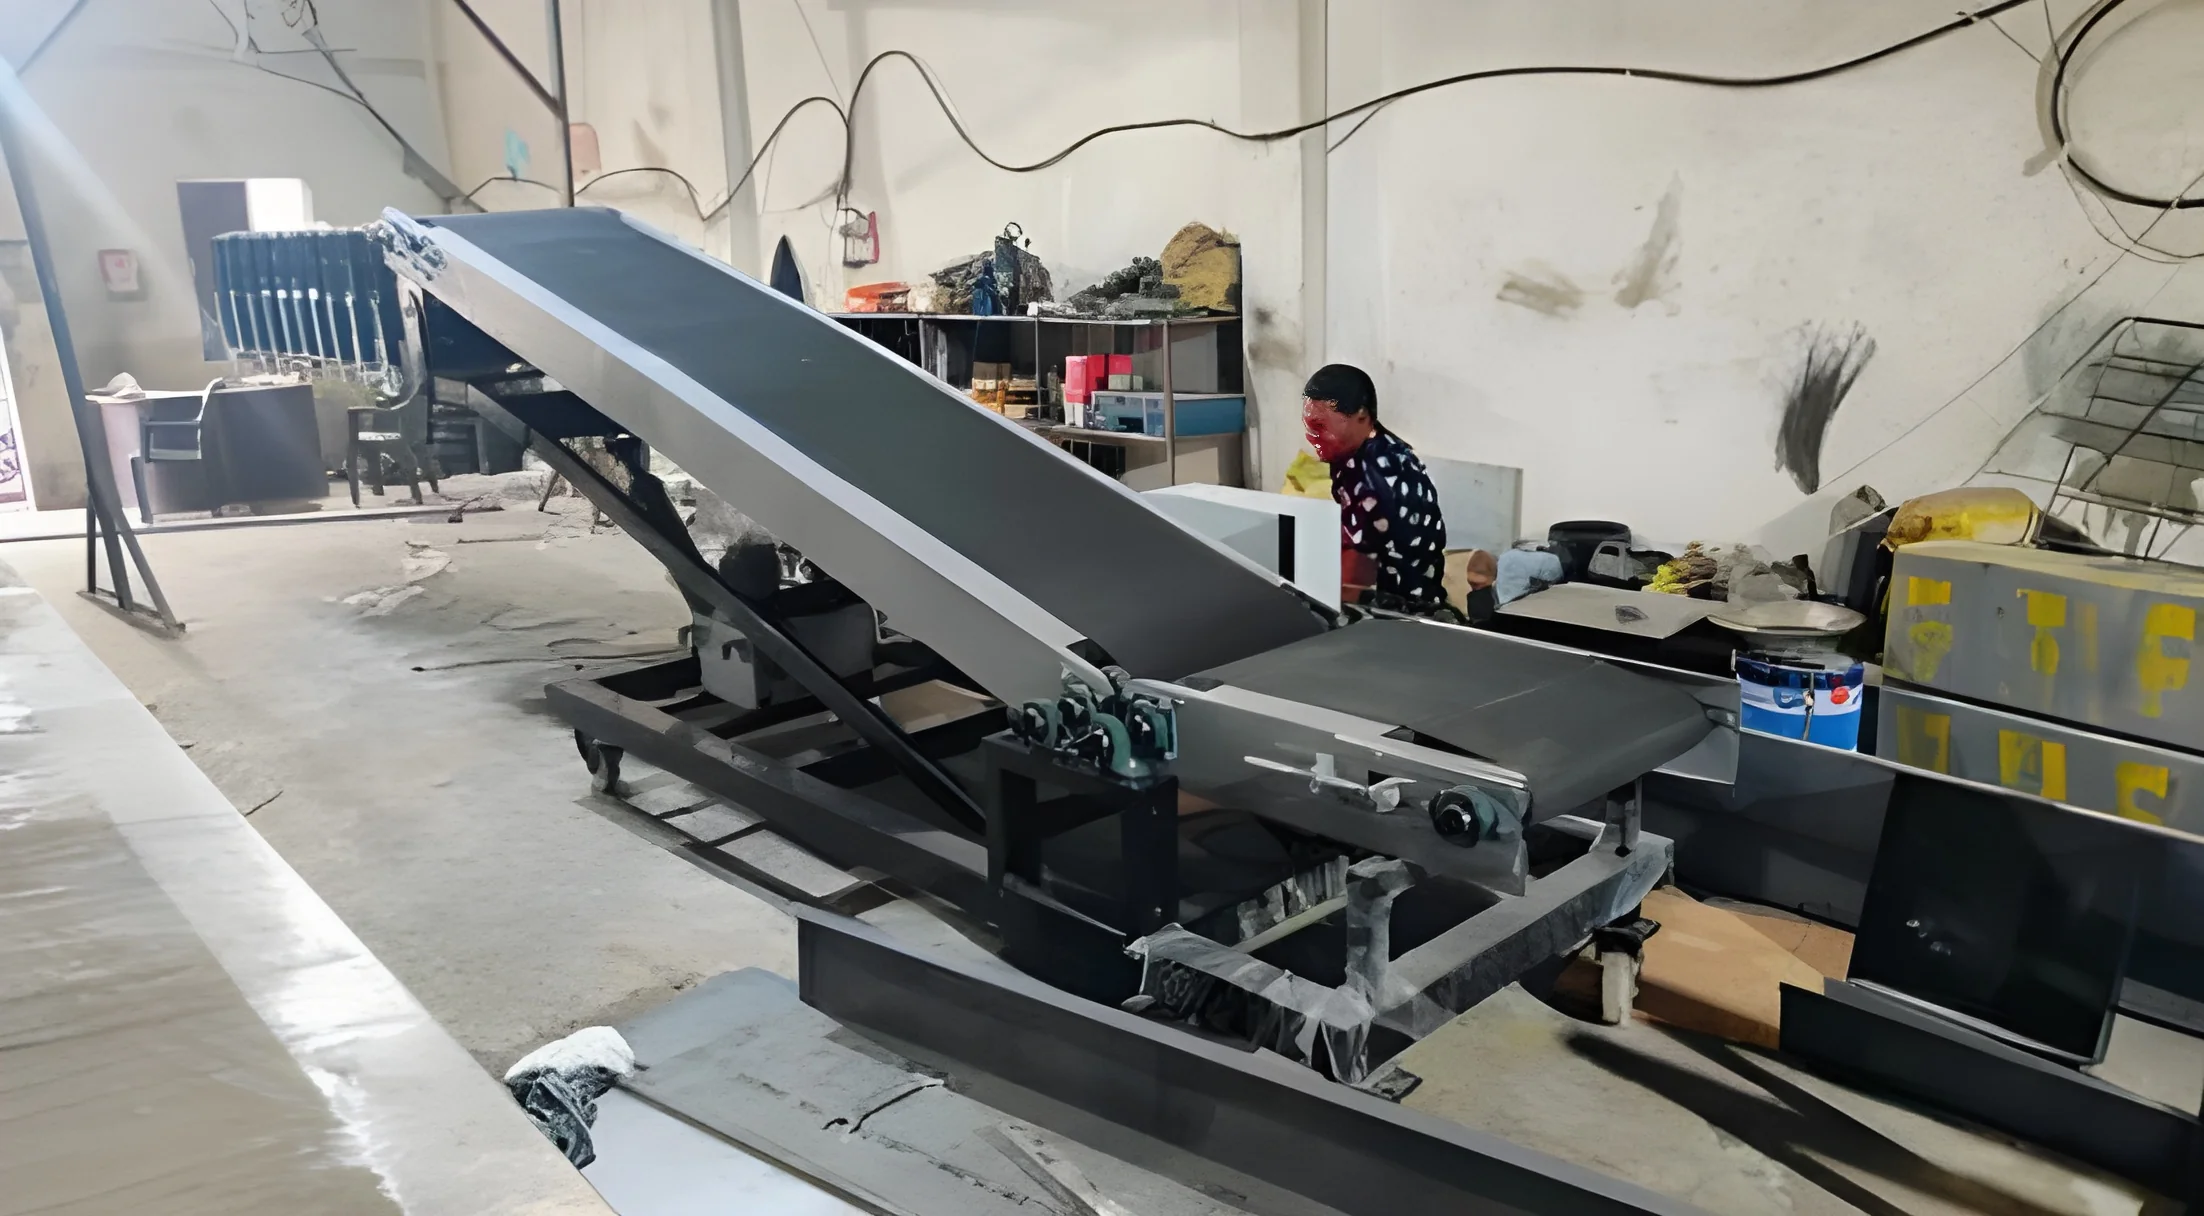
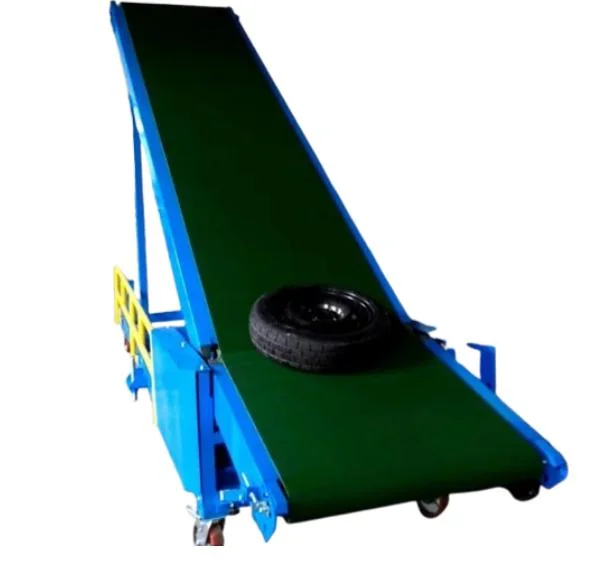
Belt conveyors are designed for transporting bulk materials and finished products. They are versatile and can be used in horizontal or inclined positions, making them suitable for a range of applications.
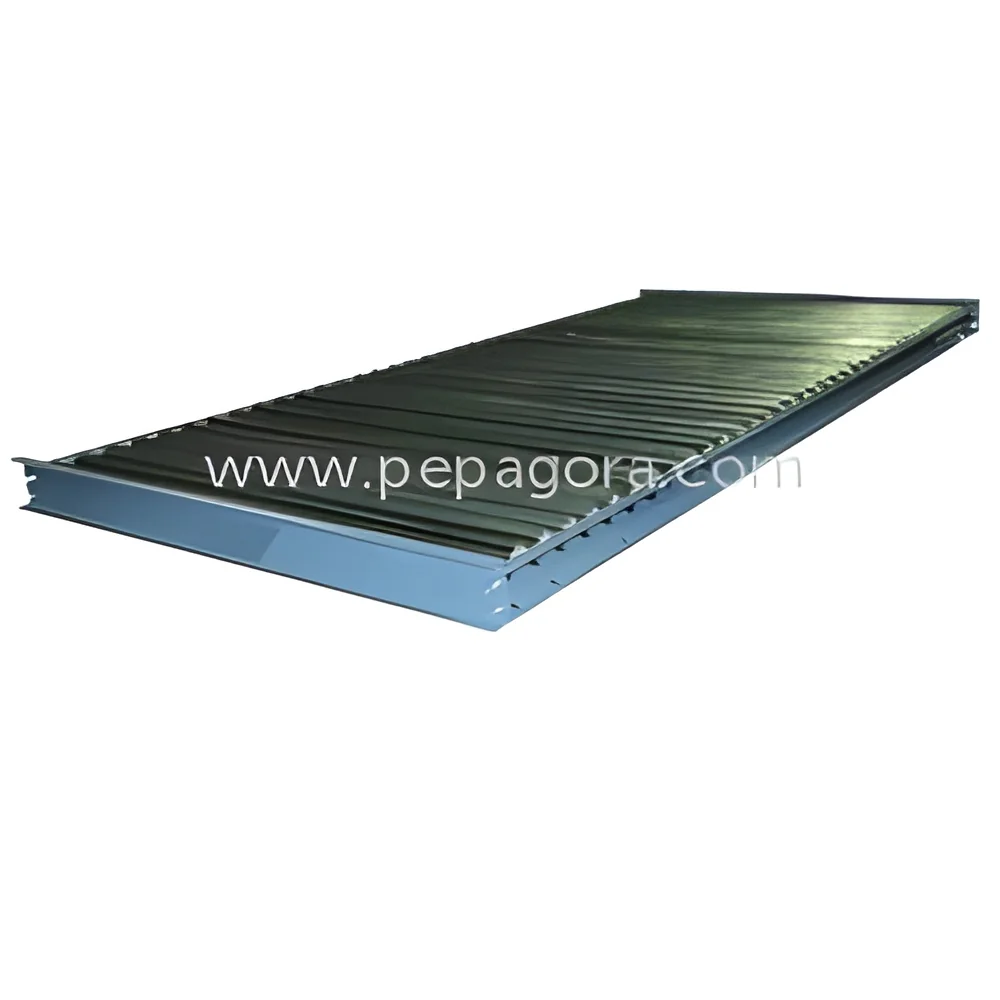
Roller Conveyors
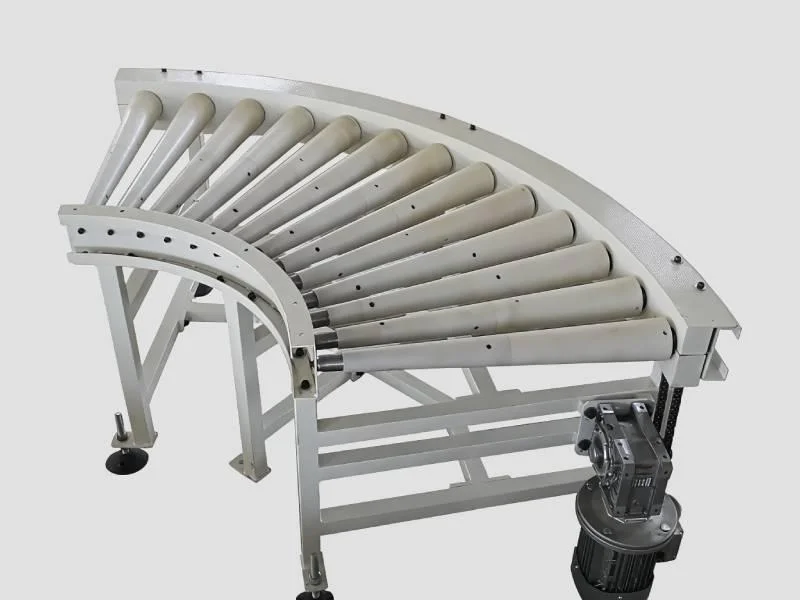
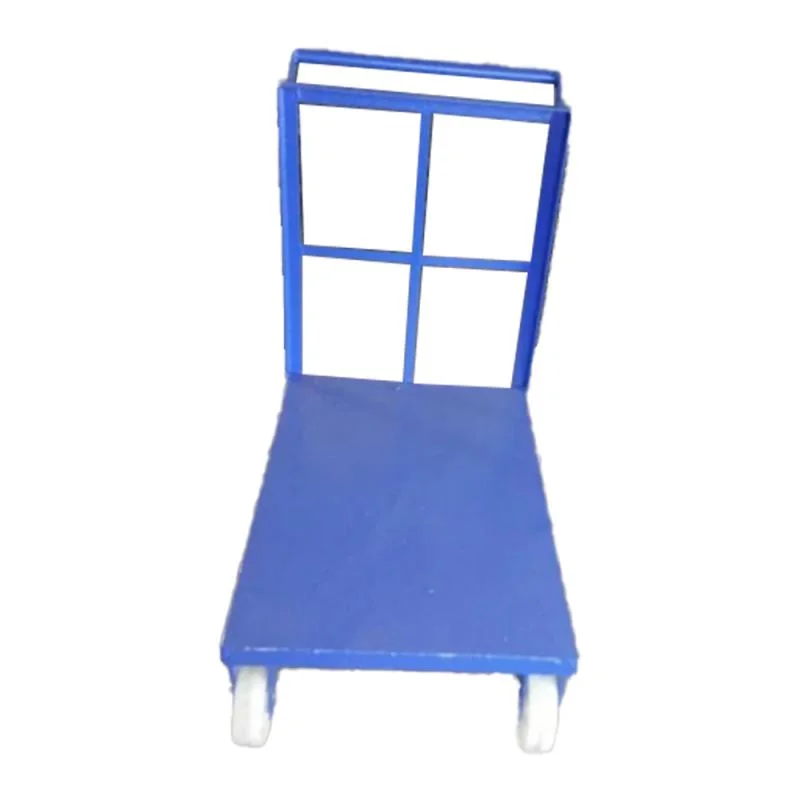
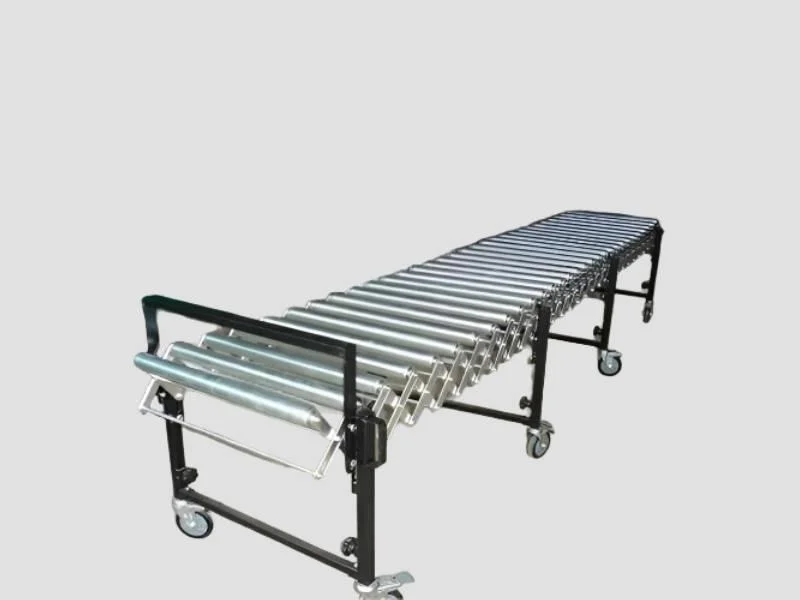
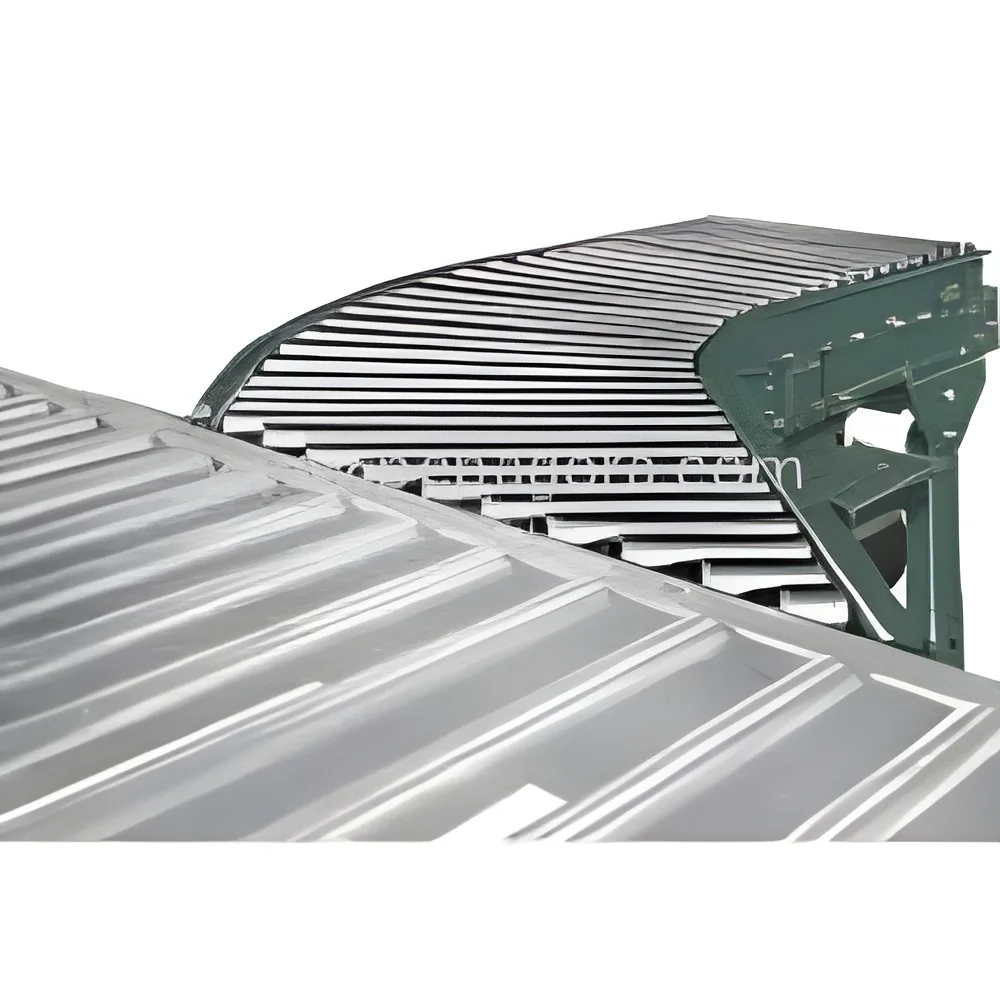
Roller conveyors utilize a series of rollers to move items along a path. They are commonly used for transporting boxes and pallets, offering ease of use and flexibility in layout design.
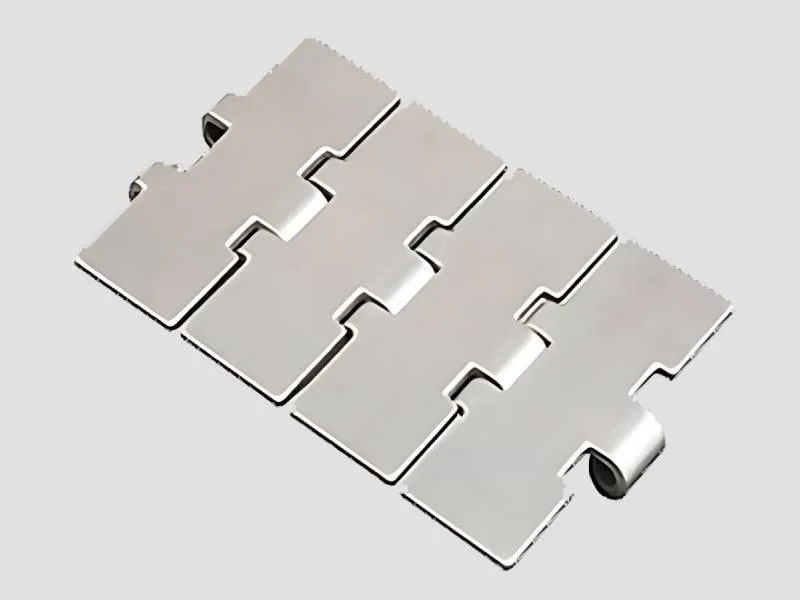
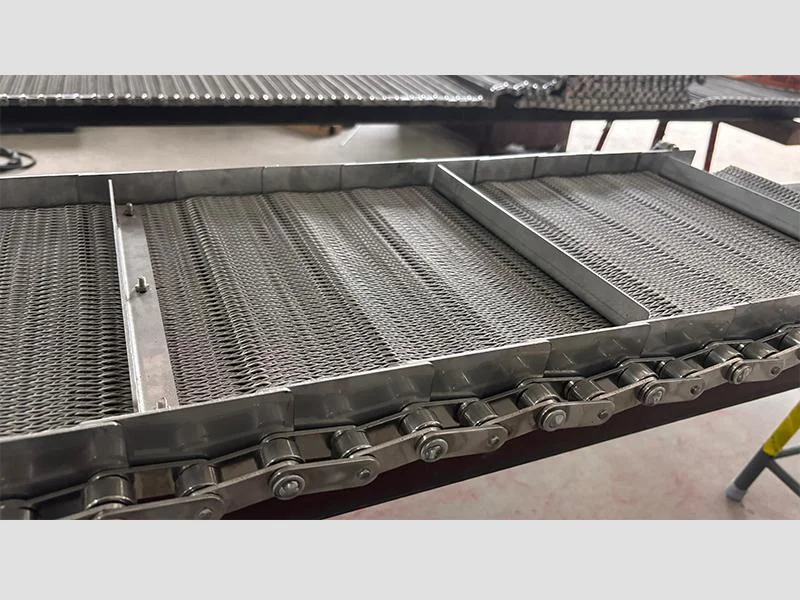
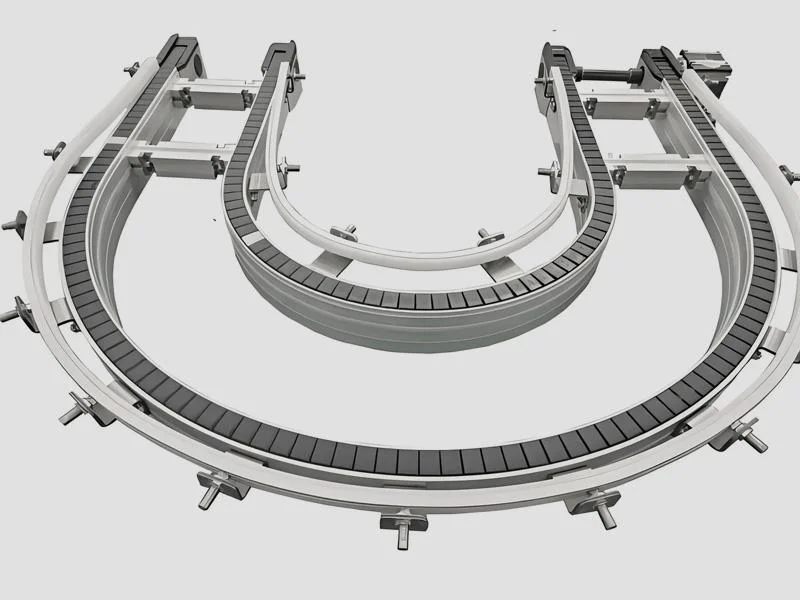
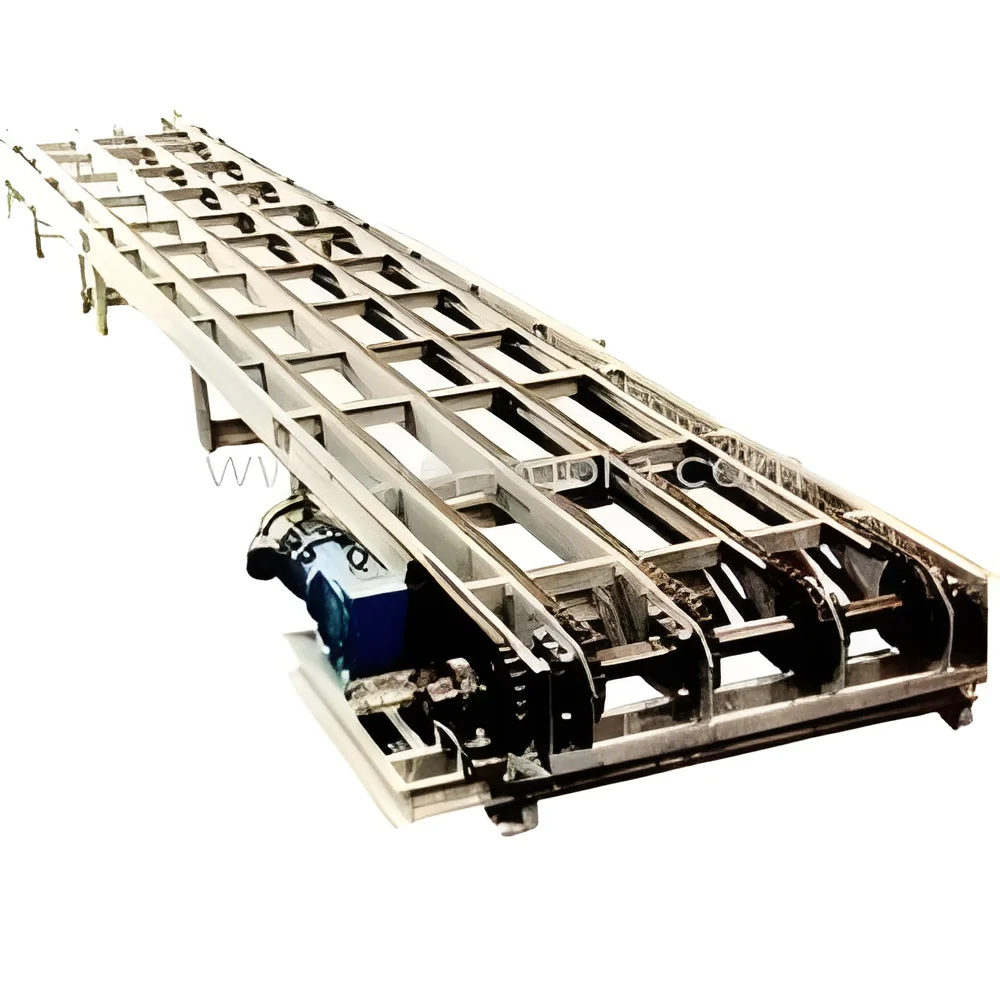
Chain Conveyors
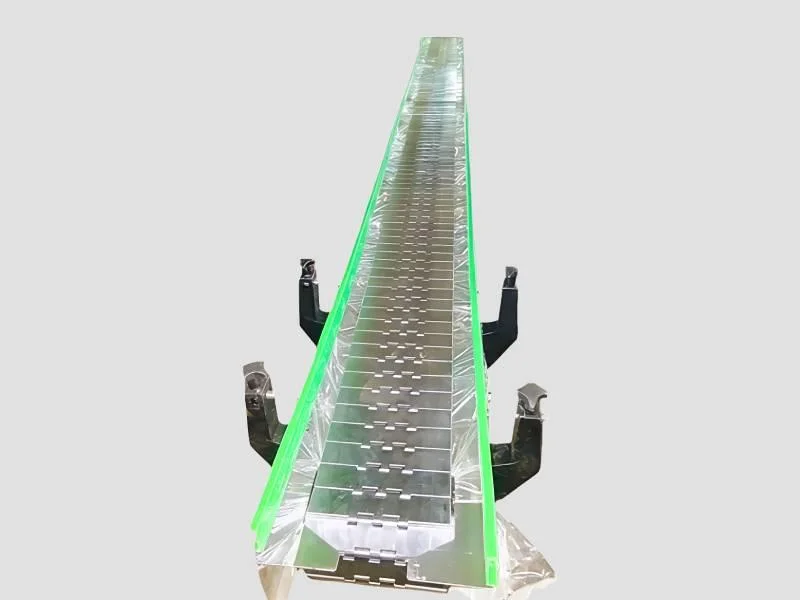
Chain conveyors are suitable for heavy loads and are often used in automotive assembly lines. They provide robust support and can handle high-stress environments.
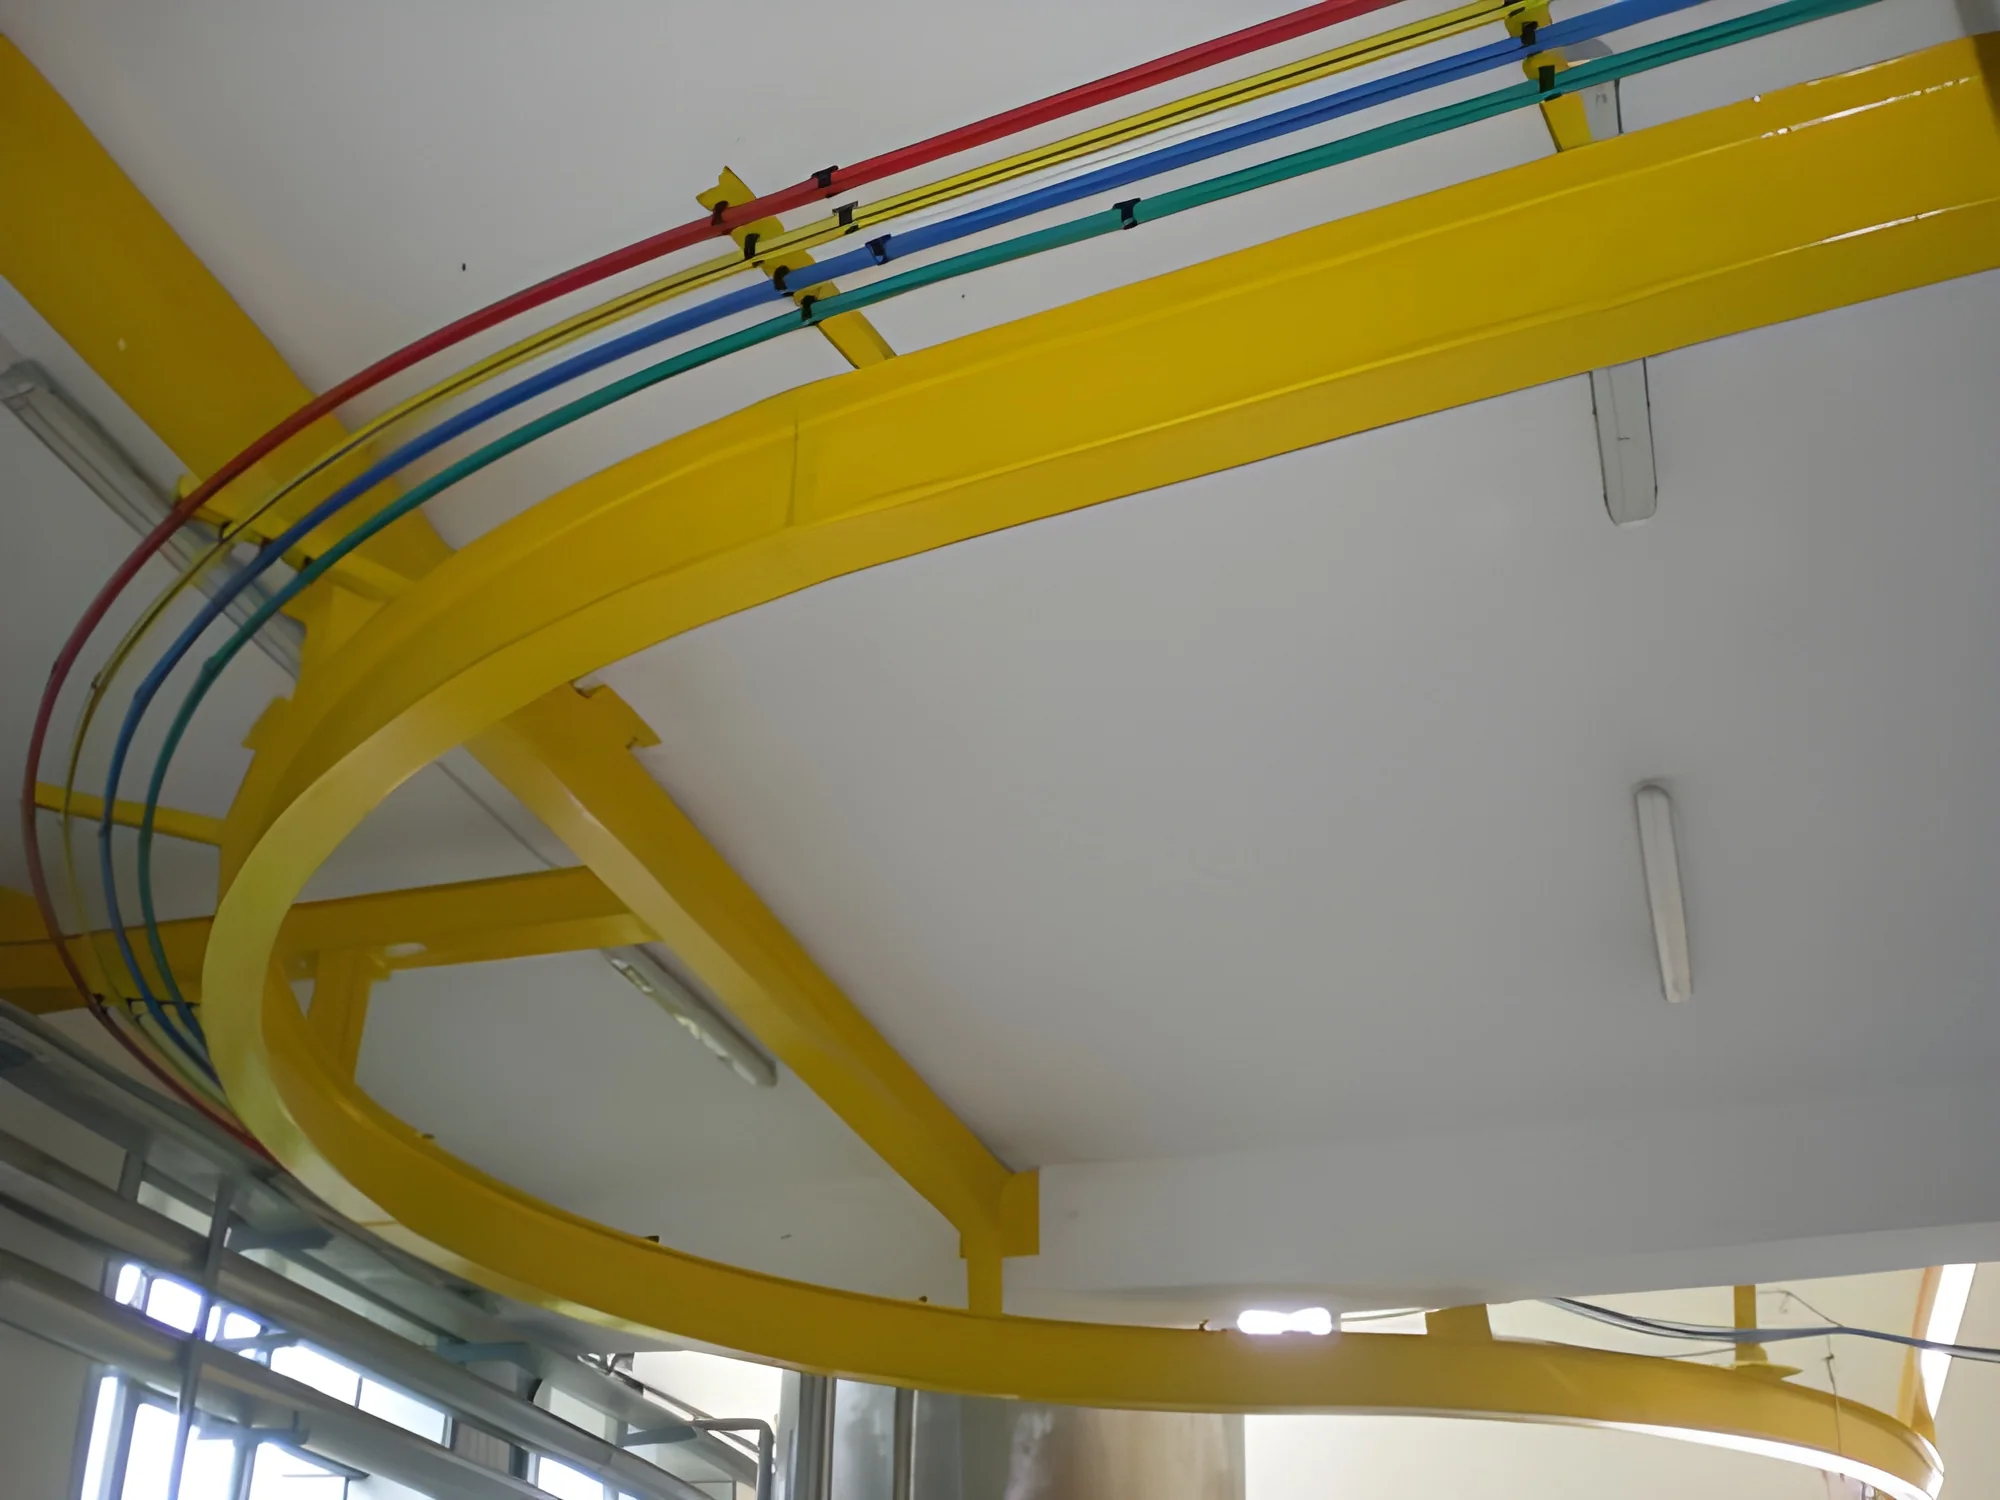
Overhead Conveyors
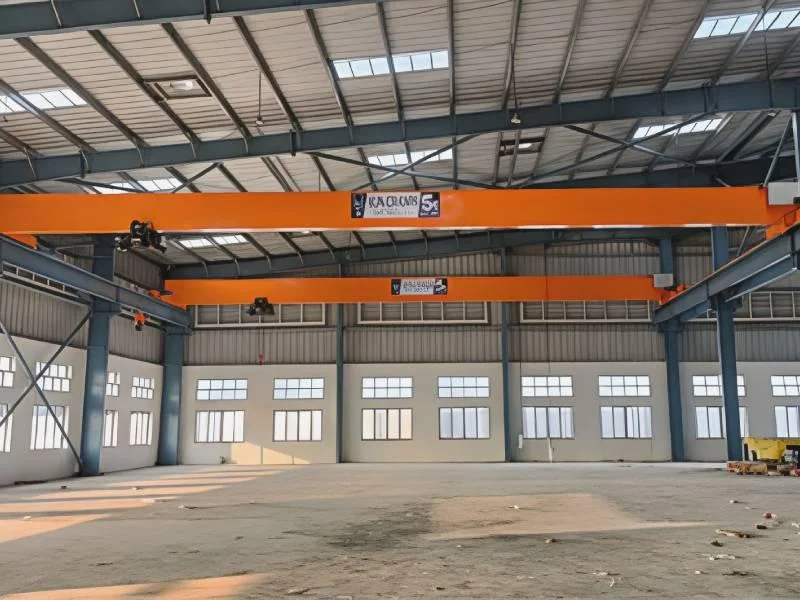
Overhead conveyors are ideal for moving products in tight spaces. They maximize floor space and are commonly used in manufacturing and warehousing.
Modular Conveyors
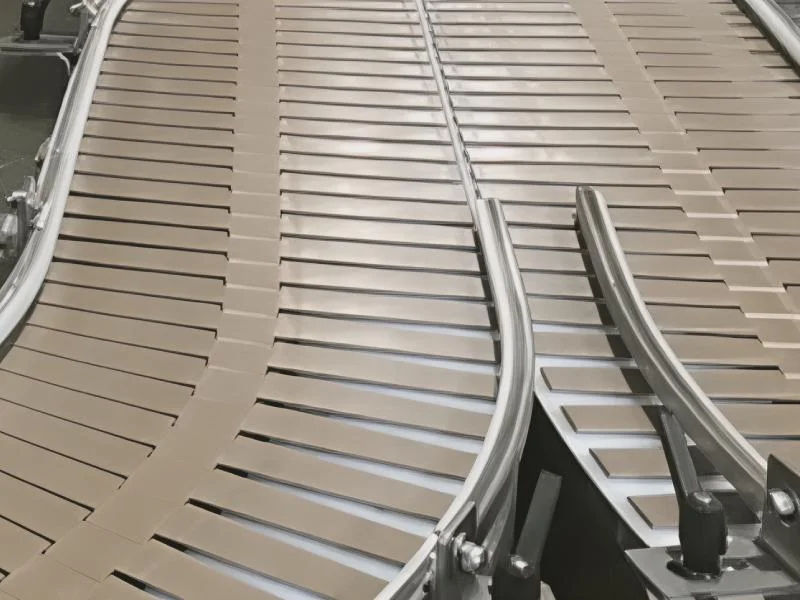
Modular conveyors allow for easy reconfiguration and customization. They are often used in dynamic environments where flexibility is essential.
𝗕𝗲𝗻𝗲𝗳𝗶𝘁𝘀 𝗮𝗻𝗱 𝗔𝗱𝘃𝗮𝗻𝘁𝗮𝗴𝗲𝘀
Investing in conveyors and material handling systems offers numerous advantages.
1. Increased Efficiency: Automating material transport reduces manual labor, allowing employees to focus on higher-value tasks.
2. Improved Safety: By minimizing manual handling, these systems reduce the risk of workplace injuries and enhance operational safety.
3. Cost Savings: Streamlined workflows lead to reduced operational costs, improving overall profitability for businesses.
4. Enhanced Productivity: With faster material movement, production rates increase, leading to shorter lead times and improved customer satisfaction.
5. Flexibility: Various system designs allow for customization to specific operational needs, adapting to changes in production requirements.
6. Quality Control: Automated systems can be integrated with monitoring technologies, ensuring consistent product quality and reducing errors.
𝗕𝘂𝘆𝗶𝗻𝗴 𝗚𝘂𝗶𝗱𝗲 𝗳𝗼𝗿 𝗕𝟮𝗕 𝗕𝘂𝘆𝗲𝗿𝘀
When sourcing conveyors and material handling systems, it is important for buyers to consider several factors to ensure they make informed decisions.
1. Quality Assessment: Evaluate the quality of materials and craftsmanship. Look for systems that meet industry standards and have a proven track record for durability.
2. Supplier Verification: Vet potential suppliers by checking their credentials and customer reviews. A reliable supplier should have experience in your specific industry.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities. Compare quotes from multiple suppliers to ensure competitive pricing.
4. Delivery and Lead Times: Discuss logistics with suppliers to confirm delivery schedules. Consider lead times that align with your operational timelines.
5. Compliance Requirements: Ensure that the systems meet all regulatory standards for safety and performance in your industry. This includes certifications such as CE.
𝗖𝗼𝗺𝗽𝗹𝗶𝗮𝗻𝗰𝗲 𝗮𝗻𝗱 𝗖𝗲𝗿𝘁𝗶𝗳𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀
Compliance with quality standards and certifications is crucial for conveyors and material handling systems. These systems should adhere to ISO 9001 standards, ensuring consistent quality management practices.
Industry certifications, such as CE, demonstrate that equipment meets European safety and environmental requirements. This certification is essential for companies looking to operate in global markets.
Safety and testing requirements are also critical. Systems should undergo rigorous testing to verify their performance and ensure they can safely handle specified loads.
Additionally, regional compliance considerations may vary based on local regulations. It is important for businesses to be aware of these differences when sourcing equipment.
𝗪𝗵𝘆 𝗦𝗼𝘂𝗿𝗰𝗲 𝗖𝗼𝗻𝘃𝗲𝘆𝗼𝗿𝘀 & 𝗠𝗮𝘁𝗲𝗿𝗶𝗮𝗹 𝗛𝗮𝗻𝗱𝗹𝗶𝗻𝗴 𝗦𝘆𝘀𝘁𝗲𝗺𝘀 𝗳𝗿𝗼𝗺 𝗣𝗲𝗽𝗮𝗴𝗼𝗿𝗮?
Pepagora provides a trusted platform for sourcing conveyors and material handling systems, offering several key advantages for B2B buyers.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, ensuring that each vendor meets stringent quality and reliability standards. This verification process helps mitigate risks associated with sourcing equipment.
Streamlined RFQ Process: The platform features a simplified request for quotation (RFQ) process. Buyers can easily request quotes from multiple suppliers, facilitating comparison and enabling informed decision-making.
Trade Assurance and Support: Pepagora offers trade assurance to protect buyers throughout the purchasing process. This includes support for negotiations and dispute resolution, providing peace of mind with every transaction.
Regional Coverage: With a presence in India, the GCC, and Southeast Asia, Pepagora offers extensive geographic reach. This allows businesses to source locally while benefiting from a broad selection of suppliers and products.

 India
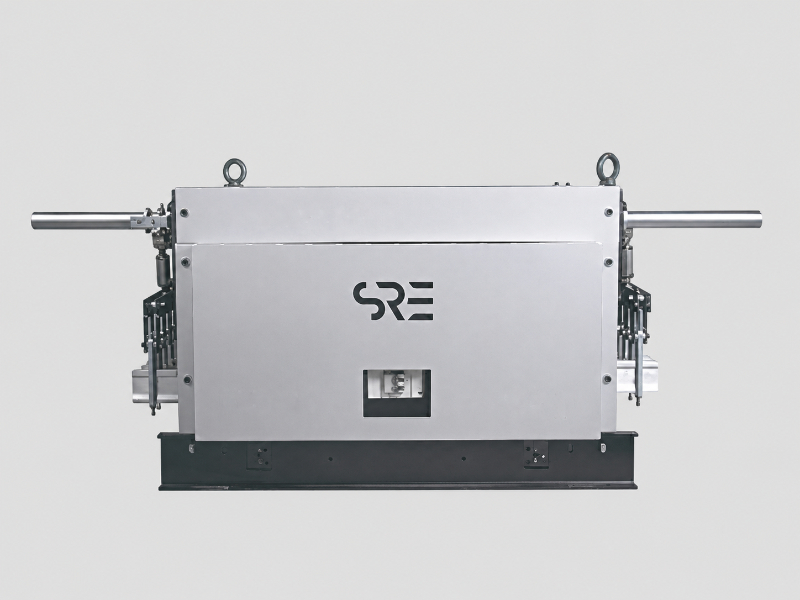
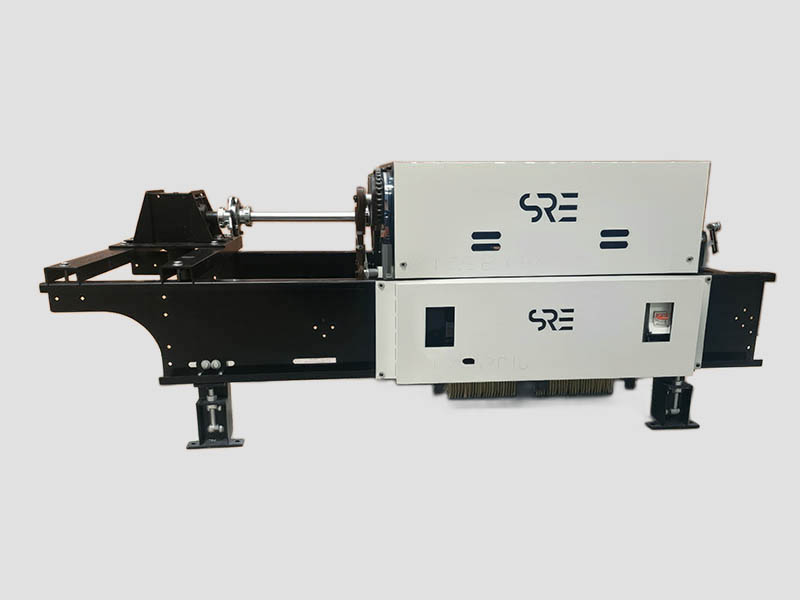
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
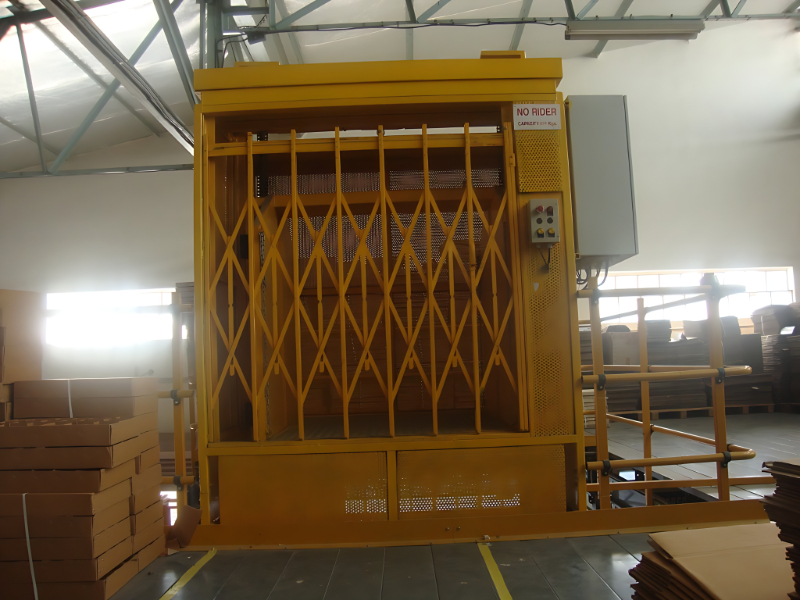
 India
 India

 India

 India
 India
 India
 India
 India


 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
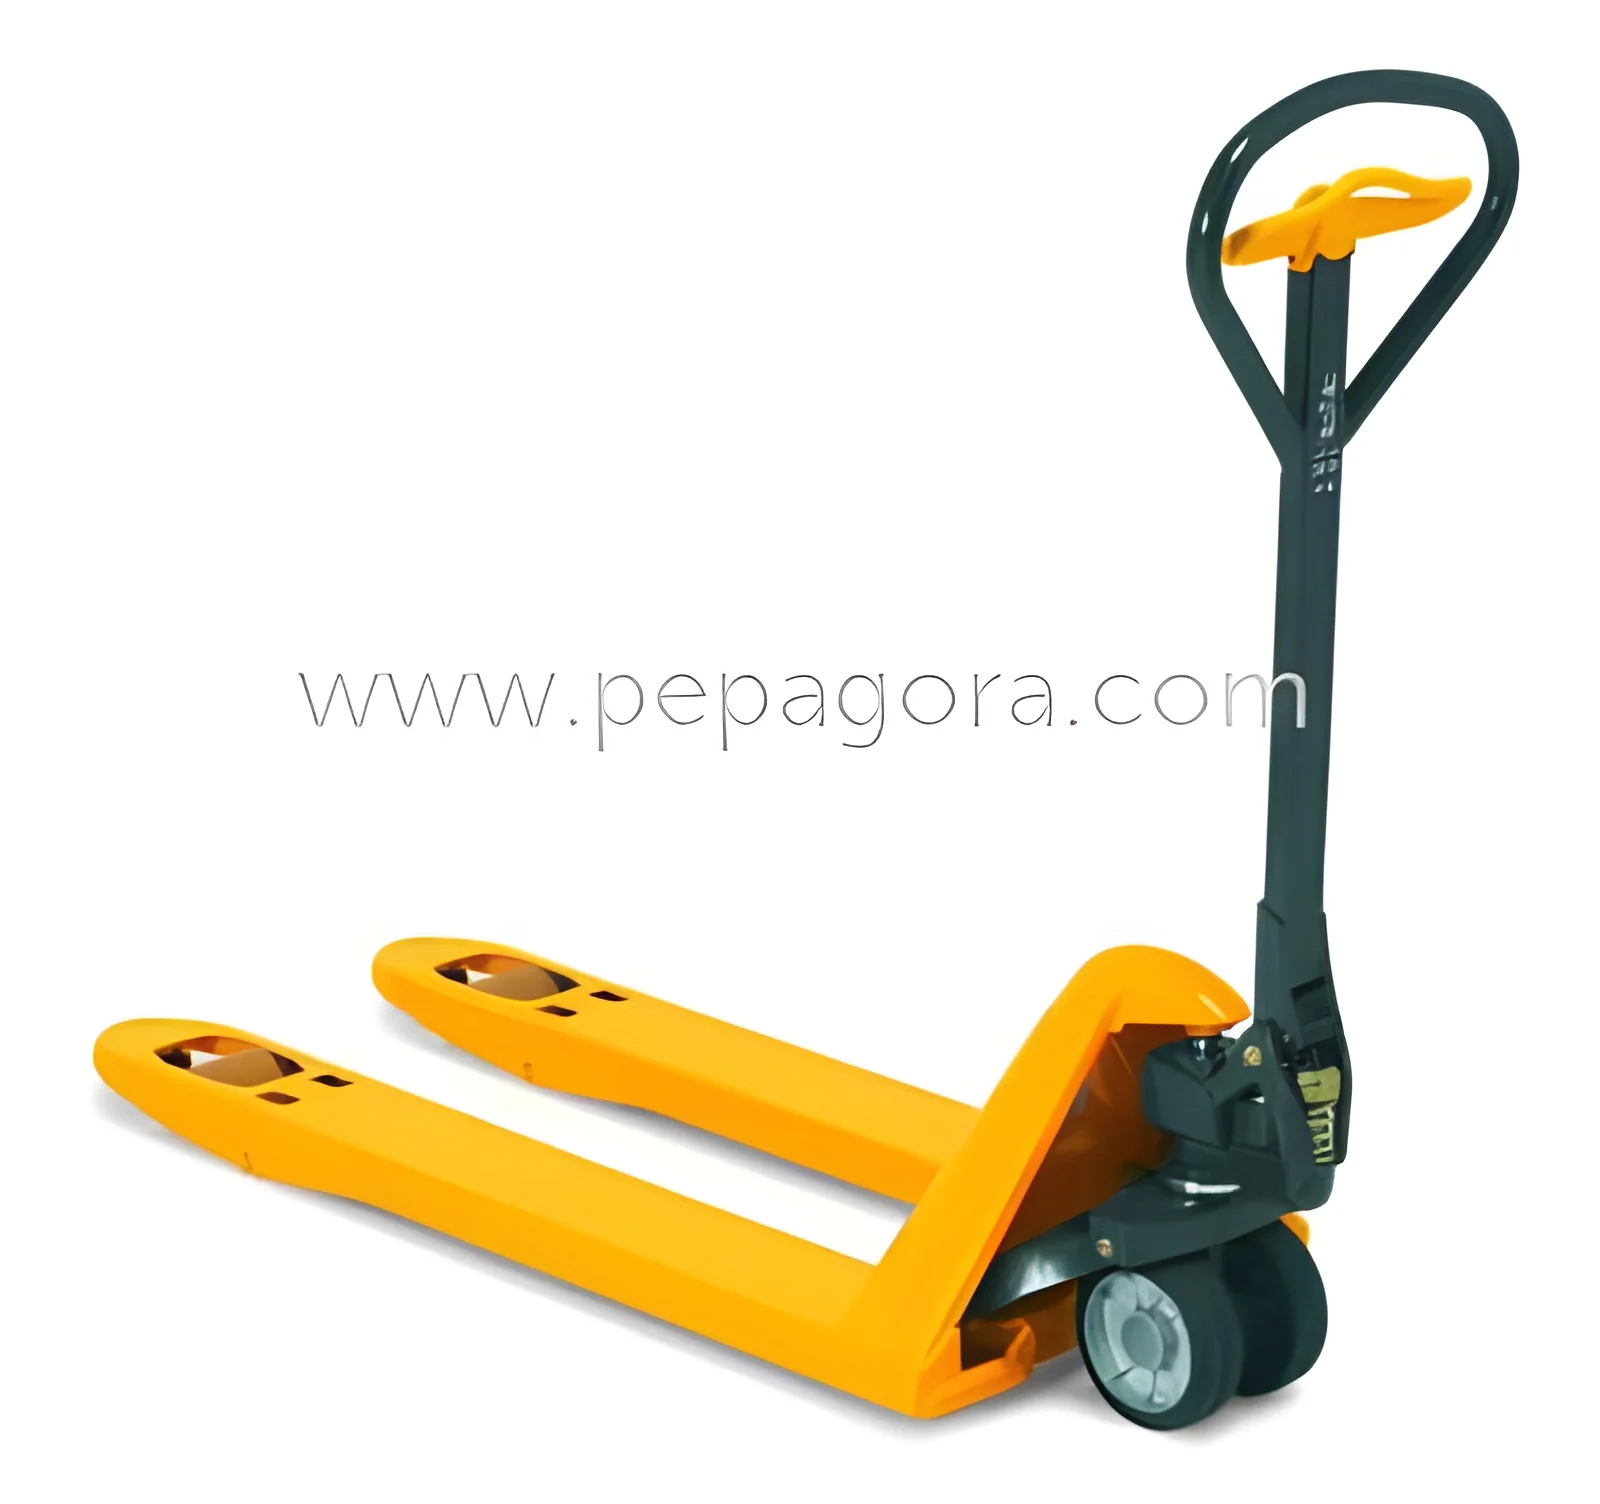 India
 India
 India

 India
 India
 India
Frequently Asked Questions
What are Conveyors & Material Handling Systems?
Conveyors & Material Handling Systems are automated solutions designed to transport materials and products within a facility. These systems enhance efficiency by streamlining the movement of goods, reducing manual labor, and minimizing the risk of injury.
What are the different types of Conveyors & Material Handling Systems?
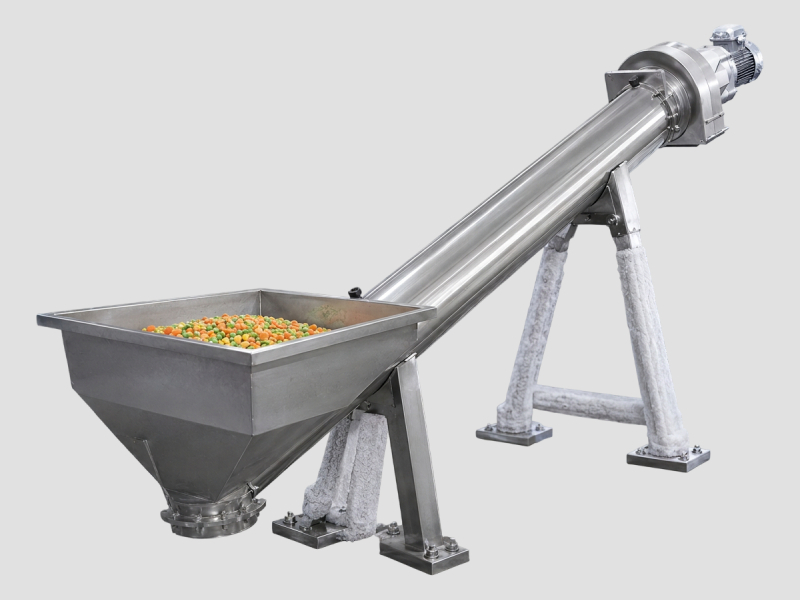
There are several types of Conveyors & Material Handling Systems, including belt conveyors, roller conveyors, chain conveyors, and screw conveyors. Each type is suited for specific applications and materials, offering different capabilities in terms of speed, load capacity, and layout.
How do I choose the right Conveyors & Material Handling Systems?
Choosing the right system involves assessing your specific needs, including the type of materials being handled, the layout of your facility, and the desired speed of transport. It is also important to consider factors such as load capacity and maintenance requirements.
What are the standard specifications for Conveyors & Material Handling Systems?
Standard specifications for Conveyors & Material Handling Systems typically include load capacity, speed, belt width, and overall dimensions. Additional specifications may also include motor power ratings, material construction, and safety features.
What is the price range for Conveyors & Material Handling Systems?
The price range for Conveyors & Material Handling Systems can vary widely based on type, specifications, and customization. Generally, prices can start from a few thousand rupees for basic models and can exceed several lakhs for more complex systems.
What quality standards apply to Conveyors & Material Handling Systems?
Quality standards for Conveyors & Material Handling Systems include compliance with ISO and ANSI guidelines, which ensure safety, reliability, and efficiency. Manufacturers may also adhere to industry-specific standards depending on the application.
Where can I find Conveyors & Material Handling Systems suppliers in India?
You can find Conveyors & Material Handling Systems suppliers in India through online B2B marketplaces like Pepagora, industry trade shows, and local manufacturing directories. Researching suppliers' credentials and customer reviews can also help in making an informed decision.
Can Conveyors & Material Handling Systems be customized?
Yes, Conveyors & Material Handling Systems can often be customized to meet specific operational needs. Customization may include adjustments in size, material, speed, and additional features to enhance functionality.
What is the typical minimum order quantity for Conveyors & Material Handling Systems?
The typical minimum order quantity (MOQ) for Conveyors & Material Handling Systems can vary by supplier and product type. It is common for manufacturers to set MOQs based on the complexity and cost of the systems.
What is the typical lead time for Conveyors & Material Handling Systems?
The typical lead time for Conveyors & Material Handling Systems can range from a few weeks to several months, depending on the complexity of the order and the manufacturer's production schedule. Custom orders may require longer lead times.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally
Source Smarter,Grow Faster