
 IN
Belt Conveyors (Flat, Inclined)
413 products available
Key Features and Specifications
Belt conveyors offer a variety of features that enhance their functionality and efficiency. Understanding these specifications is crucial for selecting the right type for specific needs.
Key specifications include:
1. Conveyor Width
- Common widths range from 18 inches to 60 inches.
- Wider belts are suitable for bulk materials, while narrower ones are used for smaller items.
2. Load Capacity
- Load capacities can range from 50 lbs to several tons per hour.
- Selection depends on the materials being conveyed and the operating environment.
3. Belt Material
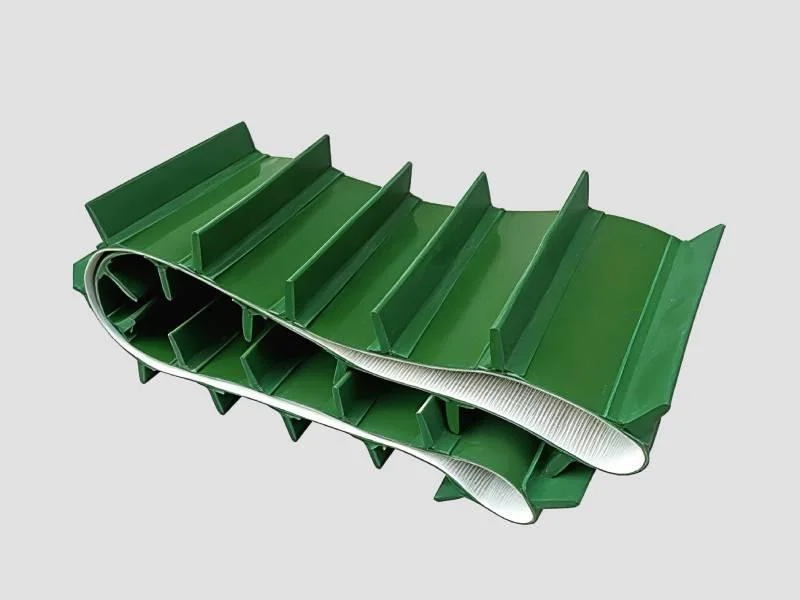
- Options include rubber, PVC, and fabric.
- Material choice affects durability and suitability for different applications.
4. Belt Speed
- Typical speeds range from 50 feet per minute to 500 feet per minute.
- Speed can be adjusted based on the material flow requirements.
5. Incline Angle
- Standard incline angles are typically between 15 and 30 degrees.
- Steeper angles require specialized designs to prevent material slippage.
6. Drive Type
- Options include electric, hydraulic, or pneumatic drives.
- The drive type influences maintenance needs and operational efficiency.
7. Length
- Conveyors can range from a few feet to hundreds of feet in length.
- Length selection is based on the specific layout of the facility.
8. Safety Features
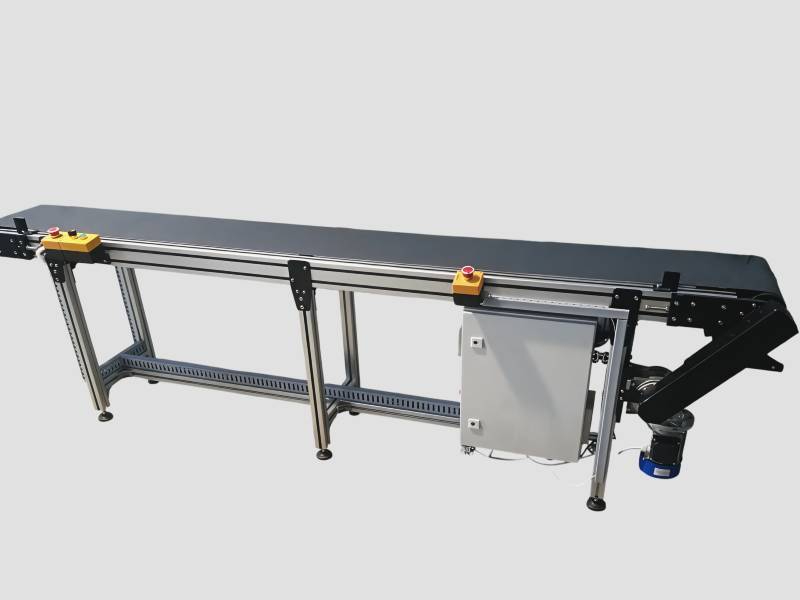
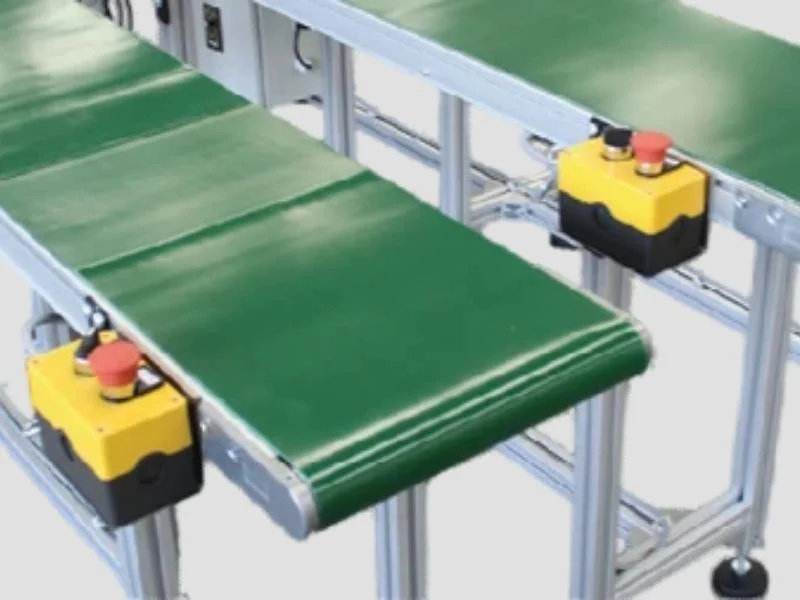
- Common safety features include emergency stop buttons and guard rails.
- These features help ensure safe operation in busy environments.
In summary, choosing the right belt conveyor involves understanding these specifications in relation to the specific application demands.
Common Applications and Use Cases
Belt conveyors are widely used across various industries for efficient material handling.
1. Mining: In mining operations, belt conveyors transport minerals and ores from extraction sites to processing plants. They enhance productivity and reduce manual labor in challenging environments.
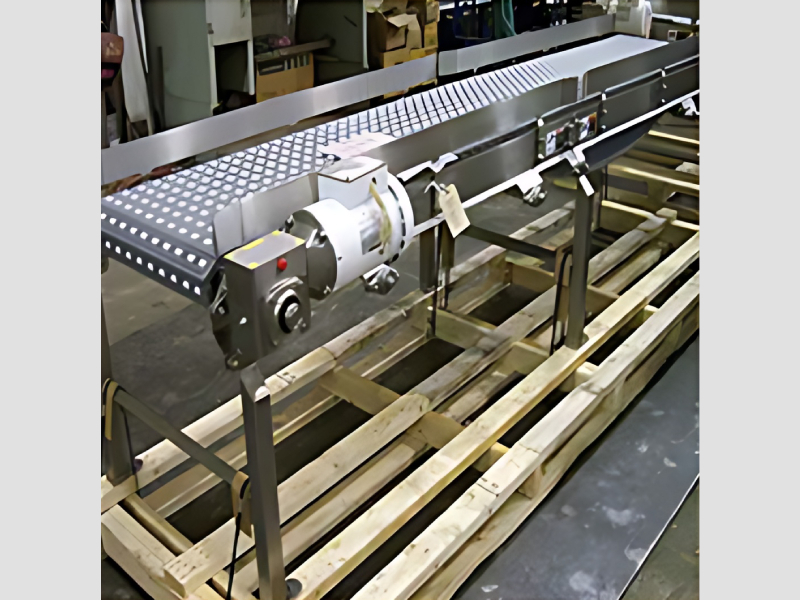
2. Food Processing: In the food industry, belt conveyors are used for transporting packaged goods or raw ingredients. They are designed to meet hygiene standards and can withstand cleaning processes.
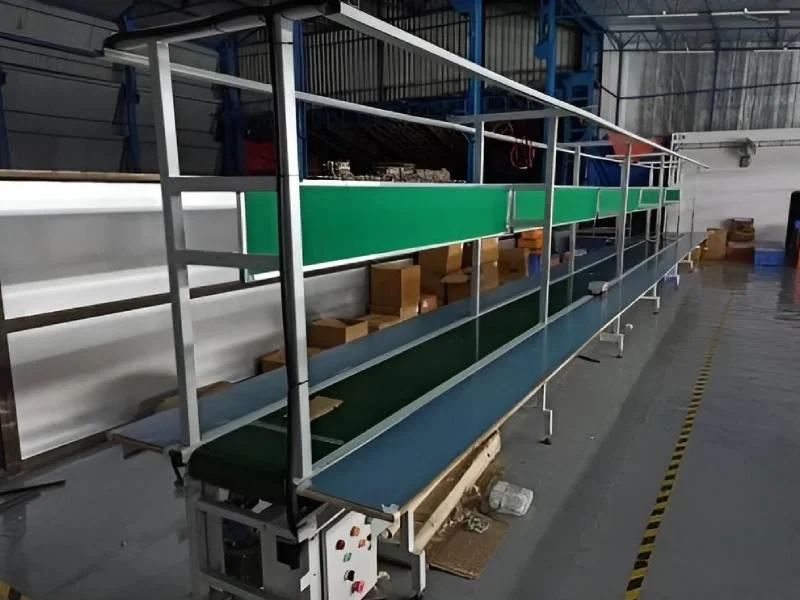
3. Manufacturing: In manufacturing facilities, belt conveyors facilitate the movement of components along assembly lines, ensuring a smooth workflow and reducing bottlenecks.
4. Warehousing: In warehouse operations, belt conveyors help automate the sorting and distribution of products, improving order fulfillment times and efficiency.
5. Construction: For construction projects, these conveyors move heavy materials like sand, gravel, and concrete. They are essential for managing site logistics.
6. Recycling: In recycling plants, belt conveyors transport sorted materials through various processing stages, aiding in efficient waste management.
7. Agriculture: In agricultural settings, belt conveyors are used for moving grains, seeds, and fertilizers, streamlining the handling process.
Product Variants and Subcategories
Belt conveyors come in various types to cater to specific operational needs. Each variant has unique features suited for different applications.
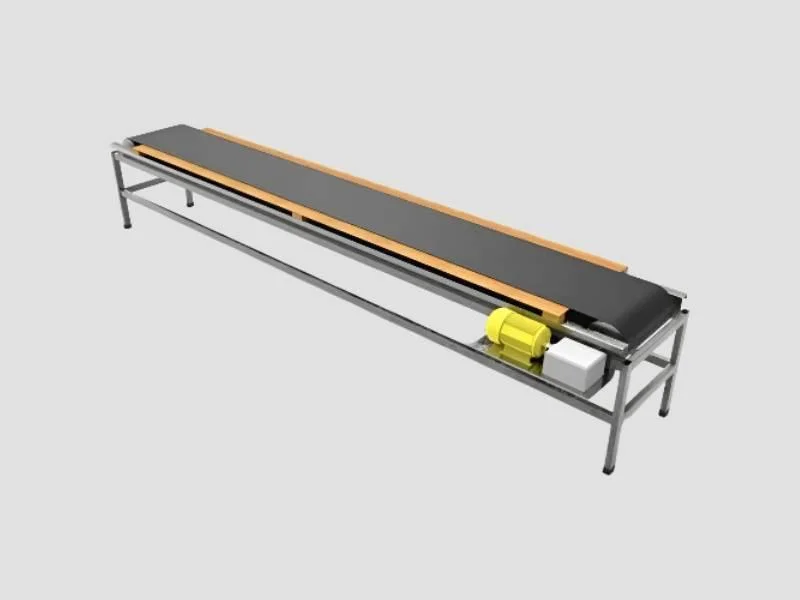
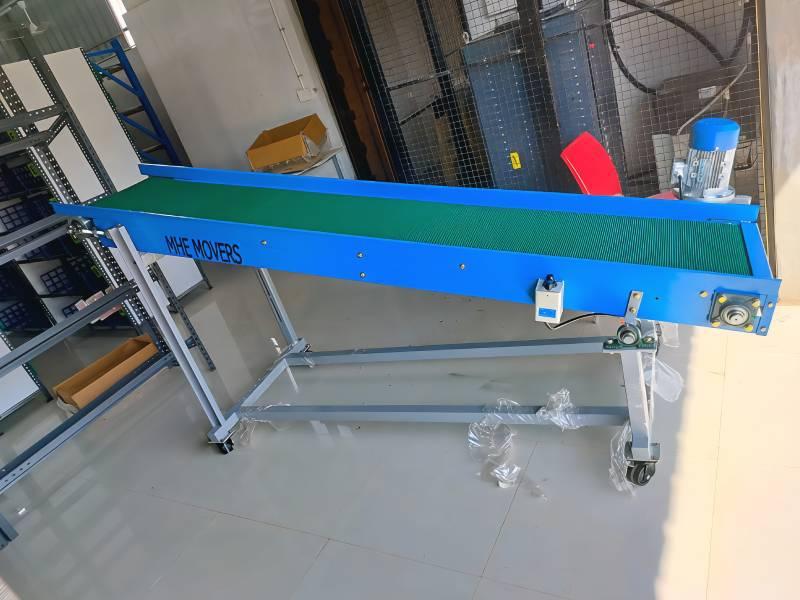
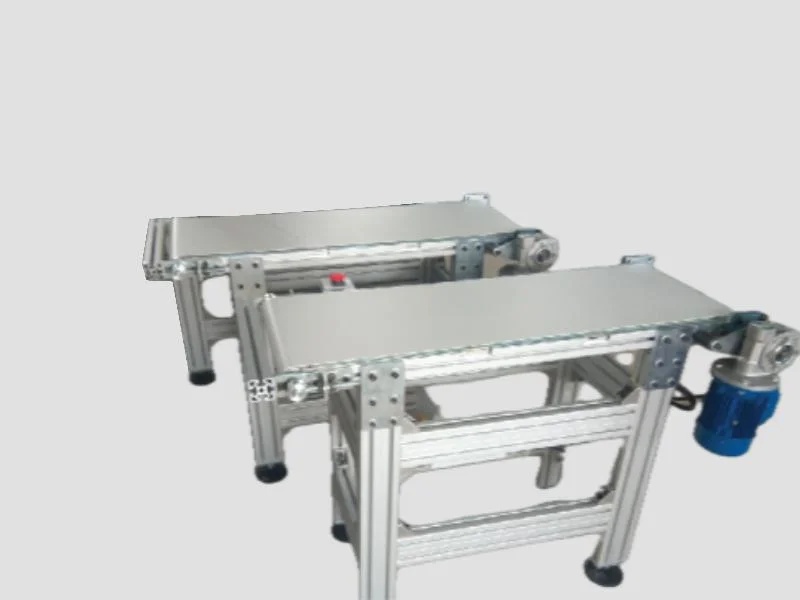
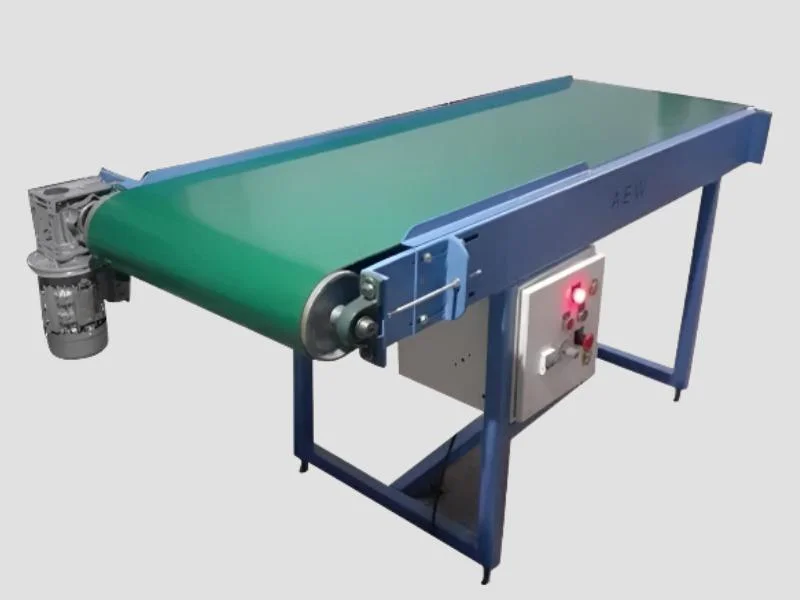
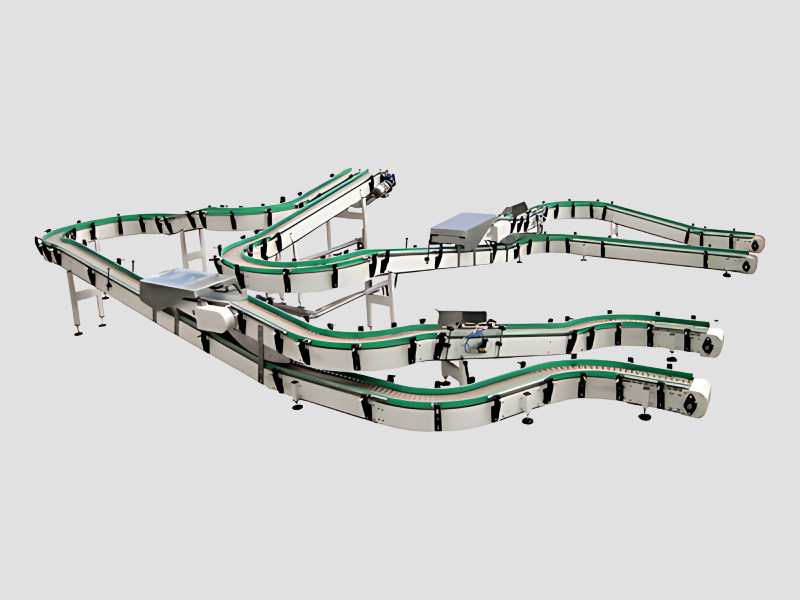
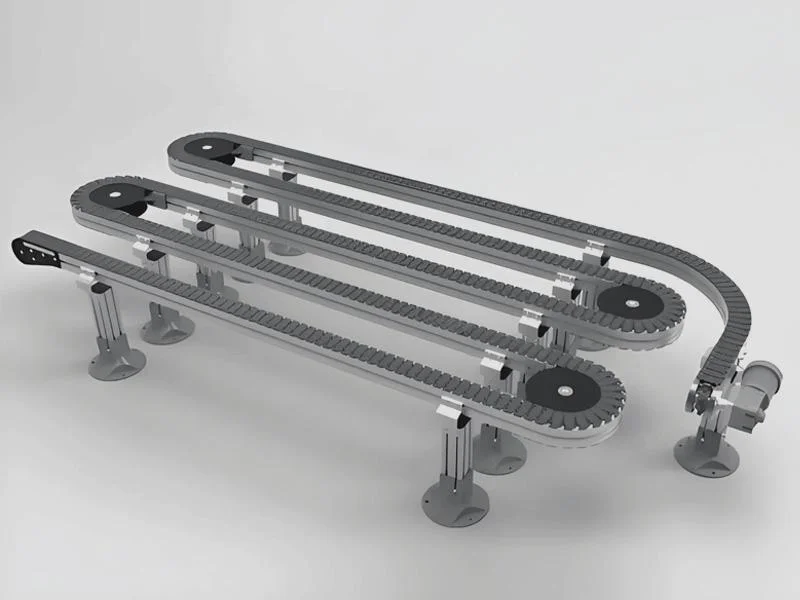
Flat Belt Conveyors: These conveyors have a flat surface and are ideal for transporting light to medium-weight products in horizontal layouts. They are commonly used in assembly lines and packaging operations.
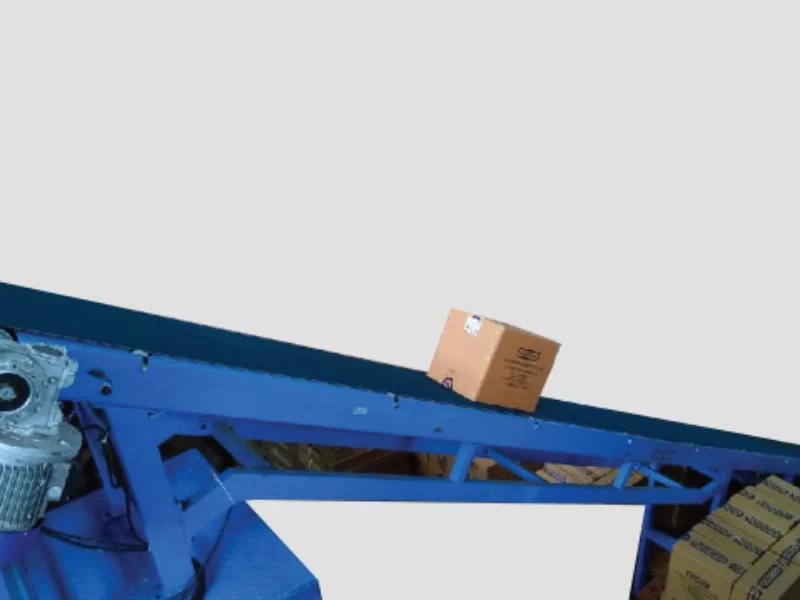
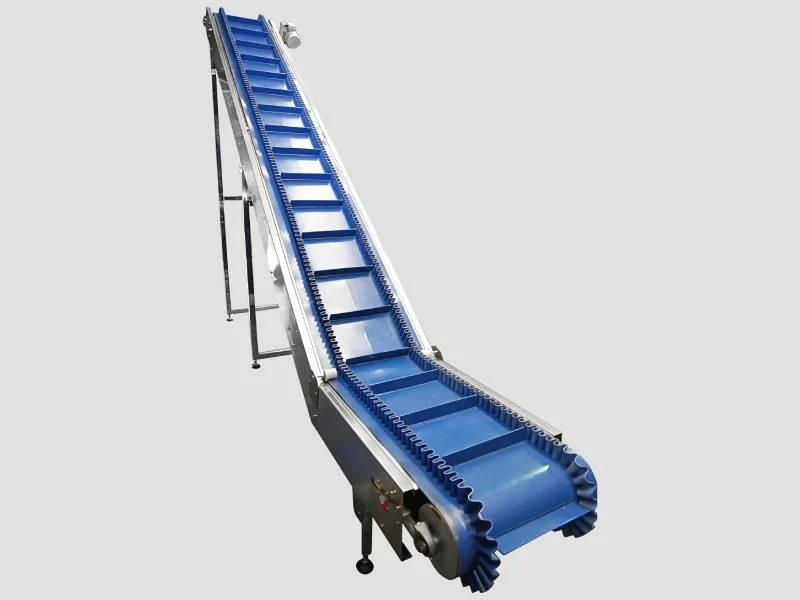
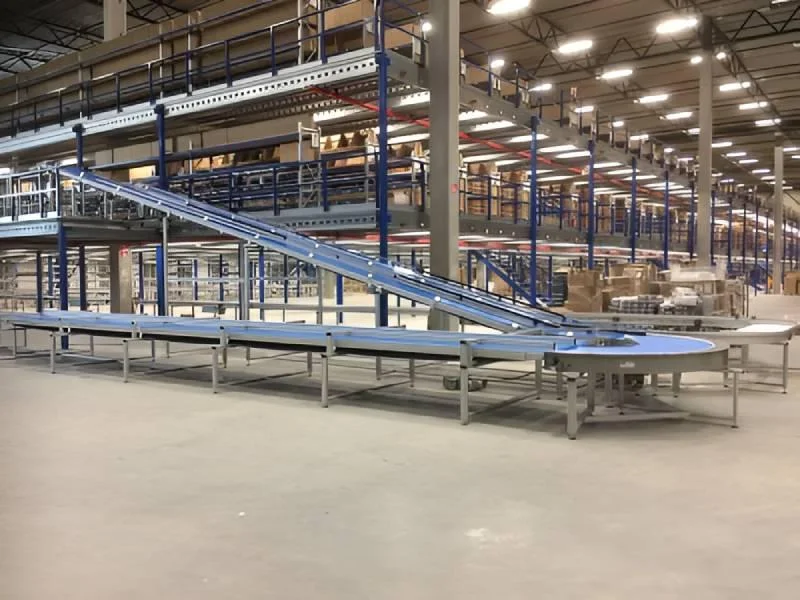
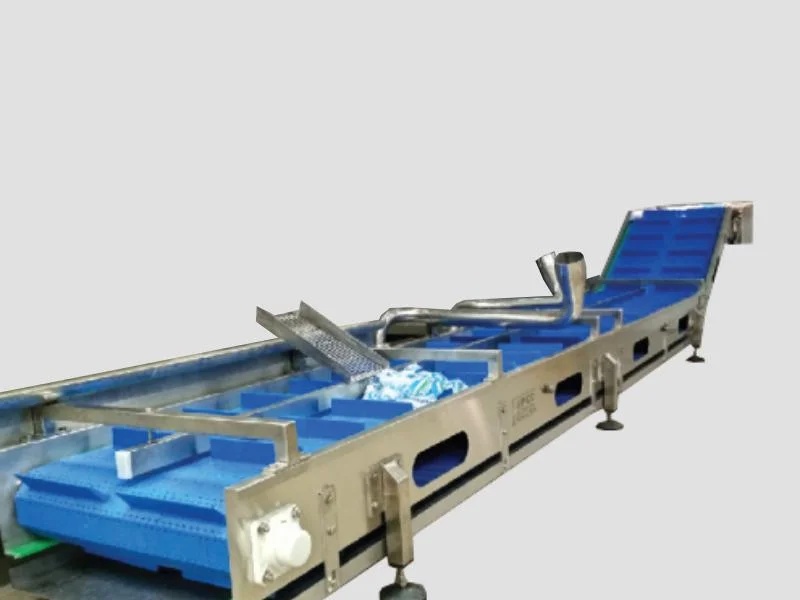
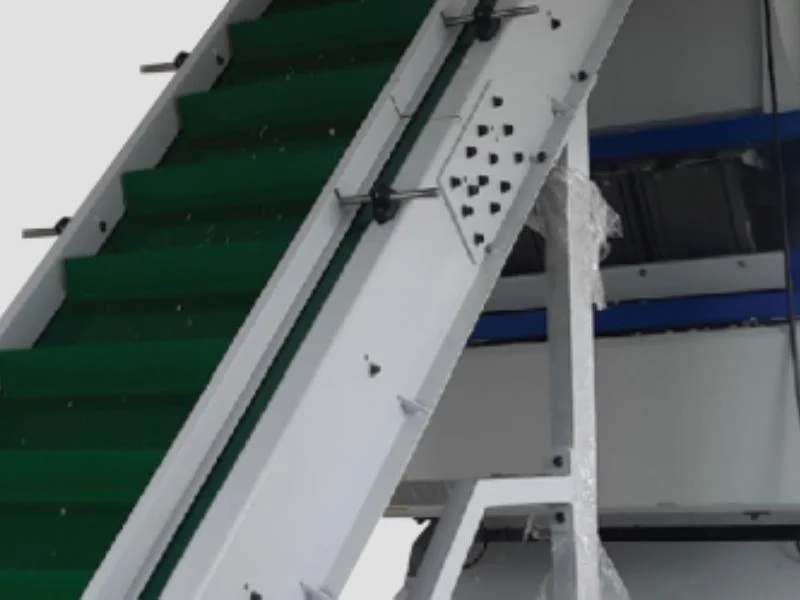
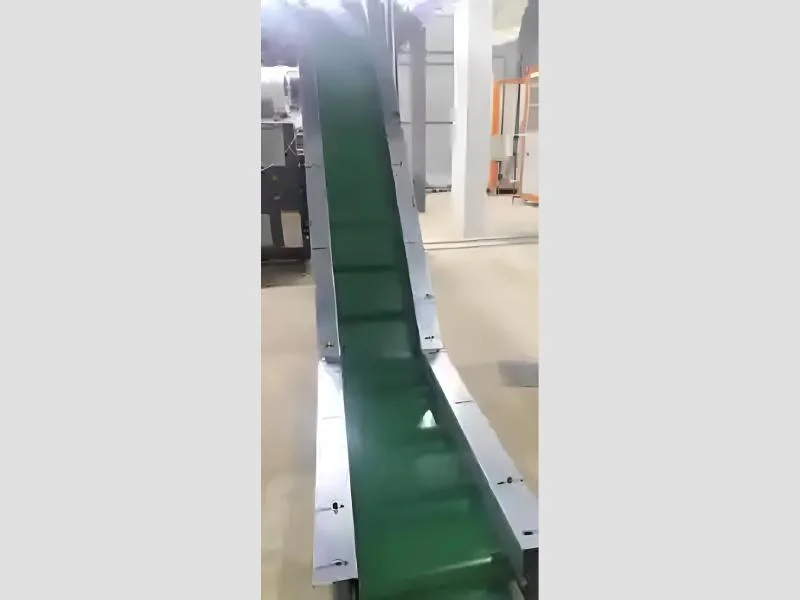
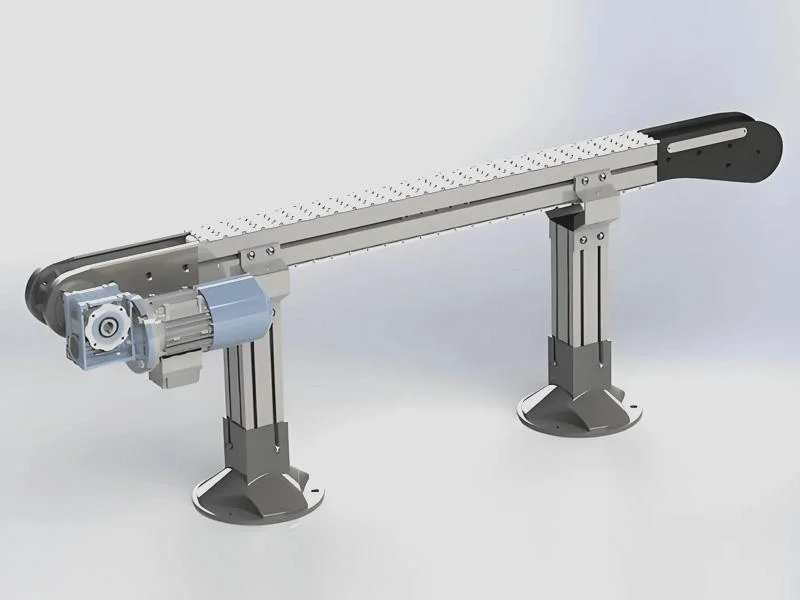
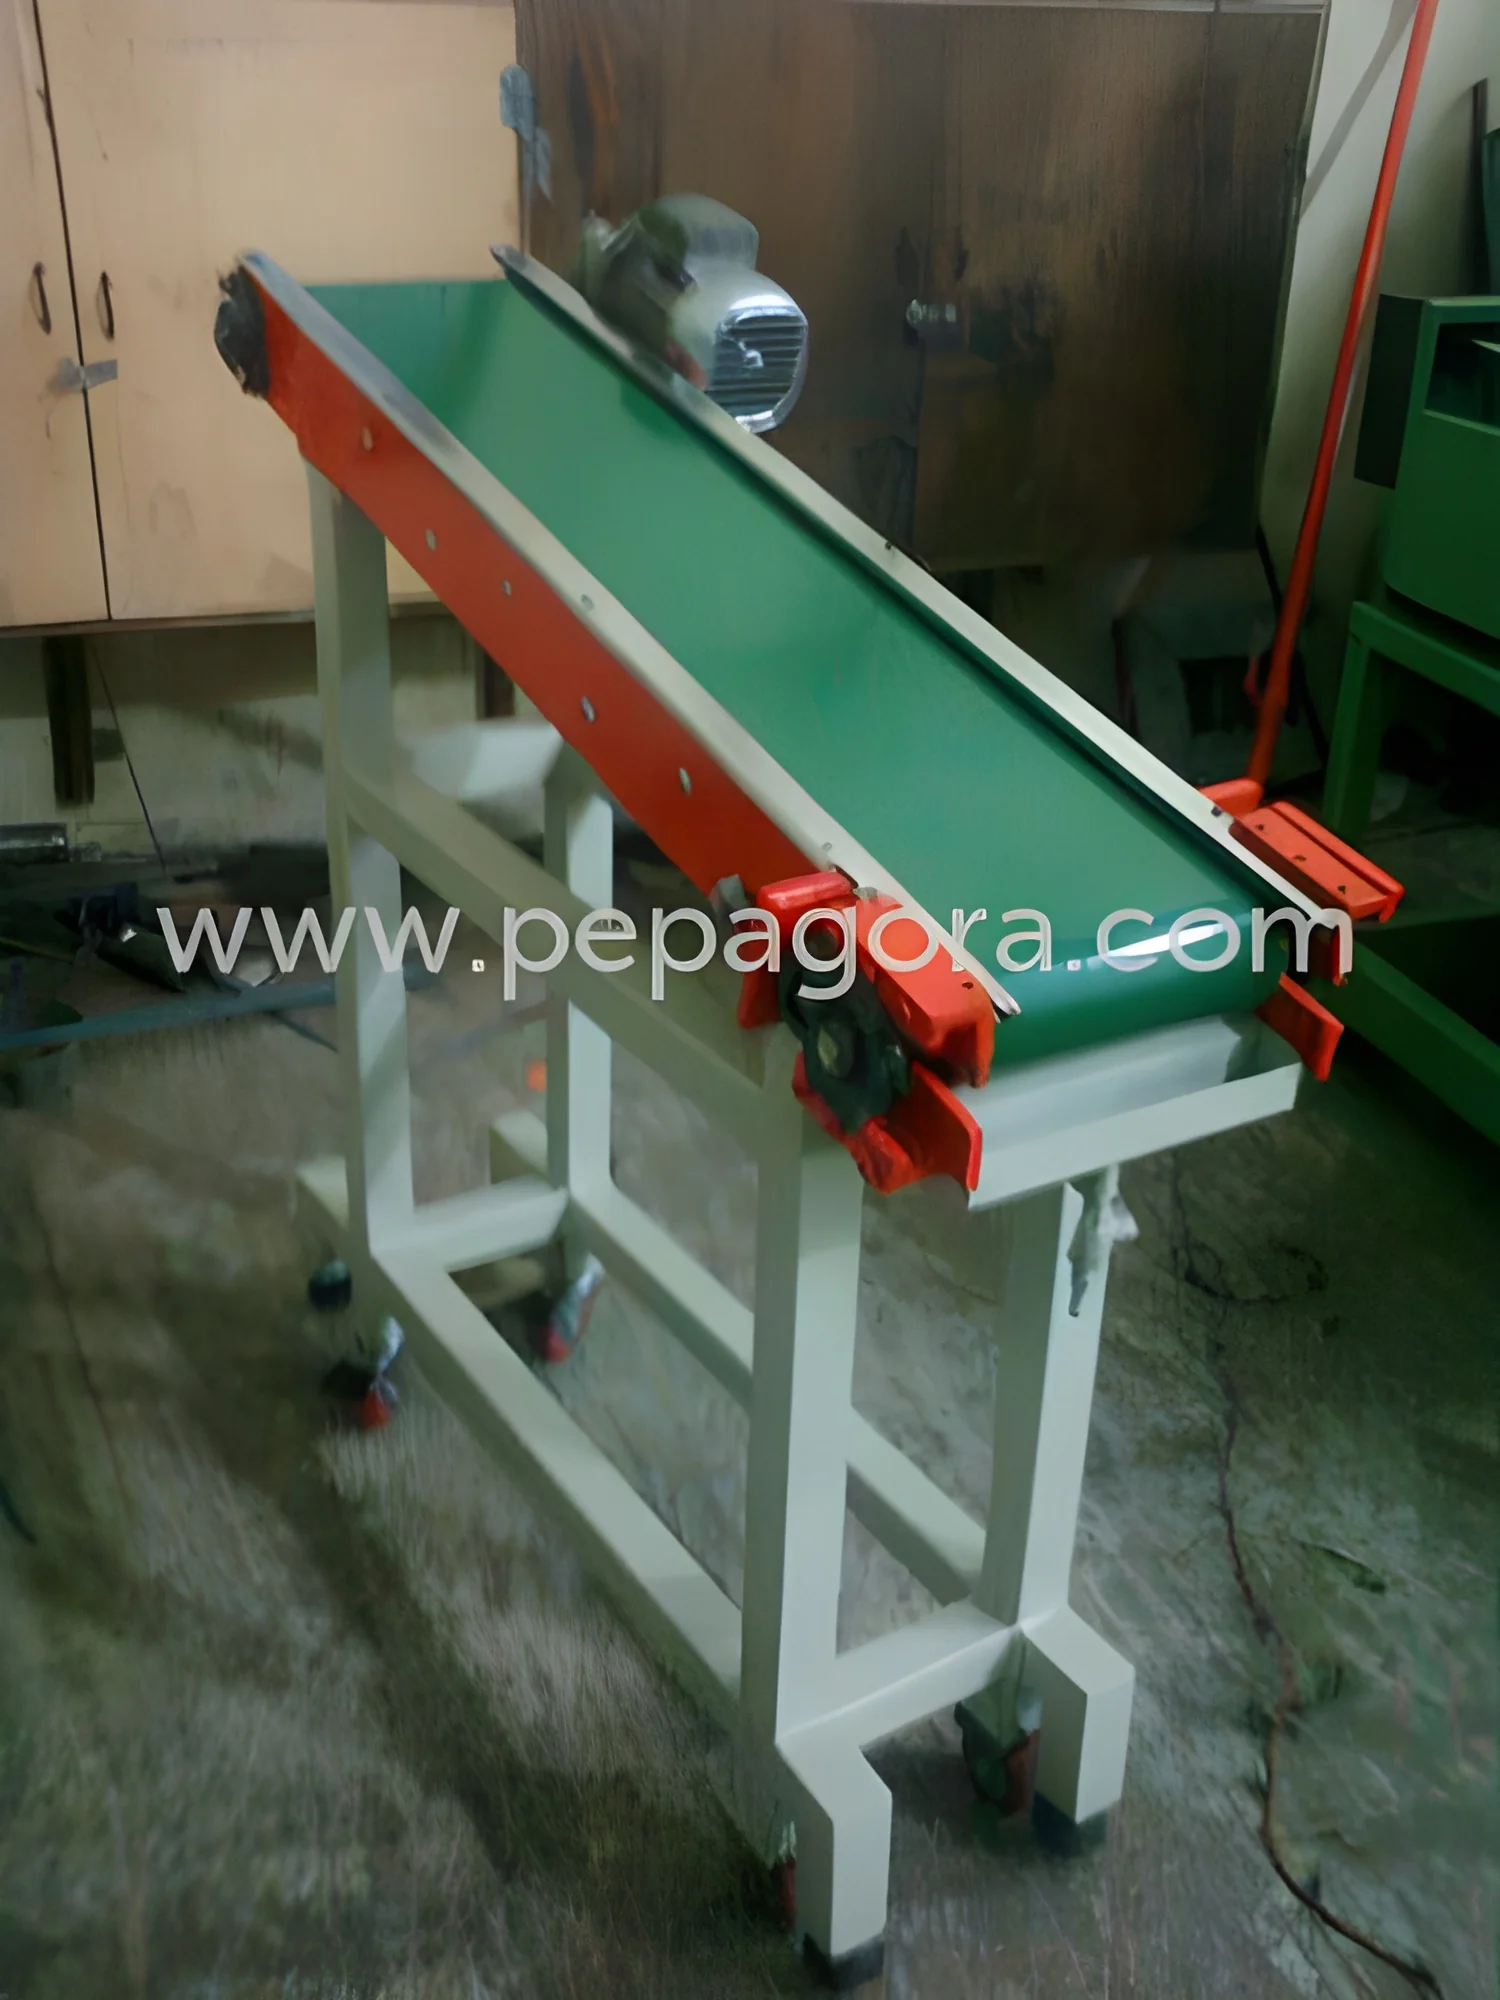
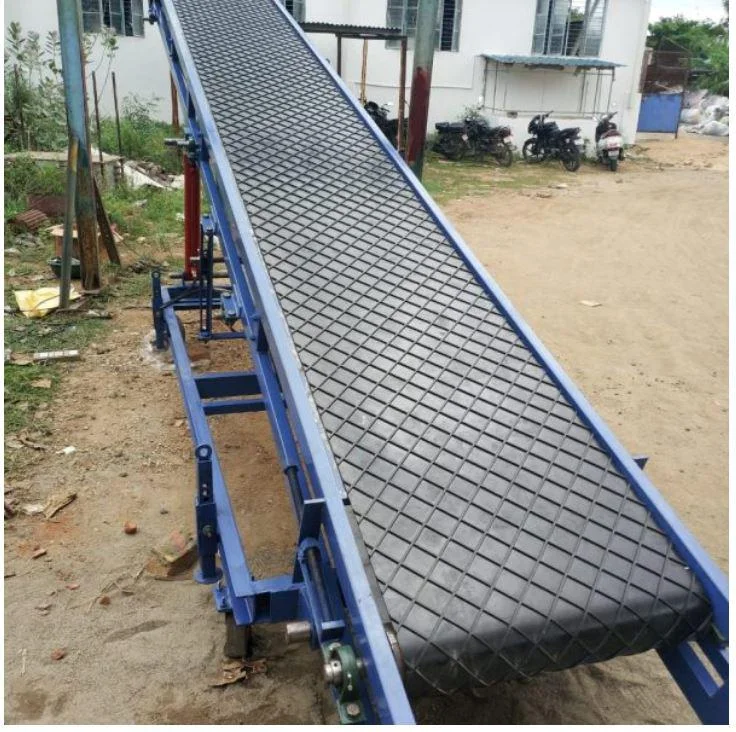
Inclined Belt Conveyors: Designed to transport materials at an angle, inclined belt conveyors are perfect for moving goods between different height levels. They are widely used in bulk material handling and logistics.
Benefits and Advantages
Belt conveyors provide numerous advantages that can significantly enhance operational efficiency.
1. Increased Efficiency: Belt conveyors automate the material handling process, reducing manual labor and increasing throughput.
2. Versatility: They can handle a wide range of materials, from light packages to heavy bulk items, making them suitable for various applications.
3. Cost-Effective: Over time, the use of belt conveyors can lower labor costs and improve productivity, leading to significant savings.
4. Reduced Risk of Injury: By minimizing manual handling, belt conveyors help reduce workplace injuries related to lifting and transporting heavy items.
5. Customization: Many belt conveyors can be customized in terms of length, width, and materials to fit specific operational needs.
6. Low Maintenance: Modern belt conveyors are designed for durability and require minimal maintenance, resulting in lower operational costs.
Buying Guide for B2B Buyers
When sourcing Belt Conveyors (Flat, Inclined), several factors should be considered to ensure the best purchase.
1. Quality Assessment: Evaluate the quality of materials and construction. Look for conveyors that meet industry standards to ensure longevity and reliability.
2. Supplier Verification: Vet potential suppliers by checking their credentials, customer reviews, and track record in the industry. A reputable supplier will provide quality products and support.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities. Compare costs among suppliers to find a competitive price while considering the quality offered.
4. Delivery and Lead Times: Discuss delivery schedules and lead times with suppliers. Ensure that they can meet your operational timelines to avoid disruptions.
5. Compliance Requirements: Verify that the conveyors meet relevant regulatory and safety standards. This includes certifications such as CE and compliance with local regulations.
Compliance and Certifications
Compliance with quality standards is essential for ensuring the safety and reliability of belt conveyors. Relevant standards include ISO 9001, which outlines quality management systems. Additionally, HACCP guidelines may apply in food processing environments, ensuring that food safety is maintained throughout the conveyor system.
Industry certifications, such as CE, indicate that the equipment meets European safety and environmental requirements. Safety and testing requirements include thorough assessments of materials and operational safety features to minimize risks during operation.
Regional compliance considerations may vary, so it is important to understand local regulations and ensure that the conveyor systems are compliant to avoid legal issues and ensure operational efficiency.
Why Source Belt Conveyors (Flat, Inclined) from Pepagora?
Pepagora offers a reliable platform for sourcing Belt Conveyors (Flat, Inclined), providing several key advantages for B2B buyers.
Verified Supplier Network: Pepagora has a robust network of verified suppliers, ensuring that buyers have access to quality products. The platform conducts thorough evaluations to maintain supplier credibility.
Streamlined RFQ Process: The Request for Quotation (RFQ) process on Pepagora is designed to be user-friendly. Buyers can easily submit their requirements and receive competitive quotes from multiple suppliers, simplifying the decision-making process.
Trade Assurance and Support: Pepagora prioritizes buyer protection, offering trade assurance to safeguard transactions. Additionally, dedicated support is available to assist buyers throughout the sourcing process.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora provides extensive regional coverage. This geographic reach enables buyers to connect with local suppliers, facilitating faster delivery and support.












Frequently Asked Questions
What are Belt Conveyors (Flat, Inclined)?
Belt Conveyors (Flat, Inclined) are mechanical devices used to transport materials from one location to another. They utilize a continuous belt that moves over pulleys, facilitating the movement of bulk materials or products across various industries.
What are the different types of Belt Conveyors (Flat, Inclined)?
The primary types of Belt Conveyors include flat belt conveyors and inclined belt conveyors. Flat belt conveyors are used for horizontal transport, while inclined belt conveyors are designed to move materials at an angle, making them suitable for elevating items to different heights.
How do I choose the right Belt Conveyors (Flat, Inclined)?
Choosing the right Belt Conveyor involves considering factors such as the type of material to be transported, the distance of transport, and the required incline angle. Additionally, evaluating the conveyor's load capacity, speed, and environment can help ensure optimal performance.
What are the standard specifications for Belt Conveyors (Flat, Inclined)?
Standard specifications for Belt Conveyors typically include belt width, length, speed, and load capacity. Other considerations may include the material of the belt, frame design, and motor specifications, which can vary based on the application.
What is the price range for Belt Conveyors (Flat, Inclined)?
The price range for Belt Conveyors can vary significantly based on specifications, size, and manufacturer. On average, prices may range from a few thousand to several lakhs of Indian Rupees, depending on the complexity and customization of the conveyor system.
What quality standards apply to Belt Conveyors (Flat, Inclined)?
Quality standards for Belt Conveyors often include compliance with industry certifications such as ISO 9001 and safety regulations. Manufacturers may also adhere to specific standards set by organizations like the American National Standards Institute (ANSI) regarding performance and safety.
Where can I find Belt Conveyors (Flat, Inclined) suppliers in India?
You can find Belt Conveyors (Flat, Inclined) suppliers in India through various B2B marketplaces, trade shows, and industry directories. Websites like Pepagora.com provide a comprehensive listing of manufacturers and suppliers, allowing for easy comparison and sourcing.
Can Belt Conveyors (Flat, Inclined) be customized?
Yes, Belt Conveyors can be customized to meet specific operational requirements. Customization options may include variations in length, width, materials, and incline angles to suit particular applications and environments.
What is the typical minimum order quantity for Belt Conveyors (Flat, Inclined)?
The typical minimum order quantity (MOQ) for Belt Conveyors can vary among manufacturers. Generally, the MOQ may range from one unit for standard models to larger quantities for custom designs, depending on the supplier's policies.
What is the typical lead time for Belt Conveyors (Flat, Inclined)?
The typical lead time for Belt Conveyors can range from a few weeks to several months, depending on factors such as customization, manufacturing capacity, and supplier location. It is advisable to consult with suppliers for specific timelines based on your order requirements.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
