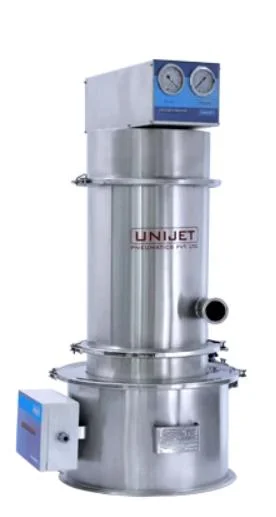
What are Vacuum Sealers?
Vacuum sealers are industrial machines designed to remove air from packaging, creating a vacuum seal that preserves the contents within. By eliminating air, these machines help extend the shelf life of perishable goods, protect against freezer burn, and prevent spoilage. Vacuum sealing is an efficient method for packaging food, pharmaceuticals, and various other products requiring preservation and protection from moisture, oxygen, and contaminants.
In business applications, vacuum sealers are essential in industries such as food processing, pharmaceuticals, and electronics. They are commonly used to package food items for storage or transportation, ensuring freshness and quality. Additionally, vacuum sealers are utilized in laboratories to store sensitive materials and in manufacturing processes to protect components from environmental factors. The growing demand for packaged goods and the need for efficient inventory management have resulted in increased adoption of vacuum sealing technology across various sectors.
The vacuum sealer market is expanding rapidly, driven by trends such as convenience, sustainability, and the need for longer shelf life. Businesses are increasingly looking for solutions that not only preserve products but also enhance brand image and customer satisfaction. As a result, vacuum sealers have become a vital tool for companies seeking to optimize their packaging processes and meet consumer demands.
Key Features and Specifications
Vacuum sealers come with a range of features designed to enhance their performance and usability. Understanding these specifications is crucial for selecting the right machine for specific business needs.
Key specifications include:
1. Sealing Speed
- This specification indicates how quickly the machine can create a seal.
- Typical ranges can vary based on the model and design.
2. Vacuum Strength
- Refers to the level of vacuum achieved within the packaging.
- Measured in millibars, a lower number indicates better vacuum sealing capabilities.
3. Chamber Size
- The dimensions of the chamber determine the maximum size of items that can be sealed.
- Common sizes range from small models for home use to larger industrial units.
4. Power Consumption
- This indicates the electrical efficiency of the vacuum sealer.
- Specifications often range from low wattage for small units to higher power for industrial models.
5. Control Features
- Many machines offer digital controls for precision in sealing.
- Features may include programmable settings for different types of products.
6. Durability and Materials
- Construction materials impact the longevity and reliability of the vacuum sealer.
- Machines made from stainless steel are typically more durable than plastic counterparts.
7. Portability
- Some models are designed to be lightweight and easy to transport.
- This can be important for businesses that require mobility.
8. Maintenance Requirements
- Regular maintenance ensures optimal performance.
- Specifications may include ease of cleaning and part replacement.
In summary, understanding the key features and specifications of vacuum sealers is essential for making informed purchasing decisions. Businesses should carefully assess these parameters to select the right machine for their specific applications.
Common Applications and Use Cases
Vacuum sealers find diverse applications across various industries, enhancing efficiency and product protection.
1. Food Processing: In this sector, vacuum sealers are used to package meats, cheese, and vegetables, extending shelf life and maintaining freshness during transportation.
2. Pharmaceuticals: Vacuum sealing is critical for protecting sensitive medical supplies and ensuring their integrity during storage and shipping processes.
3. Electronics: Manufacturers use vacuum sealers to package electronic components, preventing moisture and dust contamination that could impair functionality.
4. Retail: Vacuum sealers are employed for food packaging in retail environments, appealing to consumers looking for convenience and longer-lasting products.
5. Agriculture: Farmers utilize vacuum sealing for preserving seeds and fertilizers, ensuring they remain effective over time.
6. Industrial Packaging: Various manufacturers rely on vacuum sealers to package tools and parts, protecting them from corrosion and damage.
7. Storage Solutions: Businesses in need of bulk storage utilize vacuum sealers to save space and protect goods from environmental factors.
Product Variants and Subcategories
Vacuum sealers come in various forms tailored to different market needs. Each variant offers unique features suited for specific applications.
External Vacuum Sealers
These machines are designed for home and small business use, featuring compact designs and easy operation. They are ideal for sealing smaller items and typically have a lower price point.
Chamber Vacuum Sealers
Chamber sealers are larger and more robust, suitable for industrial applications. They can seal multiple items at once and achieve a stronger vacuum, making them ideal for packaging bulk products.
Commercial Grade Sealers
These heavy-duty machines are built for high-volume operations, suitable for restaurants and large food processing companies. They offer superior sealing speeds and durability for continuous use.
Portable Vacuum Sealers
Lightweight and easy to use, these models are ideal for on-the-go applications or small business needs. They are convenient for temporary setups or limited workspace.
Benefits and Advantages
Utilizing vacuum sealers provides numerous advantages for businesses looking to enhance their packaging processes.
Key benefits include:
1. Extended Shelf Life: Vacuum sealing significantly prolongs the freshness and quality of products, reducing waste and increasing profitability.
2. Cost Efficiency: By minimizing spoilage, businesses can save on costs associated with product loss and waste management.
3. Improved Product Integrity: Vacuum sealers protect products from environmental factors, ensuring they reach customers in optimal condition.
4. Enhanced Storage: Vacuum sealing reduces the size of packages, allowing for more efficient use of storage space.
5. Versatility: These machines can handle a wide variety of products, making them suitable for numerous applications across different industries.
6. Increased Customer Satisfaction: Providing well-packaged, fresh products improves customer experience and can enhance brand loyalty.
Buying Guide for B2B Buyers
When sourcing vacuum sealers, there are several factors that B2B buyers should consider to ensure they select the right equipment for their needs.
1. Quality Assessment: It is essential to evaluate the quality of the vacuum sealers through customer reviews, product demonstrations, and manufacturer reputation.
2. Supplier Verification: Vetting suppliers is crucial. Buyers should check certifications, product warranties, and customer support capabilities to ensure reliability.
3. Pricing and MOQ: Understanding the pricing structure and minimum order quantities is vital for budgeting and ensuring that the purchase aligns with business needs.
4. Delivery and Lead Times: Buyers should inquire about logistics, delivery schedules, and potential delays to ensure timely receipt of equipment.
5. Compliance Requirements: It is necessary to verify that the vacuum sealers meet regional and industry-specific compliance standards to avoid regulatory issues.
Compliance and Certifications
Vacuum sealers must adhere to various quality standards and certifications to ensure safety and reliability in their operations.
Relevant quality standards include ISO 9001, which focuses on maintaining a quality management system. This standard ensures that manufacturers produce vacuum sealers that meet customer and regulatory requirements.
HACCP (Hazard Analysis Critical Control Point) is another important standard, particularly in food processing, guiding businesses in identifying and controlling food safety hazards.
CE certification indicates that a product complies with European health, safety, and environmental protection standards. This certification is vital for businesses looking to operate within the European market.
Safety and testing requirements are also crucial, with manufacturers typically conducting rigorous testing to ensure that their vacuum sealers perform safely and effectively.
Finally, regional compliance considerations may vary, so businesses should be aware of local regulations regarding packaging and food safety.
Why Source Vacuum Sealers from Pepagora?
Pepagora provides a trusted platform for sourcing vacuum sealers, offering several key advantages for B2B buyers.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, ensuring quality and reliability in the purchasing process. This network helps businesses find reputable manufacturers with a proven track record.
Streamlined RFQ Process: The platform features a user-friendly request for quotation (RFQ) process, simplifying the procurement journey. Buyers can easily submit their requirements and receive competitive quotes from various suppliers.
Trade Assurance and Support: Pepagora offers trade assurance and support services to protect buyers during transactions. This includes assistance with disputes and ensuring that products meet quality standards.
Regional Coverage: The platform has a broad geographic reach, catering to businesses in India, the GCC, and Southeast Asia. This ensures that buyers can access a diverse range of vacuum sealers suited to their specific needs across different markets.

 IN