
 IN
Other Conveyors & Material Handling Systems
208 products available
What are Other Conveyors & Material Handling Systems?
Other Conveyors & Material Handling Systems refer to a diverse range of equipment designed to move products, materials, or components efficiently within a facility. These systems are essential in streamlining operations, reducing manual labor, and enhancing productivity. They encompass various conveyor types and material handling solutions that can be tailored to meet specific industry needs.
These systems find applications in multiple sectors, including manufacturing, logistics, food processing, and pharmaceuticals. Businesses utilize them for tasks like transporting bulk materials, packaging items, and storing products. By automating these processes, companies can achieve consistency, improve safety, and reduce operational costs. The relevance of Other Conveyors & Material Handling Systems is underscored by their ability to adapt to evolving industry demands and technological advancements.
Key Features and Specifications
Other Conveyors & Material Handling Systems come equipped with various features designed to enhance performance and efficiency. Understanding these specifications is crucial for selecting the right system for your business needs.
Key specifications include:
1. Load Capacity
- This specification indicates the maximum weight the system can handle.
- Typical ranges vary based on the type of conveyor, from lightweight products to heavy materials.
2. Speed
- This defines how quickly materials can be transported along the conveyor.
- Speeds can range from a few feet per minute to several hundred feet per minute.
3. Material Construction
- Conveyors are made from materials such as steel, aluminum, or plastic.
- The choice of material affects durability and suitability for specific environments.
4. Drive Type
- Systems may feature belt-driven, chain-driven, or gravity-driven designs.
- Each type offers distinct advantages depending on the application.
5. Dimensions
- The size and layout of the conveyor system must fit the operational area.
- Dimensions can be customized to optimize space utilization.
6. Control Systems
- Many conveyors integrate automated control systems for operation.
- These can include sensors for monitoring and adjusting flow rates.
7. Safety Features
- Safety mechanisms such as emergency stop buttons and guards are vital.
- These features help prevent accidents and ensure compliance with regulations.
8. Maintenance Requirements
- Understanding the maintenance needs is crucial for longevity.
- Some systems require regular lubrication, while others may need minimal upkeep.
In summary, evaluating these specifications helps businesses choose the right Other Conveyors & Material Handling Systems for their operational requirements.
Common Applications and Use Cases
Other Conveyors & Material Handling Systems are versatile and serve multiple industries effectively.
1. Manufacturing: In manufacturing environments, these systems are used to transport raw materials and finished products along assembly lines, optimizing workflow and efficiency.
2. Logistics: Warehousing and distribution centers utilize conveyors to streamline sorting and packaging processes, enabling quick and accurate order fulfillment.
3. Food Processing: In the food industry, conveyors assist in moving items through various stages of production, from washing to packaging, ensuring hygiene and efficiency.
4. Pharmaceuticals: These systems are critical in pharmaceutical facilities for transporting sensitive materials and ensuring compliance with stringent safety standards.
5. Automotive: In automotive production, conveyors facilitate the movement of parts and assemblies, supporting just-in-time manufacturing processes.
6. Retail: Retailers use conveyor systems for efficient checkout processes, moving items from the storage area to the sales floor seamlessly.
7. Recycling: In recycling plants, conveyors help sort and transport recyclable materials, improving operational efficiency and sustainability.
Product Variants and Subcategories
The diversity of Other Conveyors & Material Handling Systems allows for various configurations and setups to address specific operational needs.
Belt Conveyors
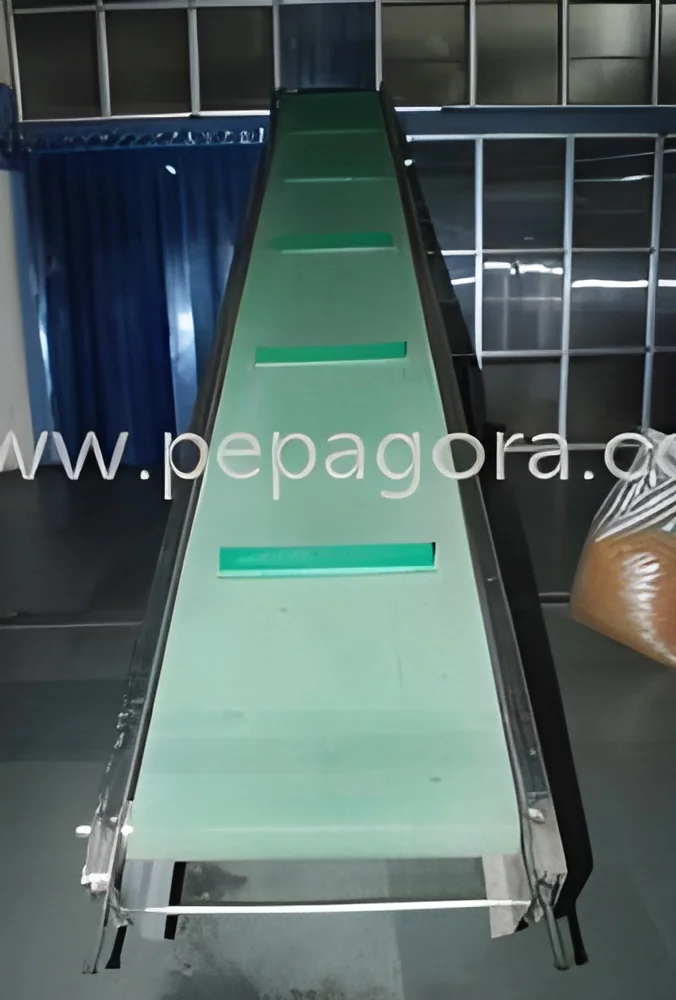
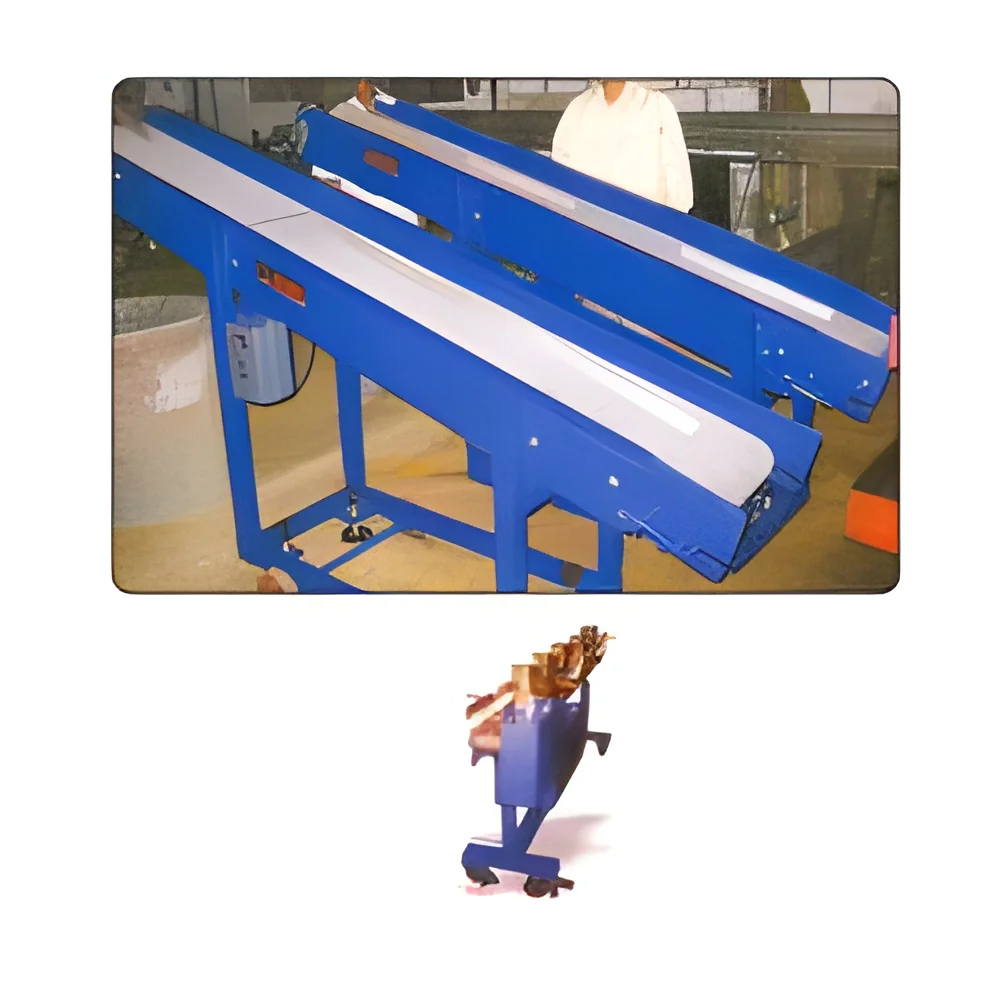
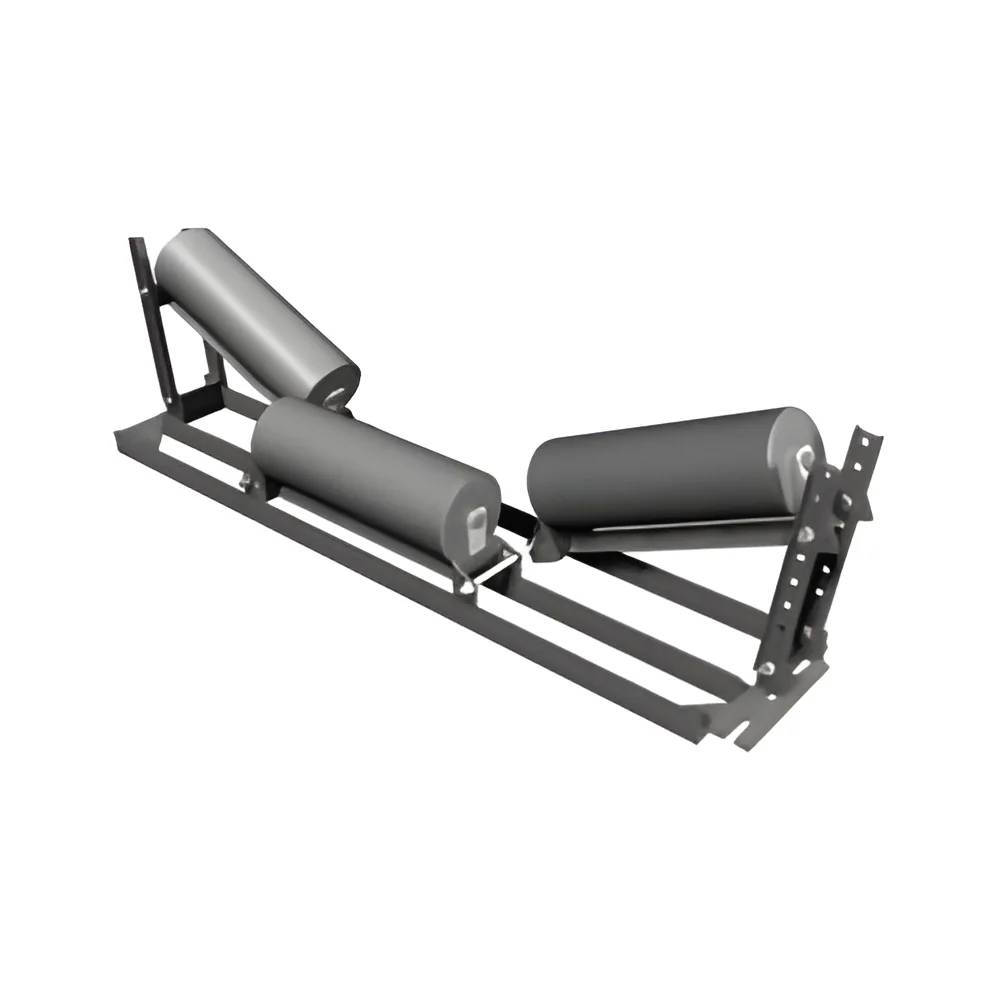
Belt conveyors are widely used for transporting materials over long distances in a continuous manner. They can handle a variety of materials, from granular substances to large packages, making them versatile for different applications.
Roller Conveyors
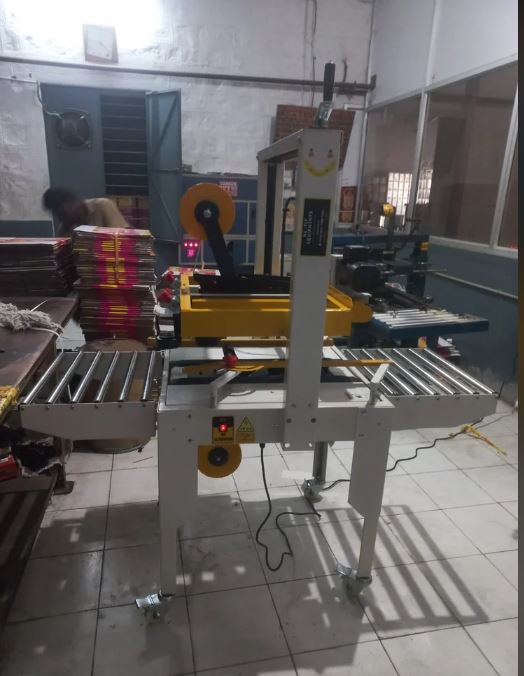
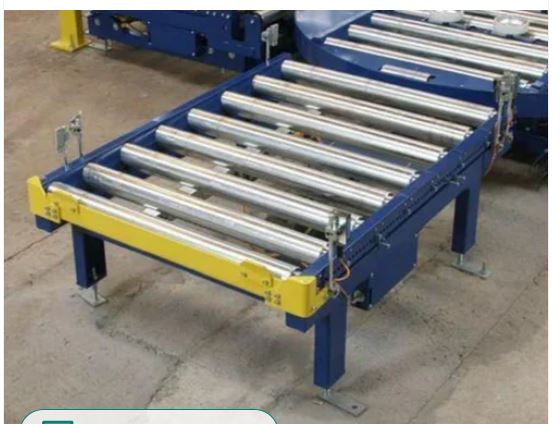
These systems utilize rollers to allow items to move along the conveyor with minimal effort. They are ideal for heavy loads and are often used in warehouses and distribution centers for sorting and transporting packages.
Chain Conveyors
Chain conveyors are designed for heavy-duty applications and are particularly effective in moving large or bulky items. They are commonly found in manufacturing environments where durability and strength are essential.
Pneumatic Conveyors
These systems utilize air pressure to transport materials through tubes. They are especially useful for moving powders and granules in industries such as food processing and pharmaceuticals.
Benefits and Advantages
Investing in Other Conveyors & Material Handling Systems provides numerous benefits to organizations.
1. Increased Efficiency: These systems automate material transport, reducing time and labor costs associated with manual handling.
2. Enhanced Safety: By minimizing manual handling, conveyors reduce the risk of workplace injuries, making operations safer for employees.
3. Improved Accuracy: Automated systems decrease the likelihood of human error, leading to more accurate inventory management and order fulfillment.
4. Flexibility: Conveyors can be customized to meet specific operational requirements, making them suitable for various industries and applications.
5. Cost Savings: Streamlined operations lead to reduced operational costs over time, providing significant returns on investment.
6. Space Optimization: Many conveyor systems are designed to utilize vertical space, allowing for more efficient warehouse layouts.
Buying Guide for B2B Buyers
When considering Other Conveyors & Material Handling Systems, several factors should be evaluated to ensure the right choice for your business.
1. Quality Assessment: Look for systems that meet established quality standards. Evaluate materials, construction quality, and overall durability to ensure reliable performance.
2. Supplier Verification: Vet potential suppliers by checking references and industry certifications. A verified supplier network can provide peace of mind regarding product quality.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities. This helps in budgeting and ensures that the investment aligns with business needs.
4. Delivery and Lead Times: Assess logistical capabilities, including delivery schedules and lead times. Timely delivery is crucial to avoid operational disruptions.
5. Compliance Requirements: Be aware of industry-specific regulations and certifications, such as CE marking, to ensure that the systems meet necessary compliance criteria.
Compliance and Certifications
Other Conveyors & Material Handling Systems must adhere to various quality standards and certifications to ensure safe and effective operation.
Relevant quality standards include ISO 9001, which establishes guidelines for quality management systems, helping organizations enhance customer satisfaction through effective process management.
Industry certifications such as CE mark indicate compliance with European health, safety, and environmental protection standards. These certifications are crucial for manufacturers and suppliers aiming to operate in global markets.
Safety and testing requirements ensure that conveyor systems are designed with employee safety in mind. Regular testing and maintenance are essential to maintain compliance with safety regulations.
Regional compliance considerations may differ based on local laws and regulations. Companies must be aware of these variations to ensure adherence to all applicable standards.
Why Source Other Conveyors & Material Handling Systems from Pepagora?
Pepagora provides a trusted platform for sourcing Other Conveyors & Material Handling Systems with several key advantages.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, ensuring that all products meet quality and safety standards. This verification process gives buyers confidence in their purchasing decisions.
Streamlined RFQ Process: The Request for Quotation (RFQ) system simplifies the procurement process. Buyers can easily compare quotes from multiple suppliers to find the best fit for their needs.
Trade Assurance and Support: Pepagora offers trade assurance, providing buyer protection throughout the purchasing process. This support helps mitigate risks associated with sourcing equipment.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora facilitates access to a diverse range of suppliers and products across these regions. This extensive coverage enables businesses to find local solutions tailored to their operational needs.







Frequently Asked Questions
What are Other Conveyors & Material Handling Systems?
Other Conveyors & Material Handling Systems refer to a variety of equipment designed to transport, manage, and store materials in industrial settings. These systems can include various types of conveyors, as well as additional handling equipment that aids in the efficient movement of goods.
What are the different types of Other Conveyors & Material Handling Systems?
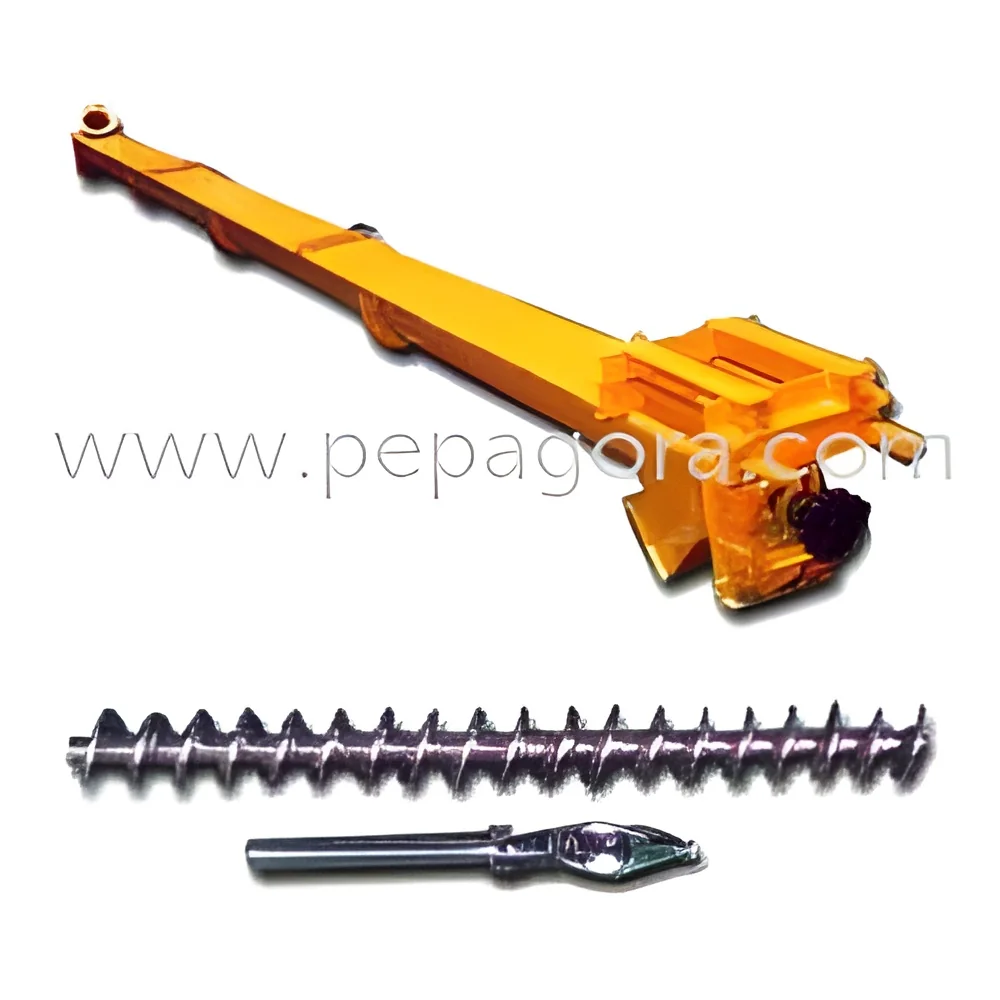
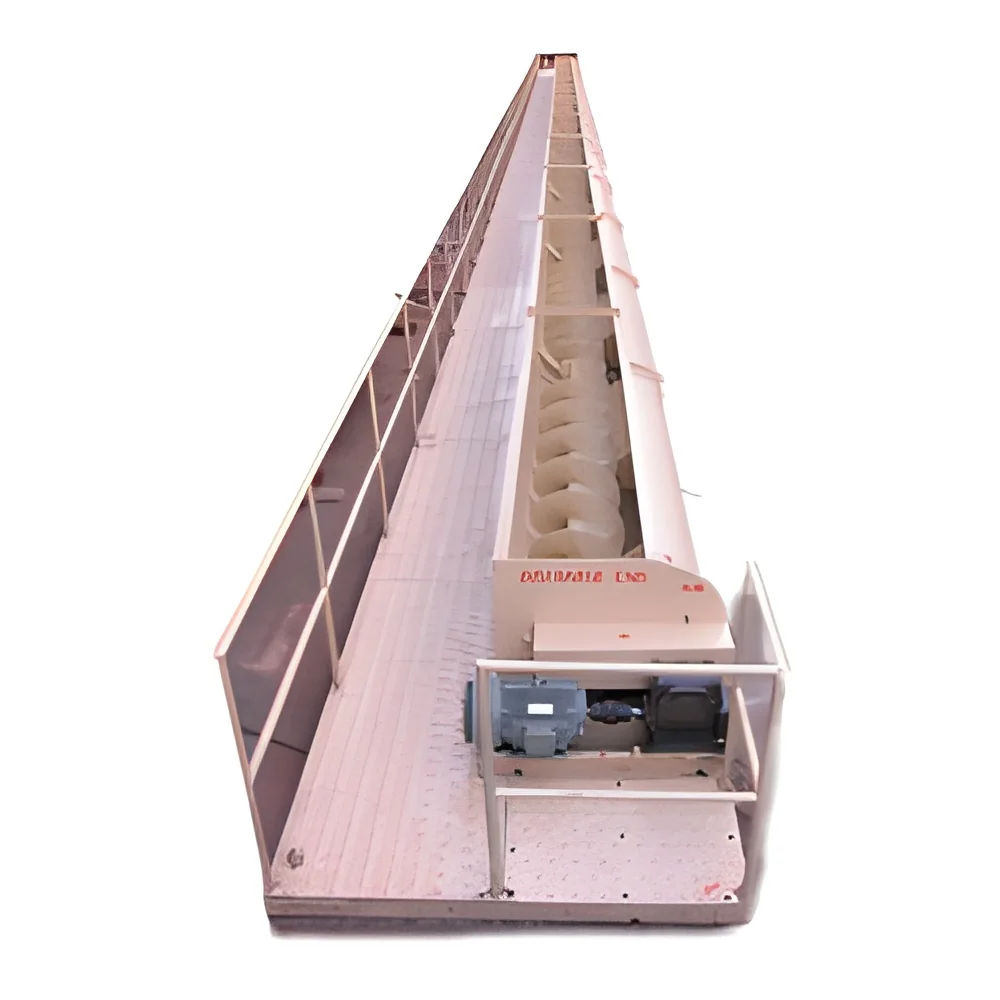
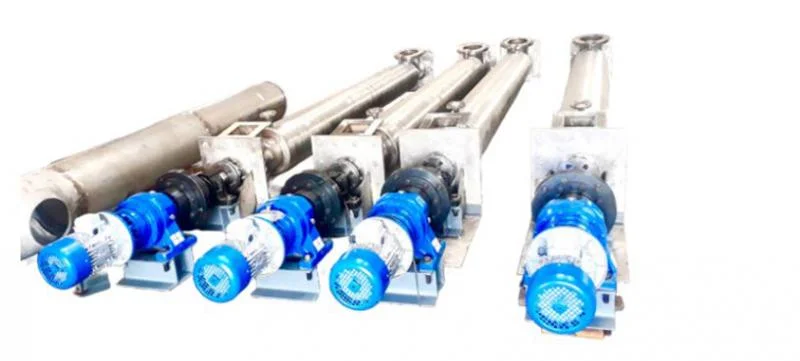
The different types of Other Conveyors & Material Handling Systems include belt conveyors, roller conveyors, chain conveyors, and screw conveyors, among others. Each type serves specific purposes and is suited to different environments and materials.
How do I choose the right Other Conveyors & Material Handling Systems?
Choosing the right Other Conveyors & Material Handling Systems involves assessing the type of materials to be handled, the layout of the facility, and the required throughput. It is also important to consider the system's durability, maintenance requirements, and compatibility with existing equipment.
What are the standard specifications for Other Conveyors & Material Handling Systems?
Standard specifications for Other Conveyors & Material Handling Systems typically include load capacity, speed, material construction, and dimensions. Additionally, specifications may cover safety features and compliance with industry standards.
What is the price range for Other Conveyors & Material Handling Systems?
The price range for Other Conveyors & Material Handling Systems can vary widely based on the type, size, and complexity of the system. Generally, prices can start from a few thousand rupees and go up to several lakhs, depending on specific requirements.
What quality standards apply to Other Conveyors & Material Handling Systems?
Quality standards for Other Conveyors & Material Handling Systems often include ISO certifications and compliance with safety regulations. Manufacturers may adhere to specific industry standards that ensure reliability and efficiency in operations.
Where can I find Other Conveyors & Material Handling Systems suppliers in India?
You can find Other Conveyors & Material Handling Systems suppliers in India through online marketplaces like Pepagora, industry trade shows, and directories. Networking within industry associations may also provide valuable contacts.
Can Other Conveyors & Material Handling Systems be customized?
Yes, Other Conveyors & Material Handling Systems can often be customized to meet specific operational needs. Customization may involve adjusting dimensions, materials, and features to fit unique applications.
What is the typical minimum order quantity for Other Conveyors & Material Handling Systems?
The typical minimum order quantity (MOQ) for Other Conveyors & Material Handling Systems can vary by supplier and the specific product type. Generally, MOQs can range from one unit for standard items to larger quantities for customized systems.
What is the typical lead time for Other Conveyors & Material Handling Systems?
The typical lead time for Other Conveyors & Material Handling Systems varies based on the complexity of the order and the supplier's production schedule. Generally, lead times can range from a few weeks to several months.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
