IN
₹
Apparel & Fashion
Description
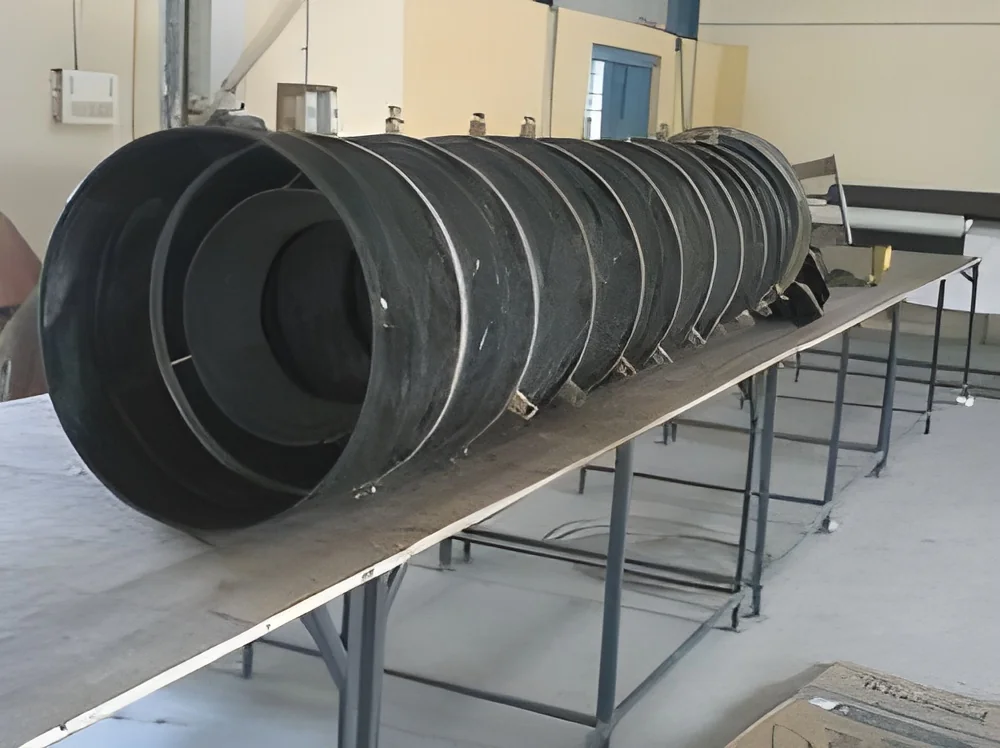
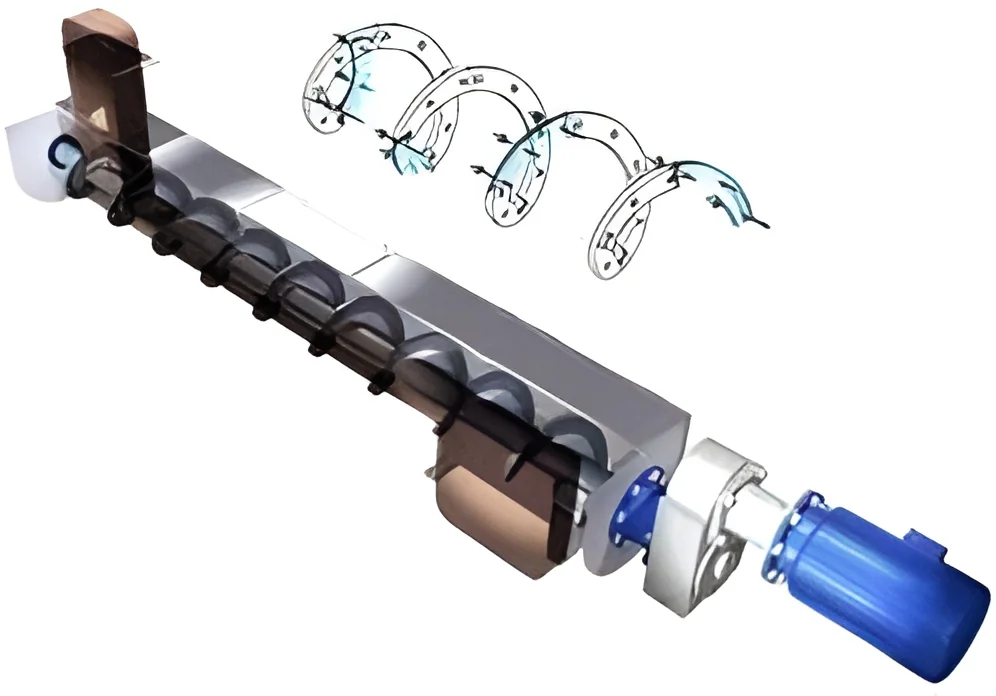
Industrial bulk material handling screw conveyors represent one of the most efficient and versatile material transport solutions available for modern industrial operations. These systems utilize a rotating helical screw blade within a tube or trough to move materials precisely from intake to discharge points. Engineered for reliability and durability, our screw conveyors feature robust construction with customizable options to match specific material characteristics and operational requirements. The enclosed design prevents environmental contamination while protecting materials from external elements, making them suitable for even the most demanding processing environments. With capacities ranging from small batch operations to high-volume continuous processing, these conveyors provide consistent performance across various material types including powders, granules, flakes, and semi-solid substances.

Multiple industries depend on screw conveyors for critical material handling applicat...
Industrial bulk material handling screw conveyors represent one of the most efficient and versatile material transport solutions available for modern industrial operations. These systems utilize a rotating helical screw blade within a tube or trough to move materials precisely from intake to discharge points. Engineered for reliability and durability, our screw conveyors feature robust construction with customizable options to match specific material characteristics and operational requirements. The enclosed design prevents environmental contamination while protecting materials from external elements, making them suitable for even the most demanding processing environments. With capacities ranging from small batch operations to high-volume continuous processing, these conveyors provide consistent performance across various material types including powders, granules, flakes, and semi-solid substances.

Multiple industries depend on screw conveyors for critical material handling applications. In food processing, they transport ingredients while meeting strict hygiene standards with food-grade materials and easy-clean designs. Agricultural operations utilize them for moving grains, feed, and fertilizers with minimal product degradation. Chemical plants employ corrosion-resistant models for handling powders and compounds, while construction material producers rely on heavy-duty versions for cement, sand, and aggregate transportation. Pharmaceutical manufacturers benefit from precision-engineered conveyors that maintain product purity, and wastewater treatment facilities use them for sludge handling. The mining sector utilizes abrasion-resistant designs for mineral ores and processing materials.

Businesses select our screw conveyors for their proven reliability and significant operational value. These systems reduce labor costs by automating material transfer while minimizing product loss through enclosed transportation. The low maintenance requirements and simple design translate to reduced downtime and longer service life, delivering strong return on investment. Customization options ensure perfect integration with existing production lines, while robust construction materials withstand harsh operating conditions. These conveyors enhance workplace safety by containing materials within enclosed systems, reducing dust emissions and contamination risks. Their energy-efficient operation and space-saving designs further contribute to operational cost reductions while improving overall processing efficiency.

Key Features:
- Heavy-duty construction with customizable lengths and diameters
- Enclosed trough design prevents material spillage and contamination
- Multiple mounting options including horizontal, inclined, and vertical configurations
- Variety of material options including carbon steel, stainless steel, and abrasion-resistant alloys
- Tailored flight designs including ribbon, cut, and folded options for different materials

Benefits:
- Reduced labor costs through automated material transfer systems
- Minimal product loss with enclosed transportation design
- Low maintenance requirements and reduced operational downtime
- Enhanced workplace safety with contained material handling
- Energy-efficient operation with space-saving compact designs
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Screw conveyors efficiently move bulk materials horizontally, vertically, or at inclined angles within industrial operations. Their enclosed design prevents material spillage and contamination, making them ideal for handling powders, granules, and semi-solid materials across diverse processing environments. These systems operate reliably under continuous heavy-duty conditions while maintaining consistent flow rates with minimal maintenance requirements.
These conveyors serve critical roles in industries requiring precise material transfer including food processing, pharmaceuticals, agriculture, chemicals, and construction. Their versatility allows customization of length, diameter, and construction materials to handle specific products from fragile food grains to abrasive industrial minerals. The robust design ensures long service life even when handling hot, corrosive, or hazardous materials with proper specification.
- Transporting grains, flour, and ingredients in food processing facilities
- Moving cement, sand, and aggregates in construction material production
- Handling fertilizers, animal feed, and agricultural products in farming operations
- Transferring plastic pellets, powders, and compounds in manufacturing plants
- Conveying wastewater treatment sludge and municipal solid waste in processing facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Alta Vista, Tamil Nadu
 Tamil Nadu, India
Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Bulk Material Handling Screw Conveyors For Efficient Transport
Industrial bulk material handling screw conveyors provide reliable transport for powders, granules, and materials. These customizable systems ensure seamless production line integration with enhanced productivity and cost-effective solutions for various industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Alta Vista
 Tamil Nadu, India
Manufacturer