IN
₹
Apparel & Fashion

Description
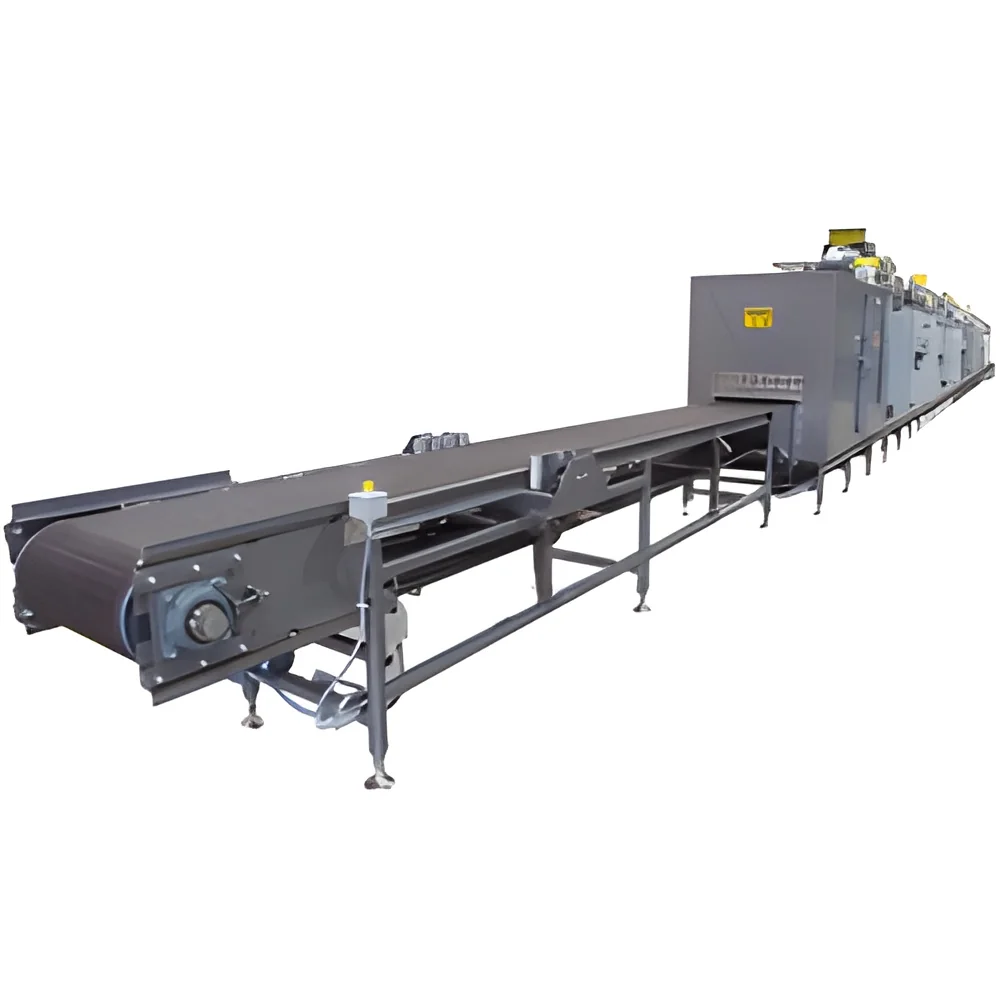
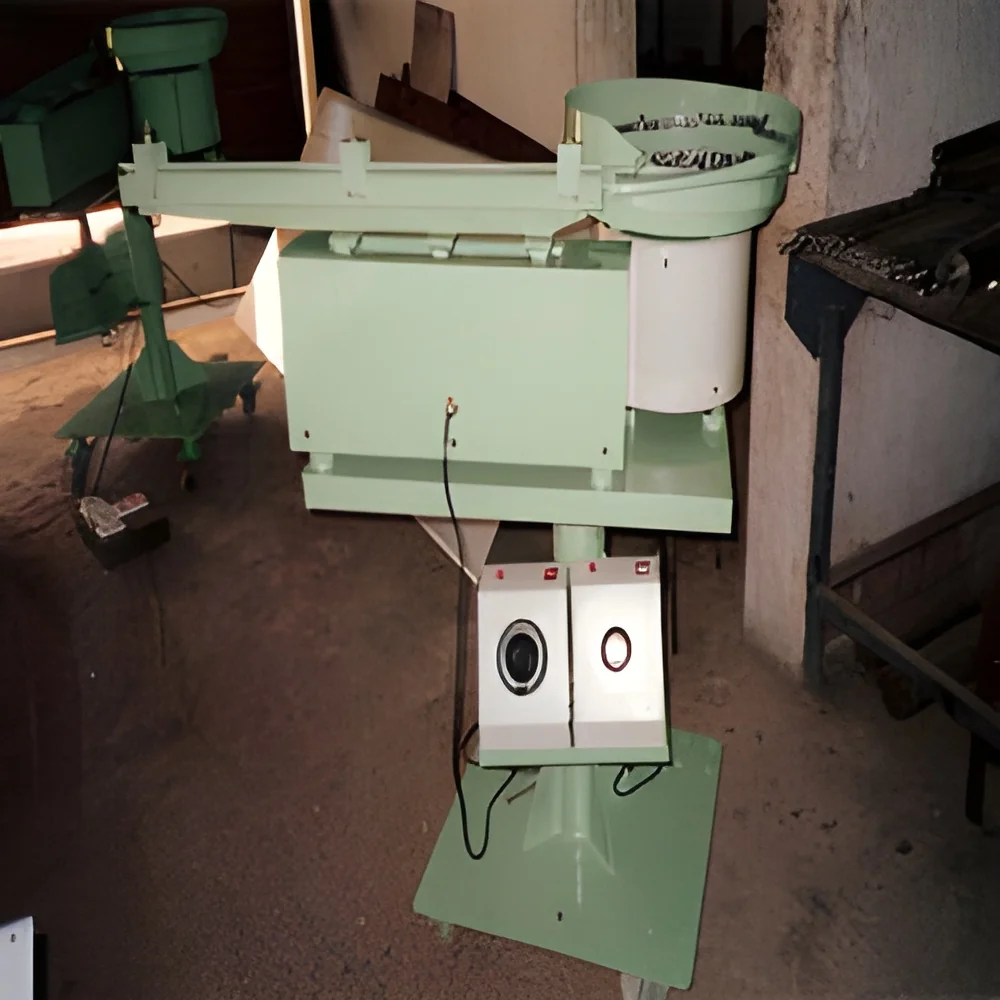
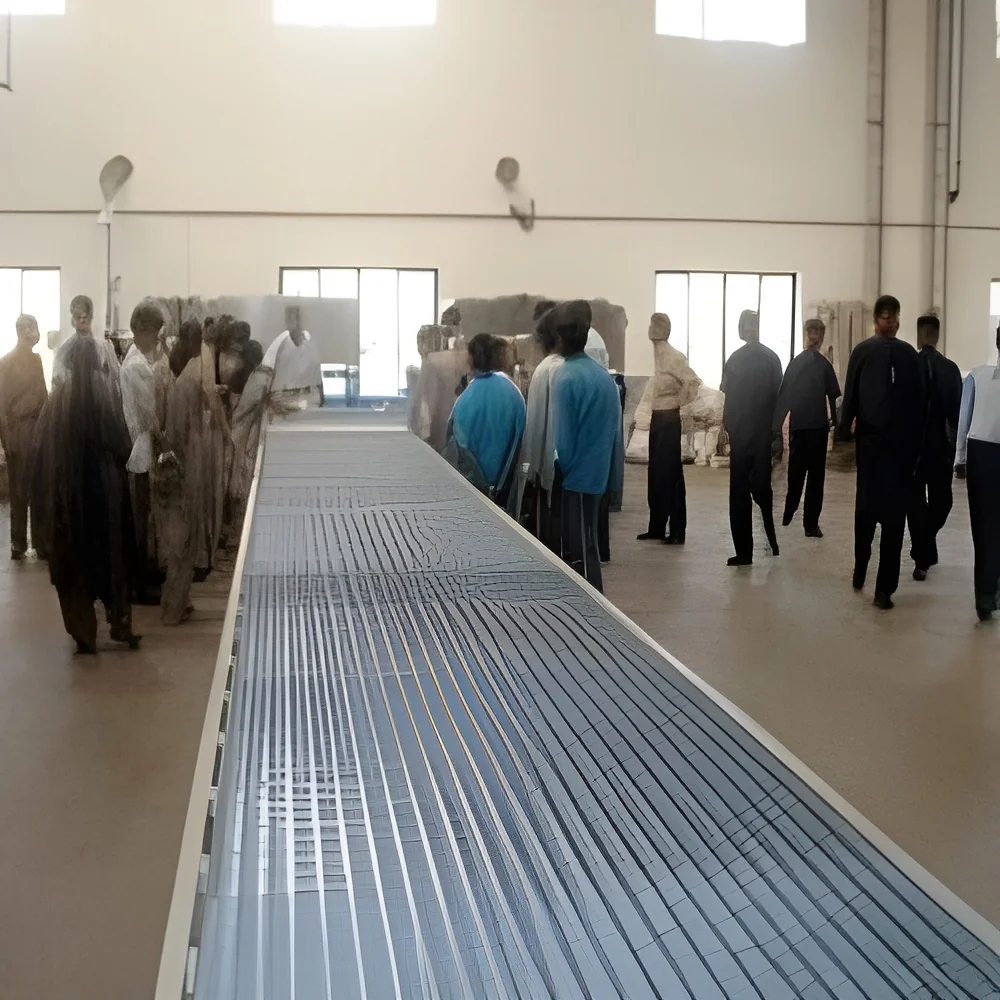
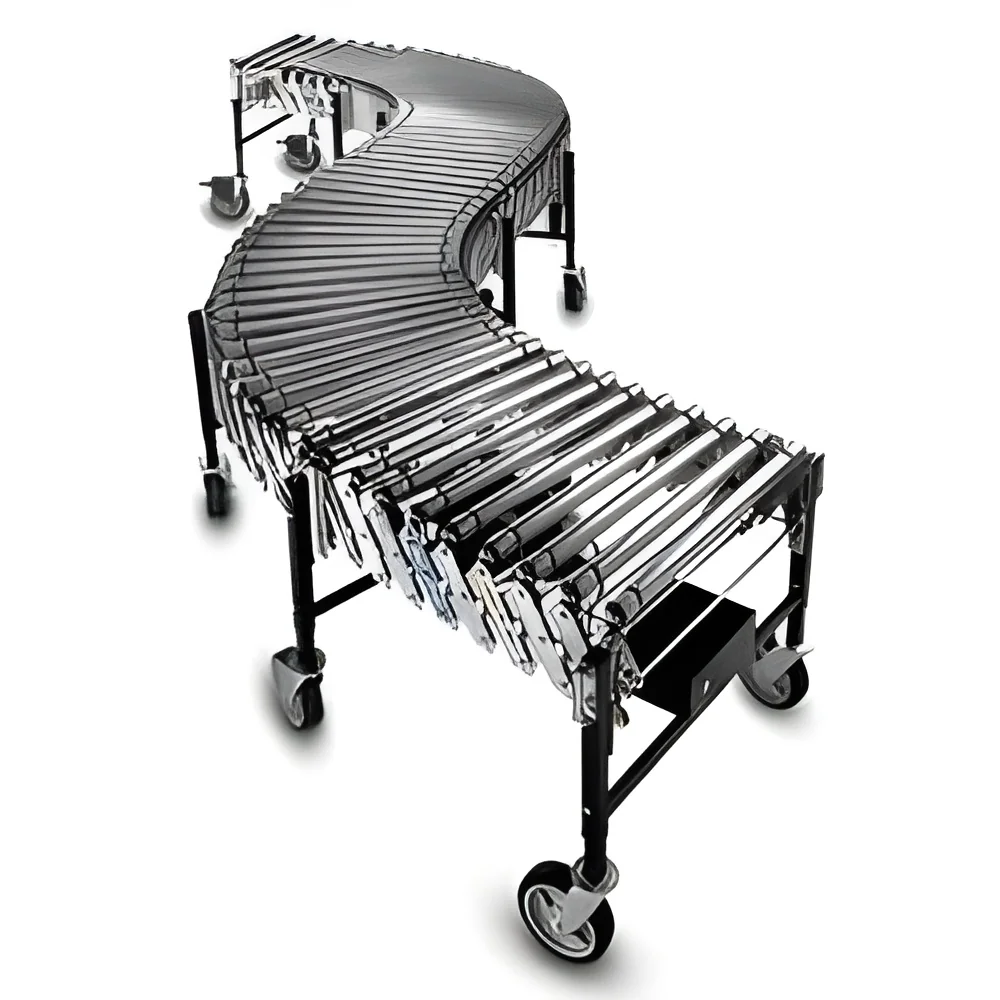
Industrial infeed conveyor systems deliver reliable material handling solutions designed for modern production environments. These conveyors serve as critical links between different manufacturing stages, ensuring continuous material flow into processing, packaging, and assembly operations. Engineered for precision and durability, they accommodate diverse product types, weights, and dimensions while maintaining consistent performance. The systems feature robust construction and are designed for straightforward integration with existing equipment, making them suitable for both new installations and facility upgrades. Their reliable design ensures long-term operation with minimal maintenance requirements.

These conveyor systems serve multiple industries including food processing, pharmaceutical manufacturing, packaging operations, automotive production, and logistics centers. Food processing plants utilize them for handling raw ingredients and packaged goods with hygienic design conside...
Industrial infeed conveyor systems deliver reliable material handling solutions designed for modern production environments. These conveyors serve as critical links between different manufacturing stages, ensuring continuous material flow into processing, packaging, and assembly operations. Engineered for precision and durability, they accommodate diverse product types, weights, and dimensions while maintaining consistent performance. The systems feature robust construction and are designed for straightforward integration with existing equipment, making them suitable for both new installations and facility upgrades. Their reliable design ensures long-term operation with minimal maintenance requirements.

These conveyor systems serve multiple industries including food processing, pharmaceutical manufacturing, packaging operations, automotive production, and logistics centers. Food processing plants utilize them for handling raw ingredients and packaged goods with hygienic design considerations. Pharmaceutical manufacturers depend on them for precise handling of sensitive products under controlled conditions. Packaging operations rely on infeed conveyors to maintain continuous material flow to wrapping, sealing, and labeling equipment. The automotive sector uses them for supplying components to assembly lines, while distribution centers integrate them into sortation systems for efficient order processing and fulfillment.

The operational value of our infeed conveyors lies in their ability to enhance efficiency, reduce labor requirements, and minimize production interruptions. These systems provide dependable performance that manufacturers trust for continuous operation, decreasing the risk of production stoppages and associated costs. The reliable construction ensures each conveyor solution matches specific operational needs, delivering maximum return on investment. With durable materials and quality components, these conveyors offer extended service life and minimal maintenance demands. Their seamless integration capabilities allow businesses to implement them without significant disruption to existing operations, while improved material flow contributes to overall productivity gains and operational consistency.

Key Features:
- Robust construction using durable materials for long-term reliability
- Customizable dimensions including length, width, and height specifications
- Smooth belt surface design for gentle product handling and minimal damage
- Easy integration capability with existing packaging and processing machinery
- Precision speed control for synchronized operation with downstream equipment

Benefits:
- Enhanced operational efficiency through continuous material flow
- Reduced labor costs by automating manual handling processes
- Minimized production downtime with reliable performance
- Long service life with minimal maintenance requirements
- Improved productivity through consistent material handling operations
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial infeed conveyor systems efficiently transport raw materials, components, and finished goods into production and packaging machinery. They ensure consistent flow rates while reducing manual handling and eliminating bottlenecks in automated operations. These systems handle various items including boxes, containers, ingredients, and assembly parts with precision and care.
These conveyors integrate seamlessly with labeling equipment, filling machines, sealing systems, and sortation units. They support high-speed operations while maintaining proper product orientation and spacing throughout the process. The systems are essential in environments requiring hygienic design, gentle handling capabilities, or specific timing for downstream processing stages.
- Feeding products into packaging machinery for boxing, wrapping, and sealing operations
- Moving raw materials into processing equipment within food and beverage facilities
- Supplying components to assembly stations in manufacturing and automotive plants
- Transporting items to labeling, coding, and quality inspection systems
- Integrating with sortation systems in distribution centers and fulfillment operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Sai Systems, Karnataka
 Karnataka, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Infeed Conveyor Systems For Material Handling
Industrial infeed conveyor systems provide reliable material handling for packaging, food processing, and manufacturing industries with smooth production line integration and consistent performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Sai Systems
 Karnataka, India
Industrial Equipment & MachineryManufacturer