What are Bucket Elevators?
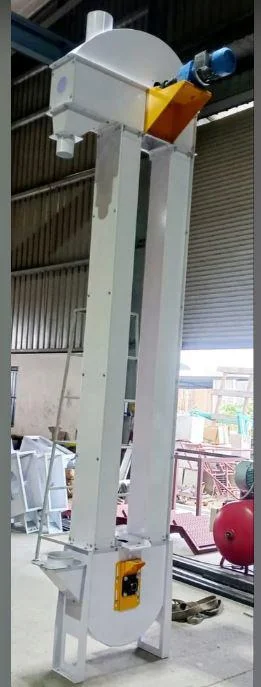
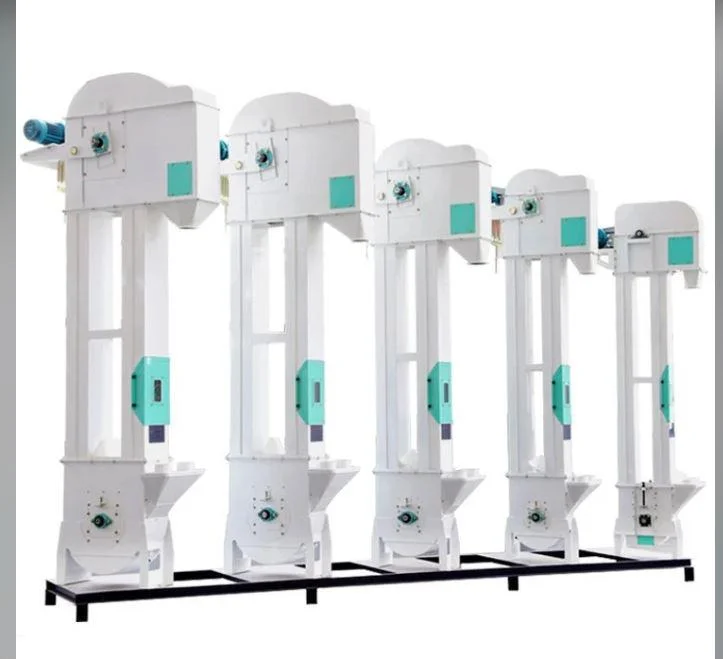
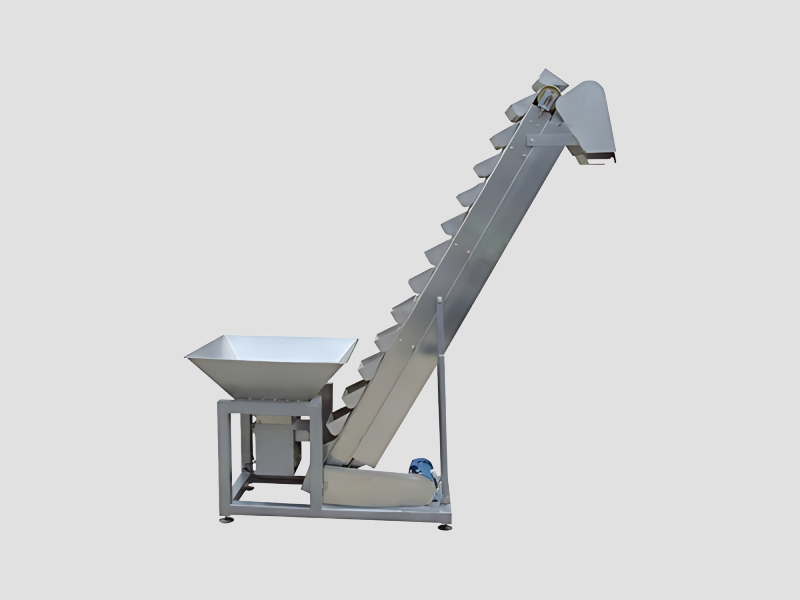
Bucket elevators are mechanical devices used for vertical lifting of bulk materials. They consist of a series of buckets attached to a belt or chain that moves in a loop, allowing for the efficient transport of materials to various heights. The buckets scoop up the material from a lower level and discharge it at a higher level, making them a crucial component in many industrial operations.
These elevators are primarily used in industries that handle bulk materials such as agriculture, mining, and manufacturing. Common applications include transporting grains, coal, fertilizers, and various other materials. Their ability to move materials vertically minimizes the footprint required for operations and enhances overall efficiency. In a competitive market, bucket elevators play a vital role in improving productivity and facilitating the smooth operation of many businesses.
Key Features and Specifications
Bucket elevators are designed with several key features that enhance their performance and reliability. Understanding these specifications can help businesses select the right equipment for their needs.
Key specifications include:
1. Capacity
- The capacity of bucket elevators can range from a few tons per hour to several hundred tons per hour, depending on the model and application.
2. Lift Height
- Standard lift heights can vary significantly, often reaching up to 60 feet or more, allowing for flexibility in installation.
3. Bucket Size
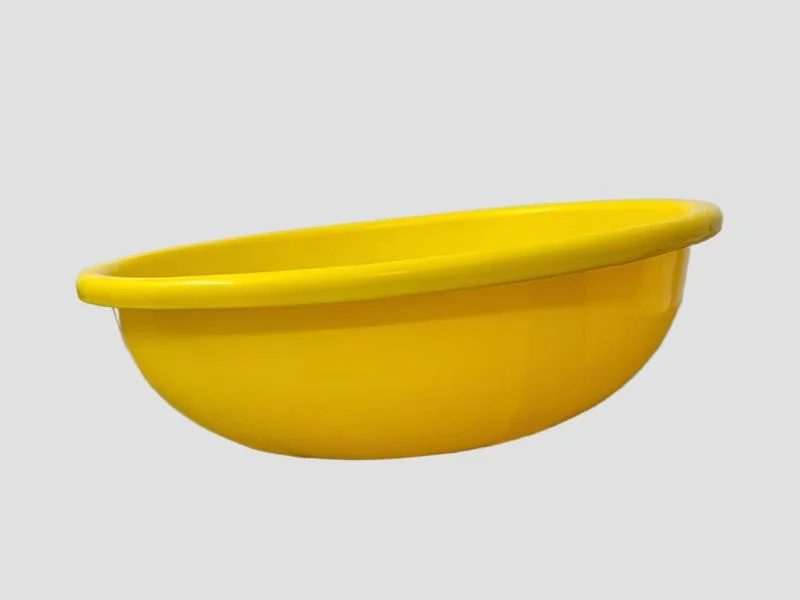
- Buckets are available in various sizes, typically ranging from 0.5 liters to over 100 liters, depending on the material being handled.
4. Material of Construction
- Buckets and components can be made from materials such as plastic, steel, or stainless steel to suit different environments and materials.
5. Drive System
- Bucket elevators can be equipped with different drive systems, including electric motors, to ensure reliable operation.
6. Speed
- The speed of the elevator typically ranges from 30 to 100 feet per minute, which can be adjusted depending on the application.
7. Chain or Belt Type
- Bucket elevators can use either chains or belts for movement, with each type having its own advantages in terms of durability and maintenance.
8. Customization Options
- Many manufacturers offer customization options to meet specific operational requirements, including special coating and bucket designs.
In summary, the key features and specifications of bucket elevators highlight their versatility and adaptability for various industrial applications.
Common Applications and Use Cases
Bucket elevators are employed across multiple industries due to their efficient material handling capabilities.
1. Agriculture: In the agricultural sector, bucket elevators are commonly used to transport grains, seeds, and fertilizers, ensuring proper handling and storage.
2. Mining: Mining operations utilize bucket elevators to move bulk materials like coal, ores, and aggregates from lower levels to processing areas.
3. Food Processing: In food processing plants, these elevators help in the movement of bulk ingredients, such as sugar, flour, and feed, while adhering to hygiene regulations.
4. Chemical Industry: The chemical industry uses bucket elevators for transporting various powders and granules, ensuring efficient production flows.
5. Plastics and Polymers: In this sector, bucket elevators move plastic pellets and resins, facilitating smooth operations in manufacturing processes.
6. Cement Industry: Bucket elevators efficiently handle cement and other related materials, contributing to the overall production and logistics of cement plants.
7. Recycling: In recycling facilities, bucket elevators are vital for transporting shredded materials, contributing to effective waste management processes.
Product Variants and Subcategories
Bucket elevators come in various designs and configurations to suit different operational needs.
Heavy-Duty Bucket Elevators
These variants are designed for handling abrasive or heavy materials. They feature robust construction and enhanced durability, making them suitable for mining and heavy industrial applications.
Modular Bucket Elevators
Modular designs allow for flexible configurations and easy installation. These elevators are perfect for facilities that require frequent changes in layout or material handling processes.
Continuous Bucket Elevators
These elevators operate on a continuous basis, allowing for the efficient handling of bulk materials without interruption. They are ideal for applications with high throughput demands.
High-Temperature Bucket Elevators
Designed to withstand extreme temperatures, these elevators are suitable for industries such as cement and metal processing, where high heat is a factor.
Benefits and Advantages
Bucket elevators offer numerous advantages that enhance operational efficiency in various industries.
1. Space Efficiency: By moving materials vertically, bucket elevators minimize the floor space required for material handling.
2. High Capacity: Their ability to transport large volumes of material quickly makes them ideal for high-demand environments.
3. Versatility: Bucket elevators can be designed to handle a wide range of materials, from powders to large bulk items.
4. Low Maintenance: With proper installation and regular maintenance, bucket elevators typically have a long service life and require minimal upkeep.
5. Customization: Many models can be tailored to specific operational needs, ensuring optimal performance for unique applications.
6. Safety Features: Modern bucket elevators incorporate safety features to protect operators and reduce the risk of accidents in the workplace.
Buying Guide for B2B Buyers
When sourcing bucket elevators, it is essential to consider several key factors to ensure the right choice for your business needs.
1. Quality Assessment: Evaluate the quality of materials and construction. Look for manufacturers that adhere to industry standards and offer warranties to ensure reliability.
2. Supplier Verification: Conduct thorough research on suppliers to verify their reputation and reliability. Check for certifications and customer reviews to gauge their performance.
3. Pricing and MOQ: Compare pricing strategies and minimum order quantities across different suppliers. Understanding the cost structure can help in budgeting and negotiations.
4. Delivery and Lead Times: Inquire about delivery schedules and lead times to ensure that your operations are not disrupted. Timely delivery is crucial for project management.
5. Compliance Requirements: Ensure that the bucket elevators meet all relevant regulatory and safety standards, especially if operating in highly regulated industries.
Compliance and Certifications
Bucket elevators must adhere to various compliance and certification standards to ensure safety and quality. Common quality standards include ISO 9001, which outlines requirements for a quality management system, ensuring consistent product quality and customer satisfaction.
Industry certifications such as CE mark demonstrate compliance with European safety standards, confirming that the equipment meets essential health and safety requirements.
In addition to quality and safety certifications, bucket elevators are often subject to rigorous testing to ensure they can handle specific loads and operate efficiently under various conditions. Regional compliance considerations may vary, so it is essential to consult local regulations to ensure adherence.
Why Source Bucket Elevators from Pepagora?
Pepagora provides a trusted platform for sourcing bucket elevators with several key advantages.
Verified Supplier Network: The platform ensures that all suppliers are thoroughly vetted, providing buyers with access to reliable manufacturers and suppliers in the industry.
Streamlined RFQ Process: Pepagora offers a straightforward request for quotation process, allowing buyers to easily compare prices and specifications from multiple suppliers.
Trade Assurance and Support: Buyers receive protection through trade assurance programs, ensuring that purchases meet agreed standards and timelines.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora offers extensive geographic reach, connecting buyers to suppliers across various regions for their bucket elevator needs.

 IN


 India