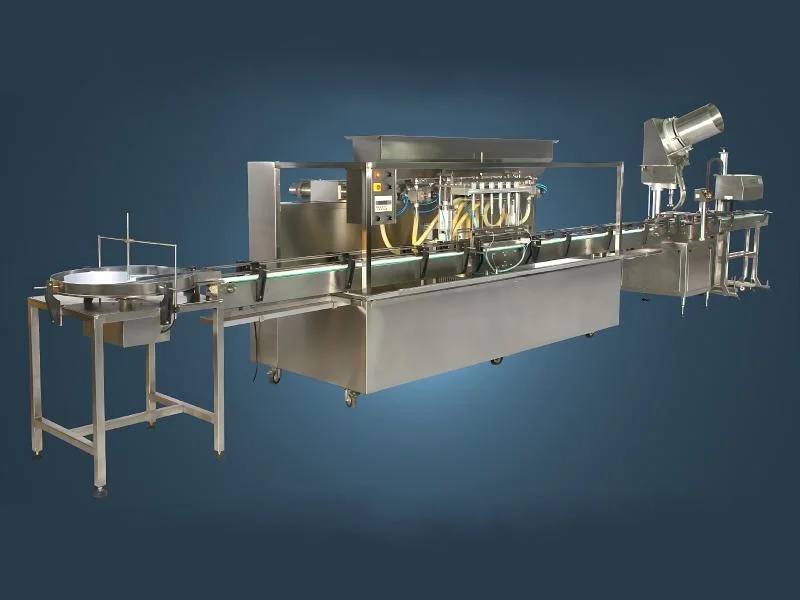
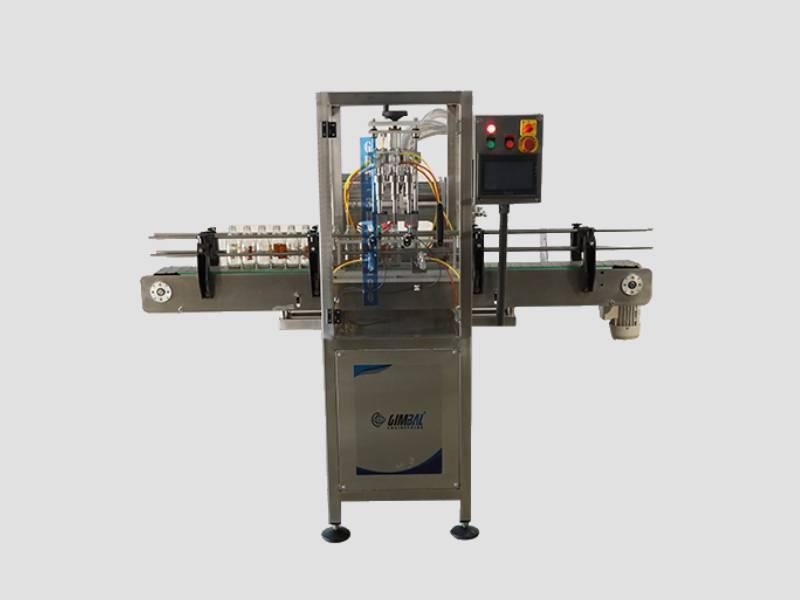
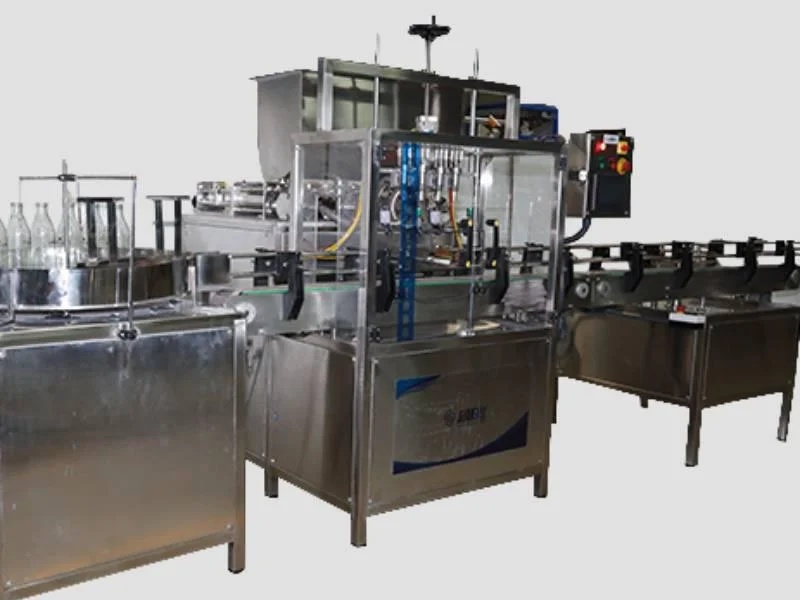
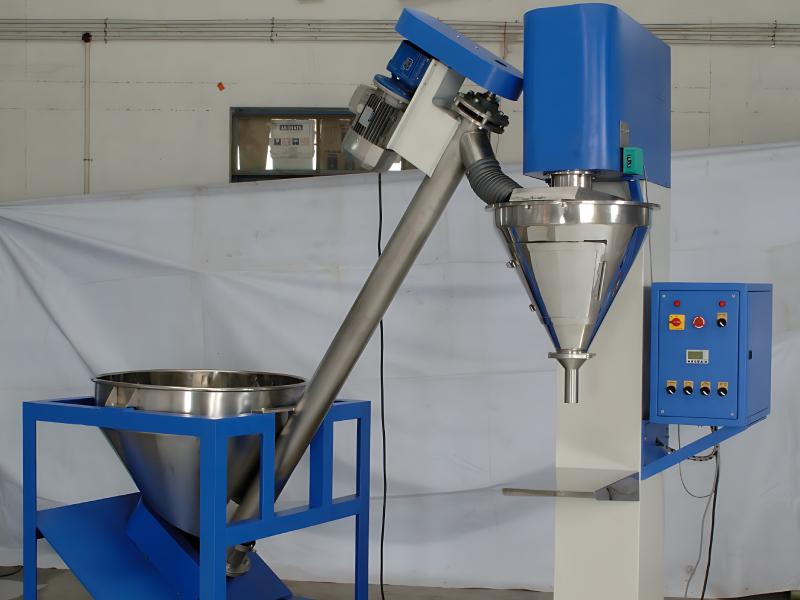
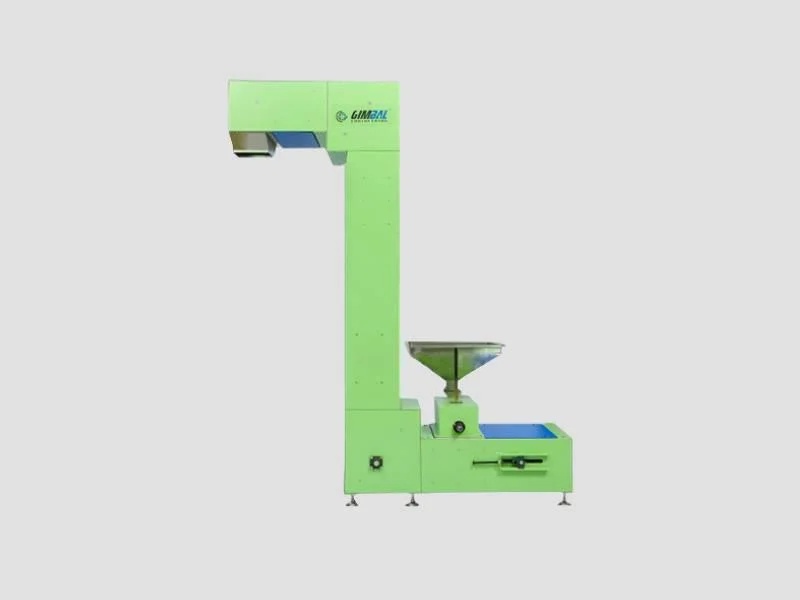
The Bucket Conveyor is an essential component in material handling systems designed for a variety of industrial applications. With a capacity of 25.75 TPH and a conveyor length of 13.25 m, it efficiently transports bulk materials while ensuring durability with its metal construction and hydraulic drive system. • Used extensively in manufacturing facilities • Ideal for logistics operations requiring bulk material transport • Commonly utilized in warehouses and distribution centers The design adheres to CE certifications, ensuring compliance with safety standards applicable across various operational environments. Its reliability makes it suitable for businesses focusing on efficient supply chain management.

 IN
₹
Apparel & Fashion
Description
The Bucket Conveyor, a specialized type of Bucket Elevator, is engineered for efficient and reliable material handling across various industrial applications. With its robust design and advanced hydraulic drive system, this conveyor ensures smooth operation even under demanding conditions. • Capacity: Handles up to 25.75 TPH, making it ideal for high-volume operations. • Length: Measures 13.25 m in total length, providing ample reach for various setups. • Construction: Crafted from durable metal to withstand heavy usage while ensuring longevity. • Certifications: CE certified to meet European safety standards. This Bucket Conveyor is suitable for industries such as manufacturing, logistics, and construction where effective material transport is critical. Its robust features make it a valuable addition to any procurement strategy looking to optimize operational efficiency.
Specifications
| Key Attributes | |
|---|---|
| Capacity (TPH | 25.75 TPH |
| Conveyor Length (m | 13.25 m |
| Material Type | Metal |
| Certifications | CE |
| Drive System Type | Hydraulic Drive |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Company Profile
Gimbal Engineering, Tamil Nadu
 Tamil Nadu, India
20 yrs
Manufacturer
Turn Over
₹25 Lakhs – ₹1 Crore
Factory Details
Factory Size1000-5000 sqm
Main Markets
North America
Mid East
Western Europe
Bucket Conveyor
Bucket Conveyor, a type of Bucket Elevator, is designed for efficient material handling. It has a capacity of 25.75 TPH and a conveyor length of 13.25 m. The construction is metal, and it features a hydraulic drive system. This product is commonly sourced by businesses involved in manufacturing, logistics, and material handling.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Gimbal Engineering
 Tamil Nadu, India
Manufacturer