What are Snack Food Packaging Machines?
Snack Food Packaging Machines are specialized equipment designed to package a variety of snack foods efficiently and effectively. These machines automate the packaging process, ensuring that products are sealed, protected, and ready for distribution. They can handle a range of packaging types including bags, pouches, and boxes, allowing manufacturers to meet diverse consumer needs.
These machines are primarily used in the food processing industry, where speed and accuracy are critical. They are essential for businesses that produce chips, popcorn, nuts, granola bars, and other snack items. By employing advanced technology, these machines help maintain product freshness, extend shelf life, and reduce labor costs. The growing demand for packaged snacks drives the need for efficient packaging solutions, making these machines increasingly relevant in today’s market.
As the snack food industry continues to expand, the importance of reliable packaging solutions cannot be overstated. The market for snack food packaging machines is evolving, with trends leaning towards automation, sustainability, and customization. Manufacturers are looking for machines that not only meet their production demands but also align with consumer preferences for eco-friendly packaging.
Key Features and Specifications
Snack Food Packaging Machines boast a variety of features that enhance their effectiveness and usability. When selecting a machine, it is important to consider specifications that align with your production needs.
Key specifications include:
1. Speed
- Machines can operate at speeds ranging from 30 to 100 packages per minute depending on the model.
2. Package Size Compatibility
- Capable of handling various sizes, typically from 50 grams to several kilograms.
3. Sealing Type
- Options for heat sealing, vacuum sealing, or nitrogen flushing to preserve freshness.
4. Control System
- Equipped with user-friendly interfaces, often featuring digital displays for easy monitoring.
5. Material Compatibility
- Suitable for various packaging materials such as plastic, foil, and paper.
6. Maintenance Requirements
- Designed for easy cleaning and maintenance to minimize downtime.
7. Energy Consumption
- Efficient machines that comply with energy-saving standards, typically consuming between 1 to 3 kW.
8. Customization Options
- Ability to customize machine settings for different snack types and packaging requirements.
These specifications help businesses select the right equipment to optimize their production processes and meet market demands.
Common Applications and Use Cases
Snack Food Packaging Machines serve a wide array of industries, showcasing their versatility and necessity.
1. Food Manufacturing: These machines are essential for companies producing chips, pretzels, and other snack foods, ensuring products are packaged quickly and securely.
2. Confectionery: Producers of candy and chocolate-covered snacks utilize these machines to maintain product integrity and freshness during packaging.
3. Health Foods: Manufacturers of granola bars and protein snacks rely on advanced packaging solutions to cater to health-conscious consumers seeking convenient on-the-go options.
4. Pet Food: The pet food industry also benefits from snack packaging machines, enabling efficient packaging of treats and kibble.
5. Frozen Foods: Some machines are designed to package frozen snack items, ensuring they are sealed in a way that preserves quality during storage.
6. Retail Packaging: Retailers often use these machines to package bulk snack items into consumer-friendly sizes for display.
7. Organic Products: As organic snacks gain popularity, packaging machines help maintain the integrity and shelf life of these products.
Product Variants and Subcategories
Snack Food Packaging Machines come in various forms to cater to different industry needs.
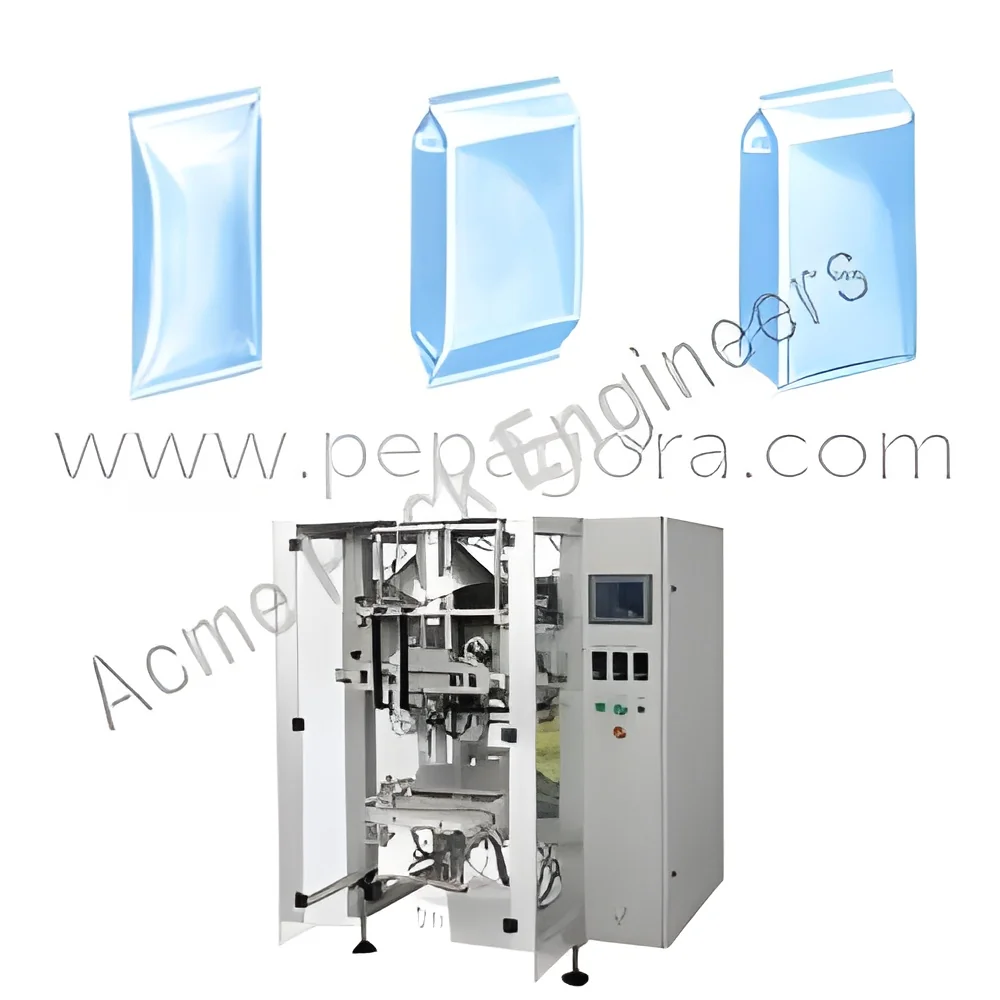
Vertical Form Fill Seal Machines: These machines create pouches from a roll of film, fill them with snacks, and seal them, making them ideal for high-volume production lines.
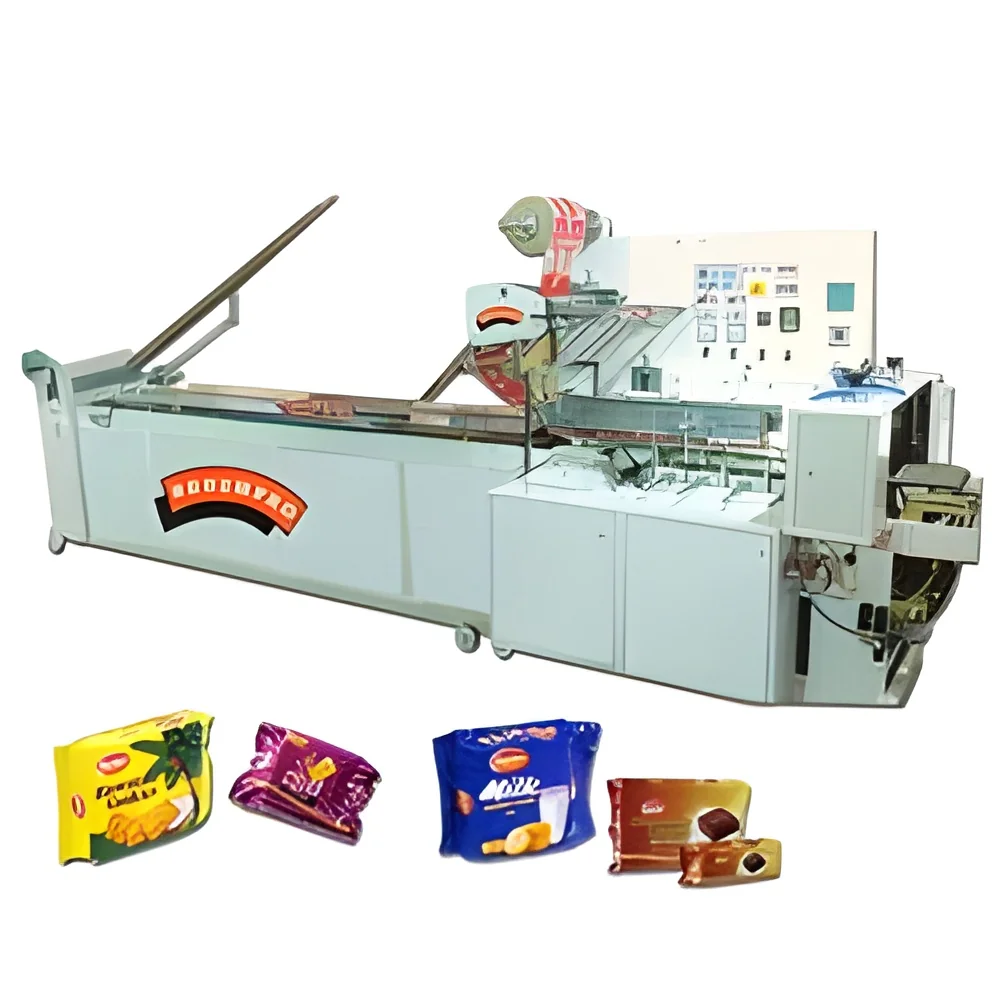
Horizontal Flow Wrap Machines: Suitable for individually wrapped snacks, these machines package products in a continuous flow, ensuring quick and efficient operation.
Multi-Head Weighers: Often used in conjunction with packaging machines, these devices accurately weigh snacks before packaging, improving precision and reducing waste.
Automatic Pouch Fillers: Designed for pre-made pouches, these machines fill and seal packages quickly, perfect for small to medium-sized production runs.
Benefits and Advantages
Investing in Snack Food Packaging Machines offers numerous advantages for businesses in the snack food industry.
Key benefits include:
1. Increased Efficiency: Automating the packaging process significantly reduces labor costs and speeds up production.
2. Improved Product Freshness: Advanced sealing technologies help extend the shelf life of snacks, keeping them fresher for longer.
3. Enhanced Consistency: Automated machines ensure uniform packaging, which improves product presentation and consumer trust.
4. Flexibility: Many machines can handle various snack types and packaging formats, adapting to changing production needs.
5. Reduced Material Waste: Efficient packaging processes minimize excess material use, contributing to cost savings and sustainability.
6. Compliance with Industry Standards: Many machines meet rigorous safety and quality standards, ensuring businesses adhere to regulatory requirements.
Buying Guide for B2B Buyers
When sourcing Snack Food Packaging Machines, it is crucial to consider several factors to ensure a successful purchase.
1. Quality Assessment: Evaluate machines based on build quality, durability, and performance history. Consider brands with a proven track record in the industry.
2. Supplier Verification: Research potential suppliers to confirm their reputation and reliability. Look for reviews and testimonials from other businesses.
3. Pricing and MOQ: Understand the price range and minimum order quantities. Ensure they fit within your budget and production needs.
4. Delivery and Lead Times: Inquire about shipping options and lead times to ensure timely delivery. Assess the supplier’s ability to meet your production schedule.
5. Compliance Requirements: Ensure the machines comply with relevant regulations and certifications. This includes safety standards and food safety requirements applicable in your region.
Compliance and Certifications
Snack Food Packaging Machines must adhere to various quality standards and certifications to ensure safety and reliability in the food industry.
ISO 9001 certification is essential, as it guarantees that the machinery is manufactured under a quality management system. This standard ensures consistent quality and improvement in processes.
HACCP, or Hazard Analysis and Critical Control Points, is crucial for food safety. Machines designed with HACCP principles help prevent contamination and ensure safe food handling.
CE certification indicates that the machines comply with European safety and health regulations, which is important for businesses exporting to Europe.
Safety and testing requirements are also integral, ensuring that machines operate safely and efficiently without posing risks to operators.
Regional compliance considerations vary widely. Buyers should be aware of local regulations and standards that may affect machine selection and operation.
Why Source Snack Food Packaging Machines from Pepagora?
Pepagora provides an excellent platform for sourcing Snack Food Packaging Machines, offering several key advantages that enhance the buying experience.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers. This ensures that businesses can trust the quality and reliability of the machines they purchase.
Streamlined RFQ Process: The Request for Quotation system simplifies the process for buyers to receive competitive quotes. This enables informed decision-making based on clear pricing and specifications.
Trade Assurance and Support: Pepagora offers buyer protection through trade assurance, ensuring that transactions are secure and that buyers receive the support they need throughout the purchasing process.
Regional Coverage: With a strong presence in India, GCC, and Southeast Asia, Pepagora provides access to a broad market, enabling businesses to find suitable packaging solutions tailored to their specific regional needs.

 IN