
 IN
Dust Collection Units
2 products available
What are Dust Collection Units?
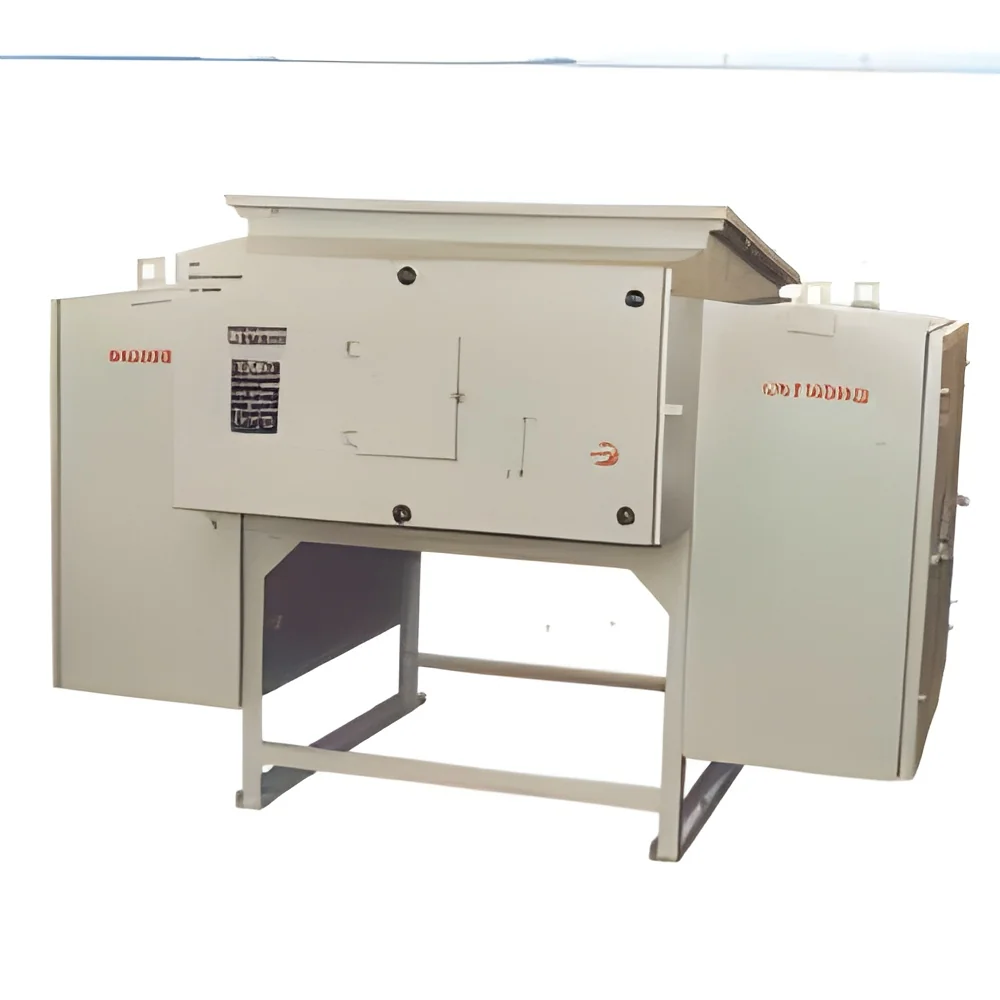
Dust Collection Units are specialized systems designed to capture and filter airborne particulate matter generated during various industrial processes. These units play a crucial role in maintaining air quality and ensuring a safe working environment by removing dust, debris, and other contaminants from the air. They operate by drawing in contaminated air through a network of ducts, where it is then filtered and cleaned before being released back into the environment.
These units are widely used across multiple industries, including woodworking, metalworking, pharmaceuticals, and food processing. In these sectors, dust collection is essential not only for compliance with health and safety regulations but also for protecting machinery and improving overall operational efficiency. The relevance of dust collection systems has grown with increasing awareness of workplace safety and environmental standards, making them a vital investment for businesses looking to enhance their production processes while safeguarding employee health.
Key Features and Specifications
Dust Collection Units come with a range of features designed to enhance their performance and efficiency. Understanding these specifications is crucial for selecting the right unit for specific industrial needs.
Key specifications include:
1. Filtration Efficiency
- High-efficiency particulate air (HEPA) filters can capture up to 99.97% of particles as small as 0.3 microns.
2. Airflow Capacity
- Measured in cubic feet per minute (CFM), airflow capacities typically range from 500 to 10,000 CFM, depending on the application.
3. Noise Level
- Noise output generally ranges between 60 to 85 decibels, ensuring compliance with workplace noise regulations.
4. Power Consumption
- Units typically operate on standard voltage, with power requirements ranging from 1 HP to 15 HP.
5. Collection Bin Size
- Bin capacities vary from 30 to 200 gallons, accommodating different dust volumes and minimizing frequent emptying.
6. Filter Cleaning System
- Automatic or manual cleaning systems are available, enhancing maintenance efficiency.
7. Dimensions
- Units come in various sizes, with widths ranging from 24 inches to over 60 inches.
8. Mobility Options
- Many units offer portability features, such as wheels or mobile bases for easy relocation.
In summary, selecting a Dust Collection Unit involves considering various technical specifications that align with specific operational requirements.
Common Applications and Use Cases
Dust Collection Units are integral to several industries, ensuring a clean and safe working environment.
1. Woodworking: In woodworking shops, these units efficiently capture sawdust and wood shavings, preventing respiratory issues among workers and maintaining equipment cleanliness.
2. Metalworking: Metal fabrication facilities utilize dust collection systems to manage metal shavings and particles, which can pose fire hazards and affect production quality.
3. Pharmaceutical: In pharmaceutical manufacturing, dust collection is critical for maintaining sterile environments and ensuring compliance with health regulations.
4. Food Processing: These units help in controlling flour and spice dust, which can compromise product quality and worker safety.
5. Construction: On construction sites, dust collection systems mitigate the risks associated with silica dust and other hazardous materials.
6. Chemical Processing: Dust collection is essential for capturing harmful chemical particulates, ensuring worker safety and regulatory compliance.
7. Textile Manufacturing: In textile production, these units manage lint and fabric dust, protecting both workers and machinery.
Product Variants and Subcategories
Dust Collection Units come in various designs to meet different industrial needs and preferences.
Portable Dust Collectors
These units are compact and designed for mobility, making them ideal for smaller workshops or job sites. They can be easily moved to different locations as needed, offering flexibility in operation.
Centralized Dust Collection Systems
These systems are designed for larger facilities, featuring a network of ducts that connect multiple machines to a central dust collection unit. This setup provides efficient dust management across extensive production areas.
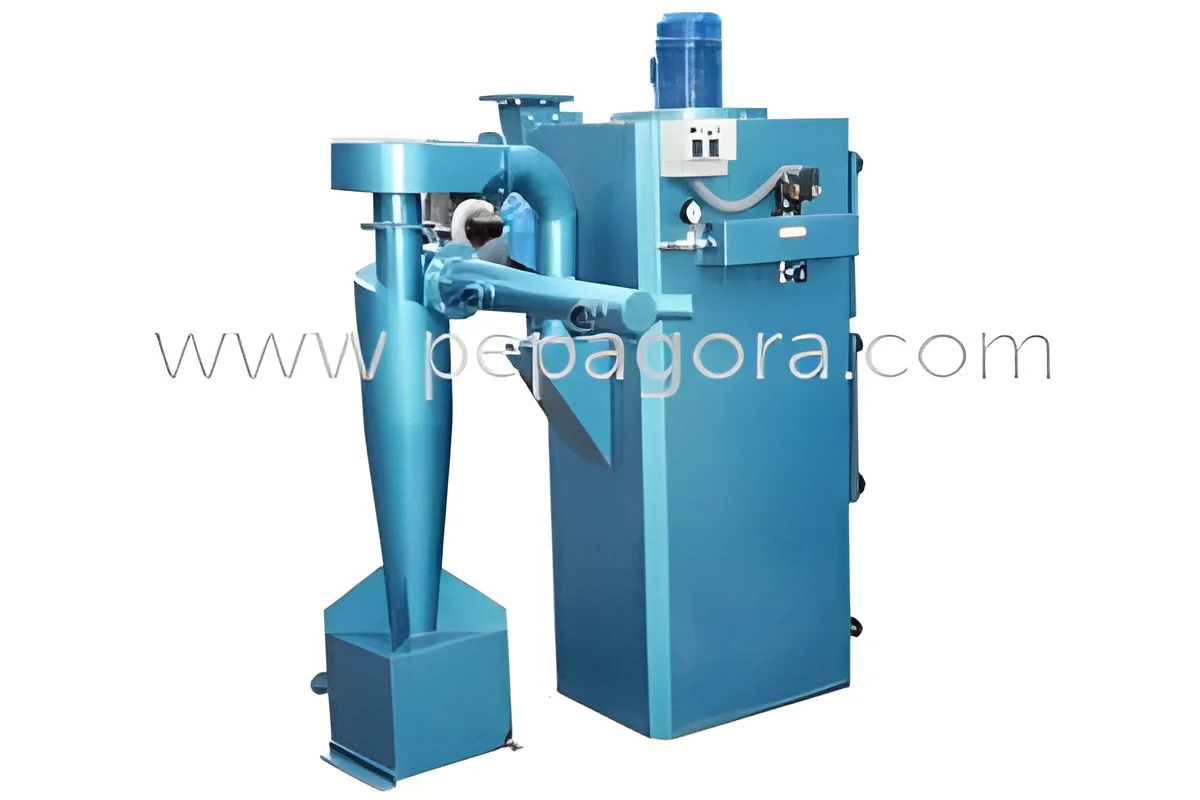
Cyclone Dust Collectors
Cyclone units utilize centrifugal force to separate larger particles from the airflow, reducing the load on filters and extending their lifespan. They are ideal for heavy-duty applications with high dust volumes.
Baghouse Dust Collectors
These systems use fabric bags for filtration, suitable for applications generating fine dust. They are often employed in industries like cement and mining.
Benefits and Advantages
Dust Collection Units provide numerous benefits that enhance workplace safety and operational efficiency.
1. Improved Air Quality: These units significantly reduce airborne dust levels, promoting a healthier work environment for employees.
2. Enhanced Equipment Longevity: By capturing dust and debris, these systems help protect machinery from wear and tear, reducing maintenance costs.
3. Regulatory Compliance: Using dust collection systems ensures adherence to occupational safety standards and environmental regulations.
4. Increased Productivity: Cleaner working conditions lead to fewer disruptions and enhanced focus among workers, improving overall productivity.
5. Customization Options: Many systems can be tailored to specific operational needs, providing flexibility in design and functionality.
6. Energy Efficiency: Modern units are designed to minimize energy consumption while maximizing airflow, providing cost savings on electricity bills.
Buying Guide for B2B Buyers
When sourcing Dust Collection Units, several factors should be carefully considered to ensure an appropriate investment.
1. Quality Assessment: Evaluate the quality of materials and construction, ensuring the unit meets industry standards for durability and performance.
2. Supplier Verification: Conduct thorough background checks on potential suppliers to ensure they have a proven track record of reliability and product quality.
3. Pricing and MOQ: Understand the price range and minimum order quantity (MOQ) for the units, considering budget constraints and future needs.
4. Delivery and Lead Times: Factor in delivery schedules and lead times for production to avoid disruptions in operations.
5. Compliance Requirements: Ensure that the chosen units meet local and international compliance standards for safety and environmental impact.
Compliance and Certifications
Dust Collection Units must adhere to various quality and safety standards to ensure optimal performance and regulatory compliance.
ISO 9001 is a widely recognized standard that ensures quality management systems are in place, fostering continuous improvement in product quality.
The CE certification indicates compliance with health, safety, and environmental protection standards within the European market.
Safety and testing requirements often include evaluations for performance efficiency and durability under various operating conditions.
Additionally, regional compliance considerations may vary, necessitating attention to specific local regulations governing dust emissions and workplace safety.
Why Source Dust Collection Units from Pepagora?
Pepagora offers a reliable platform for sourcing Dust Collection Units, providing numerous advantages for businesses seeking quality and efficiency.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, ensuring access to high-quality products that meet industry standards.
Streamlined RFQ Process: The platform simplifies the request for quotation (RFQ) process, enabling buyers to easily compare options and make informed decisions.
Trade Assurance and Support: Buyers benefit from trade assurance programs that protect their investments and provide support throughout the procurement process.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora offers extensive geographic reach, facilitating access to a diverse range of suppliers and products.


Frequently Asked Questions
What are Dust Collection Units?
Dust Collection Units are systems designed to capture and filter airborne dust particles generated during various industrial processes. These units help maintain a clean and safe working environment by reducing dust exposure, thereby improving air quality and compliance with safety regulations.
What are the different types of Dust Collection Units?
There are several types of Dust Collection Units, including baghouse collectors, cartridge collectors, and cyclonic separators. Each type is suited for different applications and dust types, offering varying levels of efficiency and filtration capabilities.
How do I choose the right Dust Collection Units?
When selecting a Dust Collection Unit, consider factors such as the type and volume of dust produced, the size of your workspace, and local regulations. It's also important to evaluate the filtration efficiency, energy consumption, and maintenance requirements of the unit.
What are the standard specifications for Dust Collection Units?
Standard specifications for Dust Collection Units typically include airflow capacity (measured in CFM), filtration efficiency, and the type of filters used. Additionally, dimensions, noise levels, and power consumption are also critical specifications to consider.
What is the price range for Dust Collection Units?
The price range for Dust Collection Units can vary significantly based on the type, size, and features. Generally, prices can start from a few thousand Indian Rupees for smaller units and can go up to several lakhs for larger, industrial-grade systems.
What quality standards apply to Dust Collection Units?
Dust Collection Units are often required to meet specific quality standards such as ISO 9001 for quality management systems and ISO 14001 for environmental management. Compliance with local health and safety regulations is also essential.
Where can I find Dust Collection Units suppliers in India?
You can find Dust Collection Units suppliers in India through online B2B marketplaces like Pepagora, industry trade shows, and local directories. It's advisable to verify the suppliers' credentials and customer reviews before making a purchase.
Can Dust Collection Units be customized?
Yes, many manufacturers offer customization options for Dust Collection Units to meet specific requirements. Customizations may include size, filtration type, and additional features, depending on the application and dust characteristics.
What is the typical minimum order quantity for Dust Collection Units?
The typical minimum order quantity (MOQ) for Dust Collection Units can vary by supplier and product type. Generally, MOQs can range from one unit for smaller models to larger quantities for industrial systems.
What is the typical lead time for Dust Collection Units?
The typical lead time for Dust Collection Units varies based on the supplier and the complexity of the order. Generally, lead times can range from a few weeks to several months, especially for customized units.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
