
 IN
Other Chemical Processing Equipment
21 products available
What are Other Chemical Processing Equipment?
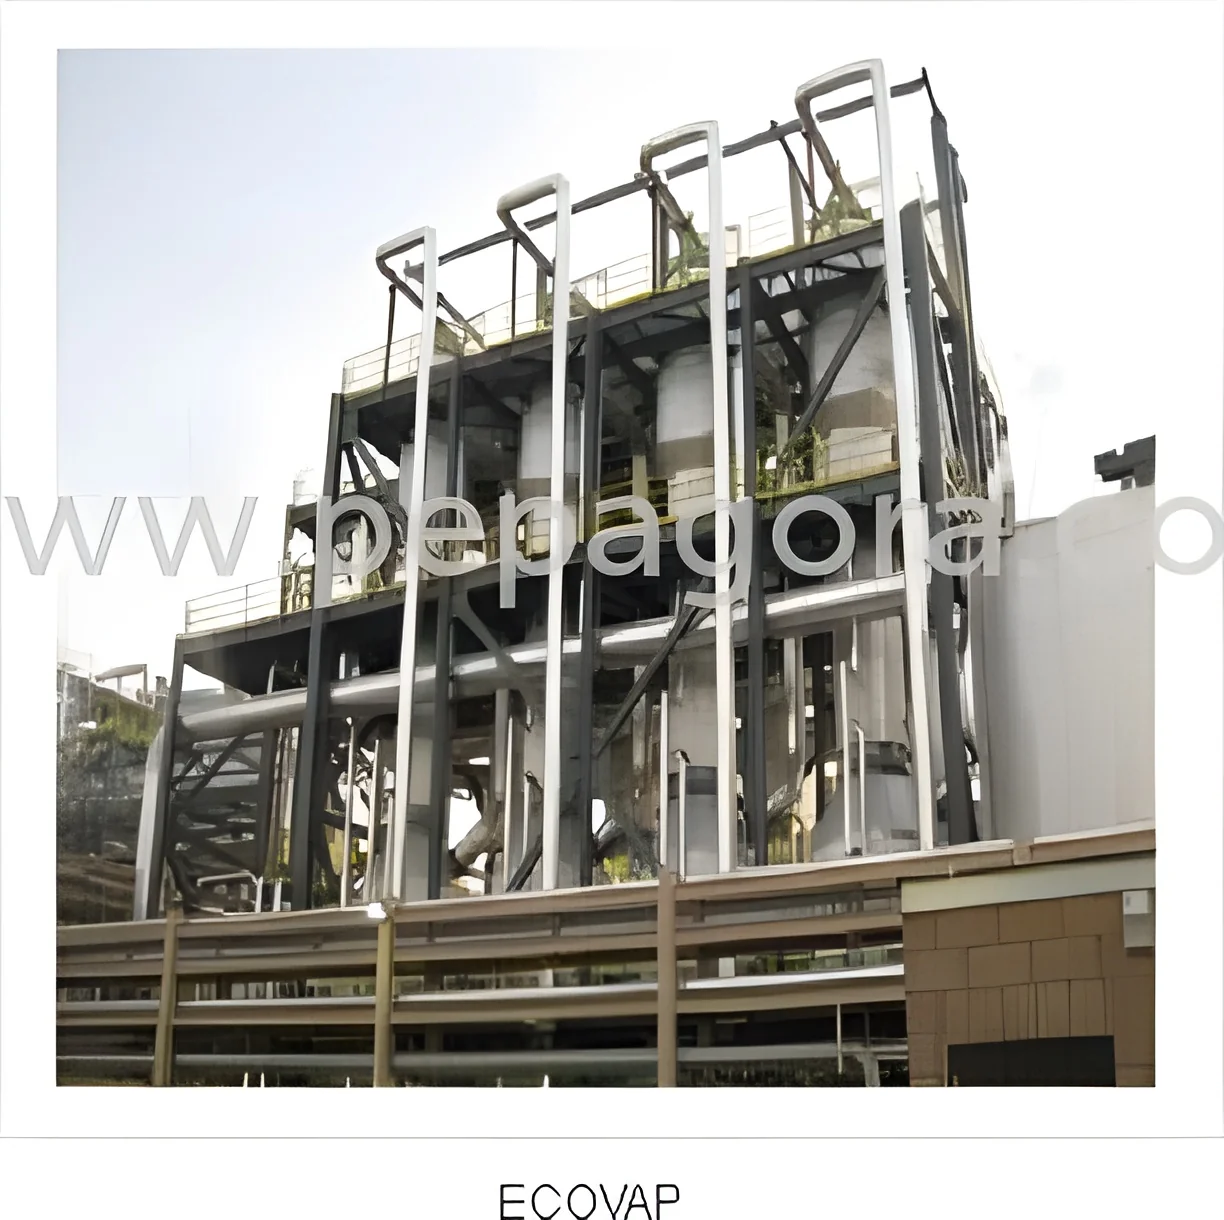
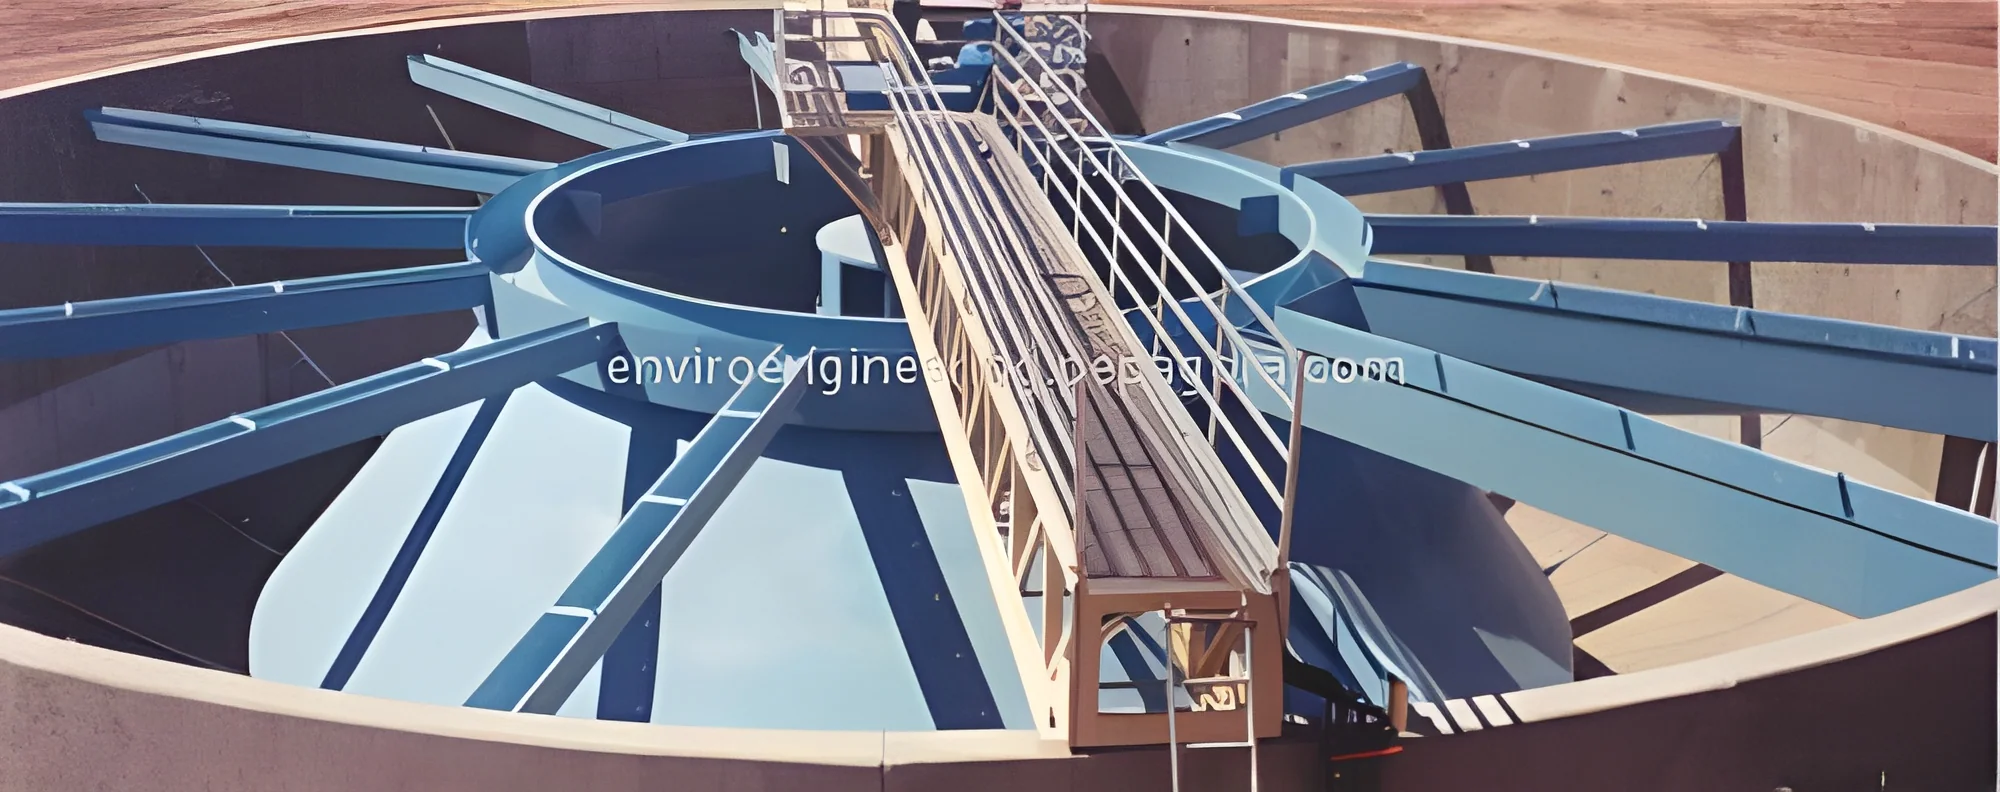
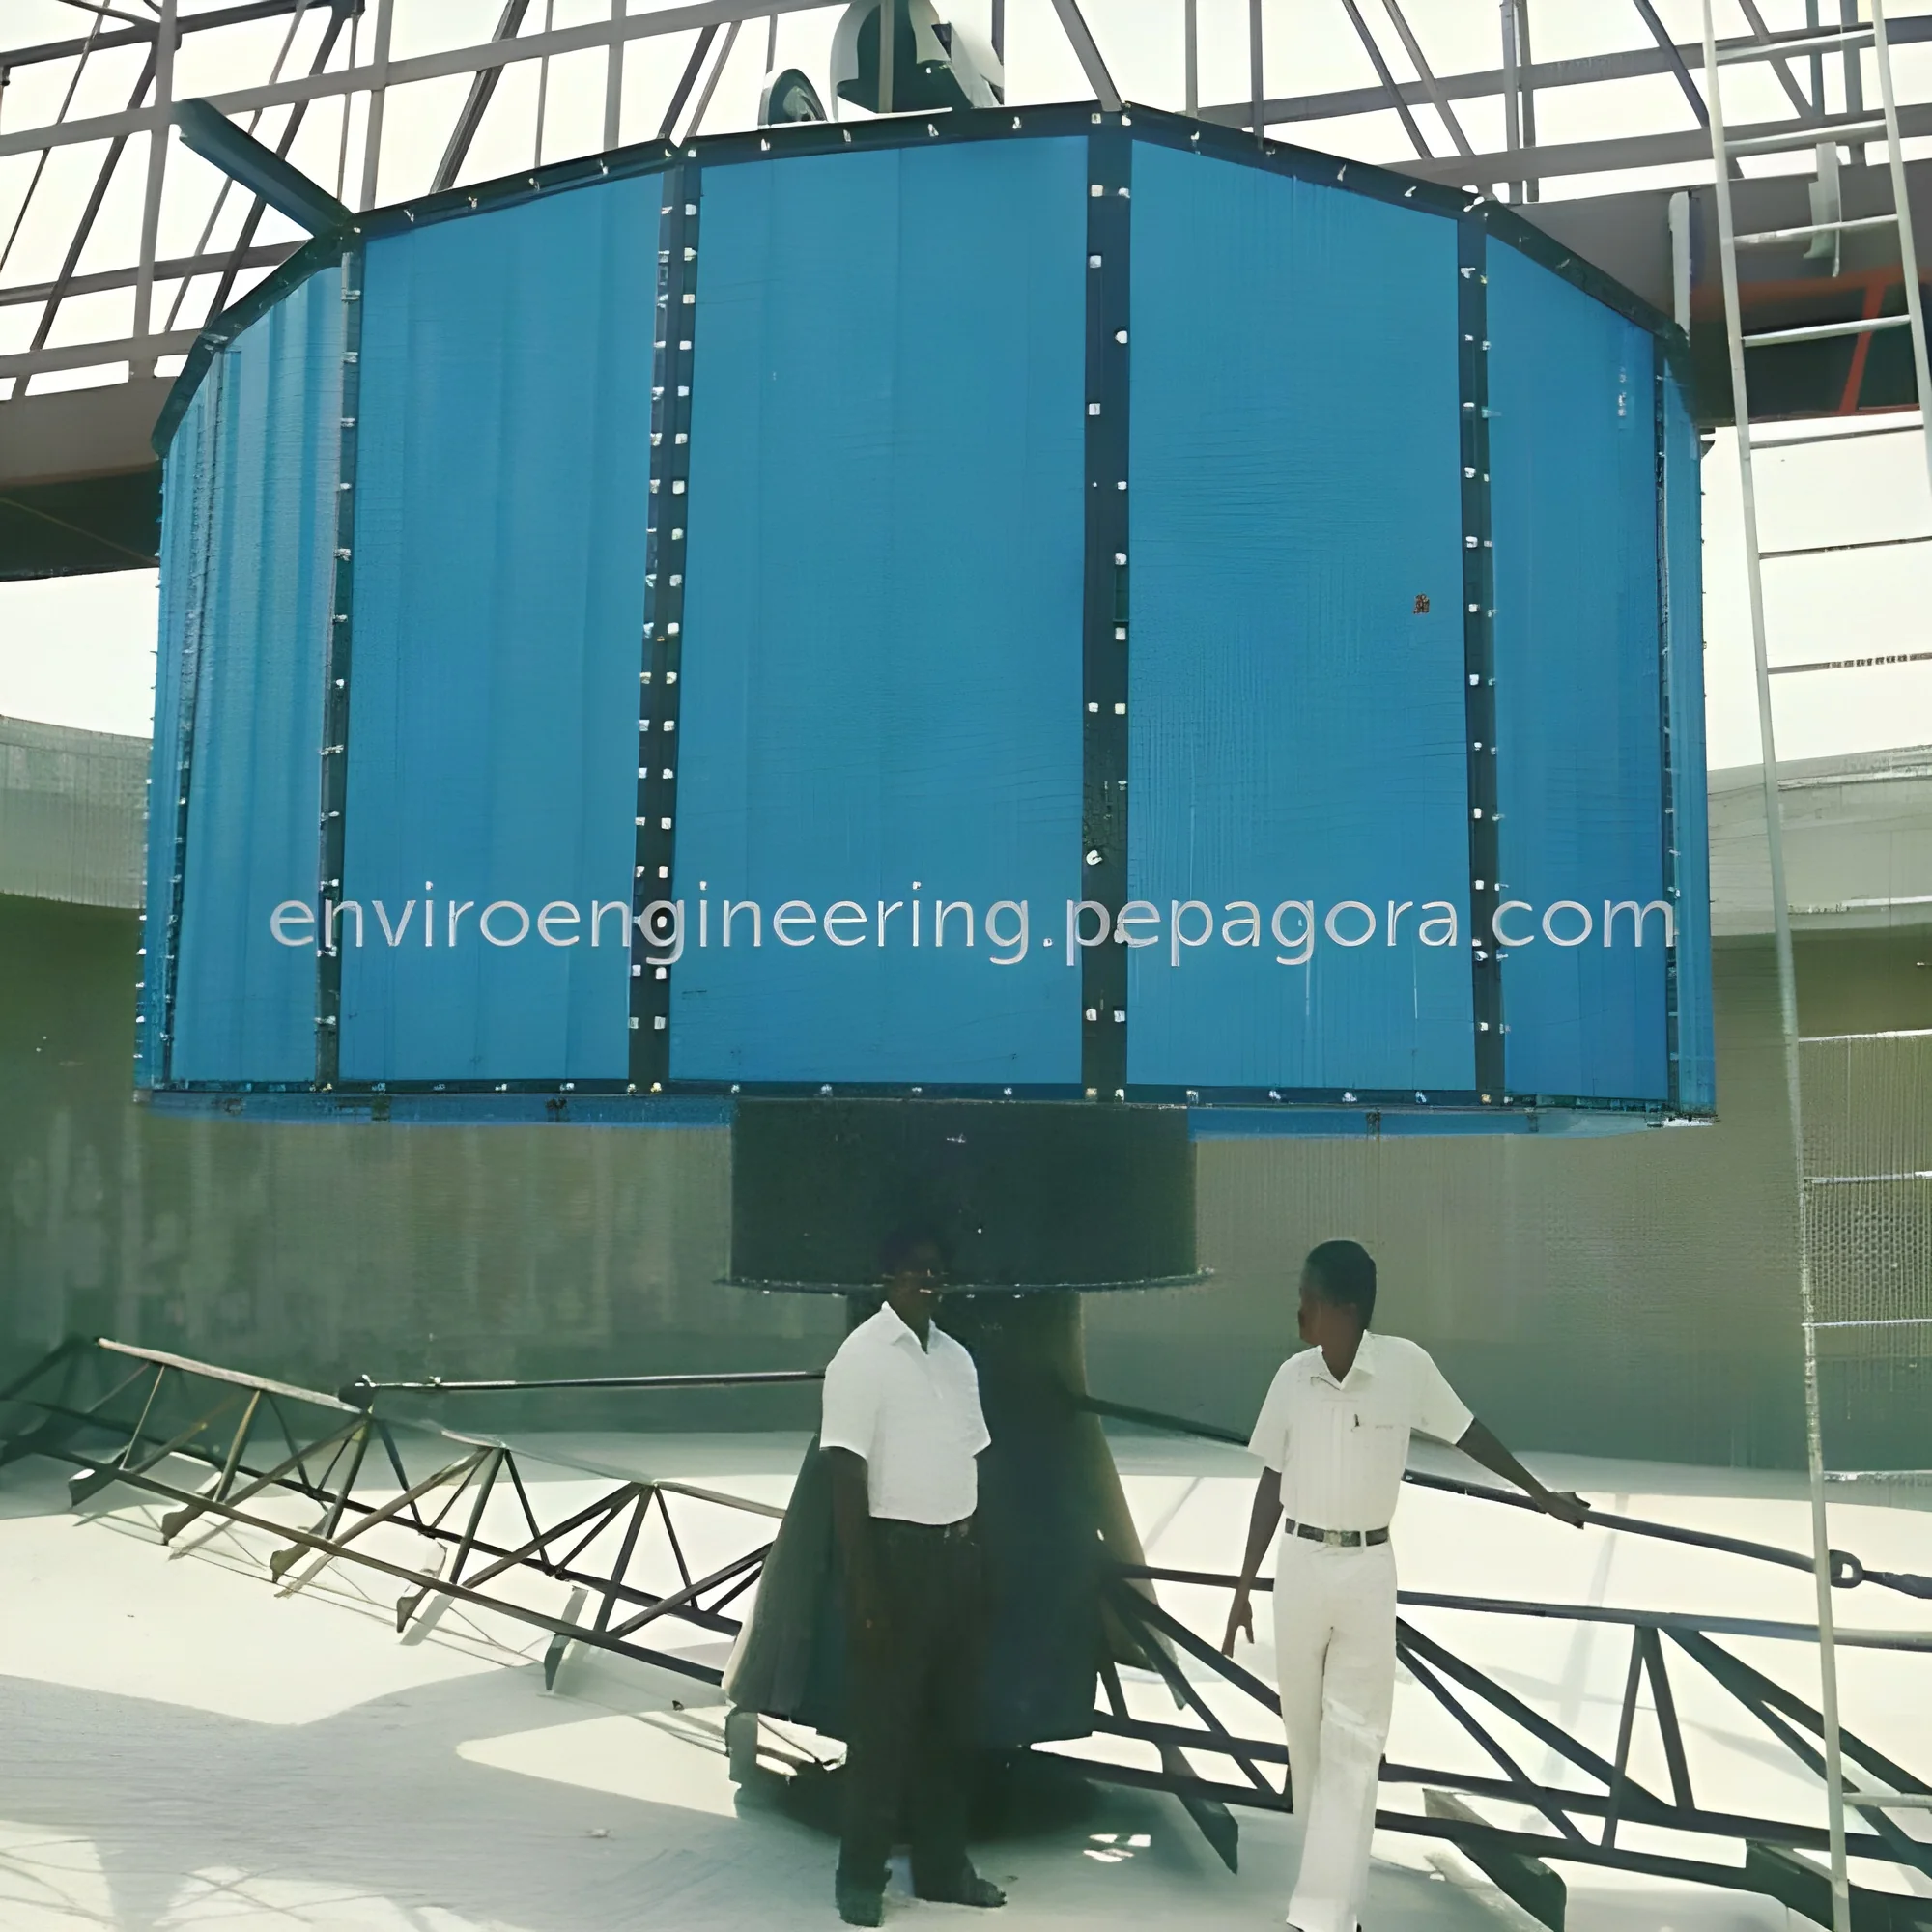
Other Chemical Processing Equipment encompasses a range of devices and systems used in the chemical manufacturing industry. These tools are crucial for various processes such as mixing, heating, cooling, and separating chemical compounds. Unlike specialized equipment that focuses on specific tasks, Other Chemical Processing Equipment includes a broader array of technologies that support the overall operation within chemical plants and facilities.
The primary uses of this equipment span multiple applications including the production of pharmaceuticals, agrochemicals, and specialty chemicals. Businesses rely on these tools to enhance their production efficiency and ensure product quality. For instance, reactors, heat exchangers, and filtration systems are integral to chemical processing. The relevance of these applications highlights the equipment's role in supporting vital industries, ensuring compliance with safety and quality standards, and contributing to economic growth.
With the increasing demand for sustainable and efficient chemical production, the market for Other Chemical Processing Equipment is expanding. Companies are investing in advanced technologies to optimize their processes and reduce environmental impact. As a result, understanding the features and specifications of this equipment is essential for businesses looking to enhance their operational capabilities.
Key Features and Specifications
When considering Other Chemical Processing Equipment, it is essential to understand the key features and specifications that define its performance and suitability for various applications. These specifications help businesses select the right equipment for their specific needs and ensure compliance with industry standards.
Key specifications include:
1. Material Compatibility
- Equipment must be compatible with various chemicals to prevent corrosion and degradation.
- Common materials include stainless steel, glass, and high-grade plastics.
2. Temperature Range
- Equipment should operate effectively within a specified temperature range.
- Typical ranges can vary depending on the type of process, usually from ambient to high temperatures.
3. Pressure Ratings
- Equipment should be assessed for its ability to withstand different pressure levels.
- This can range from low-pressure systems to high-pressure reactors.
4. Capacity
- The equipment should meet the production volume requirements of the facility.
- This can include batch sizes or continuous flow rates.
5. Automation Features
- Modern equipment often includes automation capabilities for enhanced control and monitoring.
- Features can include programmable logic controllers and remote monitoring systems.
6. Energy Efficiency
- Equipment should be designed to minimize energy consumption while maximizing output.
- This is increasingly important for reducing operational costs.
7. Safety Features
- Equipment must incorporate safety mechanisms to protect operators and prevent accidents.
- Features may include pressure relief valves, emergency shut-offs, and fail-safes.
8. Maintenance Requirements
- Equipment should be designed for ease of maintenance to minimize downtime.
- Regular checks and replacements of parts should be straightforward.
In summary, understanding these specifications helps businesses make informed decisions when selecting Other Chemical Processing Equipment, ensuring they choose equipment that meets their operational needs and complies with industry standards.
Common Applications and Use Cases
Other Chemical Processing Equipment serves a wide array of industries, each with unique applications and requirements. Understanding these applications can help businesses identify the right equipment for their specific needs.
1. Pharmaceutical Industry: Equipment is used for the synthesis of active pharmaceutical ingredients (APIs), ensuring precise control over temperature and pressure during reactions.
2. Agrochemical Industry: Equipment facilitates the production of fertilizers and pesticides, requiring robust materials to handle corrosive chemicals safely.
3. Food and Beverage Industry: Equipment is used for processes like extraction and purification, ensuring compliance with safety and quality standards.
4. Petrochemical Industry: Equipment aids in refining processes, where it is crucial to manage high pressures and temperatures effectively.
5. Specialty Chemicals: Equipment supports the production of niche chemicals, requiring customization to meet specific performance criteria.
6. Water Treatment: Equipment is essential for processes like filtration and disinfection, ensuring safe and clean water supplies.
7. Cosmetics Industry: Equipment is used to create formulations for creams and lotions, requiring precision in mixing and heat control.
In conclusion, the diverse applications of Other Chemical Processing Equipment highlight its importance across various industries, underscoring the need for businesses to understand their specific requirements.
Product Variants and Subcategories
The diversity of Other Chemical Processing Equipment allows businesses to select from various variants tailored to specific needs. Each variant comes with unique features and applications that enhance operational efficiency.
Batch Reactors: These systems are designed for producing small to medium quantities of chemicals. They offer flexibility in operations and are ideal for processes requiring precise control over reaction conditions.
Continuous Flow Reactors: These reactors are designed for high-volume production. They ensure consistent quality and efficiency, making them suitable for large-scale operations in industries like petrochemicals.
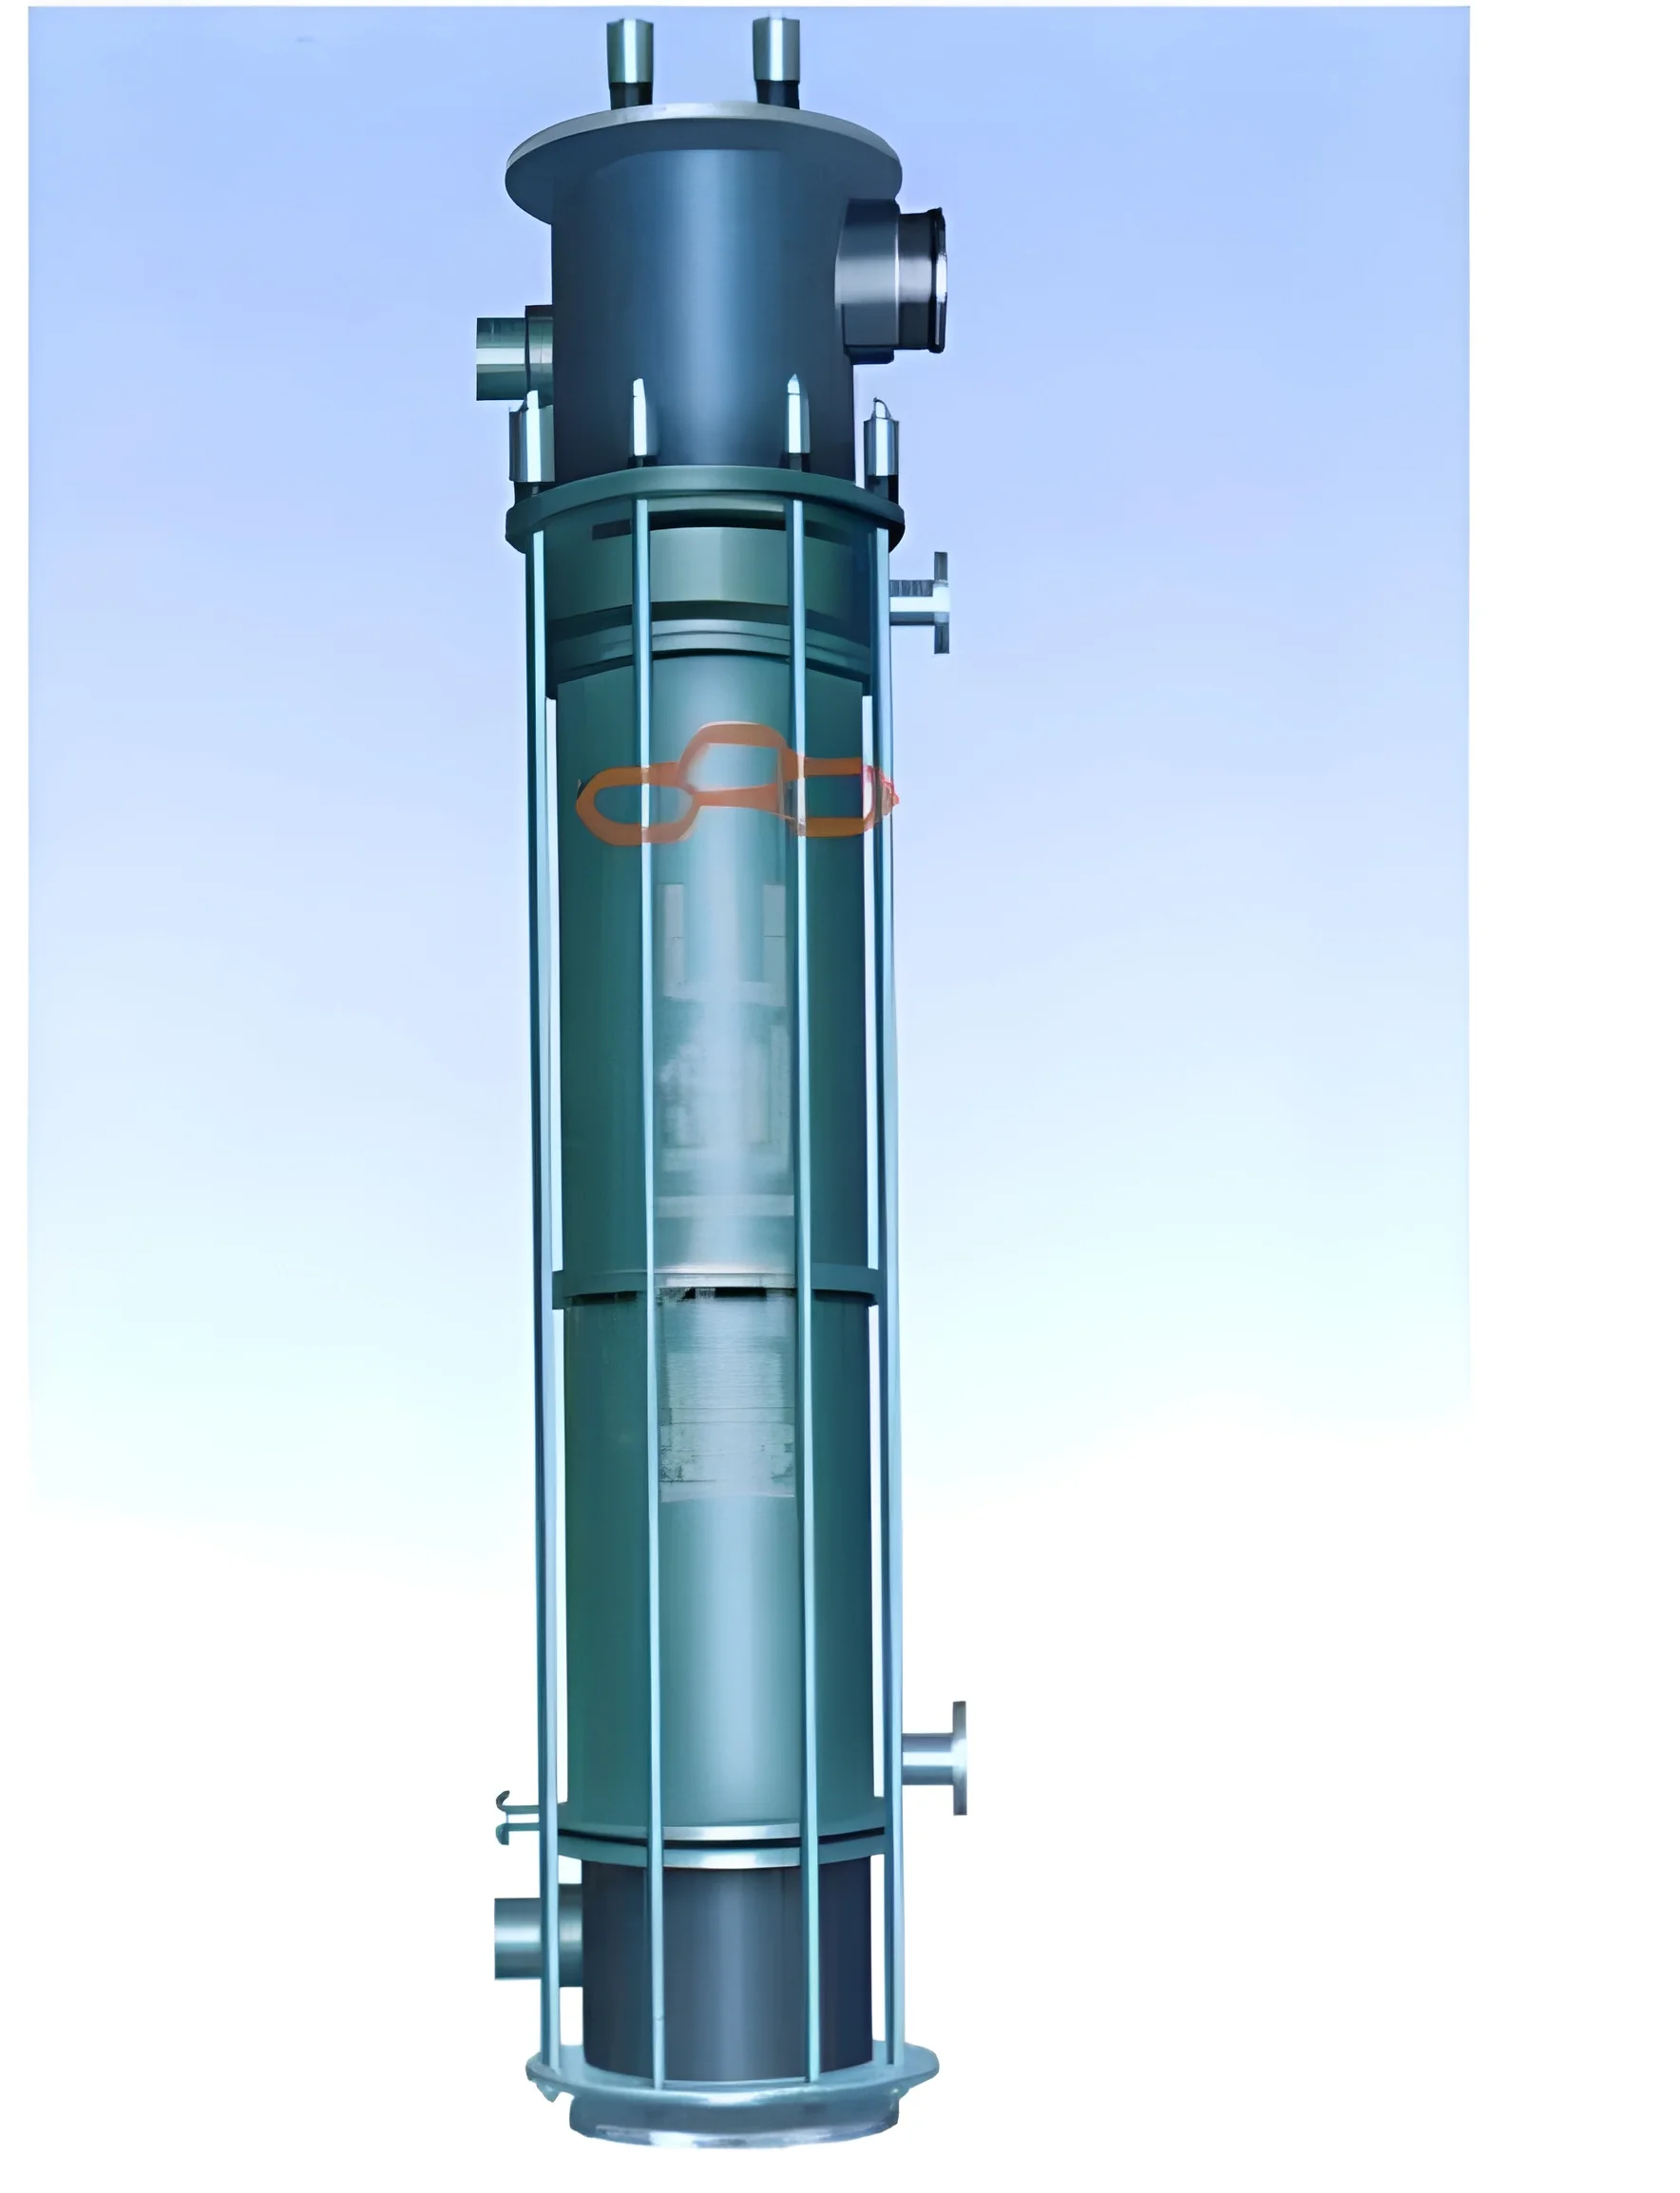
Heat Exchangers: Essential for managing heat transfer in chemical processes, these devices can be customized for various applications, including cooling and heating fluids in production lines.
Filtration Systems: These systems are crucial for separating solids from liquids in various processes. They come in different designs, including membrane filters and cartridge filters, depending on the application.
Mixing Equipment: This variant is vital for achieving homogeneity in chemical mixtures. Options range from simple stirrers to advanced dynamic mixers designed for complex formulations.
Benefits and Advantages
Investing in Other Chemical Processing Equipment offers numerous benefits to businesses aiming to enhance their production capabilities and operational efficiency.
Key benefits include:
1. Increased Efficiency: Advanced equipment is designed to optimize processes, leading to higher throughput and reduced cycle times.
2. Improved Product Quality: Precision control over processing conditions helps ensure consistent quality in the final product.
3. Enhanced Safety: Modern equipment incorporates safety features that protect operators and reduce the risk of accidents.
4. Cost Savings: Energy-efficient designs and reduced downtime can lead to significant cost savings in operations.
5. Regulatory Compliance: Equipment designed to meet industry standards helps businesses comply with safety and environmental regulations.
6. Flexibility: The availability of various equipment types allows businesses to adapt to changing production needs and market demands.
In summary, the benefits of Other Chemical Processing Equipment underscore its value in improving operational performance and ensuring product quality.
Buying Guide for B2B Buyers
When sourcing Other Chemical Processing Equipment, businesses should consider several critical factors to ensure they make informed decisions.
1. Quality Assessment: Evaluate the quality of equipment based on manufacturer reputation, material specifications, and performance metrics. Consider equipment that meets recognized industry standards.
2. Supplier Verification: Vet suppliers to ensure they have a proven track record in the industry. Look for certifications and customer reviews to gauge reliability.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities to align with budget constraints. Compare quotes from multiple suppliers for the best value.
4. Delivery and Lead Times: Inquire about delivery schedules and lead times to ensure timely procurement. Consider suppliers with a track record of meeting deadlines.
5. Compliance Requirements: Ensure that the equipment complies with relevant regulations and standards, such as safety and environmental guidelines. This is crucial for avoiding potential legal issues.
In conclusion, taking these factors into account can help B2B buyers make informed decisions when sourcing Other Chemical Processing Equipment, ultimately leading to better operational outcomes.
Compliance and Certifications
Compliance and certifications play a vital role in the manufacturing and operation of Other Chemical Processing Equipment. Adhering to quality standards helps ensure that equipment meets safety and performance requirements.
Relevant quality standards include ISO 9001, which emphasizes quality management systems, and HACCP, which focuses on food safety management. These standards guide manufacturers in maintaining consistent quality in their products.
Industry certifications, such as CE marking, indicate that products comply with European health, safety, and environmental protection standards. This is essential for gaining market access and ensuring consumer safety.
Safety and testing requirements are critical, with equipment often undergoing rigorous testing to verify its performance under various conditions. This includes pressure testing, temperature tolerance assessments, and material compatibility evaluations.
Additionally, regional compliance considerations may vary, necessitating a thorough understanding of local regulations. Businesses must ensure that their equipment aligns with these requirements to avoid potential legal challenges.
In summary, compliance and certifications are essential components that enhance the reliability and safety of Other Chemical Processing Equipment, providing reassurance to users and regulatory bodies alike.
Why Source Other Chemical Processing Equipment from Pepagora?
Pepagora provides a trusted platform for sourcing Other Chemical Processing Equipment, offering numerous advantages for businesses seeking high-quality solutions.
Verified Supplier Network: Pepagora maintains a network of verified suppliers, ensuring that businesses can confidently source equipment from reputable manufacturers. This reduces the risk of purchasing subpar equipment and enhances buyer assurance.
Streamlined RFQ Process: The platform features a straightforward Request for Quotation (RFQ) process, allowing businesses to quickly obtain quotes from multiple suppliers. This saves time and helps buyers make informed decisions based on competitive pricing.
Trade Assurance and Support: Pepagora offers trade assurance, providing buyer protection throughout the procurement process. This includes support for resolving any issues that may arise, ensuring a smooth transaction.
Regional Coverage: With a strong presence in India, GCC, and Southeast Asia, Pepagora facilitates access to a wide range of suppliers and equipment options. This geographic reach helps businesses find solutions tailored to their specific regional needs.
In conclusion, sourcing Other Chemical Processing Equipment from Pepagora offers a reliable and efficient solution for businesses looking to enhance their operational capabilities while ensuring quality and compliance.



 India
 India
 India

 India
 India
 India
 India
 India
 India
 India
 India
 India
 India
 India

 India
 India
 India
Frequently Asked Questions
What are Other Chemical Processing Equipment?
Other Chemical Processing Equipment refers to a diverse range of machinery and tools used in the chemical industry for various processes, such as mixing, heating, cooling, and separation. These equipment types are essential for facilitating chemical reactions and ensuring product quality in manufacturing.
What are the different types of Other Chemical Processing Equipment?
Different types of Other Chemical Processing Equipment include reactors, heat exchangers, mixers, filters, and separators. Each type serves a specific function in the chemical processing workflow, contributing to the overall efficiency and effectiveness of production.
How do I choose the right Other Chemical Processing Equipment?
Choosing the right Other Chemical Processing Equipment involves considering factors such as the specific chemical processes, production capacity, and compatibility with existing machinery. It is also important to evaluate the supplier's expertise and the equipment's technical specifications.
What are the standard specifications for Other Chemical Processing Equipment?
Standard specifications for Other Chemical Processing Equipment vary by type but generally include material construction, pressure and temperature ratings, and capacity or throughput. It's essential to consult manufacturer guidelines and industry standards to ensure compliance.
What is the price range for Other Chemical Processing Equipment?
The price range for Other Chemical Processing Equipment can vary significantly based on type, size, and manufacturer. Generally, prices can start from a few thousand rupees for smaller units and can go up to several lakhs for more complex machinery.
What quality standards apply to Other Chemical Processing Equipment?
Quality standards for Other Chemical Processing Equipment typically include ISO certifications, industry-specific standards, and adherence to safety regulations. These standards ensure the equipment is reliable, safe to operate, and suitable for chemical processing applications.
Where can I find Other Chemical Processing Equipment suppliers in India?
You can find Other Chemical Processing Equipment suppliers in India by exploring B2B marketplaces, industry trade shows, and online directories. Websites like Pepagora.com provide a platform to connect with reputable manufacturers and suppliers.
Can Other Chemical Processing Equipment be customized?
Yes, Other Chemical Processing Equipment can often be customized to meet specific operational requirements. Many manufacturers offer customization options to cater to unique production processes, sizes, and material specifications.
What is the typical minimum order quantity for Other Chemical Processing Equipment?
The typical minimum order quantity (MOQ) for Other Chemical Processing Equipment can vary by supplier and type of equipment. Generally, MOQs can range from one unit for standard equipment to larger quantities for specialized or custom machinery.
What is the typical lead time for Other Chemical Processing Equipment?
The typical lead time for Other Chemical Processing Equipment usually ranges from a few weeks to several months, depending on the type of equipment, customization requirements, and supplier capabilities. It's advisable to confirm lead times with the supplier during the ordering process.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
