
 IN
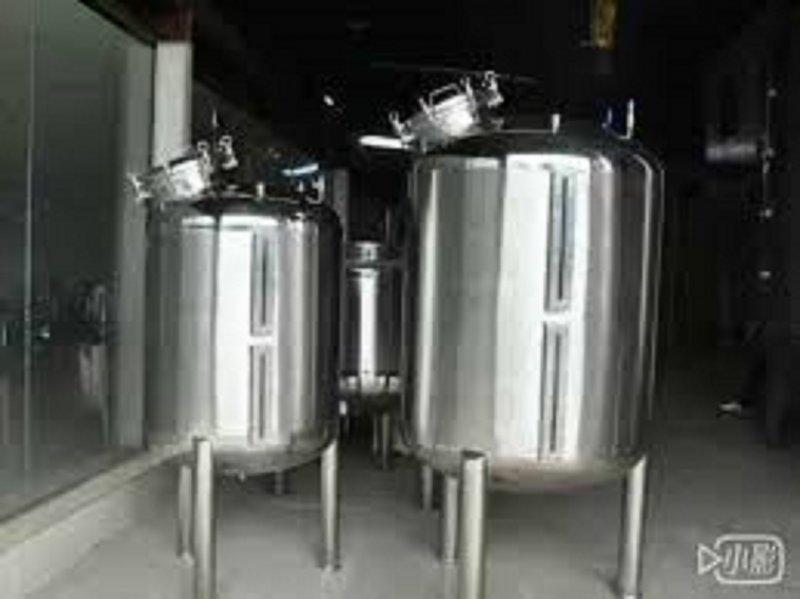
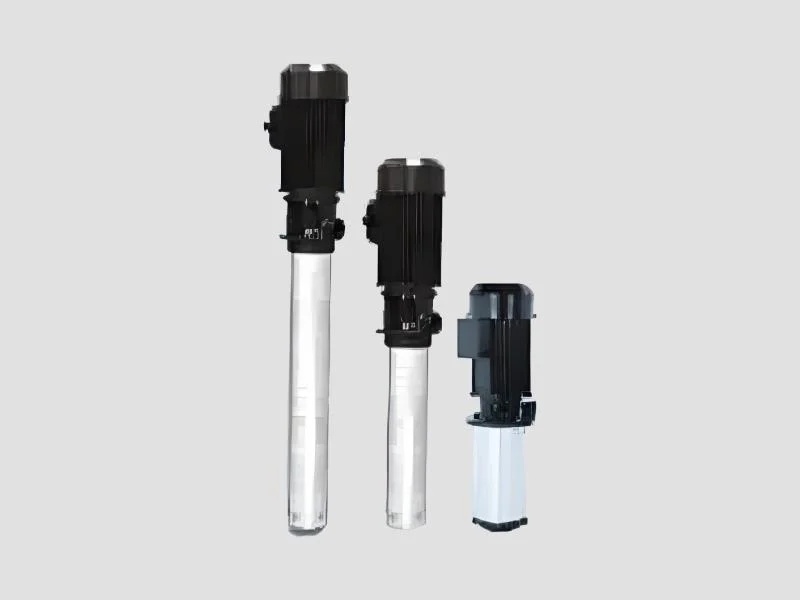
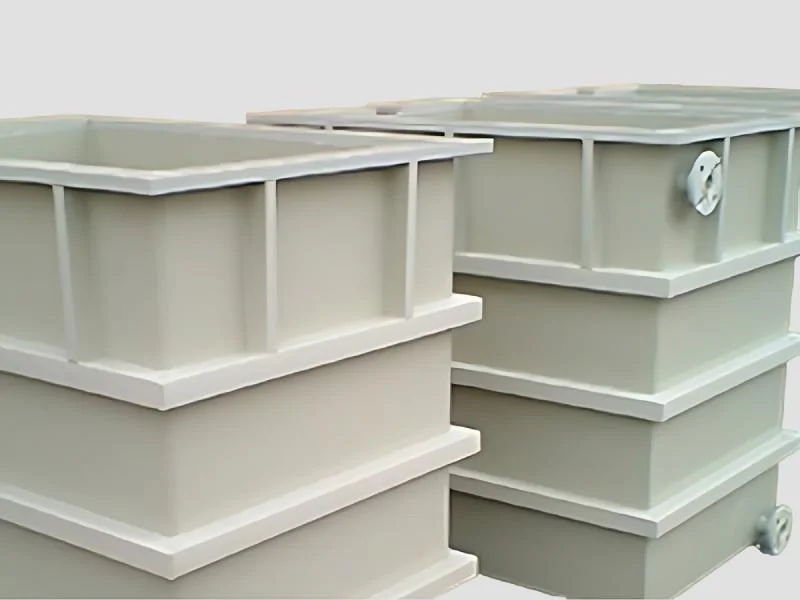
Chemical Processing Equipment
1027 products available
𝗪𝗵𝗮𝘁 𝗮𝗿𝗲 𝗖𝗵𝗲𝗺𝗶𝗰𝗮𝗹 𝗣𝗿𝗼𝗰𝗲𝘀𝘀𝗶𝗻𝗴 𝗘𝗾𝘂𝗶𝗽𝗺𝗲𝗻𝘁?
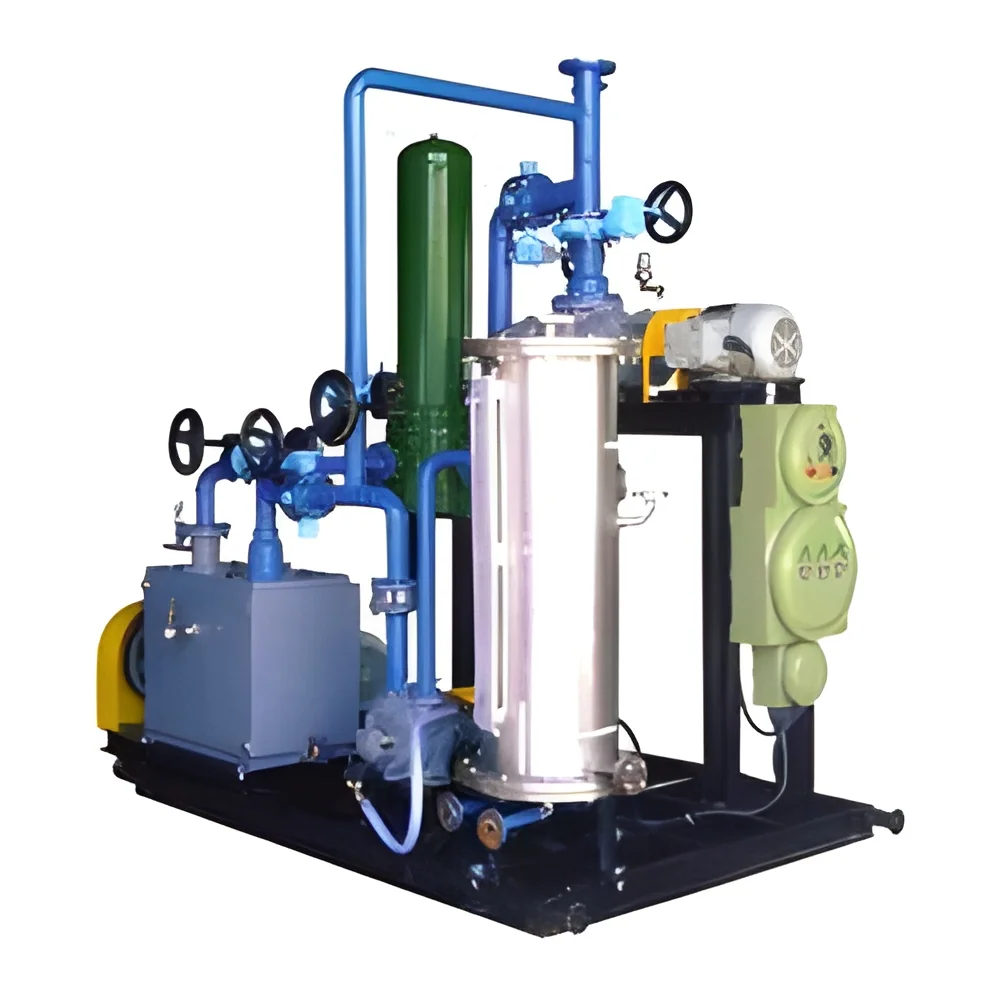
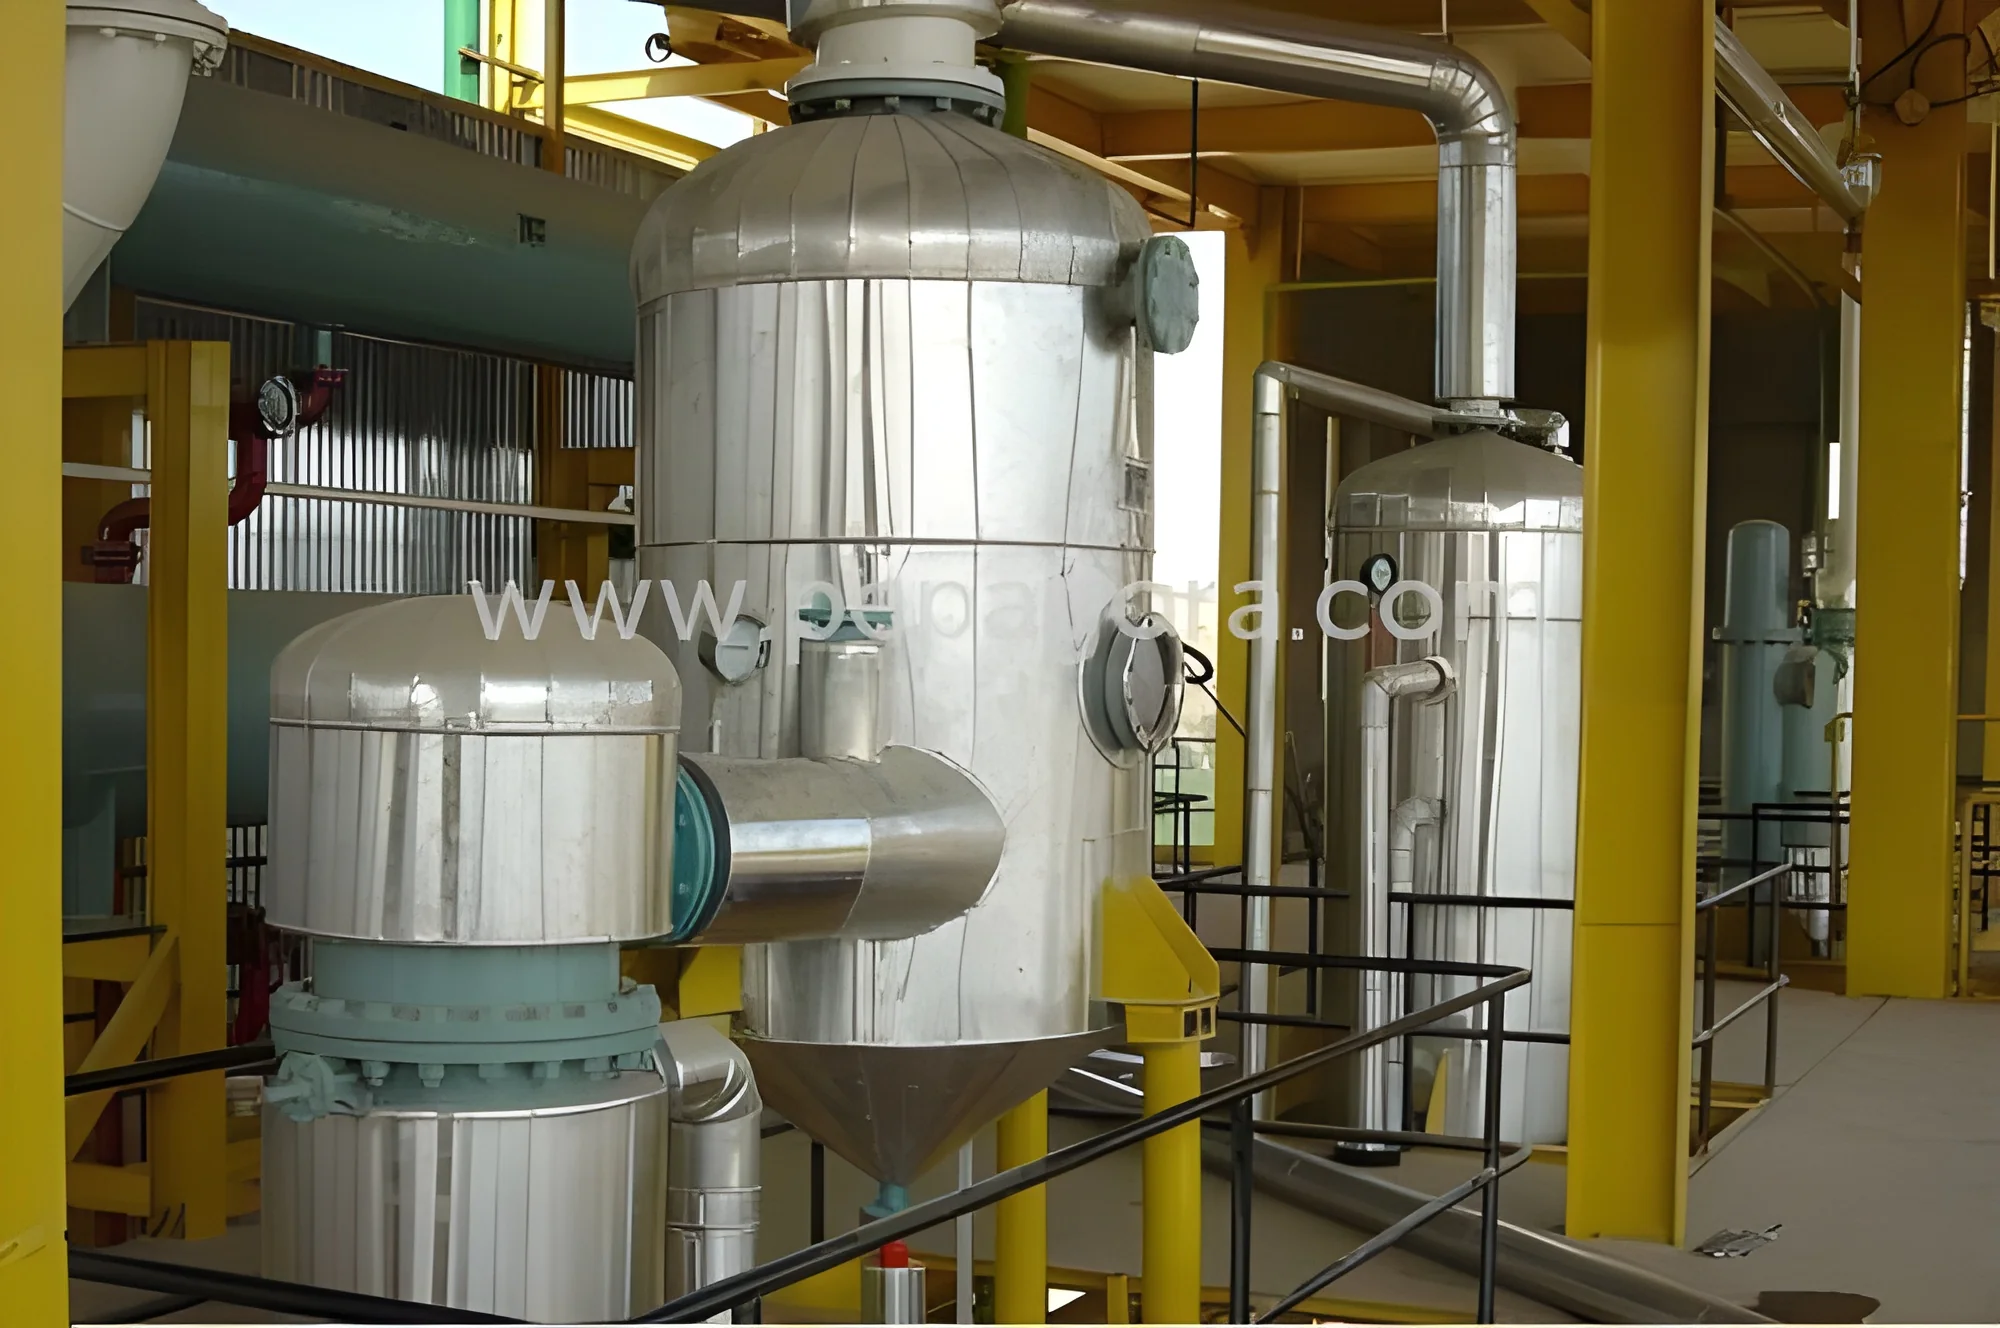
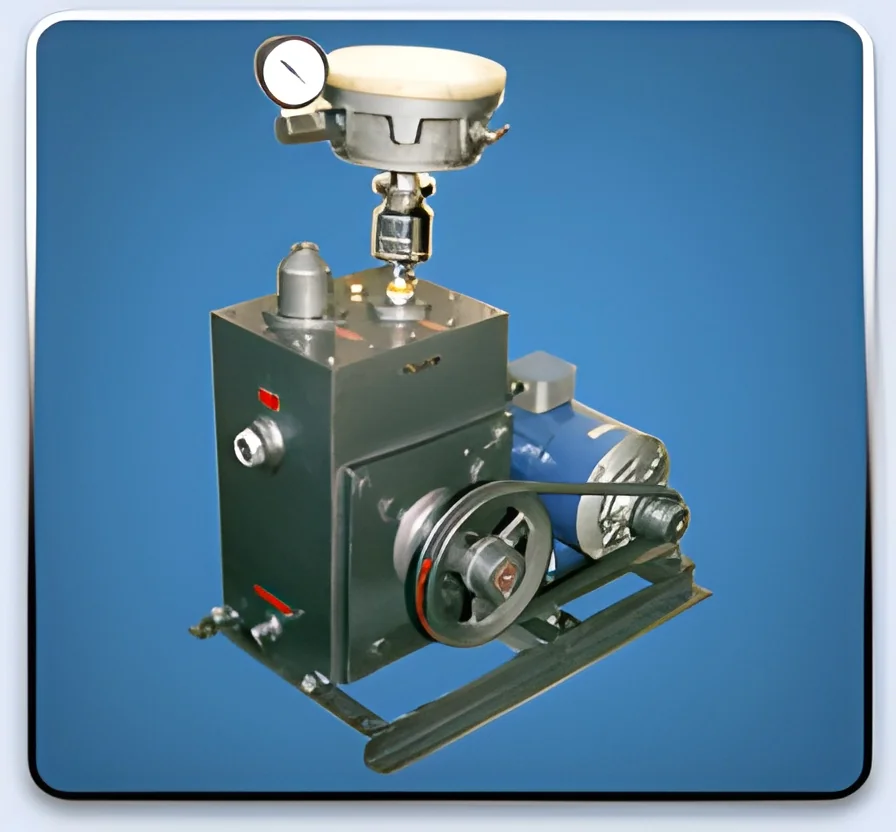
Chemical processing equipment refers to the machinery and systems used in the production and transformation of chemicals and materials. This category includes a wide range of tools and technologies designed to facilitate various processes such as mixing, heating, cooling, and separating chemical substances. These equipment pieces are essential for maintaining control over chemical reactions and ensuring product quality and safety.
The primary uses of chemical processing equipment span various industries, including pharmaceuticals, petrochemicals, food and beverage, and materials manufacturing. In each of these sectors, the equipment plays a critical role in scaling up production, optimizing processes, and ensuring compliance with safety and quality standards. For example, in pharmaceuticals, precise temperature and mixing control are crucial for developing effective medications.
In the broader market context, the demand for chemical processing equipment continues to grow, driven by advancements in technology and increasing industrialization. Companies are seeking more efficient and sustainable solutions to minimize waste and energy consumption. As industries evolve, the relevance of chemical processing equipment becomes more pronounced, highlighting the need for reliable and innovative machinery.
𝗞𝗲𝘆 𝗙𝗲𝗮𝘁𝘂𝗿𝗲𝘀 𝗮𝗻𝗱 𝗦𝗽𝗲𝗰𝗶𝗳𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀
Chemical processing equipment is characterized by several technical specifications that determine its efficiency and suitability for specific applications. Understanding these specifications is essential for businesses to make informed choices when sourcing equipment.
Key specifications include:
1. Material Construction
- Typically made from stainless steel, carbon steel, or specialized alloys
- Must withstand corrosive and high-temperature environments
2. Capacity
- Varies from small laboratory-scale units to large industrial systems
- Measured in liters, gallons, or tons per hour
3. Temperature Control
- Capable of operating within specific temperature ranges
- Essential for maintaining reaction conditions
4. Pressure Ratings
- Designed to operate under varying pressure conditions
- Important for processes like distillation and extraction
5. Energy Efficiency
- Features that reduce energy consumption during operation
- Incorporates advanced technology for optimization
6. Automation and Monitoring
- Equipped with control systems for automation of processes
- May include monitoring features for real-time data collection
7. Safety Features
- Compliance with safety standards to prevent accidents
- May include emergency shut-off systems and pressure relief valves
8. Maintenance Requirements
- Designed for ease of cleaning and maintenance
- Necessary to ensure longevity and operational efficiency
In summary, understanding the key features and specifications of chemical processing equipment is crucial for businesses to select the right equipment that meets their operational needs.
𝗖𝗼𝗺𝗺𝗼𝗻 𝗔𝗽𝗽𝗹𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀 𝗮𝗻𝗱 𝗨𝘀𝗲 𝗖𝗮𝘀𝗲𝘀
Chemical processing equipment serves a wide array of industries, each with specific applications that leverage the capabilities of the equipment.
1. Pharmaceuticals: Used for mixing and compounding active ingredients, ensuring precise dosages and consistent product quality.
2. Petrochemicals: Facilitates the refining of crude oil into various fuels and chemicals through processes like distillation and cracking.
3. Food and Beverage: Employed in the production of sauces, beverages, and other food products, focusing on hygiene and flavor preservation.
4. Water Treatment: Utilizes chemical processes to purify water, making it safe for consumption and industrial use.
5. Agriculture: Aids in the formulation of fertilizers and pesticides, ensuring proper chemical composition for effective crop management.
6. Cosmetics: Involved in the blending and formulation of beauty products, maintaining quality and safety standards.
7. Electronics: Used in the manufacturing of semiconductors and other electronic components, requiring high precision and controlled environments.
𝗣𝗿𝗼𝗱𝘂𝗰𝘁 𝗩𝗮𝗿𝗶𝗮𝗻𝘁𝘀 𝗮𝗻𝗱 𝗦𝘂𝗯𝗰𝗮𝘁𝗲𝗴𝗼𝗿𝗶𝗲𝘀
Chemical processing equipment is diverse, catering to various applications and industry requirements. Different variants are designed to meet specific needs.
Batch Reactors
Batch reactors are used for conducting chemical reactions in discrete batches. They allow for precise control over reaction conditions and are ideal for small to medium-scale production.
Continuous Reactors
Continuous reactors facilitate ongoing chemical processes, providing efficiency for large-scale production. They are typically used in industries like petrochemicals and food processing.
Mixers and Blenders
These machines are essential for uniformly mixing different substances, ensuring consistent quality in products like paints, coatings, and food items.
Heat Exchangers
Heat exchangers transfer heat between two or more fluids, optimizing energy use in processes such as heating and cooling in chemical plants.
𝗕𝗲𝗻𝗲𝗳𝗶𝘁𝘀 𝗮𝗻𝗱 𝗔𝗱𝘃𝗮𝗻𝘁𝗮𝗴𝗲𝘀
Sourcing chemical processing equipment offers several advantages that can significantly impact operational efficiency and product quality.
Key benefits include:
1. Enhanced Efficiency: Efficient equipment reduces production time and energy consumption, leading to cost savings.
2. Improved Product Quality: High-quality equipment ensures consistent processing, resulting in superior product quality.
3. Increased Safety: Modern equipment is designed with safety features that minimize risks associated with chemical processing.
4. Scalability: Equipment can be selected based on production needs, allowing businesses to scale up operations as demand increases.
5. Regulatory Compliance: Reliable equipment meets industry standards and regulations, helping businesses avoid legal issues.
6. Technological Advancements: The latest equipment incorporates innovative technology, improving overall operational capabilities.
𝗕𝘂𝘆𝗶𝗻𝗴 𝗚𝘂𝗶𝗱𝗲 𝗳𝗼𝗿 𝗕𝟮𝗕 𝗕𝘂𝘆𝗲𝗿𝘀
When sourcing chemical processing equipment, there are several key factors to consider to ensure a successful purchase.
1. Quality Assessment: Evaluate the quality of the equipment based on construction materials, design, and manufacturer reputation. Look for equipment that meets industry standards.
2. Supplier Verification: Vet suppliers thoroughly to ensure they have a proven track record in providing reliable equipment. Check for certifications and customer reviews.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantity (MOQ) requirements. Compare costs from multiple suppliers for better negotiation.
4. Delivery and Lead Times: Discuss delivery schedules and lead times with suppliers to ensure the equipment arrives when needed. Consider potential delays in logistics.
5. Compliance Requirements: Verify that the equipment complies with relevant regulations and industry standards. This is crucial for safety and operational success.
𝗖𝗼𝗺𝗽𝗹𝗶𝗮𝗻𝗰𝗲 𝗮𝗻𝗱 𝗖𝗲𝗿𝘁𝗶𝗳𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀
Compliance and certification are critical aspects of chemical processing equipment. Relevant quality standards, such as ISO 9001, ensure that equipment meets international quality management criteria. This certification indicates a commitment to producing high-quality products consistently.
Industry certifications, such as CE marking, signify that equipment complies with European safety and health requirements. This is particularly important for businesses operating in or exporting to Europe.
Safety and testing requirements are also vital. Equipment must undergo rigorous testing to ensure it operates safely under specified conditions. Additionally, regional compliance considerations must be taken into account, as regulations can vary significantly between different markets.
𝗪𝗵𝘆 𝗦𝗼𝘂𝗿𝗰𝗲 𝗖𝗵𝗲𝗺𝗶𝗰𝗮𝗹 𝗣𝗿𝗼𝗰𝗲𝘀𝘀𝗶𝗻𝗴 𝗘𝗾𝘂𝗶𝗽𝗺𝗲𝗻𝘁 𝗳𝗿𝗼𝗺 𝗣𝗲𝗽𝗮𝗴𝗼𝗿𝗮?
Pepagora provides a trusted platform for sourcing chemical processing equipment, offering several key advantages for B2B buyers.
Verified Supplier Network: Pepagora features a network of thoroughly vetted suppliers. This ensures that buyers can access high-quality equipment from reputable manufacturers.
Streamlined RFQ Process: The platform simplifies the request for quotation (RFQ) process, allowing buyers to quickly gather and compare quotes from multiple suppliers. This efficiency saves time and enhances decision-making.
Trade Assurance and Support: Pepagora offers trade assurance, providing buyers with protection throughout the purchasing process. This includes assistance in resolving disputes and ensuring satisfaction.
Regional Coverage: With a strong presence in India, GCC, and Southeast Asia, Pepagora connects buyers with suppliers across a wide geographic area. This regional coverage facilitates access to local and international markets, enhancing sourcing opportunities.












Frequently Asked Questions
What are Chemical Processing Equipment?
Chemical Processing Equipment refers to the machinery and tools used in the production and processing of chemicals. This equipment is essential for various operations such as mixing, heating, cooling, and chemical reactions in industries like pharmaceuticals, petrochemicals, and food processing.
What are the different types of Chemical Processing Equipment?
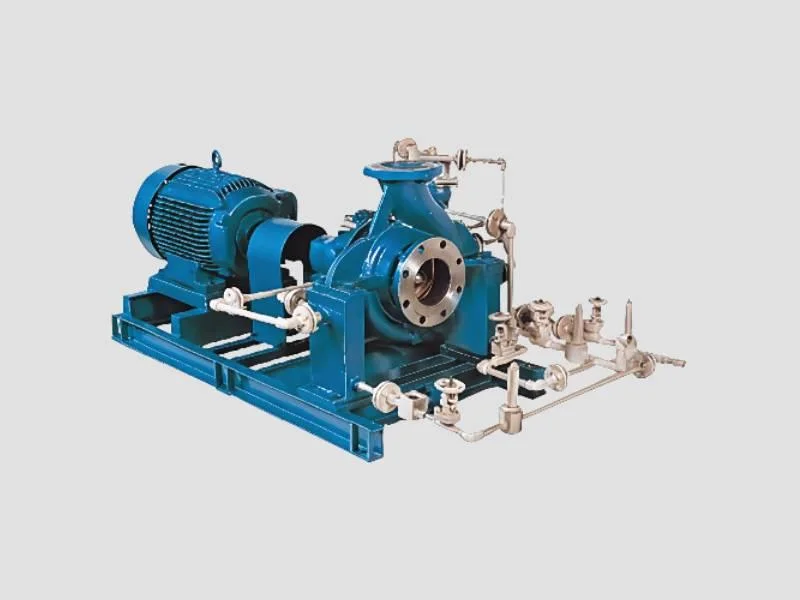
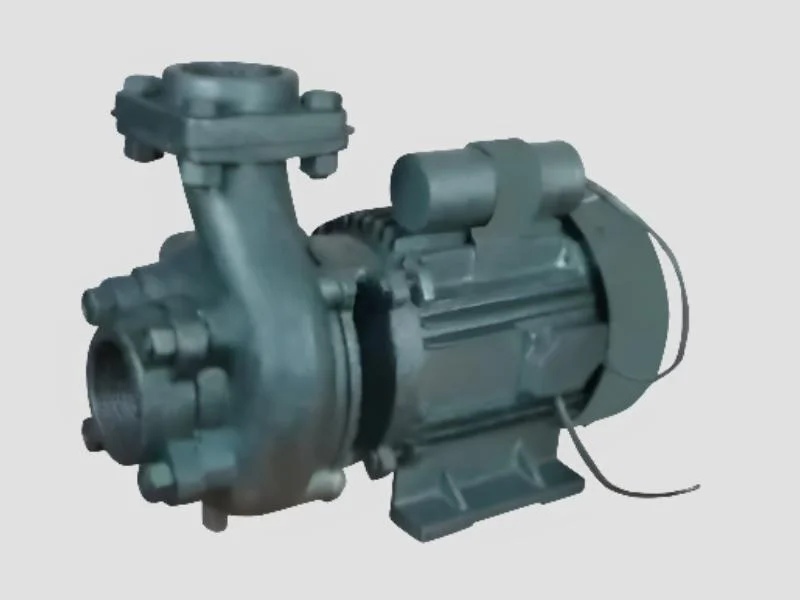
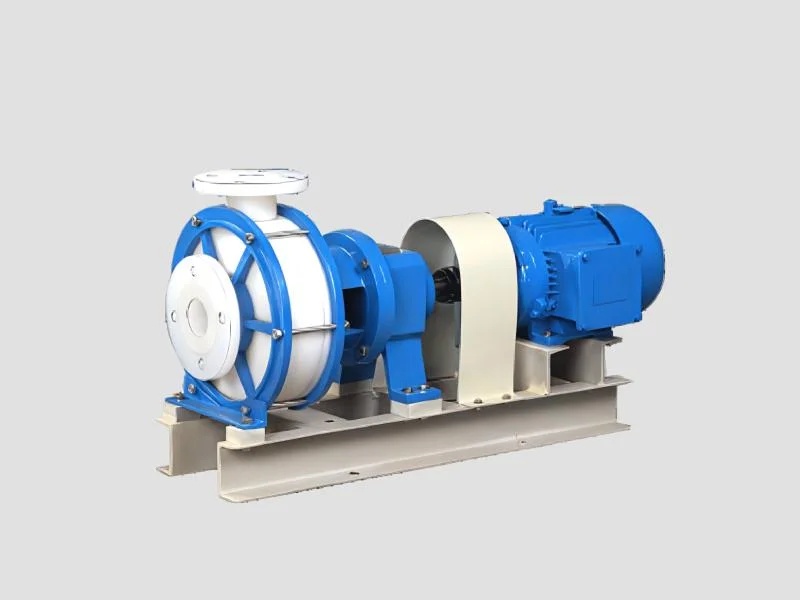
The different types of Chemical Processing Equipment include reactors, mixers, heat exchangers, distillation columns, pumps, and filtration systems. Each type serves a specific function in the chemical manufacturing process and is designed to handle various chemical properties and process requirements.
How do I choose the right Chemical Processing Equipment?
Choosing the right Chemical Processing Equipment involves assessing your specific processing needs, including the type of chemicals, production capacity, and desired outcomes. It's also important to consider factors such as equipment compatibility, maintenance requirements, and industry standards.
What are the standard specifications for Chemical Processing Equipment?
Standard specifications for Chemical Processing Equipment typically include material composition, operating temperature and pressure, capacity, and safety features. Additionally, equipment must comply with relevant industry regulations and standards to ensure safe and efficient operation.
What is the price range for Chemical Processing Equipment?
The price range for Chemical Processing Equipment can vary widely based on the type, specifications, and manufacturer. Generally, prices can range from a few thousand to several hundred thousand dollars, depending on the complexity and technology used in the equipment.
What quality standards apply to Chemical Processing Equipment?
Chemical Processing Equipment must adhere to various quality standards such as ISO 9001, ASME standards, and other industry-specific certifications. These standards ensure that the equipment meets safety, efficiency, and reliability requirements for chemical processing.
Where can I find Chemical Processing Equipment suppliers in India?
You can find Chemical Processing Equipment suppliers in India through B2B marketplaces like Pepagora, industry trade shows, and online directories. Additionally, many manufacturers have websites that provide detailed information about their products and services.
Can Chemical Processing Equipment be customized?
Yes, many manufacturers offer customization options for Chemical Processing Equipment to meet specific client requirements. Customization may include adjustments to size, capacity, materials, and additional features to enhance performance and efficiency.
What is the typical minimum order quantity for Chemical Processing Equipment?
The typical minimum order quantity (MOQ) for Chemical Processing Equipment varies by manufacturer and type of equipment. Generally, MOQs can range from a single unit for specialized items to larger quantities for standard equipment.
What is the typical lead time for Chemical Processing Equipment?
The typical lead time for Chemical Processing Equipment can range from a few weeks to several months, depending on the complexity of the equipment and the manufacturer's production schedule. It's advisable to consult directly with suppliers for accurate lead time estimates.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
