
 IN
Distillation Columns & Units
67 products available
What are Distillation Columns & Units?
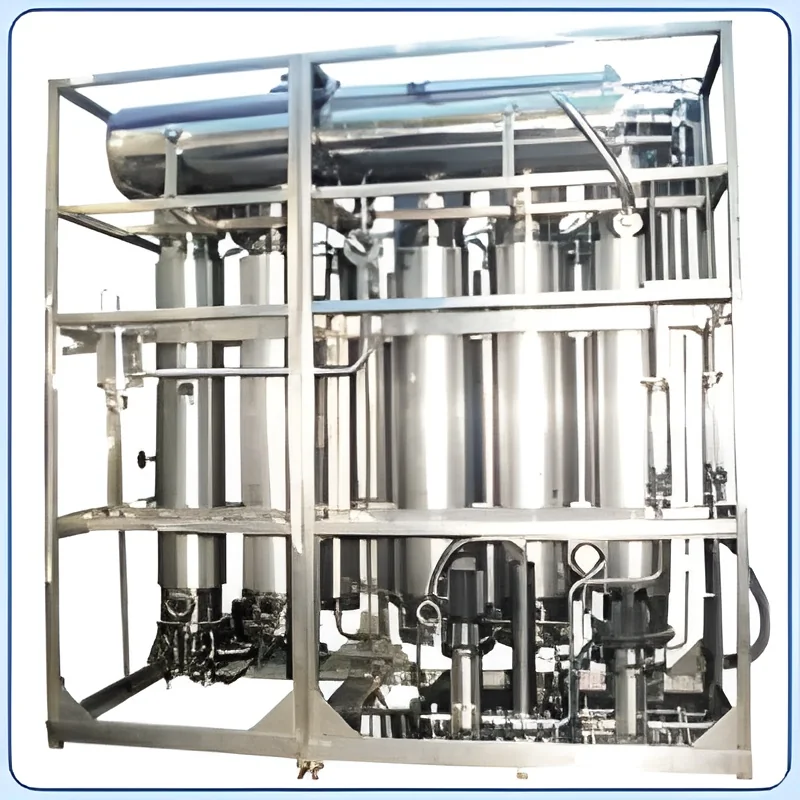
Distillation columns and units are essential equipment used in the industrial separation process. They operate on the principle of vaporization and condensation to separate mixtures based on differences in boiling points. A distillation column is typically a vertical vessel containing packing material or trays that enhance contact between vapor and liquid phases, facilitating efficient separation. These units can vary in size and complexity, ranging from small laboratory setups to large-scale industrial systems.
These systems find primary applications in various sectors, including petrochemicals, pharmaceuticals, food and beverage, and environmental services. In these industries, distillation is employed to purify liquids, recover solvents, and separate valuable components from mixtures. As businesses strive for efficiency and purity in their processes, the demand for advanced distillation columns and units continues to grow. The market is characterized by technological advancements, with manufacturers focusing on improving energy efficiency and reducing operational costs.
Key Features and Specifications
Distillation columns and units come with a range of features that enhance their performance and applicability. Understanding these specifications is crucial for selecting the right unit for specific industrial needs.
Key specifications include:
1. Column Design
- Types include packed columns and tray columns
- Designed for optimal mass transfer and separation efficiency
2. Capacity
- Available in various sizes to accommodate different throughput requirements
- Ranges from small laboratory models to large industrial units
3. Material of Construction
- Common materials include stainless steel and carbon steel
- Chosen based on chemical compatibility and operational conditions
4. Operating Temperature
- Units designed to operate at varying temperature ranges
- Ensures flexibility for different processes
5. Pressure Rating
- Capable of operating under vacuum or high-pressure conditions
- Important for specific separation processes
6. Efficiency Rating
- Measured by the number of theoretical plates or height equivalent to a theoretical plate (HETP)
- Determines separation performance
7. Control Systems
- Advanced systems for monitoring and controlling temperature, pressure, and flow rates
- Enhances operational efficiency and safety
8. Safety Features
- Includes pressure relief valves and emergency shutdown systems
- Ensures safe operation in industrial environments
In summary, understanding the features and specifications of distillation columns and units is vital for optimizing their use in various applications.
Common Applications and Use Cases
Distillation columns and units are utilized across multiple industries, each with unique needs and applications.
1. Petrochemical Industry: These columns are used for separating hydrocarbons in oil refineries, facilitating the production of gasoline, diesel, and other fuels.
2. Pharmaceutical Industry: Distillation is employed to purify solvents and separate active pharmaceutical ingredients from impurities.
3. Food and Beverage Industry: In this sector, distillation is used to produce alcohol, extract flavors, and purify water.
4. Chemical Manufacturing: Distillation units help in separating and purifying chemicals for various processes, ensuring product quality.
5. Environmental Services: These systems are used to treat wastewater and recover solvents, aiding in pollution control efforts.
6. Biotechnology: Distillation is applied in the purification of biological products, ensuring high purity levels for research and development.
7. Research and Development: Small-scale distillation columns are essential in laboratories for testing and refining chemical processes.
Product Variants and Subcategories
Distillation columns and units come in various types to meet specific industrial needs. Although specific subcategories are not available, here are some notable variants.
Continuous Distillation Units: These units operate continuously, allowing for uninterrupted processing. They are suitable for large-scale operations where constant feed and product withdrawal are required.
Batch Distillation Units: Designed for smaller quantities, batch distillation units allow for flexibility in processing different mixtures. They are ideal for applications where varied product requirements exist.
Fractional Distillation Columns: These columns are specifically designed for separating mixtures into their component parts based on different boiling points. They are widely used in the petrochemical and chemical industries.
Benefits and Advantages
Investing in distillation columns and units offers numerous advantages for industrial operations.
1. High Efficiency: These units provide effective separation of components, ensuring high purity levels in the final products.
2. Cost-Effective: Enhanced operational efficiencies can lead to significant cost savings in terms of energy and material usage.
3. Versatility: Distillation columns can be tailored to handle various mixtures, making them suitable for diverse applications.
4. Automation Potential: Advanced control systems enable automation, reducing manual intervention and improving process reliability.
5. Environmental Compliance: Efficient distillation processes can help industries meet regulatory requirements by minimizing waste and emissions.
6. Scalability: Units can be designed to scale according to production needs, from small laboratory setups to large industrial systems.
Buying Guide for B2B Buyers
When sourcing distillation columns and units, it is essential to consider several key factors to ensure an informed purchase.
1. Quality Assessment: Evaluate the manufacturing quality and materials used in the construction of the unit. Look for certifications and compliance with industry standards.
2. Supplier Verification: Vet potential suppliers by checking their reputation, previous projects, and customer feedback to ensure reliability.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities to align with your budget and operational needs.
4. Delivery and Lead Times: Confirm the supplier's ability to meet your delivery requirements and the expected lead times for production and shipping.
5. Compliance Requirements: Ensure that the distillation columns meet all necessary regulatory and safety standards specific to your industry.
Compliance and Certifications
Compliance and certifications are crucial in ensuring the quality and safety of distillation columns and units. Key quality standards include ISO 9001, which focuses on quality management systems, and HACCP, which is critical in food and beverage applications.
Many distillation units also hold CE certification, indicating compliance with European safety standards. This is important for manufacturers aiming to access European markets.
Safety and testing requirements often involve thorough evaluations of the equipment to ensure it can operate safely under specified conditions. Additionally, regional compliance considerations may vary, so it is essential to be aware of local regulations that may impact the design and operation of these units.
Why Source Distillation Columns & Units from Pepagora?
Pepagora provides an excellent platform for sourcing distillation columns and units, offering several key advantages for B2B buyers.
Verified Supplier Network: Pepagora ensures that all suppliers in its network have been thoroughly vetted for credibility and reliability. This gives buyers confidence in the quality of the products offered.
Streamlined RFQ Process: The request for quotation (RFQ) system simplifies the procurement process. Buyers can easily compare prices and specifications from multiple suppliers, saving time and effort.
Trade Assurance and Support: Pepagora offers buyer protection services, ensuring that transactions are secure and that buyers receive the products as promised. This support minimizes risks associated with purchasing industrial equipment.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora connects buyers with local and regional suppliers, enhancing accessibility and reducing shipping times. This geographic reach benefits businesses looking for timely and efficient sourcing solutions.

Frequently Asked Questions
What are Distillation Columns & Units?
Distillation Columns & Units are industrial equipment used for separating mixtures based on differences in their volatilities. They operate on the principle of distillation, which involves heating a liquid to create vapor and then cooling it to separate the components.
What are the different types of Distillation Columns & Units?
The main types of Distillation Columns & Units include continuous columns, batch columns, packed columns, and tray columns. Each type serves specific applications and varies in design, efficiency, and operational methodology.
How do I choose the right Distillation Columns & Units?
Choosing the right Distillation Columns & Units involves considering factors such as the nature of the mixture, required separation efficiency, capacity, and available space. It is also important to assess the operating conditions and the specific application needs.
What are the standard specifications for Distillation Columns & Units?
Standard specifications for Distillation Columns & Units typically include column diameter, height, number of trays or packing, material of construction, and design pressure and temperature. These specifications can vary based on the application and industry requirements.
What is the price range for Distillation Columns & Units?
The price range for Distillation Columns & Units can vary widely based on size, complexity, and manufacturer. Generally, prices may start from a few lakhs for smaller units and can go up to several crores for large, specialized systems.
What quality standards apply to Distillation Columns & Units?
Quality standards for Distillation Columns & Units often include ISO certifications, as well as adherence to industry-specific regulations such as ASME and API standards. These standards ensure safety, reliability, and efficiency in operation.
Where can I find Distillation Columns & Units suppliers in India?
Suppliers of Distillation Columns & Units can be found through online B2B marketplaces like Pepagora, industry trade shows, and specialized equipment manufacturers. Conducting a search for the best Distillation Columns & Units suppliers in India can also yield valuable contacts.
Can Distillation Columns & Units be customized?
Yes, Distillation Columns & Units can often be customized to meet specific operational requirements. Customization may include adjustments in size, materials, and design features to suit particular applications.
What is the typical minimum order quantity for Distillation Columns & Units?
The typical minimum order quantity (MOQ) for Distillation Columns & Units varies by manufacturer and the scale of the units. It can range from one unit for custom installations to larger quantities for standard models.
What is the typical lead time for Distillation Columns & Units?
The typical lead time for Distillation Columns & Units can range from a few weeks to several months, depending on the complexity of the design and the manufacturer's production schedule. Custom orders usually require longer lead times.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
