IN
₹
Description
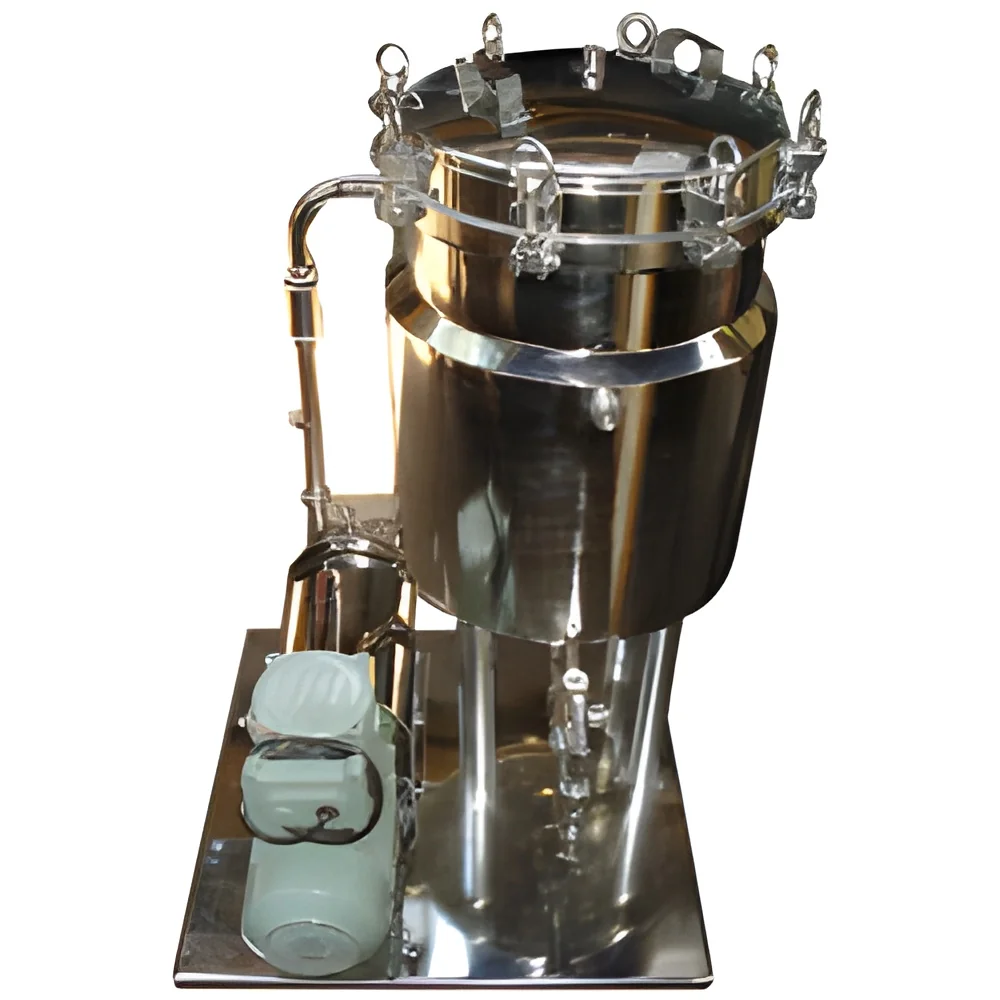
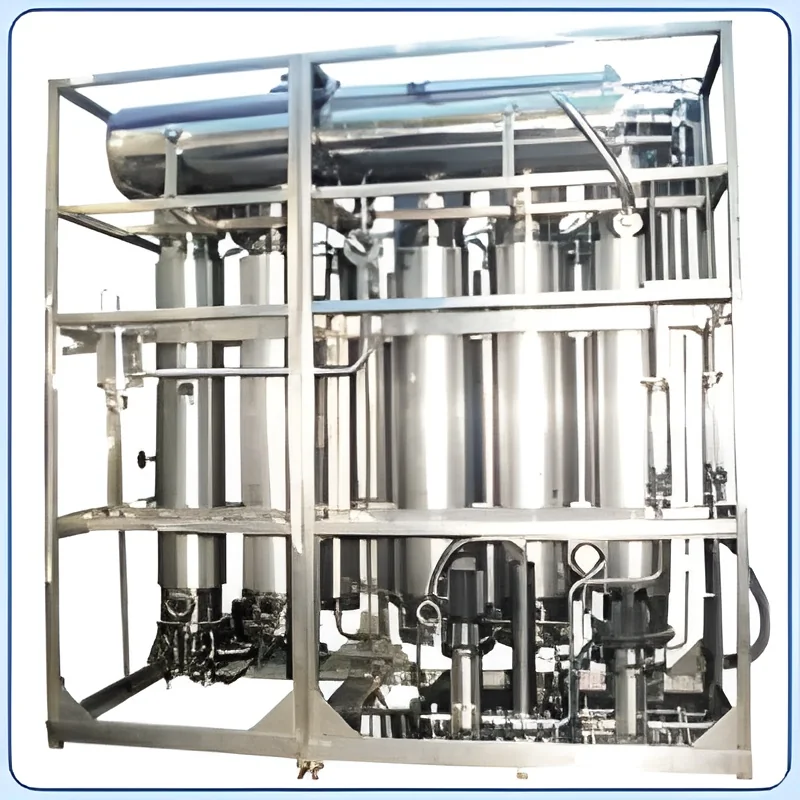
The Industrial Multi Column Distillation Plant represents advanced separation technology designed for precise purification of complex liquid mixtures. This sophisticated system utilizes multiple distillation columns operating in series or parallel configuration to achieve superior purity levels and handle separations that single-column units cannot accomplish. Each column functions as an independent separation stage, enabling targeted removal of specific components based on their distinct boiling points and vapor pressure characteristics. The plant is engineered with high-grade corrosion-resistant materials that withstand continuous operation under demanding thermal and chemical conditions. Advanced control systems provide real-time monitoring of temperature, pressure, and flow rates, ensuring optimal performance throughout operation cycles. The robust construction and precision engineering make this equipment suitable for handling mixtures with close boiling points and those requiring...
The Industrial Multi Column Distillation Plant represents advanced separation technology designed for precise purification of complex liquid mixtures. This sophisticated system utilizes multiple distillation columns operating in series or parallel configuration to achieve superior purity levels and handle separations that single-column units cannot accomplish. Each column functions as an independent separation stage, enabling targeted removal of specific components based on their distinct boiling points and vapor pressure characteristics. The plant is engineered with high-grade corrosion-resistant materials that withstand continuous operation under demanding thermal and chemical conditions. Advanced control systems provide real-time monitoring of temperature, pressure, and flow rates, ensuring optimal performance throughout operation cycles. The robust construction and precision engineering make this equipment suitable for handling mixtures with close boiling points and those requiring multiple purification stages for maximum purity output.

This distillation system serves critical roles across multiple industries where product purity directly impacts quality and compliance. Pharmaceutical manufacturers rely on it for purifying active pharmaceutical ingredients and intermediates to meet strict regulatory standards and ensure product safety. The essential oil industry utilizes its precise separation capabilities to extract and refine volatile compounds from plant materials while preserving their therapeutic properties and aromatic qualities. Chemical processing plants employ this technology for separating solvents, reagents, and specialty chemicals with exceptional accuracy and consistency. Biofuel production facilities depend on its efficient fractional distillation to produce high-concentration alcohol and renewable fuels. Environmental applications include recovering valuable chemicals from industrial waste streams, supporting sustainability initiatives while reducing operational waste and improving resource utilization across various manufacturing sectors.

The business value of this Multi Column Distillation Plant stems from its operational reliability, process efficiency, and performance consistency. The system delivers minimal downtime through robust construction and intelligent design, reducing operational costs while maximizing output quality and production throughput. Energy-efficient operation with integrated heat recovery systems significantly lowers utility expenses, contributing to better cost management and environmental compliance. The durable construction minimizes maintenance requirements and extends equipment service life, providing long-term operational stability and predictable performance. These combined advantages deliver substantial return on investment through improved product yield, reduced material waste, and enhanced product value in competitive markets. The equipment's proven reliability, backed by rigorous testing protocols and quality assurance measures, ensures safe operation under demanding industrial conditions, making it a trusted solution for businesses prioritizing process optimization and quality consistency.

Key Features:
- Multiple distillation columns configured for complex separations and high-purity outputs
- Advanced control systems enabling precise monitoring of temperature, pressure, and flow parameters
- Customizable design with flexible options for column configuration, size, and material selection
- Constructed from corrosion-resistant industrial-grade materials ensuring durability and longevity
- Energy-efficient operation incorporating heat integration and process optimization features

Benefits:
- Achieves superior separation accuracy for complex mixtures with close boiling points
- Enhances product purity and consistency meeting stringent industry quality standards
- Reduces operational costs through energy efficiency and minimal maintenance requirements
- Provides reliable continuous operation with robust construction and advanced controls
- Delivers rapid return on investment through improved yields and reduced waste generation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Multi Column Distillation Plants provide precise separation of complex liquid mixtures through multiple purification stages, achieving high-purity outputs essential for industries where separation accuracy is critical. These systems handle diverse chemical compositions with consistent results, supporting continuous operation across various production scales from pilot plants to full industrial facilities.
The advanced multi-column design enables complex separations unattainable with single-column systems, making it ideal for high-value compound production in pharmaceuticals, essential oils, and specialty chemicals. This equipment processes various feedstocks efficiently while maintaining operational flexibility and scalability for different production requirements and volume needs.
- Purifying pharmaceutical intermediates and active ingredients to meet stringent regulatory standards
- Extracting and refining essential oils from botanical sources for aromatherapy and cosmetics
- Separating chemical solvents and reagents in industrial chemical manufacturing processes
- Producing high-purity alcohol and biofuels through efficient fractional distillation
- Recovering valuable compounds from industrial waste streams in environmental operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anmol Pharma Equipments, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Multi Column Distillation Plant For Chemical Separation
Industrial Multi Column Distillation Plant delivers high-efficiency chemical separation and purification for pharmaceuticals, essential oils, and chemical processing with reliable performance and customizable configurations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anmol Pharma Equipments
 Maharashtra, India
Industrial Equipment & MachineryManufacturer