What are Agitators & Stirrer Systems?
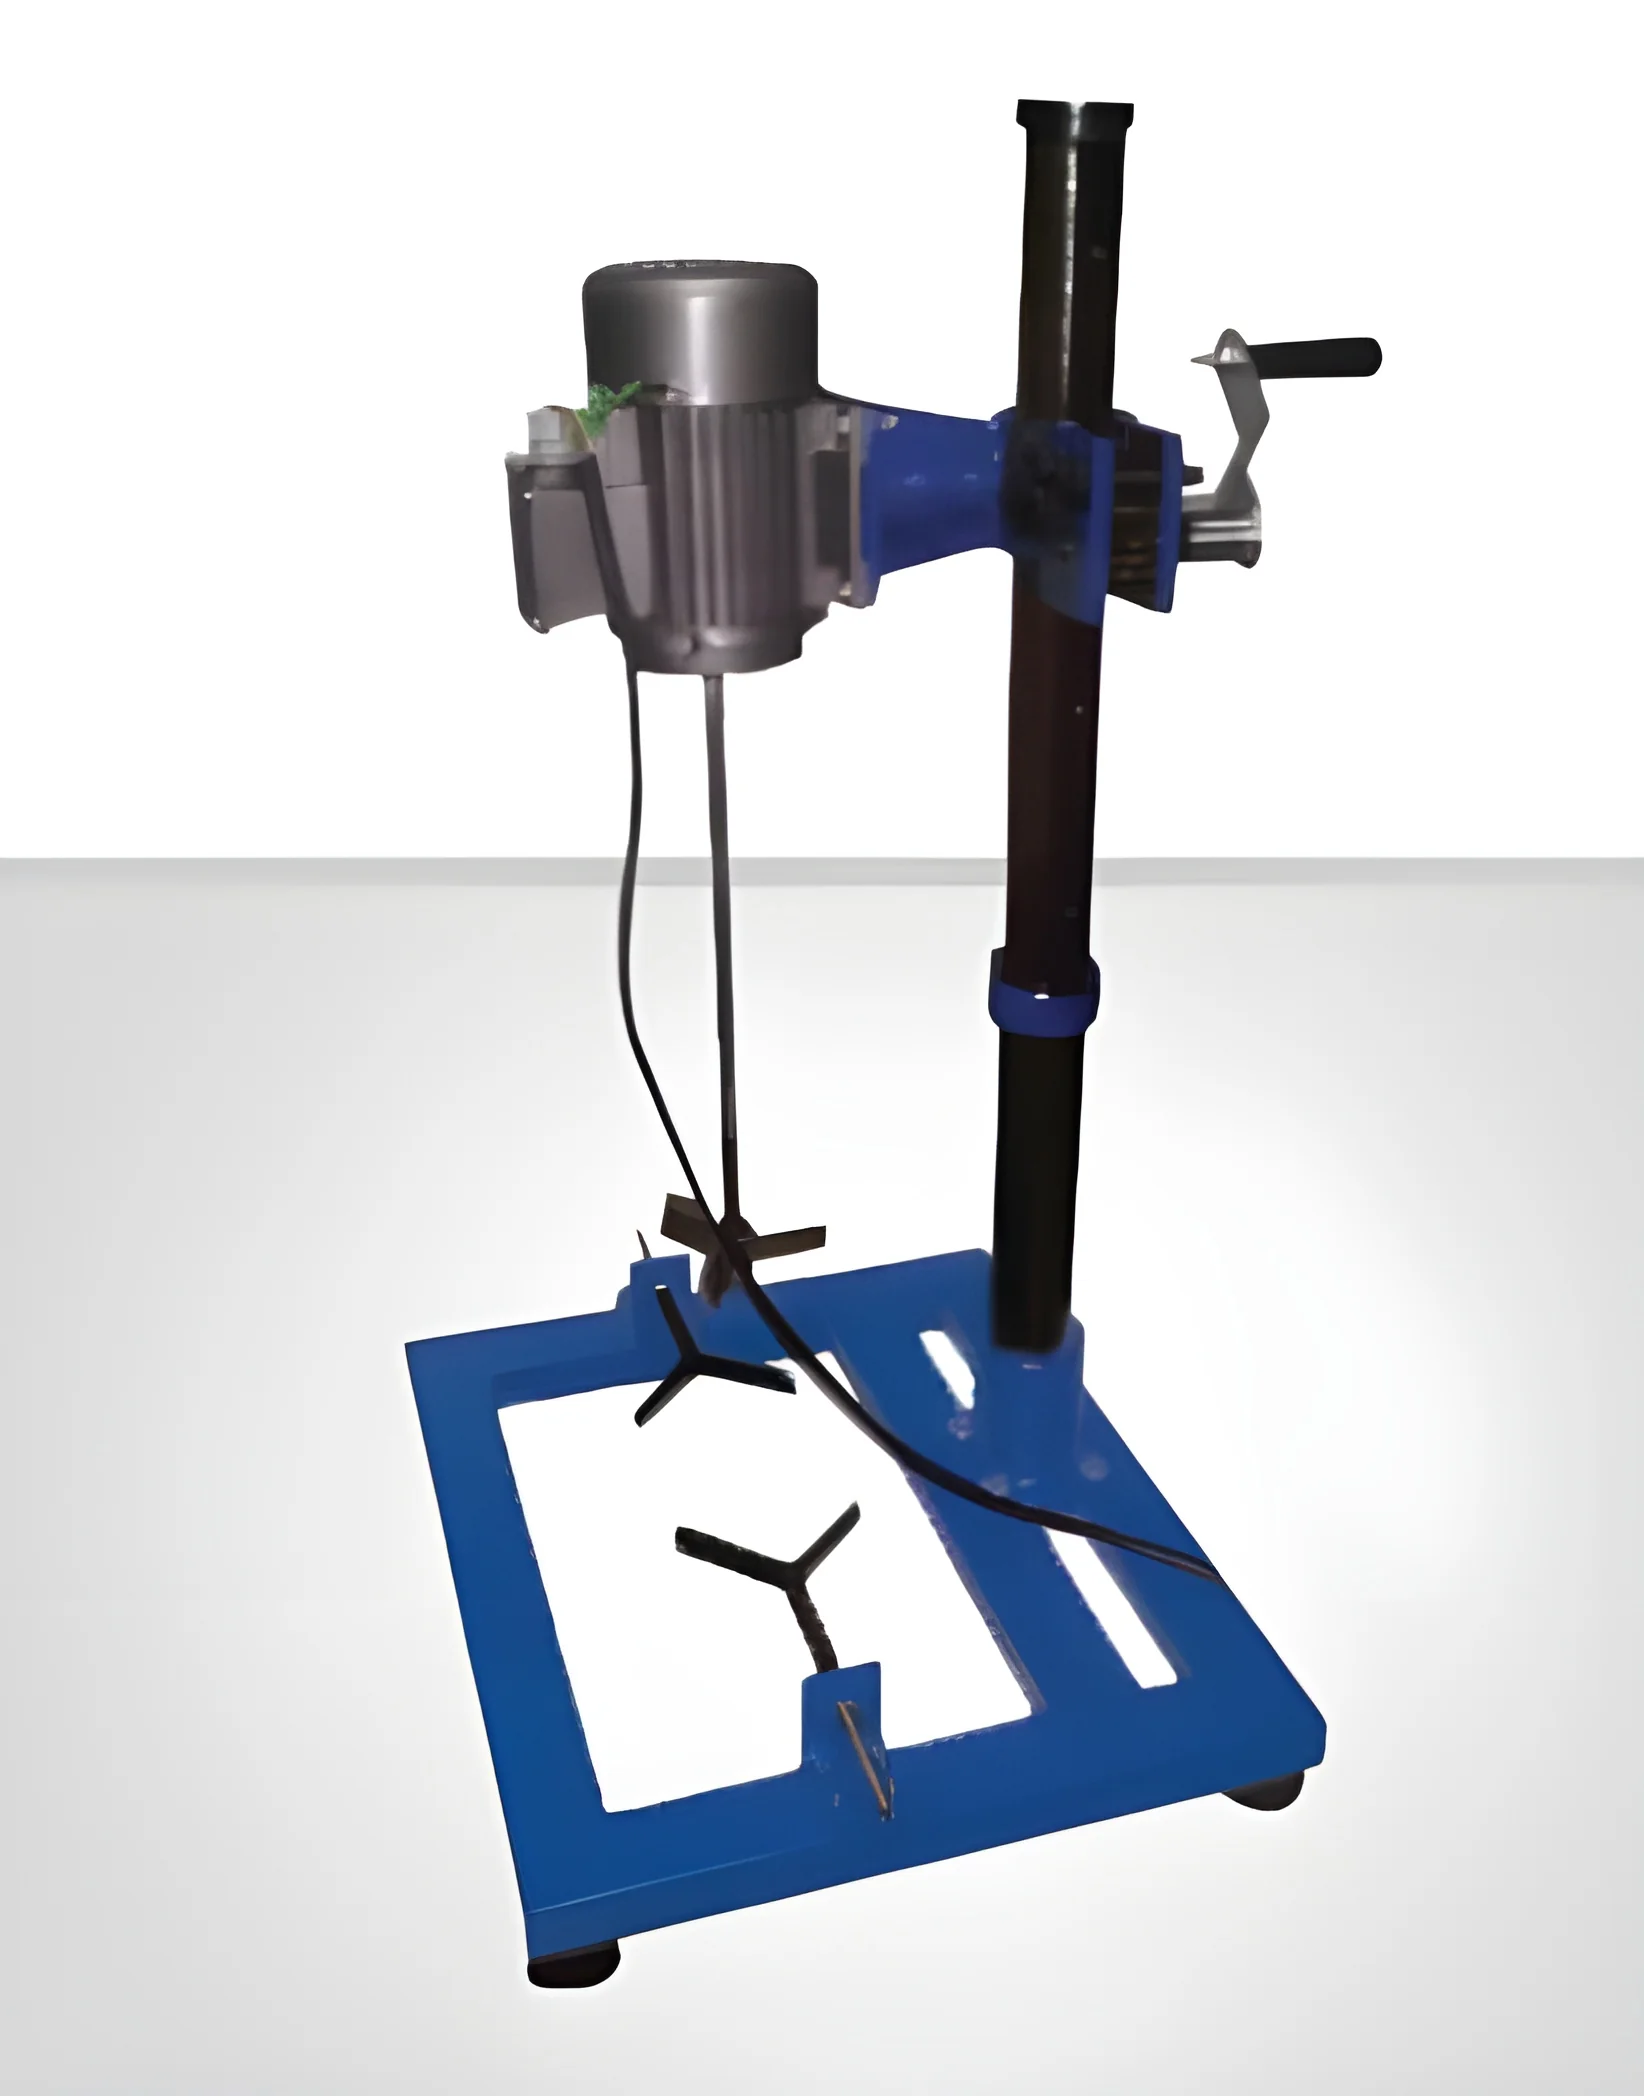
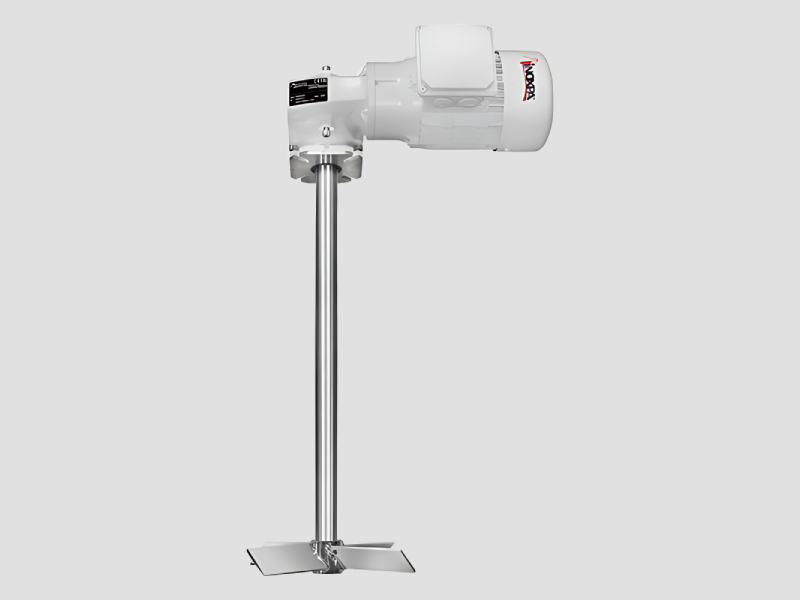
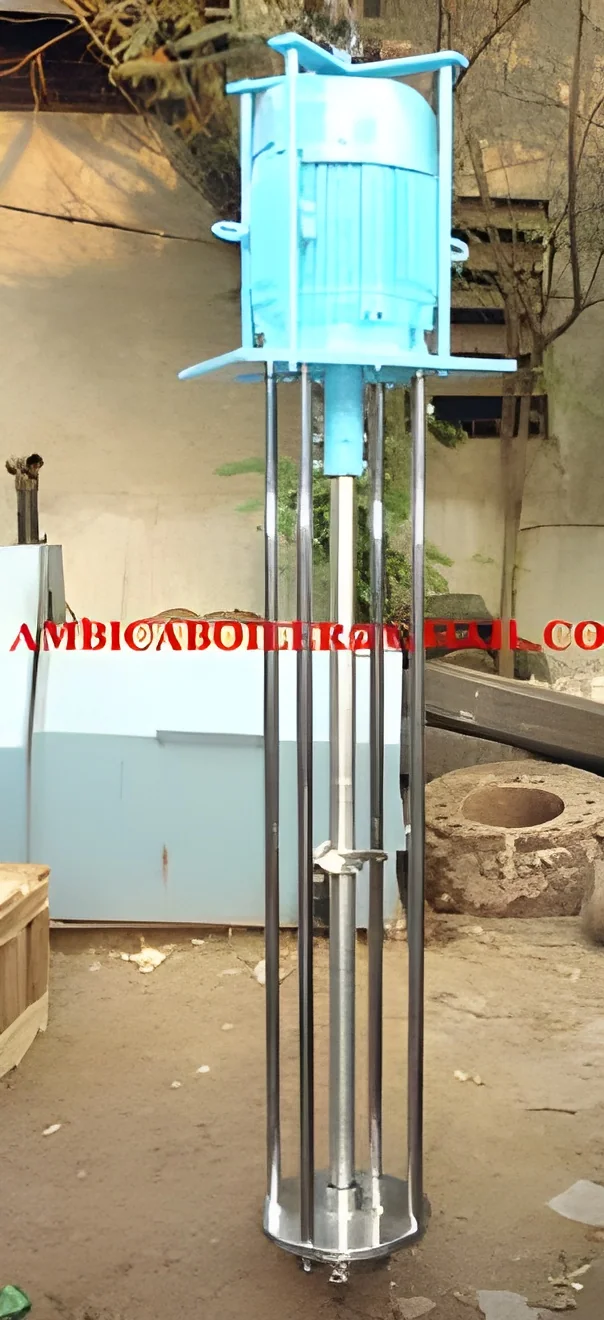
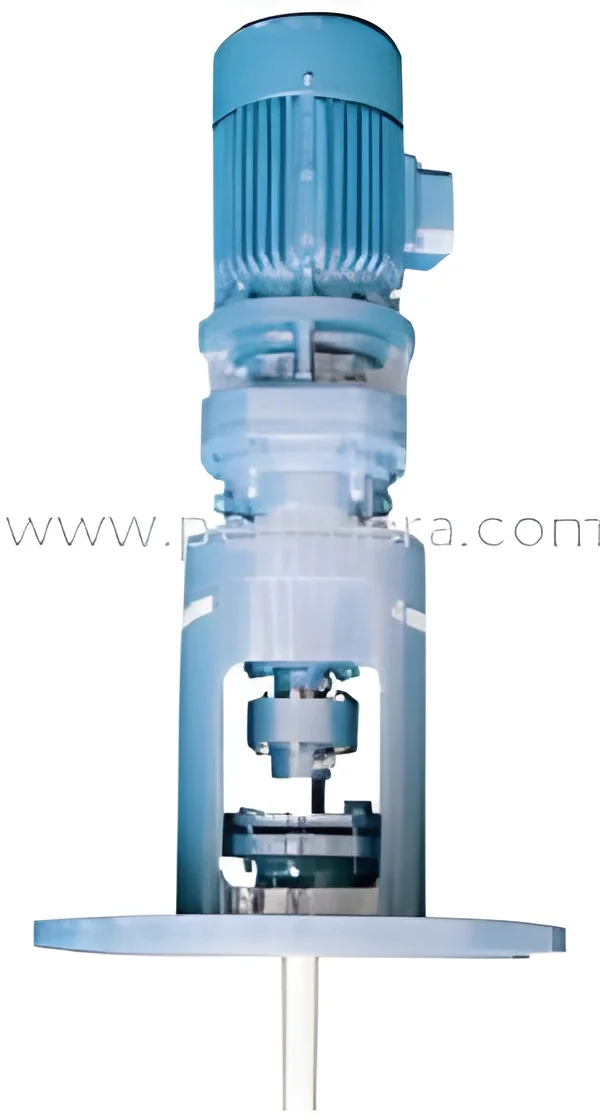
Agitators and stirrer systems are mechanical devices used to mix, blend, or agitate fluids and solids in various industrial processes. These systems employ different types of blades or impellers to create motion within a liquid or slurry, ensuring uniformity and consistency in the final product. They are vital in applications where precise mixing is crucial, such as chemical processing, food and beverage production, and pharmaceuticals.
These systems find extensive use across multiple sectors due to their ability to handle various materials, including viscous substances and slurries. In the chemical industry, they help in reactions and blending of raw materials. In food production, they ensure even mixing of ingredients, while in pharmaceuticals, they facilitate the preparation of solutions and suspensions. As industries continue to evolve, the demand for efficient and reliable agitators and stirrer systems grows, highlighting their importance in production processes.
Key Features and Specifications
Agitators and stirrer systems come with a range of features and specifications tailored to meet diverse industrial needs. These specifications ensure that the systems perform optimally under various conditions, providing reliability and efficiency.
Key specifications include:
1. Drive Type
- Electric or pneumatic options available
- Varying power capacities
2. Speed Range
- Adjustable speed settings for different applications
- Typically ranges from 10 to 1000 RPM
3. Material of Construction
- Options include stainless steel, plastic, and other corrosion-resistant materials
- Suitable for different chemical environments
4. Impeller Design
- Varied designs such as turbine, propeller, or paddle types
- Each design serves specific mixing requirements
5. Tank Compatibility
- Designed to fit various tank sizes and shapes
- Customization options available for specific projects
6. Automation Features
- Integration with control systems for automated processes
- Monitoring capabilities for enhanced operational oversight
In summary, the diverse features and specifications of agitators and stirrer systems make them adaptable to numerous applications, ensuring efficient mixing and blending processes across various industries.
Common Applications and Use Cases
Agitators and stirrer systems are integral to many industries due to their mixing capabilities.
1. Chemical Industry: Utilized for blending raw materials and facilitating chemical reactions, ensuring uniformity and efficiency in production.
2. Food and Beverage: Critical in mixing ingredients, creating emulsions, and ensuring consistent product quality in products like sauces and dressings.
3. Pharmaceutical: Employed in the preparation of solutions and suspensions, maintaining high standards of hygiene and precision.
4. Water Treatment: Used for mixing chemicals in water treatment processes, ensuring effective distribution of treatment agents.
5. Cosmetics: Important for blending formulations, ensuring even consistency in creams, lotions, and other cosmetic products.
6. Paint and Coatings: Facilitates the mixing of pigments and resins, ensuring uniform color and texture in finished products.
7. Oil and Gas: Involved in the mixing of various fluids and chemicals used in extraction and processing.
Product Variants and Subcategories
Agitators and stirrer systems come in various configurations to meet specific industrial demands.
Electric Agitators: These systems are powered by electric motors and are designed for efficiency and precision. They are suitable for a wide range of applications, from low to high viscosity materials.
Pneumatic Stirrer Systems: Utilizing compressed air for operation, these systems are ideal for environments where electrical equipment may pose a hazard. They provide versatility and are often lightweight.
Portable Agitators: Designed for mobility, these systems can be easily transported between different workstations or locations, making them ideal for smaller operations or pilot projects.
High-Shear Mixers: Specifically designed for high-viscosity applications, these mixers provide intense mixing and are ideal for emulsifying or homogenizing products.
Benefits and Advantages
Agitators and stirrer systems offer numerous benefits that enhance operational efficiency and product quality.
1. Improved Mixing Efficiency: These systems provide consistent and thorough mixing, resulting in uniform products.
2. Versatility: Suitable for a wide range of materials and applications, making them adaptable to various industrial needs.
3. Enhanced Control: Many systems offer adjustable speed and automation features, allowing for precise control over mixing parameters.
4. Durability: Constructed from robust materials, they are designed to withstand harsh operating conditions and long-term use.
5. Reduced Labor Costs: Automation and efficiency reduce the need for manual mixing, saving time and labor costs.
6. Compliance with Standards: Many systems are designed to comply with industry standards, ensuring safety and reliability.
Buying Guide for B2B Buyers
When sourcing agitators and stirrer systems, it is essential to consider several key factors to ensure you select the right equipment for your needs.
1. Quality Assessment: Evaluate the quality of materials and construction. Look for systems that meet industry standards to ensure durability and reliability.
2. Supplier Verification: Vet suppliers by checking their reputation, customer reviews, and certifications. This helps ensure you are working with a reliable partner.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities. This is crucial for budgeting and planning your purchases effectively.
4. Delivery and Lead Times: Inquire about delivery options and lead times to ensure that you can meet your production schedules without delays.
5. Compliance Requirements: Ensure the systems meet relevant regulatory and safety standards. This is vital for maintaining operational compliance and safety.
Compliance and Certifications
Agitators and stirrer systems must adhere to relevant quality and safety standards to ensure consistent performance and safety in operations.
ISO 9001 is a widely recognized standard that emphasizes quality management systems, ensuring that manufacturers maintain high production and service standards.
HACCP (Hazard Analysis and Critical Control Points) is essential in food processing applications, ensuring that systems are designed to minimize risks associated with food safety.
CE certification indicates compliance with European health and safety standards, providing assurance that products are safe for use.
Additionally, safety and testing requirements are crucial for protecting operators and ensuring equipment reliability. Regional compliance considerations may vary, so it is important to check local regulations to ensure adherence.
Why Source Agitators & Stirrer Systems from Pepagora?
Pepagora provides a trusted platform for sourcing agitators and stirrer systems, offering several key advantages to B2B buyers.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, ensuring that you can source high-quality products with confidence.
Streamlined RFQ Process: The request for quotation process is designed to be efficient, allowing buyers to quickly receive competitive quotes from multiple suppliers, facilitating informed decision-making.
Trade Assurance and Support: Pepagora offers buyer protection through its trade assurance program, providing peace of mind in your purchasing decisions.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora ensures geographic reach, making it easier for businesses to access the products they need.
In summary, sourcing agitators and stirrer systems through Pepagora offers a reliable and efficient way to meet your industrial mixing needs while ensuring compliance and quality.

 IN

 India