What are Cleanroom Equipment?
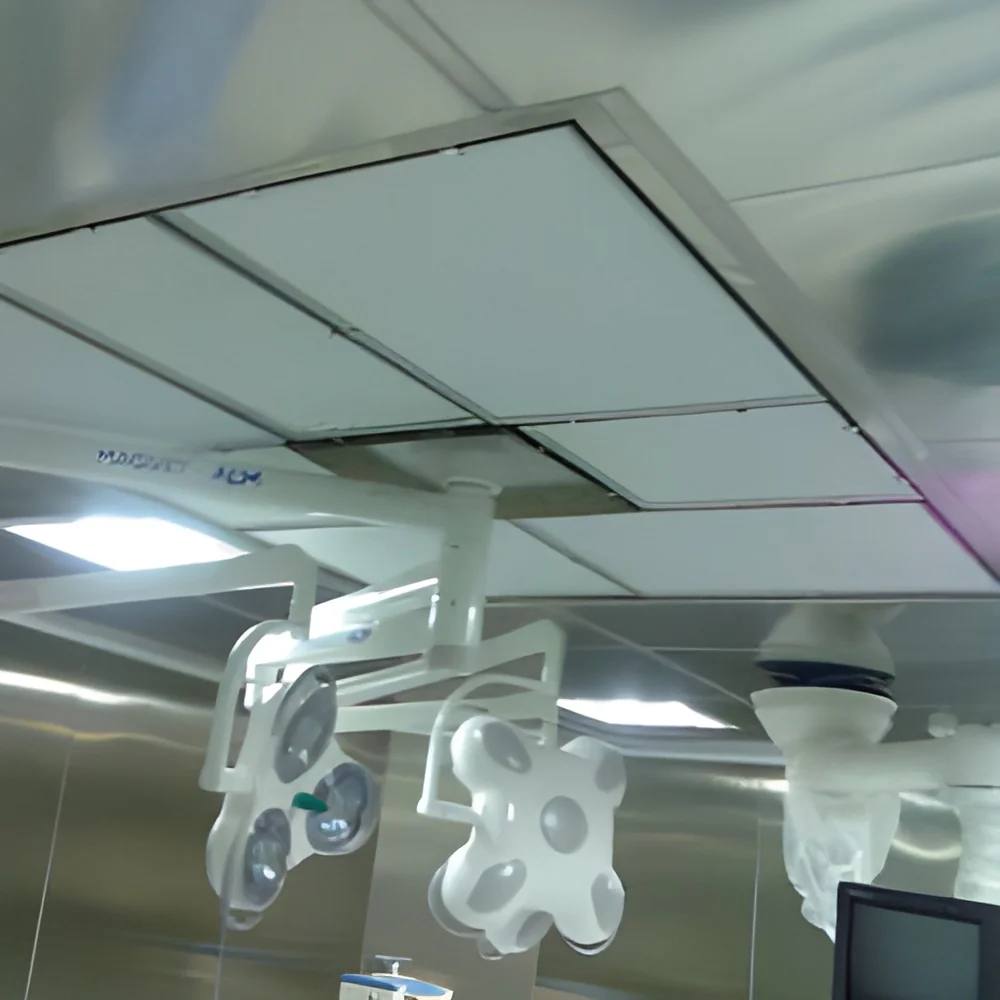
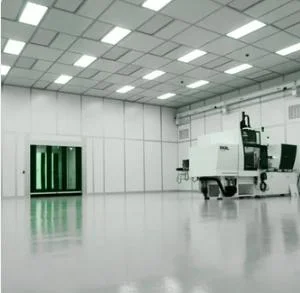
Cleanroom equipment refers to specialized tools and devices designed to maintain controlled environments with minimal contamination. These environments are crucial in various industries where even the smallest particle can compromise product quality and safety. Cleanroom equipment aids in controlling air quality, humidity, temperature, and particulate levels to ensure compliance with stringent industry standards.
The primary uses of cleanroom equipment span across sectors such as pharmaceuticals, biotechnology, electronics, and aerospace. In these industries, maintaining a sterile or controlled environment is essential for manufacturing and research processes. The equipment is employed to facilitate safe product handling, secure sensitive processes, and support regulatory compliance, ultimately ensuring high-quality outcomes.
As industries increasingly prioritize quality and safety, the relevance of cleanroom equipment continues to grow. The market for such equipment is expanding, driven by advancements in technology and stricter regulations. Companies are investing in cleanroom solutions to enhance operational efficiency and product reliability, making cleanroom equipment a critical component in modern manufacturing and research environments.
Key Features and Specifications
Cleanroom equipment encompasses a range of features designed to optimize performance in controlled environments. These features ensure that the equipment meets industry standards while maintaining operational efficiency.
Key specifications include:
1. Air Quality Control
- Ensures low particulate levels and optimal air changes per hour.
- Technical parameters typically range from ISO Class 1 to ISO Class 9.
2. Temperature Regulation
- Maintains consistent temperature levels within specified ranges.
- Technical parameters may vary, but common ranges are 18°C to 25°C.
3. Humidity Control
- Regulates humidity levels to prevent moisture-related contamination.
- Typical parameters often range from 30% to 50% relative humidity.
4. Filtration System
- Utilizes high-efficiency particulate air (HEPA) or ultra-low penetration air (ULPA) filters.
- Filters can capture particles down to 0.3 microns or smaller.
5. Monitoring Capabilities
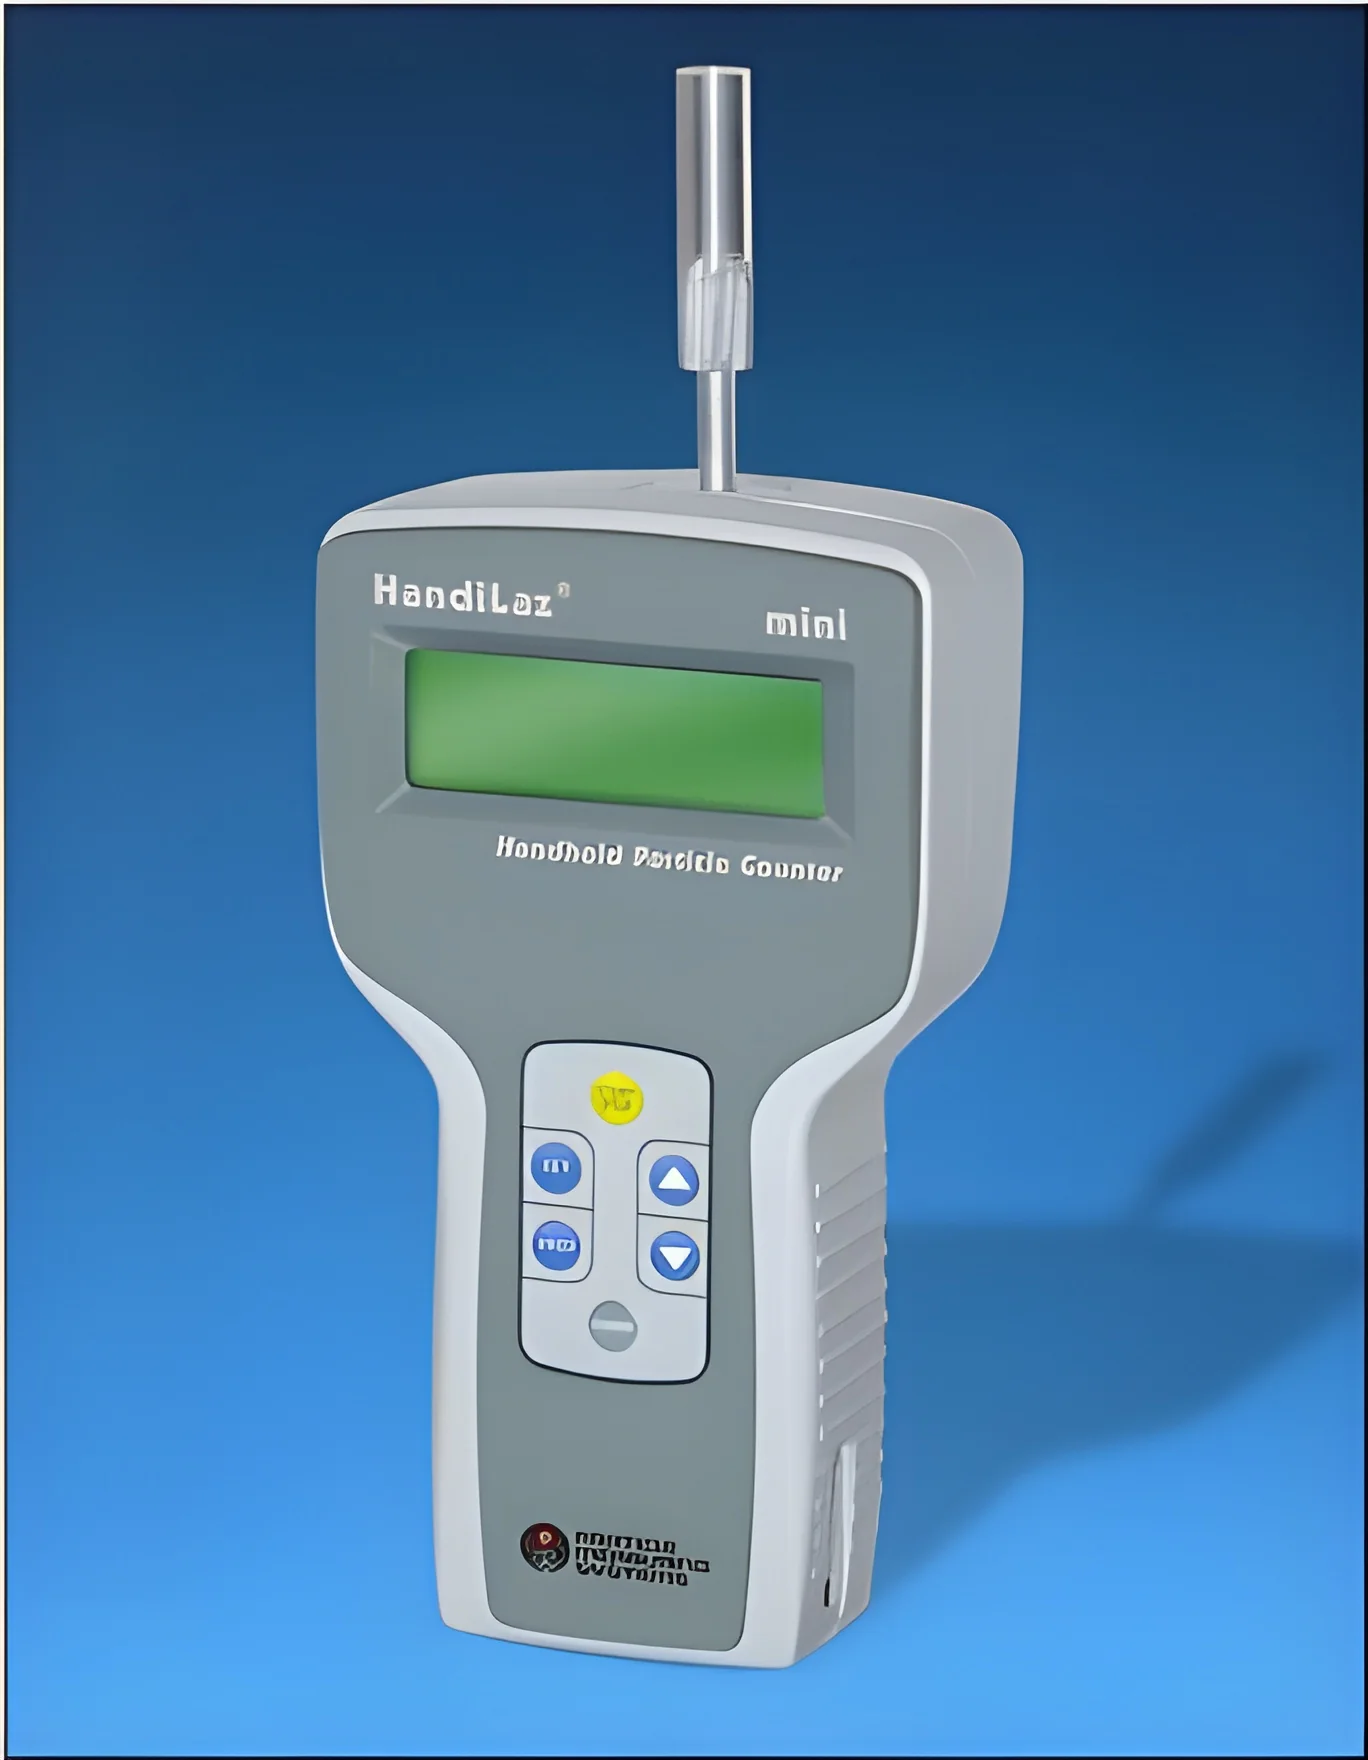
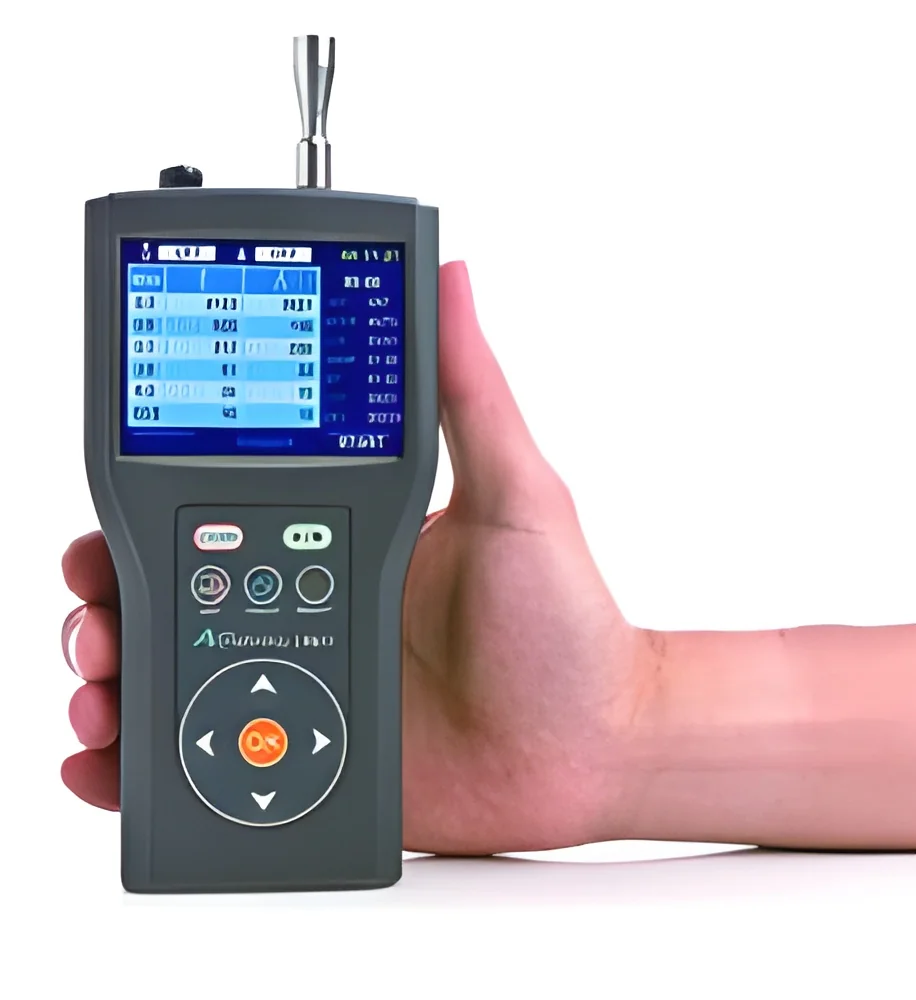
- Includes sensors and alarms to continuously assess environmental conditions.
- Data logging features for compliance documentation.
6. Materials Used
- Constructed from non-porous materials to minimize contamination risk.
- Common materials include stainless steel and specialized plastics.
7. Design Flexibility
- Customizable configurations to meet specific operational needs.
- Modular designs for easy expansion and reconfiguration.
8. Compliance Standards
- Adheres to industry regulations such as ISO 14644 and GMP guidelines.
- CE certification for safety and performance assurance.
In summary, understanding the features and specifications of cleanroom equipment is essential for selecting the right solutions to meet industry requirements and operational goals.
Common Applications and Use Cases
Cleanroom equipment finds applications across multiple sectors, each with unique needs.
1. Pharmaceutical Industry: Cleanroom equipment is vital for drug manufacturing and research. It ensures the integrity of sterile products and compliance with Good Manufacturing Practice (GMP) standards.
2. Biotechnology: In biotechnology labs, cleanrooms help maintain sterile environments for cell cultures and genetic research, safeguarding against contamination.
3. Electronics Manufacturing: Cleanrooms are essential in the production of microchips and electronic components, where even minute particles can lead to product failure.
4. Aerospace: Cleanroom equipment is used in the assembly and testing of aerospace components, where precision and cleanliness are critical.
5. Food Industry: This equipment aids in packaging and processing food products to prevent contamination, ensuring safety and quality.
6. Medical Device Manufacturing: Cleanrooms are crucial for producing medical devices, ensuring they meet stringent quality and safety standards.
7. Research Laboratories: Cleanroom environments support a variety of scientific research applications, providing controlled conditions for experiments.
Product Variants and Subcategories
Cleanroom equipment is diverse, catering to various operational needs within controlled environments.
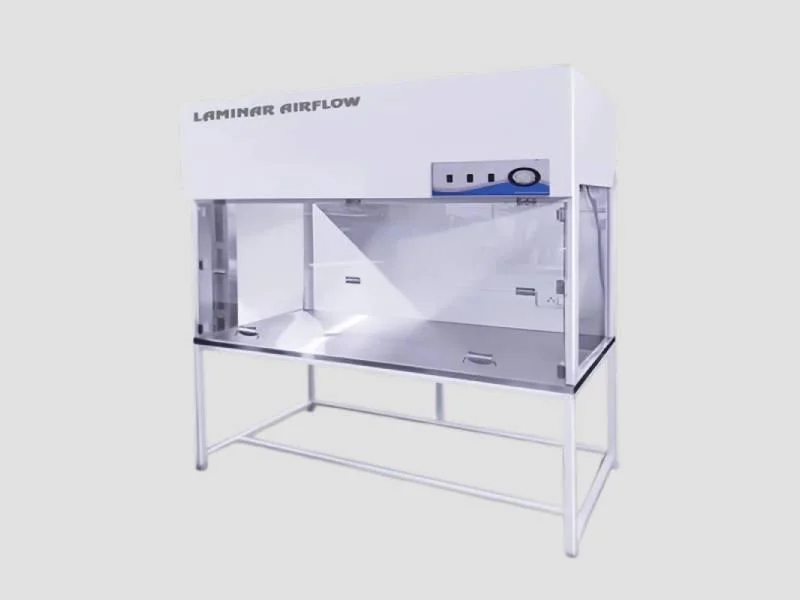
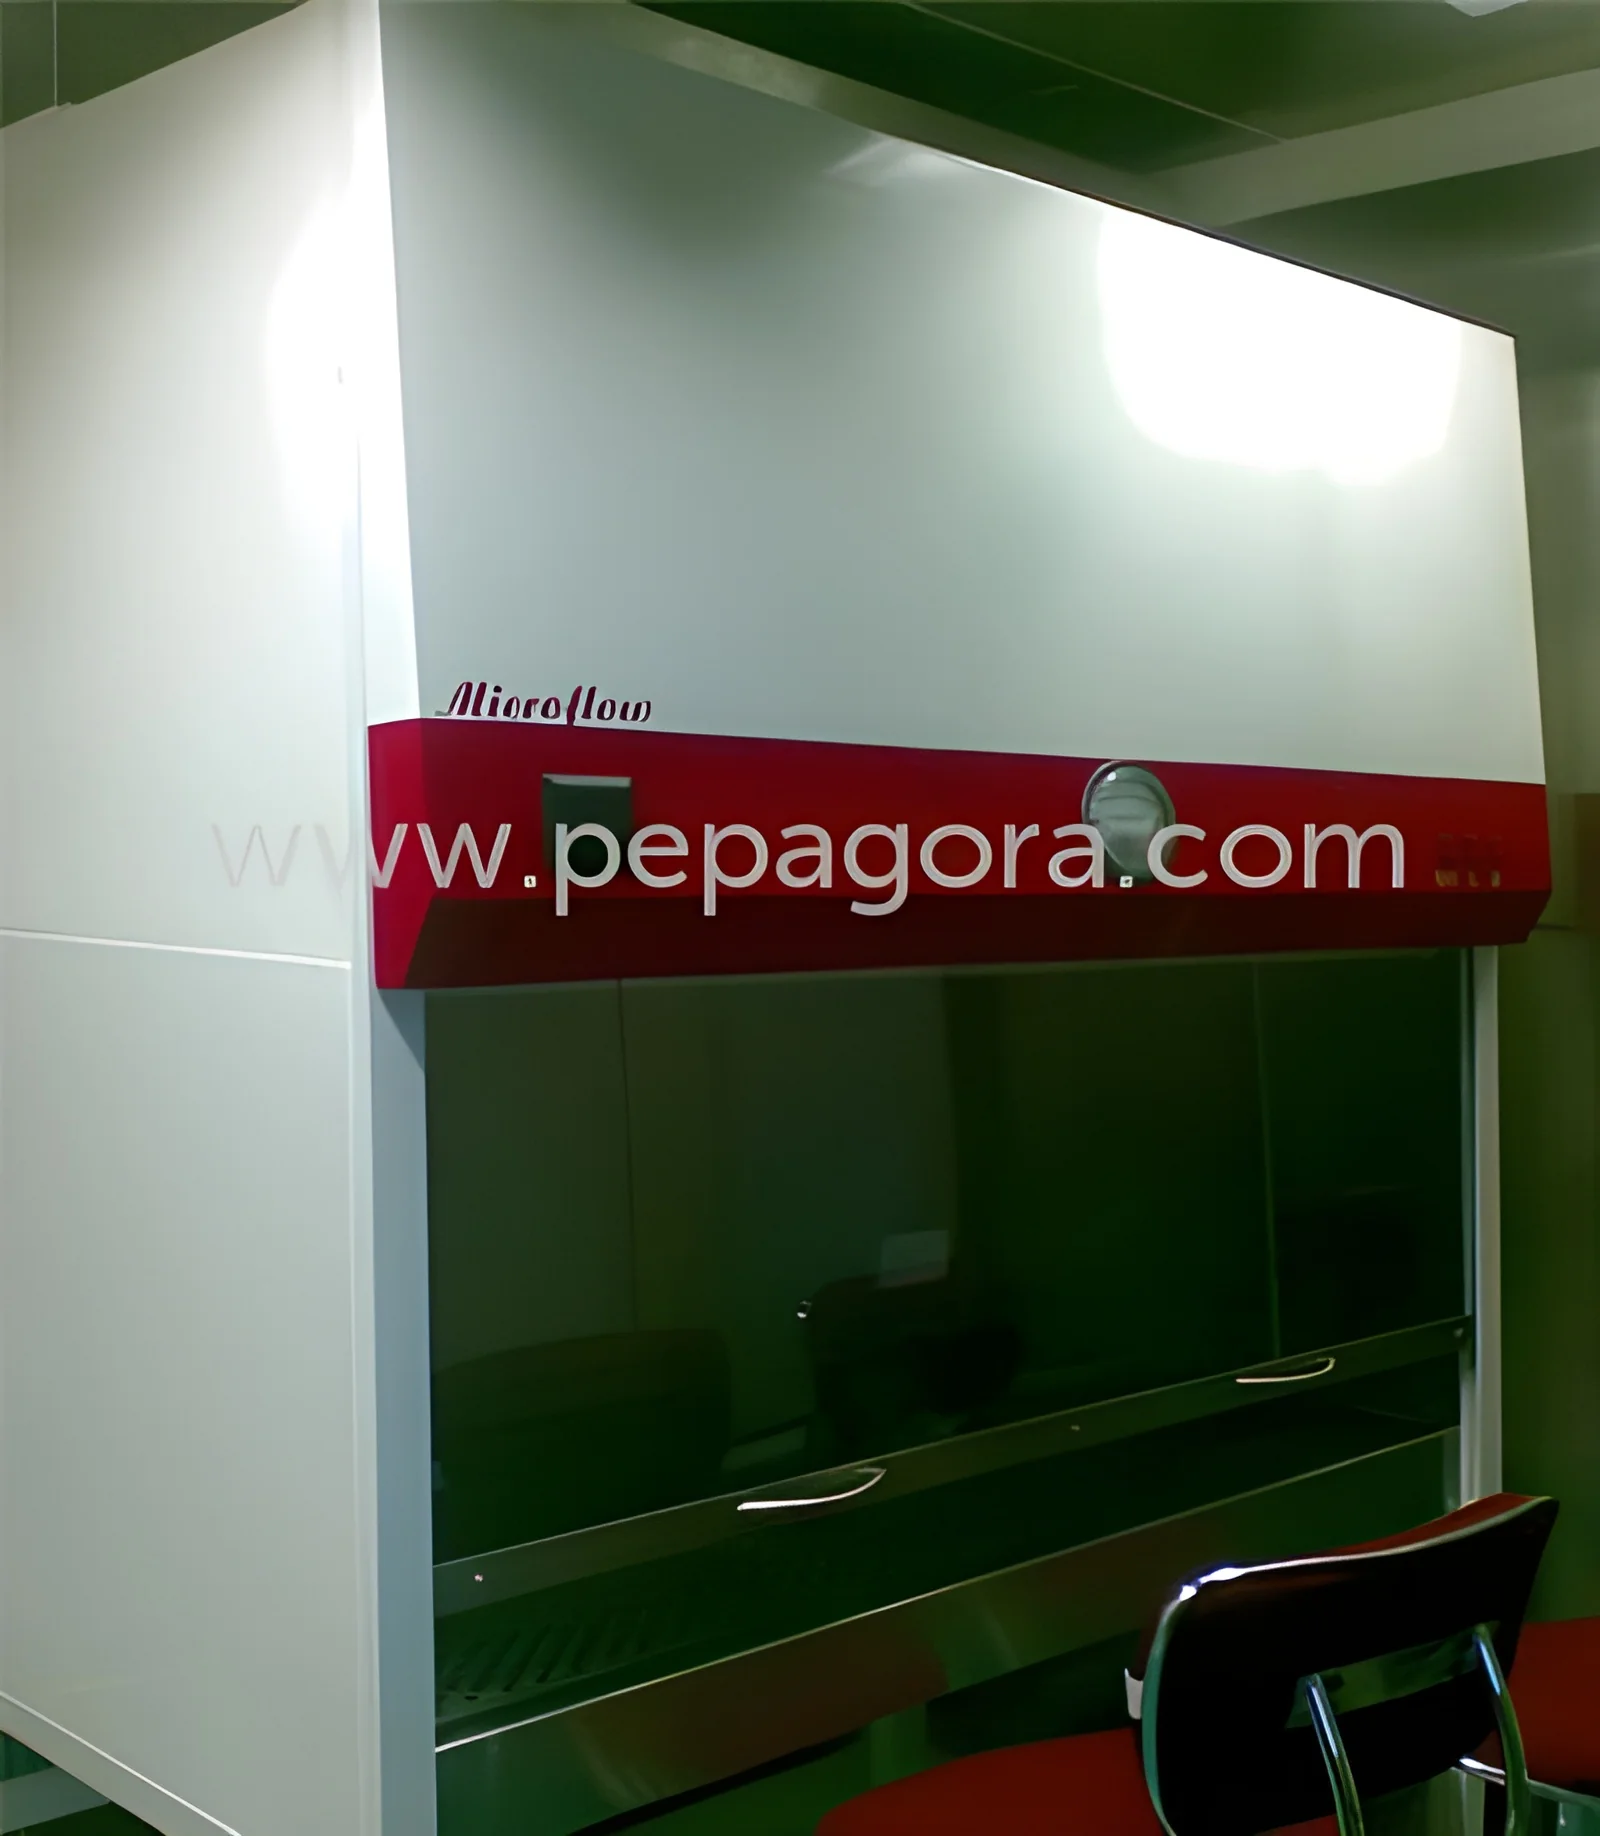
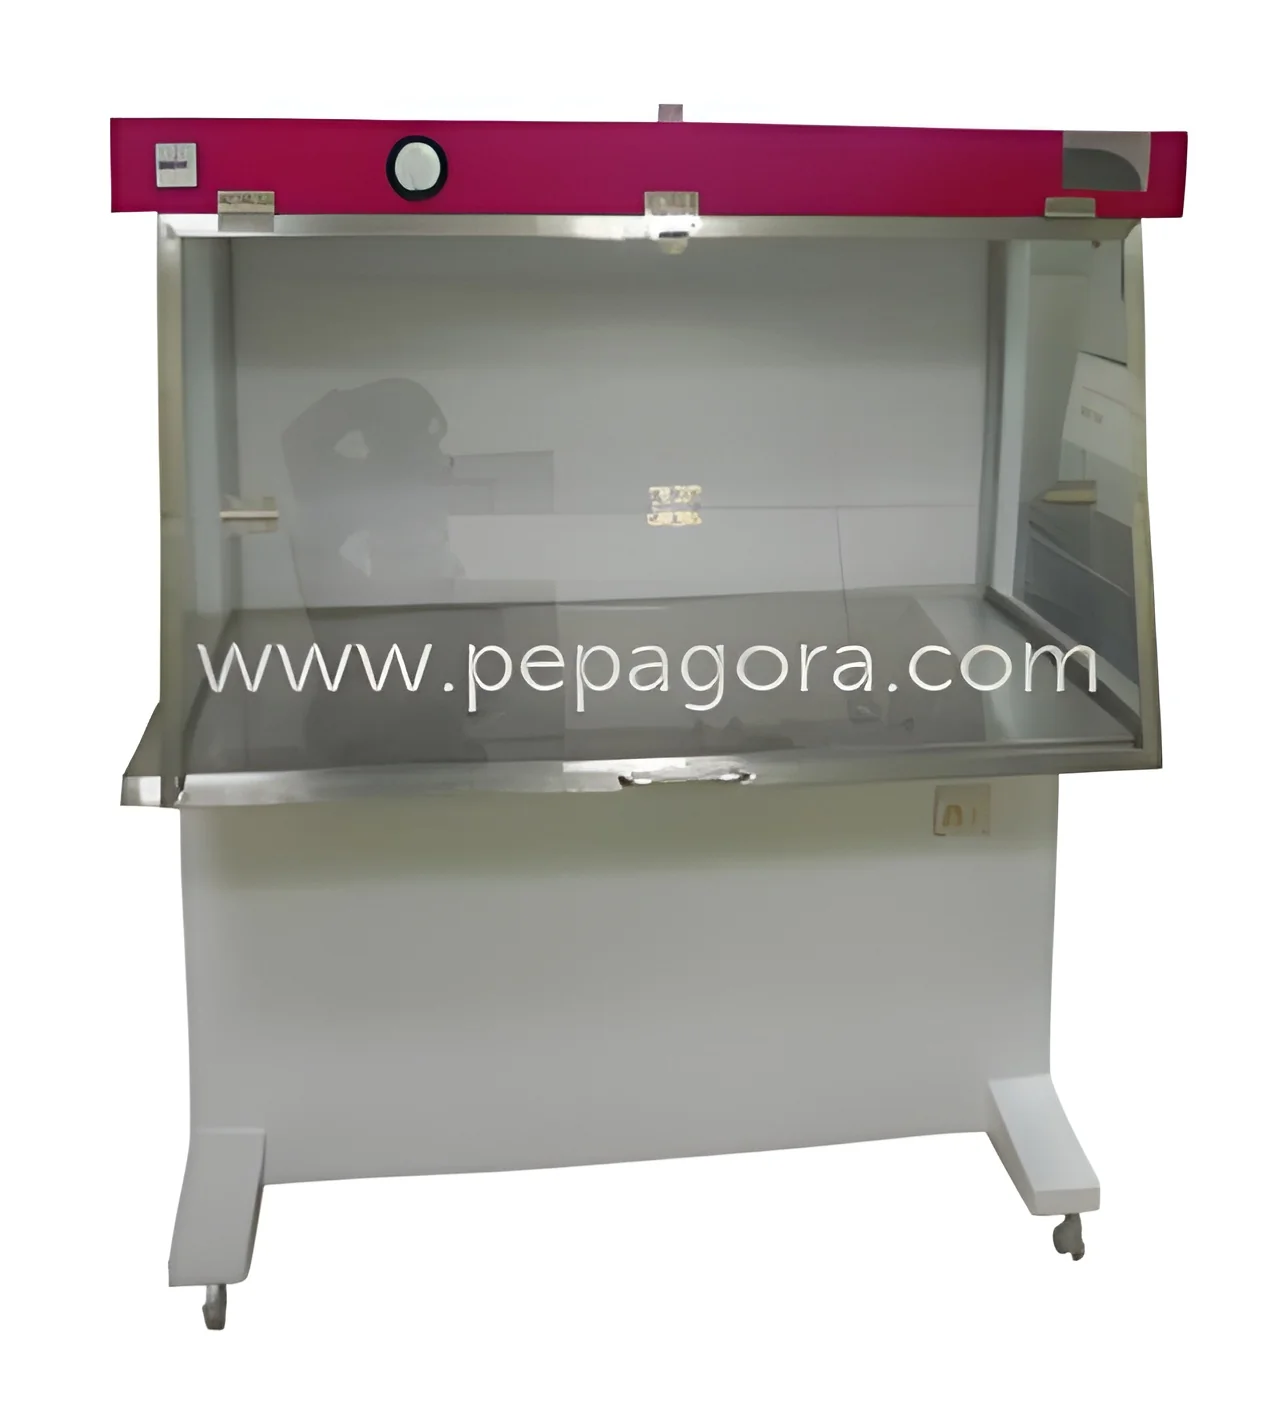
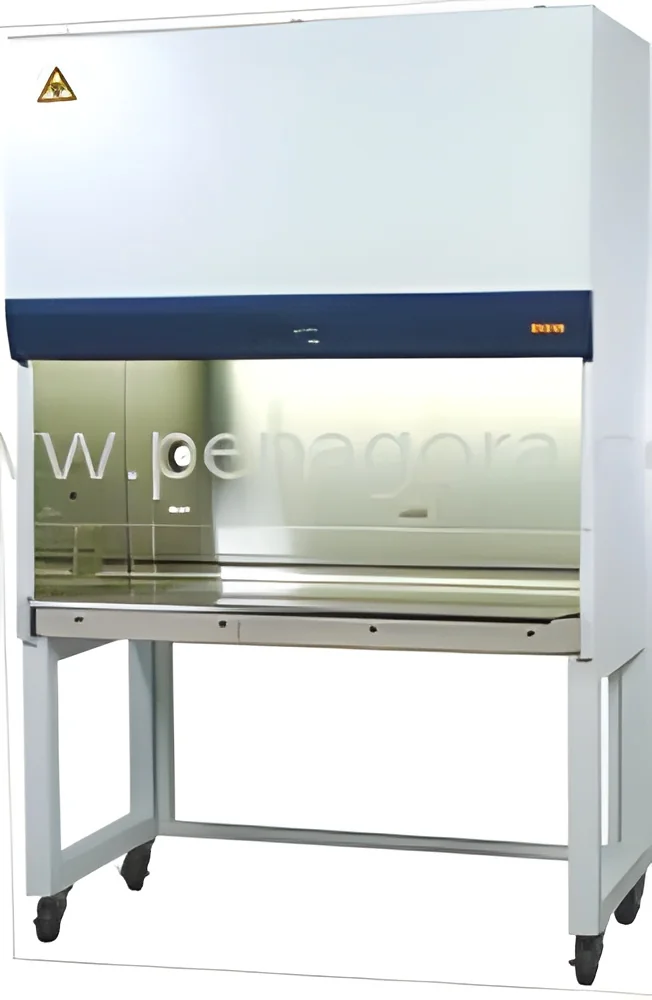
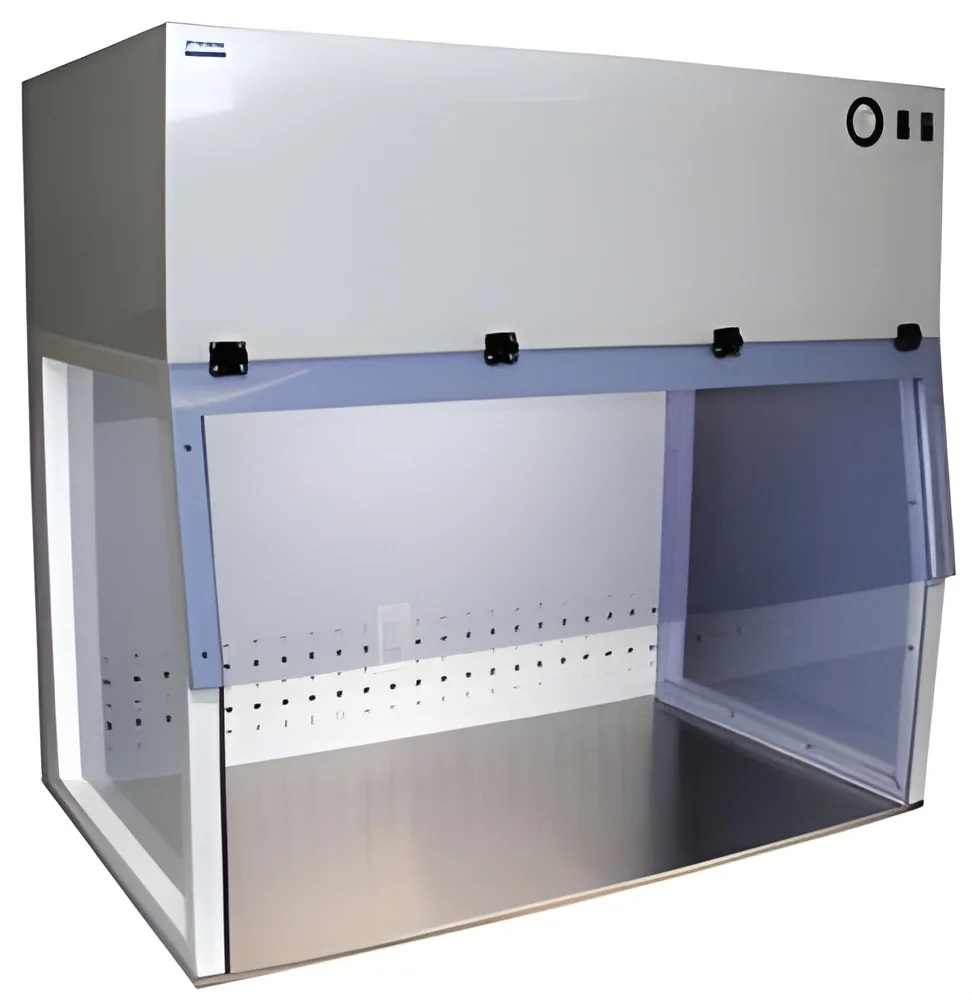
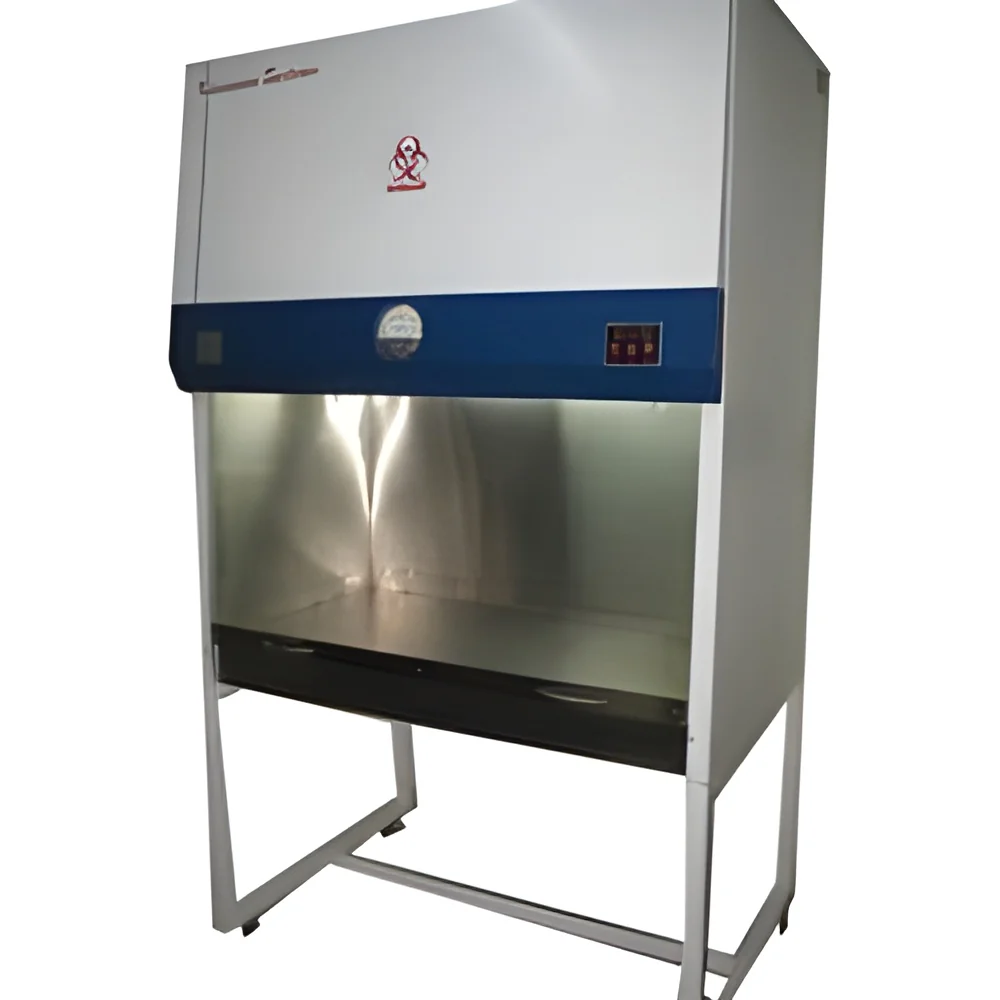
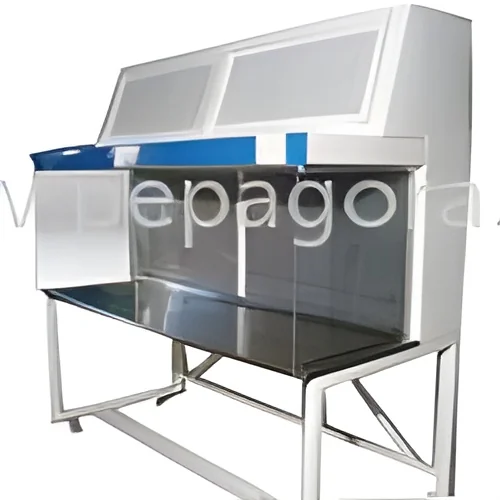
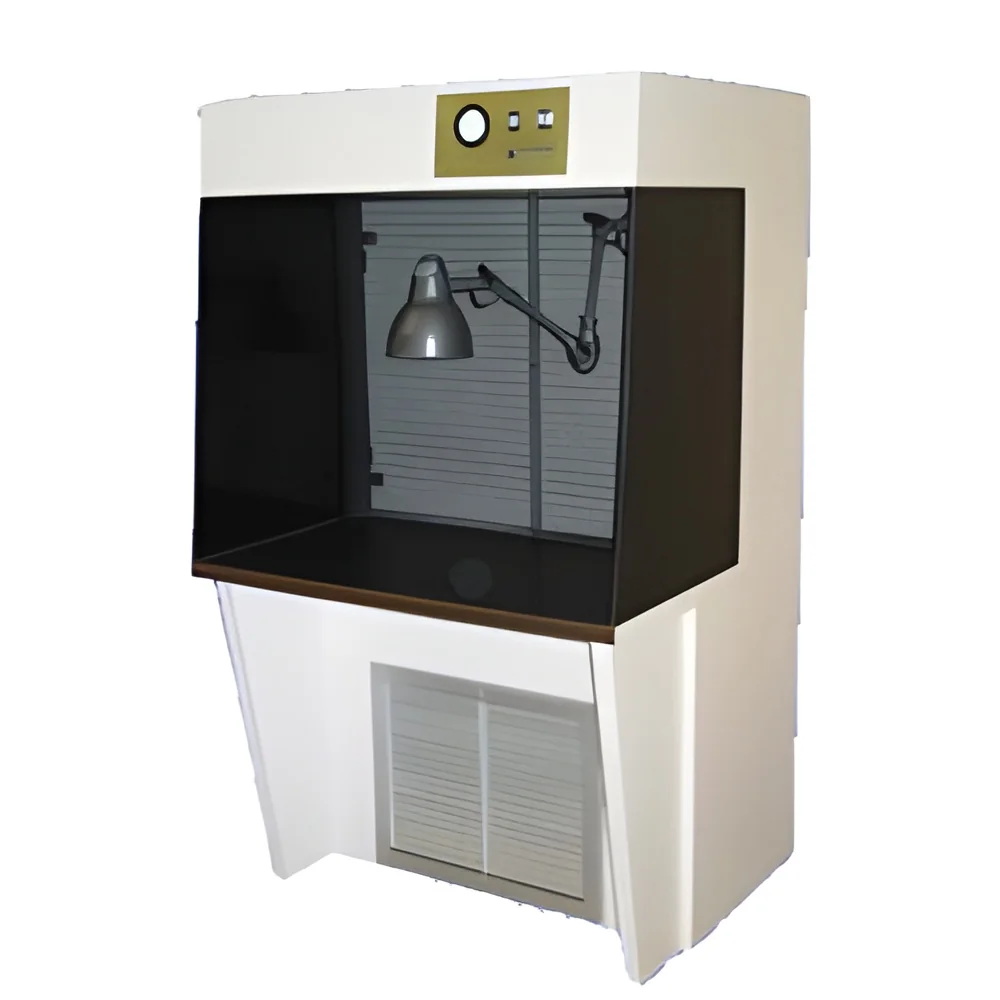
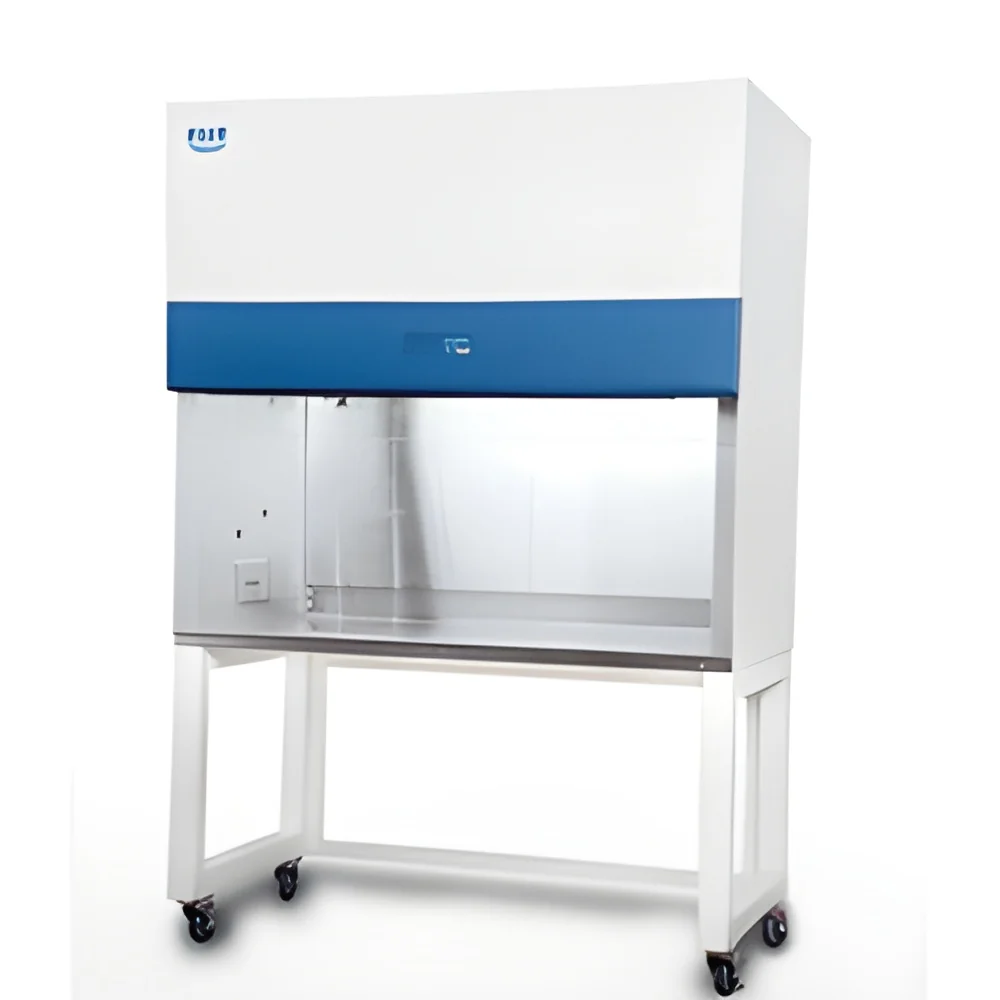
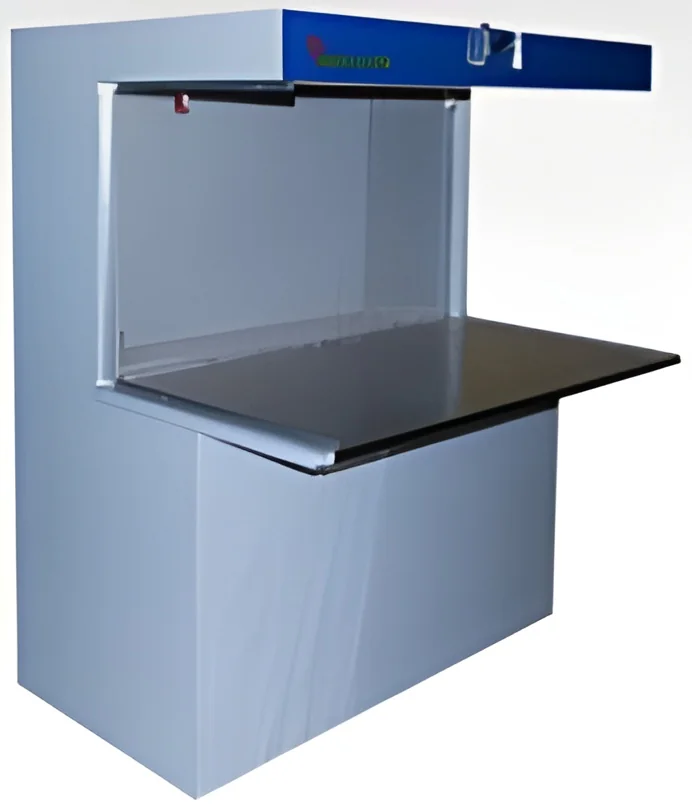
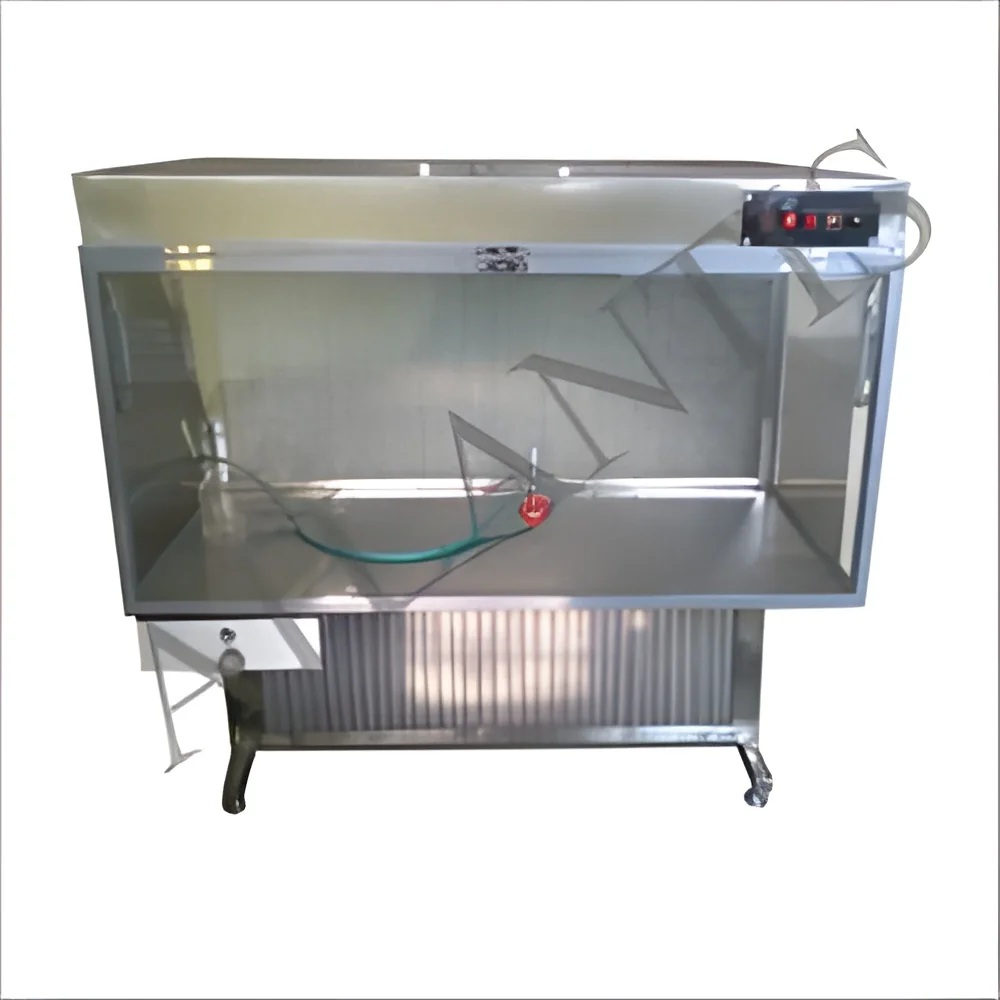
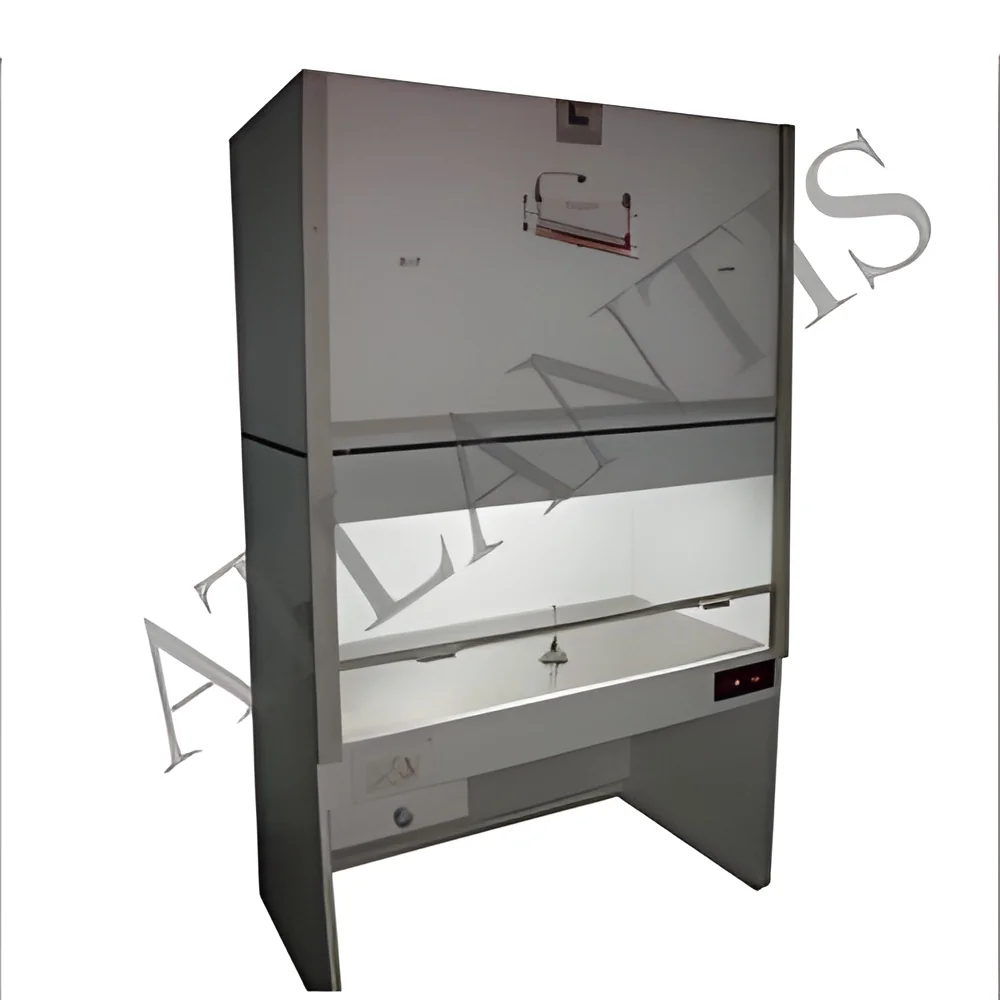
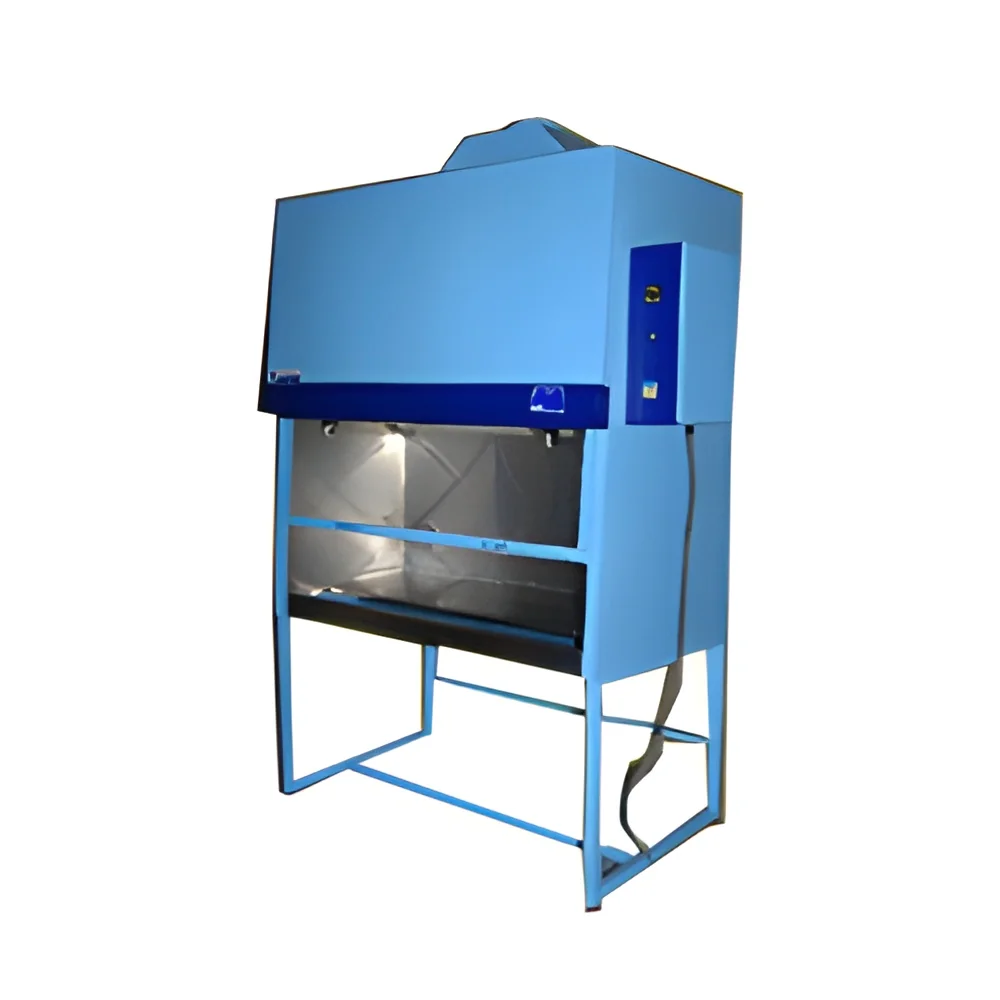
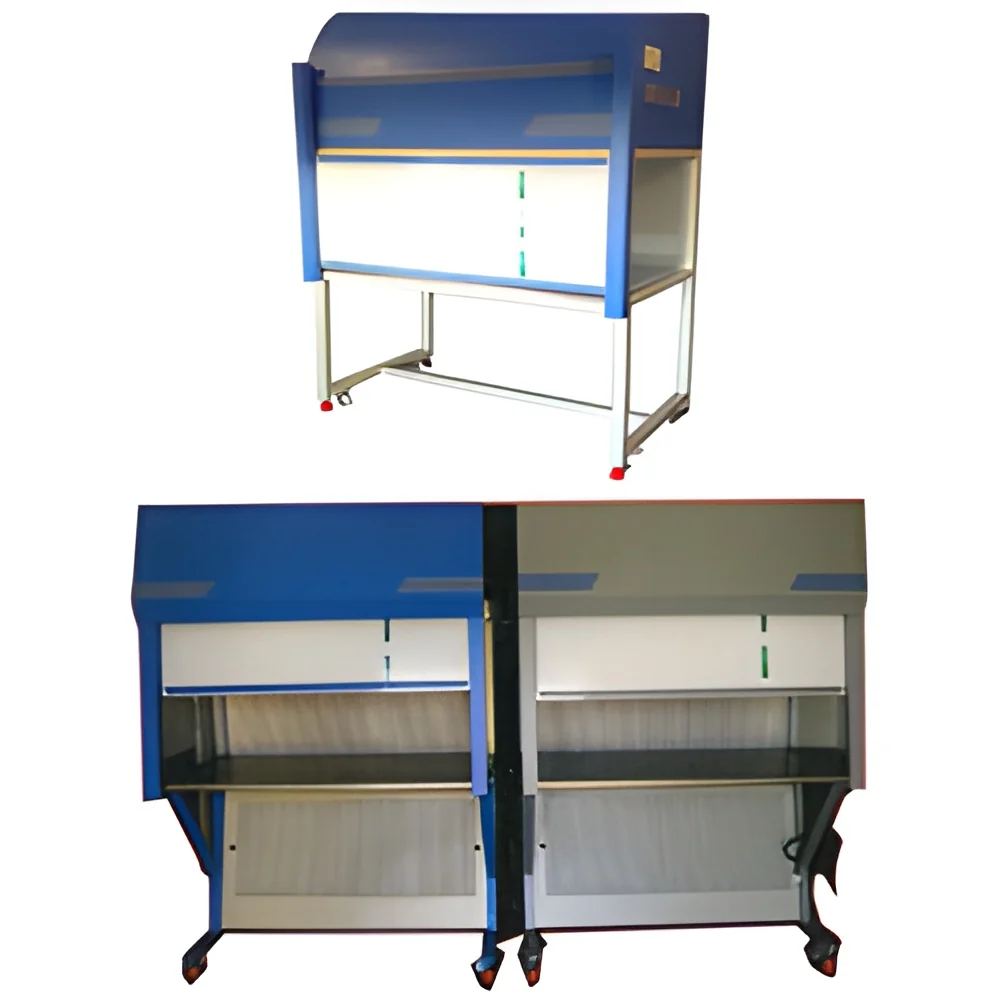
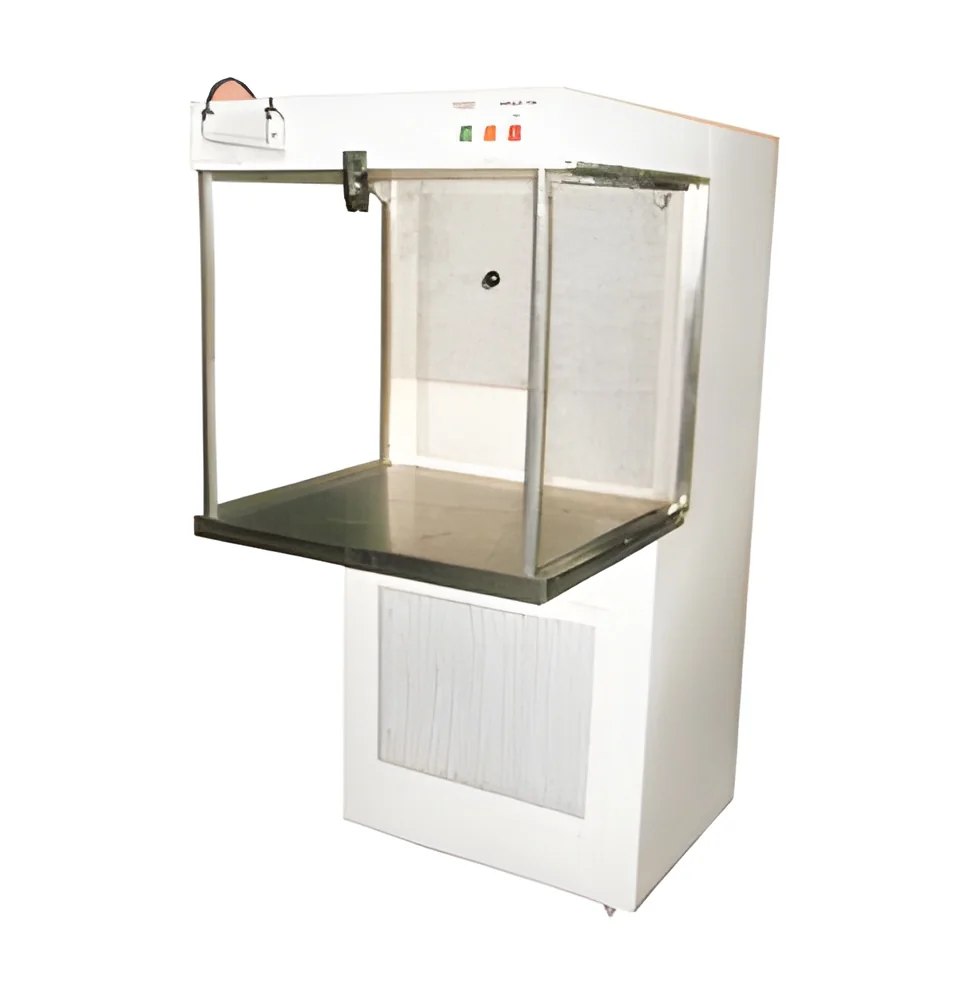
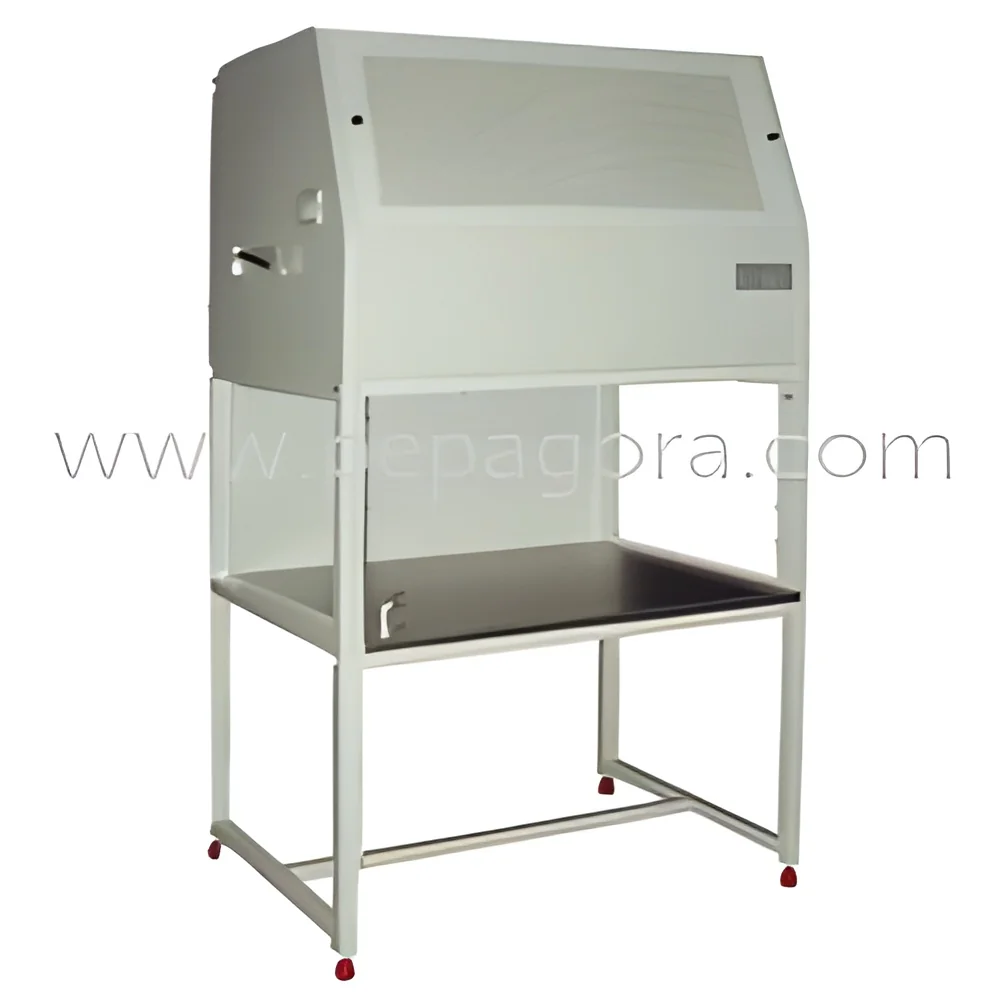
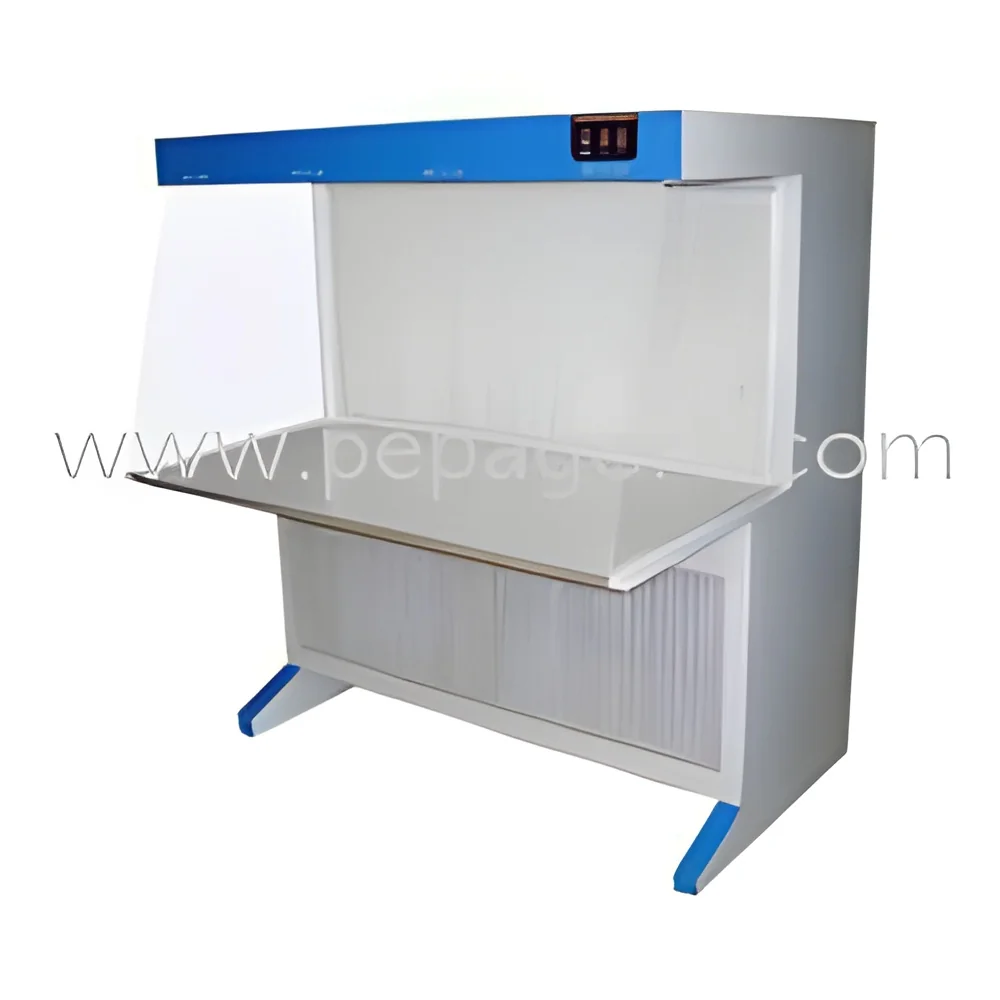
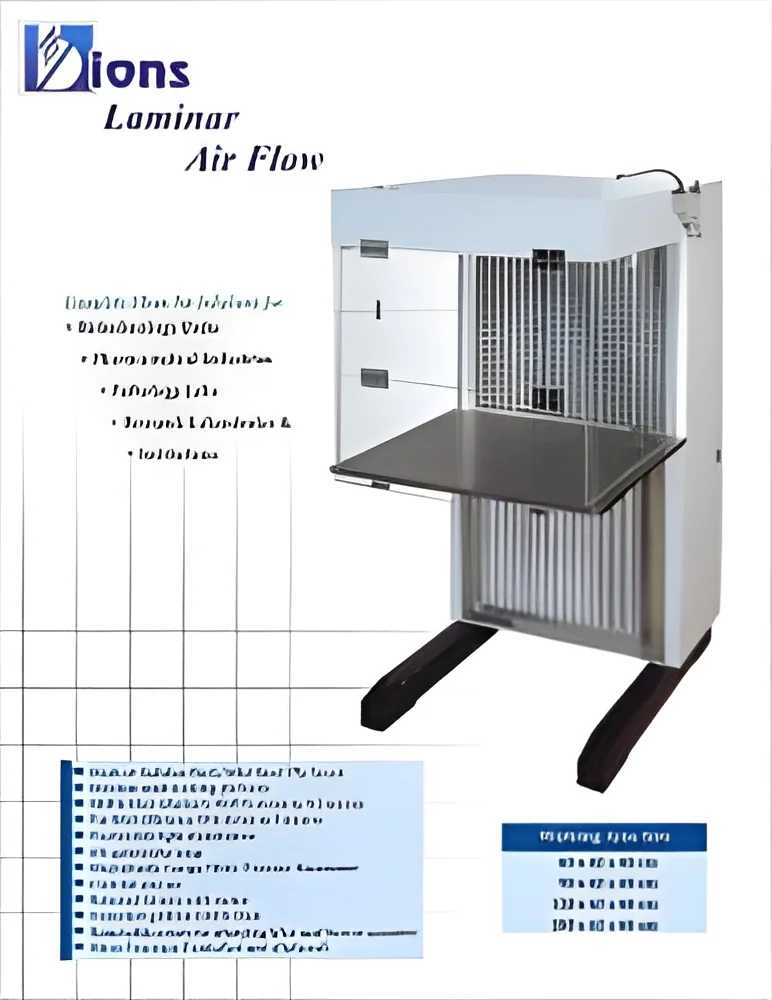
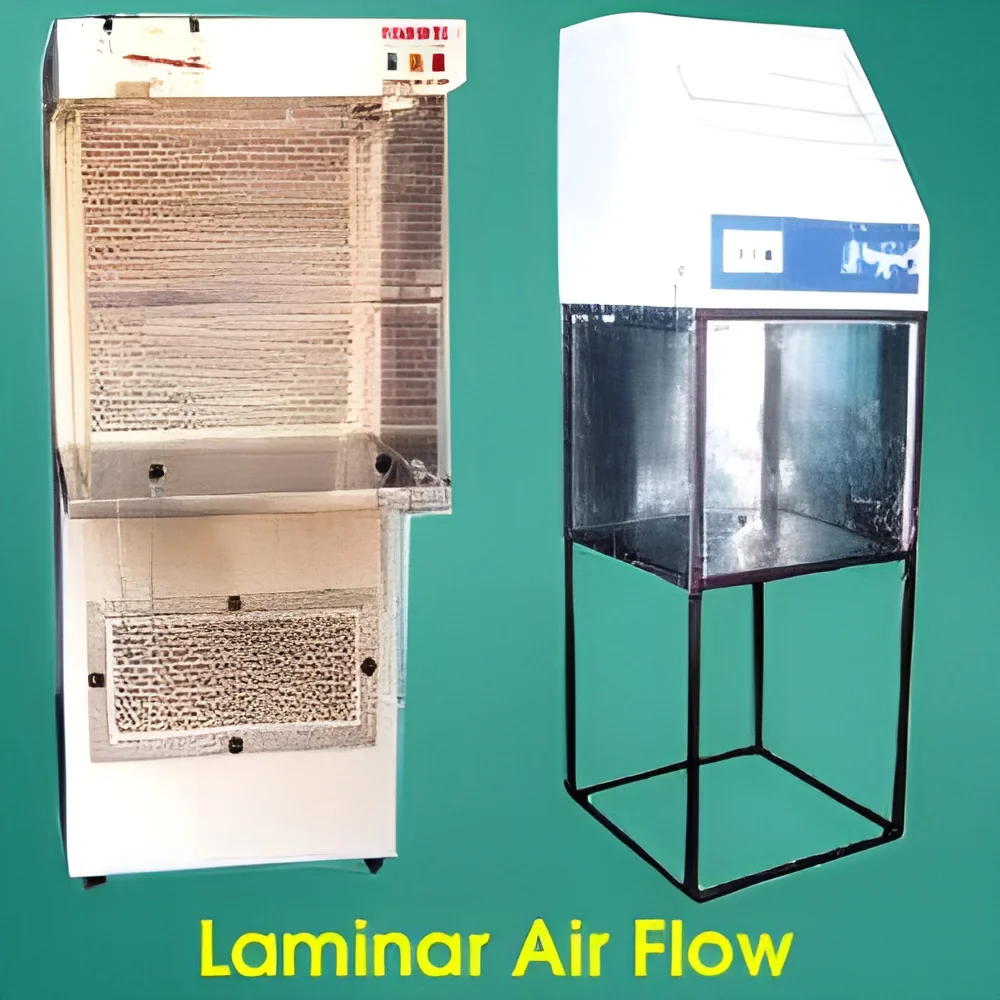
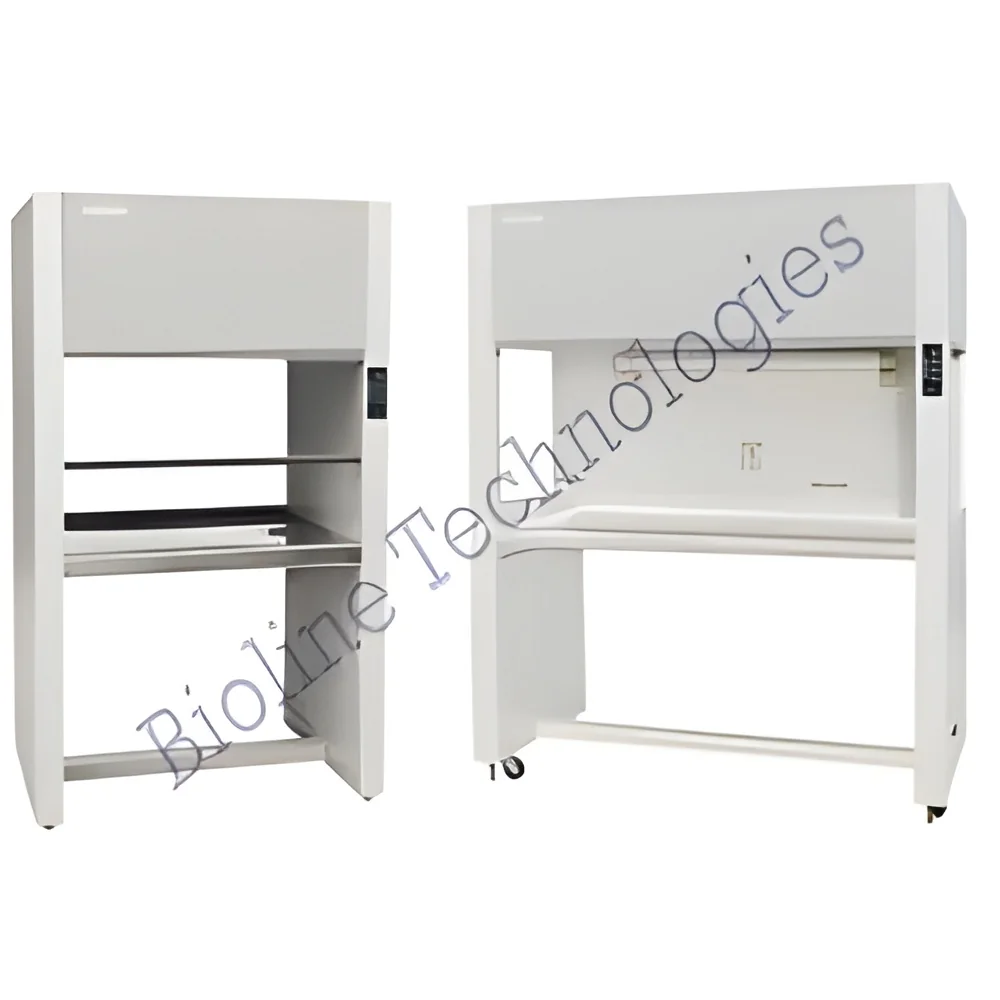
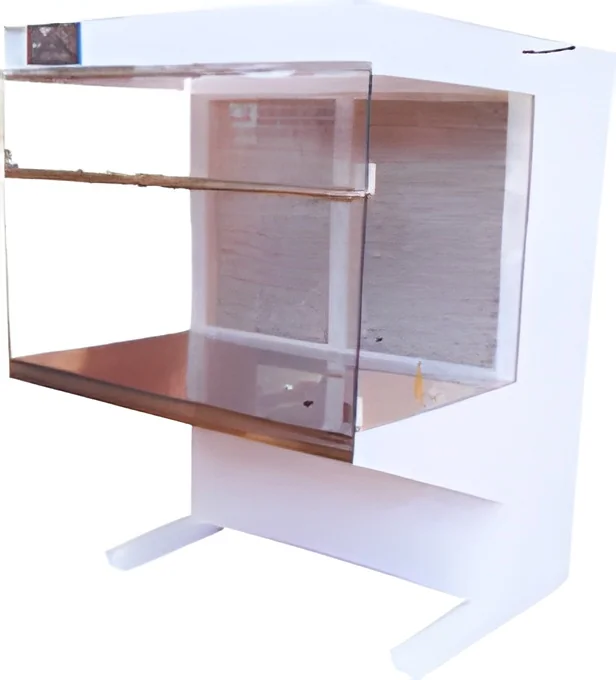
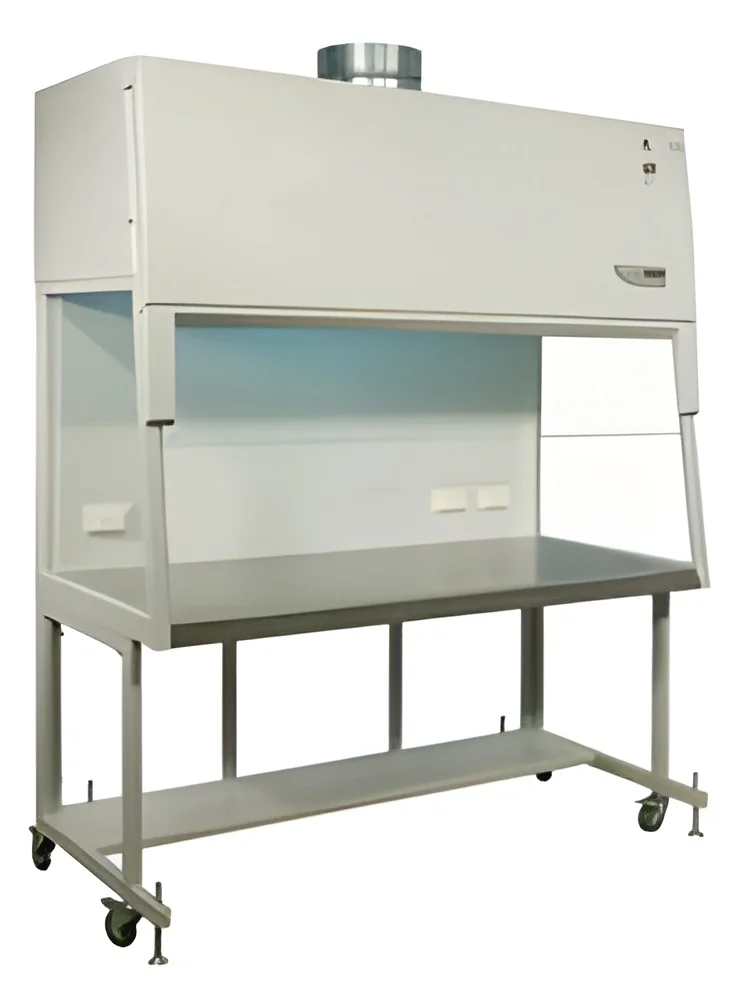
Laminar Flow Cabinets: These units provide a sterile work area by directing filtered air in a laminar flow pattern, ideal for handling sensitive samples.
Cleanroom Garments: Specialized clothing designed to reduce the risk of contamination from personnel, including gowns, gloves, and masks.
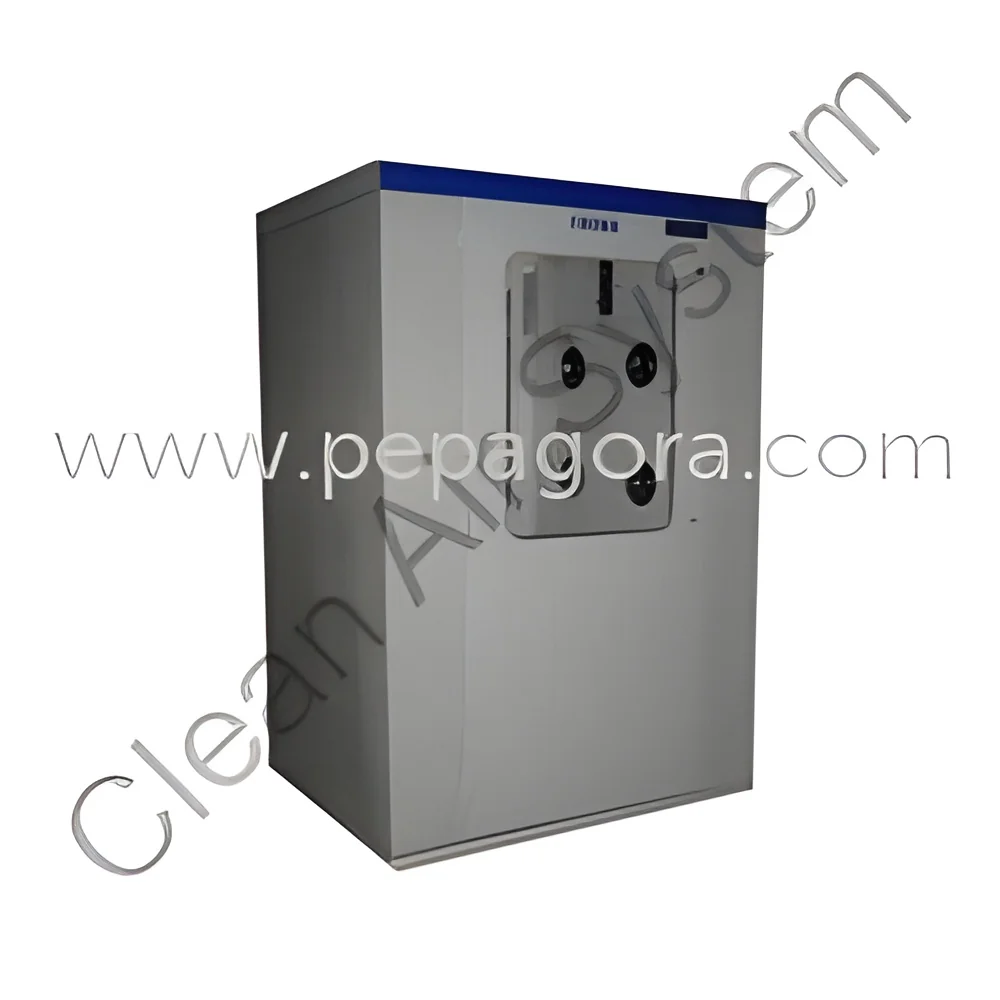
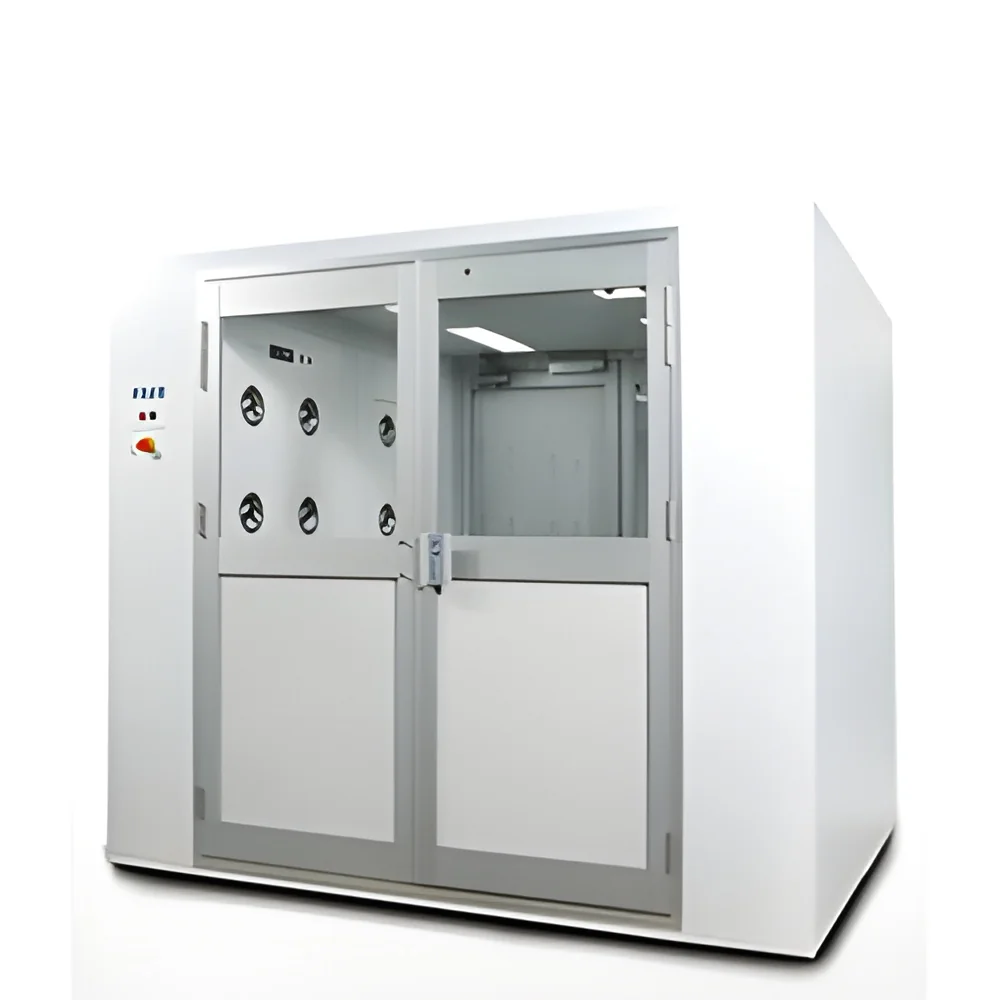
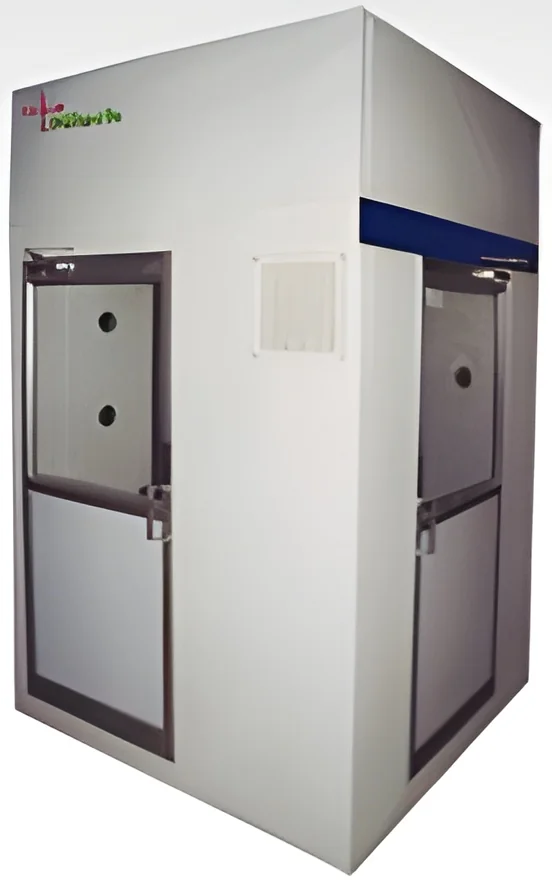
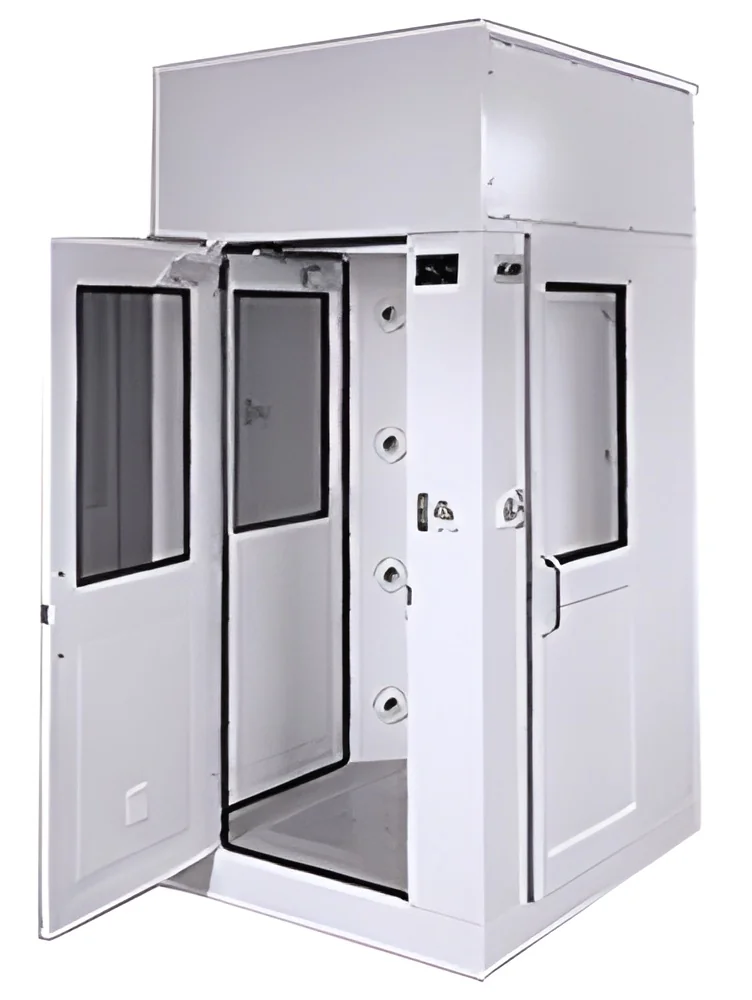
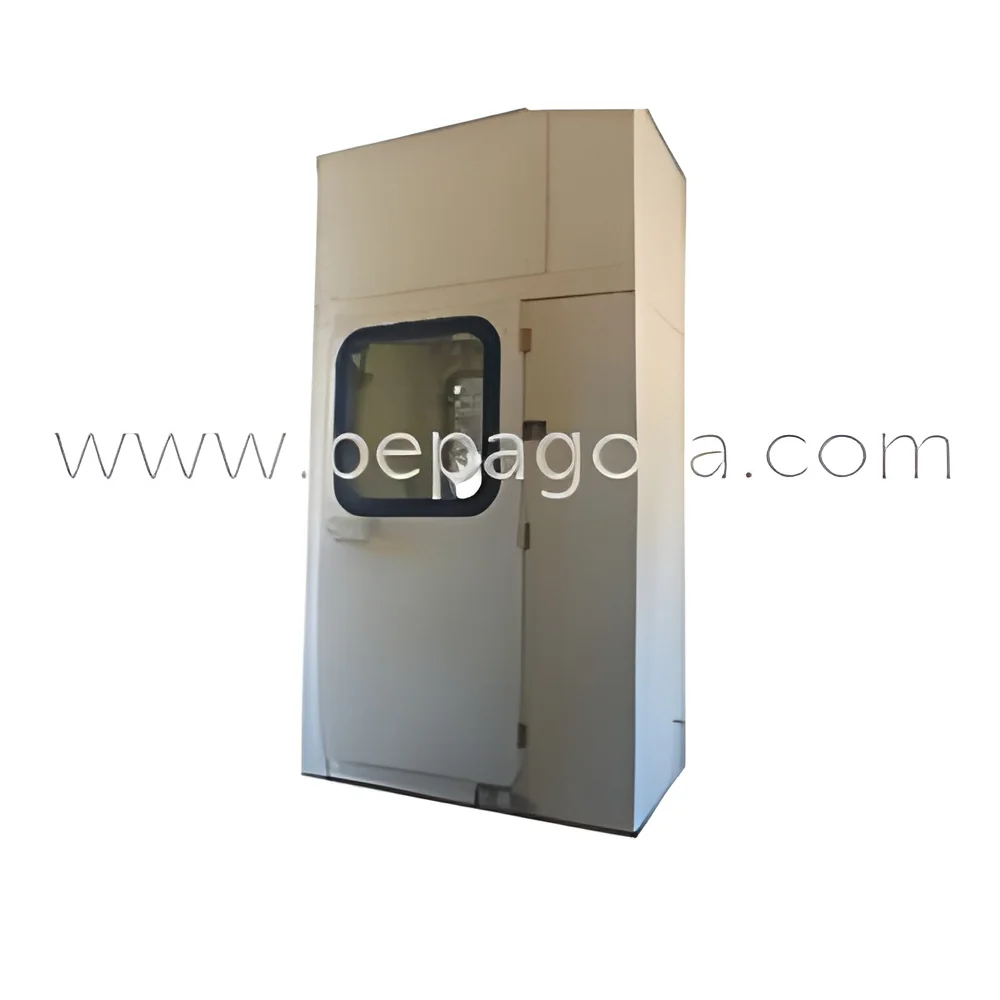
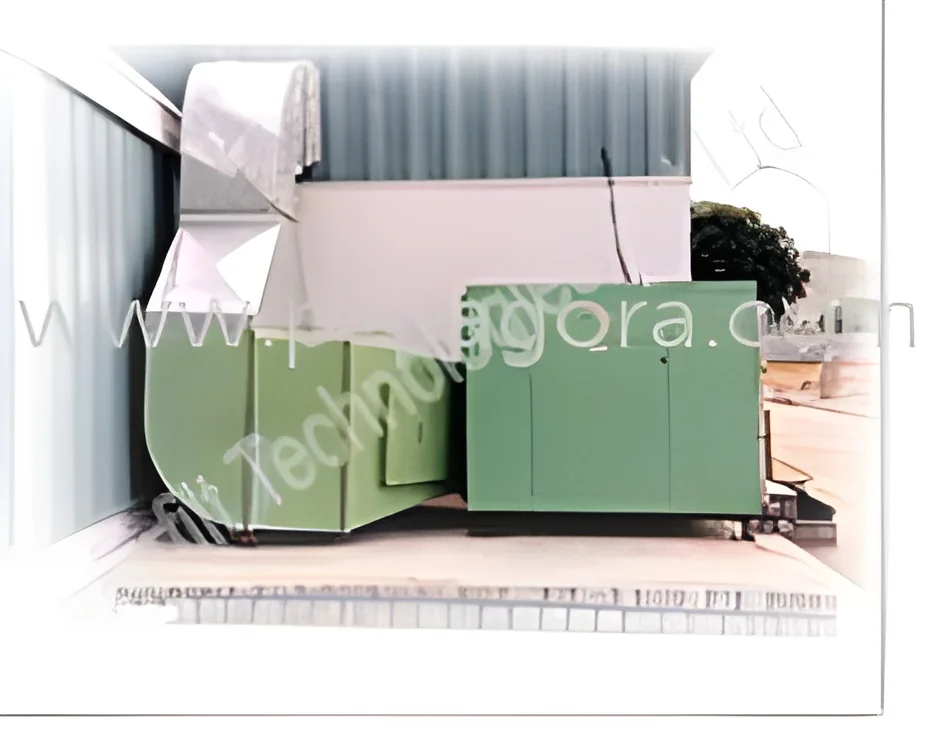
Air Showers: These units help decontaminate personnel and materials before entering cleanroom environments, minimizing the introduction of contaminants.
HEPA Filters: Essential for maintaining air quality in cleanrooms, these filters capture airborne particles and are used in various cleanroom applications.
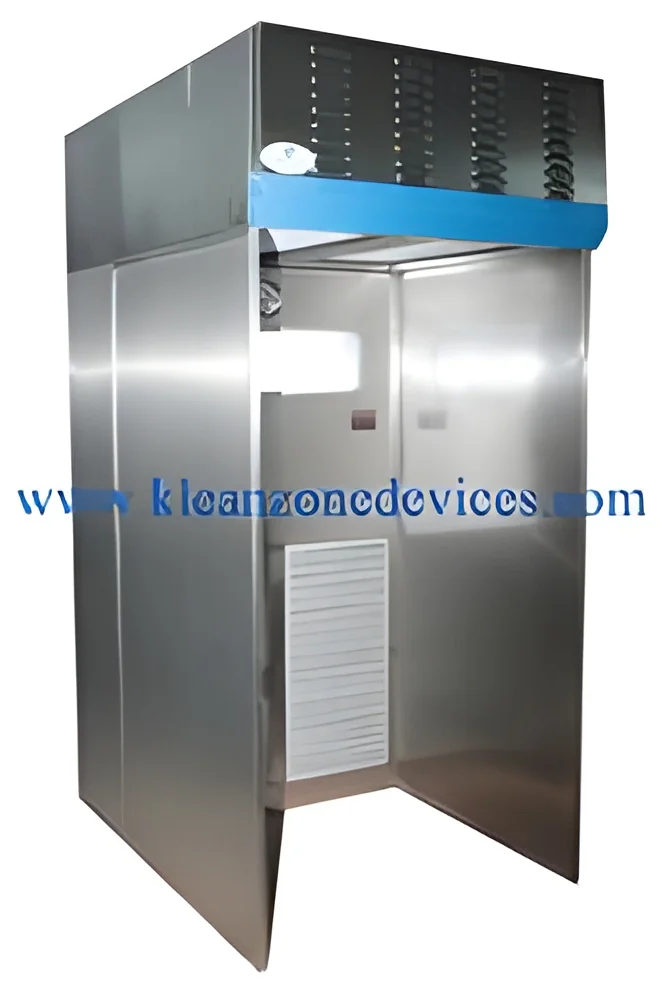
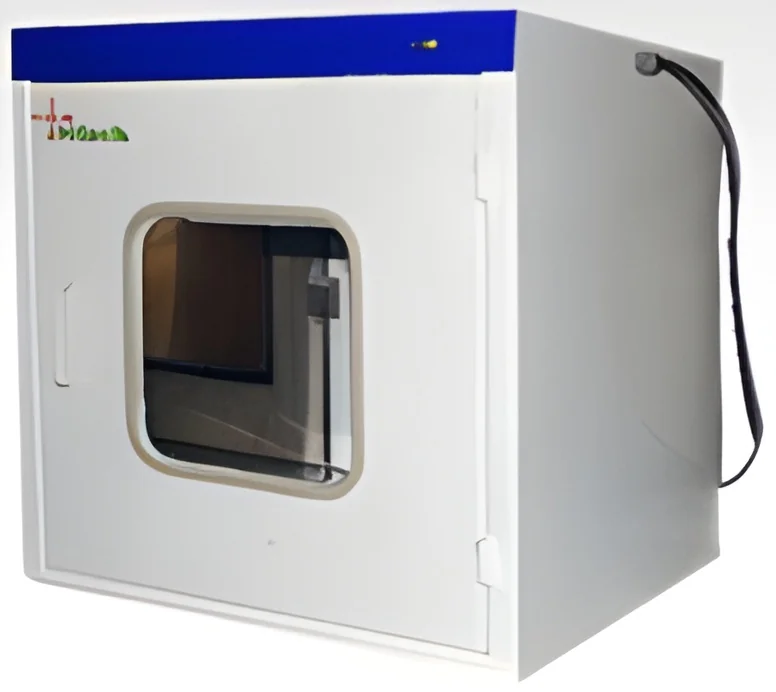
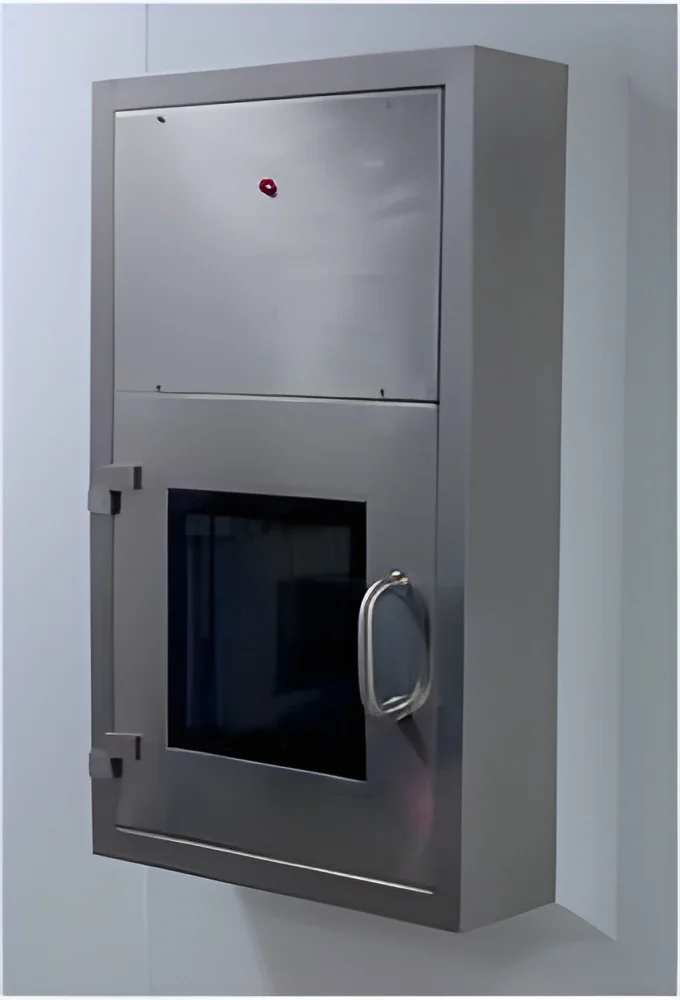
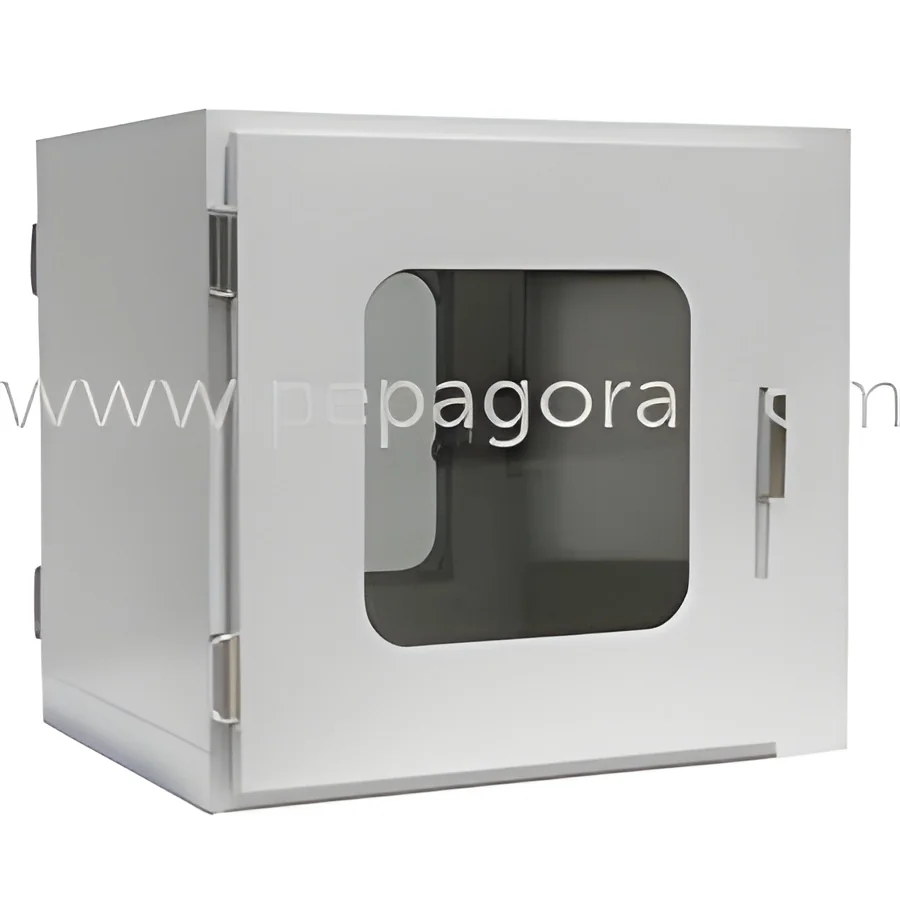
Pass-Through Chambers: These are designed for transferring materials in and out of cleanrooms without compromising the controlled environment.
Benefits and Advantages
Investing in cleanroom equipment offers numerous advantages for businesses operating in regulated environments.
1. Enhanced Product Quality: Cleanroom equipment helps maintain contamination-free environments, resulting in higher quality products.
2. Regulatory Compliance: Utilizing proper cleanroom solutions ensures adherence to industry regulations, reducing the risk of penalties.
3. Increased Efficiency: Streamlined processes and controlled environments lead to faster production times and reduced waste.
4. Improved Worker Safety: Cleanroom environments protect employees from hazardous materials and contaminants, promoting a safer workplace.
5. Customization Options: Various equipment configurations allow businesses to tailor solutions to their specific operational needs.
6. Long-term Cost Savings: Investing in high-quality cleanroom equipment can lead to reduced operational costs through improved efficiency and product reliability.
Buying Guide for B2B Buyers
When sourcing cleanroom equipment, several factors should be carefully considered to ensure optimal purchasing decisions.
1. Quality Assessment: Evaluate the quality of cleanroom equipment by examining materials, design, and compliance with industry standards. Look for certifications that guarantee performance.
2. Supplier Verification: Vet potential suppliers by checking their reputation, customer reviews, and experience in providing cleanroom solutions. Ensure they have a verified track record.
3. Pricing and MOQ: Understand the pricing structures and minimum order quantities (MOQ) required by suppliers. Consider bulk purchasing for potential cost savings.
4. Delivery and Lead Times: Clarify delivery schedules and lead times to avoid disruptions in operations. Timely delivery is crucial for maintaining production schedules.
5. Compliance Requirements: Ensure that the equipment meets all necessary regulatory requirements specific to your industry to avoid compliance issues.
Compliance and Certifications
Cleanroom equipment is subject to various quality standards and certifications to ensure safety and performance in regulated environments. Key standards include ISO 9001, which focuses on quality management systems, and Good Manufacturing Practice (GMP) standards relevant to the pharmaceutical and food industries.
Industry certifications, such as CE marking, indicate that the equipment meets European health, safety, and environmental protection standards. Additionally, cleanroom equipment must comply with safety and testing requirements specific to its use, ensuring that it functions effectively in controlled environments.
Regional compliance considerations are also essential, as different regions may have unique regulations governing cleanroom operations. Understanding these requirements is crucial for companies operating in multiple markets.
Why Source Cleanroom Equipment from Pepagora?
Pepagora provides a trusted platform for sourcing cleanroom equipment, ensuring that businesses can find reliable solutions for their operational needs.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, enhancing trust and ensuring quality products.
Streamlined RFQ Process: The platform simplifies the request for quotation (RFQ) process, allowing buyers to efficiently compare options and make informed decisions.
Trade Assurance and Support: Pepagora offers trade assurance, providing buyers with protection throughout the purchasing process, ensuring satisfaction with their acquisitions.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora ensures that businesses can access cleanroom equipment tailored to their specific regional requirements.

 IN

 India