
 IN
Centrifuges
17 products available
What are Centrifuges?
Centrifuges are mechanical devices that use centrifugal force to separate components of different densities within a mixture. By spinning samples at high speeds, centrifuges create a force that pushes heavier particles outward to the bottom of a container, while lighter particles remain closer to the top. This principle is widely applied in various industries to achieve efficient separation and purification of materials.
Centrifuges are primarily used in laboratories, manufacturing, and industrial processes. They play a crucial role in fields such as pharmaceuticals, biotechnology, food and beverage, and wastewater treatment. In these settings, centrifuges facilitate the separation of solids from liquids, the clarification of liquids, and the concentration of specific components. The significance of centrifuges in these industries underscores their value in enhancing productivity and efficiency.
The centrifuge market is evolving with advancements in technology, leading to increased demand for more efficient and reliable units. As industries strive for better process optimization, the role of centrifuges becomes increasingly vital. Moreover, the demand for automation and smart features in centrifuges is shaping their development, ensuring they meet modern operational needs.
Key Features and Specifications
Centrifuges come with a variety of features and specifications tailored to different applications. Understanding these specifications is essential for selecting the right centrifuge for your needs.
Key specifications include:
1. Maximum Speed
- This specification indicates the highest rotational speed the centrifuge can achieve, usually measured in revolutions per minute (RPM).
- Typical ranges can vary from 1,000 RPM to over 20,000 RPM, depending on the model and application.
2. Rotor Capacity
- Refers to the volume of samples the centrifuge can accommodate in a single run.
- Capacities can range from small microcentrifuge tubes (1.5 mL) to large industrial models capable of handling several liters.
3. Temperature Control
- Some centrifuges offer temperature control features to maintain optimal conditions during separation.
- Temperature ranges typically span from -20°C to +40°C, depending on the centrifuge design.
4. Noise Level
- Indicates the sound produced by the centrifuge during operation.
- Noise levels can vary, with quieter models operating around 50 dB.
5. Safety Features
- Includes mechanisms such as lid locks and imbalance detection to enhance user safety during operation.
6. User Interface
- Refers to the ease of use of the control panel and programming options.
- Modern centrifuges may include digital displays and programmable settings for enhanced user experience.
7. Compliance Standards
- Many centrifuges meet specific industry standards and certifications, such as CE marking, indicating compliance with safety and health regulations.
8. Power Consumption
- This specification outlines the energy efficiency of the centrifuge.
- Power ratings can range from a few hundred watts for small units to several kilowatts for larger industrial centrifuges.
In summary, selecting a centrifuge involves understanding these key features and specifications to ensure it aligns with your specific operational requirements.
Common Applications and Use Cases
Centrifuges are highly versatile and find applications across various industries.
1. Pharmaceutical Industry: Centrifuges are used for separating biological samples and purifying proteins and other compounds during drug development.
2. Biotechnology: In biotech labs, centrifuges assist in the isolation of cells, viruses, and DNA, playing a crucial role in research and diagnostics.
3. Food and Beverage: Centrifuges are employed for clarifying juices, separating cream from milk, and extracting essential oils, ensuring product quality and consistency.
4. Chemical Industry: In chemical processing, centrifuges help separate solids from liquids in the production of chemicals and related products.
5. Wastewater Treatment: Centrifuges are used to dewater sludge, allowing for the efficient treatment and disposal of wastewater materials.
6. Clinical Laboratories: Centrifuges enable the separation of blood components for various diagnostic tests, making them essential in medical settings.
7. Mining and Mineral Processing: Centrifuges facilitate the separation of valuable minerals from ore, improving recovery rates.
Product Variants and Subcategories
Centrifuges are available in various configurations to suit specific needs and applications.
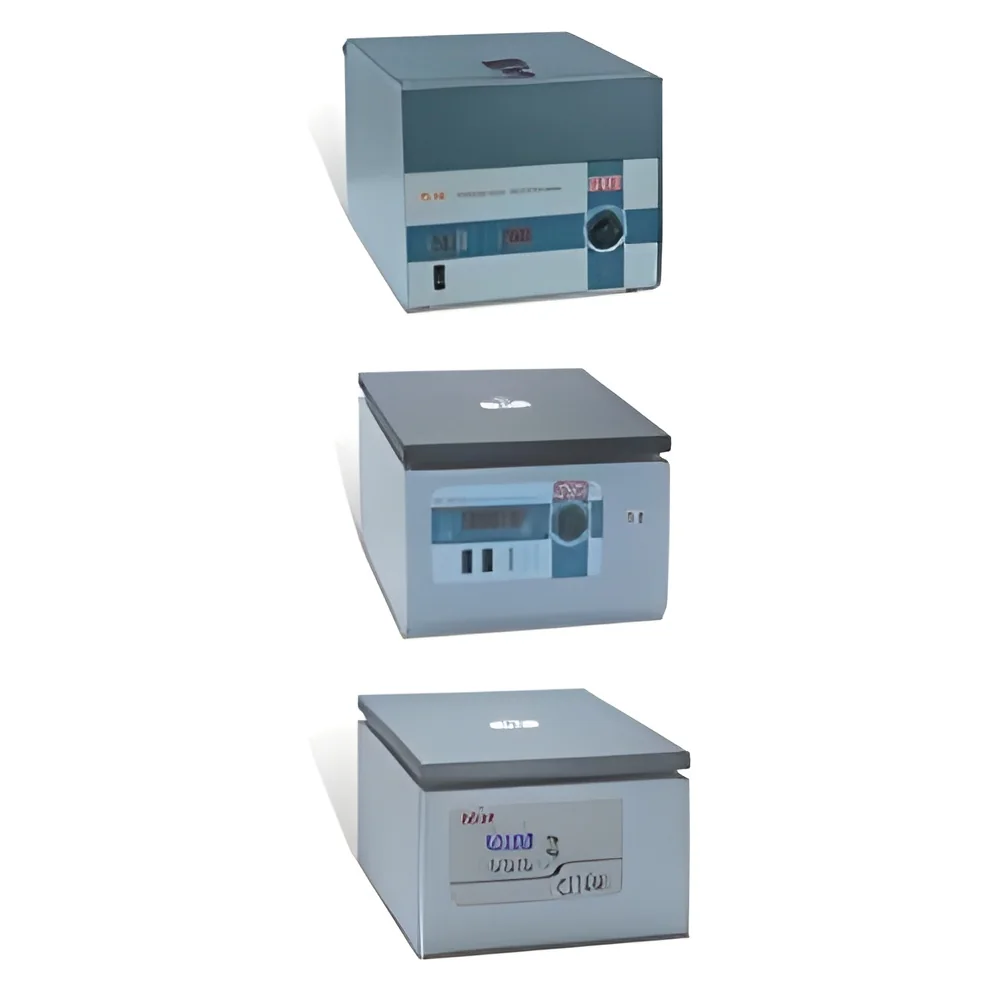
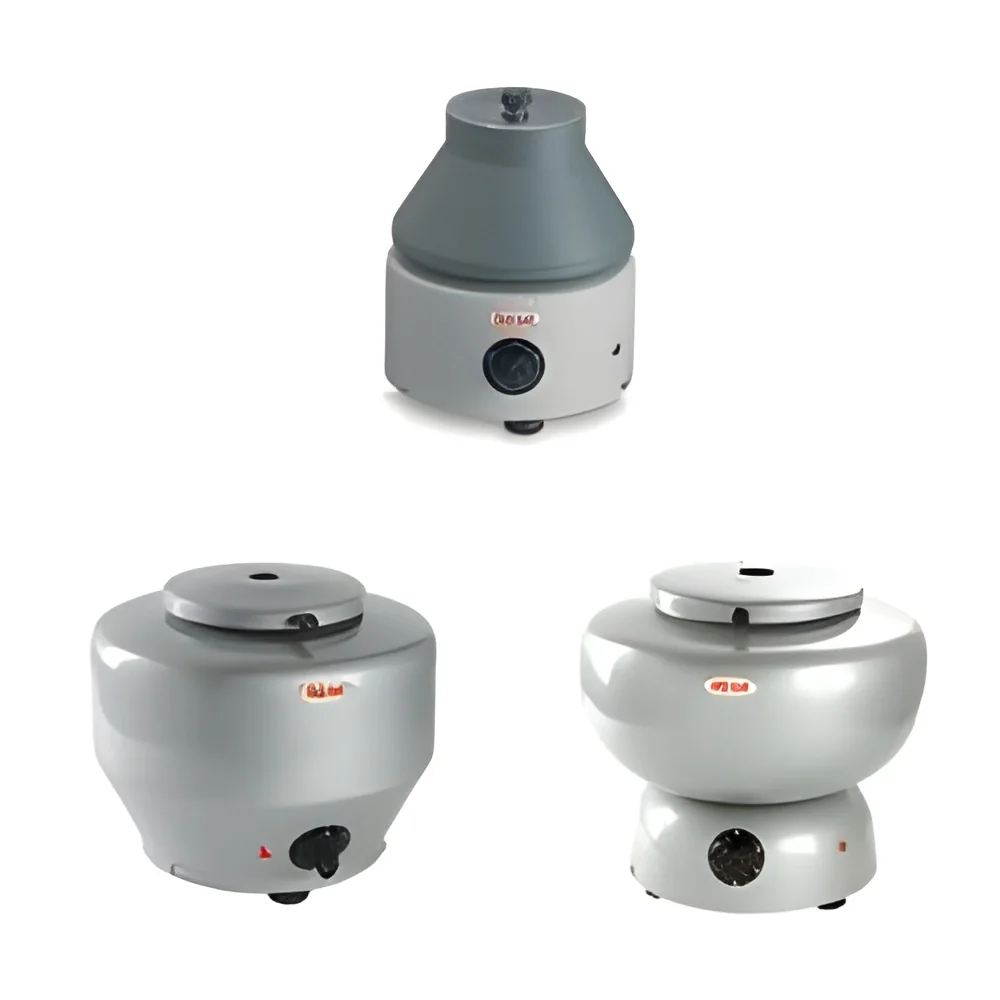
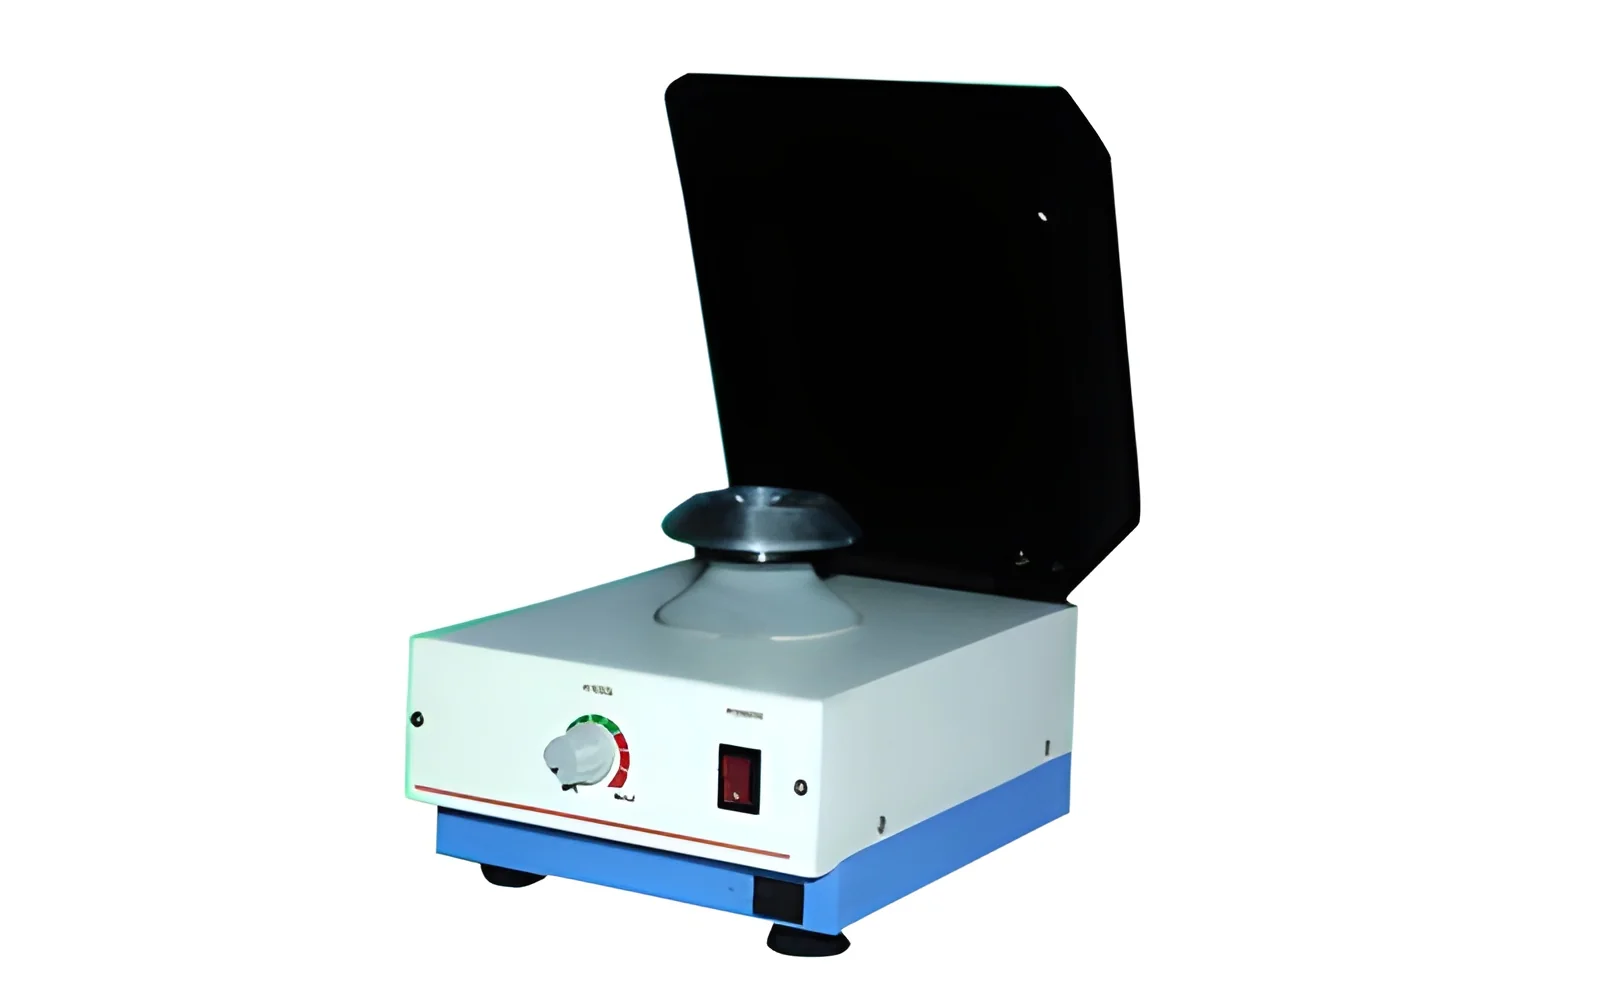
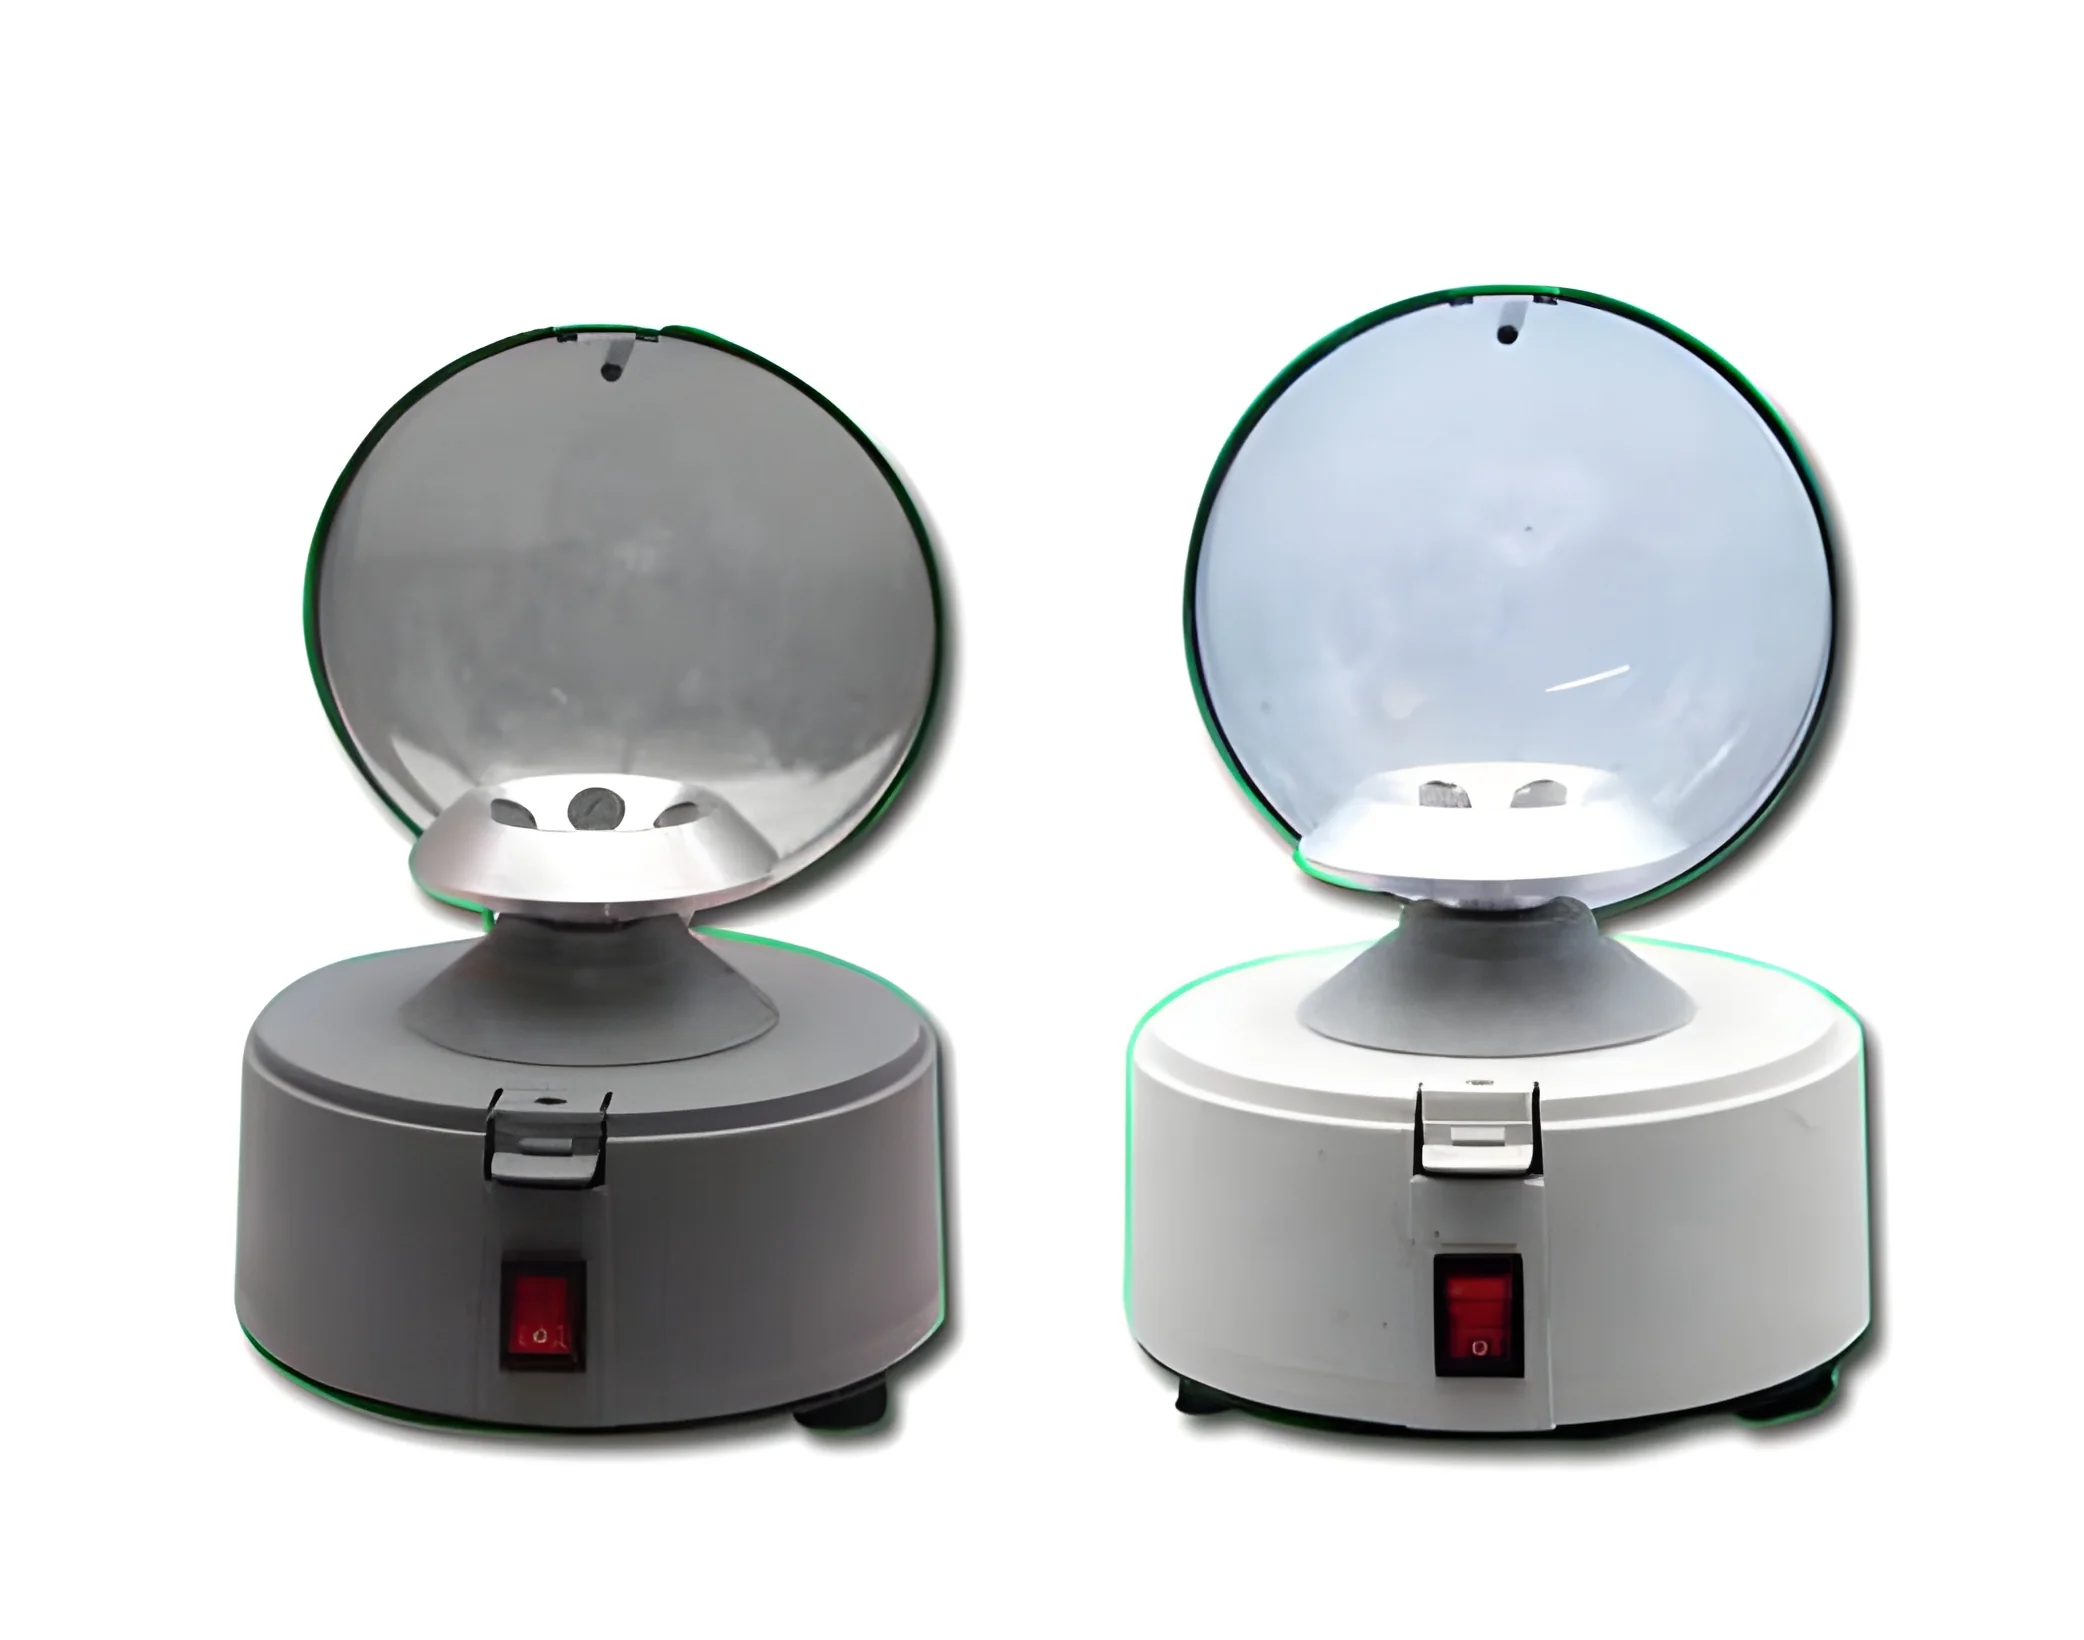
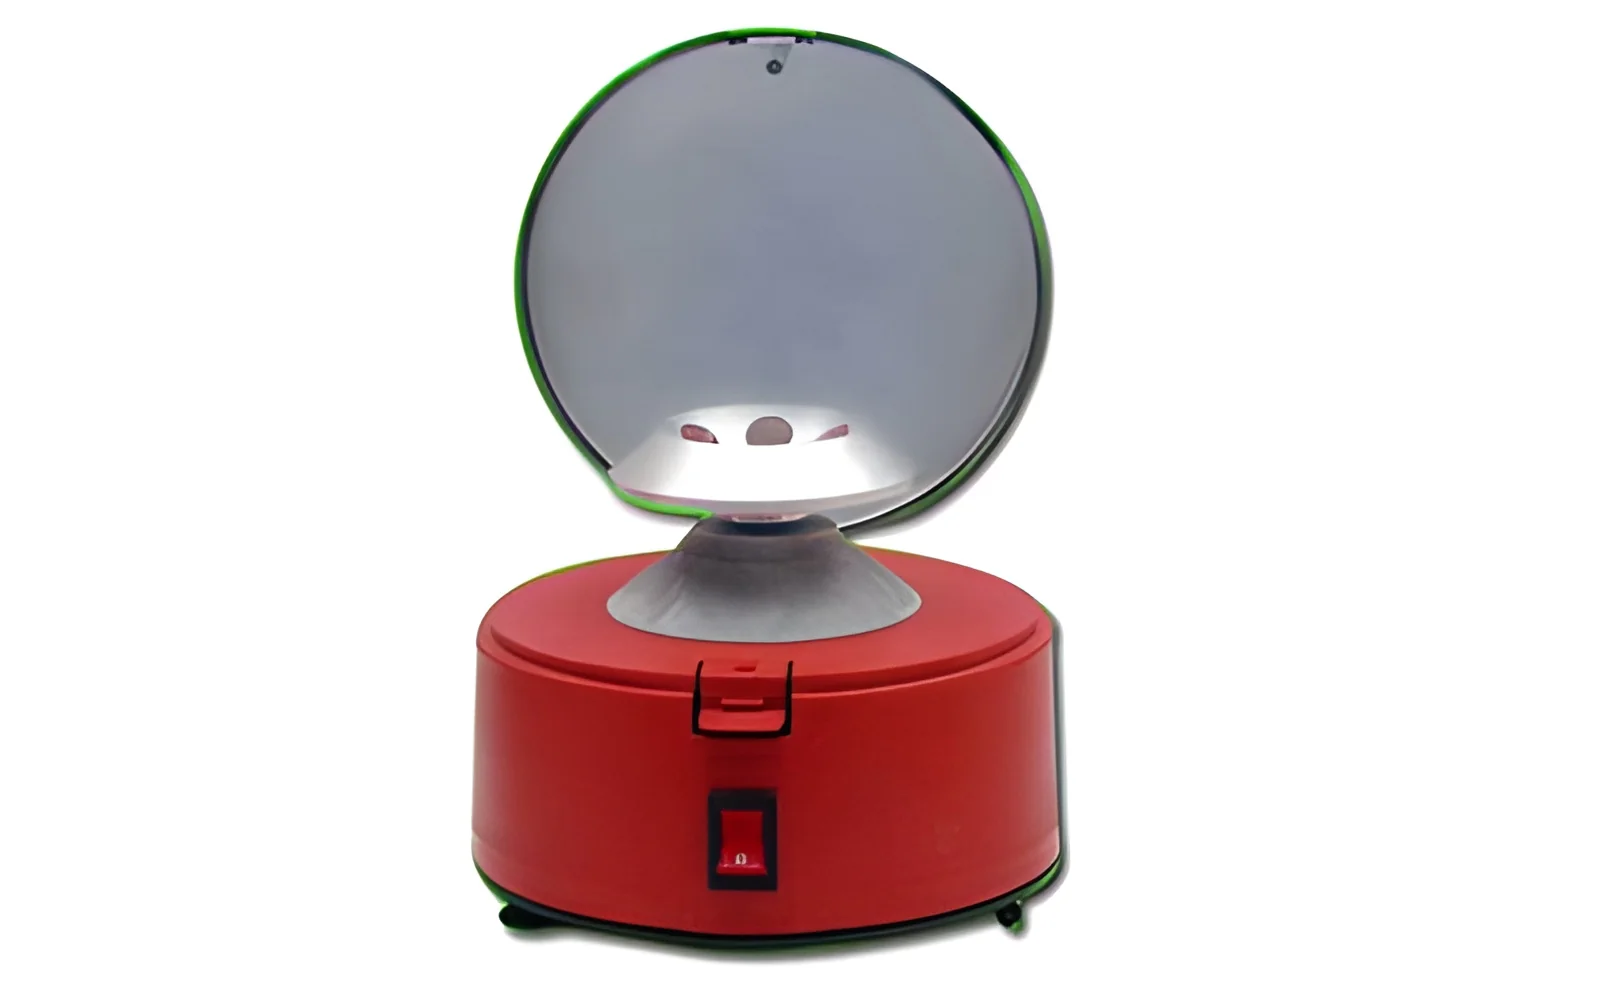
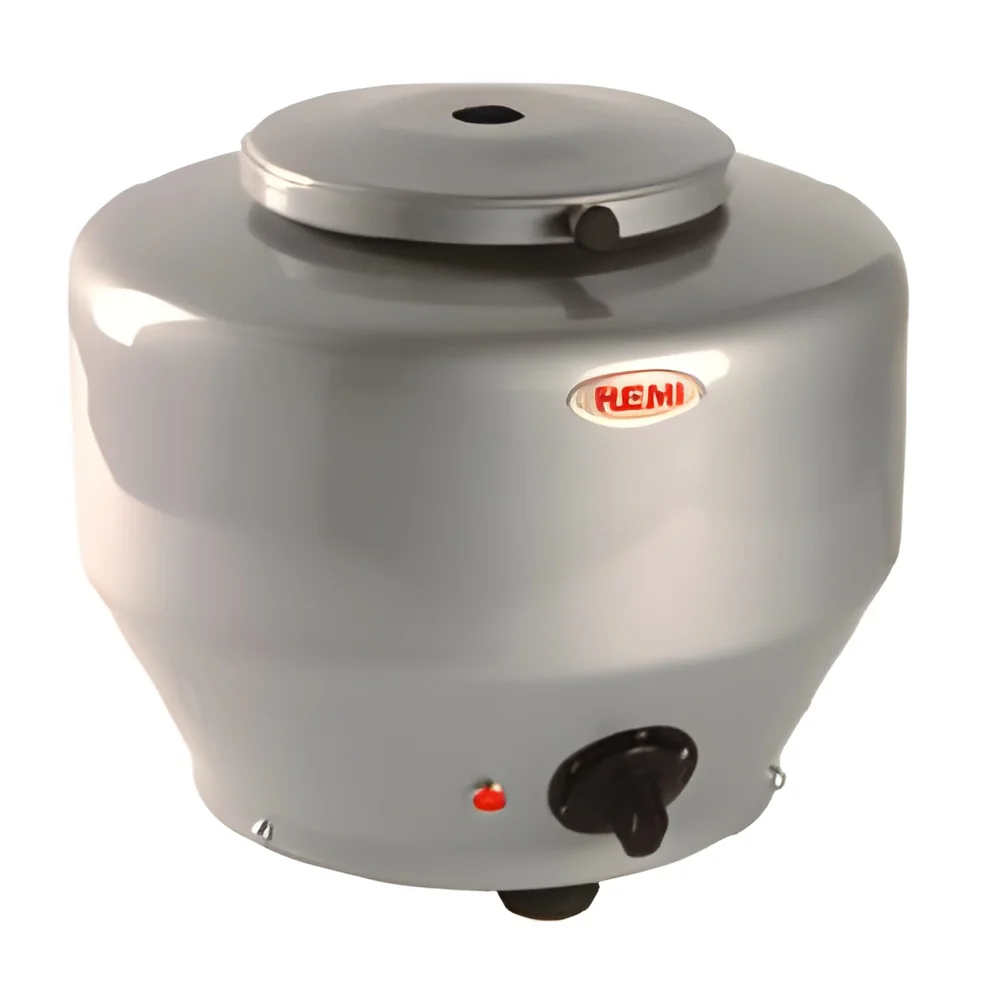
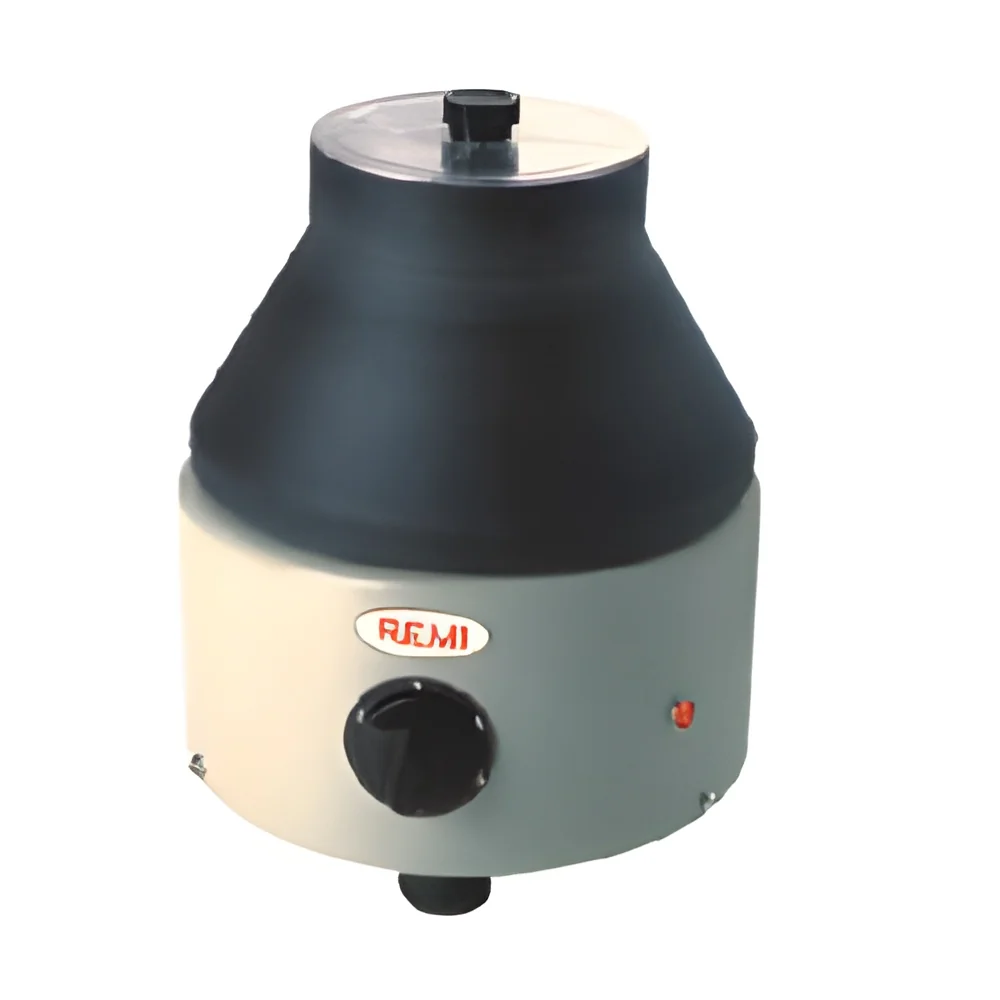
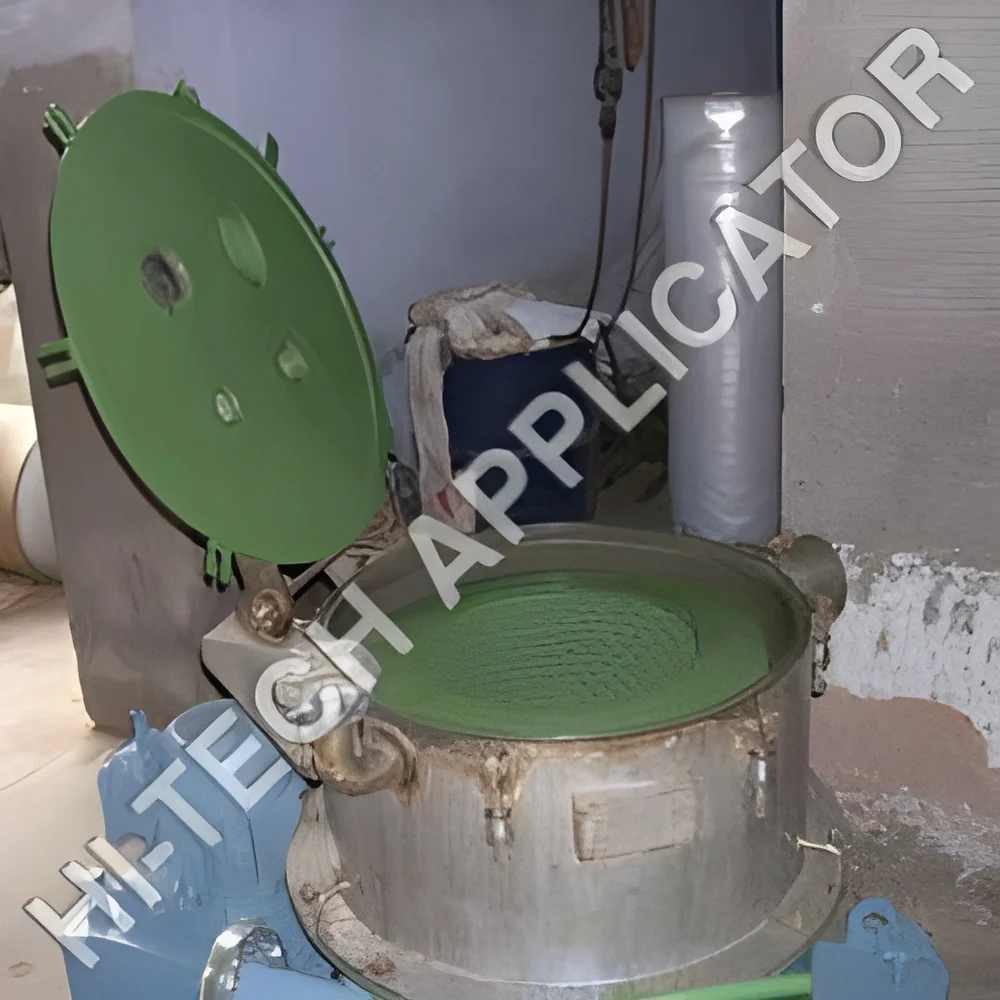
Laboratory Centrifuges: These compact units are designed for research and clinical applications. They typically feature variable speed settings and small rotor capacities for precise sample processing.
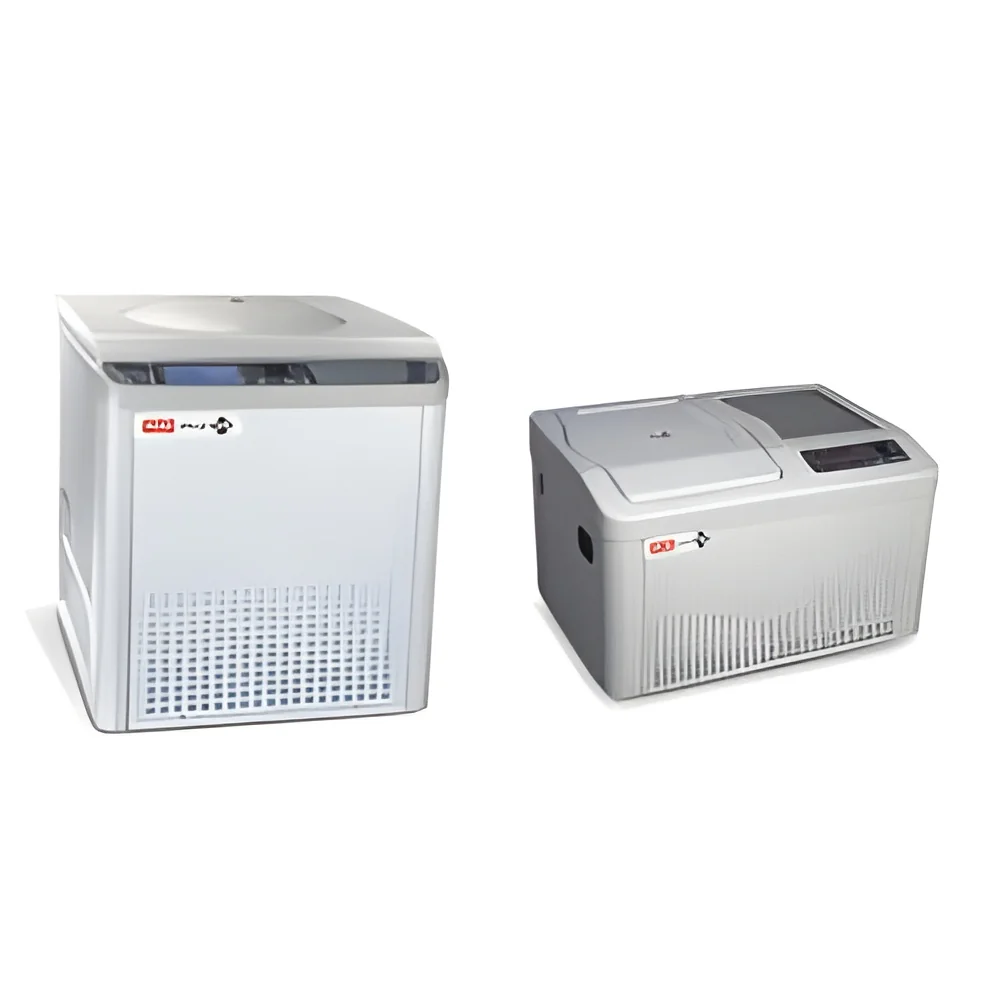
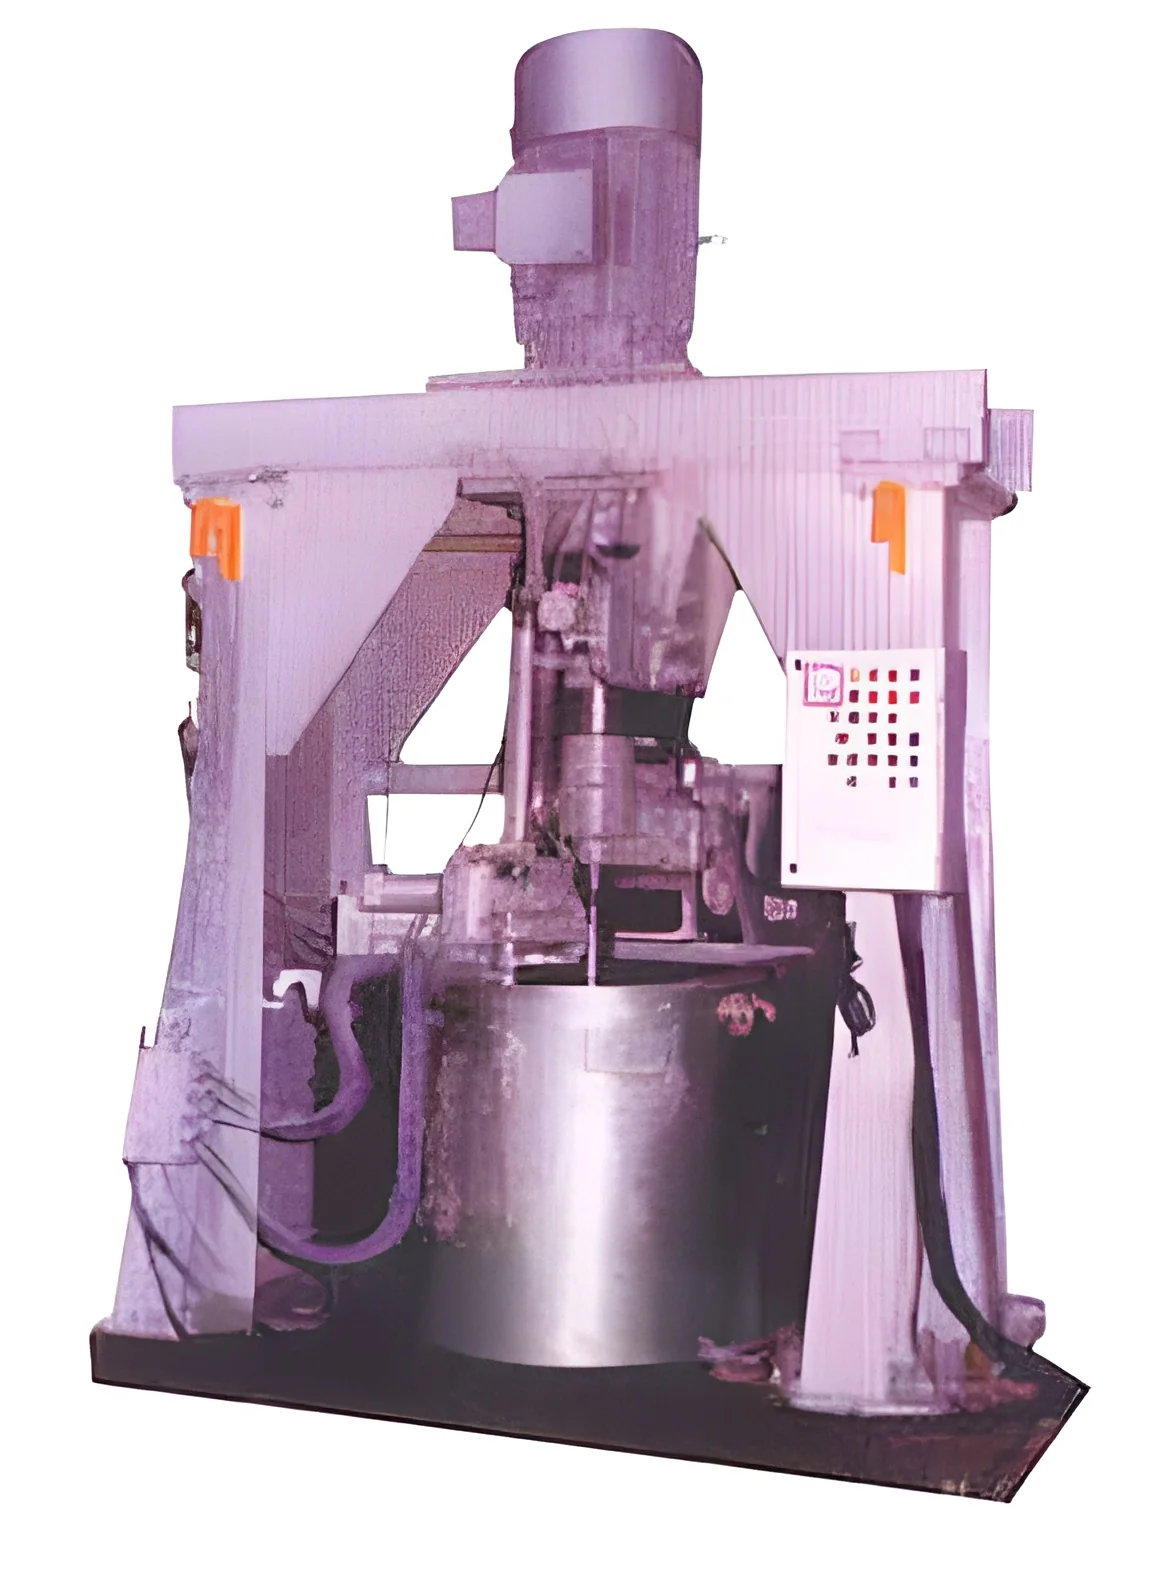
Industrial Centrifuges: Built for large-scale operations, industrial centrifuges can handle high volumes and are often equipped with advanced features for efficiency and automation.
Refrigerated Centrifuges: These models come with temperature control, allowing sensitive biological samples to be processed without degradation due to heat.
Ultracentrifuges: Designed for high-speed separation, ultracentrifuges are used in research settings to isolate subcellular components, such as organelles and macromolecules.
Benefits and Advantages
Centrifuges offer numerous benefits that enhance operational efficiency in various industries.
1. Efficient Separation: Centrifuges provide rapid and effective separation of components, reducing processing times compared to traditional methods.
2. Improved Purity: The use of centrifuges leads to higher purity levels in separated materials, which is crucial in industries like pharmaceuticals and food processing.
3. Versatility: These devices can handle a wide range of sample types and sizes, making them valuable across multiple applications.
4. Automation Capabilities: Many modern centrifuges feature automated controls, allowing for hands-free operation and reduced human error.
5. Space Efficiency: Laboratory centrifuges are designed to occupy minimal space while providing robust performance, ideal for facilities with limited room.
6. Enhanced Safety: Advanced safety features protect users from potential hazards associated with high-speed operations.
Buying Guide for B2B Buyers
When sourcing centrifuges, it's important to consider several key factors to make an informed decision.
1. Quality Assessment: Evaluate centrifuge quality by looking for certifications and industry standards, such as CE marking. A well-built unit ensures reliability and longevity.
2. Supplier Verification: Vet suppliers through references, reviews, and industry reputation to ensure they provide genuine products and support.
3. Pricing and MOQ: Understand the pricing structure and minimum order quantities (MOQ) required by suppliers to optimize procurement costs.
4. Delivery and Lead Times: Consider the logistics involved, including lead times for delivery, to ensure timely availability of centrifuges for your operations.
5. Compliance Requirements: Ensure that the centrifuge meets relevant regulatory requirements for your industry, which may include safety and environmental standards.
Compliance and Certifications
Centrifuges must adhere to specific compliance standards and certifications that ensure their safety and effectiveness.
ISO 9001 is a quality management standard that applies to manufacturers of centrifuges, ensuring they maintain consistent quality in their production processes.
HACCP (Hazard Analysis Critical Control Point) is relevant in food and beverage applications, where centrifuges must meet safety protocols to prevent contamination.
CE certification indicates that a centrifuge meets European safety, health, and environmental protection standards. This certification is essential for market acceptance in Europe.
Safety and testing requirements also include thorough assessments of centrifuge performance under various conditions to ensure user safety during operation.
Regional compliance may vary, so it's crucial to understand local regulations governing centrifuge use, particularly in specialized industries.
Why Source Centrifuges from Pepagora?
Pepagora provides a trusted platform for sourcing centrifuges, offering several distinct advantages for B2B buyers.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers, ensuring that all products meet quality standards and industry requirements.
Streamlined RFQ Process: The platform simplifies the request for quotation (RFQ) process, allowing buyers to efficiently compare options and select the best supplier for their needs.
Trade Assurance and Support: Buyers receive protection through trade assurance policies, which safeguard transactions and provide support throughout the sourcing process.
Regional Coverage: With a focus on markets in India, the Gulf Cooperation Council (GCC), and Southeast Asia, Pepagora offers extensive regional coverage, making it easier for buyers to find local suppliers that suit their operational needs.

 India
 India
 India
 India
 India
Frequently Asked Questions
What are Centrifuges?
Centrifuges are devices that use centrifugal force to separate substances of different densities within a mixture. They are commonly utilized in laboratories and industrial applications to isolate liquids, solids, or gas particles from fluids.
What are the different types of Centrifuges?
There are various types of centrifuges, including laboratory centrifuges, industrial centrifuges, and medical centrifuges. Each type is designed for specific applications, such as separating blood components, purifying chemicals, or processing wastewater.
How do I choose the right Centrifuges?
Choosing the right centrifuge depends on factors such as the type of materials you need to separate, the volume of the samples, and the required speed. It's essential to assess your specific application needs and consult with suppliers to find the most suitable model.
What are the standard specifications for Centrifuges?
Standard specifications for centrifuges typically include maximum speed (RPM), maximum RCF (relative centrifugal force), capacity, and temperature control features. Additionally, safety features and power requirements are also important specifications to consider.
What is the price range for Centrifuges?
The price range for centrifuges can vary significantly based on their type, size, and features, typically ranging from a few thousand to several lakhs of Indian Rupees. Industrial models tend to be more expensive than laboratory versions due to their larger capacity and more robust design.
What quality standards apply to Centrifuges?
Centrifuges are subject to various quality standards, including ISO certifications and safety regulations. These standards ensure that the devices are reliable, efficient, and safe for use in their intended applications.
Where can I find Centrifuges suppliers in India?
You can find centrifuge suppliers in India by searching online B2B marketplaces like Pepagora, industry directories, or contacting manufacturers directly. It's advisable to compare multiple suppliers to ensure you are getting quality products and competitive pricing.
Can Centrifuges be customized?
Yes, many manufacturers offer customization options for centrifuges to meet specific requirements. Customizations can include modifications in size, speed, and features tailored to particular industrial or laboratory applications.
What is the typical minimum order quantity for Centrifuges?
The minimum order quantity (MOQ) for centrifuges varies by manufacturer and model, with some suppliers offering single units while others may require bulk orders. It's best to check with the specific supplier for their MOQ policies.
What is the typical lead time for Centrifuges?
The typical lead time for centrifuges can range from a few days to several weeks, depending on the supplier and whether the centrifuge is standard or customized. Always confirm the lead time with the supplier when placing an order.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally

Source Smarter,Grow Faster
