What are PCBA Testing & Quality Control?
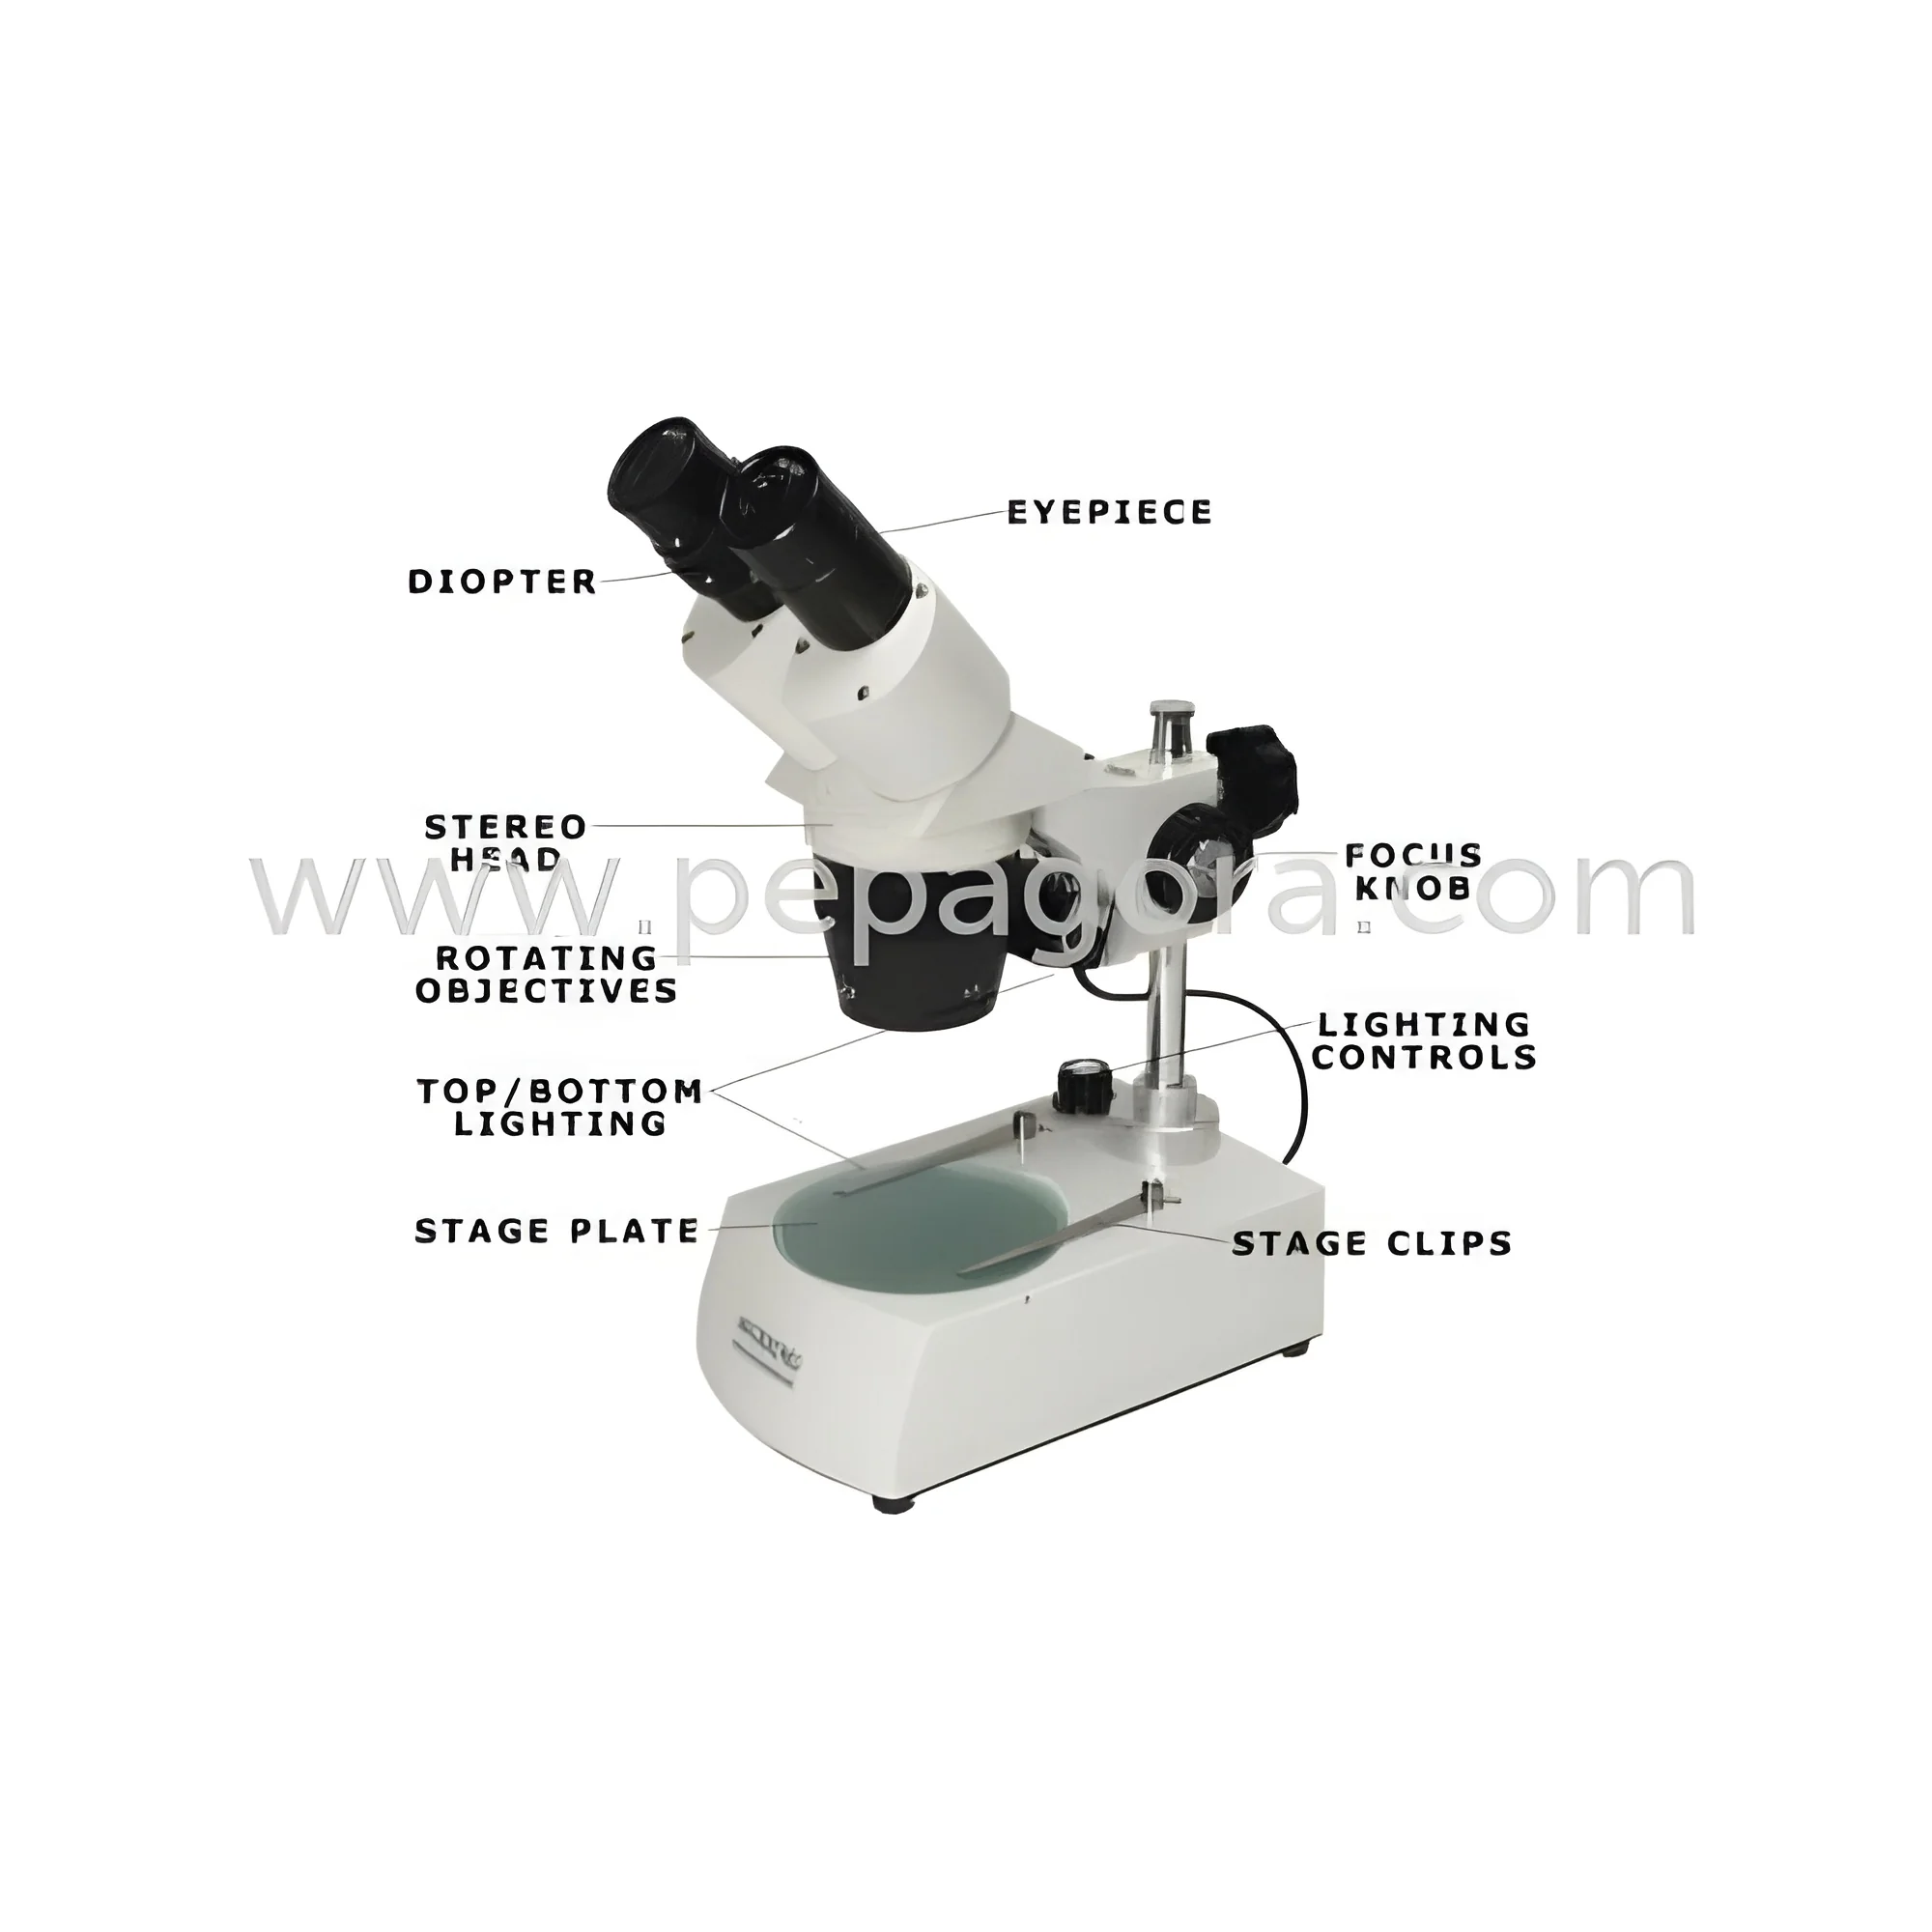
PCBA Testing and Quality Control refer to the processes involved in ensuring that printed circuit board assemblies (PCBAs) meet specific performance and quality standards. These practices are critical in verifying that electronic components operate correctly and reliably. Testing methods can include visual inspections, functional testing, and stress testing, among others. Quality control processes help identify defects early in the production cycle, ultimately leading to improved product reliability and customer satisfaction.
Primarily, PCBA Testing and Quality Control are used in industries that manufacture electronic devices, such as telecommunications, automotive, and consumer electronics. These testing procedures are essential for maintaining compliance with industry standards and ensuring that products meet customer expectations. As the demand for electronic devices continues to rise, effective testing and quality assurance become increasingly relevant in the market, allowing businesses to deliver high-quality products while minimizing costs associated with returns and failures.
Key Features and Specifications
PCBA Testing and Quality Control encompass various features and specifications designed to ensure optimal performance and reliability. These specifications guide manufacturers in maintaining consistent quality throughout the production process.
Key specifications include:
1. Testing Methods
- Visual inspection, automated optical inspection (AOI), and in-circuit testing (ICT)
- Ensures thorough evaluation of assembly quality
2. Quality Standards
- Compliance with ISO 9001 and CE certifications
- Guarantees adherence to international quality benchmarks
3. Functional Testing
- Verification of operational performance under various conditions
- Includes power-on tests and signal integrity checks
4. Environmental Testing
- Assessment of performance under extreme temperatures and humidity levels
- Ensures reliability in diverse operating conditions
5. Documentation and Reporting
- Comprehensive test reports and quality assurance documentation
- Provides traceability and accountability
6. Fault Detection Rate
- Measurement of the effectiveness of testing methods in identifying defects
- Helps in continuous improvement of testing processes
7. Return Rates
- Analysis of the frequency of product returns due to defects
- Assists in evaluating the overall quality control process
8. Compliance Verification
- Regular audits to ensure adherence to industry regulations
- Builds trust with customers and stakeholders
In summary, PCBA Testing and Quality Control are essential for delivering reliable electronic devices. Adhering to specific features and specifications allows manufacturers to maintain high standards of quality.
Common Applications and Use Cases
PCBA Testing and Quality Control find applications across various industries, ensuring that electronic products function reliably and meet customer expectations.
1. Telecommunications: These processes are vital in the production of communication devices, ensuring they operate correctly under various conditions.
2. Automotive: PCBA Testing is crucial for electronic components in vehicles, contributing to safety and functionality.
3. Consumer Electronics: Ensures that products like smartphones and tablets meet quality standards before reaching the market.
4. Medical Devices: Strict testing protocols are essential to guarantee the performance and safety of medical equipment.
5. Industrial Automation: PCBA Testing helps maintain high standards in control systems, enhancing operational efficiency.
6. Aerospace: Testing and quality control are critical for ensuring the reliability of electronic systems used in aircraft.
7. Military: PCBA Testing is essential for meeting rigorous standards required for defense electronics.
Product Variants and Subcategories
While specific product variants are not available, PCBA Testing and Quality Control can be tailored to meet the diverse needs of different sectors. This flexibility ensures that various applications receive the appropriate testing methodologies.
One potential variant includes high-reliability testing for sectors like aerospace and military. This type of testing focuses on extreme conditions and longevity, ensuring that components can withstand rigorous operational demands.
Another variant could involve rapid prototyping testing for consumer electronics. This approach allows manufacturers to quickly assess new designs and make adjustments before mass production.
Benefits and Advantages
PCBA Testing and Quality Control offer various benefits that enhance product reliability and company reputation.
1. Improved Product Reliability: Consistent testing ensures that products function as intended, reducing the likelihood of failures.
2. Cost Savings: Early detection of defects minimizes costly recalls and warranty claims.
3. Enhanced Customer Satisfaction: High-quality products lead to greater customer trust and loyalty.
4. Regulatory Compliance: Adhering to quality standards helps avoid legal issues and ensures market access.
5. Streamlined Production Processes: Effective testing reduces bottlenecks and enhances overall operational efficiency.
6. Competitive Advantage: Companies that prioritize quality control can differentiate themselves in the market.
Buying Guide for B2B Buyers
When sourcing PCBA Testing and Quality Control services, several factors should be considered to ensure the best outcomes.
1. Quality Assessment: Evaluate potential suppliers based on their adherence to quality standards, such as ISO certifications.
2. Supplier Verification: Conduct thorough background checks to ensure suppliers have a proven track record of reliability and quality.
3. Pricing and MOQ: Compare costs and minimum order quantities to find a balance between quality and budget constraints.
4. Delivery and Lead Times: Consider logistics and ensure suppliers can meet required timelines without compromising quality.
5. Compliance Requirements: Verify that suppliers are compliant with relevant regulations and standards in your industry.
Compliance and Certifications
Compliance and certifications are crucial for maintaining high standards in PCBA Testing and Quality Control. Relevant quality standards, such as ISO 9001, ensure that manufacturers adhere to established practices for quality management. This certification demonstrates the ability to consistently provide products that meet customer and regulatory requirements.
Industry certifications, like CE marking, signify that products conform to health, safety, and environmental protection standards. This is particularly important for devices intended for the European market.
Safety and testing requirements must also be considered, as they vary across industries. Regulatory compliance ensures that products are safe for use and meet the necessary legal and market demands. Additionally, regional compliance considerations may vary, emphasizing the importance of understanding local regulations and standards.
Why Source PCBA Testing & Quality Control from Pepagora?
Pepagora offers a reliable platform for sourcing PCBA Testing and Quality Control with several advantages that set it apart from competitors.
Verified Supplier Network: Pepagora maintains a robust network of verified suppliers, ensuring that buyers have access to reputable manufacturers. This network helps streamline the sourcing process and enhances trust.
Streamlined RFQ Process: The request for quotation (RFQ) system simplifies the procurement process. Buyers can quickly receive multiple quotes, allowing for better comparison and decision-making.
Trade Assurance and Support: Pepagora provides trade assurance, protecting buyers from potential risks in transactions. This support helps foster confidence in sourcing decisions.
Regional Coverage: With a focus on regions like India, the GCC, and Southeast Asia, Pepagora connects buyers with suppliers that understand local market dynamics and compliance needs. This geographic reach enhances the overall sourcing experience, ensuring that businesses can find suitable partners for their PCBA Testing and Quality Control requirements.

 IN

 India