IN
₹
Apparel & Fashion

Description
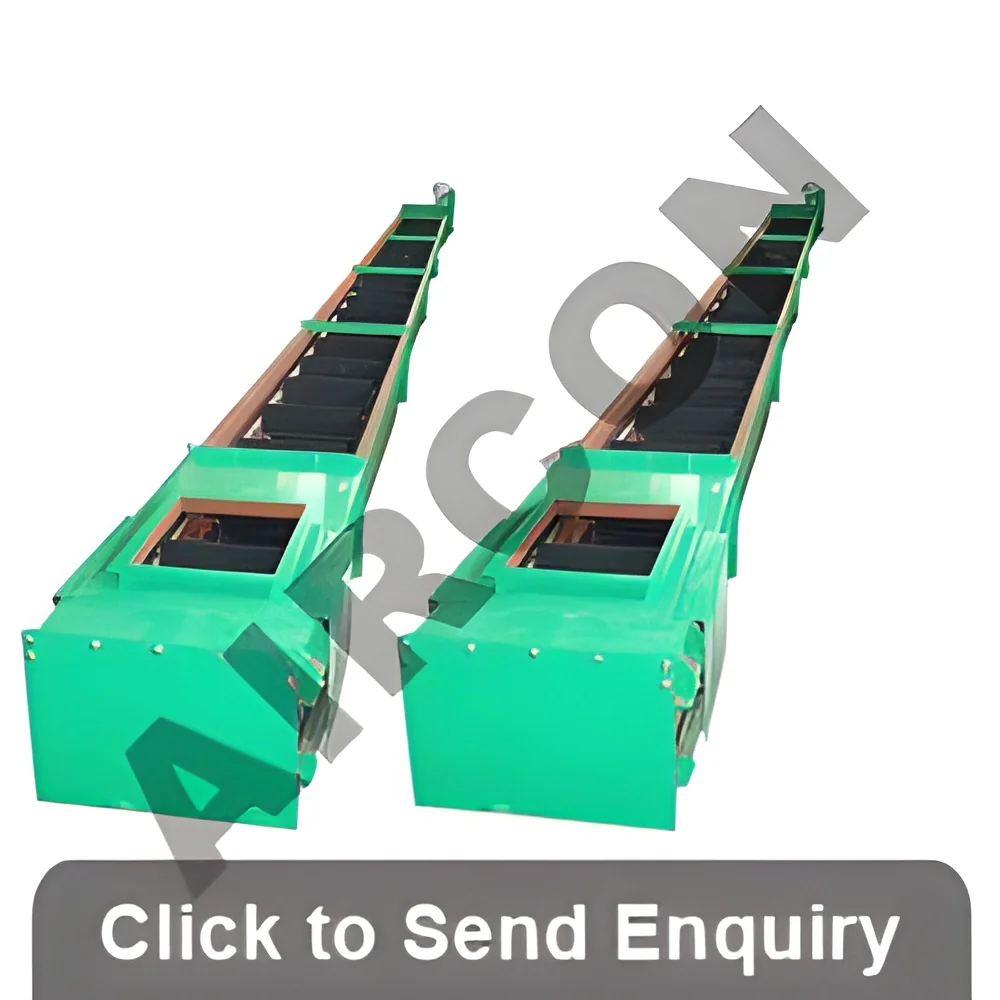
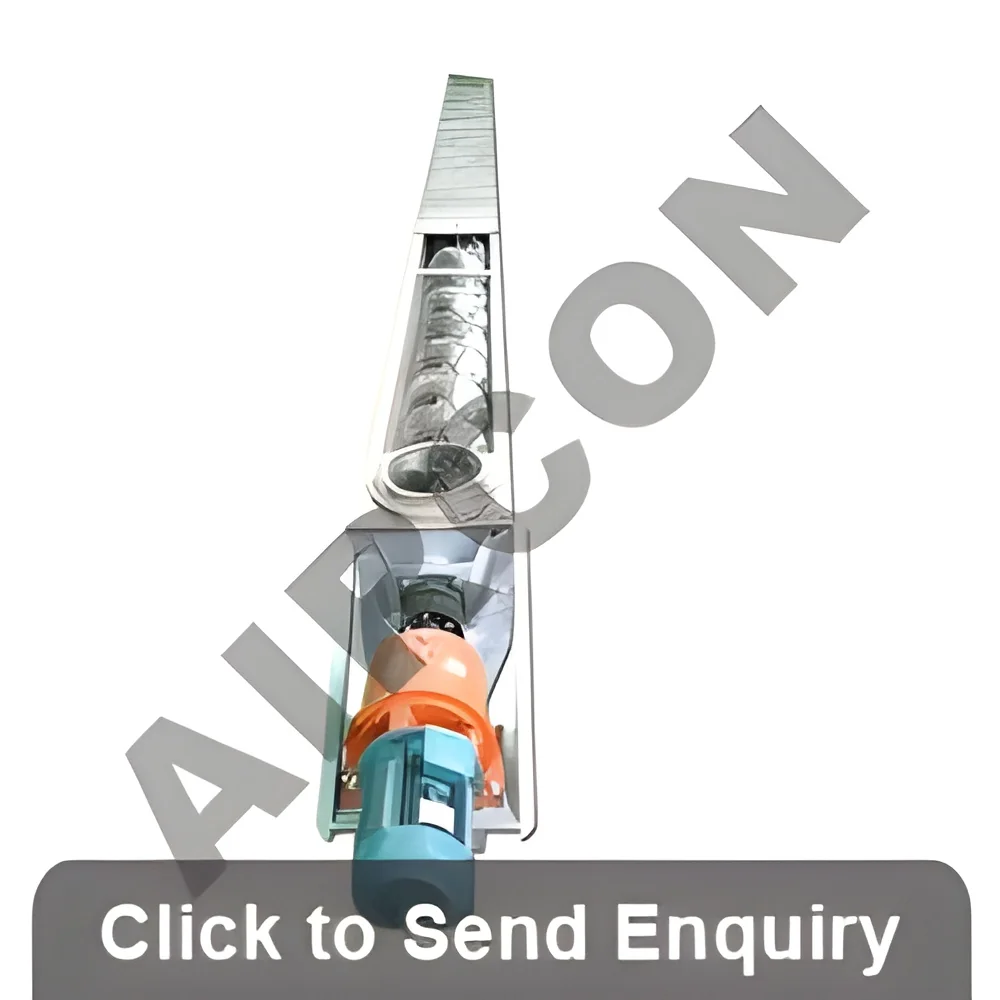
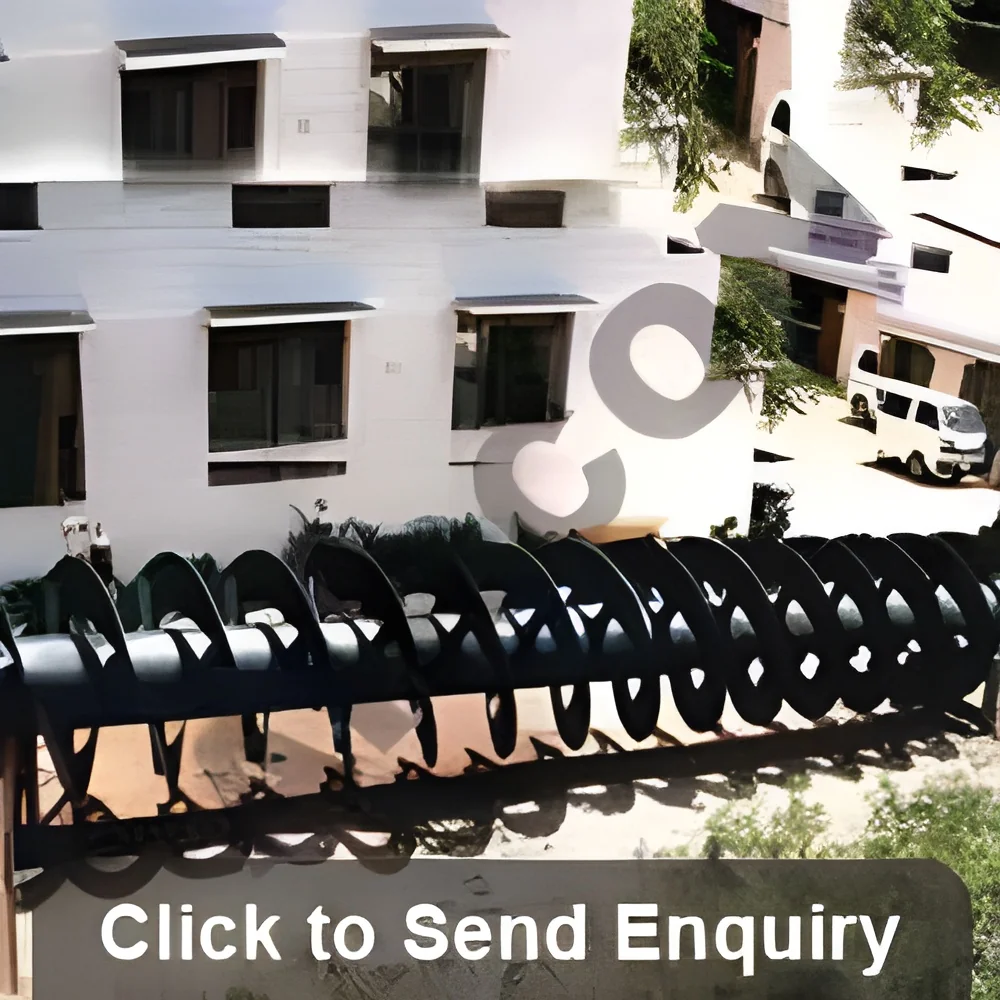
Our industrial paddle conveyors are engineered for superior performance in demanding bulk material handling applications. These robust systems efficiently combine conveying and mixing operations in a single unit, handling everything from fine powders to coarse granules without degradation. The unique paddle design ensures thorough blending while transporting materials, eliminating the need for separate mixing equipment and streamlining your production process. This dual functionality provides a cost-effective, space-saving solution that delivers both reliability and versatility for various industrial processing requirements.

These conveyors serve critical functions across multiple industries where precision blending during transport is essential. In food processing, they ensure uniform mixing of ingredients like flour, spices, and additives while moving through production lines. Chemical plants rely on them for consistent blending of powders and granules to maintain product quality st...
Our industrial paddle conveyors are engineered for superior performance in demanding bulk material handling applications. These robust systems efficiently combine conveying and mixing operations in a single unit, handling everything from fine powders to coarse granules without degradation. The unique paddle design ensures thorough blending while transporting materials, eliminating the need for separate mixing equipment and streamlining your production process. This dual functionality provides a cost-effective, space-saving solution that delivers both reliability and versatility for various industrial processing requirements.

These conveyors serve critical functions across multiple industries where precision blending during transport is essential. In food processing, they ensure uniform mixing of ingredients like flour, spices, and additives while moving through production lines. Chemical plants rely on them for consistent blending of powders and granules to maintain product quality standards. Agricultural operations benefit from efficient handling and mixing of grains, seeds, and fertilizers. Pharmaceutical applications require the precise mixing of active ingredients during conveyance, while construction sectors use them for homogeneous blending of cement, sand, and other building materials to ensure batch consistency.

Businesses choose our paddle conveyors for their exceptional reliability and operational efficiency improvements. Constructed with high-quality materials and robust engineering, these systems require minimal maintenance and reduce downtime, providing long-term value. Customizable dimensions, capacities, and configurations ensure perfect integration with existing production lines, while adjustable controls allow precise management of material flow and blending intensity. This combination of features delivers consistent process results, supports scalable growth, and enhances overall production efficiency for industrial operations.

Key Features:
- Robust construction designed for demanding industrial environments and continuous operation
- Unique paddle design that ensures efficient mixing while conveying materials
- Customizable dimensions, capacities, and configurations to fit specific operational needs
- Adjustable controls for precise management of material flow and blending intensity
- Compatibility with wide range of materials including powders, granules, and coarse solids

Benefits:
- Combines conveying and mixing in one unit, reducing equipment needs and saving space
- Ensures homogeneous blending during transport for consistent product quality
- Minimizes maintenance requirements and reduces operational downtime
- Provides precise control over material flow and mixing intensity
- Handles diverse materials from fine powders to coarse granules efficiently
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial paddle conveyors perform simultaneous conveying and thorough mixing of bulk materials, handling powders, granules, and other solids with consistent efficiency. Their adjustable design provides precise control over material flow and mixing intensity, making them suitable for diverse production environments and reducing the need for separate equipment. These systems optimize processing lines by delivering reliable performance while minimizing maintenance requirements. From food processing to construction materials, paddle conveyors support consistent output quality and handle demanding industrial conditions with dependable operation.
Real-world applications:
- Food processing for uniform mixing of ingredients like flour, sugar, and spices during conveyance
- Chemical industry for blending powders and granules to ensure consistent product quality
- Agriculture for handling and mixing grains, seeds, and fertilizers efficiently
- Pharmaceuticals for precise conveying and mixing of active ingredients in production lines
- Construction materials for homogeneous blending of cement, sand, and additives
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aircon Handling Systems Private Limited, Karnataka
 Karnataka, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Oceania
Northern Europe
South America
Mid East
Southern Europe
Eastern Europe
Eastern Asia
South Asia
Southeast Asia
Western Europe
Africa
Central America
Quality & Certification
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Industrial Paddle Conveyors For Bulk Solids Mixing And Transport
Industrial paddle conveyors efficiently mix and transport bulk solids like powders and granules. These reliable systems are ideal for food, chemical, agricultural, pharmaceutical, and construction industries requiring precision blending during material handling operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aircon Handling Systems Private Limited
 Karnataka, India
Industrial Equipment & MachineryManufacturer