IN
₹
Apparel & Fashion
Description
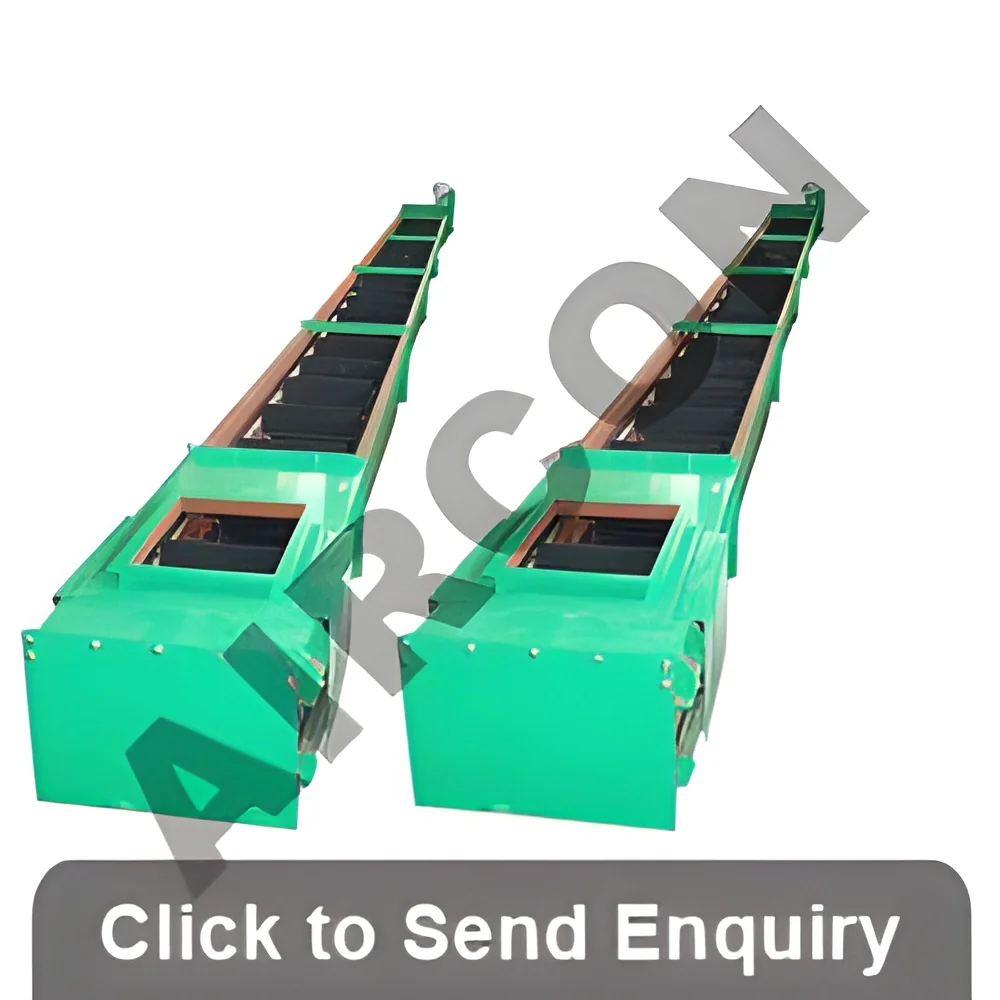
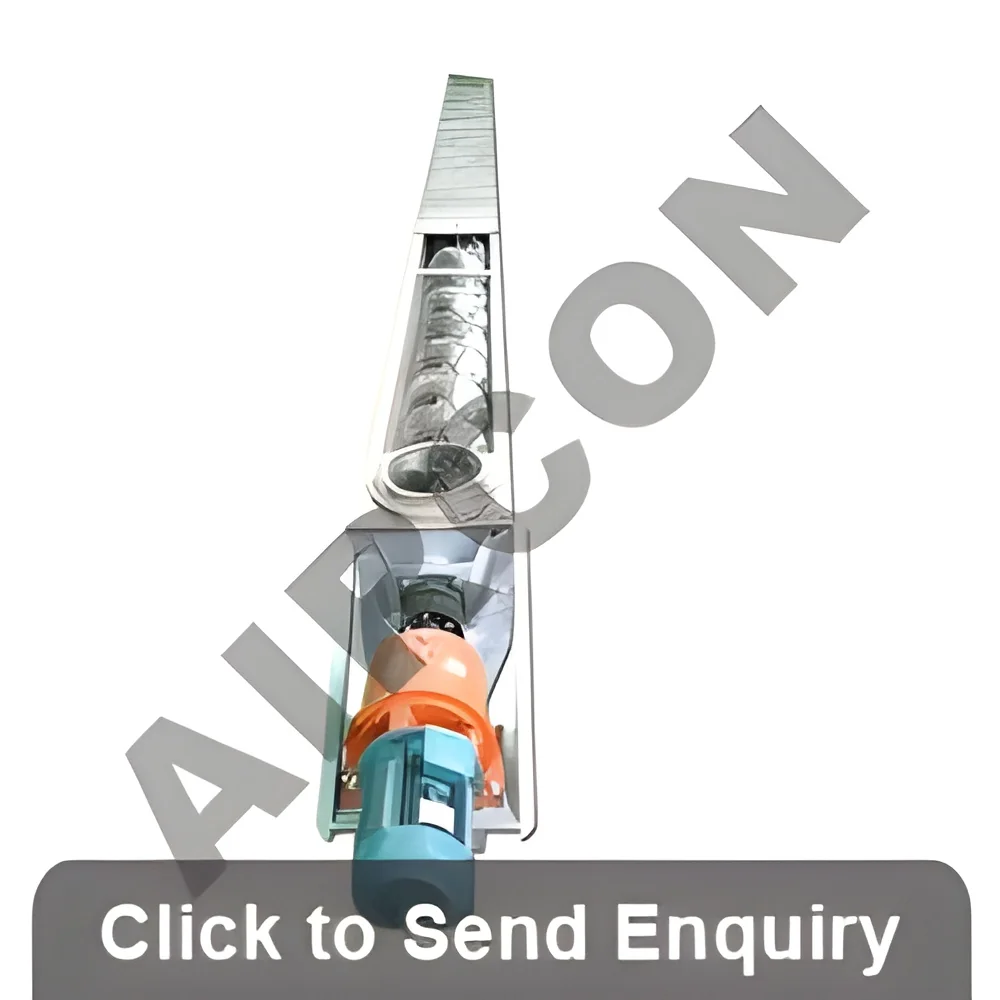
Our premium screw conveyors represent advanced bulk material handling technology engineered to meet rigorous international quality standards for superior performance in demanding industrial environments. These systems efficiently handle diverse materials including hot, abrasive, or dusty substances through precision-designed helical screws that move bulk materials through enclosed troughs with minimal spillage and contamination. The robust construction ensures reliable operation while the durable design provides perfect adaptation to specific operational requirements, making them the ideal choice for businesses seeking efficient material handling solutions that stand the test of time in challenging industrial settings.

These screw conveyors serve critical functions across multiple industries including cement and construction for handling aggregates, food processing for ingredient transportation, chemical manufacturing for powder handling, pharmaceutical production for contamination-fr...
Our premium screw conveyors represent advanced bulk material handling technology engineered to meet rigorous international quality standards for superior performance in demanding industrial environments. These systems efficiently handle diverse materials including hot, abrasive, or dusty substances through precision-designed helical screws that move bulk materials through enclosed troughs with minimal spillage and contamination. The robust construction ensures reliable operation while the durable design provides perfect adaptation to specific operational requirements, making them the ideal choice for businesses seeking efficient material handling solutions that stand the test of time in challenging industrial settings.

These screw conveyors serve critical functions across multiple industries including cement and construction for handling aggregates, food processing for ingredient transportation, chemical manufacturing for powder handling, pharmaceutical production for contamination-free material transfer, and waste management for efficient recycling operations. Each industry benefits from the conveyor's ability to maintain material integrity, prevent environmental contamination, and ensure consistent flow rates while meeting specific regulatory requirements and operational challenges unique to their sector, providing tailored solutions for diverse industrial needs.

The business value of our screw conveyors lies in their exceptional reliability, reduced maintenance requirements, and long-term cost efficiency. Built with heavy-duty components and quality materials, these systems withstand the most demanding industrial conditions while minimizing operational downtime. The enclosed design not only protects materials from external elements but also prevents dust emissions, contributing to cleaner and safer working environments while ensuring compliance with industry regulations and standards, delivering outstanding return on investment through years of trouble-free operation.

Key Features:
- Heavy-duty construction built to international quality standards
- Enclosed trough design preventing contamination and dust emission
- Precision helical screws for efficient material movement
- Durable components resistant to abrasive and corrosive materials
- Engineered for demanding industrial environments and continuous operation

Benefits:
- Reduced maintenance requirements and operational downtime
- Long-term cost efficiency and return on investment
- Consistent material flow and handling precision
- Enhanced workplace safety and environmental compliance
- Reliable performance in challenging industrial conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Screw conveyors efficiently transport bulk materials horizontally, vertically, or at inclines across diverse industrial sectors. These robust systems handle everything from fine powders and granules to semi-solid materials with consistent reliability and precision, ensuring smooth operational flow in material handling processes. Their enclosed design prevents contamination and dust emission while maintaining material integrity throughout transportation.
These systems are ideal for industries requiring hygienic handling, minimal maintenance, and continuous operation without compromising safety or efficiency. The reliable performance makes them suitable for businesses seeking durable material handling solutions that maintain consistent performance across multiple industrial applications and challenging environments.
- Transferring cement and construction aggregates in building material manufacturing plants
- Moving grains, seeds, and agricultural products in food processing and storage facilities
- Handling chemical powders, pigments, and industrial raw materials in manufacturing plants
- Transporting food ingredients, spices, and pharmaceutical components in production lines
- Managing waste materials, recyclables, and biomass in environmental processing facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aircon Handling Systems Private Limited, Karnataka
 Karnataka, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Oceania
Northern Europe
South America
Mid East
Southern Europe
Eastern Europe
Eastern Asia
South Asia
Southeast Asia
Western Europe
Africa
Central America
Quality & Certification
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Premium Screw Conveyor For Bulk Material Handling In Industrial Sectors
Premium screw conveyor for industrial bulk material handling offers reliable transport of powders, granules, and semi-solids. Built to international standards for durability and superior performance in demanding environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aircon Handling Systems Private Limited
 Karnataka, India
Industrial Equipment & MachineryManufacturer