IN
₹
Apparel & Fashion
Description
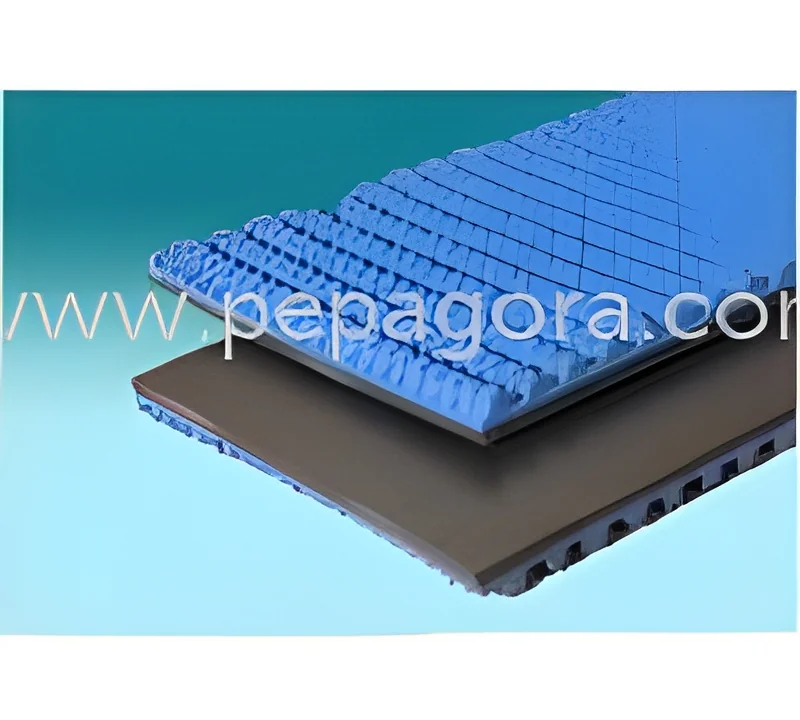
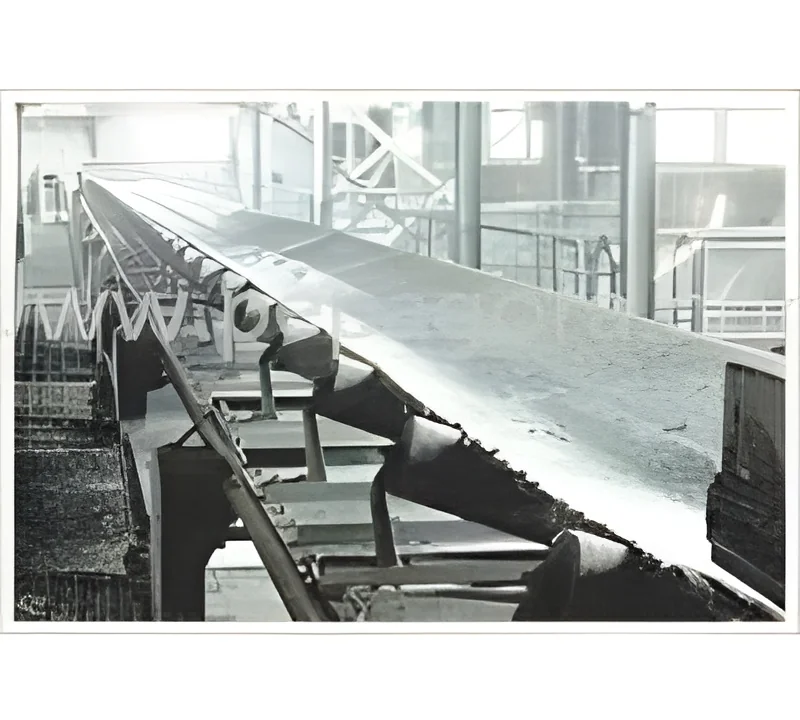
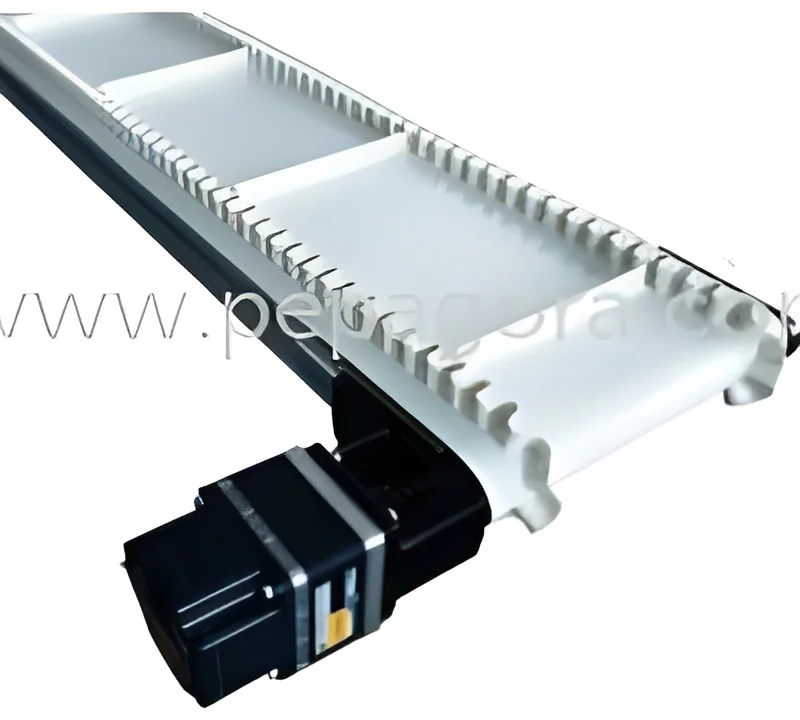
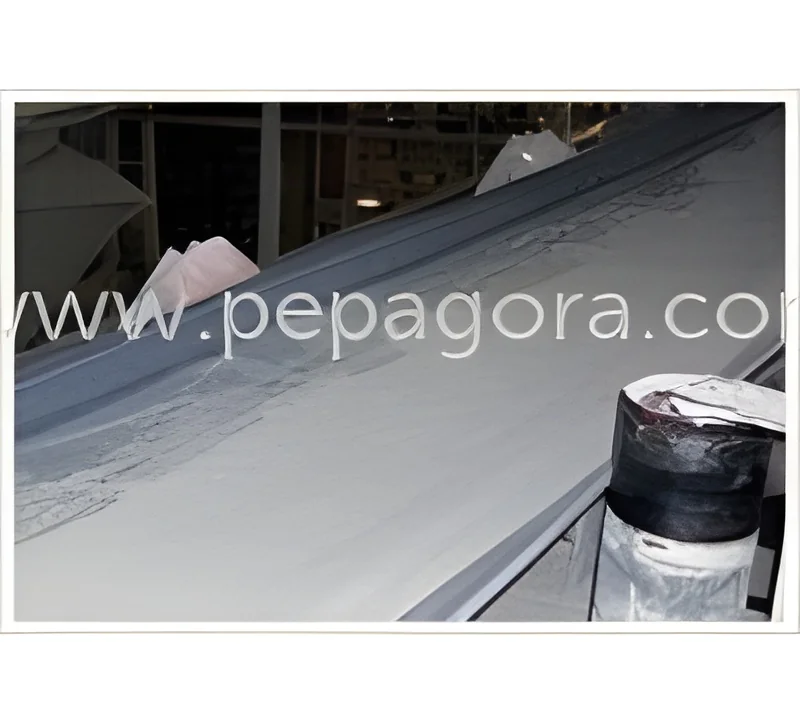
We provide premium industrial conveyor belts, manufactured to exacting ISO standards, ensuring they meet rigorous international benchmarks for quality and performance. Engineered for heavy-duty material handling, these belts are built to deliver reliable, continuous operation in the most demanding industrial environments. Their construction focuses on durability and efficiency, directly contributing to reduced downtime and lower long-term maintenance costs. This makes them a dependable core component for businesses looking to enhance their automation capabilities and streamline logistics operations, supporting uninterrupted productivity.

These conveyor belts serve as critical infrastructure across a wide range of industries. In manufacturing, they are essential for seamlessly moving components and finished products through production lines. The mining and agriculture sectors utilize them for the efficient transport of bulk materials like ores, coal, grains, and fertilizers. Within log...
We provide premium industrial conveyor belts, manufactured to exacting ISO standards, ensuring they meet rigorous international benchmarks for quality and performance. Engineered for heavy-duty material handling, these belts are built to deliver reliable, continuous operation in the most demanding industrial environments. Their construction focuses on durability and efficiency, directly contributing to reduced downtime and lower long-term maintenance costs. This makes them a dependable core component for businesses looking to enhance their automation capabilities and streamline logistics operations, supporting uninterrupted productivity.

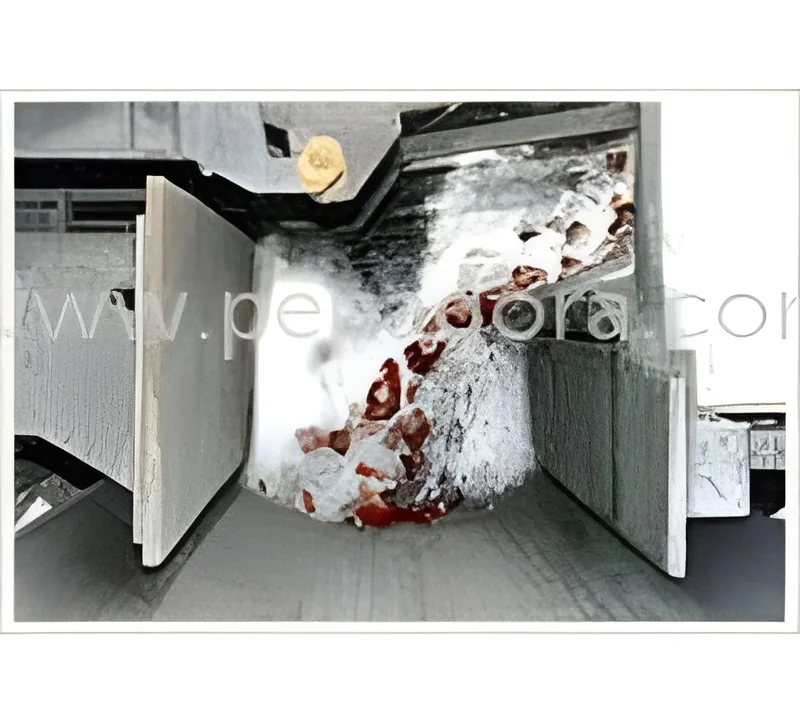
These conveyor belts serve as critical infrastructure across a wide range of industries. In manufacturing, they are essential for seamlessly moving components and finished products through production lines. The mining and agriculture sectors utilize them for the efficient transport of bulk materials like ores, coal, grains, and fertilizers. Within logistics and aviation, they are fundamental for cargo handling, baggage systems, and warehouse automation. Furthermore, they are employed in thermal power plants, shipyards, and heavy industry for operations involving significant loads, where safety and consistent output are paramount. Their reliable performance also makes them suitable for precision-driven sectors like food processing and pharmaceuticals.

The business value delivered by these conveyor belts is substantial, centered on enhancing operational efficiency, reducing reliance on manual labor, and minimizing costly production stoppages. Their inherent reliability is a product of robust construction, adherence to ISO certification protocols, and stringent quality control measures, ensuring long service life even under stressful conditions. Key differentiators include superior material quality, exceptional resistance to wear, heat, and abrasion, and engineering designed for seamless integration with existing systems. By improving throughput and enabling greater automation, they help businesses achieve higher productivity, faster turnaround times, and enhanced operational safety, representing a strategic investment for growth-focused operations.

Key Features:
- ISO-certified manufacturing process guaranteeing consistent international quality standards.
- Robust, heavy-duty construction designed for longevity and demanding operational environments.
- Engineered with high resistance to abrasion, heat, and harsh industrial conditions.
- Precision engineering ensures smooth, reliable operation with minimal vibration and noise.
- Designed for easy integration and compatibility with a wide range of existing material handling systems.

Benefits:
- Enhances operational efficiency and throughput by enabling continuous, automated material flow.
- Reduces long-term operational costs through durability and minimal maintenance requirements.
- Improves workplace safety by minimizing manual handling of heavy or hazardous materials.
- Provides reliable performance that decreases downtime and protects against production losses.
- Offers a scalable solution that supports business growth and adapts to increasing operational demands.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our ISO-certified industrial conveyor belts are engineered to handle demanding material transport across various sectors. They efficiently move bulk goods, raw materials, and packaged items, ensuring a continuous flow in production and distribution environments. The robust design minimizes operational interruptions, supporting high-volume throughput where reliability is non-negotiable. These belts form the backbone of automated systems, enhancing productivity in plants, warehouses, and processing facilities by reducing manual handling and streamlining workflows.
Industries with rigorous operational demands, such as mining, agriculture, food processing, and logistics, depend on these conveyor belts for critical daily functions. They are integral to assembly lines, sorting systems, and loading operations, enabling scalable growth and faster material turnaround. Built to withstand high loads, abrasive substances, and variable temperatures, they deliver consistent performance. Their design adapts to specific layout and operational challenges, providing a versatile and dependable solution for modern industrial material handling needs.
- Transporting raw materials and finished goods along manufacturing and assembly lines.
- Sorting and moving luggage, parcels, and cargo at airports and logistics centers.
- Handling bulk commodities like grains, minerals, and aggregates in mining and agricultural operations.
- Automating packaging, processing, and sorting lines in food, beverage, and pharmaceutical facilities.
- Facilitating efficient loading and unloading processes in ports, shipyards, and large-scale warehouses.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Eureka Conveyor Beltings Pvt Ltd, Rajasthan
 Rajasthan, India
Raw Materials & Chemicals•Manufacturer•Retailer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Conveyor Belts ISO Certified Heavy Duty Material Handling
ISO-certified industrial conveyor belts for heavy-duty material handling. Engineered for reliability in manufacturing, logistics, and mining. Durable construction ensures seamless operations and long-term performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Eureka Conveyor Beltings Pvt Ltd
 Rajasthan, India
Raw Materials & ChemicalsManufacturer