IN
₹
Apparel & Fashion
Description
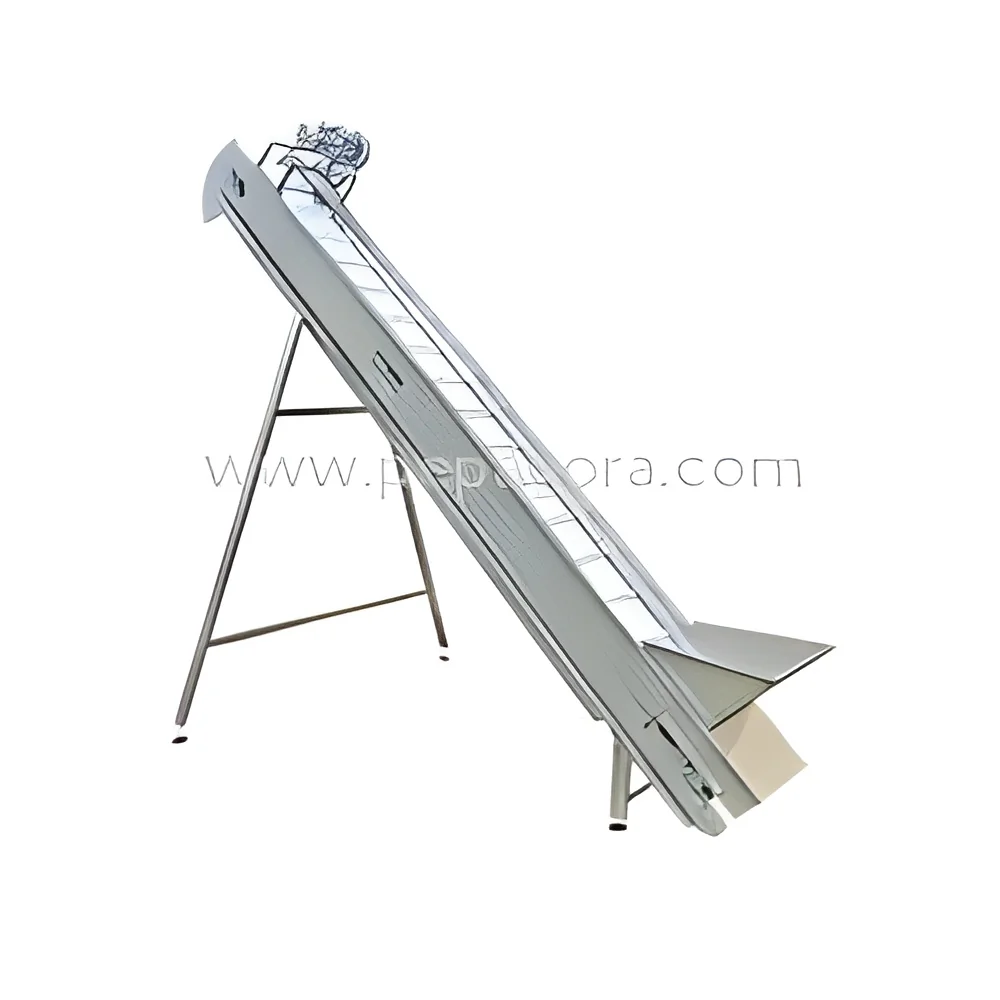
Our industrial elevator conveyor system is a premium vertical material handling solution built for demanding industrial environments. It features a robust construction of heat-resistant metal with a galvanized surface, providing exceptional durability against wear, corrosion, and high-temperature conditions. With a belt width capability of up to 3000 mm, this system is designed to handle a wide range of materials—from light packages to heavy bulk items—ensuring reliable performance and high throughput. The design prioritizes easy installation and requires minimal maintenance, making it a practical and long-lasting investment for operations that depend on continuous, efficient vertical transportation.

This conveyor system serves a vital role across multiple key industries. In manufacturing and production plants, it facilitates seamless multi-level material flow, connecting different stages of the assembly process. The mining and aggregates sector utilizes its strength to move heavy ore...
Our industrial elevator conveyor system is a premium vertical material handling solution built for demanding industrial environments. It features a robust construction of heat-resistant metal with a galvanized surface, providing exceptional durability against wear, corrosion, and high-temperature conditions. With a belt width capability of up to 3000 mm, this system is designed to handle a wide range of materials—from light packages to heavy bulk items—ensuring reliable performance and high throughput. The design prioritizes easy installation and requires minimal maintenance, making it a practical and long-lasting investment for operations that depend on continuous, efficient vertical transportation.

This conveyor system serves a vital role across multiple key industries. In manufacturing and production plants, it facilitates seamless multi-level material flow, connecting different stages of the assembly process. The mining and aggregates sector utilizes its strength to move heavy ores and minerals vertically. Agricultural operations rely on it for elevating grains and produce in processing facilities. Within food processing and pharmaceuticals, its robust and cleanable design supports hygienic material transfer. Logistics and distribution centers implement it to efficiently move pallets and packages between floors, optimizing storage density and operational speed in warehouses.

Choosing this elevator conveyor system delivers tangible business value through enhanced operational efficiency, reduced labor costs, and improved workplace safety. Its reliable performance minimizes downtime, ensuring continuous production flow and protecting your bottom line. The strong, sturdy construction and forged components guarantee long-term durability, offering a significant return on investment. With negotiable pricing, this professional-grade system is accessible for operations of various scales, providing a trustworthy solution that integrates smoothly with existing infrastructure to boost productivity and handling capacity immediately.

Key Features:
- Heat-resistant metal construction ensures reliable operation in high-temperature industrial environments.
- Galvanized surface treatment provides superior corrosion resistance for extended system longevity.
- Belt width up to 3000 mm accommodates high-capacity handling of diverse materials and loads.
- Forged processing type delivers strong, sturdy structural integrity for heavy-duty applications.
- Designed for easy installation and requires only minimum maintenance, reducing operational overhead.

Benefits:
- Enhances vertical material handling efficiency, increasing throughput and operational productivity.
- Durable heat-resistant and galvanized build reduces long-term replacement and repair costs.
- Wide belt capacity allows for handling varied material types, from bulk goods to packaged items.
- Robust construction ensures reliable, continuous performance with minimal risk of downtime.
- Easy integration and low maintenance design lower total cost of ownership and simplify operations.
Specifications
| Key Attributes | |
|---|---|
| Condition | New |
| Belt Width | Up to 3000 mm |
| Structure | Conveyor System |
| Material | Metal |
| Material Feature | Heat Resistant |
| Price | Negotiable |
| Processed Type | Forging |
| Surface | Galvanized |
| Installation | Easy |
| Performance | Excellent |
| Maintenance | Minimum |
| Construction | Strong And Sturdy |
| Application | Material Handling |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This industrial elevator conveyor system is engineered for efficient vertical transportation of bulk materials, packaged goods, and raw components across multiple levels in industrial facilities. It ensures a continuous, smooth material flow, significantly reducing manual labor while enhancing operational throughput and workplace safety in production and storage environments. The robust construction and versatile design make it suitable for diverse sectors where reliable vertical material handling is critical for daily operations and long-term productivity.
Industries that benefit from this system include agriculture, mining, food processing, pharmaceuticals, and logistics. It is particularly effective in warehouses, distribution centers, and manufacturing plants for tasks such as stacking, sorting, and order fulfillment. The system's ability to utilize vertical space efficiently helps operations maximize their floor plan, streamline processes, and meet high-volume handling demands with consistent reliability.
- Elevating bulk grains, seeds, and cereals in agricultural processing and storage silos.
- Handling powdered chemicals, minerals, and raw materials in pharmaceutical and chemical production plants.
- Transporting ores, aggregates, and heavy minerals in mining and metallurgical operations.
- Moving packaged goods, boxes, and pallets vertically in warehouse and distribution center logistics.
- Sorting and transferring products between different production levels in automated manufacturing and assembly lines.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
V. P. Engineering Works, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Mid East
Eastern Asia
South Asia
Southeast Asia
Industrial Elevator Conveyor System Heat Resistant Metal Galvanized
Industrial elevator conveyor system for vertical material handling, featuring heat-resistant galvanized metal construction with widths up to 3000 mm for reliable, efficient performance in demanding industrial applications.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
V. P. Engineering Works
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer