IN
₹
Apparel & Fashion
Description
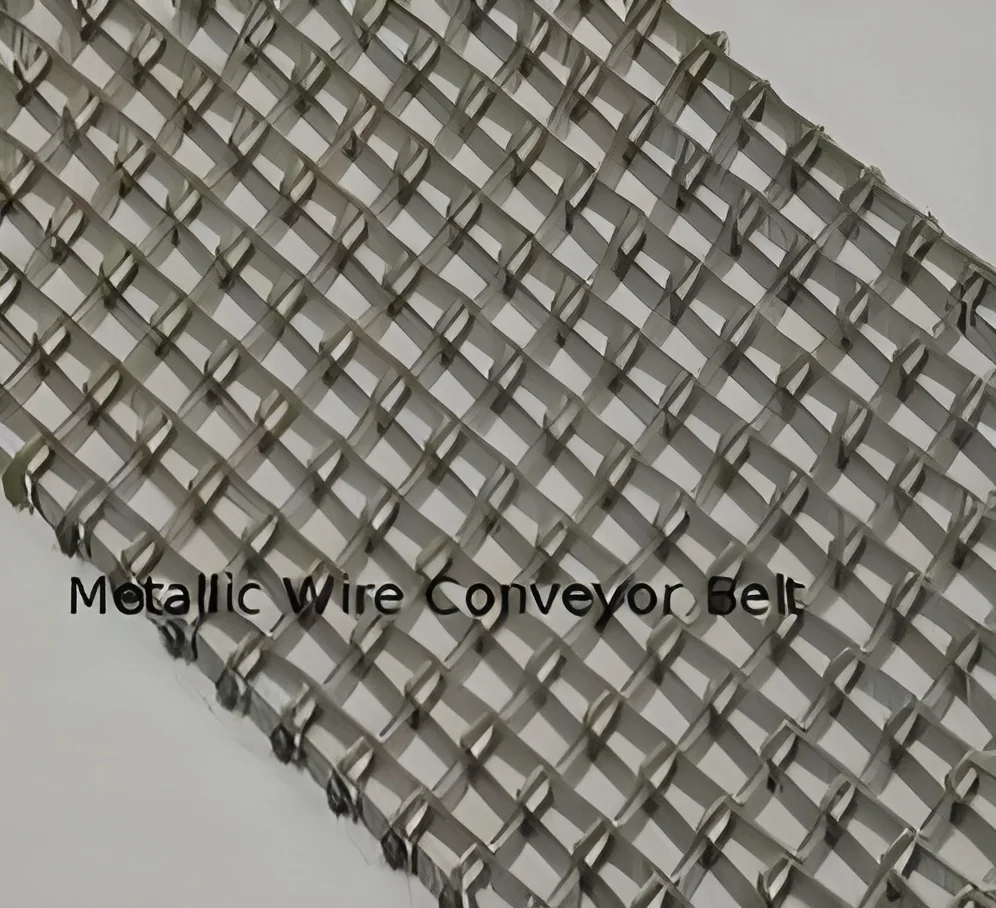
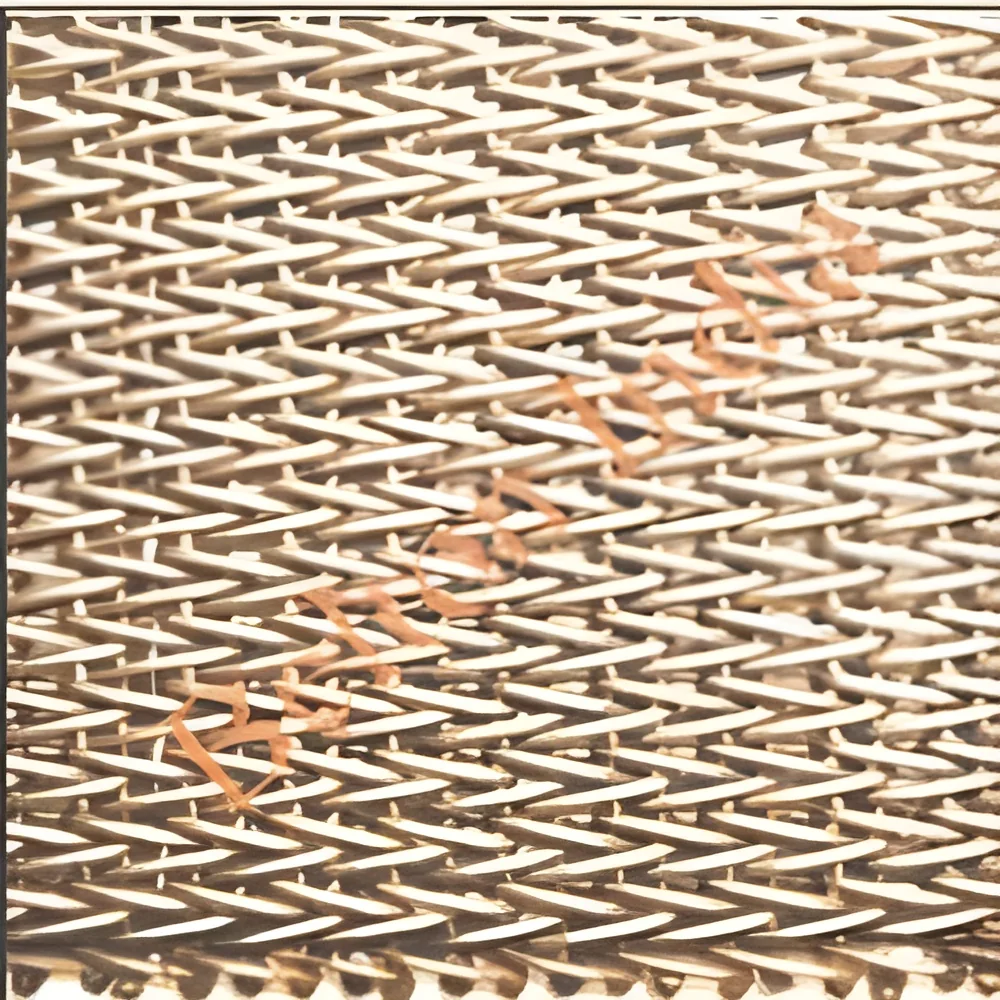
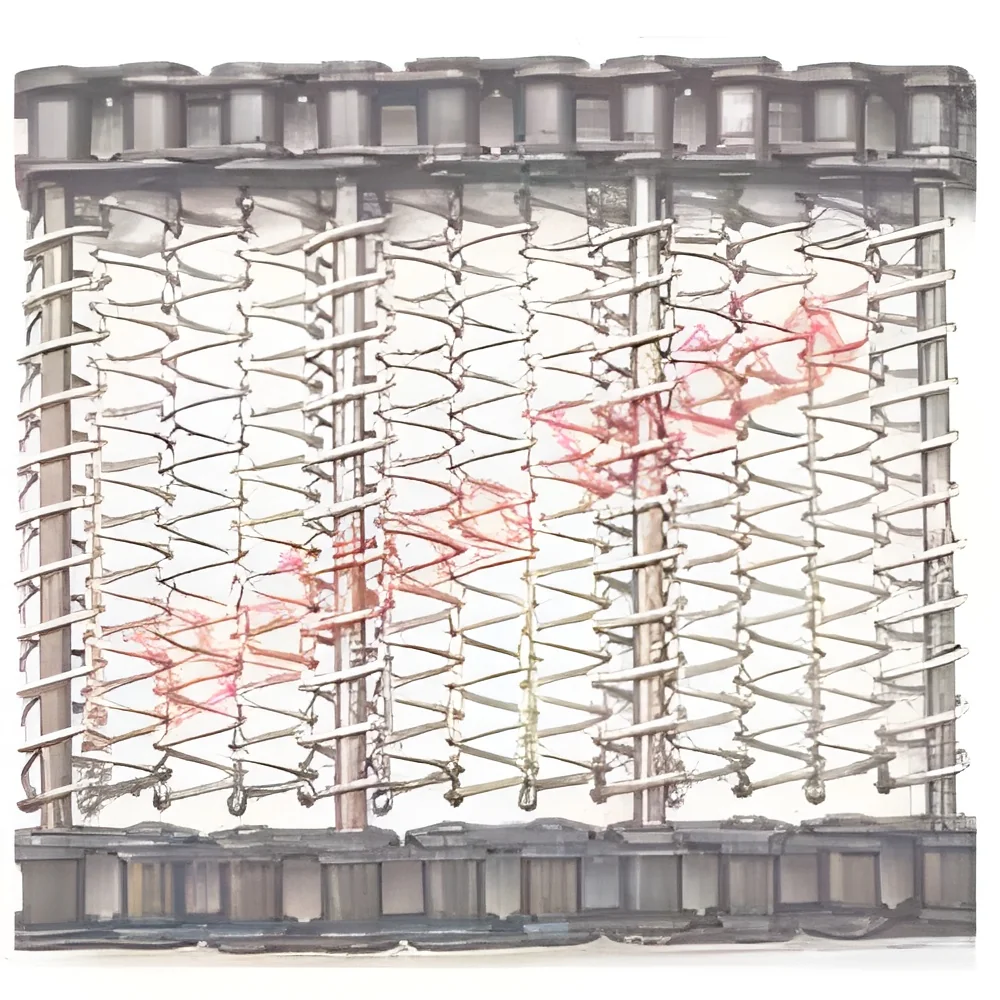
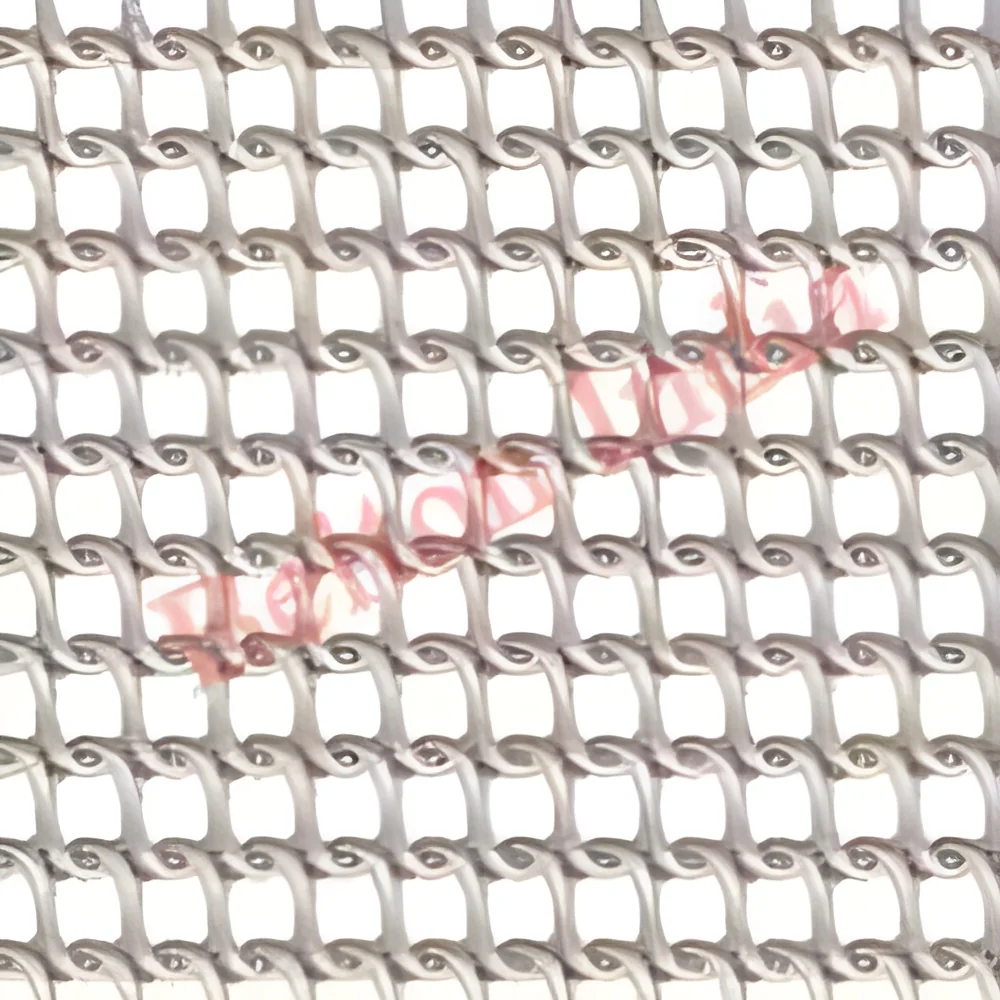
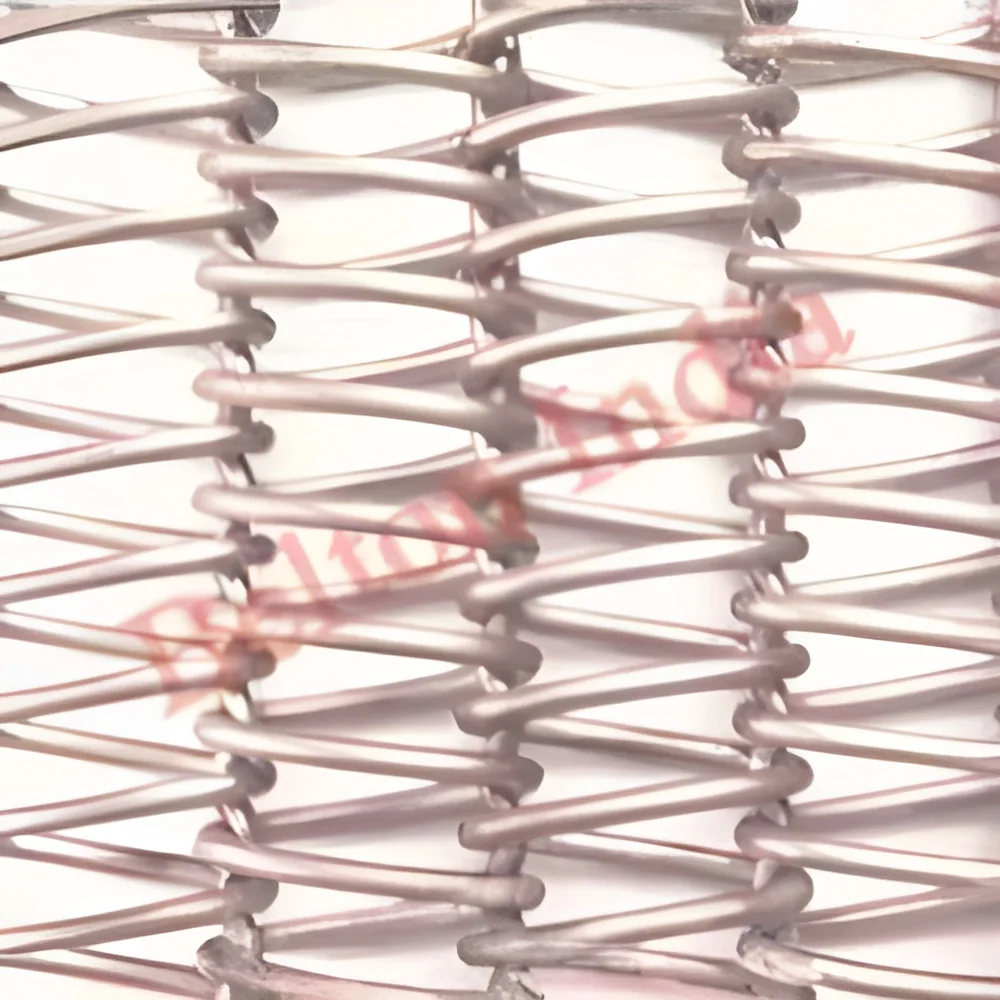
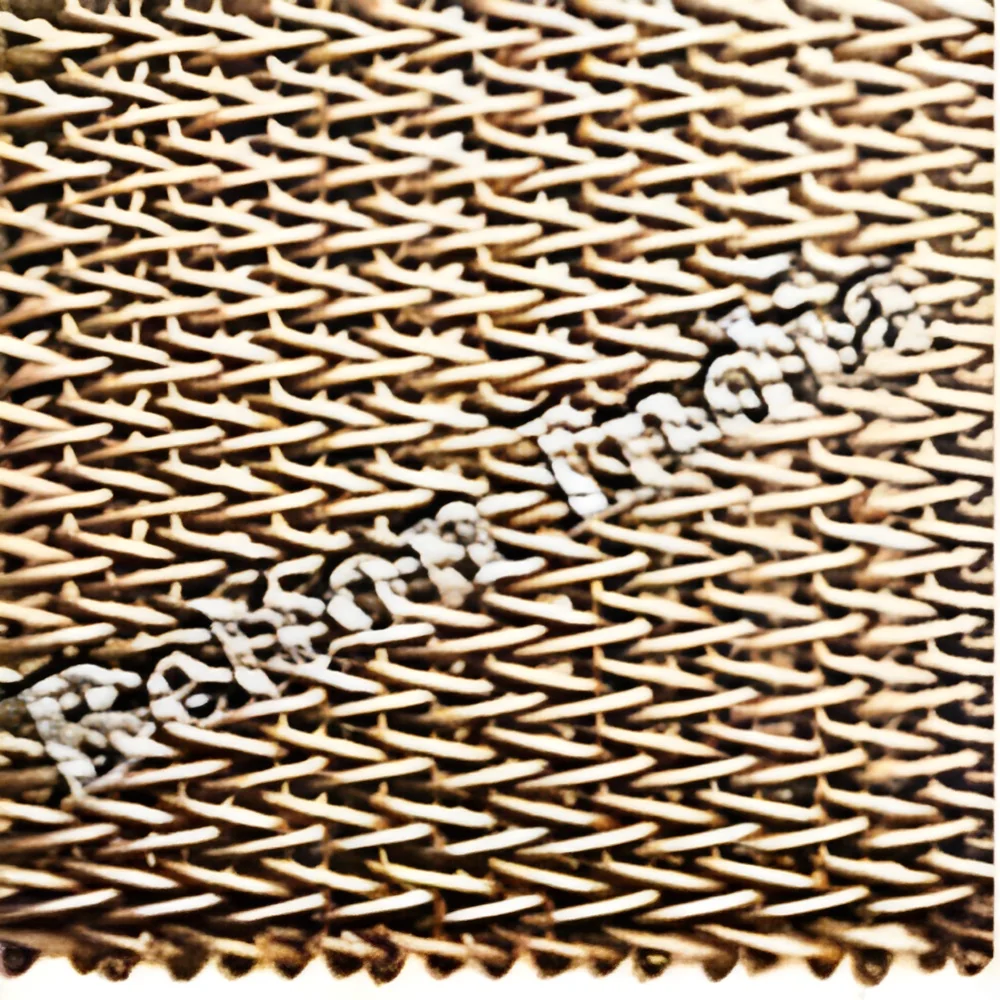
The MC-25 wire conveyor belt represents a premium industrial solution engineered for precision handling of delicate and small components across various sectors. Manufactured using high-quality 0.50mm thin wire with a tight 2mm pitch and 2.5mm coil diameter, this belt features a sophisticated locked-edge construction that ensures minimal thickness while delivering maximum operational stability. The fine mesh design, uncommon in many markets, provides exceptional durability and smooth performance even in the most demanding applications. Ideal for industries where accuracy and cleanliness are critical, the MC-25 belt supports efficient automation systems while significantly reducing product damage and loss during transportation. Its robust engineering and reliable performance make it a preferred choice for businesses seeking long-term operational consistency and superior handling capabilities.

This versatile wire conveyor belt finds extensive application across multiple industries includ...
The MC-25 wire conveyor belt represents a premium industrial solution engineered for precision handling of delicate and small components across various sectors. Manufactured using high-quality 0.50mm thin wire with a tight 2mm pitch and 2.5mm coil diameter, this belt features a sophisticated locked-edge construction that ensures minimal thickness while delivering maximum operational stability. The fine mesh design, uncommon in many markets, provides exceptional durability and smooth performance even in the most demanding applications. Ideal for industries where accuracy and cleanliness are critical, the MC-25 belt supports efficient automation systems while significantly reducing product damage and loss during transportation. Its robust engineering and reliable performance make it a preferred choice for businesses seeking long-term operational consistency and superior handling capabilities.

This versatile wire conveyor belt finds extensive application across multiple industries including electronics manufacturing, food processing, pharmaceuticals, packaging, and automotive sectors. In electronics production, it facilitates the safe and precise transport of microchips, PCBs, and sensitive components through various production stages. Food processing industries benefit from its open mesh design for operations such as frying, cooling, washing, and freezing, where excellent airflow and drainage are essential. Pharmaceutical manufacturers utilize the belt for handling tablets, capsules, and medical devices while maintaining strict hygiene standards. Packaging operations employ it for sorting and inspection tasks, while automotive manufacturers rely on its precision for accurate part placement during assembly processes. The belt's adaptability to different environmental conditions and requirements makes it an indispensable solution for diverse industrial needs.

The MC-25 conveyor belt delivers substantial business value through enhanced operational efficiency, reduced downtime, and minimized maintenance requirements. Its exceptional quality and reliability ensure consistent performance that directly translates to reduced product waste and improved production throughput. The belt's precision engineering supports high-speed automation systems, enabling companies to meet production targets while maintaining stringent quality standards. Its durable construction and proven suitability for fine applications make it a reliable long-term investment for businesses focused on achieving operational excellence and sustainable return on investment. The belt's design focuses on delivering trouble-free operation, helping companies optimize their production processes and maintain competitive advantage in their respective markets.

Key Features:
- Constructed from 0.50mm thin wire for fine mesh and minimal thickness
- 2mm pitch and 2.5mm coil diameter enabling precise handling of small components
- Locked-edge construction ensuring enhanced durability and operational stability
- Open mesh design facilitating efficient airflow, drainage, and cooling processes
- Robust engineering supporting continuous operation in demanding environments

Benefits:
- Prevents product loss and damage during transportation of delicate components
- Enables high-speed automation while maintaining precision and accuracy
- Reduces maintenance requirements and operational downtime
- Supports efficient cooling, drainage, and airflow in processing applications
- Ensures consistent performance across extended operational periods
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The MC-25 wire conveyor belt specializes in environments requiring meticulous handling of miniature components. Its fine mesh construction and minimal thickness prevent product loss or damage during transportation, making it perfect for electronics manufacturing, pharmaceutical processing, and food production where precision and hygiene standards are non-negotiable. This belt maintains stability and durability even during high-speed automated operations, ensuring consistent performance across production cycles.
Industries including electronics assembly, precision engineering, and packaging rely on the MC-25 for its dependable operation and consistent results. The open mesh design facilitates efficient cooling, drainage, and airflow, which proves essential during processes like soldering, washing, coating, or thermal treatment. Its robust construction handles continuous operation while meeting specific layout and load demands, enhancing overall operational efficiency across diverse industrial settings and applications.
- Electronics manufacturing for transporting microchips and small PCB components through assembly lines
- Food processing operations for cooling, frying, or freezing small items like nuts, snacks, and confectionery
- Pharmaceutical production for handling tablets, capsules, and medical devices under strict hygiene protocols
- Packaging facilities for sorting, inspecting, and transferring lightweight products and components
- Automotive manufacturing for precise part placement during assembly and quality testing processes
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Belton India, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
MC 25 Wire Conveyor Belt For Electronics And Food Processing
MC-25 wire conveyor belt handles small electronic components and food items with precision. Featuring 0.50mm wire, 2mm pitch, and 2.5mm coil diameter for reliable performance in demanding industrial applications requiring smooth operation and superior quality.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Belton India
 Punjab, India
Industrial Equipment & MachineryManufacturer