IN
₹
Description
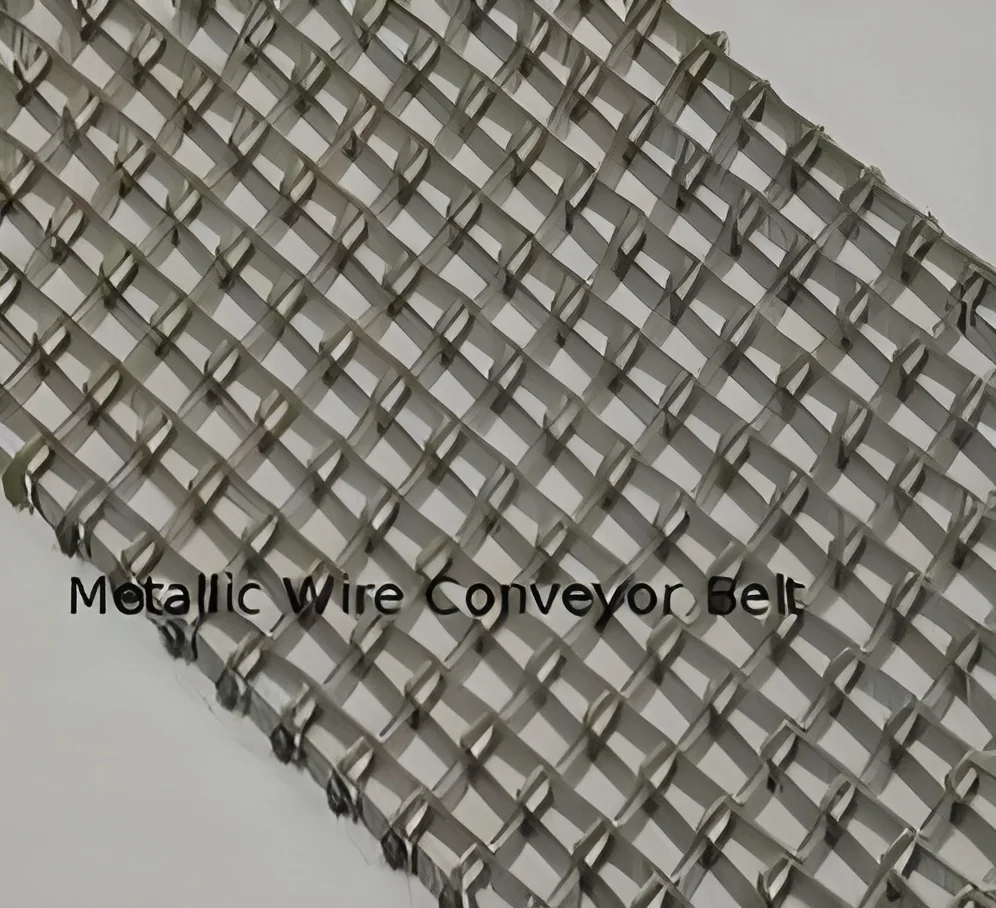
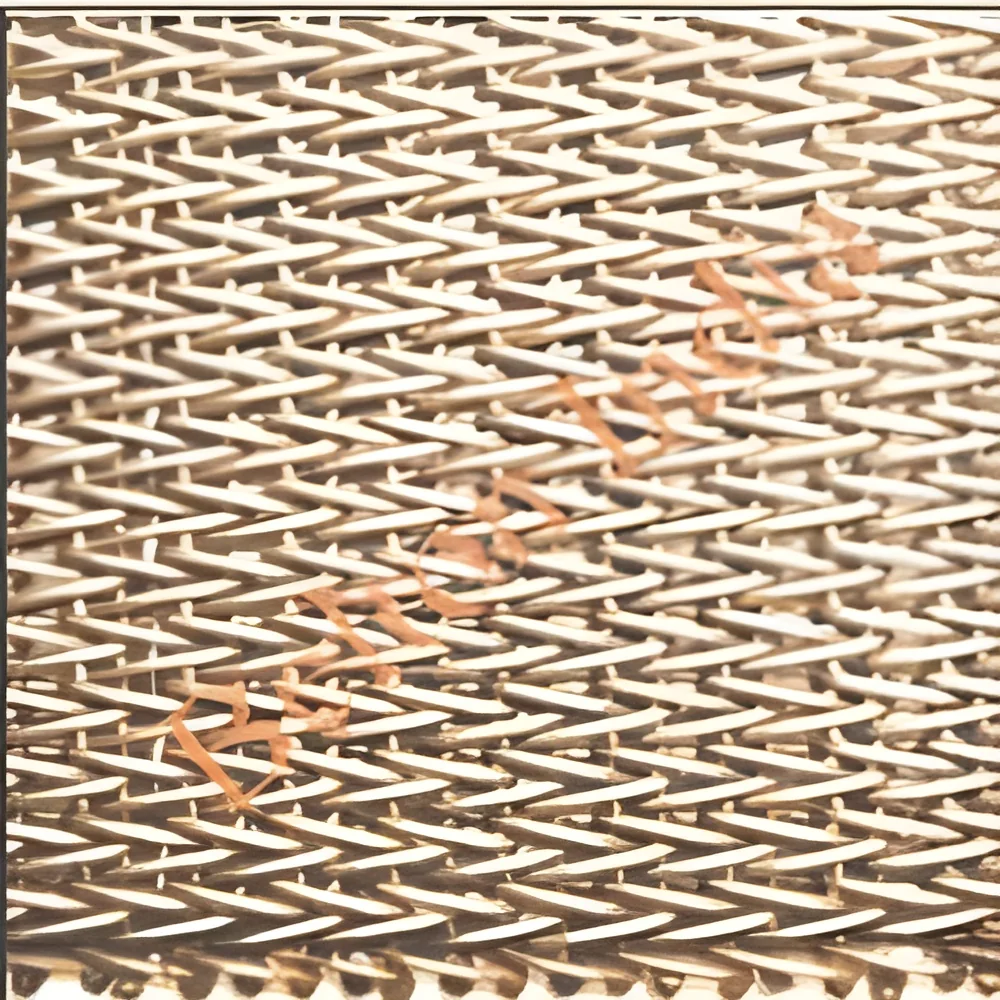
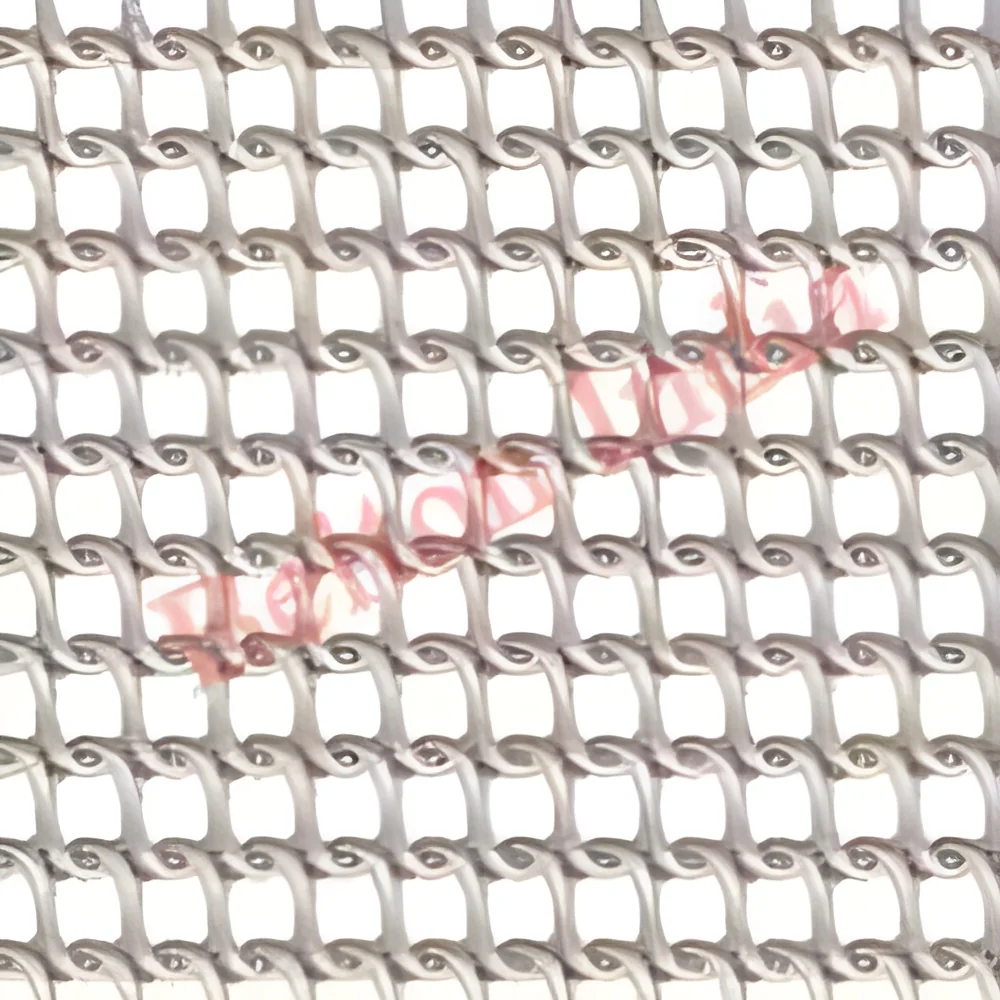
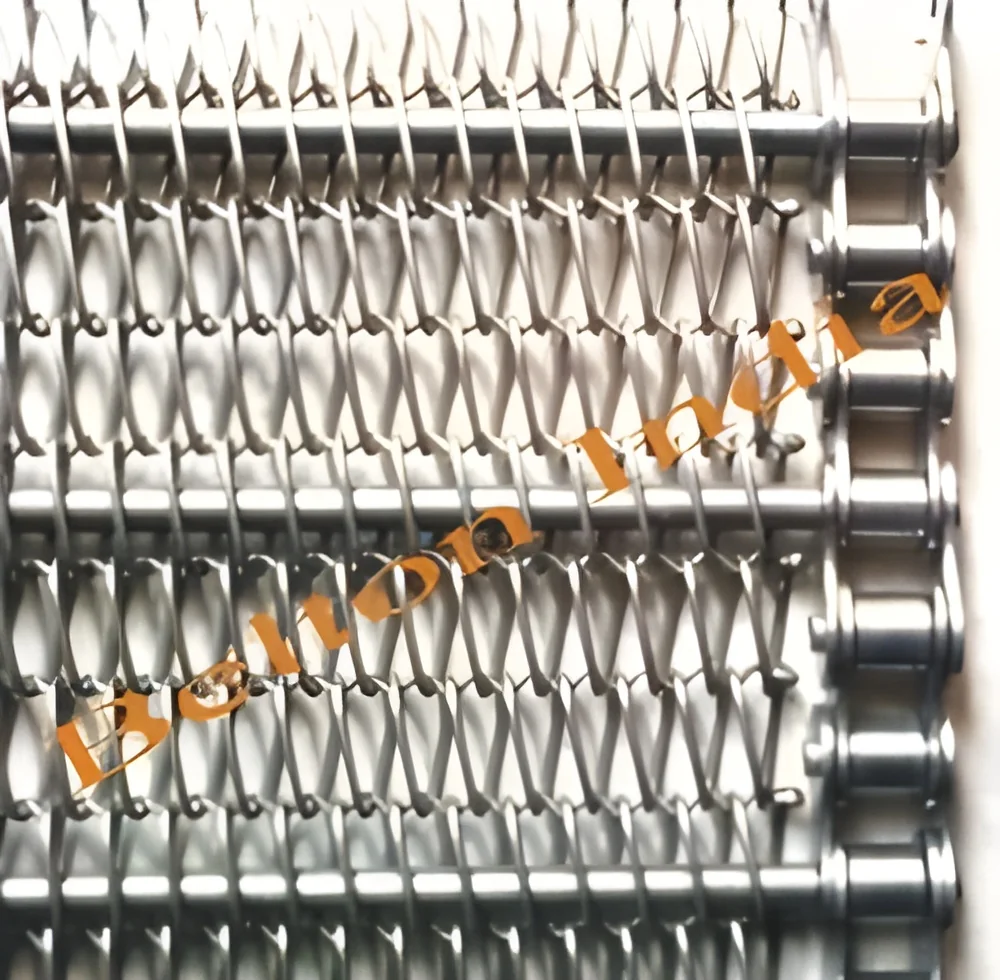
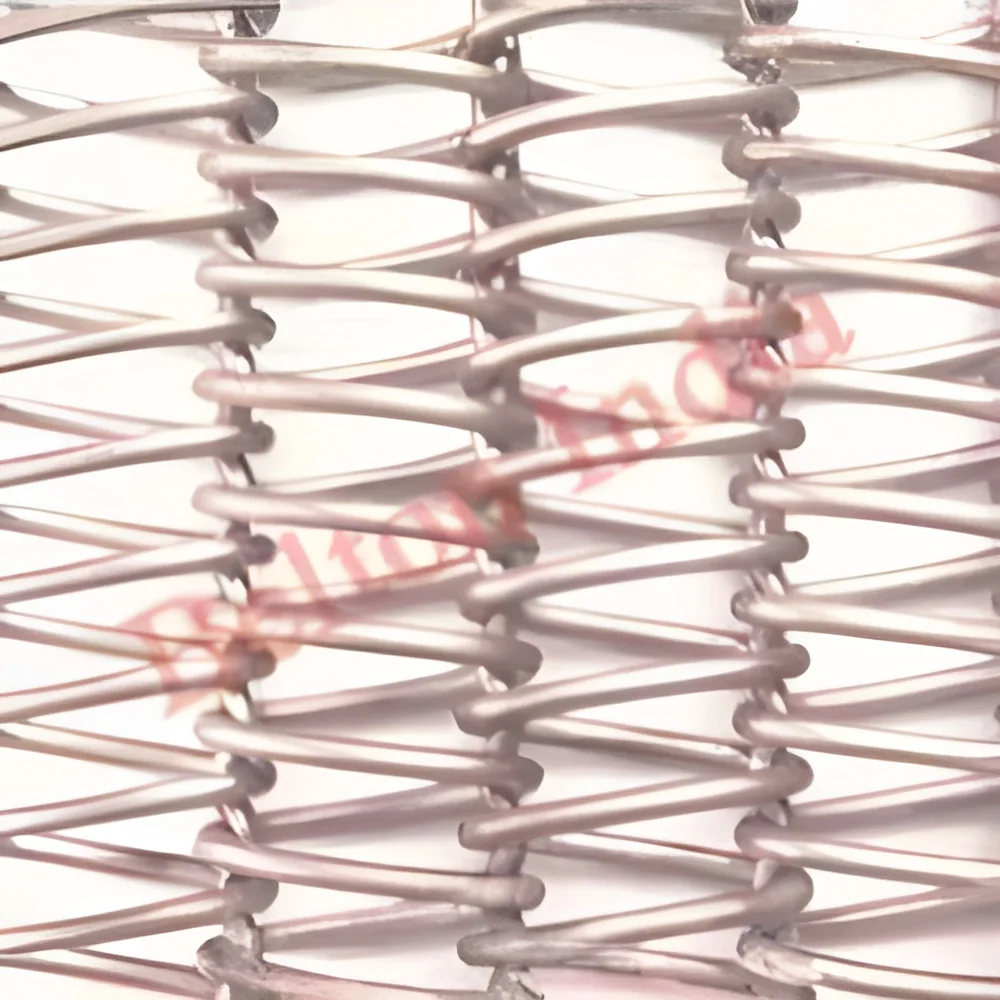
Our food grade conveyor belts with reinforced roller chain edges represent the pinnacle of reliability in industrial food handling systems. Designed with reinforced roller chains attached at both edges using thick rods inserted at precise intervals, these belts deliver exceptional longevity and consistent performance under demanding conditions. Available in multiple chain pitches including 3/8”, 1/2”, 5/8”, 3/4”, and 1”, they accommodate both mild steel and stainless steel chains based on specific operational requirements. The robust construction ensures minimal maintenance while providing superior traction and product handling capabilities for various food processing applications, making them a trusted choice for continuous production environments.

These conveyor belts serve critical functions across multiple food industry sectors including snack manufacturing, bakery operations, and ready-to-eat food production facilities. They are particularly valuable in namkeen making plants, cha...
Our food grade conveyor belts with reinforced roller chain edges represent the pinnacle of reliability in industrial food handling systems. Designed with reinforced roller chains attached at both edges using thick rods inserted at precise intervals, these belts deliver exceptional longevity and consistent performance under demanding conditions. Available in multiple chain pitches including 3/8”, 1/2”, 5/8”, 3/4”, and 1”, they accommodate both mild steel and stainless steel chains based on specific operational requirements. The robust construction ensures minimal maintenance while providing superior traction and product handling capabilities for various food processing applications, making them a trusted choice for continuous production environments.

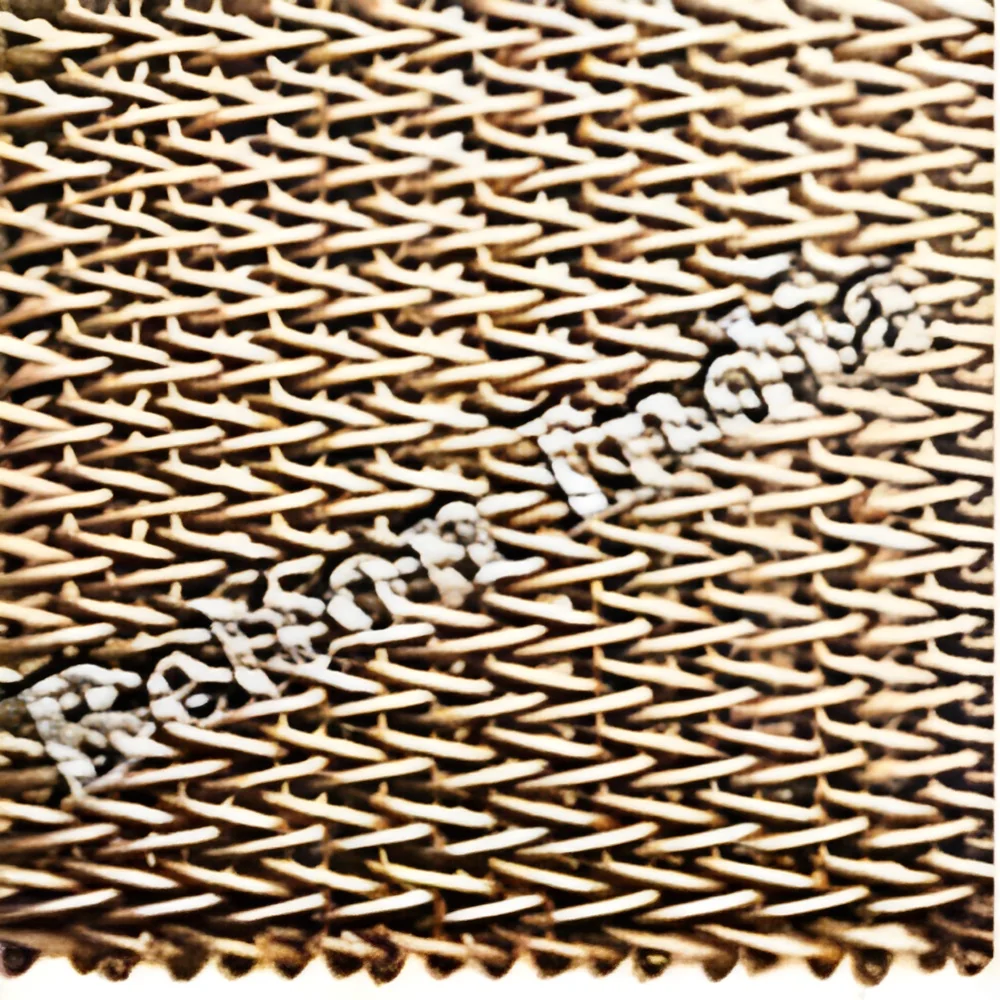
These conveyor belts serve critical functions across multiple food industry sectors including snack manufacturing, bakery operations, and ready-to-eat food production facilities. They are particularly valuable in namkeen making plants, chapati production units, papad manufacturing facilities, and comprehensive food processing systems involving frying, baking, or cooling processes. The hygiene-compliant design makes them suitable for direct food contact applications while maintaining operational efficiency in high-temperature environments and continuous production settings. Their versatility extends to packaging lines, sorting operations, and various food transfer applications where precision and reliability are essential for maintaining production quality and throughput.

The business value of these conveyor systems lies in their exceptional reliability and reduced total cost of ownership. The reinforced edge design with roller chains prevents stretching and misalignment, significantly extending operational life compared to conventional belts. This durability translates to fewer production interruptions, lower maintenance costs, and consistent output quality throughout extended service periods. The availability of multiple chain pitches and material options allows operations to select the perfect configuration for their specific machinery and process requirements, ensuring optimal performance and seamless integration into existing production lines while maximizing equipment utilization and minimizing downtime.

Key Features:
- Reinforced roller chain edges for enhanced durability and precise tracking
- Multiple chain pitch options including 3/8”, 1/2”, 5/8”, 3/4”, and 1”
- Choice between mild steel and stainless steel chain materials
- Thick rod reinforcement at precise intervals for structural integrity
- Food-grade compliant construction for safe direct food handling

Benefits:
- Extended service life with reduced maintenance requirements
- Superior stability and tracking precision in continuous operations
- Compatibility with existing machinery through multiple pitch options
- Resistance to high temperatures and rigorous washdown procedures
- Consistent performance meeting strict food safety standards
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our food grade conveyor belts with reinforced roller chain edges are engineered for demanding food processing environments where hygiene and durability are critical. The reinforced edges provide exceptional stability and precise tracking, making these belts ideal for continuous operation in high-temperature applications like frying, baking, and cooking systems. They maintain consistent performance while meeting strict food safety standards across various production settings.
These conveyor systems serve diverse food production sectors including snack manufacturing, ready-to-eat food processing, and bakery operations. Available in multiple chain pitches (3/8”, 1/2”, 5/8”, 3/4”, 1”) and material options (MS or SS chains), they ensure perfect compatibility with existing machinery. From namkeen and chapati production to papad frying and packaging operations, these belts handle various food products without contamination risk while withstanding rigorous daily use.
- Continuous frying systems for snack foods including namkeen, chips, and papads
- Automated chapati and roti production lines in commercial bakeries
- Food packaging and sorting operations requiring precise movement control
- High-temperature cooking and baking conveyor systems in food plants
- Food processing facilities requiring washdown-compatible equipment
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Belton India, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Food Grade Conveyor Belts With Reinforced Roller Chain Edges
Food grade conveyor belts with reinforced roller chain edges deliver exceptional durability for food processing, frying systems, and packaging lines. Available in multiple chain pitches and materials including stainless steel for reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Belton India
 Punjab, India
Industrial Equipment & MachineryManufacturer