IN
₹
Apparel & Fashion
Description
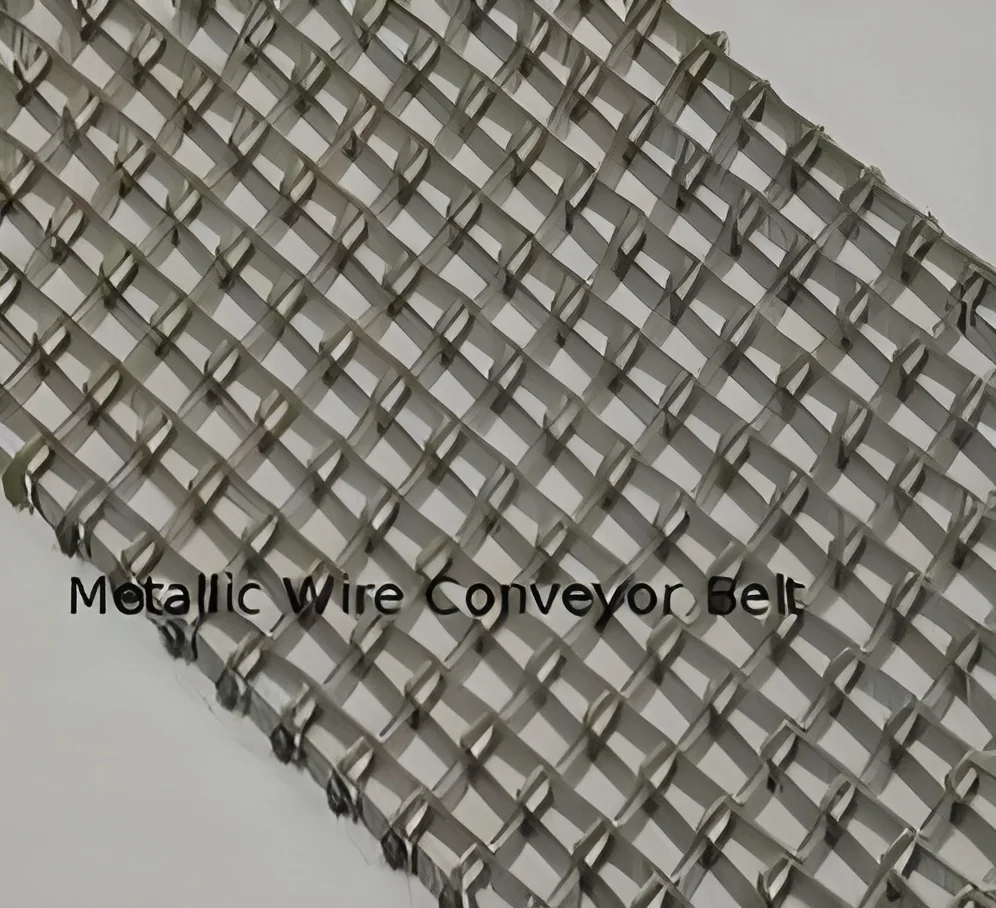
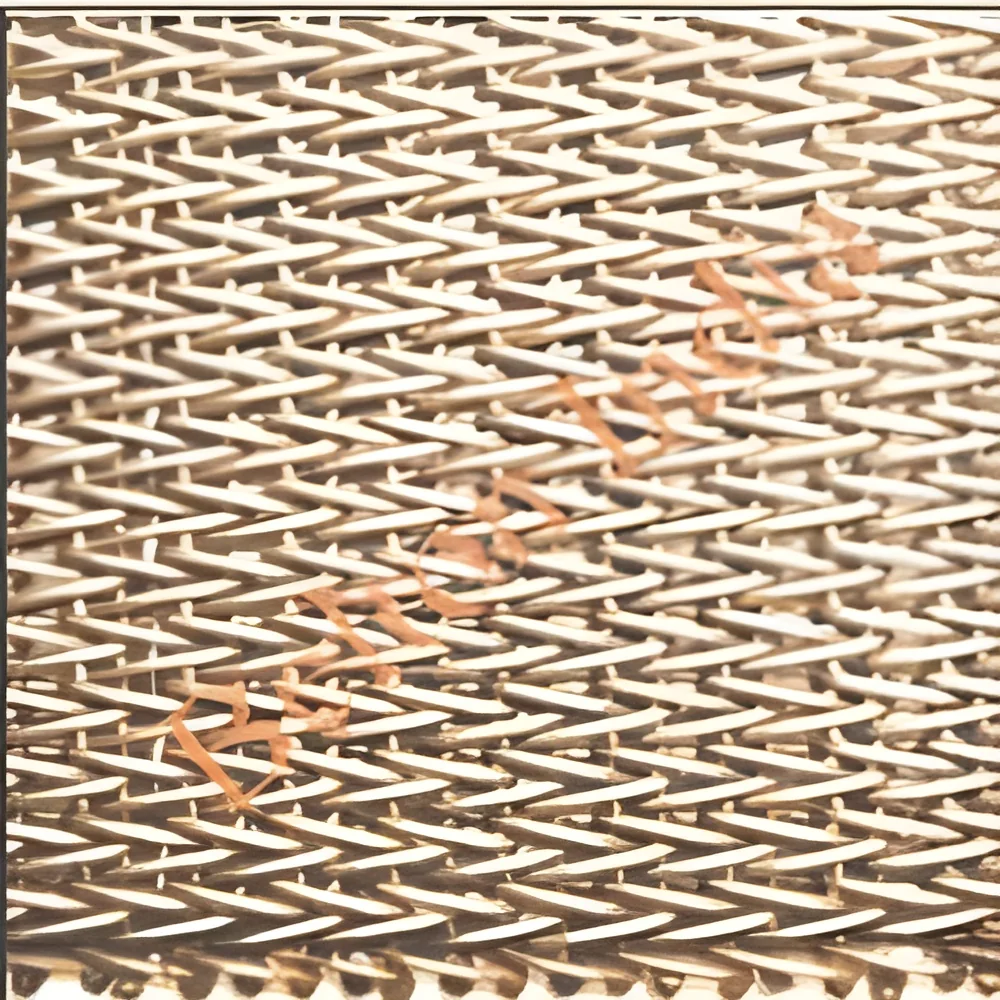
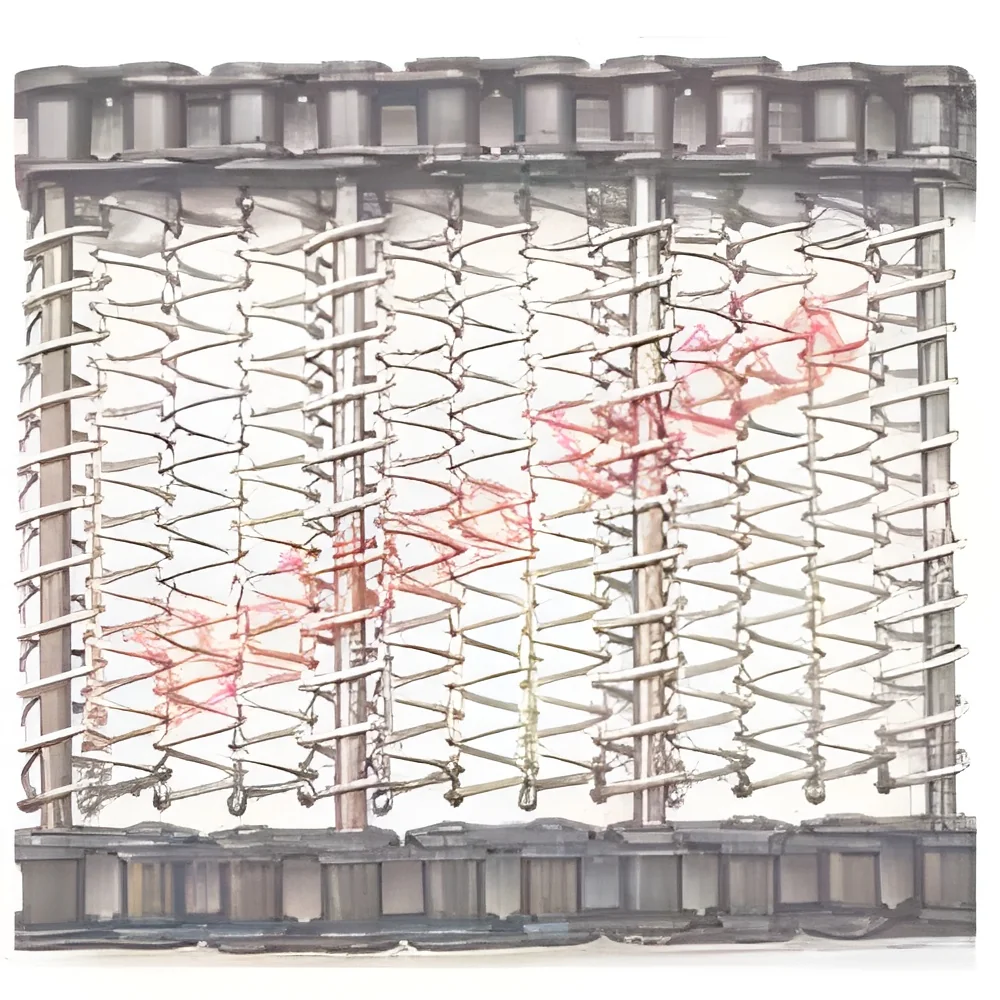
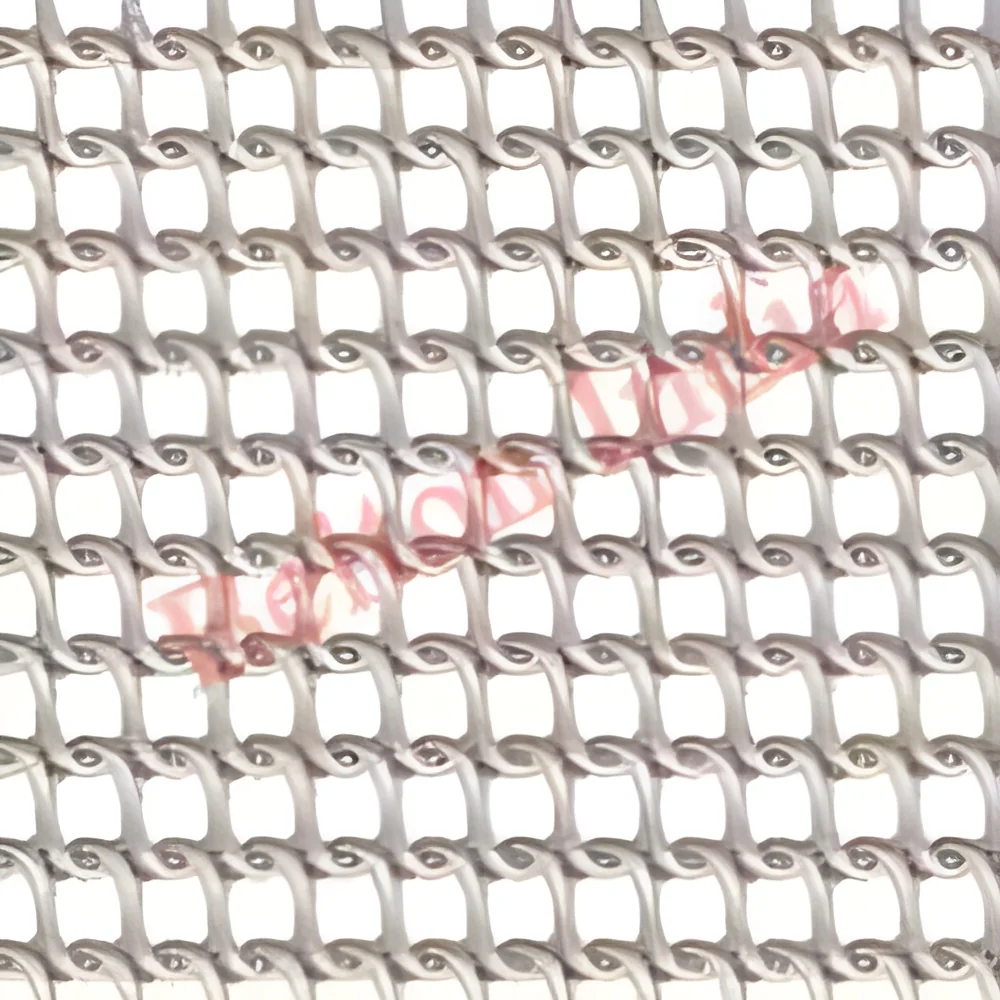
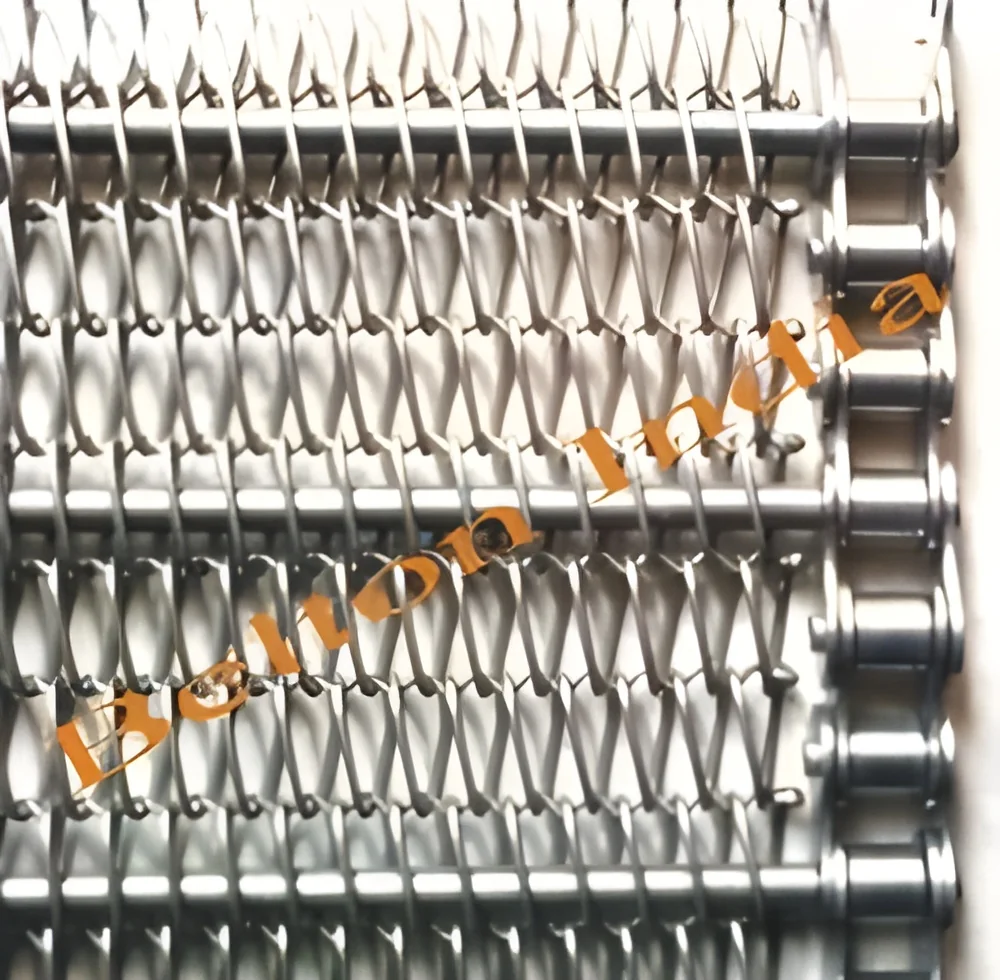
The Food Processing Horizontal Conveyor Belt is a robust, purpose-built system designed for the reliable and gentle horizontal transport of granular food products. It specializes in moving grains, cereals, and similar dry materials through processing and packaging lines with minimal spillage or damage. Engineered with a focus on modularity, this conveyor offers a practical and efficient solution for operations that require a consistent, dependable flow of materials. Its design prioritizes ease of integration, allowing it to connect various stages of production—from initial intake to final packaging—seamlessly. This ensures that your processing line maintains optimal efficiency, reducing manual handling and supporting automated workflows for improved productivity and product integrity.

This conveyor belt serves as a critical component in industries where handling dry, free-flowing materials is a daily operation. In food processing, it is indispensable for moving grains through sequenti...
The Food Processing Horizontal Conveyor Belt is a robust, purpose-built system designed for the reliable and gentle horizontal transport of granular food products. It specializes in moving grains, cereals, and similar dry materials through processing and packaging lines with minimal spillage or damage. Engineered with a focus on modularity, this conveyor offers a practical and efficient solution for operations that require a consistent, dependable flow of materials. Its design prioritizes ease of integration, allowing it to connect various stages of production—from initial intake to final packaging—seamlessly. This ensures that your processing line maintains optimal efficiency, reducing manual handling and supporting automated workflows for improved productivity and product integrity.

This conveyor belt serves as a critical component in industries where handling dry, free-flowing materials is a daily operation. In food processing, it is indispensable for moving grains through sequential stages like cleaning, dehulling, polishing, and sorting. Agricultural cooperatives and grain mills utilize it to transport harvests from receiving docks to drying beds or storage units. Within the packaging sector, it reliably feeds products into filling machines, cartoners, and palletizers. Its application extends to any facility managing bulk powders, seeds, or pellets, providing a hygienic and efficient transfer method that meets the stringent demands of food-grade material handling and general industrial use.

Investing in this horizontal conveyor belt translates to tangible business value through enhanced operational reliability and reduced long-term costs. Its durable construction and quality components minimize unplanned downtime and lower maintenance expenses, ensuring a steady return on investment. The system's gentle handling directly reduces product loss and waste, protecting your raw material investment. By streamlining material movement, it accelerates throughput and optimizes labor allocation. Furthermore, its modular and adaptable design future-proofs your operations, allowing for cost-effective scaling or reconfiguration as production needs evolve, making it a strategic asset for sustainable growth.

Key Features:
- Modular design enables straightforward customization of length and width to fit specific layout requirements.
- Engineered specifically for the horizontal conveyance of food grains, cereals, and other granular products.
- Constructed with durable materials for reliable, long-lasting performance in industrial environments.
- Designed for gentle handling to minimize product degradation, breakage, or dust generation during transport.
- Features a simple integration capability with existing production line equipment and control systems.

Benefits:
- Enhances production line efficiency by providing a consistent and automated flow of materials.
- Reduces operational costs by minimizing manual handling, product loss, and frequent maintenance needs.
- Improves product quality and safety through gentle transportation that prevents damage and contamination.
- Offers operational flexibility with a modular design that can be adapted or expanded as business needs change.
- Delivers reliable performance that decreases downtime, ensuring smoother and more predictable production schedules.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Horizontal conveyor belts provide the essential link in material handling systems, moving granular products like grains and cereals with consistent reliability. Their modular design integrates smoothly into existing production layouts, ensuring a steady flow of materials from one processing stage to the next. This reduces bottlenecks and supports continuous operation, which is vital for maintaining high throughput in demanding industrial environments.
These systems are engineered for versatility across sectors that handle dry, granular goods. The straightforward horizontal path minimizes product agitation and damage, preserving the quality of sensitive materials like food grains. With flexible sizing options for length and width, they can be configured to fit specific spatial constraints and capacity requirements, offering a practical solution for upgrading or expanding material flow without major infrastructure changes.
- Transporting raw grains and cereals between cleaning, sorting, and milling stations in food processing plants.
- Moving harvested crops like rice, wheat, and corn from intake points to storage silos in agricultural facilities.
- Conveying granular products through automated filling, weighing, and bagging lines in packaging operations.
- Handling bulk ingredients like flour, sugar, or seeds between production stages in manufacturing facilities.
- Facilitating efficient loading and unloading of sacks or containers in warehouse and distribution center logistics.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Belton India, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Food Processing Horizontal Conveyor Belt For Grains And Cereals
Food Processing Horizontal Conveyor Belt efficiently transports grains and cereals with modular reliability. Ideal for food processing, agriculture, and packaging industries seeking durable conveying solutions.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Belton India
 Punjab, India
Industrial Equipment & MachineryManufacturer