IN
₹
Apparel & Fashion
Description
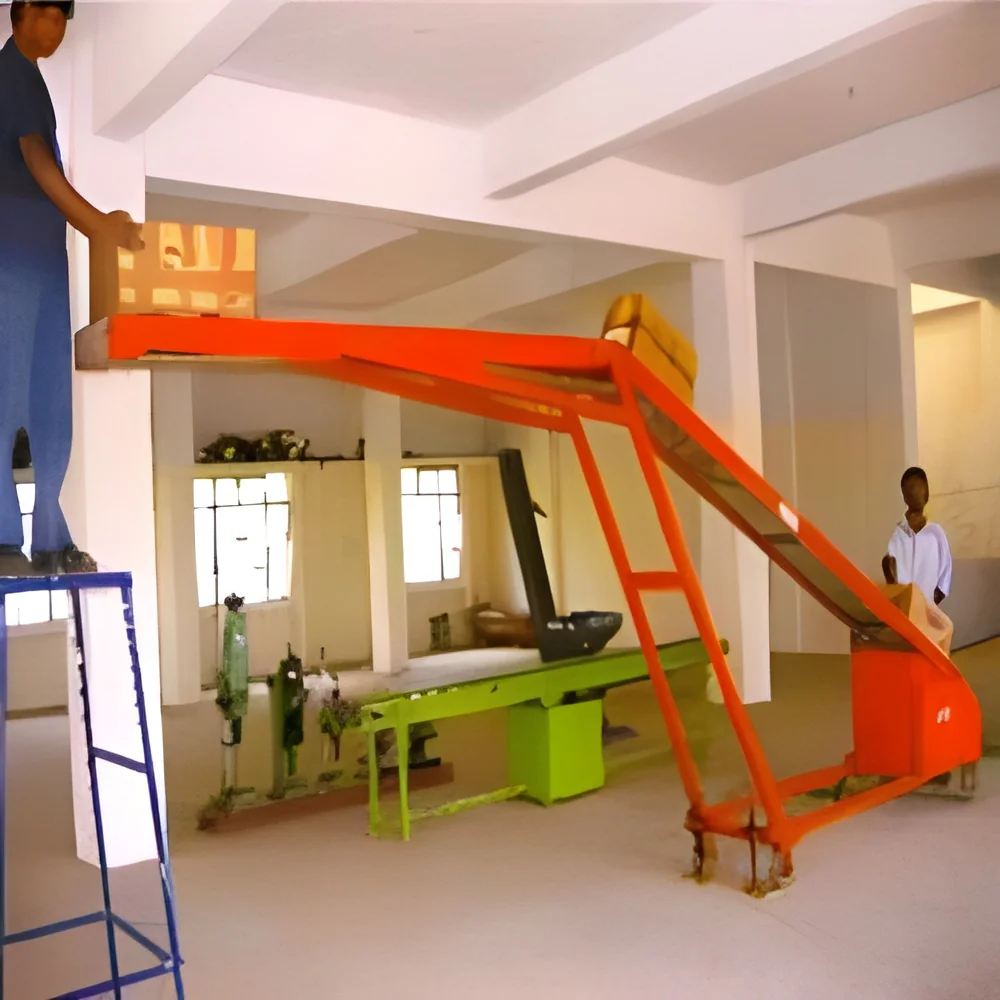
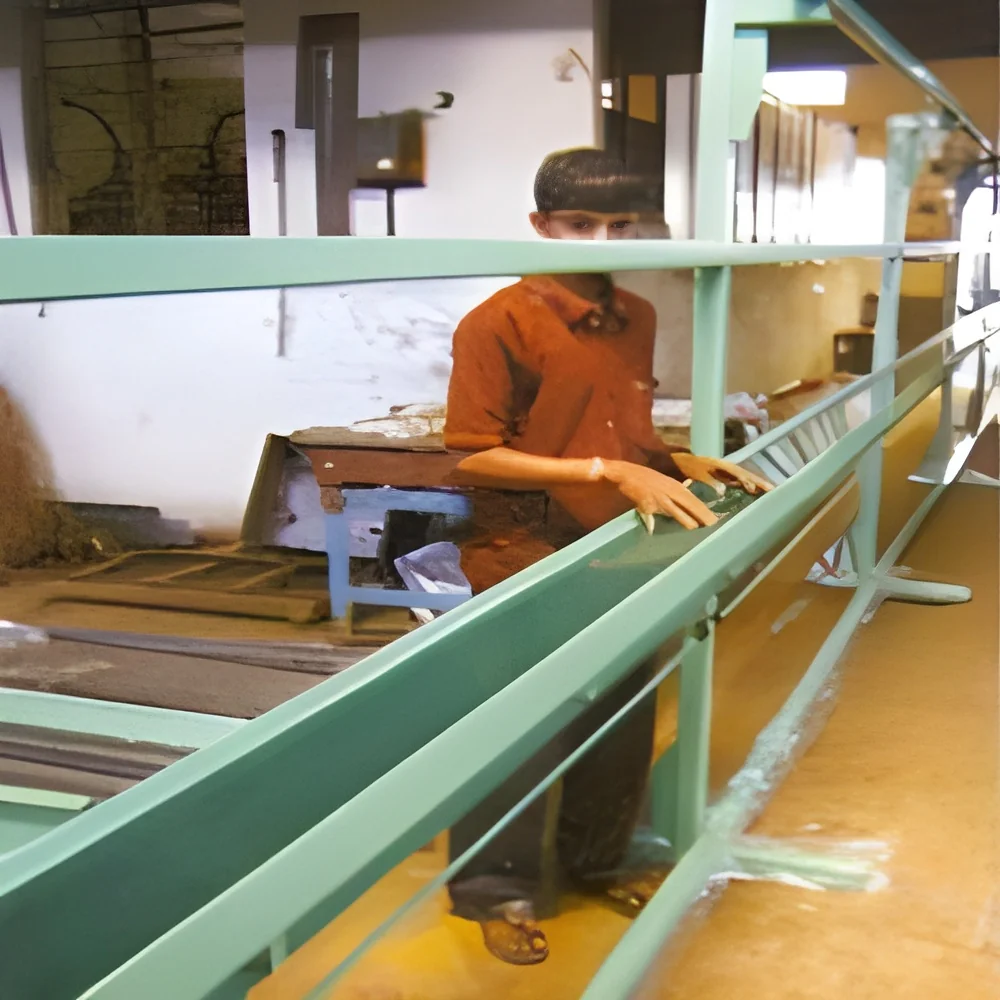
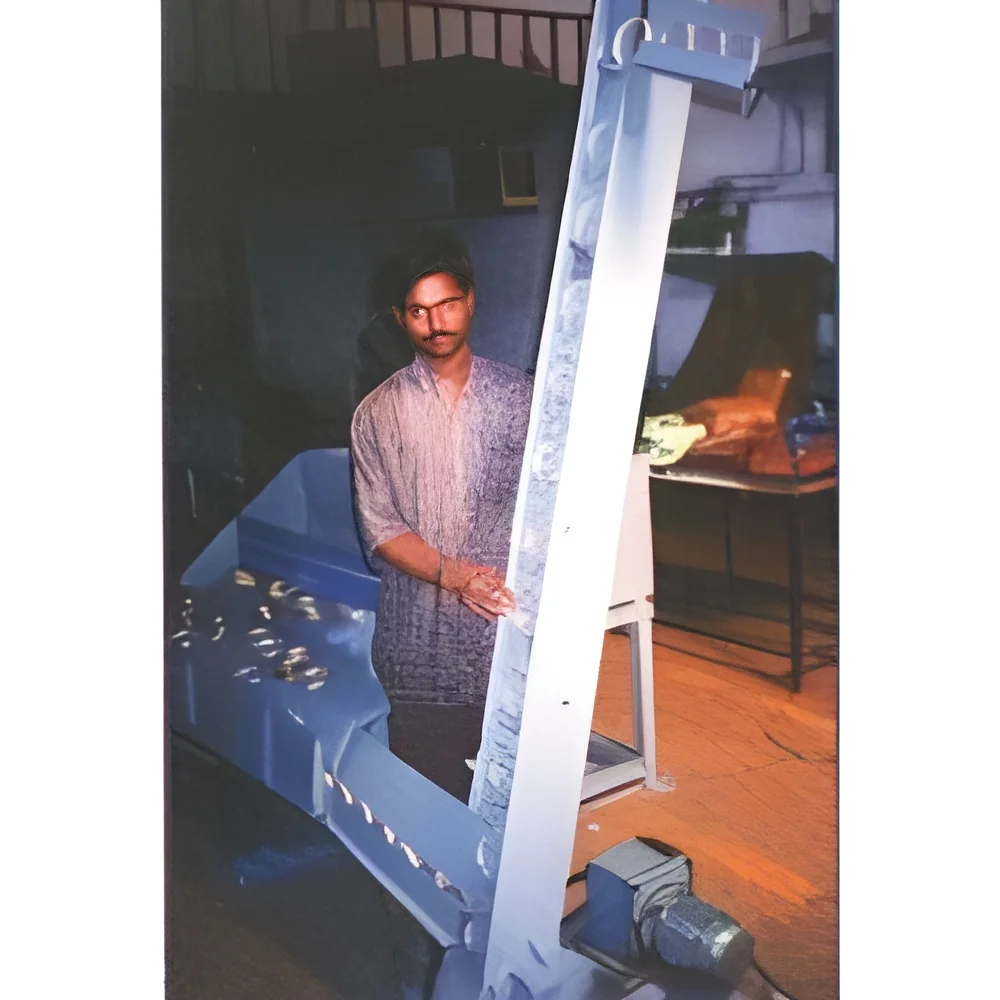
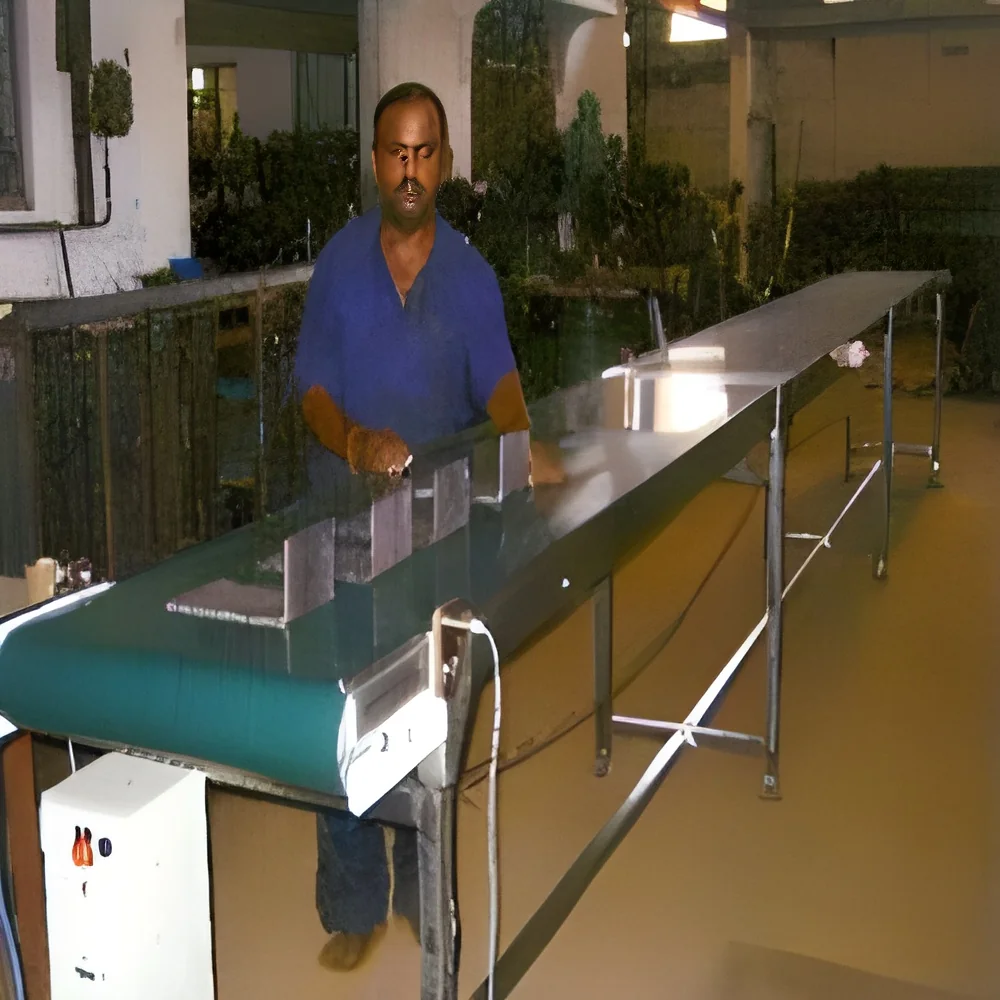
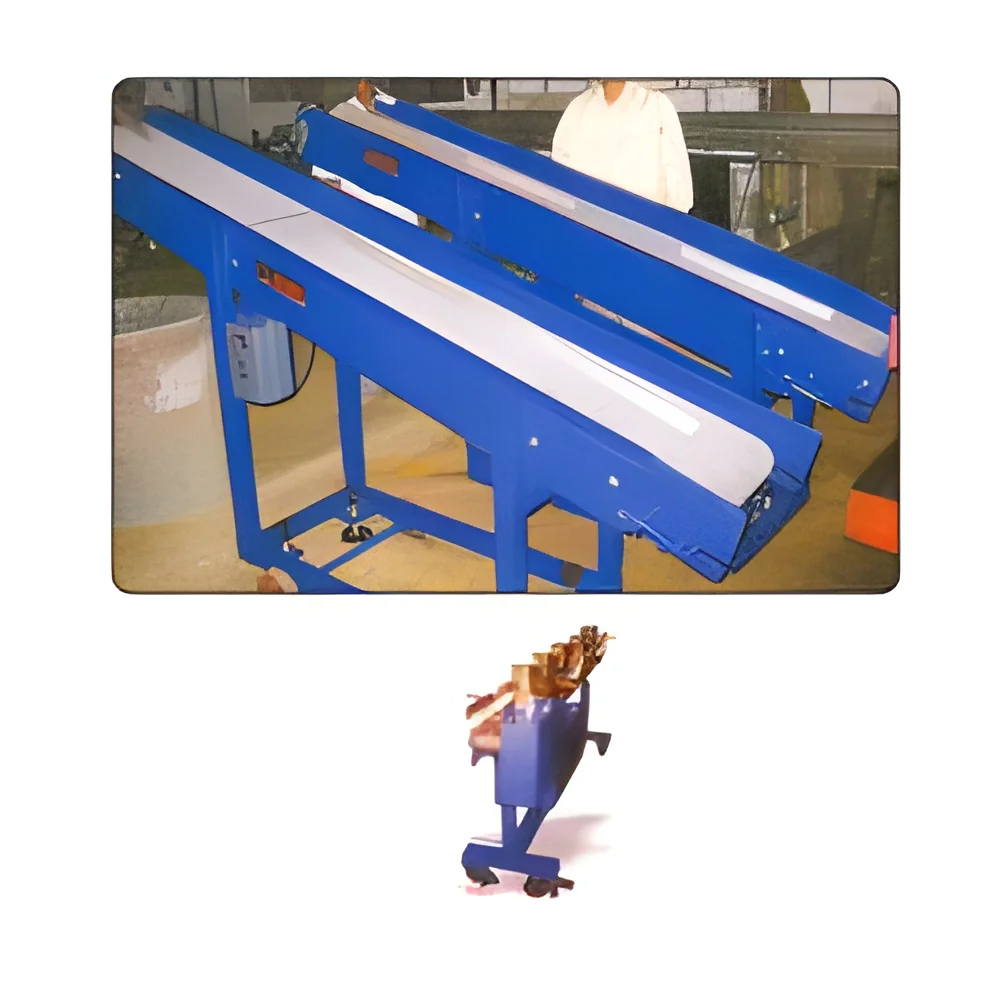
Our industrial automation infeed conveyors deliver reliable bulk material handling solutions for demanding operational environments. Engineered for consistent performance, these short-length transport systems provide dependable material input to primary production machinery, ensuring workflow continuity and operational efficiency. The conveyors feature robust construction capable of handling units of varying dimensions while maintaining precise flow control. Designed for flexibility, they operate effectively in both horizontal and inclined configurations, accommodating different installation requirements and spatial limitations across industrial settings.

These conveyor systems serve essential functions across multiple industrial sectors including mining operations, manufacturing facilities, metallurgy plants, and bulk processing centers. In mining applications, they efficiently feed raw materials into crushers and primary processing equipment. Manufacturing plants utilize them for ma...
Our industrial automation infeed conveyors deliver reliable bulk material handling solutions for demanding operational environments. Engineered for consistent performance, these short-length transport systems provide dependable material input to primary production machinery, ensuring workflow continuity and operational efficiency. The conveyors feature robust construction capable of handling units of varying dimensions while maintaining precise flow control. Designed for flexibility, they operate effectively in both horizontal and inclined configurations, accommodating different installation requirements and spatial limitations across industrial settings.

These conveyor systems serve essential functions across multiple industrial sectors including mining operations, manufacturing facilities, metallurgy plants, and bulk processing centers. In mining applications, they efficiently feed raw materials into crushers and primary processing equipment. Manufacturing plants utilize them for maintaining consistent material supply to assembly lines and production stations. The metallurgy industry employs these systems for handling ores and processed metals through various production stages. Their adaptability makes them suitable for food processing, packaging operations, and bulk material handling facilities where reliable material transport is crucial for maintaining production efficiency and output quality.

The business value of our infeed conveyors lies in their proven reliability, operational efficiency, and long-term durability. These systems significantly reduce manual handling requirements while ensuring consistent material supply to production lines, minimizing operational disruptions. Built with quality components and engineering excellence, they deliver minimal maintenance requirements and extended service life. This operational reliability translates directly to reduced downtime, increased production output, and improved return on investment for industrial operations seeking dependable material handling solutions that withstand demanding working conditions and deliver consistent performance over time.

Key Features:
- Short-length design optimized for space-efficient industrial installation
- Robust construction engineered for handling heavy bulk materials
- Customizable specifications to match specific operational requirements
- Compatibility with various production line equipment and systems
- Flexible operation in both horizontal and inclined positions

Benefits:
- Enhanced operational efficiency through consistent material flow
- Reduced manual handling requirements and labor costs
- Minimal maintenance needs with extended service life
- Improved production output with reliable performance
- Space-optimized design for flexible installation options
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial infeed conveyors automate material intake processes in production and processing facilities, efficiently transporting bulk materials like minerals, coal, and manufactured goods from loading points to primary equipment. They maintain consistent flow rates while handling various unit sizes and weights, ensuring uninterrupted operations across different industrial environments with diverse material requirements and spatial constraints.
These conveyor systems serve critical functions across heavy industries including mining operations, manufacturing plants, metallurgy facilities, and bulk processing centers. They integrate seamlessly with existing production equipment and can operate in both horizontal and inclined positions, providing operational flexibility for different installation scenarios and material handling needs while maintaining reliability and performance standards.
- Feeding raw materials into crushers and processing equipment in mining operations
- Supplying consistent material flow to assembly lines in manufacturing facilities
- Transporting coal and minerals to processing systems in power generation plants
- Moving bulk goods between production stages in food processing operations
- Loading and unloading materials in warehouse and distribution center operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Suresh Industries, Karnataka
 Karnataka, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial Automation Infeed Conveyors For Bulk Material Handling
Industrial Automation Infeed Conveyors for reliable bulk material handling. These short-length conveyors ensure consistent input to production lines in mining, manufacturing, and processing industries with robust construction and flexible operation.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Suresh Industries
 Karnataka, India
Manufacturer