IN
₹
Apparel & Fashion
Description
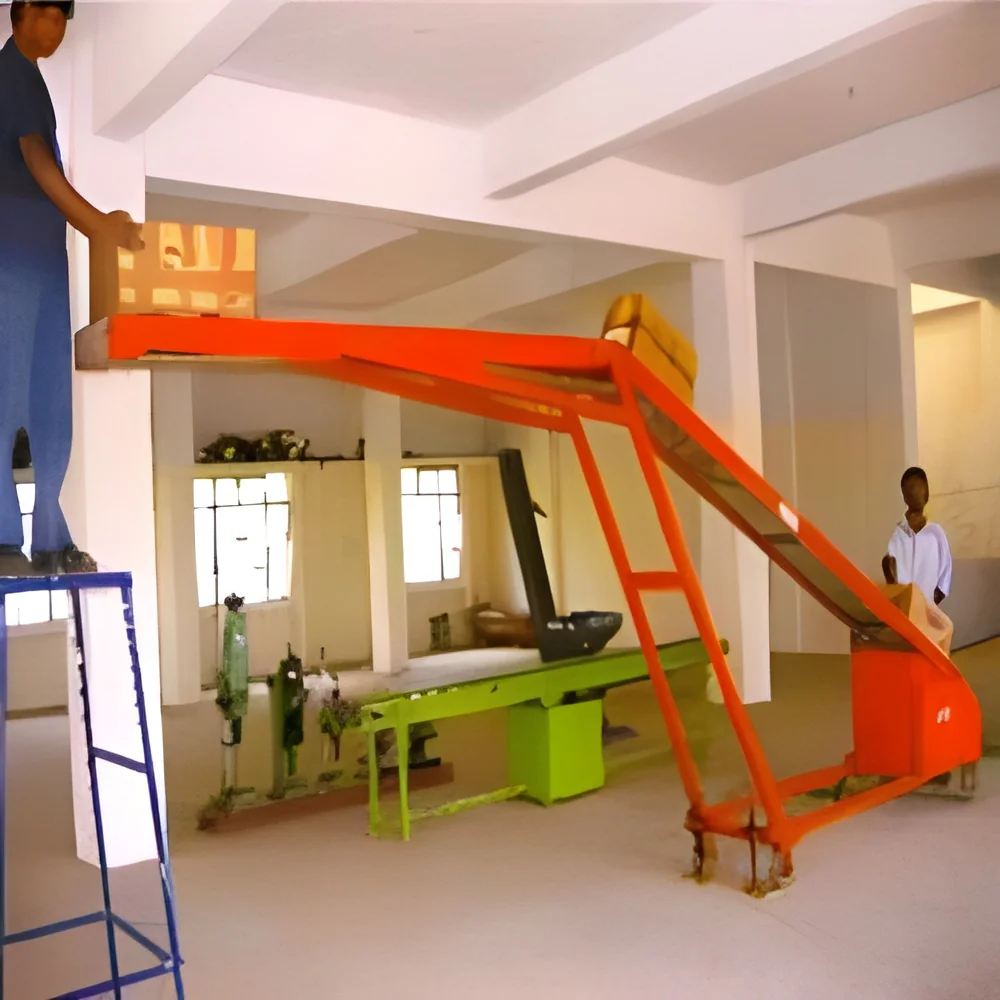
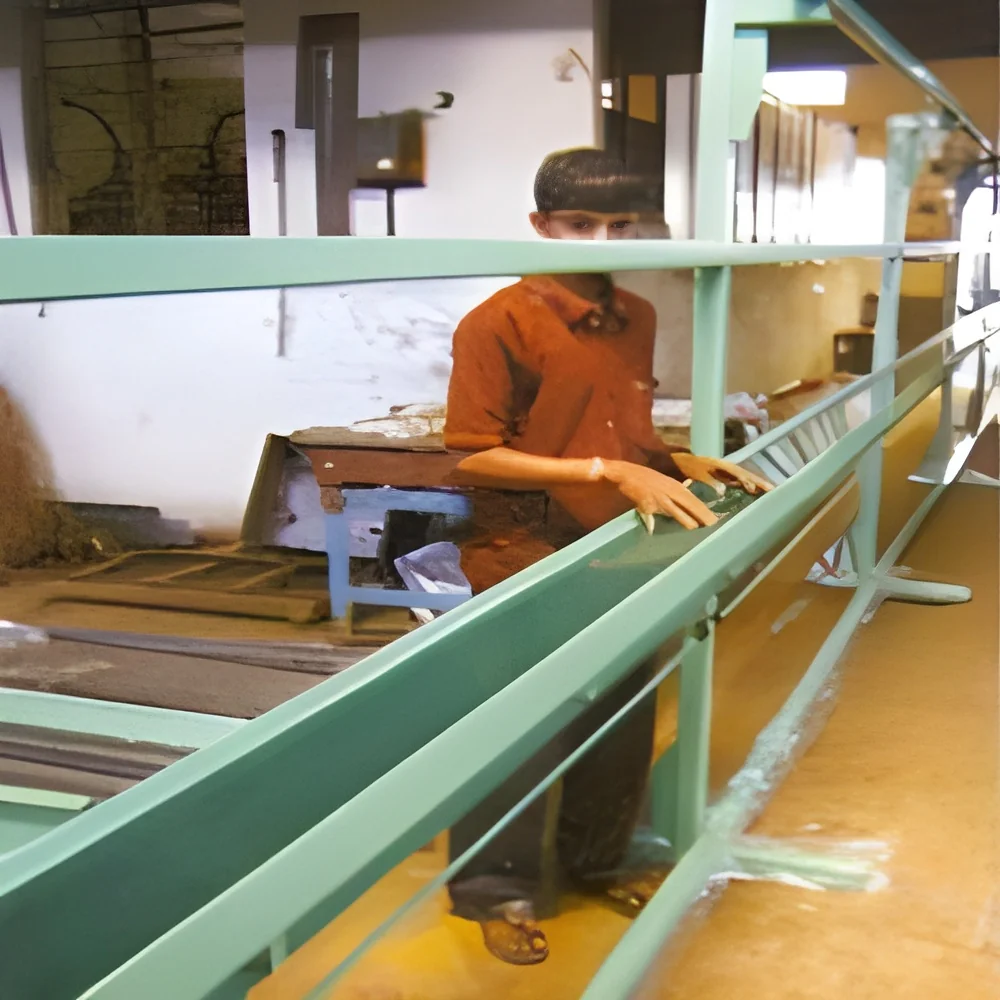
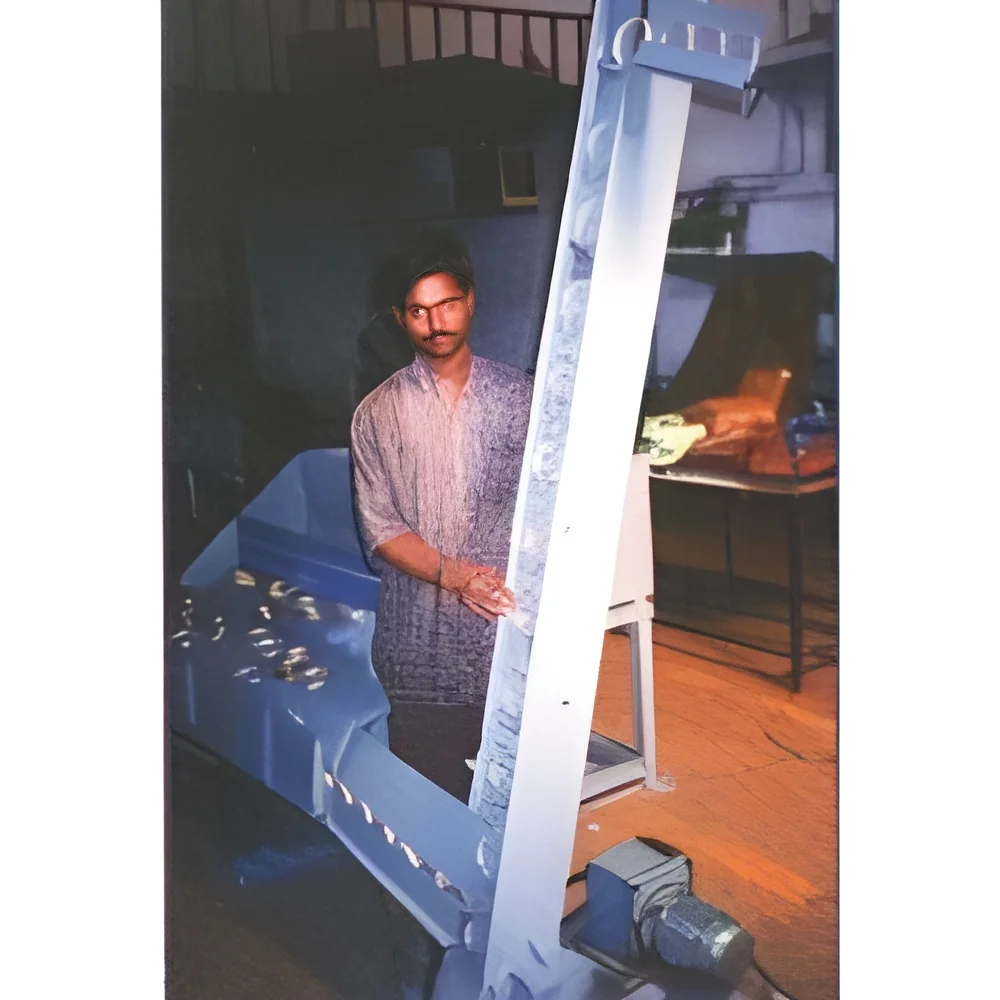
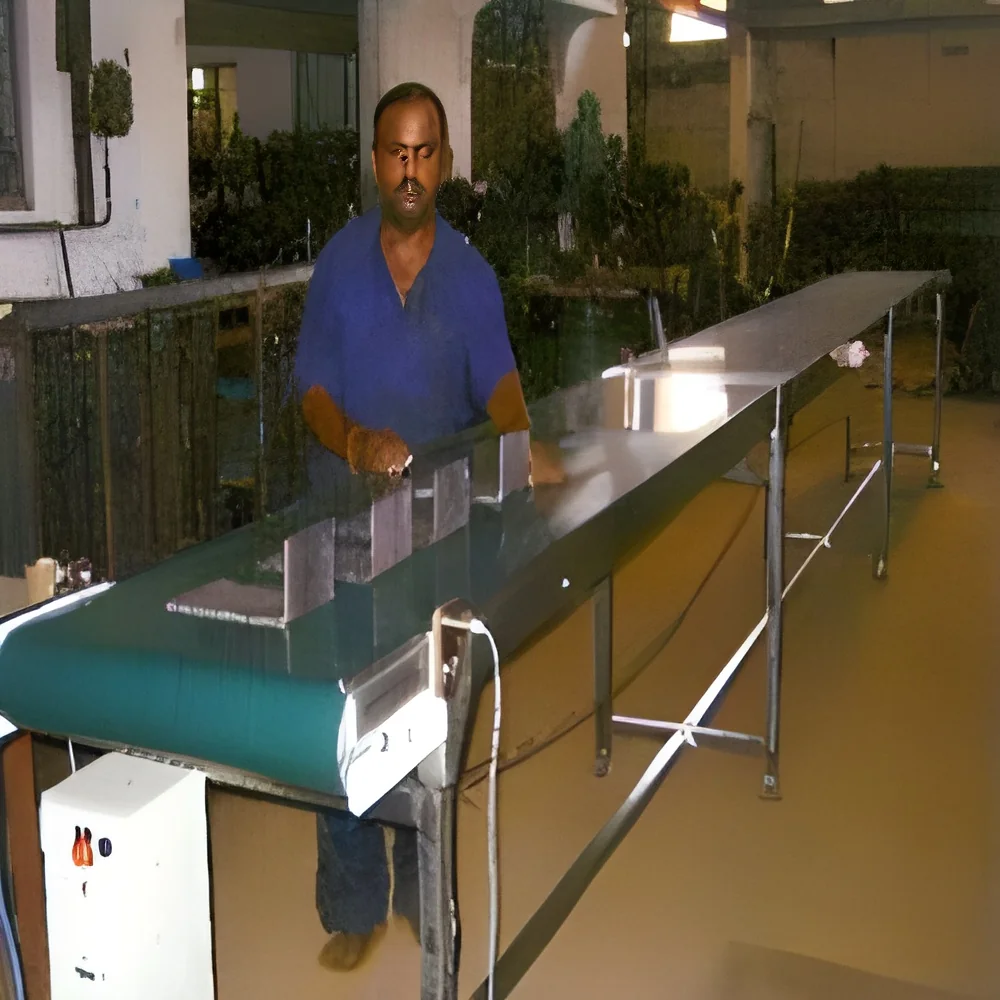
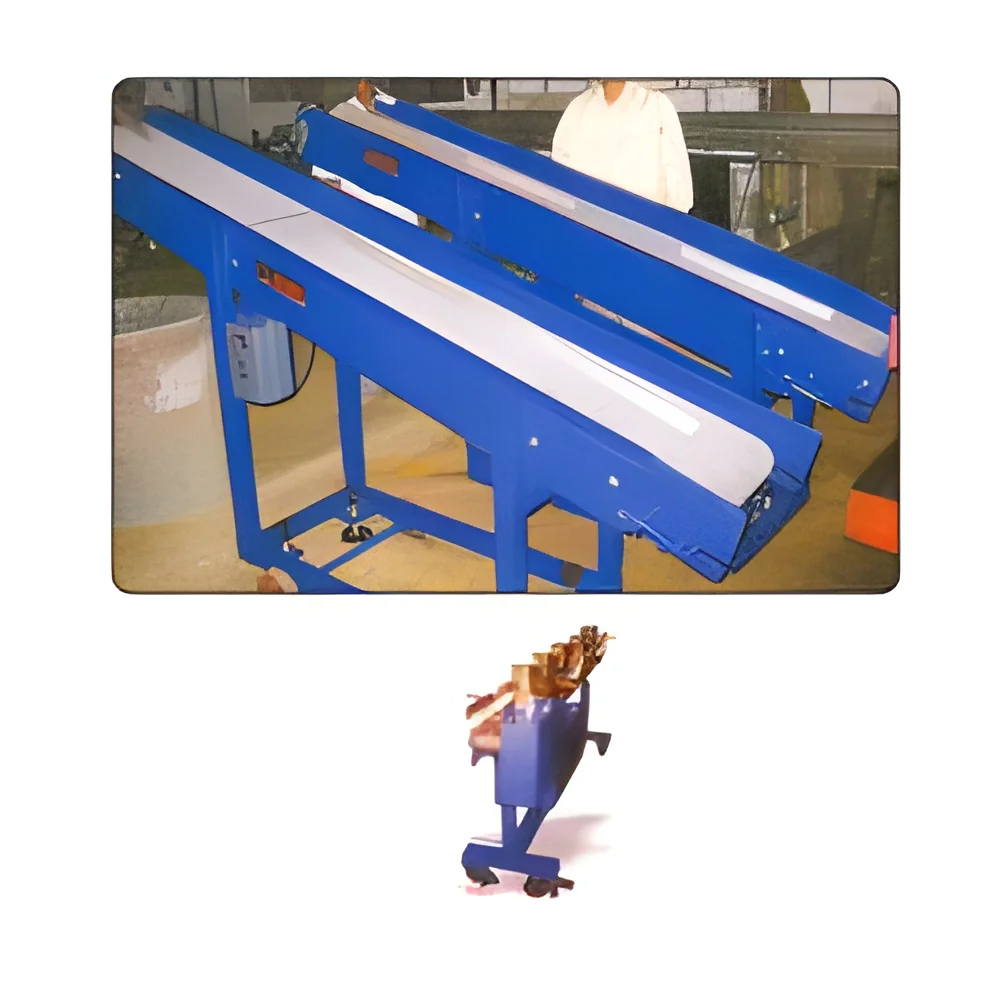
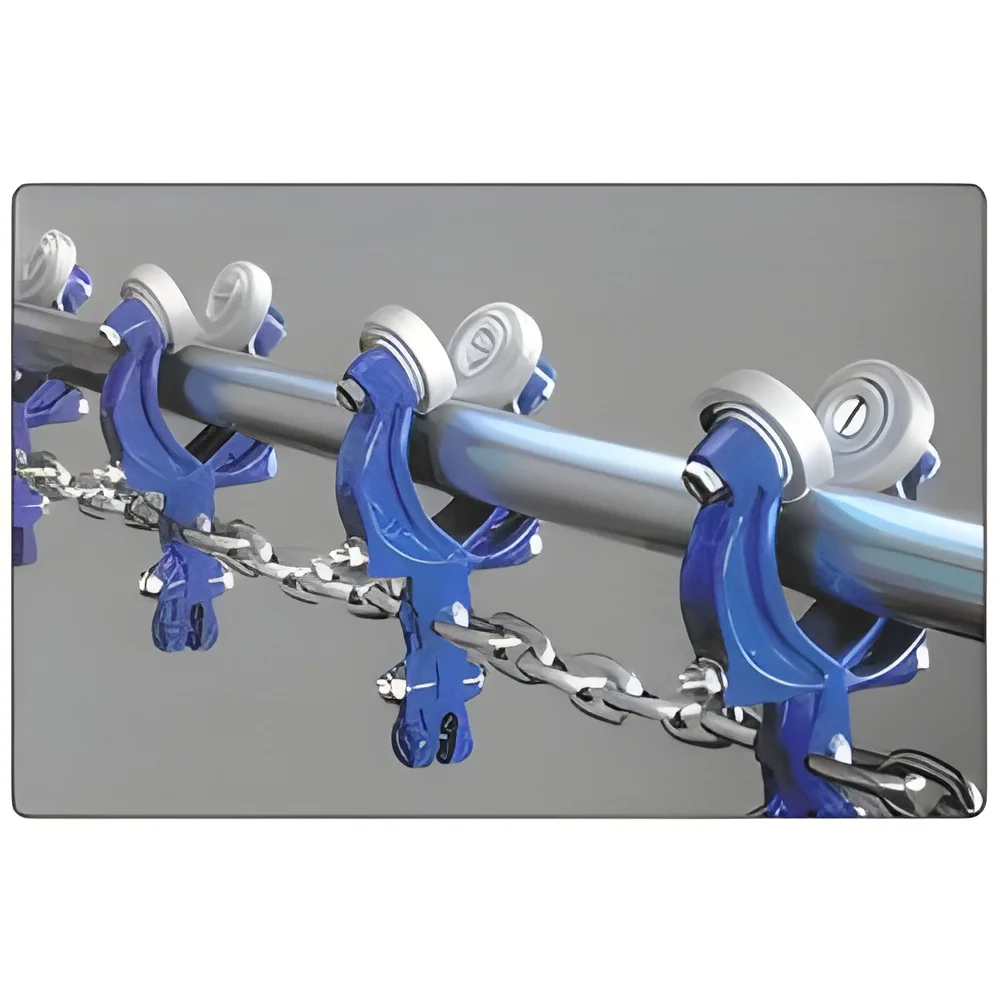
Our heavy-duty overhead conveyor systems represent engineering excellence in material handling technology, specifically designed for industrial environments where reliability and efficiency are paramount. These engineered systems transport bulk materials and heavy components through elevated pathways, optimizing floor space while maintaining continuous operational flow. Engineered with precision, these conveyors handle substantial loads starting from 100 kilograms and can be configured for horizontal or inclined operation based on specific process requirements. The systems offer flexibility through single or multiple transport line configurations and seamless integration with other material handling equipment, providing comprehensive logistics solutions for demanding industrial applications.

These overhead conveyors serve critical roles across multiple heavy industries including mining operations, metallurgy plants, and coal processing facilities. In mining, they efficiently move extr...
Our heavy-duty overhead conveyor systems represent engineering excellence in material handling technology, specifically designed for industrial environments where reliability and efficiency are paramount. These engineered systems transport bulk materials and heavy components through elevated pathways, optimizing floor space while maintaining continuous operational flow. Engineered with precision, these conveyors handle substantial loads starting from 100 kilograms and can be configured for horizontal or inclined operation based on specific process requirements. The systems offer flexibility through single or multiple transport line configurations and seamless integration with other material handling equipment, providing comprehensive logistics solutions for demanding industrial applications.

These overhead conveyors serve critical roles across multiple heavy industries including mining operations, metallurgy plants, and coal processing facilities. In mining, they efficiently move extracted materials between processing stages while conserving valuable floor space. Metallurgy plants utilize them for transporting metal components through heat treatment and finishing processes where traditional conveyors cannot operate. Coal handling facilities benefit from their ability to transfer materials between processing and storage areas reliably. The systems also find applications in automotive manufacturing and large-scale warehouse operations where overhead material movement enhances operational efficiency.

The value of our overhead conveyor systems lies in their exceptional reliability, engineering capabilities, and long-term operational efficiency. These systems reduce floor space requirements while increasing material handling capacity, directly impacting operational costs and productivity. Their robust construction ensures minimal downtime and maintenance requirements, providing consistent performance in the most demanding industrial environments. The systems are designed to meet specific operational needs, ensuring optimal integration with existing processes and equipment. This combination of reliability and efficiency makes our overhead conveyors a strategic investment for businesses looking to enhance their material handling capabilities.

Key Features:
- Heavy-duty construction for demanding industrial environments
- Horizontal and incline configuration flexibility
- Load capacity from 100 kilograms upwards
- Single or multiple transport line options
- Integration compatibility with material handling equipment

Benefits:
- Optimized floor space utilization in facilities
- Continuous material flow throughout operations
- Reduced operational costs through efficiency
- Minimal downtime and maintenance requirements
- Enhanced productivity in material handling processes
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These heavy-duty overhead conveyor systems provide efficient material transport solutions where floor space optimization is critical. They move bulk materials through production facilities with precision, adapting to both horizontal and inclined pathways while maximizing usable floor space and maintaining continuous material flow throughout industrial processes.
Engineered for demanding environments where traditional floor conveyors cannot operate effectively, these systems handle heavy loads from 100 kilograms upwards. They can be configured as single or multiple transport lines according to production needs and integrate seamlessly with other material handling equipment, creating comprehensive logistics solutions for large-scale industrial operations.
- Mining operations for transporting ore and extracted materials between processing stages
- Metallurgy plants moving metal components through heat treatment and finishing processes
- Coal handling facilities for efficient transfer between processing and storage areas
- Automotive manufacturing plants for moving large components between assembly stations
- Warehouse operations for overhead sorting and transportation of heavy goods
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Suresh Industries, Karnataka
 Karnataka, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Heavy Duty Overhead Conveyors For Mining, Metallurgy, And Coal Industries
Heavy duty overhead conveyors for mining, metallurgy, and coal industries handle loads from 100kg+ with horizontal or incline configurations for reliable material transport in demanding industrial environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Suresh Industries
 Karnataka, India
Manufacturer