IN
₹
Apparel & Fashion
Description
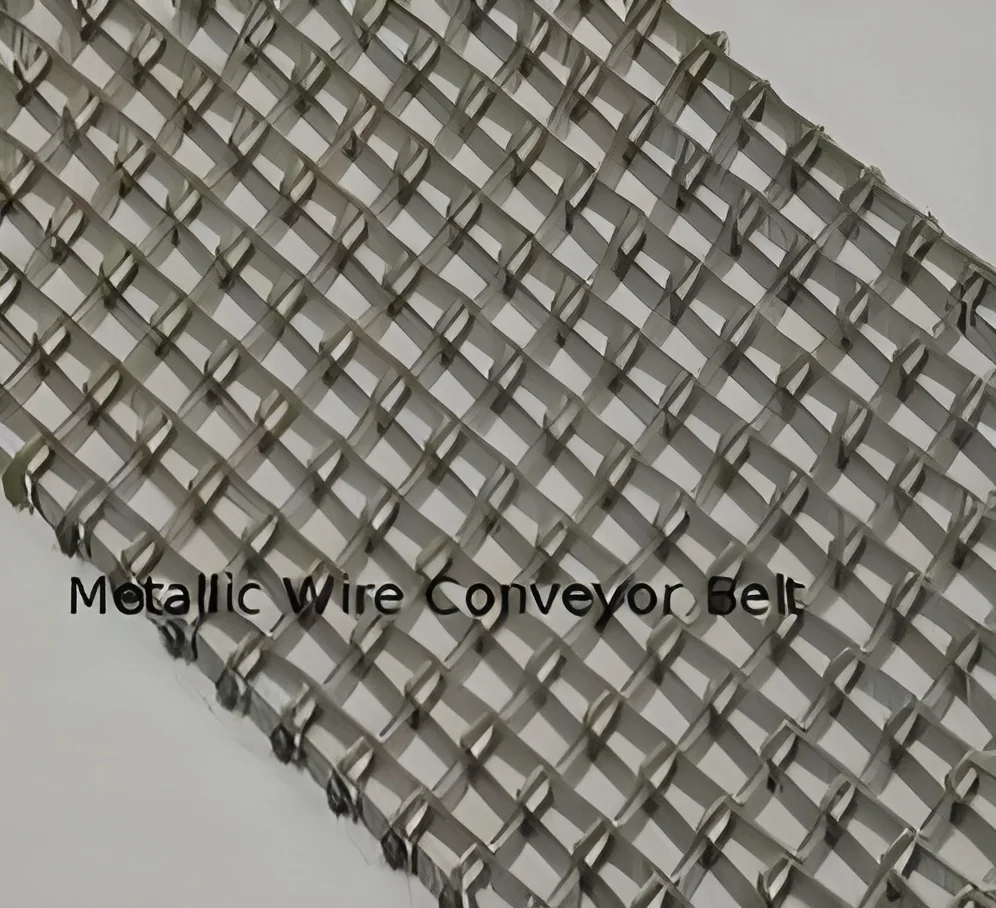
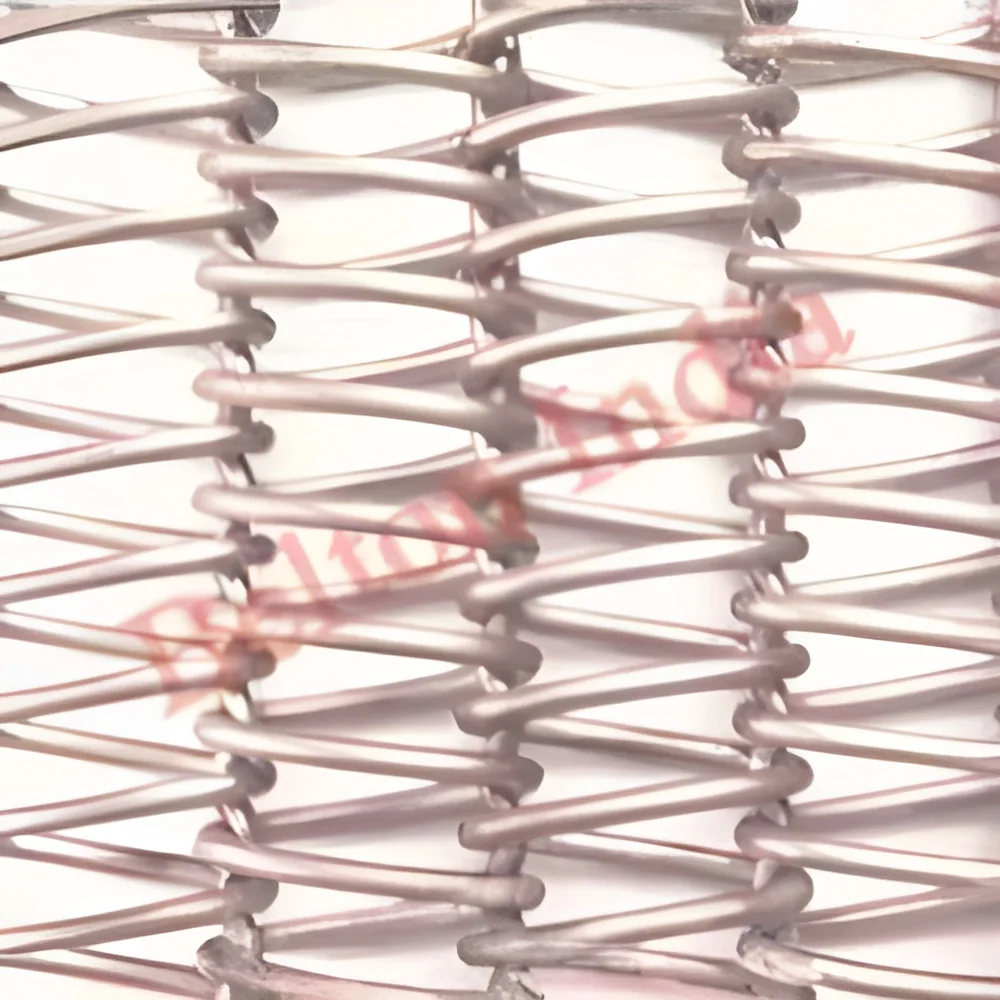
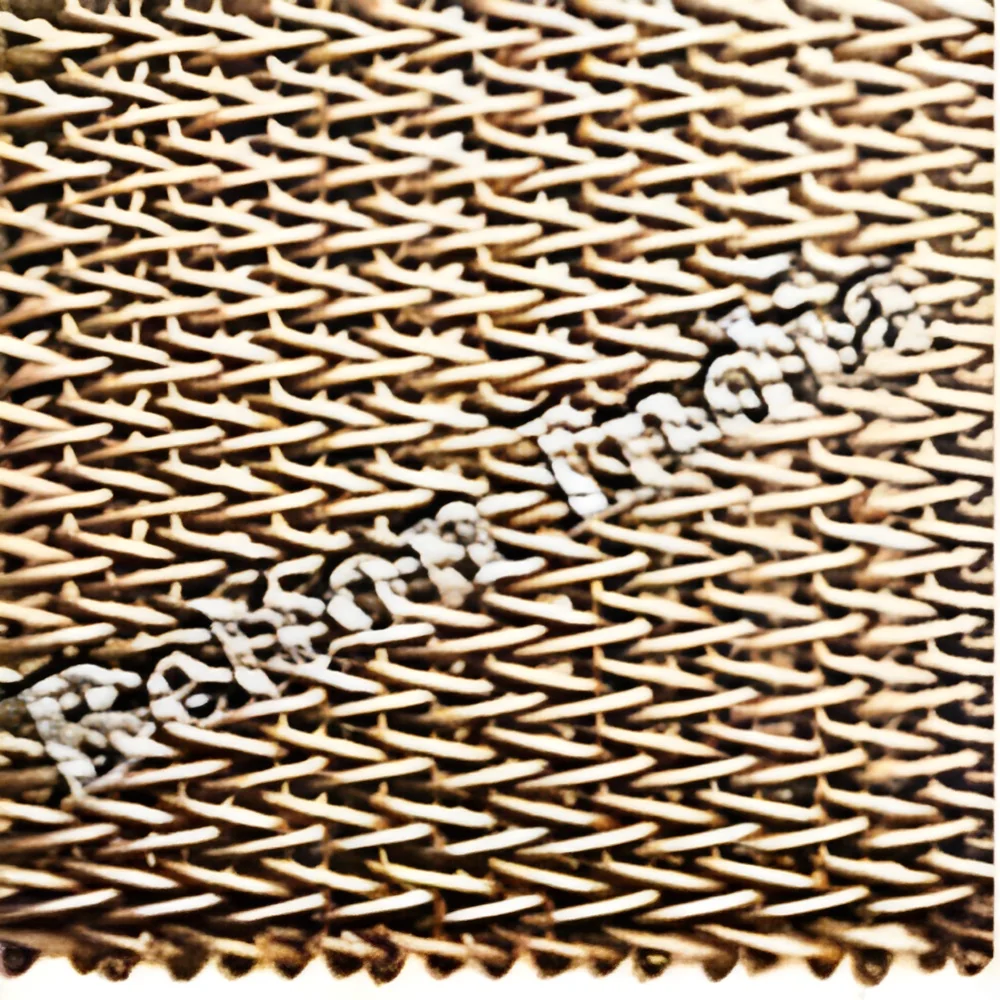
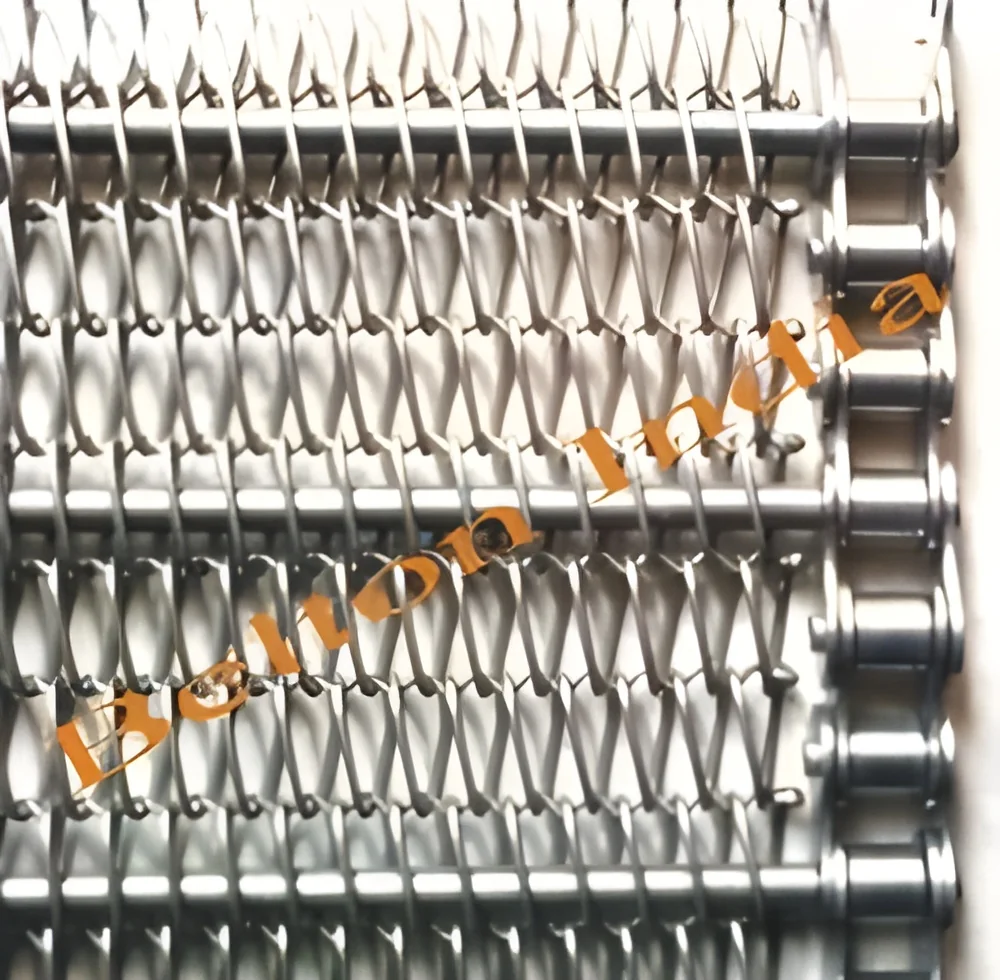
Industrial chain conveyors represent heavy-duty automation solutions engineered for reliable material transportation across demanding production environments. These systems utilize robust chain mechanisms to move products continuously along predetermined paths, handling significant loads while maintaining consistent operation. Designed with durability as a core principle, they withstand the rigors of continuous industrial use while adhering to strict quality standards. Their construction accommodates various operational requirements through customizable sizing and material selections, including stainless steel for corrosive environments and mild steel for general applications, ensuring optimal performance tailored to specific facility layouts and processing needs.

These conveyor systems serve critical roles across multiple industrial sectors due to their versatility and reliability. In food processing facilities, they enable hygienic transportation of products through washing, cooking...
Industrial chain conveyors represent heavy-duty automation solutions engineered for reliable material transportation across demanding production environments. These systems utilize robust chain mechanisms to move products continuously along predetermined paths, handling significant loads while maintaining consistent operation. Designed with durability as a core principle, they withstand the rigors of continuous industrial use while adhering to strict quality standards. Their construction accommodates various operational requirements through customizable sizing and material selections, including stainless steel for corrosive environments and mild steel for general applications, ensuring optimal performance tailored to specific facility layouts and processing needs.

These conveyor systems serve critical roles across multiple industrial sectors due to their versatility and reliability. In food processing facilities, they enable hygienic transportation of products through washing, cooking, and packaging stages while meeting sanitation standards. Footwear manufacturers utilize them to move components through assembly lines, maintaining consistent workflow from cutting to finishing operations. Glass industry applications include careful handling of fragile sheets during cutting, tempering, and inspection processes, where stable transport prevents damage and ensures product quality. Additional sectors like automotive manufacturing and logistics rely on these conveyors for moving parts between workstations and facilitating efficient sorting operations in distribution centers.

The business value of chain conveyors lies in their ability to enhance operational efficiency while reducing labor costs and minimizing production interruptions. Their heavy-duty construction ensures long-term reliability, decreasing maintenance requirements and associated downtime. Customization capabilities allow businesses to optimize floor space utilization and process flow, leading to more streamlined operations and improved productivity. By automating material movement, these systems enhance workplace safety through reduced manual handling while increasing overall throughput capacity. This combination of reliability, adaptability, and performance makes them a strategic investment for companies seeking to scale production capabilities, maintain consistent output quality, and strengthen competitive positioning in their markets.

Key Features:
- Heavy-duty chain mechanism designed for continuous operation under high loads
- Customizable dimensions and configurations to match specific layout requirements
- Multiple material options including stainless steel and mild steel constructions
- Engineered for demanding industrial environments with strict quality compliance
- Robust design ensuring durability and long service life in production settings

Benefits:
- Enhanced operational efficiency through automated material handling
- Reduced labor costs by minimizing manual transportation requirements
- Decreased downtime due to reliable performance and durable construction
- Improved workplace safety through reduced manual handling of products
- Increased production throughput with consistent and continuous operation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Chain conveyors deliver robust material handling for high-volume production lines, ensuring continuous product flow through assembly, processing, and packaging stages. Their durable construction and smooth operation minimize downtime, making them essential for maintaining efficiency in fast-paced industrial settings where consistent throughput is critical for meeting production targets and operational deadlines.
These systems are designed to adapt to diverse industry needs, with configurations suitable for handling everything from delicate food items to heavy glass panels. Their flexibility in layout integration allows seamless addition to existing workflows, supporting various load capacities and environmental conditions while ensuring reliable performance across multiple shifts and demanding applications.
- Transporting packaged food products through sorting, sealing, and palletizing stages in processing facilities.
- Moving footwear components between stitching, assembly, and quality checkpoints in manufacturing plants.
- Safely conveying glass sheets through cutting, washing, and tempering processes in glass production units.
- Automating part movement between workstations in automotive component assembly lines.
- Facilitating product accumulation and distribution in warehouse sorting and logistics operations.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Belton India, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Chain Conveyors For Food Footwear Glass Automation
Industrial chain conveyors for automation in food, footwear, and glass manufacturing. Engineered for reliability, heavy-duty performance, and quality compliance in demanding production environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Belton India
 Punjab, India
Industrial Equipment & MachineryManufacturer