IN
₹
Apparel & Fashion
Description
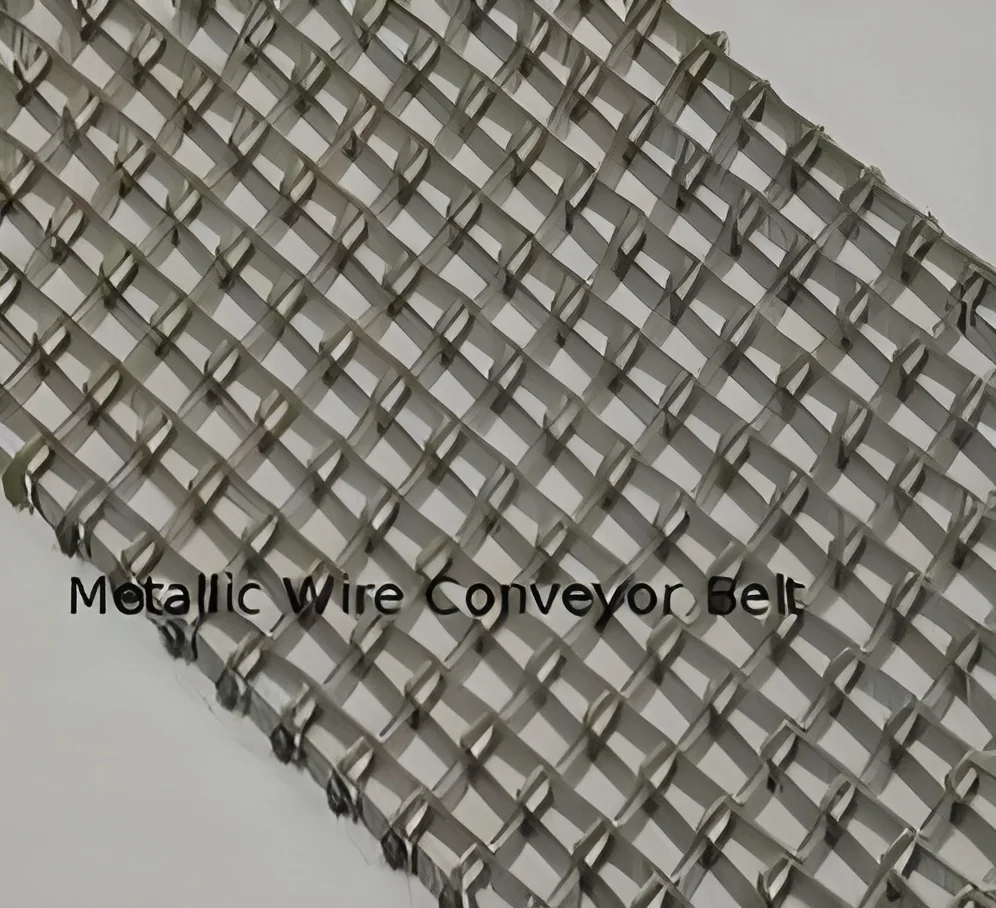
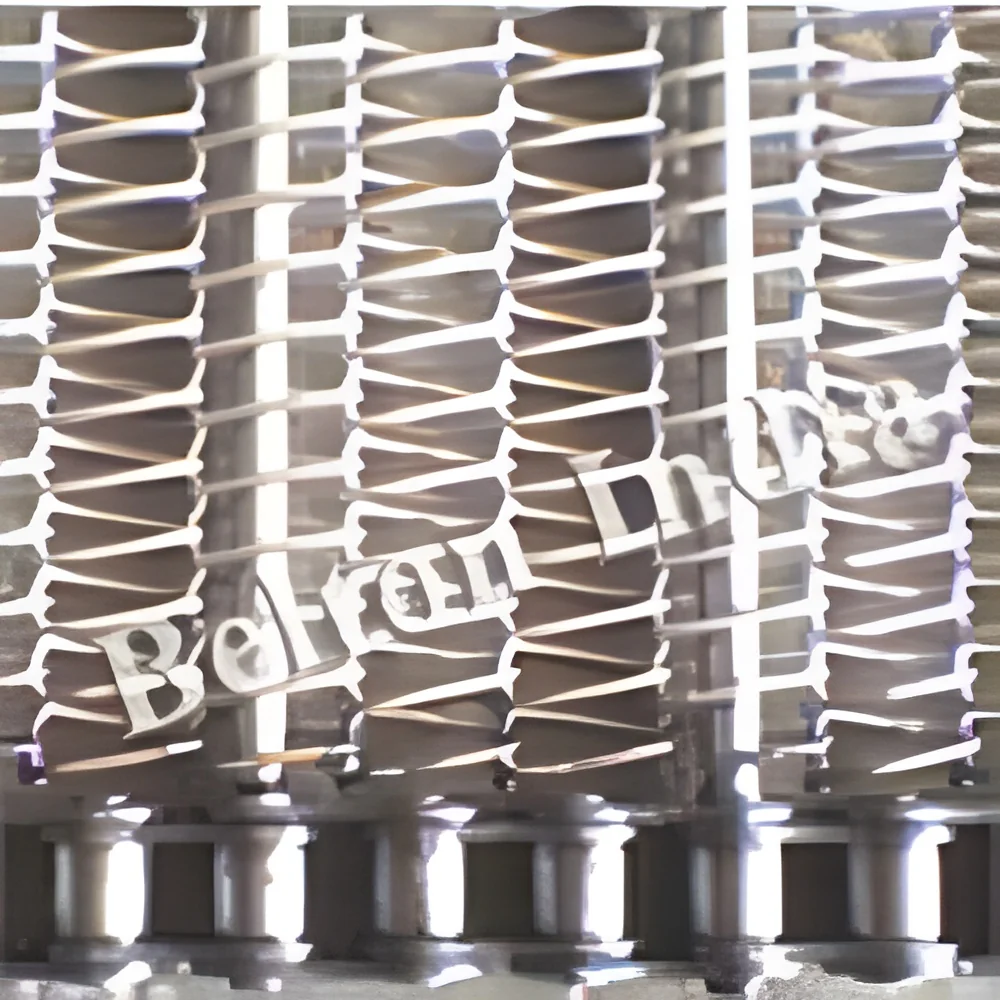
Our heavy-duty chain conveyor belts represent a cornerstone of efficient industrial bulk material handling. Engineered specifically for reliability and endurance, these systems are built to transport substantial loads across extended distances within manufacturing plants, processing facilities, and logistics hubs. They utilize a robust chain-driven mechanism that provides superior traction and load-bearing capacity compared to standard belt systems, ensuring consistent movement of pallets, containers, raw materials, and finished goods. The focus is on creating a seamless link in your operational workflow, minimizing interruptions and maximizing the flow of materials from one point to the next. This design is the result of understanding the rigorous demands of industrial environments where equipment failure is not an option.

These conveyor systems find essential usage across a broad spectrum of heavy industries. In automotive manufacturing, they form the backbone of assembly lines, mov...
Our heavy-duty chain conveyor belts represent a cornerstone of efficient industrial bulk material handling. Engineered specifically for reliability and endurance, these systems are built to transport substantial loads across extended distances within manufacturing plants, processing facilities, and logistics hubs. They utilize a robust chain-driven mechanism that provides superior traction and load-bearing capacity compared to standard belt systems, ensuring consistent movement of pallets, containers, raw materials, and finished goods. The focus is on creating a seamless link in your operational workflow, minimizing interruptions and maximizing the flow of materials from one point to the next. This design is the result of understanding the rigorous demands of industrial environments where equipment failure is not an option.

These conveyor systems find essential usage across a broad spectrum of heavy industries. In automotive manufacturing, they form the backbone of assembly lines, moving heavy vehicle frames and large components between workstations. Within the food processing sector, specific configurations handle the movement of bulk ingredients and packaged products, often in environments requiring strict hygiene. The mining and construction industries deploy them for transporting heavy, abrasive materials like ores and aggregates. Logistics and large-scale warehousing operations utilize these conveyors for sorting and transferring heavy palletized goods, enabling efficient order fulfillment and distribution. Their fundamental role is to provide a reliable, mechanical solution for material transfer where volume, weight, or operational tempo makes manual or lighter-duty methods impractical.

Investing in these heavy-duty chain conveyors delivers tangible business value through enhanced operational reliability and reduced long-term costs. Their durable construction, using high-grade materials and components, ensures an extended service life even under constant, heavy use, directly lowering total cost of ownership by reducing replacement frequency. The inherent reliability minimizes unplanned downtime, protecting production schedules and output targets. By automating the movement of heavy or bulky items, they significantly decrease reliance on manual labor, reducing associated costs and improving workplace safety by minimizing physical strain and forklift traffic. Their design facilitates smooth integration into both new and existing material handling layouts, providing a scalable solution that grows with your operational needs without requiring complete system overhauls.

Key Features:
- Constructed with heavy-duty industrial-grade chains and components for maximum load capacity and longevity
- Engineered for continuous operation in demanding environments with minimal performance degradation
- Designed to handle bulk materials, palletized goods, and heavy components with stability and precision
- Features a robust drive system and frame construction to withstand high stress and impact loads
- Offers reliable performance with consistent speed and traction for seamless material flow

Benefits:
- Ensures high operational uptime and reliability, critical for meeting production and distribution schedules
- Reduces long-term operational costs through durability, lower maintenance needs, and decreased manual handling
- Enhances workplace safety by automating the movement of heavy loads and reducing forklift dependency
- Provides a scalable and integrable solution that supports business growth and process optimization
- Delivers consistent, efficient material transfer, improving overall workflow productivity and throughput
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These heavy-duty chain conveyor belts are designed for continuous, high-capacity material transport in demanding industrial environments. They excel at moving bulk goods, raw materials, and packaged products across production floors, warehouses, and processing facilities with consistent reliability. Their robust construction handles significant weight and volume, making them indispensable for operations where uptime and throughput are critical.
Industries from automotive manufacturing to mining rely on these systems for their strength and adaptability. They integrate seamlessly into existing production lines for assembly, sorting, and distribution tasks. The design prioritizes smooth operation under heavy loads, reducing product damage and manual handling while maintaining a steady flow of materials through various stages of processing and logistics.
- Automotive assembly lines for transporting engine blocks, chassis components, and finished vehicles
- Food and beverage plants for moving bulk ingredients, bottled products, and packaged goods on pallets
- Mining and aggregate operations for hauling extracted ores, coal, and crushed materials
- Large-scale warehouse and distribution centers for sorting and moving heavy parcels and containers
- Manufacturing facilities for transferring raw materials between processing stations and storage areas
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Belton India, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Heavy Duty Chain Conveyor Belts For Industrial Bulk Material Handling
Heavy Duty Chain Conveyor Belts for industrial bulk material handling. Engineered for durability and reliability in manufacturing, food processing, and logistics applications. Features robust construction for seamless high-load operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Belton India
 Punjab, India
Industrial Equipment & MachineryManufacturer