IN
₹
Apparel & Fashion
Description
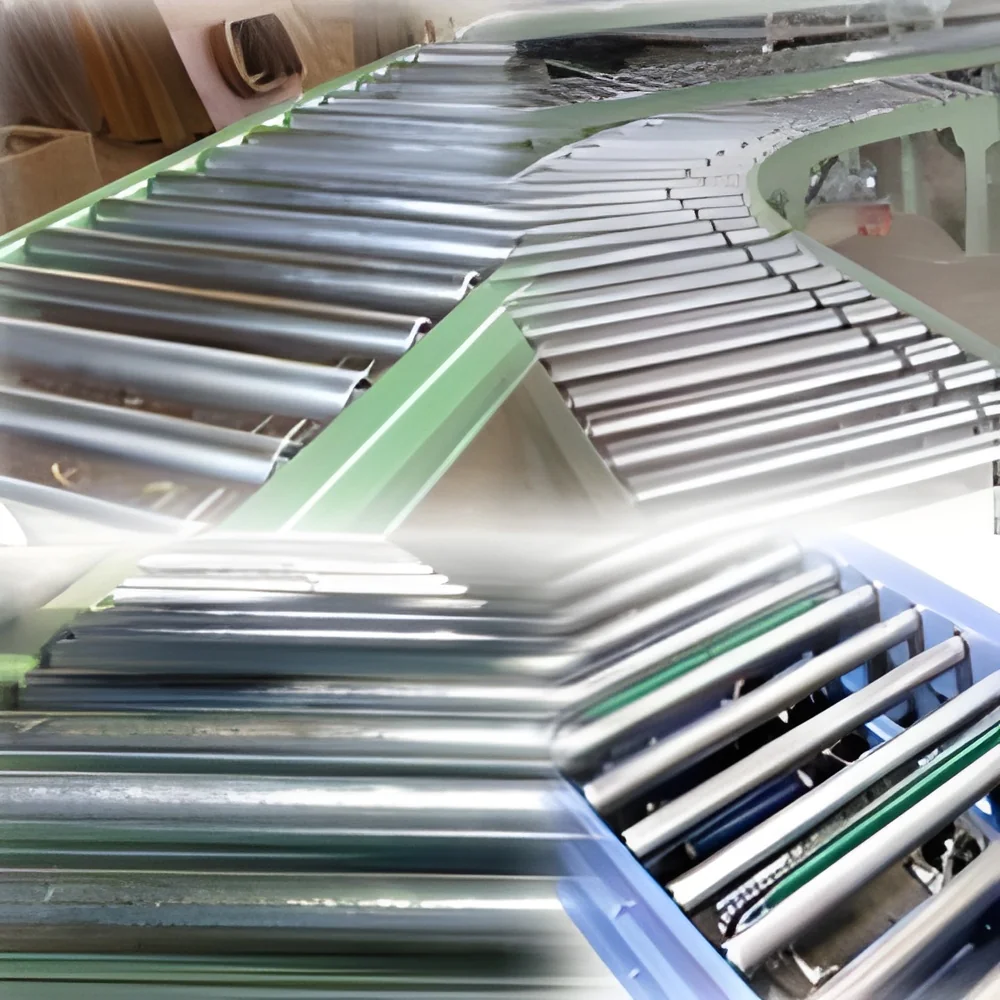
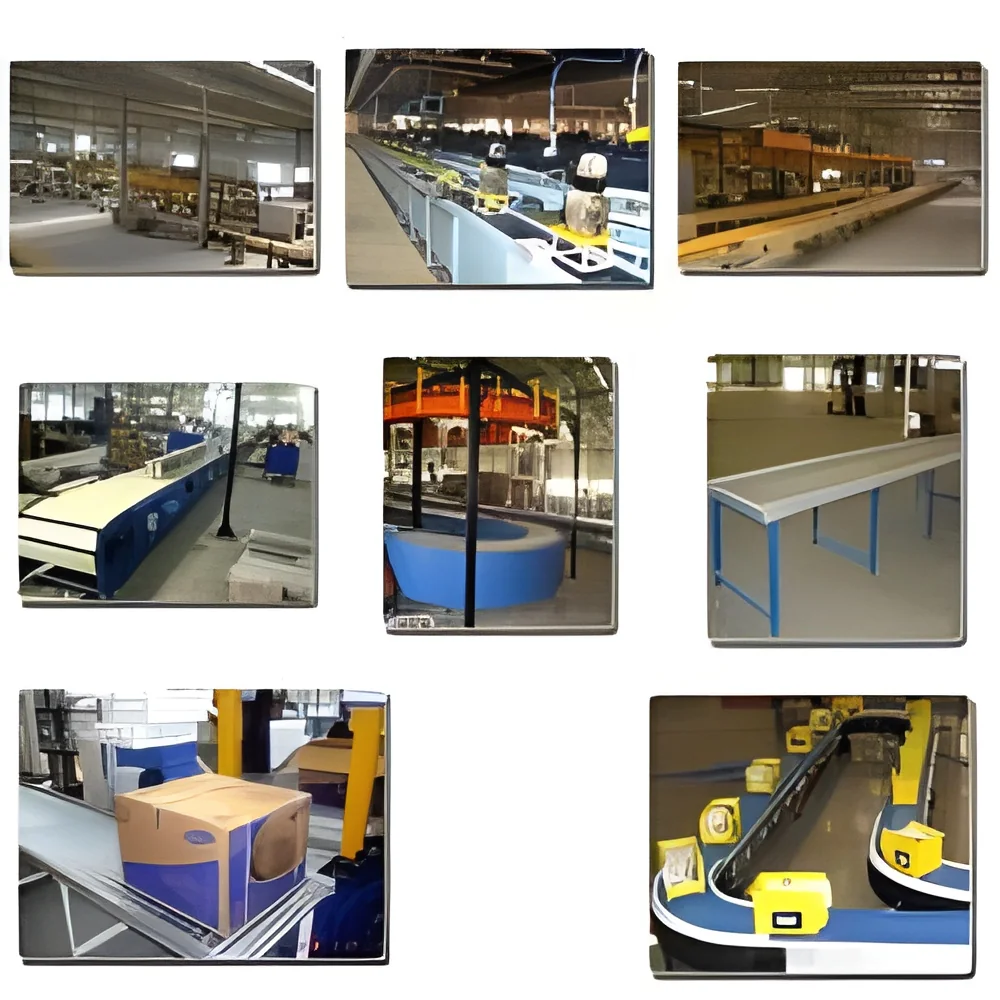
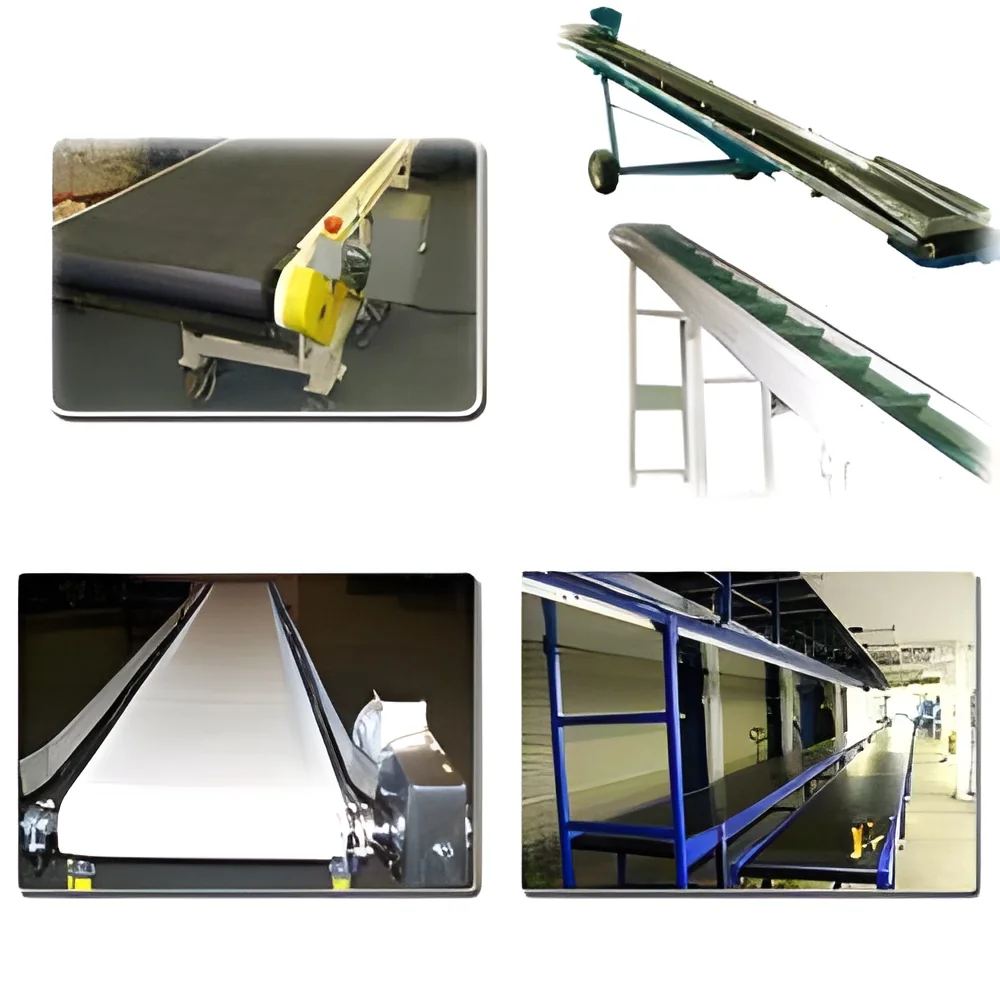
Our industrial belt conveyors are precision-engineered systems designed for reliable and efficient material transport in demanding operational environments. Built with high-grade materials and advanced drive mechanisms, they offer durable performance for continuous heavy-duty applications. The product range includes versatile flat belt, portable, and inclined/declined models, each constructed for low power consumption and minimal maintenance. This focus on robust engineering and operational simplicity provides a cost-effective backbone for material handling, ensuring smooth, uninterrupted movement of goods to support your productivity goals.

These conveyor systems are integral to a wide spectrum of industries, including manufacturing, mining, agriculture, logistics, and food processing. In manufacturing plants, they seamlessly integrate into assembly lines to move parts and products. Within mining and agriculture, they handle heavy, abrasive bulk materials over long distances. Logisti...
Our industrial belt conveyors are precision-engineered systems designed for reliable and efficient material transport in demanding operational environments. Built with high-grade materials and advanced drive mechanisms, they offer durable performance for continuous heavy-duty applications. The product range includes versatile flat belt, portable, and inclined/declined models, each constructed for low power consumption and minimal maintenance. This focus on robust engineering and operational simplicity provides a cost-effective backbone for material handling, ensuring smooth, uninterrupted movement of goods to support your productivity goals.

These conveyor systems are integral to a wide spectrum of industries, including manufacturing, mining, agriculture, logistics, and food processing. In manufacturing plants, they seamlessly integrate into assembly lines to move parts and products. Within mining and agriculture, they handle heavy, abrasive bulk materials over long distances. Logistics centers utilize them for efficient package sorting and distribution, while food processing facilities rely on their design for hygienic transport. This cross-industry suitability stems from their ability to adapt to various layouts, weights, and material types, enhancing workflow efficiency and reducing physical strain across sectors.

We deliver reliable material handling solutions backed by a commitment to quality and performance. Each conveyor system is built to offer long-term operational suitability, reducing total cost of ownership through durable construction and energy-efficient operation. Our focus on reliability means less unexpected downtime, while the potential for tailored configurations ensures the system fits your specific spatial and functional requirements perfectly. This combination of robust engineering, adaptability, and competitive value supports businesses in achieving seamless workflows, maximizing return on investment through sustained efficiency and lower operational costs.

Key Features:
- Precision-engineered flat belt design for versatile handling of unit loads and bulk materials.
- Available in portable, stationary, inclined, and declined configurations for layout flexibility.
- Constructed with heavy-duty frames, rollers, and drive systems for continuous industrial use.
- Designed for easy integration with existing production lines and sorting systems.
- Engineered for low operational noise, energy efficiency, and straightforward maintenance access.

Benefits:
- Enhances operational throughput by enabling continuous, automated material movement.
- Significantly reduces manual handling requirements, lowering labor costs and improving workplace safety.
- Adaptable design allows customization to specific load capacities, lengths, and facility layouts.
- Durable construction ensures long service life and reliability in harsh industrial environments.
- Low maintenance design and energy-efficient operation contribute to reduced long-term operational expenses.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial belt conveyors automate the movement of raw materials, components, and finished goods within production and distribution facilities. They are engineered to handle continuous, high-volume transport over long distances and between different elevations, significantly reducing manual labor and streamlining core operational workflows for enhanced throughput and safety.
These systems are adaptable to diverse layouts and material types, from bulk aggregates to packaged items. Their robust construction ensures reliable performance in demanding environments, supporting just-in-time manufacturing processes, efficient sorting operations, and rapid loading/unloading cycles to minimize downtime and optimize floor space utilization.
- Transporting raw materials and components along automotive and electronics assembly lines.
- Moving bulk grains, fertilizers, and harvested produce in agricultural processing and storage facilities.
- Sorting and conveying parcels and packages in large-scale logistics and e-commerce fulfillment centers.
- Handling ores, coal, and minerals in mining and quarrying operations for processing and stockpiling.
- Conveying food products through washing, inspection, cooking, and packaging stages in food processing plants.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Asian Innovative Manufacturers, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Belt Conveyors For Efficient Material Handling Systems
Industrial Belt Conveyors for efficient, heavy-duty material handling systems. Precision-engineered for reliability across manufacturing, logistics, and mining. Customizable designs ensure seamless integration and superior performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Asian Innovative Manufacturers
 Maharashtra, India
Industrial Equipment & MachineryManufacturer