IN
₹
Apparel & Fashion
Description
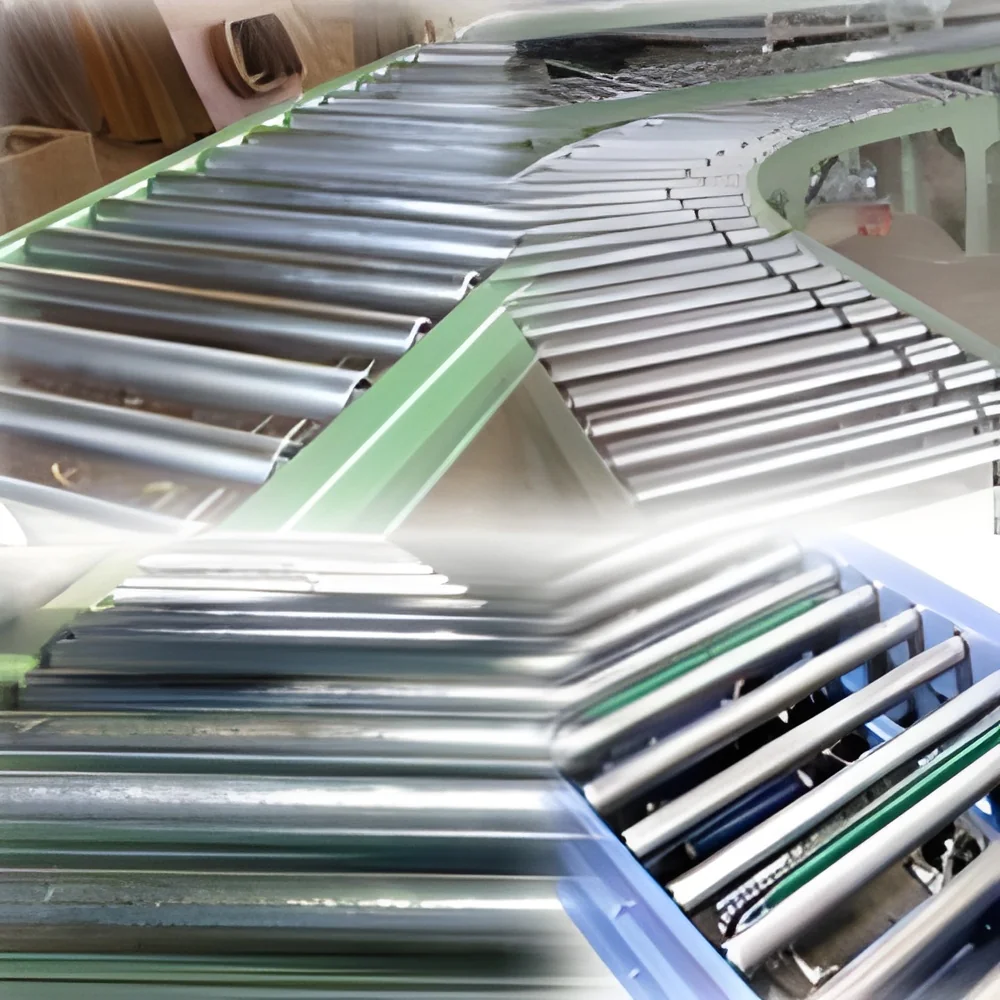
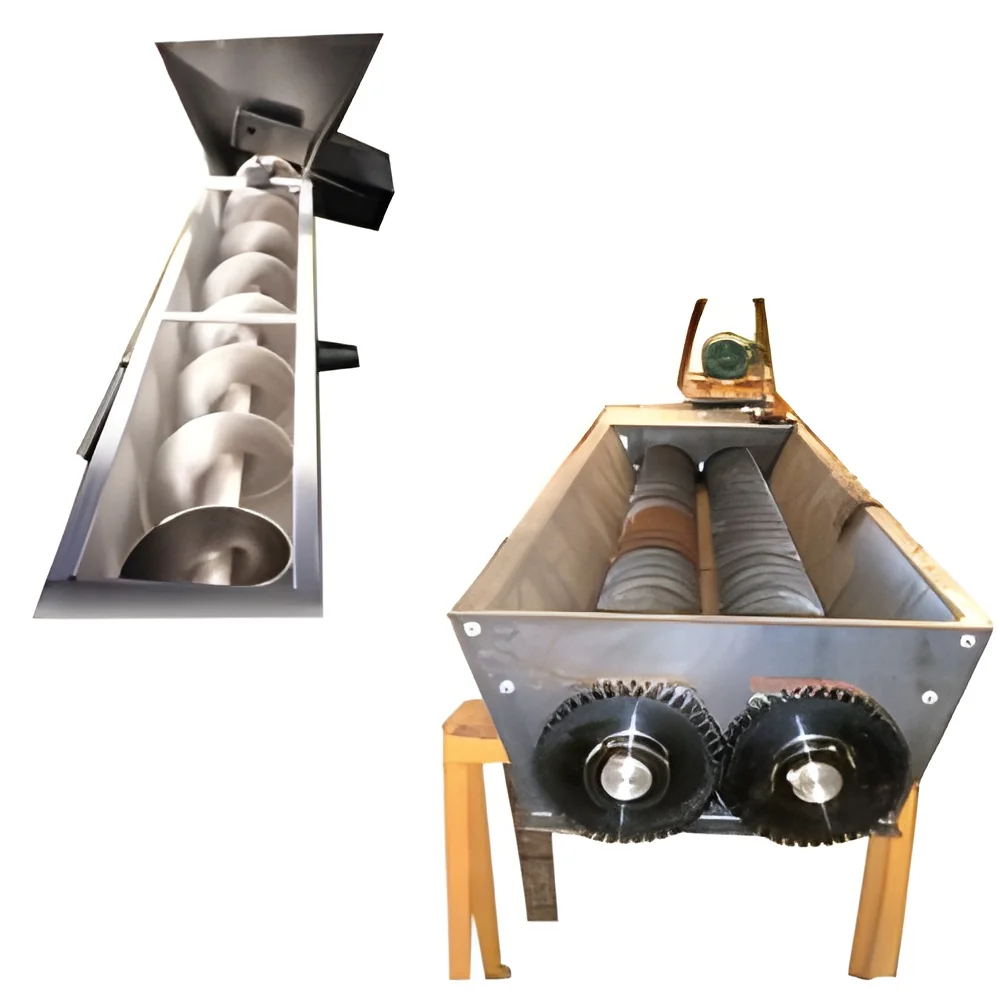
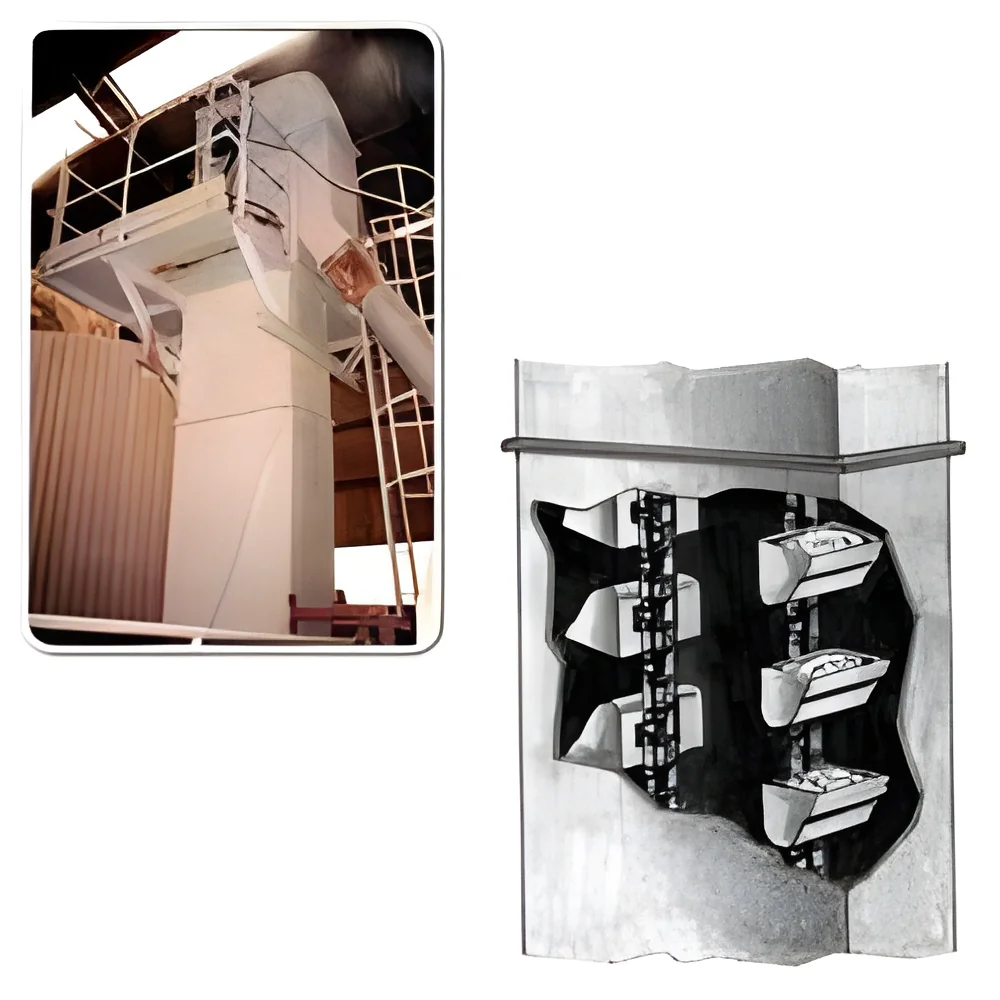
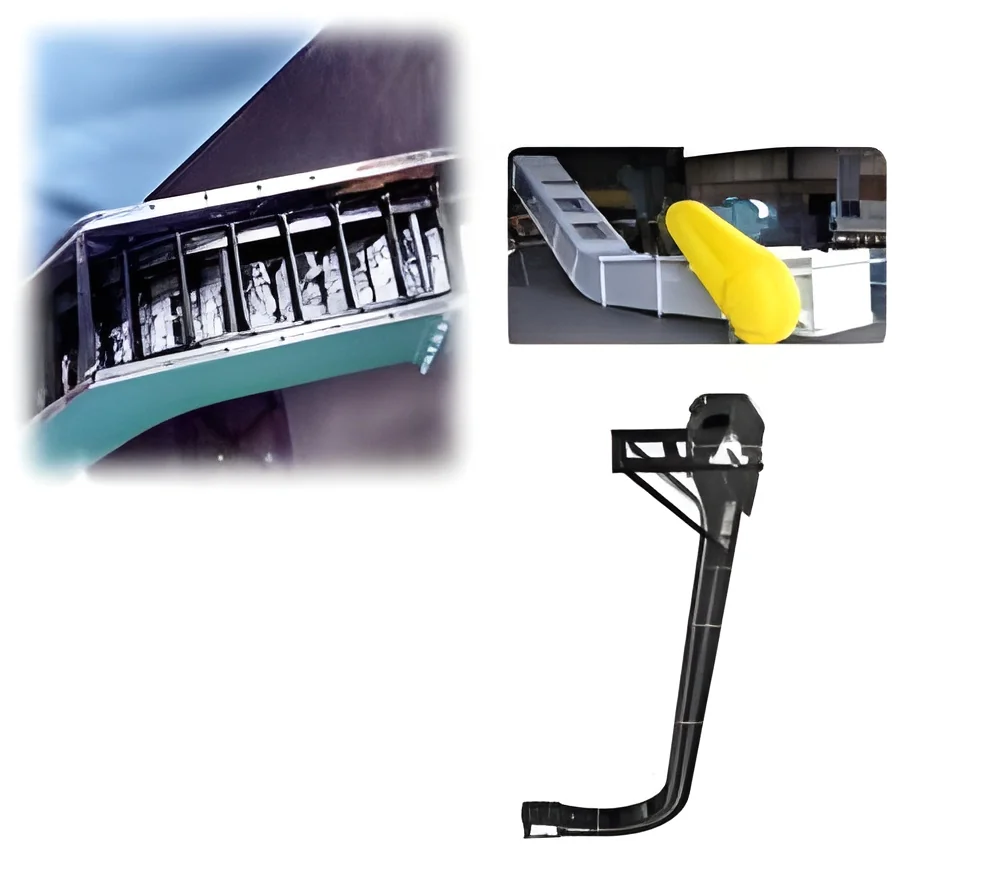
Industrial Heavy Duty Chain Conveyors are engineered solutions designed for the demanding task of bulk material handling in industrial settings. Built with robust components and advanced engineering principles, these conveyors deliver exceptional durability and reliable performance where it matters most. They efficiently transport large volumes of materials—from fine powders to heavy, abrasive aggregates—with remarkably low power consumption, reducing operational costs while maintaining consistent throughput. Their construction withstands the rigors of continuous operation in harsh environments, ensuring long service life and minimal maintenance requirements for facilities that cannot afford unexpected downtime.

These conveyors serve as critical infrastructure across numerous heavy industries. In mining and quarrying operations, they handle abrasive materials with superior wear resistance, moving ores and aggregates through processing stages. Cement plants rely on them to transport ho...
Industrial Heavy Duty Chain Conveyors are engineered solutions designed for the demanding task of bulk material handling in industrial settings. Built with robust components and advanced engineering principles, these conveyors deliver exceptional durability and reliable performance where it matters most. They efficiently transport large volumes of materials—from fine powders to heavy, abrasive aggregates—with remarkably low power consumption, reducing operational costs while maintaining consistent throughput. Their construction withstands the rigors of continuous operation in harsh environments, ensuring long service life and minimal maintenance requirements for facilities that cannot afford unexpected downtime.

These conveyors serve as critical infrastructure across numerous heavy industries. In mining and quarrying operations, they handle abrasive materials with superior wear resistance, moving ores and aggregates through processing stages. Cement plants rely on them to transport hot clinker from kilns, while metal processing facilities use them for moving hot materials from furnaces. Food processing plants benefit from their ability to handle bulk powders and grains hygienically, and manufacturing facilities integrate them into automated production lines for efficient material flow. Their versatility makes them indispensable assets wherever reliable, high-volume material transport is required.

The business value of these heavy-duty chain conveyors lies in their proven reliability and long-term operational efficiency. By minimizing unplanned downtime and reducing maintenance frequency, they deliver significant return on investment through consistent production uptime. Their energy-efficient design lowers ongoing power costs, while their durable construction ensures years of trouble-free service. This combination of reliability, efficiency, and durability makes them a smart investment for operations seeking to optimize material handling processes, reduce total cost of ownership, and improve overall plant productivity with equipment that performs consistently under pressure.

Key Features:
- Heavy-duty construction using premium materials for maximum durability in industrial environments
- Engineered for low power consumption to reduce operational energy costs significantly
- Designed specifically for continuous operation under demanding conditions and heavy loads
- Superior wear resistance for handling abrasive materials without premature failure
- Long service life with minimal maintenance requirements for reduced operational interruptions

Benefits:
- Ensures reliable material transport with minimal downtime for continuous production flow
- Reduces operational costs through energy efficiency and lower maintenance requirements
- Withstands harsh conditions including high temperatures, heavy loads, and abrasive materials
- Provides consistent performance that integrates seamlessly into existing production systems
- Delivers long-term value through durable construction and extended equipment lifespan
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Heavy duty chain conveyors are engineered to transport large volumes of bulk materials efficiently and reliably. They excel in harsh industrial environments where continuous operation is critical, moving everything from fine powders and granules to abrasive aggregates and hot materials directly from processing equipment. Their robust design ensures minimal downtime and consistent performance, making them essential for maintaining production flow in facilities that demand dependable material transport solutions.
These versatile systems integrate seamlessly into existing production lines across multiple sectors. From raw material intake to finished product handling, they provide a continuous, automated flow that optimizes workflow and reduces manual labor. Their ability to withstand extreme conditions—including high temperatures, heavy loads, and abrasive materials—makes them suitable for the most challenging operational settings where standard equipment would fail quickly.
- Transporting raw materials like ores, coal, and aggregates in mining and quarrying operations
- Moving hot cement clinker and other materials from kilns in cement production plants
- Handling abrasive materials such as sand, gravel, and crushed stone in aggregate processing facilities
- Conveying bulk powders, grains, and food products in food processing and agricultural industries
- Automated material supply and product transfer in large-scale manufacturing and metal processing plants
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Asian Innovative Manufacturers, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Heavy Duty Chain Conveyors For Bulk Material Handling
Industrial Heavy Duty Chain Conveyors provide robust bulk material handling with low power consumption and reliable performance. Engineered for demanding environments in mining, cement, and manufacturing industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Asian Innovative Manufacturers
 Maharashtra, India
Industrial Equipment & MachineryManufacturer