IN
₹
Apparel & Fashion
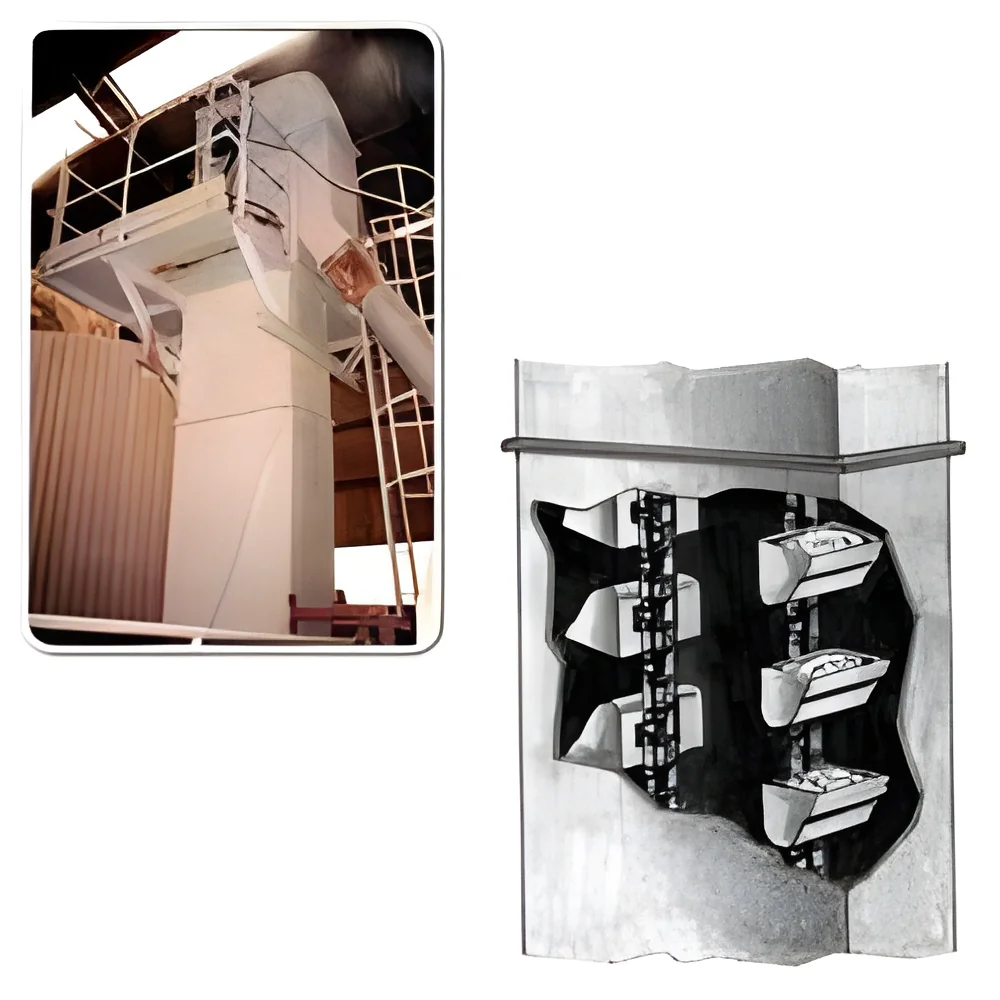
Description
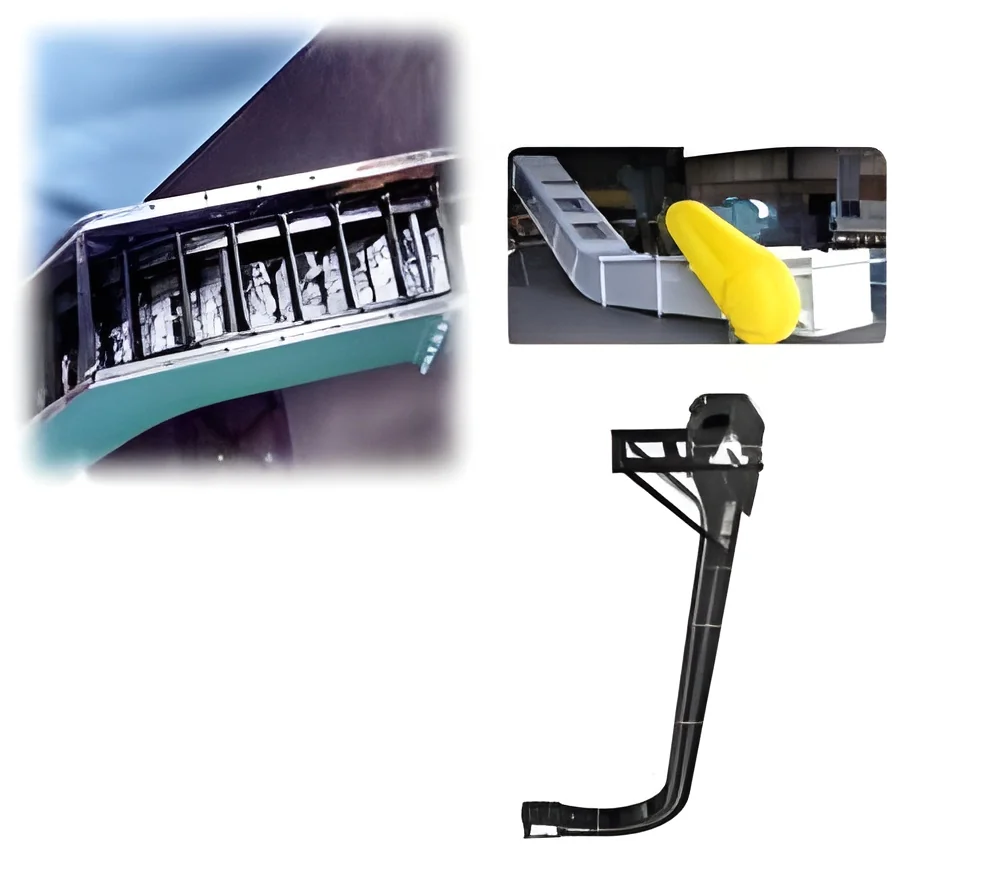
Our premium bucket elevators represent advanced vertical material handling technology engineered to international quality standards for demanding industrial applications. These robust systems efficiently move bulk materials upward with minimal footprint and maximum reliability. Available in both belt and chain configurations, they accommodate various material types including powders, granules, and abrasive substances. Each elevator is designed for specific capacity requirements and operational conditions, ensuring optimal performance in diverse industrial environments. The construction utilizes quality materials including M.S., S.S., and specialized plastics to provide durability and corrosion resistance for extended service life.

These bucket elevators serve critical functions across multiple industries where vertical material transfer is essential. In cement manufacturing, they handle raw meal, clinker, and finished cement products with precision and reliability. The fertilizer indu...
Our premium bucket elevators represent advanced vertical material handling technology engineered to international quality standards for demanding industrial applications. These robust systems efficiently move bulk materials upward with minimal footprint and maximum reliability. Available in both belt and chain configurations, they accommodate various material types including powders, granules, and abrasive substances. Each elevator is designed for specific capacity requirements and operational conditions, ensuring optimal performance in diverse industrial environments. The construction utilizes quality materials including M.S., S.S., and specialized plastics to provide durability and corrosion resistance for extended service life.

These bucket elevators serve critical functions across multiple industries where vertical material transfer is essential. In cement manufacturing, they handle raw meal, clinker, and finished cement products with precision and reliability. The fertilizer industry utilizes them for moving granules and powders through production processes while maintaining material integrity. Agricultural sectors depend on these elevators for grain handling, storage transfer, and processing operations where gentle handling is crucial. Chemical plants benefit from their ability to handle abrasive and corrosive materials safely without contamination. Additional applications include power generation for coal handling and food processing for hygienic material movement.

The business value of these bucket elevators lies in their reliability, efficiency, and performance capabilities. They ensure continuous operation with high uptime, reducing production bottlenecks and maintenance costs significantly. Their energy-efficient design minimizes operational expenses while maintaining high throughput capacity for improved productivity. The robust construction allows businesses to handle demanding materials with confidence, ensuring optimal performance for unique applications. Built with durable materials and precision engineering, these elevators provide long service life with minimal maintenance requirements, delivering exceptional return on investment for industrial operations.

Key Features:
- Vertical conveying design with minimal footprint requirements
- Available in both belt bucket and chain bucket configurations
- Multiple discharge types including centrifugal and continuous options
- Constructed from M.S., S.S., plastic, or material combinations for specific applications
- Single or double strand construction options for different capacity needs

Benefits:
- Efficient vertical material handling with minimal energy consumption
- Reliable performance in demanding industrial environments
- Reduced material spillage and contamination risks
- Long service life with minimal maintenance requirements
- Adaptable to various material types and industry applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Premium bucket elevators deliver efficient vertical transport for bulk materials across multiple industrial sectors. They handle powders, granules, and abrasive substances with minimal spillage and optimized energy consumption, making them essential for continuous material transfer operations in demanding environments. These systems are engineered for reliability and adaptability, serving industries that require consistent performance under heavy loads and varying material characteristics. Their robust design ensures seamless material flow from raw intake to finished product stages in diverse industrial settings with minimal maintenance requirements.
Real-world applications:
- Cement plants for vertical transport of clinker, raw meal, and finished cement products
- Fertilizer production facilities handling granules, powders, and chemical compounds
- Grain processing and storage facilities for efficient vertical movement of cereals and pulses
- Chemical manufacturing plants transferring abrasive and corrosive materials safely
- Power plants for coal handling and ash removal systems in thermal power generation
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Asian Innovative Manufacturers, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Premium Bucket Elevators For Vertical Material Handling In Bulk Industries
Premium bucket elevators for vertical material handling in bulk industries like cement, fertilizers, and grains. Reliable and built to international standards with belt or chain options for heavy-duty performance and minimal spillage.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Asian Innovative Manufacturers
 Maharashtra, India
Industrial Equipment & MachineryManufacturer