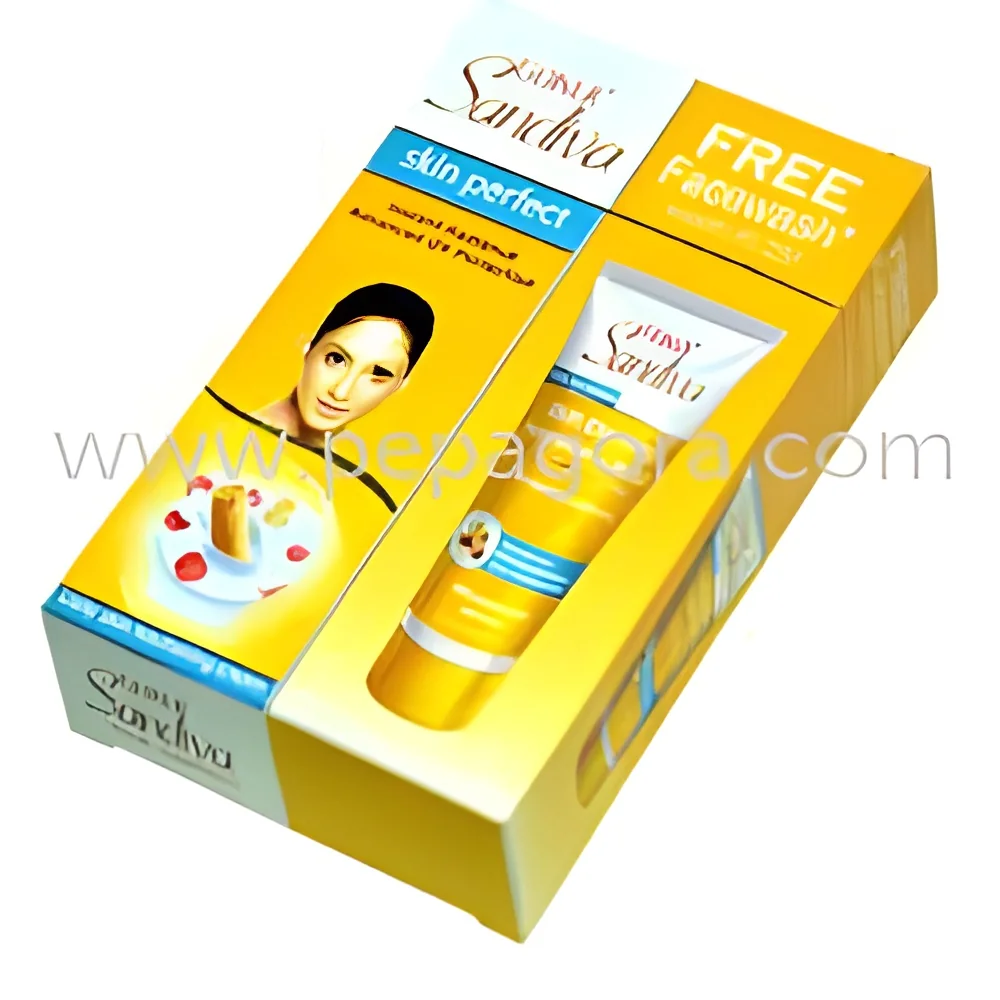
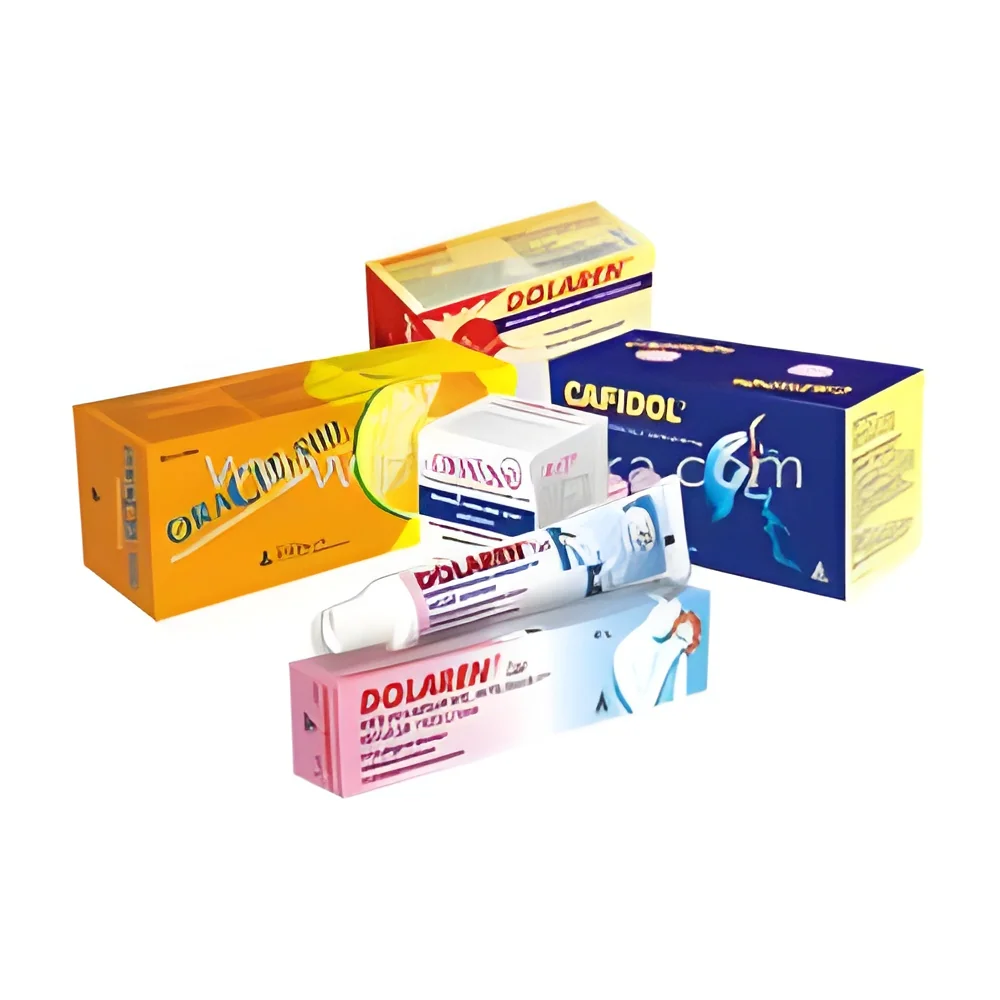
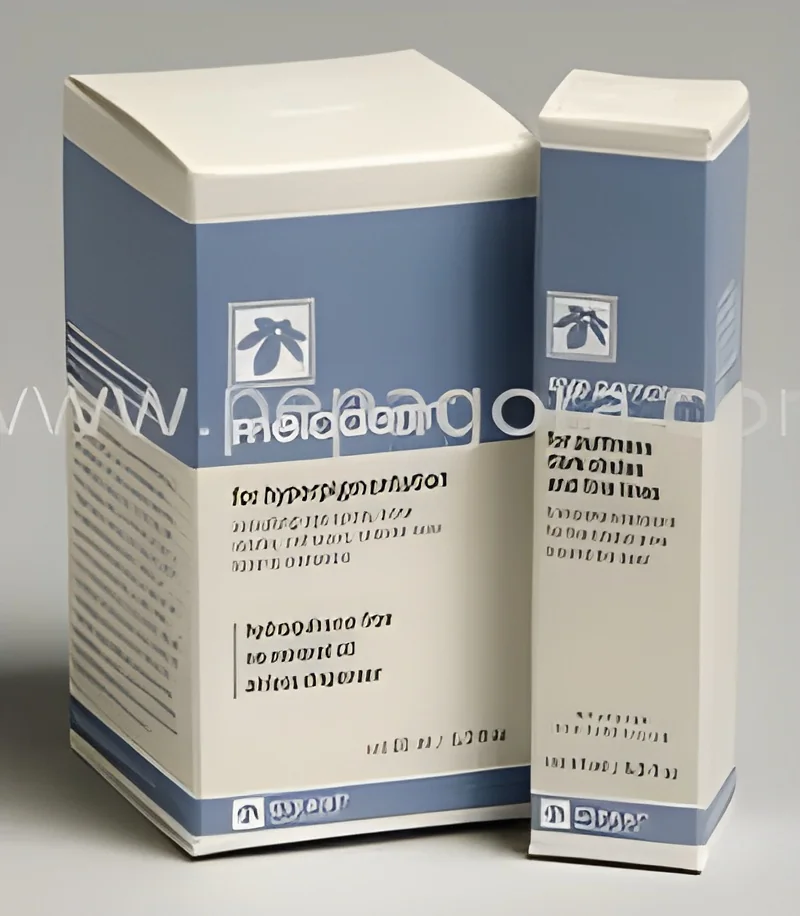
What are Pharmaceutical Corrugated Boxes?
Pharmaceutical corrugated boxes are specialized packaging solutions designed to safely transport and store pharmaceutical products. These boxes are made from corrugated cardboard, which provides strength and durability while remaining lightweight. The design ensures that the contents are protected from physical damage and environmental factors during transit and storage.
These boxes serve critical roles in the pharmaceutical industry, such as protecting medications, medical devices, and other sensitive products. They help maintain product integrity and safety, which is vital in a sector where quality is paramount. Businesses often utilize these boxes in distribution centers, pharmacies, and healthcare facilities to ensure that products reach their destinations in optimal condition.
The pharmaceutical packaging market has seen significant growth due to increasing demand for healthcare products. The need for efficient and reliable packaging solutions has prompted manufacturers to innovate and comply with stringent regulations. Pharmaceutical corrugated boxes are an essential part of this trend, providing a balance of cost-effectiveness and quality assurance.
Key Features and Specifications
Pharmaceutical corrugated boxes are defined by several key features that enhance their utility in the industry. These features cater to the unique demands of pharmaceutical products, ensuring safety and compliance.
Key specifications include:
1. Material Quality
- Made from high-grade, recyclable corrugated cardboard
- Ensures strength and durability for transportation
2. Custom Dimensions
- Available in various sizes to accommodate different products
- Tailored dimensions prevent movement of contents
3. Moisture Resistance
- Provides a barrier against humidity and moisture
- Essential for preserving sensitive pharmaceuticals
4. Printing Options
- Capable of high-quality printing for branding and labeling
- Allows for clear product information and compliance labeling
5. Ventilation Features
- Some models include ventilation holes to prevent heat buildup
- Important for temperature-sensitive pharmaceuticals
6. Secure Closure Mechanisms
- Equipped with locking tabs or adhesive seals
- Ensures the boxes remain closed during transit
7. Stackability
- Designed for easy stacking in warehouses and transportation
- Maximizes space efficiency during storage
8. Compliance with Standards
- Meets industry standards for safety and quality assurance
- Essential for regulatory compliance in pharmaceutical distribution
These key features contribute to the overall effectiveness of pharmaceutical corrugated boxes, making them a preferred choice among manufacturers and distributors.
Common Applications and Use Cases
Pharmaceutical corrugated boxes are versatile and find use across various sectors within the pharmaceutical industry.
1. Pharmaceutical Manufacturing: Used for packaging bulk medications and raw materials during manufacturing processes.
2. Distribution Centers: Essential for transporting products from manufacturers to retailers, ensuring safe delivery.
3. Healthcare Facilities: Employed in hospitals and clinics for storing and distributing medications to patients.
4. Online Pharmacies: Used for shipping pharmaceuticals directly to consumers, ensuring secure and compliant delivery.
5. Research Laboratories: Ideal for transporting sensitive samples and research materials that require protection.
6. Cold Chain Logistics: Critical in transporting temperature-sensitive products, ensuring compliance with temperature control standards.
7. Veterinary Medicine: Used for packaging and delivering veterinary pharmaceuticals, ensuring safe handling.
Product Variants and Subcategories
Pharmaceutical corrugated boxes come in various configurations to meet specific needs within the industry.
Standard Pharmaceutical Box
This variant is designed for general pharmaceutical products. It offers robust protection and is customizable in size and printing. Suitable for a wide range of medications and supplements.
Temperature-Controlled Box
This variant includes insulation and ventilation features to maintain temperature-sensitive products. It is ideal for transporting vaccines and biologics that require strict temperature control.
Tamper-Evident Box
This variant is designed to indicate if the box has been opened. It provides added security for high-value pharmaceuticals, ensuring product integrity from manufacturer to end-user.
Custom Printed Box
This variant allows for bespoke designs and branding, making it suitable for companies looking to enhance their market presence while ensuring compliance with labeling requirements.
Benefits and Advantages
Pharmaceutical corrugated boxes offer numerous benefits that enhance their appeal in the industry.
Key benefits include:
1. Enhanced Protection: They safeguard medications from damage during transit, ensuring that products arrive intact.
2. Cost-Effectiveness: Lightweight material reduces shipping costs while maintaining high durability.
3. Customization Options: Tailored sizes and designs cater to specific product needs, enhancing brand visibility.
4. Sustainability: Made from recyclable materials, these boxes support eco-friendly practices in packaging.
5. Compliance Assurance: Adhering to industry standards ensures that products remain safe and effective.
6. Efficient Storage: Stackable design maximizes warehouse space, improving logistical efficiency.
Buying Guide for B2B Buyers
When sourcing pharmaceutical corrugated boxes, several factors should be considered to ensure a successful purchase.
1. Quality Assessment: Evaluate the material quality and construction of the boxes to ensure they meet safety standards. Look for certifications that verify compliance with industry regulations.
2. Supplier Verification: Vet suppliers thoroughly by checking their reputations and customer reviews. Ensure they have a reliable history of delivering quality products.
3. Pricing and MOQ: Understand the pricing structures and minimum order quantities. This will help in budgeting and ensuring that you can meet demand without excess inventory.
4. Delivery and Lead Times: Discuss logistics with suppliers to understand lead times for production and shipping. Timely delivery is crucial in the pharmaceutical sector.
5. Compliance Requirements: Ensure that the boxes meet all relevant regulatory standards for pharmaceutical packaging. This is vital for maintaining product integrity and safety.
Compliance and Certifications
Pharmaceutical corrugated boxes must adhere to rigorous standards to ensure safety and quality.
Relevant quality standards such as ISO 9001 focus on effective quality management systems. Compliance with these standards is essential for maintaining high-quality production processes.
Additionally, HACCP (Hazard Analysis and Critical Control Points) certifications are important for ensuring food safety in pharmaceutical applications. These guidelines help in identifying and mitigating risks throughout the packaging process.
Compliance with Good Distribution Practices (GDP) is also critical. It ensures that pharmaceutical products are consistently stored, transported, and handled according to quality standards.
Furthermore, obtaining CE certification indicates that the packaging meets European safety, health, and environmental protection standards. This is particularly important for companies operating in regions that require such certifications.
Finally, regional compliance considerations should be taken into account, as regulations can vary significantly between different markets.
Why Source Pharmaceutical Corrugated Boxes from Pepagora?
Pepagora provides a trusted platform for sourcing pharmaceutical corrugated boxes, offering several key advantages to B2B buyers.
Verified Supplier Network: Pepagora connects buyers with a network of verified suppliers. Each supplier is thoroughly vetted to ensure they meet industry standards and quality requirements.
Streamlined RFQ Process: The request for quotation process is efficient and straightforward. Buyers can easily compare quotes from multiple suppliers, allowing for informed purchasing decisions.
Trade Assurance and Support: Pepagora offers trade assurance, ensuring buyer protection during transactions. This support builds confidence in sourcing decisions and helps mitigate risks.
Regional Coverage: With a broad geographic reach, Pepagora serves customers in India, the GCC, and Southeast Asia. This extensive coverage ensures that buyers can access quality products regardless of their location.

 IN