IN
₹
Apparel & Fashion
Description
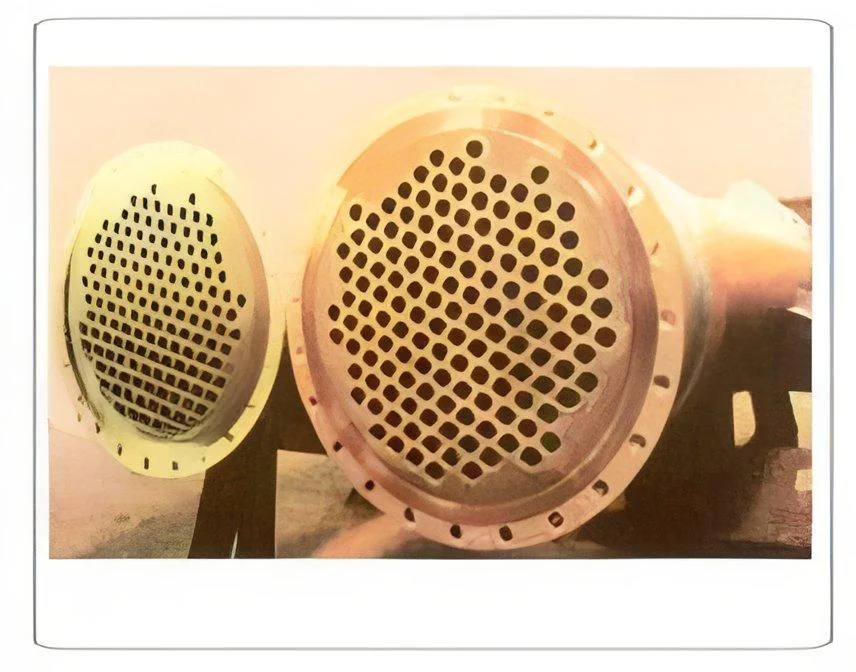
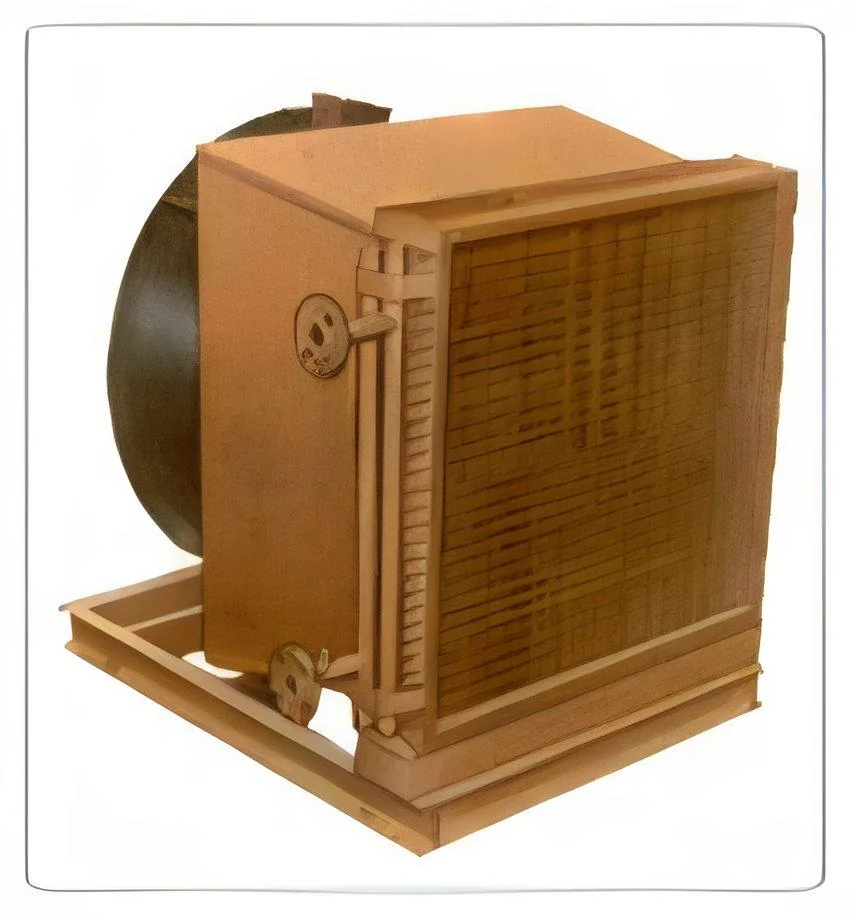
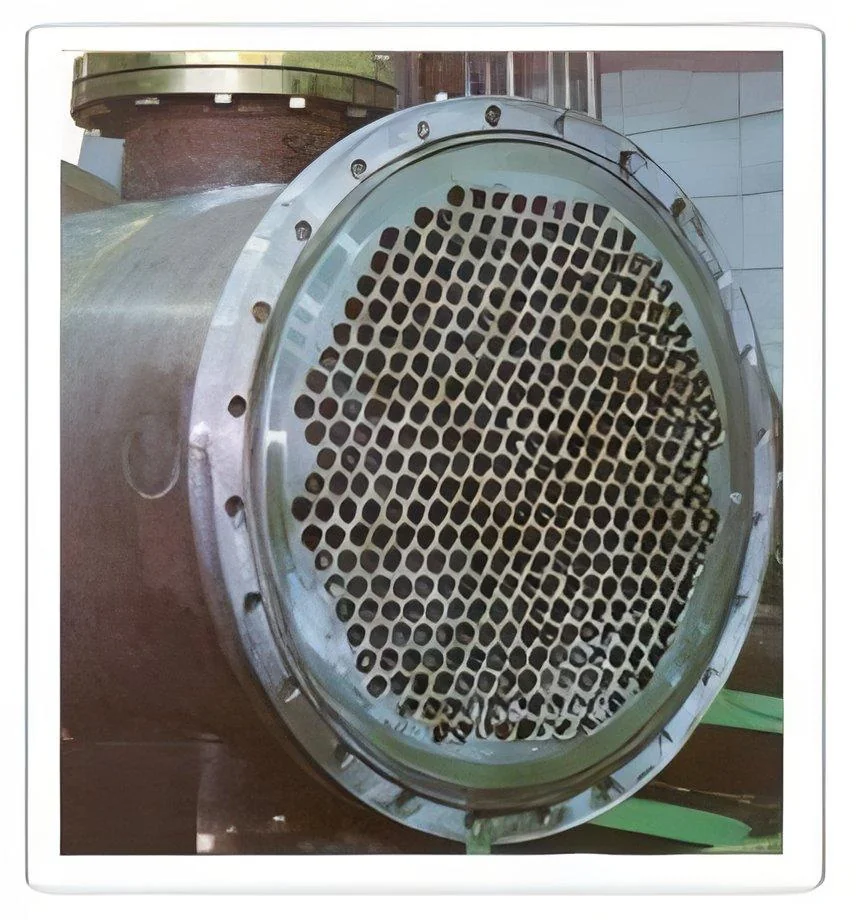
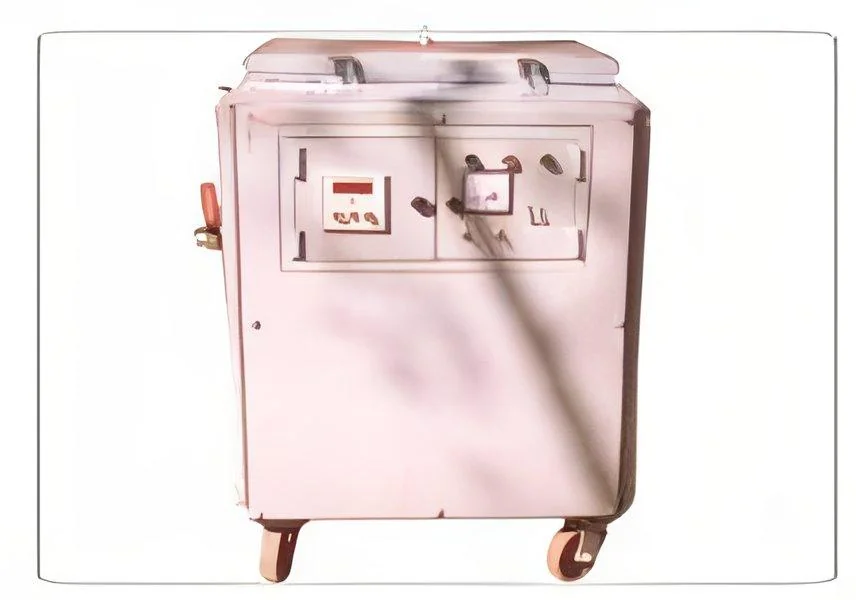
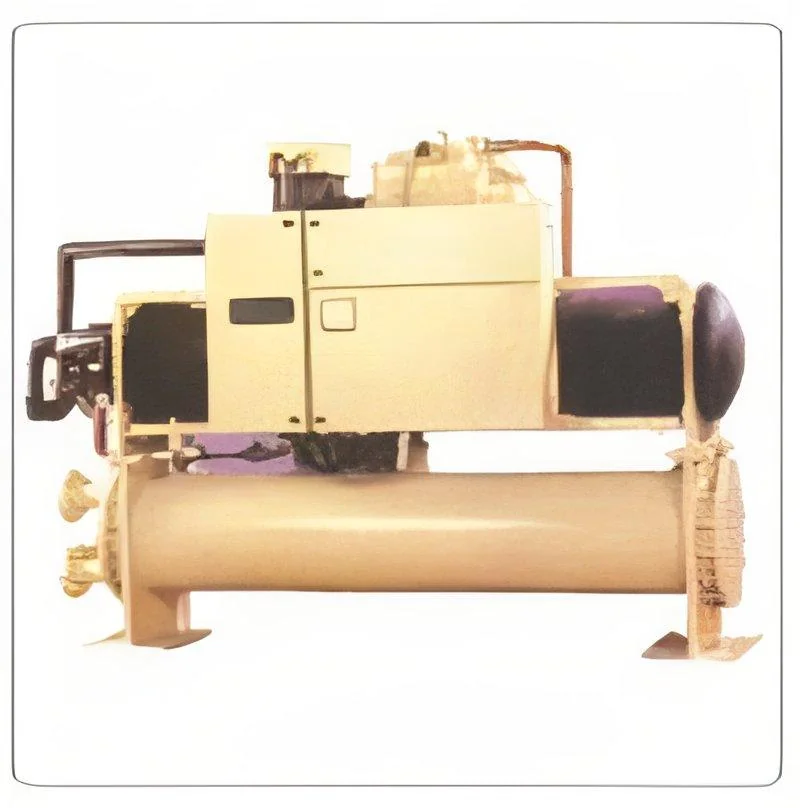
Our industrial water cooled oil chillers represent precision engineering solutions designed for manufacturing environments where exact temperature control is critical. These robust systems efficiently extract heat from industrial processes, maintaining optimal thermal conditions that prevent equipment degradation and ensure consistent operational performance. The units incorporate advanced heat exchange technology that delivers reliable cooling capacity while operating efficiently in various industrial configurations, providing dependable thermal management for demanding applications.

These chillers serve essential functions across multiple industries including plastic processing, metal fabrication, automotive manufacturing, and food processing operations. In injection molding facilities, they maintain precise mold temperatures for quality production consistency, while in metalworking plants they ensure lubricants maintain proper viscosity under extreme operating conditions. The autom...
Our industrial water cooled oil chillers represent precision engineering solutions designed for manufacturing environments where exact temperature control is critical. These robust systems efficiently extract heat from industrial processes, maintaining optimal thermal conditions that prevent equipment degradation and ensure consistent operational performance. The units incorporate advanced heat exchange technology that delivers reliable cooling capacity while operating efficiently in various industrial configurations, providing dependable thermal management for demanding applications.

These chillers serve essential functions across multiple industries including plastic processing, metal fabrication, automotive manufacturing, and food processing operations. In injection molding facilities, they maintain precise mold temperatures for quality production consistency, while in metalworking plants they ensure lubricants maintain proper viscosity under extreme operating conditions. The automotive industry relies on these chillers for consistent manufacturing processes, and food processing plants utilize them for maintaining precise temperature management in production equipment to ensure product quality and safety standards.

The operational value of these industrial chillers extends beyond basic cooling functionality to deliver significant advantages including reduced energy consumption through efficient heat transfer technology, minimized maintenance requirements due to durable construction, and extended machinery lifespan through consistent thermal management. Built for reliability in challenging industrial environments, these systems operate continuously with minimal supervision, reducing downtime risks while providing stable performance that protects manufacturing investments and maintains consistent production quality standards across various applications.

Key Features:
- High-efficiency titanium shell and tube heat exchanger for optimal thermal transfer
- Durable corrosion-resistant components constructed from industrial-grade materials
- Precision digital temperature control system with clear display and monitoring
- Compact space-saving design for easy integration into existing facilities
- Low noise operation suitable for indoor industrial environments

Benefits:
- Reduced energy consumption through efficient heat transfer technology
- Extended equipment lifespan through consistent thermal management
- Minimal maintenance requirements with durable industrial construction
- Reliable continuous operation in demanding manufacturing environments
- Consistent performance protecting manufacturing investments and quality standards
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Water cooled oil chillers provide essential thermal management for industrial equipment operating in high-temperature environments. These systems maintain precise temperature control for hydraulic oils and lubricants, preventing overheating while ensuring consistent machinery performance during continuous production cycles across various manufacturing sectors.
These robust cooling units efficiently regulate temperatures in industrial processes where heat generation threatens equipment reliability. Their superior heat transfer capability makes them ideal for applications requiring stable thermal conditions, from plastic manufacturing to metalworking operations, protecting valuable machinery investments while maintaining product quality standards.
- Temperature control for hydraulic systems in injection molding machines
- Cooling industrial lubricants in metal stamping and forging equipment
- Heat management for CNC machining centers and robotic systems
- Process cooling in plastic extrusion and blow molding operations
- Thermal regulation for food processing and industrial refrigeration systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Parkaire Engineering Company Pvt Ltd, New Delhi
 New Delhi, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Water Cooled Oil Chillers For Precision Temperature Control
Industrial water cooled oil chillers deliver precision temperature control for machinery, ensuring energy efficiency and extended equipment life in demanding manufacturing environments with reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Parkaire Engineering Company Pvt Ltd
 New Delhi, India
Industrial Equipment & MachineryManufacturer