IN
₹
Apparel & Fashion
Description
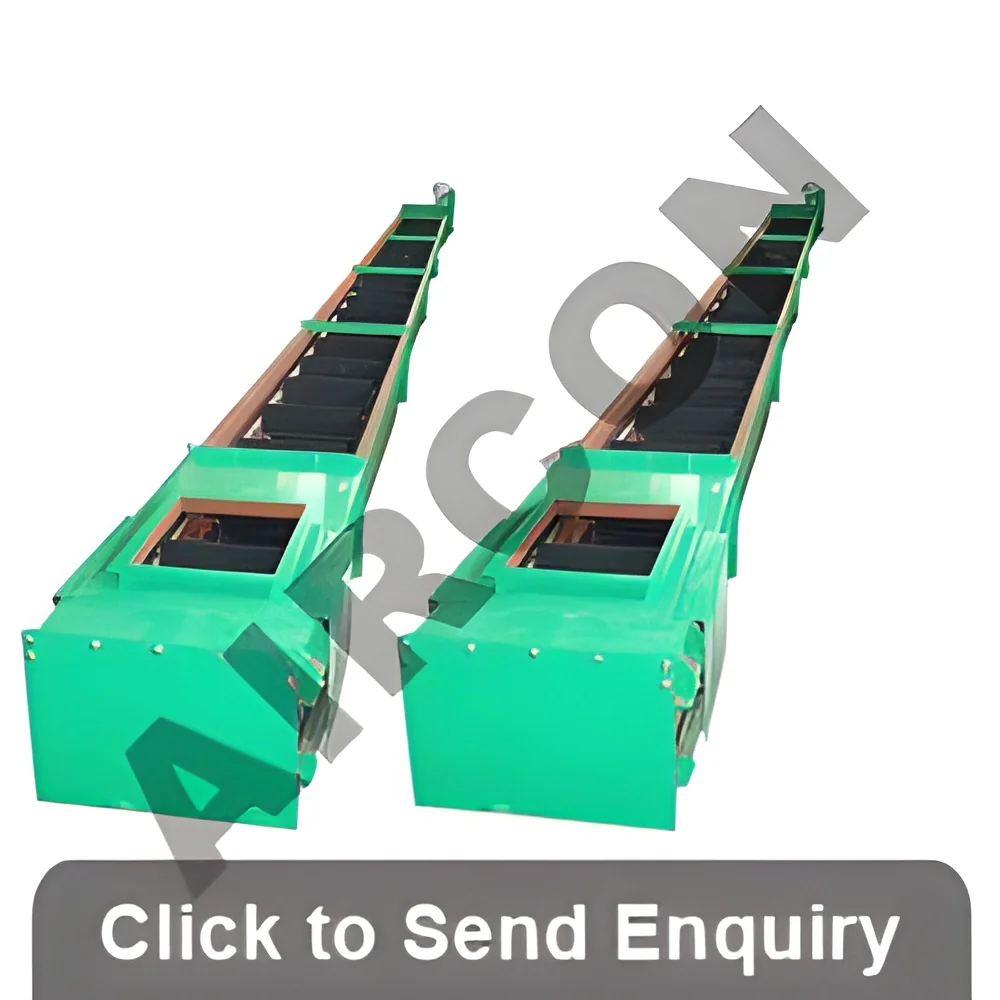
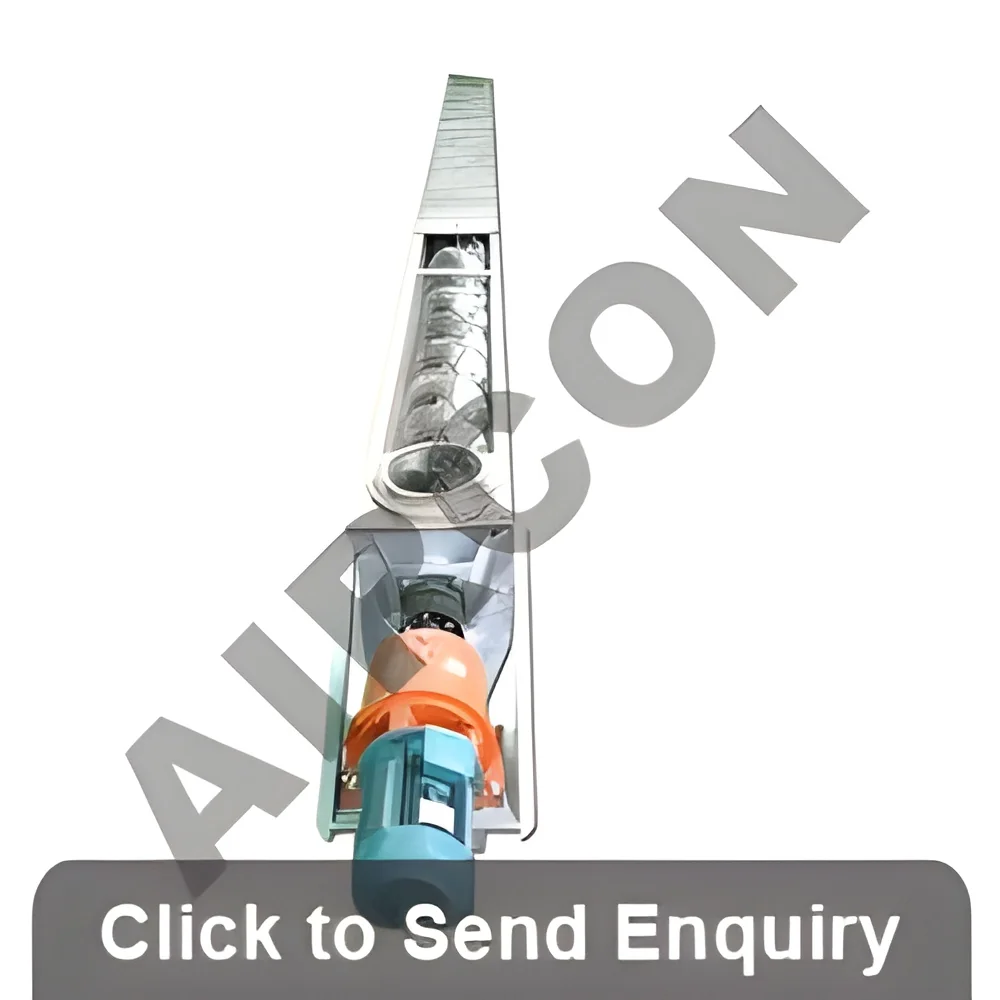
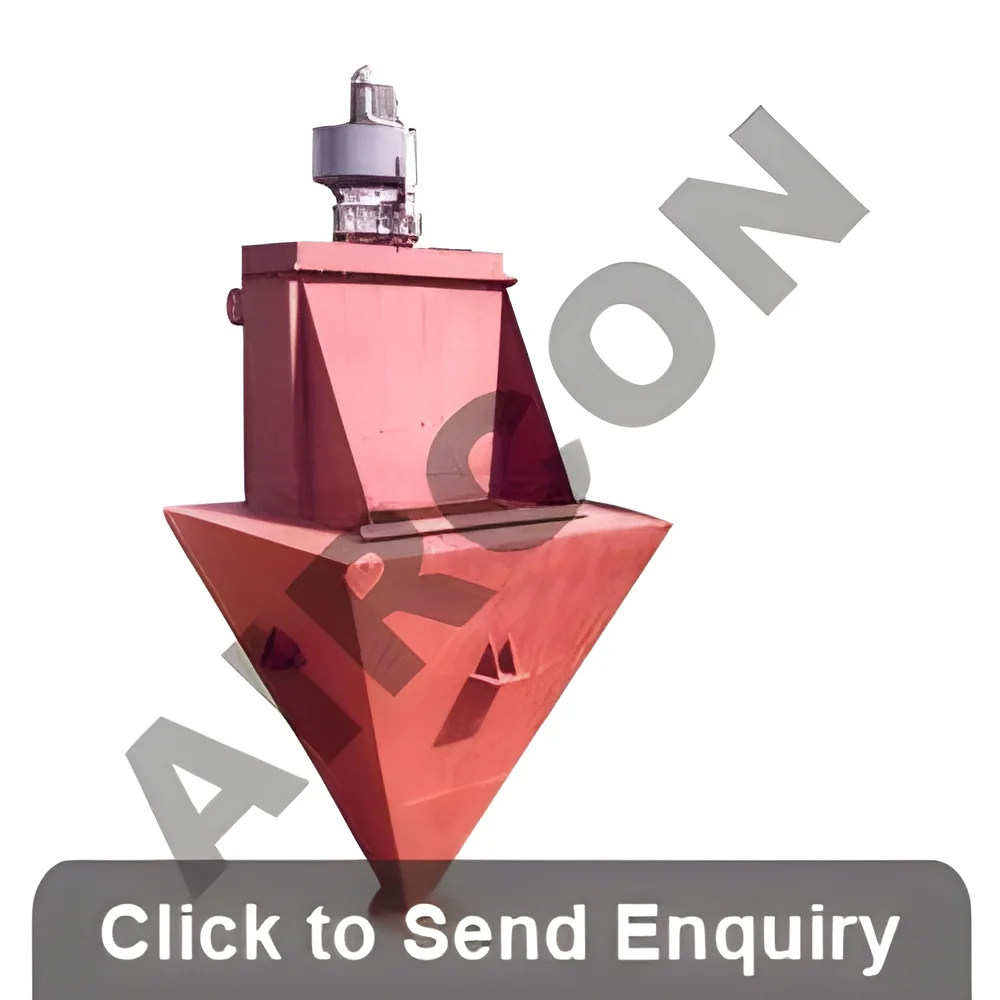
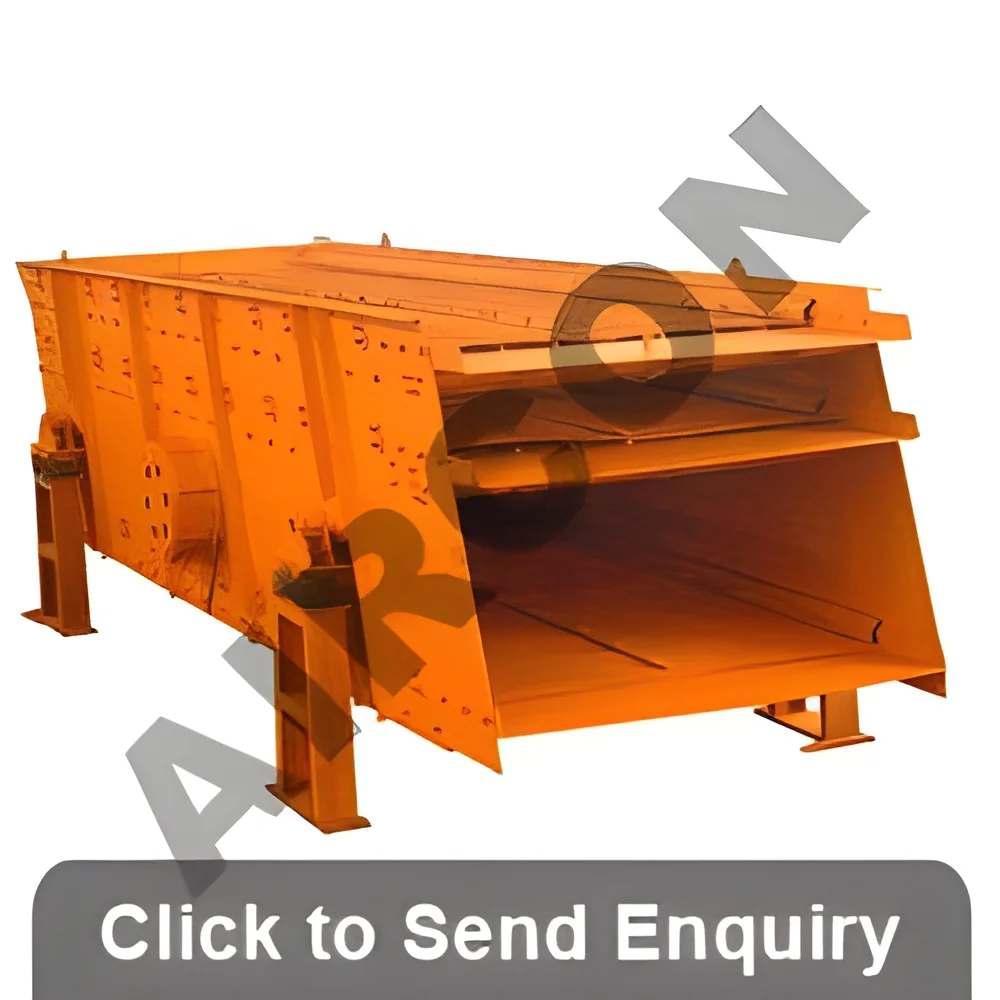
Our industrial vibratory screen represents precision engineering for demanding material separation applications. Designed specifically for mining, quarrying, and construction sectors, this equipment delivers accurate grading and high-capacity screening through advanced vibration technology. The robust construction ensures reliable performance in harsh environments while maintaining efficient particle separation and consistent output quality. Engineered for minimal maintenance requirements, this screening solution integrates seamlessly into existing production lines, providing dependable operation that professionals trust for critical material processing tasks.

This screening equipment serves industries where precise particle size distribution directly impacts product quality and operational efficiency. In mining operations, it separates valuable minerals from waste material. Construction and quarrying operations rely on it for producing accurately sized aggregates for concrete and asp...
Our industrial vibratory screen represents precision engineering for demanding material separation applications. Designed specifically for mining, quarrying, and construction sectors, this equipment delivers accurate grading and high-capacity screening through advanced vibration technology. The robust construction ensures reliable performance in harsh environments while maintaining efficient particle separation and consistent output quality. Engineered for minimal maintenance requirements, this screening solution integrates seamlessly into existing production lines, providing dependable operation that professionals trust for critical material processing tasks.

This screening equipment serves industries where precise particle size distribution directly impacts product quality and operational efficiency. In mining operations, it separates valuable minerals from waste material. Construction and quarrying operations rely on it for producing accurately sized aggregates for concrete and asphalt production. The unit also supports chemical processing facilities in screening raw materials and finished products, while recycling operations utilize its capabilities for material recovery and waste reduction. Its versatile design handles various material types and moisture conditions, making it suitable for diverse industrial applications.

Built with quality components and durable materials, this vibratory screen delivers exceptional value through reduced operational costs and extended service life. The energy-efficient design minimizes power consumption while maintaining high throughput capacity. Low maintenance requirements translate to less downtime and higher productivity. Professionals choose this equipment for its reliability in demanding conditions, consistent performance under heavy loads, and strong return on investment through improved processing efficiency and reduced material waste.

Key Features:
- Heavy-duty construction with reinforced frame for durability in demanding environments
- Precision vibration mechanism ensuring consistent and accurate screening results
- Low maintenance design with easily accessible components for serviceability
- Durable screen decks resistant to wear, abrasion, and material impact
- Efficient drive system providing reliable operation with minimal energy consumption

Benefits:
- Consistent particle separation improving product quality and process efficiency
- Reduced downtime through robust construction and minimal maintenance needs
- Long service life with durable components built for harsh industrial conditions
- High throughput capacity supporting large-scale production requirements
- Reliable performance ensuring continuous operation in demanding applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial vibratory screens deliver precise particle separation and material classification across demanding processing environments. They ensure consistent sizing, improve product quality, and enhance operational efficiency in high-volume applications. These robust machines handle diverse materials from coarse aggregates to fine powders, maintaining smooth workflow and minimizing production interruptions.
These screening units are essential in mining for mineral sorting, construction for aggregate grading, and quarrying for material sizing. Their reliable performance also supports chemical processing, recycling operations, and bulk material handling facilities. The design accommodates both wet and dry screening processes, adapting to various material characteristics and production requirements.
- Mining operations for efficient separation of ores, coal, and minerals by size
- Construction and quarrying sites for precise classification of aggregates and sand
- Recycling facilities for sorting and recovering valuable materials from waste streams
- Chemical processing plants for screening powders and ensuring product uniformity
- Bulk material handling in ports and logistics centers for grading commodities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aircon Handling Systems Private Limited, Karnataka
 Karnataka, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Oceania
Northern Europe
South America
Mid East
Southern Europe
Eastern Europe
Eastern Asia
South Asia
Southeast Asia
Western Europe
Africa
Central America
Quality & Certification
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.
Our objective is to consistently improve quality and design highly advanced product by familiarizing the latest technology in the globe. From the production stage up to the delivery of the product, always stick to the international standard organization quality terms. We are certified with ISO 9001:2008 certification.Industrial Vibratory Screen For Mining And Construction Grading
Industrial Vibratory Screen for precise grading and high-capacity screening in mining, quarrying, and construction applications. Built for durability with low maintenance, ensuring efficient particle separation and reliable performance in demanding environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aircon Handling Systems Private Limited
 Karnataka, India
Industrial Equipment & MachineryManufacturer