IN
₹
Description
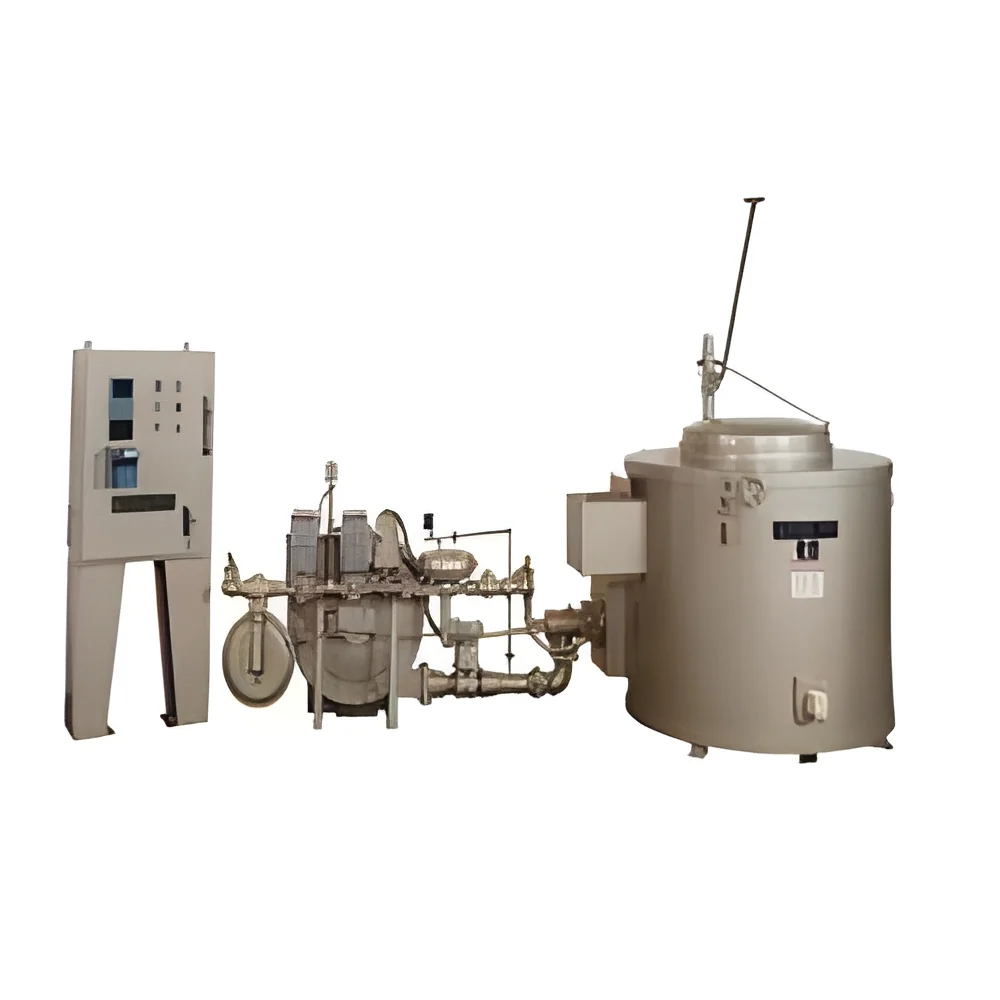
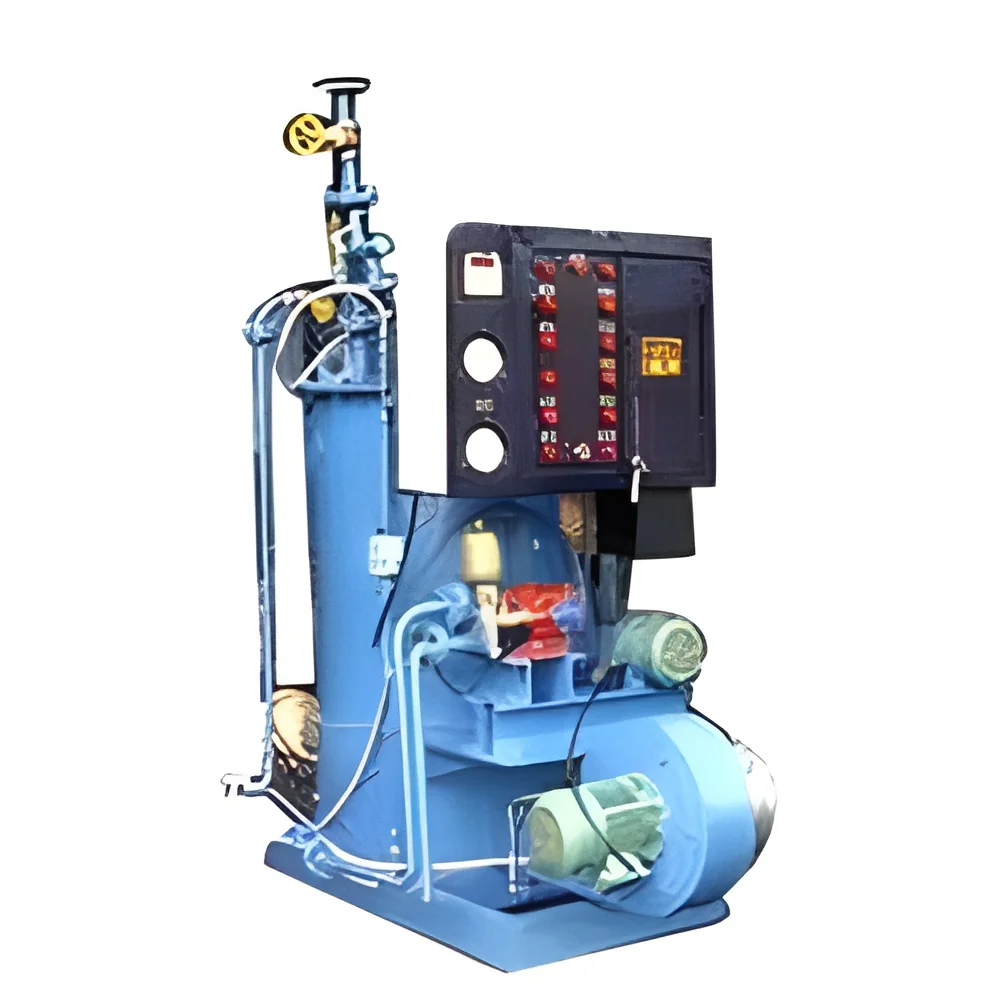
Our industrial steam boilers represent the pinnacle of thermal engineering, incorporating advanced reverse flame technology and air-tight helical coil membrane construction to deliver exceptional performance and reliability. These boilers are meticulously designed with a double-jacketed MS shell and integrated aluminum radiator assembly, ensuring maximum heat retention and efficient fuel consumption. The unique reverse flame technology optimizes combustion efficiency while the helical coil membrane provides superior structural integrity and heat transfer capabilities. Each unit undergoes rigorous quality control processes, guaranteeing consistent performance even under the most demanding industrial conditions and continuous operation requirements.

These versatile steam boilers find extensive application across numerous industrial sectors due to their robust performance and operational flexibility. In textile manufacturing, they provide essential steam for dyeing processes and fabric f...
Our industrial steam boilers represent the pinnacle of thermal engineering, incorporating advanced reverse flame technology and air-tight helical coil membrane construction to deliver exceptional performance and reliability. These boilers are meticulously designed with a double-jacketed MS shell and integrated aluminum radiator assembly, ensuring maximum heat retention and efficient fuel consumption. The unique reverse flame technology optimizes combustion efficiency while the helical coil membrane provides superior structural integrity and heat transfer capabilities. Each unit undergoes rigorous quality control processes, guaranteeing consistent performance even under the most demanding industrial conditions and continuous operation requirements.

These versatile steam boilers find extensive application across numerous industrial sectors due to their robust performance and operational flexibility. In textile manufacturing, they provide essential steam for dyeing processes and fabric finishing operations. Food processing plants rely on them for sterilization, cooking, and cleaning applications where consistent steam quality is paramount. Pharmaceutical facilities utilize these boilers for production processes and equipment sanitation, while chemical plants depend on their reliable output for various heating and reaction systems. The adaptability of these units makes them suitable for any industry requiring efficient and dependable steam generation solutions.

The business value of our steam boilers lies in their exceptional reliability, operational efficiency, and long-term cost savings. These units are engineered to reduce operational expenses through superior fuel efficiency and minimal maintenance requirements, delivering significant return on investment. The reverse flame technology ensures even heat distribution throughout the system, lowering energy consumption and supporting sustainability initiatives. The robust construction and quality manufacturing processes ensure extended operational lifespan with minimal downtime, providing businesses with a dependable steam solution that enhances productivity and operational continuity in critical industrial processes.

Key Features:
- Advanced reverse flame technology for superior heat transfer efficiency
- Air-tight helical coil membrane construction for enhanced durability
- Double-jacketed MS shell with integrated aluminum radiator assembly
- Precision engineering for consistent performance under demanding conditions
- Robust design suitable for continuous industrial operation

Benefits:
- Significant fuel efficiency reducing operational costs and energy consumption
- Enhanced durability and extended operational lifespan with minimal maintenance
- Consistent steam generation ensuring reliable process performance
- Superior heat retention capabilities improving overall system efficiency
- Reduced environmental impact through optimized combustion technology
Specifications
| Key Attributes | |
|---|---|
| membrane | air tight helical coil |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial steam boilers are engineered for demanding environments where consistent steam generation is critical for operational success. The reverse flame technology ensures optimal heat transfer and superior fuel efficiency, making these units ideal for continuous operation in manufacturing plants, processing facilities, and large-scale industrial operations. The robust air-tight helical coil membrane construction provides enhanced durability and safety, meeting rigorous demands across multiple sectors while maintaining consistent performance under heavy usage conditions.
These boilers serve as essential equipment for processes requiring precise temperature control and reliable steam supply. Industries including textiles, food processing, pharmaceuticals, and chemical manufacturing benefit from the high-performance output and operational efficiency. The air-tight helical coil design minimizes heat loss and maximizes energy utilization, significantly reducing operational costs while supporting sustainable practices in industrial settings through improved fuel consumption and reduced environmental impact.
- Textile manufacturing for dyeing, drying, and fabric finishing processes requiring consistent steam
- Food processing facilities for sterilization, cooking, cleaning, and pasteurization applications
- Pharmaceutical production where pure, reliable steam is essential for sanitation and manufacturing
- Chemical plants supporting various heating, distillation, and reaction processes
- Manufacturing facilities for industrial cleaning, processing, and temperature control systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aarathi Engineers, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory Size1000-5000 sqm
Annual Production Capacity0
Main Markets
North America
Oceania
Northern Europe
South America
Mid East
Southern Europe
Eastern Europe
Eastern Asia
South Asia
Southeast Asia
Western Europe
Africa
Central America
Domestic
Industrial Steam Boilers with Reverse Flame and Air Tight Helical Coil
Industrial steam boilers with reverse flame technology and air-tight helical coil membrane construction deliver high-efficiency steam generation for manufacturing, food processing, and textile industries requiring reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aarathi Engineers
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer