IN
₹
Apparel & Fashion

Description
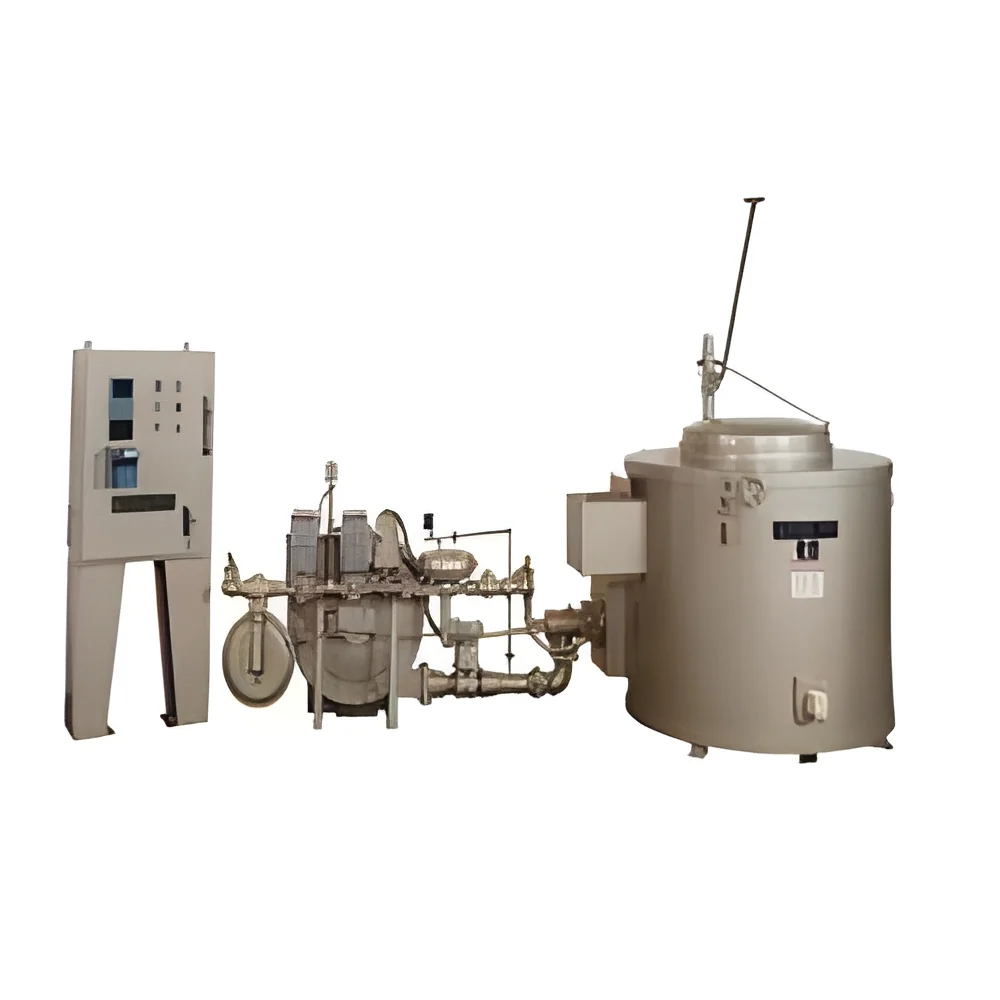
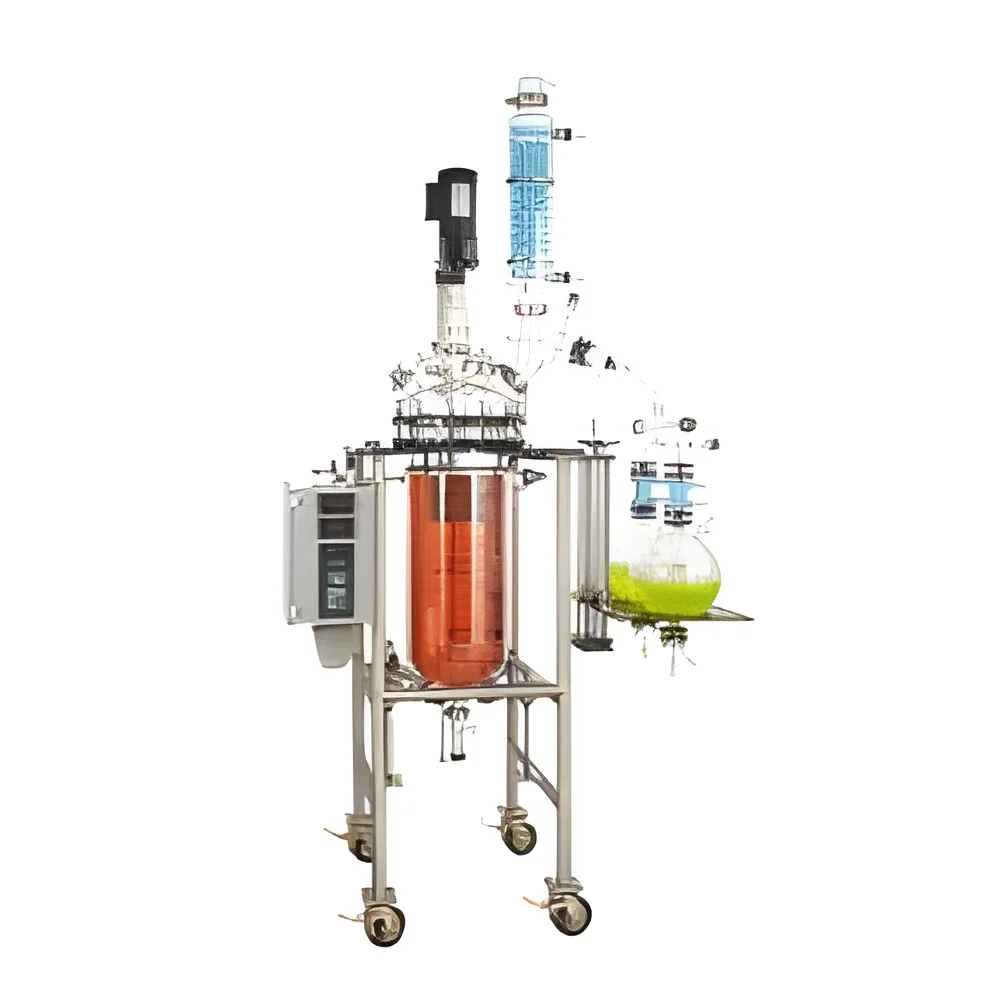
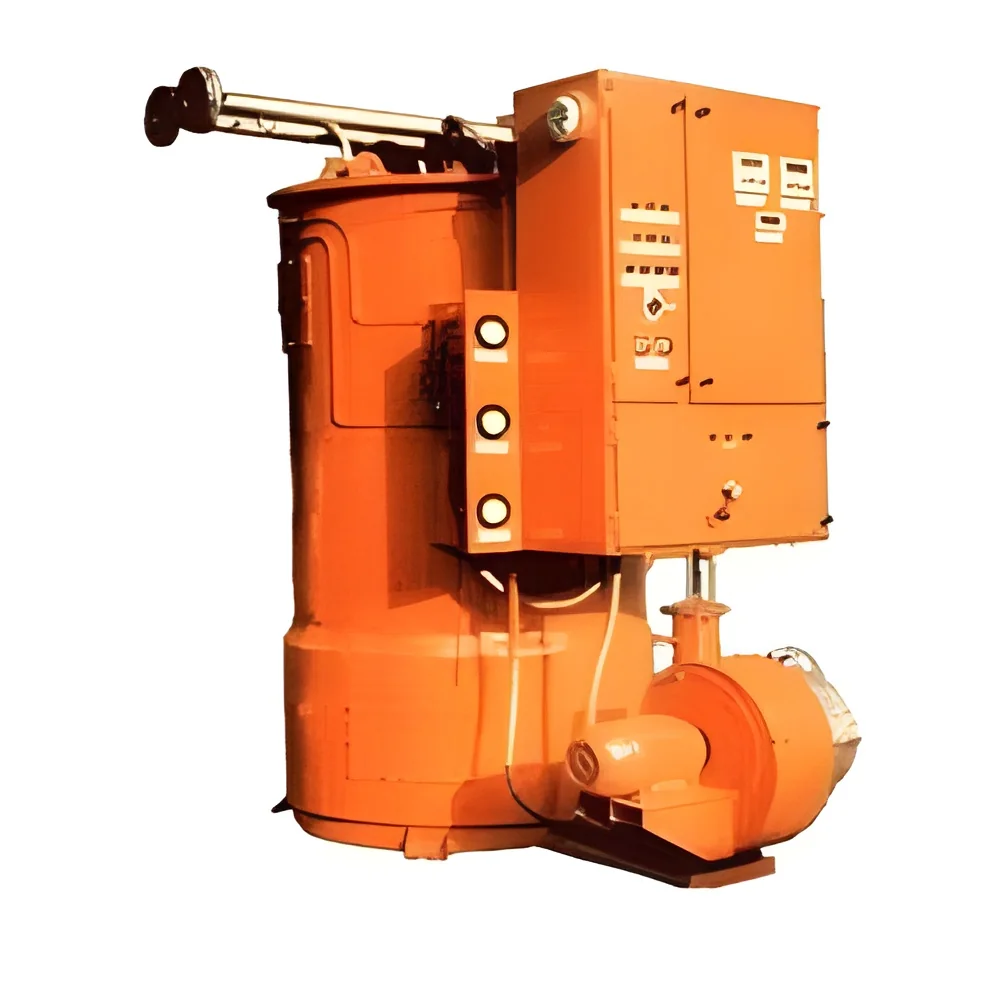
Our industrial evaporators are precision-engineered for maximum efficiency in liquid concentration, utilizing advanced thermal technology to ensure reliable performance even with complex and viscous materials. Built with high-grade, corrosion-resistant materials and intelligent control systems, these units optimize energy usage while maintaining exact concentration levels throughout extended operation cycles. Designed for straightforward integration into existing production lines, our evaporators provide robust construction that guarantees long-term reliability with minimal maintenance, representing a cost-effective and dependable solution for continuous industrial processing demands.

These evaporation systems are indispensable across critical industries where precise concentration and purity are paramount. In the food sector, they concentrate juices and dairy products while preserving flavor and nutritional value. Chemical plants rely on them for solvent recovery and brine management...
Our industrial evaporators are precision-engineered for maximum efficiency in liquid concentration, utilizing advanced thermal technology to ensure reliable performance even with complex and viscous materials. Built with high-grade, corrosion-resistant materials and intelligent control systems, these units optimize energy usage while maintaining exact concentration levels throughout extended operation cycles. Designed for straightforward integration into existing production lines, our evaporators provide robust construction that guarantees long-term reliability with minimal maintenance, representing a cost-effective and dependable solution for continuous industrial processing demands.

These evaporation systems are indispensable across critical industries where precise concentration and purity are paramount. In the food sector, they concentrate juices and dairy products while preserving flavor and nutritional value. Chemical plants rely on them for solvent recovery and brine management, while pharmaceutical manufacturers use them to purify sensitive active ingredients. The wastewater treatment and pulp and paper industries also depend on these systems for effective volume reduction, helping facilities meet environmental regulations and reduce disposal costs through efficient operation.

The business value of these evaporators lies in their proven reliability and operational efficiency, directly impacting your bottom line. They significantly reduce energy consumption and waste volume, leading to lower operational costs and enhanced sustainability credentials. Their durable construction minimizes downtime and maintenance expenses, while their consistent performance ensures product quality batch after batch. This reliability makes them a sound long-term investment for businesses focused on process optimization, cost control, and maintaining a competitive edge in their respective markets.

Key Features:
- High-efficiency heat transfer surfaces for optimal thermal performance
- Corrosion-resistant construction using industrial-grade materials
- Automated control systems for precise temperature and pressure management
- Flexible capacity configurations suitable for various production scales
- Compact and robust design for reliable operation in demanding environments

Benefits:
- Significant reduction in energy consumption and operational costs
- Extended equipment service life with minimal maintenance requirements
- Consistent product quality and concentration accuracy
- Reduced waste volume for lower disposal and handling expenses
- Enhanced process reliability and overall operational efficiency
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial evaporators are engineered for concentrating liquids by removing water, significantly reducing volume before further processing or disposal. This process helps recover valuable solids, minimizes waste handling costs, and improves product stability for long-term storage, supporting operational efficiency across various demanding sectors. These systems are widely adopted for their adaptability to different feed materials and specific concentration requirements. They support key sustainability objectives by lowering energy consumption and substantially reducing waste volume compared to traditional thermal methods, making them a responsible choice for modern industrial operations.
Real-world applications:
- Concentrating fruit juices and dairy products in the food industry
- Recovering solvents and concentrating brines in chemical manufacturing
- Purifying and concentrating active pharmaceutical ingredients
- Reducing sludge volume in industrial wastewater treatment plants
- Concentrating black liquor in the pulp and paper manufacturing process
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aarathi Engineers, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory Size1000-5000 sqm
Annual Production Capacity0
Main Markets
North America
Oceania
Northern Europe
South America
Mid East
Southern Europe
Eastern Europe
Eastern Asia
South Asia
Southeast Asia
Western Europe
Africa
Central America
Domestic
Industrial Evaporators For Efficient Volume Reduction And Water Removal
Industrial evaporators deliver efficient volume reduction and water removal for food, chemical, and pharmaceutical processing. These reliable systems ensure consistent performance and extended product shelf life.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aarathi Engineers
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer