IN
₹

Description
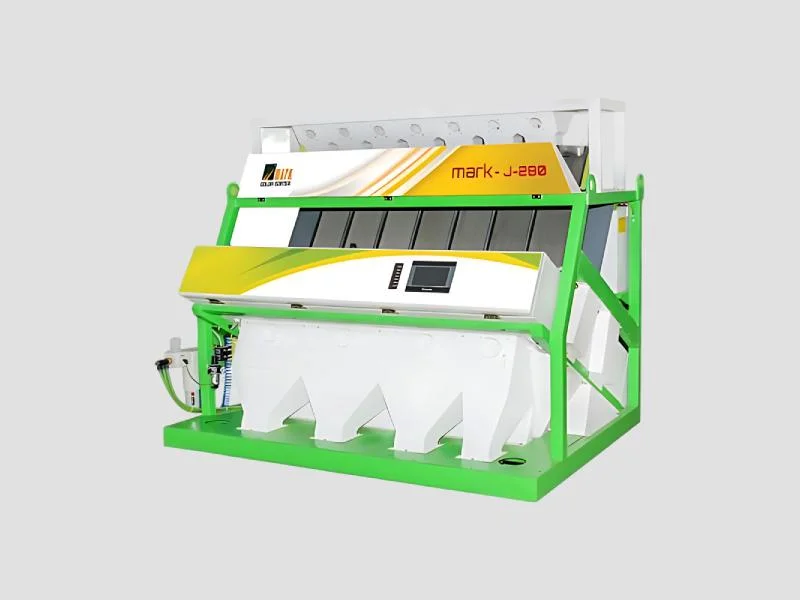
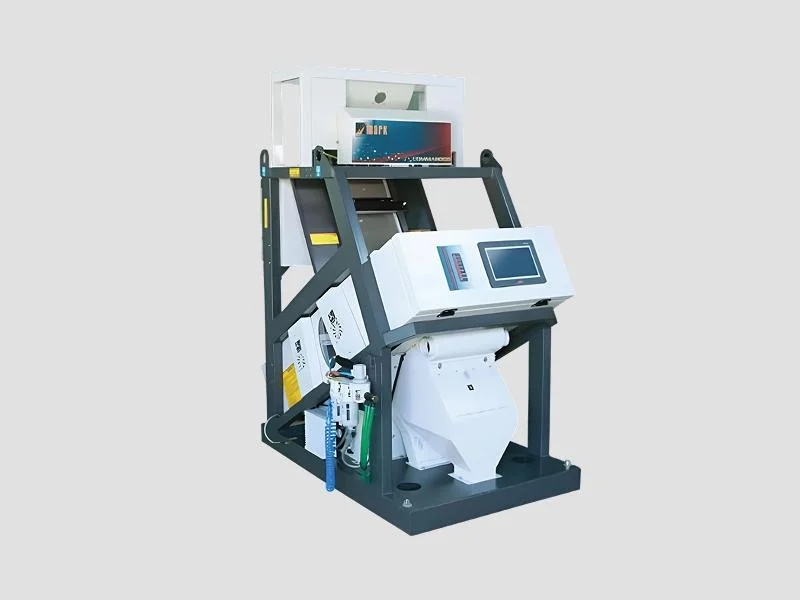
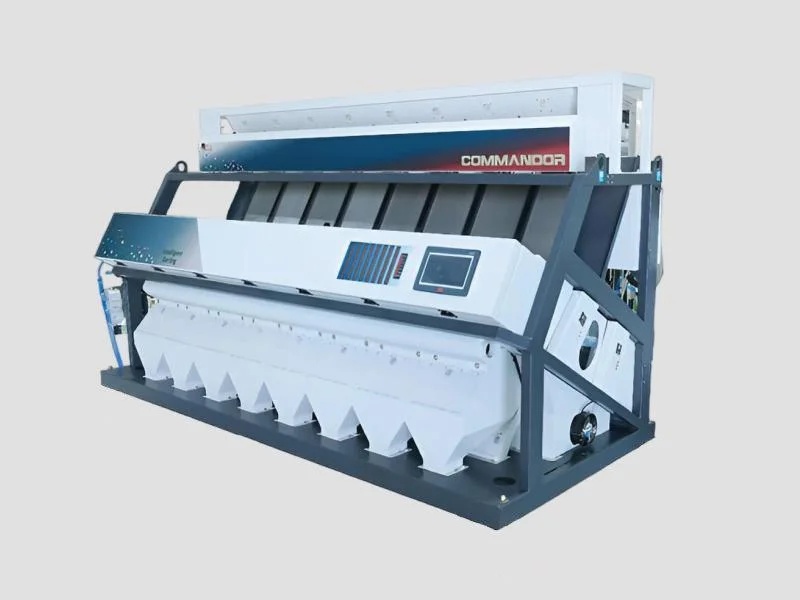
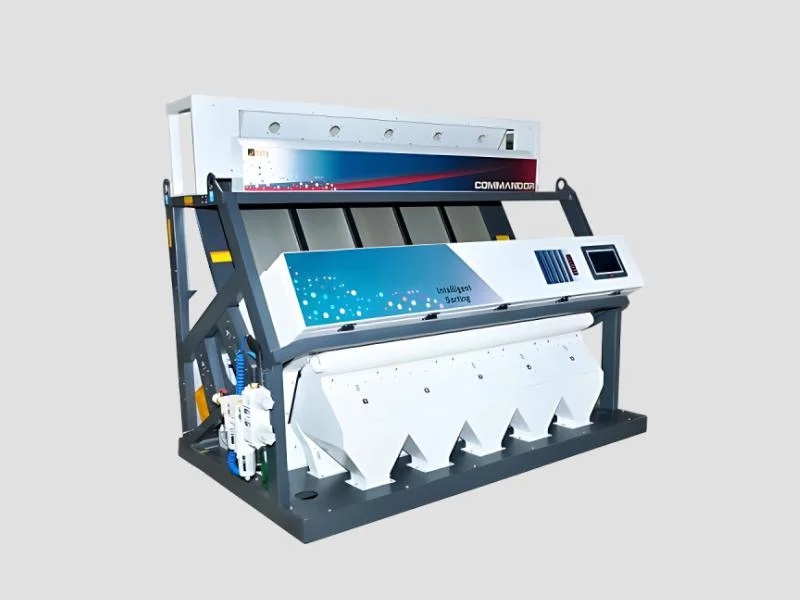
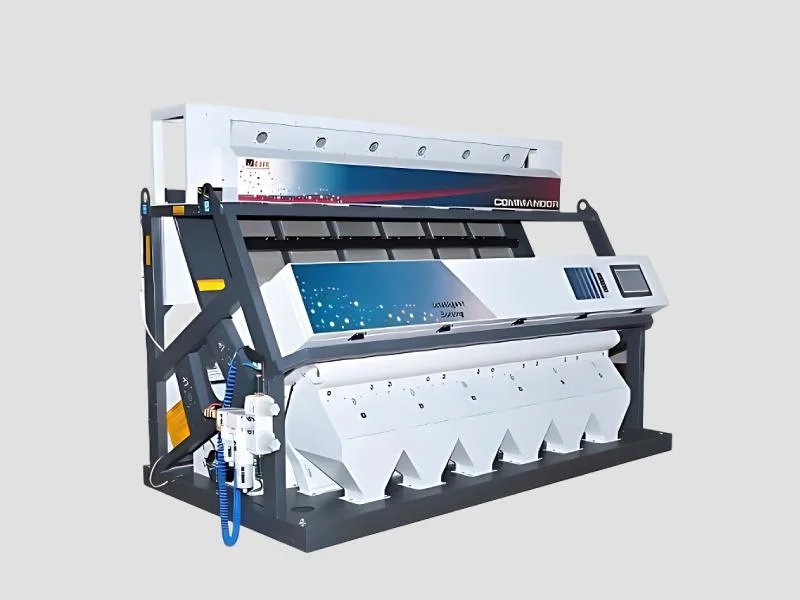
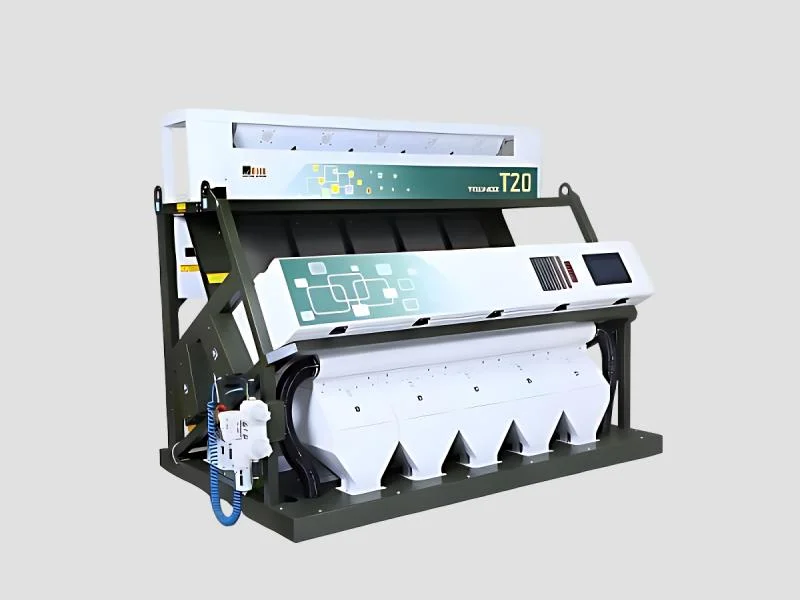
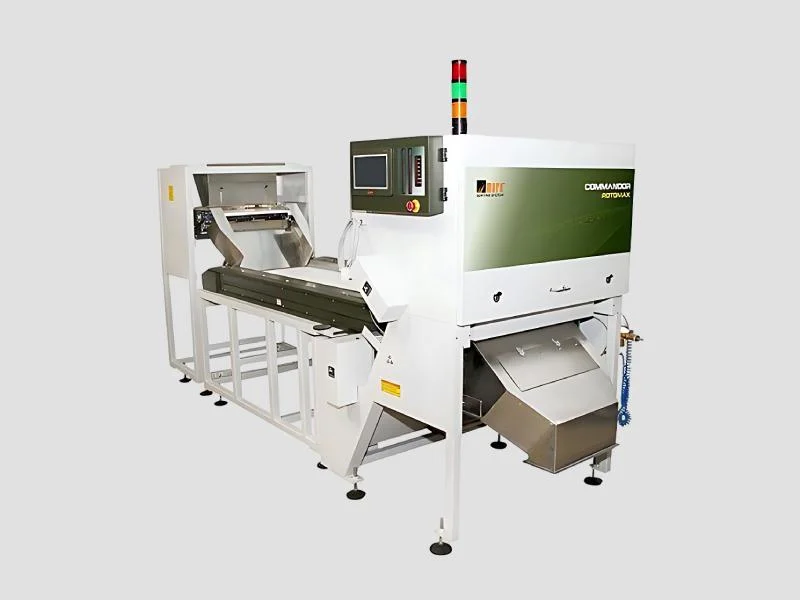
The Industrial Rice Color Sorter 12 Chute represents cutting-edge optical sorting technology designed for industrial-scale food processing operations. This high-performance machine combines tri-chromatic RGB cameras with 5400 x 3 pixel resolution, FPGA digital processing, and advanced AI algorithms to achieve unprecedented sorting precision. With a robust 8 ton per hour capacity and 12 independent chutes equipped with matrix valves, the system ensures optimal material flow while maintaining 99% accuracy in defect detection and removal. The energy-efficient design operates at 4.5 kW power consumption, making it both economically and environmentally sustainable for continuous operation in demanding processing environments.

This sorting machine serves critical roles across multiple industries including rice milling, pulses processing, spice manufacturing, and grain packaging. Rice mills utilize the technology to remove discolored, broken, or contaminated grains from premium varieties, en...
The Industrial Rice Color Sorter 12 Chute represents cutting-edge optical sorting technology designed for industrial-scale food processing operations. This high-performance machine combines tri-chromatic RGB cameras with 5400 x 3 pixel resolution, FPGA digital processing, and advanced AI algorithms to achieve unprecedented sorting precision. With a robust 8 ton per hour capacity and 12 independent chutes equipped with matrix valves, the system ensures optimal material flow while maintaining 99% accuracy in defect detection and removal. The energy-efficient design operates at 4.5 kW power consumption, making it both economically and environmentally sustainable for continuous operation in demanding processing environments.

This sorting machine serves critical roles across multiple industries including rice milling, pulses processing, spice manufacturing, and grain packaging. Rice mills utilize the technology to remove discolored, broken, or contaminated grains from premium varieties, ensuring only the highest quality product reaches consumers. Pulses processing plants benefit from its ability to sort dhal, beans, and lentils by color and quality, while spice manufacturers rely on the machine for consistent color quality in products like peppercorns, seeds, and dried herbs. The 12-chute configuration allows simultaneous processing of different product types, making it invaluable for facilities handling diverse agricultural commodities.

The business value of this rice color sorter lies in its exceptional reliability and significant return on investment for serious buyers. The machine's robust construction and advanced air system featuring 180 CFM capacity with a 40 HP compressor ensure continuous operation with minimal downtime. Single-phase 220V operation makes it accessible for various industrial settings without requiring specialized electrical infrastructure. For importers, distributors, and wholesalers, this machine represents a trusted solution that enhances product quality, reduces manual sorting costs, and increases throughput capacity, ultimately improving competitive advantage in both domestic and international markets.

Key Features:
- 12 independent chutes with matrix valves for optimal material flow and high-volume processing
- Tri-chromatic RGB cameras with 5400 x 3 pixel resolution for precise color differentiation
- FPGA digital processor and AI technology ensuring 99% sorting accuracy
- 8 ton per hour capacity with energy-efficient 4.5 kW power consumption
- Advanced air ejection system with 180 CFM capacity and 40 HP compressor

Benefits:
- High-volume processing capability increases production throughput and operational efficiency
- Superior sorting accuracy ensures consistent product quality and reduces waste
- Energy-efficient operation lowers electricity costs and environmental impact
- Reliable performance minimizes downtime and maintenance requirements
- Enhanced product quality meets international standards for export markets
Specifications
| Key Attributes | |
|---|---|
| Capacity | 8 Ton/hour |
| Accuracy: | 99% |
| Power Consumption: | 4.5 kW |
| Camera: | Tri-chromatic RGB 5400 x 3 Pixel |
| Channels | 12 Chute, Ø756 channels, Matrix Valves |
| Chute available | 1,2,3,4,5,6,7,8,10,12 |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This high-performance rice color sorter is engineered for food processing facilities requiring industrial-scale sorting operations. Its advanced optical technology ensures consistent quality control across various agricultural products, making it ideal for large processing plants that demand reliability and efficiency in their production lines. The machine serves rice mills, pulses processing units, spice manufacturers, and grain packaging facilities. The 12-channel configuration allows simultaneous processing while maintaining 99% accuracy in defect removal, meeting stringent food safety standards and export quality requirements for serious buyers worldwide.
Real-world applications:
- Rice mills removing discolored, broken, or contaminated grains from premium rice varieties
- Pulses and legumes processing plants sorting dhal, beans, and lentils by color and quality
- Spice manufacturing facilities ensuring consistent color quality in peppercorns and seeds
- Grain packaging companies requiring high-speed sorting before bulk packaging operations
- Food export businesses meeting international quality standards for agricultural products
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Promech Industries Pvt Ltd, Tamil Nadu
 Tamil Nadu, India
Manufacturer
Turn Over
Below ₹25 Lakhs
Factory Details
Factory Size1000-5000 sqm
Main Markets
South Asia
Southeast Asia
Africa
Industrial Rice Color Sorter 12 Chute 8 Ton/Hour 99% Accuracy
Industrial Rice Color Sorter 12 Chute delivers 8 ton/hour capacity with 99% accuracy using AI-powered tri-chromatic RGB cameras for superior grain quality in food processing applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Promech Industries Pvt Ltd Tamil Nadu, India
Manufacturer