IN
₹
Apparel & Fashion
Description
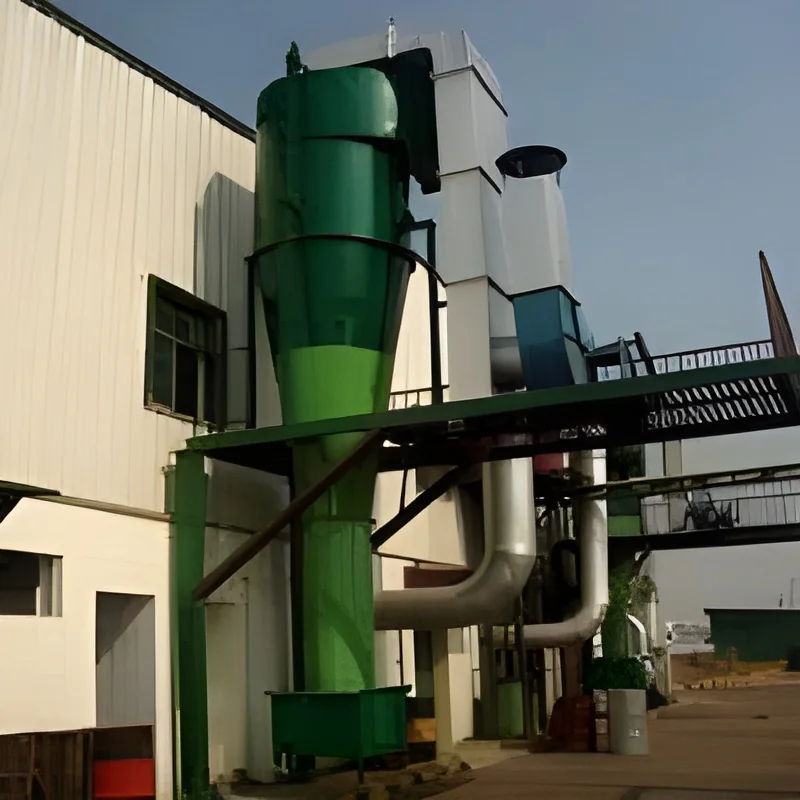
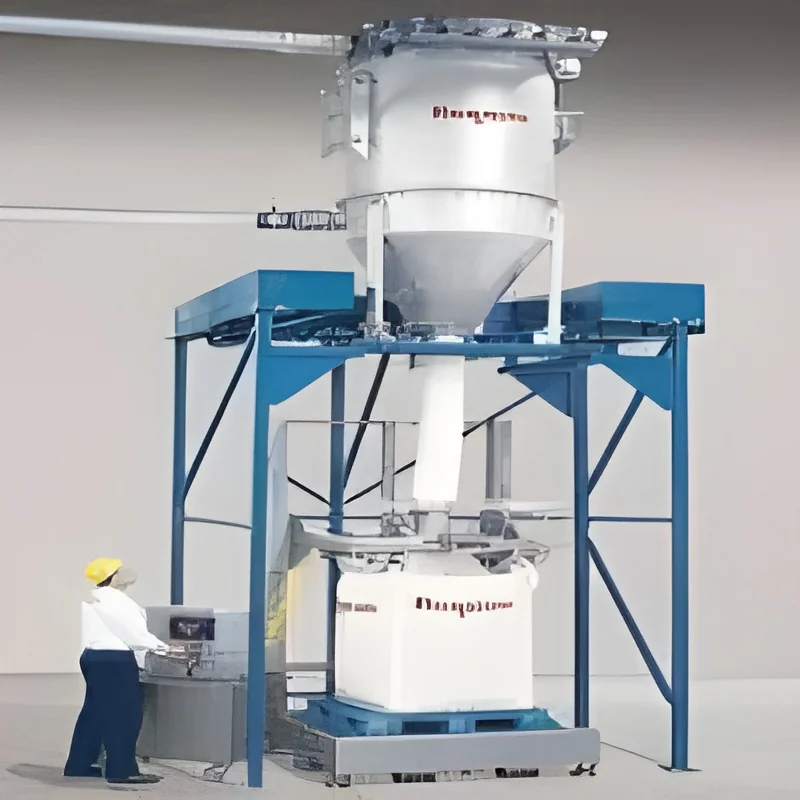
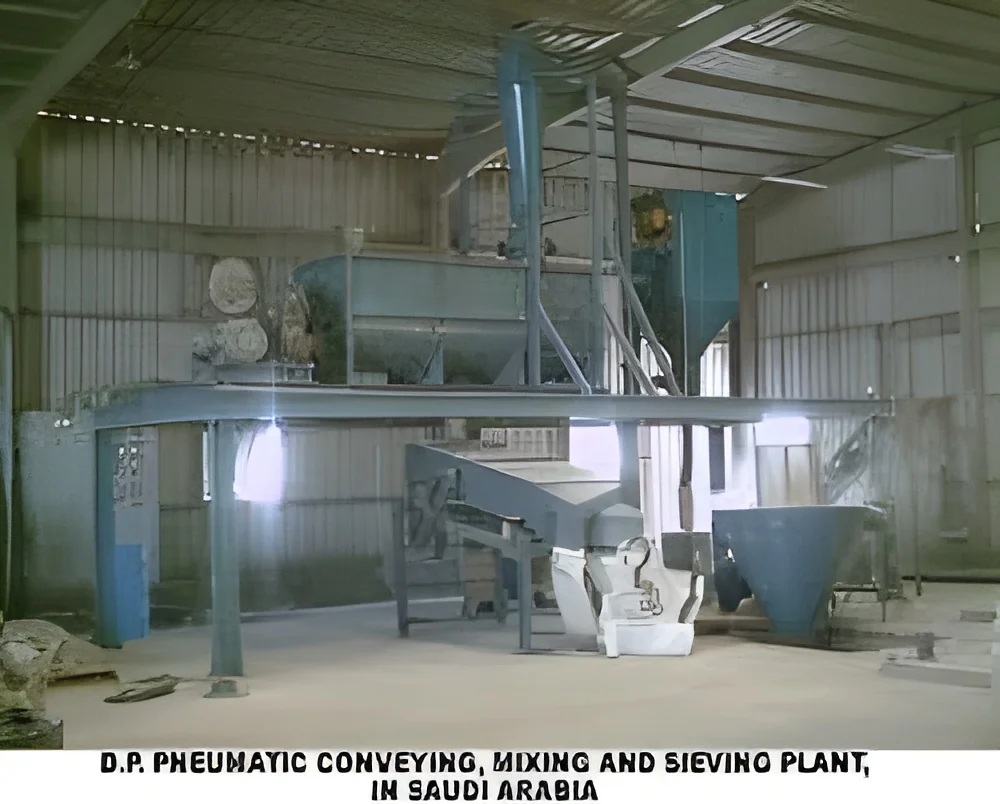
Our Industrial Pneumatic Conveying System provides a sophisticated, enclosed solution for transporting powdered and granular materials with exceptional efficiency and hygiene. Utilizing controlled air pressure or vacuum, it moves materials through a sealed pipeline network, preventing exposure to the environment. This design is particularly valuable for operations constrained by space, as it requires minimal footprint compared to mechanical conveyors. Engineered for high-capacity transfer, the system ensures a consistent, reliable flow of material while maintaining a completely dust-free operation. Its robust construction and intelligent design focus on continuous, trouble-free performance, making it a cornerstone for modern, automated material handling.

This system finds critical application across a spectrum of industries that handle bulk powders. In food processing, it is used for hygienic transfer of ingredients like flour, spices, and powdered flavors, meeting strict safety stand...
Our Industrial Pneumatic Conveying System provides a sophisticated, enclosed solution for transporting powdered and granular materials with exceptional efficiency and hygiene. Utilizing controlled air pressure or vacuum, it moves materials through a sealed pipeline network, preventing exposure to the environment. This design is particularly valuable for operations constrained by space, as it requires minimal footprint compared to mechanical conveyors. Engineered for high-capacity transfer, the system ensures a consistent, reliable flow of material while maintaining a completely dust-free operation. Its robust construction and intelligent design focus on continuous, trouble-free performance, making it a cornerstone for modern, automated material handling.

This system finds critical application across a spectrum of industries that handle bulk powders. In food processing, it is used for hygienic transfer of ingredients like flour, spices, and powdered flavors, meeting strict safety standards. Pharmaceutical manufacturers rely on it to move sensitive powders under controlled, contamination-free conditions. Chemical plants employ it for safe handling of various powders and pellets, while the construction sector utilizes it for efficient cement and fly ash conveyance. Agricultural operations benefit from its ability to move fertilizers and grains. Each sector values the system's capability to preserve product integrity, automate processes, reduce manual labor, and ensure compliance with industry-specific regulatory requirements.

The business value delivered by this pneumatic conveying system is rooted in its operational reliability, cost-effectiveness, and process suitability. It significantly lowers operational expenses by automating material transfer, reducing manual handling costs, and minimizing product loss due to spillage or contamination. The enclosed design is a key safety feature, protecting workers from dust inhalation and preventing cross-contamination between batches. While not fully customizable per the context, its reliable and proven design is suitable for a wide range of standard materials and layouts, ensuring quick integration and productivity gains. With durable components and low maintenance needs, it offers long-term operational stability and a strong return on investment for businesses seeking to modernize their material handling infrastructure.

Key Features:
- Enclosed pipeline system ensures a completely dust-free and contamination-proof transfer process.
- High-capacity conveying capability optimized for minimal spatial footprint and facility layout constraints.
- Operates on reliable pressure or vacuum principles for flexible transfer over various distances.
- Constructed with robust, industrial-grade components for enhanced durability and long service life.
- Engineered for compatibility with a wide range of powdered and granular materials across industries.

Benefits:
- Maximizes hygiene and safety by eliminating dust emissions and preventing material contamination.
- Boosts operational efficiency through automated, high-volume transfer with minimal manual intervention.
- Reduces long-term operational costs by lowering maintenance needs and minimizing product waste.
- Enhances workplace safety by containing powders and reducing exposure risks for personnel.
- Delivers reliable, consistent performance that supports continuous production and improves process uptime.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This pneumatic conveying system is engineered for industries where clean, efficient, and space-conscious material handling is non-negotiable. It seamlessly moves bulk powders like cement, flour, chemicals, and pharmaceuticals through enclosed pipelines, eliminating manual intervention. This drastically cuts contamination risks, reduces labor costs, and ensures a consistent, reliable workflow even in facilities with limited floor space.
The system's versatility allows it to adapt to diverse operational needs across sectors. It supports both pressure and vacuum-based transfer over various distances with minimal upkeep. Configurations can be tailored to specific material characteristics—such as density and flowability—and unique facility layouts. This ensures optimal integration, peak performance, and smooth material flow from intake to discharge point, enhancing overall plant efficiency. Real-world applications:
- Conveying cement, fly ash, and dry mortar in construction and ready-mix concrete plants.
- Handling food-grade powders like flour, sugar, starch, and additives in processing and packaging facilities.
- Transporting active pharmaceutical ingredients (APIs) and excipients in controlled cleanroom environments.
- Moving plastic resins, compound powders, and chemical catalysts in manufacturing and processing units.
- Transferring agricultural powders like fertilizers, grains, and feed additives in bulk handling operations.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Dolar Gold Belts And Fans Pvt Ltd, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Pneumatic Conveying System For Powdered Materials
Industrial Pneumatic Conveying System efficiently transports powdered materials with minimal space. Ideal for high-capacity, dust-free handling in food, pharma, chemical, and construction industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Dolar Gold Belts And Fans Pvt Ltd
 West Bengal, India
Industrial Equipment & MachineryManufacturer