IN
₹
Description
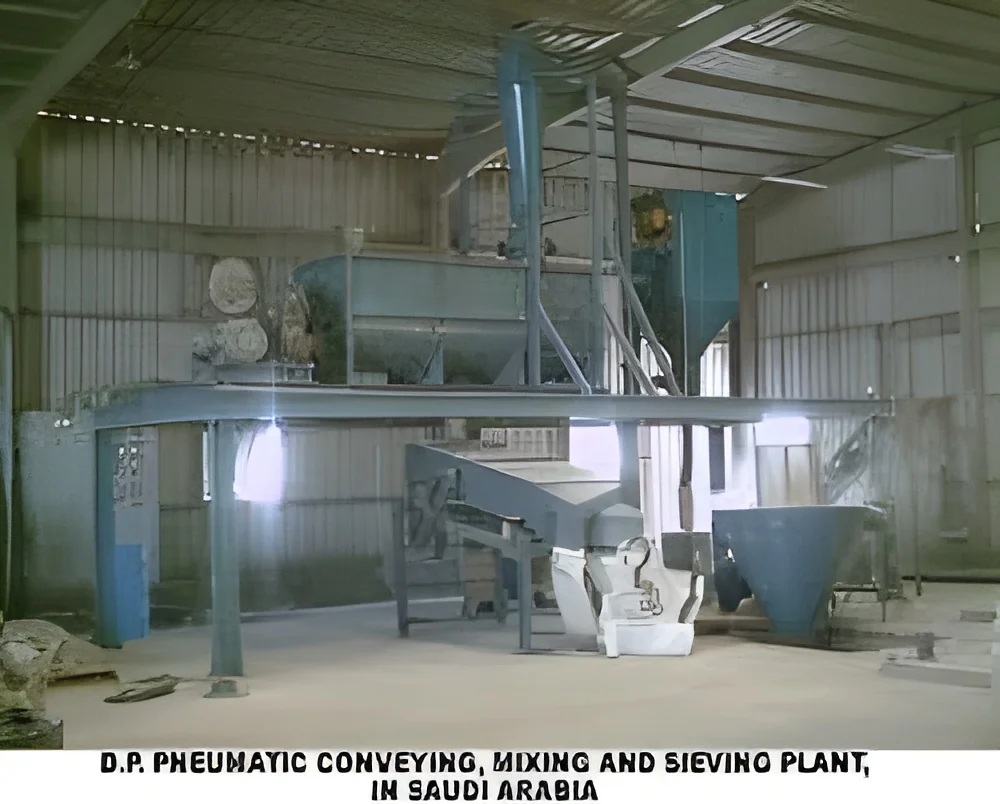
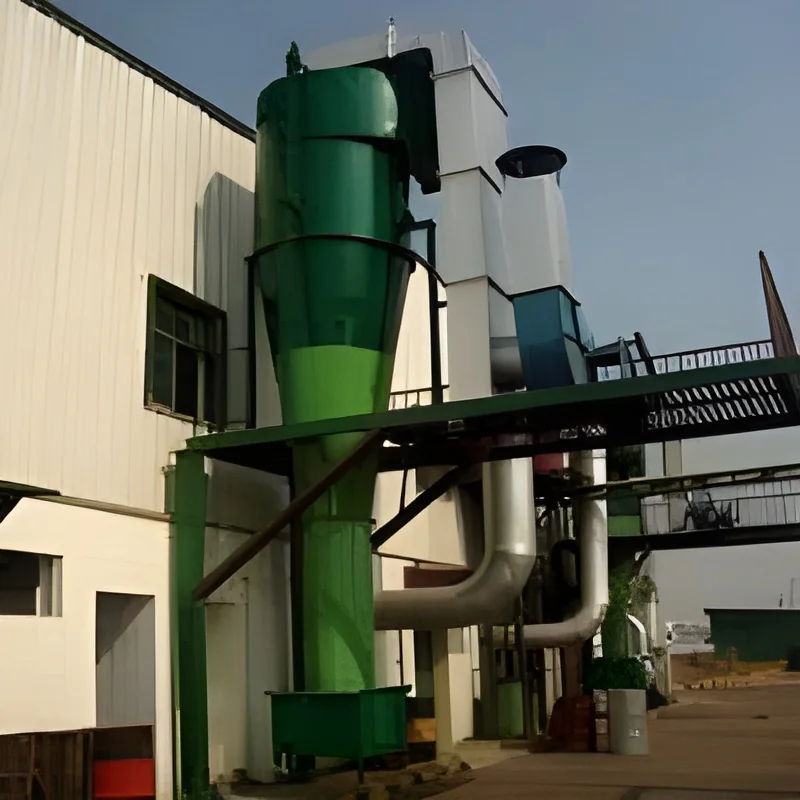
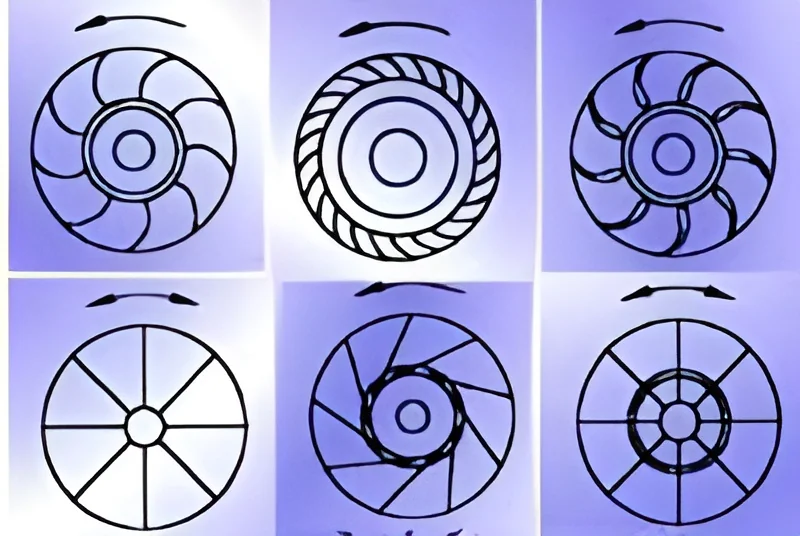
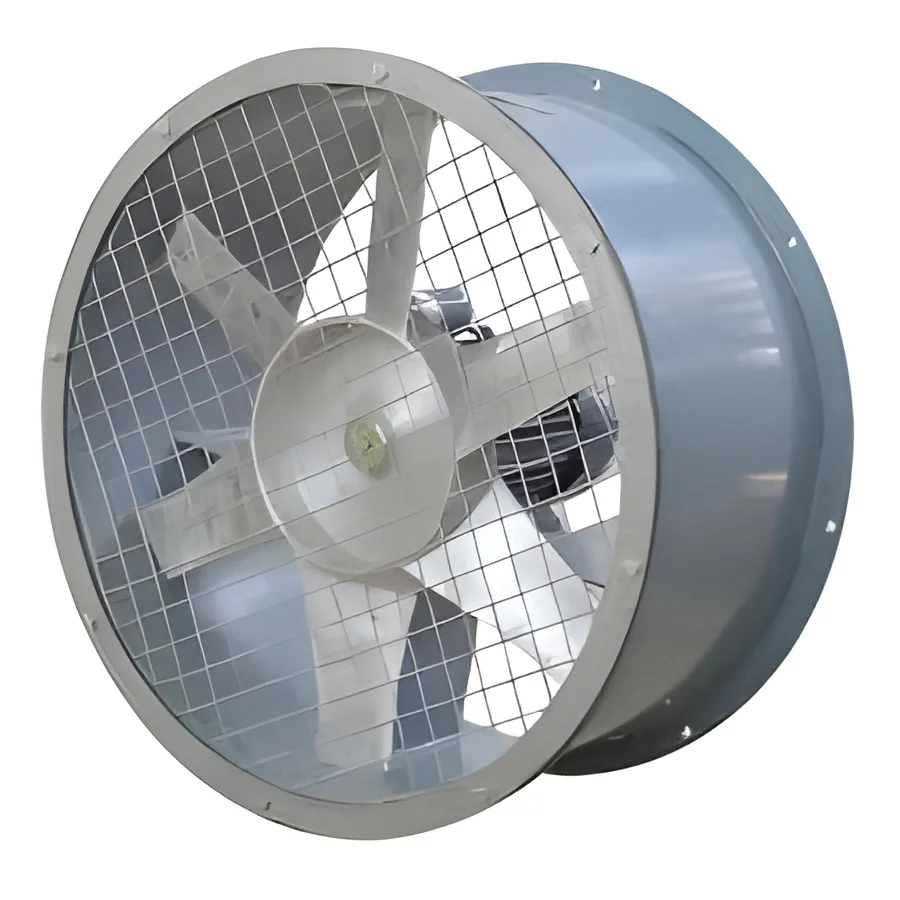
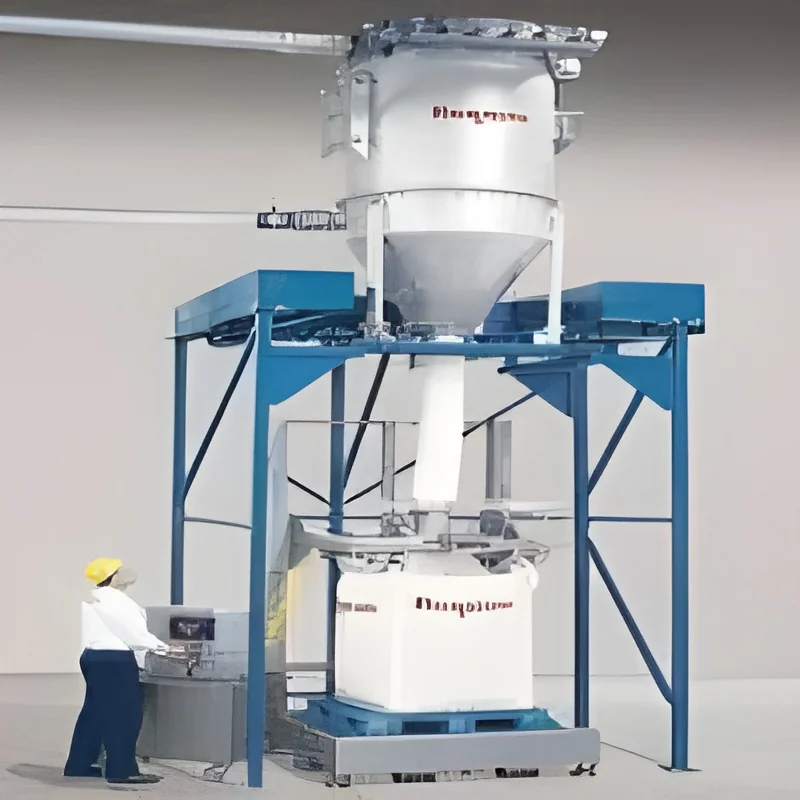
Our industrial pneumatic conveying equipment represents advanced technology for efficient bulk material handling, designed to transport dry materials through enclosed pipelines using air pressure. These systems ensure dust-free operation and minimal product contamination while handling powders, granules, and free-flowing materials with precision. Available as single or two-stage units, they accommodate various pressure applications and duty ranges, with drives configured as either direct coupled or belt driven with specialized impeller blades. The equipment provides reliable performance across diverse industrial applications with robust construction that withstands demanding environments while maintaining consistent material flow rates and operational efficiency.

These conveying systems find extensive application across multiple industries where efficient, clean material transfer is essential. In cement and construction, they handle various powders and aggregates with precision and re...
Our industrial pneumatic conveying equipment represents advanced technology for efficient bulk material handling, designed to transport dry materials through enclosed pipelines using air pressure. These systems ensure dust-free operation and minimal product contamination while handling powders, granules, and free-flowing materials with precision. Available as single or two-stage units, they accommodate various pressure applications and duty ranges, with drives configured as either direct coupled or belt driven with specialized impeller blades. The equipment provides reliable performance across diverse industrial applications with robust construction that withstands demanding environments while maintaining consistent material flow rates and operational efficiency.

These conveying systems find extensive application across multiple industries where efficient, clean material transfer is essential. In cement and construction, they handle various powders and aggregates with precision and reliability. Food processing facilities utilize them for hygienic transportation of ingredients and finished products under strict quality standards. Pharmaceutical manufacturers rely on these systems for contaminant-free transfer of active ingredients and excipients in controlled environments. Chemical plants employ them for safe handling of various powders and compounds, while plastic manufacturing facilities use them for resin and pellet transportation between processing stages.

The business value of our pneumatic conveying equipment lies in its proven reliability, operational efficiency, and performance consistency. These systems reduce operational costs through automated material handling, minimizing manual labor requirements and associated safety risks. Their enclosed design prevents material loss and environmental contamination, supporting regulatory compliance and sustainability initiatives. The equipment's durability ensures long service life with minimal downtime, while standardized configurations allow for effective integration into existing production lines. Operations benefit from improved process efficiency, reduced product waste, and enhanced workplace safety, making these systems a valuable investment for facilities requiring consistent bulk material transportation.

Key Features:
- Available as single or two stage units for different pressure requirements
- Direct coupled or belt driven configurations with specialized impeller blades
- Standardized designs for various material characteristics and flow properties
- Robust construction for continuous operation in demanding environments
- Enclosed pipeline system preventing dust emission and contamination

Benefits:
- Reduced operational costs through automated material handling
- Minimal product loss and environmental contamination prevention
- Long service life with reliable performance and minimal downtime
- Improved process efficiency and consistent material flow rates
- Enhanced workplace safety with enclosed dust-free operation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Pneumatic conveying equipment efficiently transports dry bulk materials through enclosed pipelines using air pressure, ensuring dust-free operation and minimal product degradation. These systems handle powders, granules, and free-flowing materials across industrial settings with flexible installation options for both short and long-distance transportation. Various configurations accommodate different material densities and flow properties while maintaining system integrity and performance efficiency in demanding environments.
These systems serve critical roles in industries requiring hygienic material transfer with minimal contamination risk. The enclosed design prevents environmental contamination while preserving product quality throughout transportation. Equipment configurations support different operational requirements, making them ideal for handling everything from fine powders to larger granules without compromising efficiency or reliability in continuous operations.
- Cement and construction materials transportation in manufacturing facilities
- Food grade powder handling in processing and packaging operations
- Pharmaceutical ingredient transfer in controlled environments
- Chemical powder conveyance in production and mixing processes
- Plastic pellet and resin transfer in molding and extrusion facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Dolar Gold Belts And Fans Pvt Ltd, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Pneumatic Conveying Equipment for Bulk Material Handling
Industrial pneumatic conveying equipment for bulk material handling offers reliable high-pressure and high-volume transport of powders and granules. Available as single or two-stage units for various industrial applications with proven performance and durability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Dolar Gold Belts And Fans Pvt Ltd
 West Bengal, India
Industrial Equipment & MachineryManufacturer