IN
₹
Apparel & Fashion
Description
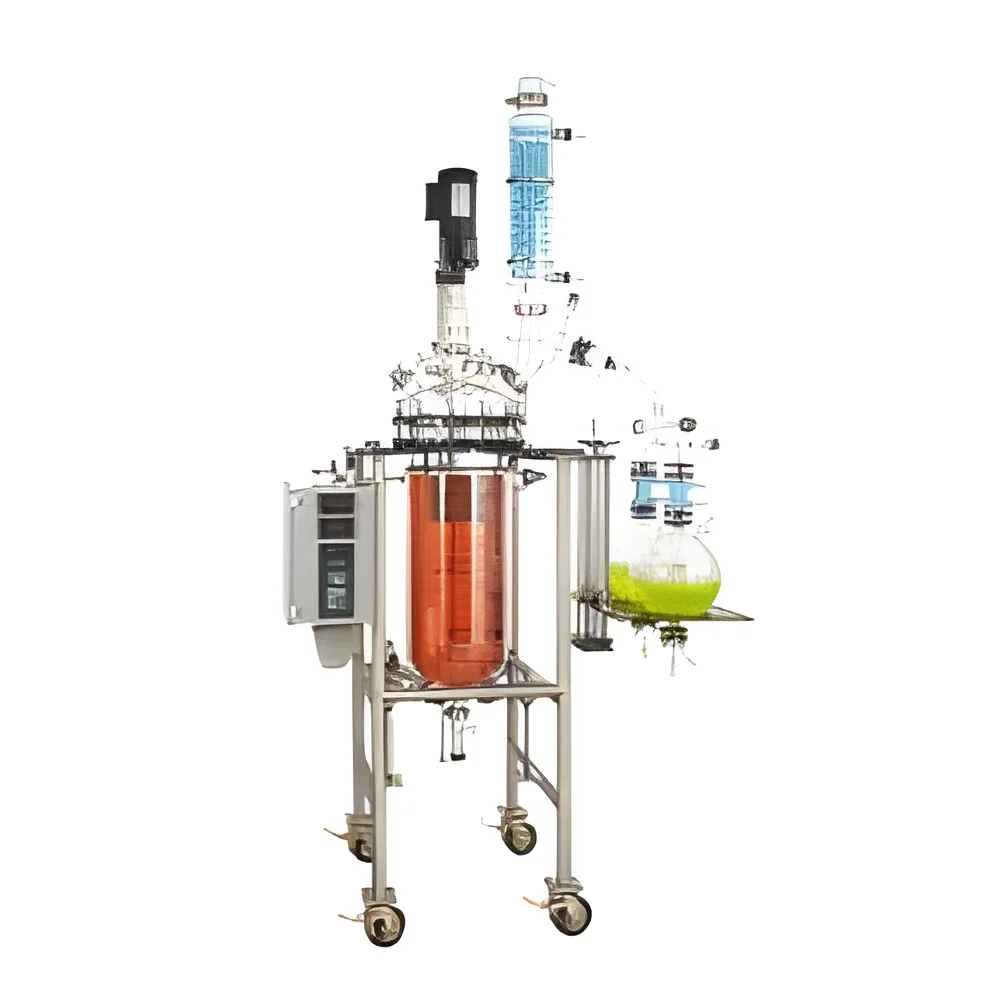
Our Industrial MS & FRP Lined Reactors represent advanced engineering solutions for chemical processing challenges. These reactors combine mild steel structural strength with fiber-reinforced plastic lining, creating a dual-protection system that withstands aggressive chemical environments while maintaining operational efficiency. Each unit undergoes comprehensive quality verification from material selection through final assembly, ensuring superior performance in demanding industrial applications. The precision engineering delivers optimal heat transfer, thorough mixing capability, and reliable operation suitable for continuous production cycles across various processing requirements.

These reactors serve essential functions across multiple industrial sectors including pharmaceutical manufacturing, chemical synthesis, fertilizer production, petrochemical processing, and environmental treatment systems. In pharmaceutical applications, they maintain strict purity standards while proces...
Our Industrial MS & FRP Lined Reactors represent advanced engineering solutions for chemical processing challenges. These reactors combine mild steel structural strength with fiber-reinforced plastic lining, creating a dual-protection system that withstands aggressive chemical environments while maintaining operational efficiency. Each unit undergoes comprehensive quality verification from material selection through final assembly, ensuring superior performance in demanding industrial applications. The precision engineering delivers optimal heat transfer, thorough mixing capability, and reliable operation suitable for continuous production cycles across various processing requirements.

These reactors serve essential functions across multiple industrial sectors including pharmaceutical manufacturing, chemical synthesis, fertilizer production, petrochemical processing, and environmental treatment systems. In pharmaceutical applications, they maintain strict purity standards while processing corrosive intermediates and active ingredients. Chemical manufacturing facilities utilize them for acid-base reactions, polymerization processes, and solvent-based operations requiring corrosion resistance. The fertilizer industry depends on their durable construction for producing ammonium compounds and phosphoric acid derivatives, while petrochemical operations employ them in hydrocarbon processing and specialized catalyst reactions requiring robust equipment.

The operational value of these reactors lies in their proven reliability, reduced maintenance demands, and extended service life under challenging conditions. The robust construction minimizes operational downtime and replacement costs, while the corrosion-resistant lining prevents product contamination and ensures consistent output quality. The engineering design supports efficient heat transfer and mixing performance, enhancing process control and production outcomes. These reactors deliver dependable performance in critical processing applications, supporting operational continuity and safety standards while meeting international quality requirements for industrial equipment.

Key Features:
- Dual-layer construction combining mild steel exterior with FRP interior lining
- Corrosion-resistant design for handling aggressive chemical substances
- Precision engineering for optimal heat transfer and mixing efficiency
- Rigorous quality testing throughout manufacturing and assembly processes
- Structural durability for continuous operation in demanding environments

Benefits:
- Extended equipment service life with reduced maintenance requirements
- Consistent product quality through corrosion-resistant interior protection
- Enhanced operational safety during chemical processing operations
- Improved heat transfer efficiency for better process control
- Reliable performance in continuous production cycles
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
MS & FRP lined reactors deliver exceptional performance in handling corrosive chemicals and high-temperature processes across industrial sectors. Their robust dual-layer construction ensures safe operation with aggressive substances including acids, alkalis, and solvents, maintaining material integrity in demanding production environments where reliability is paramount.
These reactors serve pharmaceutical manufacturing, chemical processing, fertilizer production, petrochemical refining, and wastewater treatment with consistent results. They support critical operations including mixing, reaction control, distillation, and polymerization while maintaining structural stability under extreme conditions, ensuring long-term operational efficiency with minimal maintenance requirements.
- Chemical manufacturing plants for acid neutralization and synthesis reactions
- Pharmaceutical facilities for drug intermediate processing and purification
- Fertilizer production units for handling corrosive compounds and formulations
- Petrochemical refineries for hydrocarbon processing and catalyst reactions
- Industrial wastewater treatment plants for aggressive effluent management
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aarathi Engineers, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory Size1000-5000 sqm
Annual Production Capacity0
Main Markets
North America
Oceania
Northern Europe
South America
Mid East
Southern Europe
Eastern Europe
Eastern Asia
South Asia
Southeast Asia
Western Europe
Africa
Central America
Domestic
Industrial MS & FRP Lined Reactors For Chemical Processing
Industrial MS & FRP lined reactors provide corrosion-resistant chemical processing with reliable performance for pharmaceuticals, fertilizers, and petrochemical industries. Built for demanding applications with tested materials and structural durability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aarathi Engineers
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer