IN
₹
Apparel & Fashion

Description
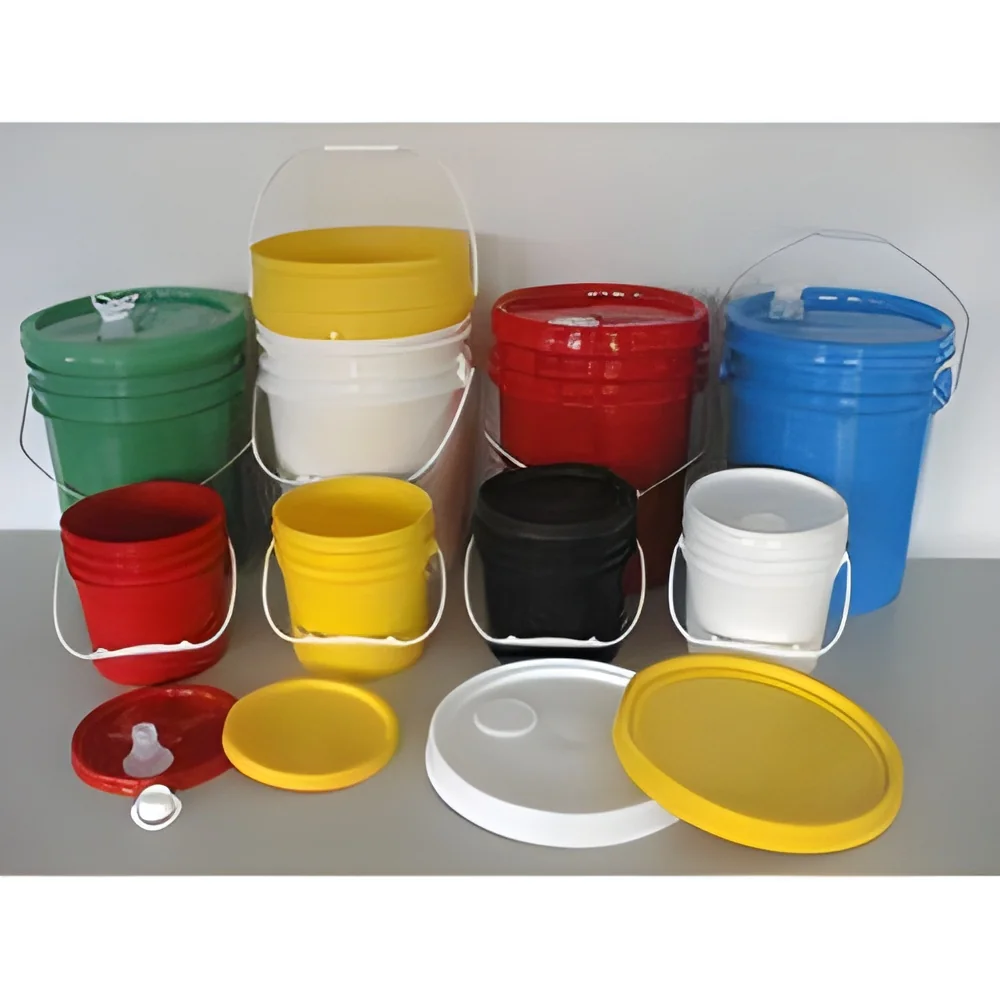
Our premium chemical buckets represent the industry standard for industrial chemical storage solutions, specifically engineered for businesses that demand maximum reliability and safety. These buckets are constructed from high-grade materials that provide exceptional corrosion resistance and structural integrity, ensuring long-term performance even with the most aggressive chemicals. Available in various sizes and configurations, they offer versatile storage options while maintaining consistent quality and durability across all variants. The design focuses on practical usability with secure lids, comfortable handles, and stackable features that optimize space and handling efficiency in industrial settings, making them ideal for operations that prioritize safety and operational efficiency.

These chemical buckets serve critical roles across multiple industries where safe chemical handling is absolutely essential. Chemical processing plants utilize them for intermediate storage and in-pr...
Our premium chemical buckets represent the industry standard for industrial chemical storage solutions, specifically engineered for businesses that demand maximum reliability and safety. These buckets are constructed from high-grade materials that provide exceptional corrosion resistance and structural integrity, ensuring long-term performance even with the most aggressive chemicals. Available in various sizes and configurations, they offer versatile storage options while maintaining consistent quality and durability across all variants. The design focuses on practical usability with secure lids, comfortable handles, and stackable features that optimize space and handling efficiency in industrial settings, making them ideal for operations that prioritize safety and operational efficiency.

These chemical buckets serve critical roles across multiple industries where safe chemical handling is absolutely essential. Chemical processing plants utilize them for intermediate storage and in-process material transfer while maintaining purity and preventing contamination throughout manufacturing operations. Water treatment facilities depend on them for handling treatment chemicals like chlorine and coagulants safely during water purification processes. Pharmaceutical manufacturers employ them for raw material storage and processing applications where material integrity and contamination control are crucial. Laboratories and research facilities rely on them for safe storage of reagents and solvents, while industrial cleaning operations use them for concentrated cleaning solutions and chemical waste collection in various maintenance scenarios.

For businesses that handle chemicals regularly, these buckets deliver significant operational value through enhanced safety protocols, reduced replacement costs, and improved handling efficiency. The leak-proof design prevents costly spills and contamination incidents that could lead to production downtime or safety hazards, while the corrosion-resistant construction ensures long service life even with aggressive substances, providing excellent return on investment. The robust construction withstands industrial handling and transportation demands, reducing damage and loss while maintaining chemical integrity throughout the storage period, making them a smart investment for any chemical-dependent operation.

Key Features:
- Premium corrosion-resistant construction for long-lasting durability with aggressive chemicals
- Multiple size options and configurations to meet specific operational requirements
- Secure leak-proof design that prevents contamination and ensures workplace safety
- Stackable design with comfortable handles for efficient space utilization and easy handling
- High-grade materials that maintain structural integrity under demanding industrial conditions

Benefits:
- Enhanced workplace safety through reliable containment of hazardous materials
- Long service life reduces replacement costs and maintenance requirements
- Efficient space utilization through stackable design optimizes storage areas
- Prevents costly spills and contamination incidents in industrial settings
- Reliable performance ensures consistent chemical handling across operations
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial chemical buckets provide secure storage and handling for aggressive chemicals including acids, solvents, and corrosive fluids. They feature robust construction with superior leak-proof design to prevent contamination and ensure workplace safety in demanding industrial environments. These buckets withstand harsh conditions and frequent use while offering reliable containment for hazardous materials throughout various industrial processes and operations.
The durable construction ensures long service life even with the most aggressive chemical substances, making them ideal for manufacturing plants, treatment facilities, and industrial operations that require dependable chemical storage solutions. The reliable performance and safety features make these buckets suitable for handling various corrosive materials across different industrial settings and applications.
- Chemical manufacturing plants use these buckets for safe storage and transport of raw materials and finished chemical products
- Water treatment facilities rely on them for handling chlorine, alum, and other treatment chemicals securely and without contamination
- Pharmaceutical companies utilize these buckets for intermediate storage and in-process material handling during manufacturing
- Laboratories depend on them for storing and moving acids, solvents, and chemical reagents safely within research environments
- Industrial cleaning and maintenance operations use these buckets for concentrated cleaning agents and chemical waste collection
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Balaji Industries, New Delhi
 New Delhi, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Chemical Buckets For Acids Solvents Corrosive Fluids
Premium industrial chemical buckets for safe storage of acids, solvents, and corrosive fluids. Corrosion-resistant construction ensures durability in demanding environments. Trusted by manufacturers worldwide for reliable chemical handling solutions.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Balaji Industries
 New Delhi, India
Industrial Equipment & MachineryManufacturer