IN
₹
Apparel & Fashion

Description
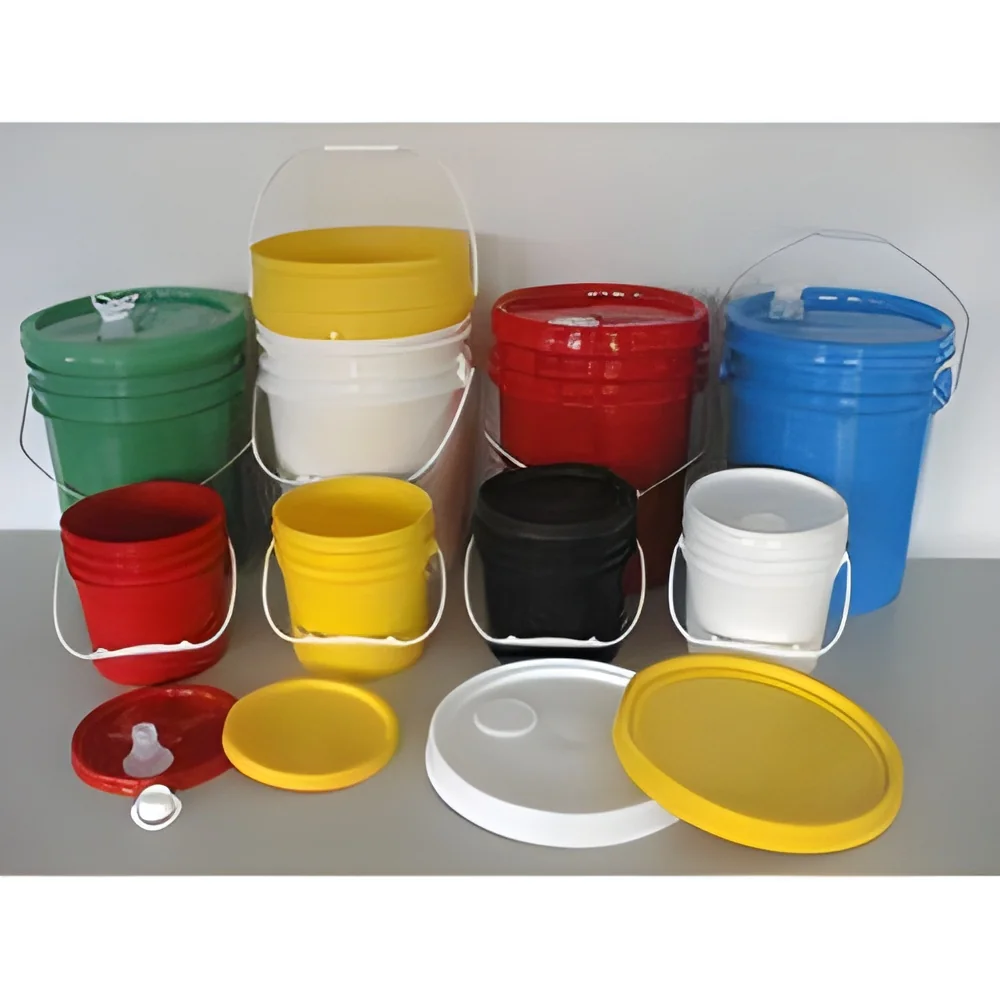
We manufacture premium food grade plastic buckets specifically designed for demanding industrial storage applications. Our containers are crafted from certified food-grade materials that meet rigorous safety standards, making them ideal for storing sensitive materials without contamination risks. These buckets are engineered to withstand heavy loads, challenging handling conditions, and repeated use while maintaining structural integrity and performance reliability. The robust construction ensures long-term durability while providing superior protection for valuable materials throughout storage and transportation processes, delivering confidence for quality-focused operations that require dependable containment solutions.

These food grade plastic buckets serve essential functions across multiple industries where material purity and secure storage are paramount. Construction professionals depend on them for secure cement and building material storage that prevents moisture contaminatio...
We manufacture premium food grade plastic buckets specifically designed for demanding industrial storage applications. Our containers are crafted from certified food-grade materials that meet rigorous safety standards, making them ideal for storing sensitive materials without contamination risks. These buckets are engineered to withstand heavy loads, challenging handling conditions, and repeated use while maintaining structural integrity and performance reliability. The robust construction ensures long-term durability while providing superior protection for valuable materials throughout storage and transportation processes, delivering confidence for quality-focused operations that require dependable containment solutions.

These food grade plastic buckets serve essential functions across multiple industries where material purity and secure storage are paramount. Construction professionals depend on them for secure cement and building material storage that prevents moisture contamination. Agricultural operations utilize them for fertilizer and chemical containment that protects against spillage and environmental exposure. Food processors rely on them for ingredient preservation that maintains freshness and prevents contamination. Chemical manufacturers benefit from their contamination-resistant properties for sensitive raw materials, while pharmaceutical companies use them for components requiring hygienic storage conditions. This versatility makes them indispensable equipment for businesses requiring safe, dependable bulk storage solutions across diverse operational environments.

The business value of our food grade plastic buckets lies in their exceptional reliability and operational cost-effectiveness. These containers represent a smart investment that reduces long-term expenses through their reusable nature and extended service life, eliminating the need for frequent replacements. They enhance supply chain efficiency by ensuring product safety during storage and transit, minimizing material waste, and simplifying handling processes through standardized designs. The food-grade certification provides assurance for sensitive applications where material purity is non-negotiable, while the durable construction delivers consistent performance under demanding industrial conditions. This combination of safety certification, durability, and practical design delivers outstanding return on investment for businesses seeking reliable storage solutions that protect their materials and streamline their operations.

Key Features:
- Certified food-grade plastic material ensuring safety and regulatory compliance
- Heavy-duty construction engineered specifically for industrial bulk storage applications
- Leak-proof and corrosion-resistant properties for secure material containment
- Stackable design optimizing storage space and transportation efficiency
- Durable material formulation withstands heavy loads and repeated handling cycles

Benefits:
- Ensures contamination-free storage for sensitive materials and ingredients
- Reduces operational costs through reusable design and extended service life
- Enhances supply chain efficiency with reliable product protection during transit
- Saves valuable storage space with practical, secure stackable design
- Provides peace of mind with certified food-grade safety standards and compliance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our food grade plastic buckets are engineered for robust bulk storage across demanding industrial environments. These containers offer secure, contamination-free storage for a wide range of materials, from dry powders to semi-solids, ensuring product integrity during handling, warehousing, and transportation. They meet stringent industry standards for safety and durability, providing reliable performance in commercial and industrial settings where material protection is critical.
These versatile buckets accommodate various industrial needs with their strong construction that withstands rigorous handling. The design maintains structural stability for repeated use across different operational cycles, making them suitable for multiple sectors. Industries including construction, agriculture, food processing, chemical manufacturing, and pharmaceuticals benefit from their consistent performance and ability to preserve material quality from production through to distribution.
- Bulk storage and transportation of cement, plaster, and construction compounds
- Safe containment and handling of fertilizers, pesticides, and agricultural chemicals
- Storage of food ingredients, grains, spices, and semi-processed food items
- Industrial chemical storage requiring leak-proof and corrosion-resistant properties
- Pharmaceutical and laboratory raw material storage ensuring compliance with hygiene standards
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Balaji Industries, New Delhi
 New Delhi, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Food Grade Plastic Buckets For Bulk Industrial Storage
Food Grade Plastic Buckets provide bulk industrial storage for cement, fertilizers, and materials. Durable, reliable containers ensure safe handling and contamination-free storage across various industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Balaji Industries
 New Delhi, India
Industrial Equipment & MachineryManufacturer