IN
₹
Apparel & Fashion
Description
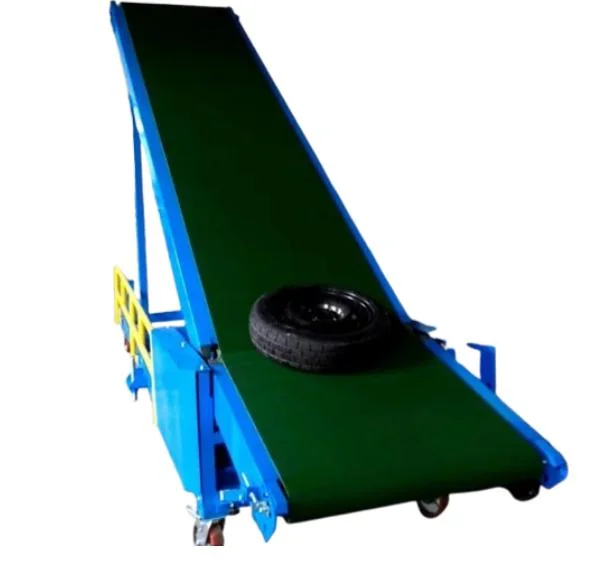
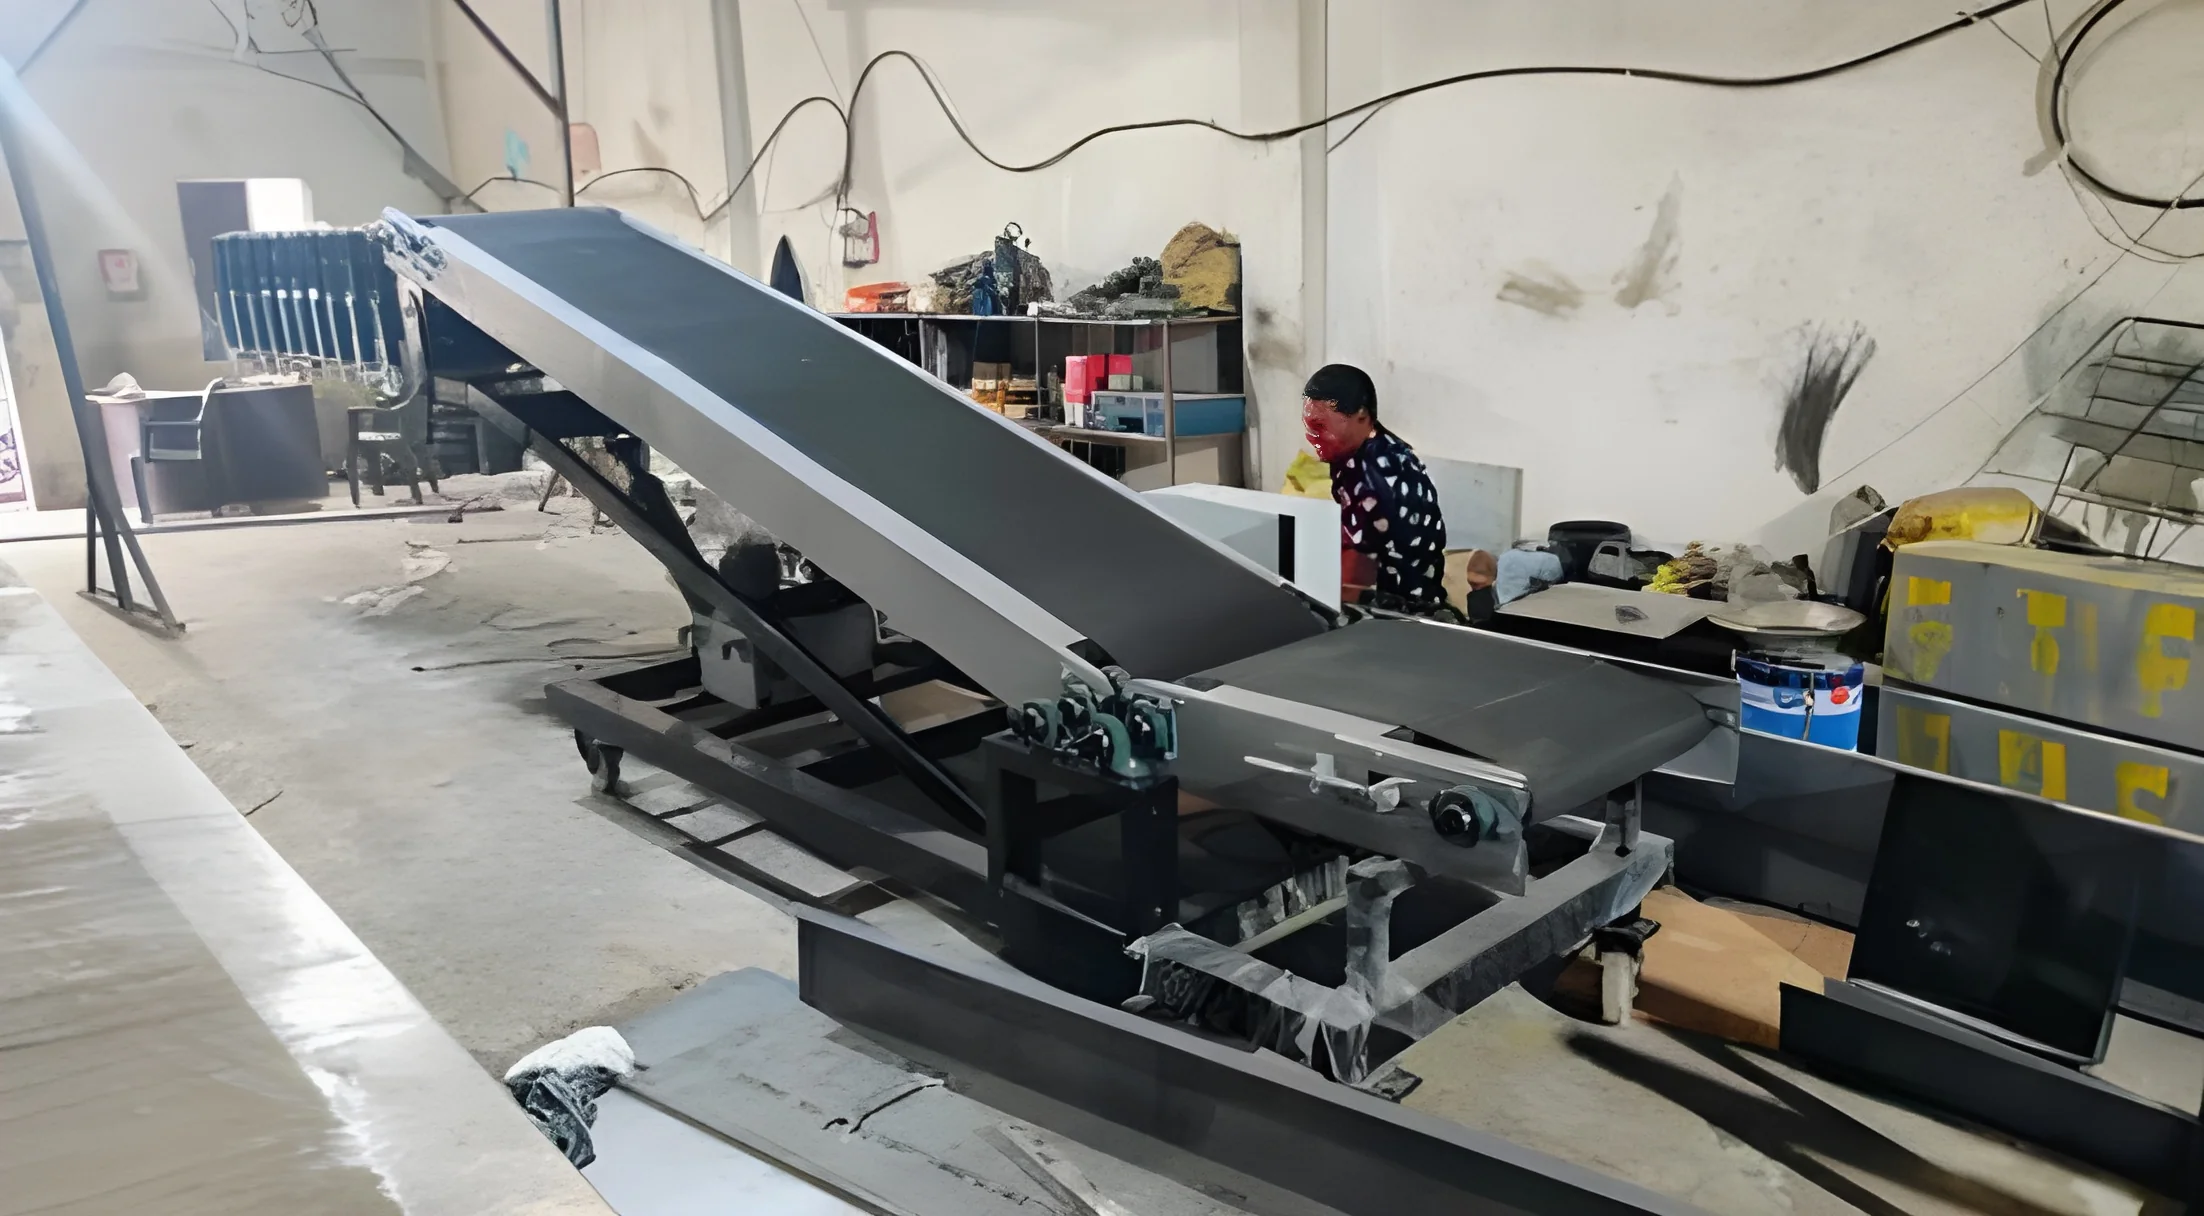
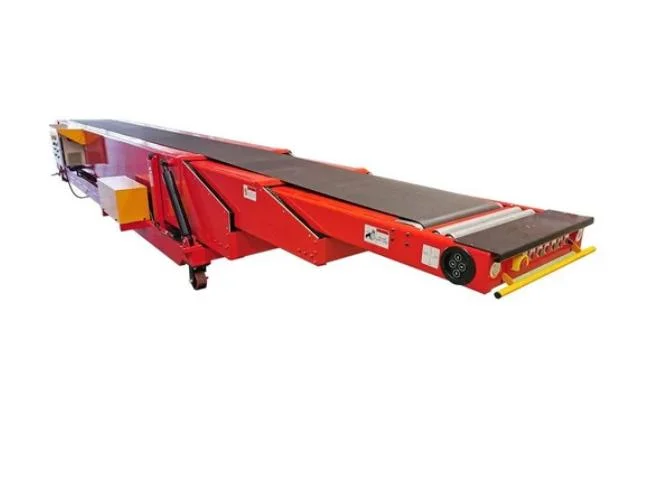
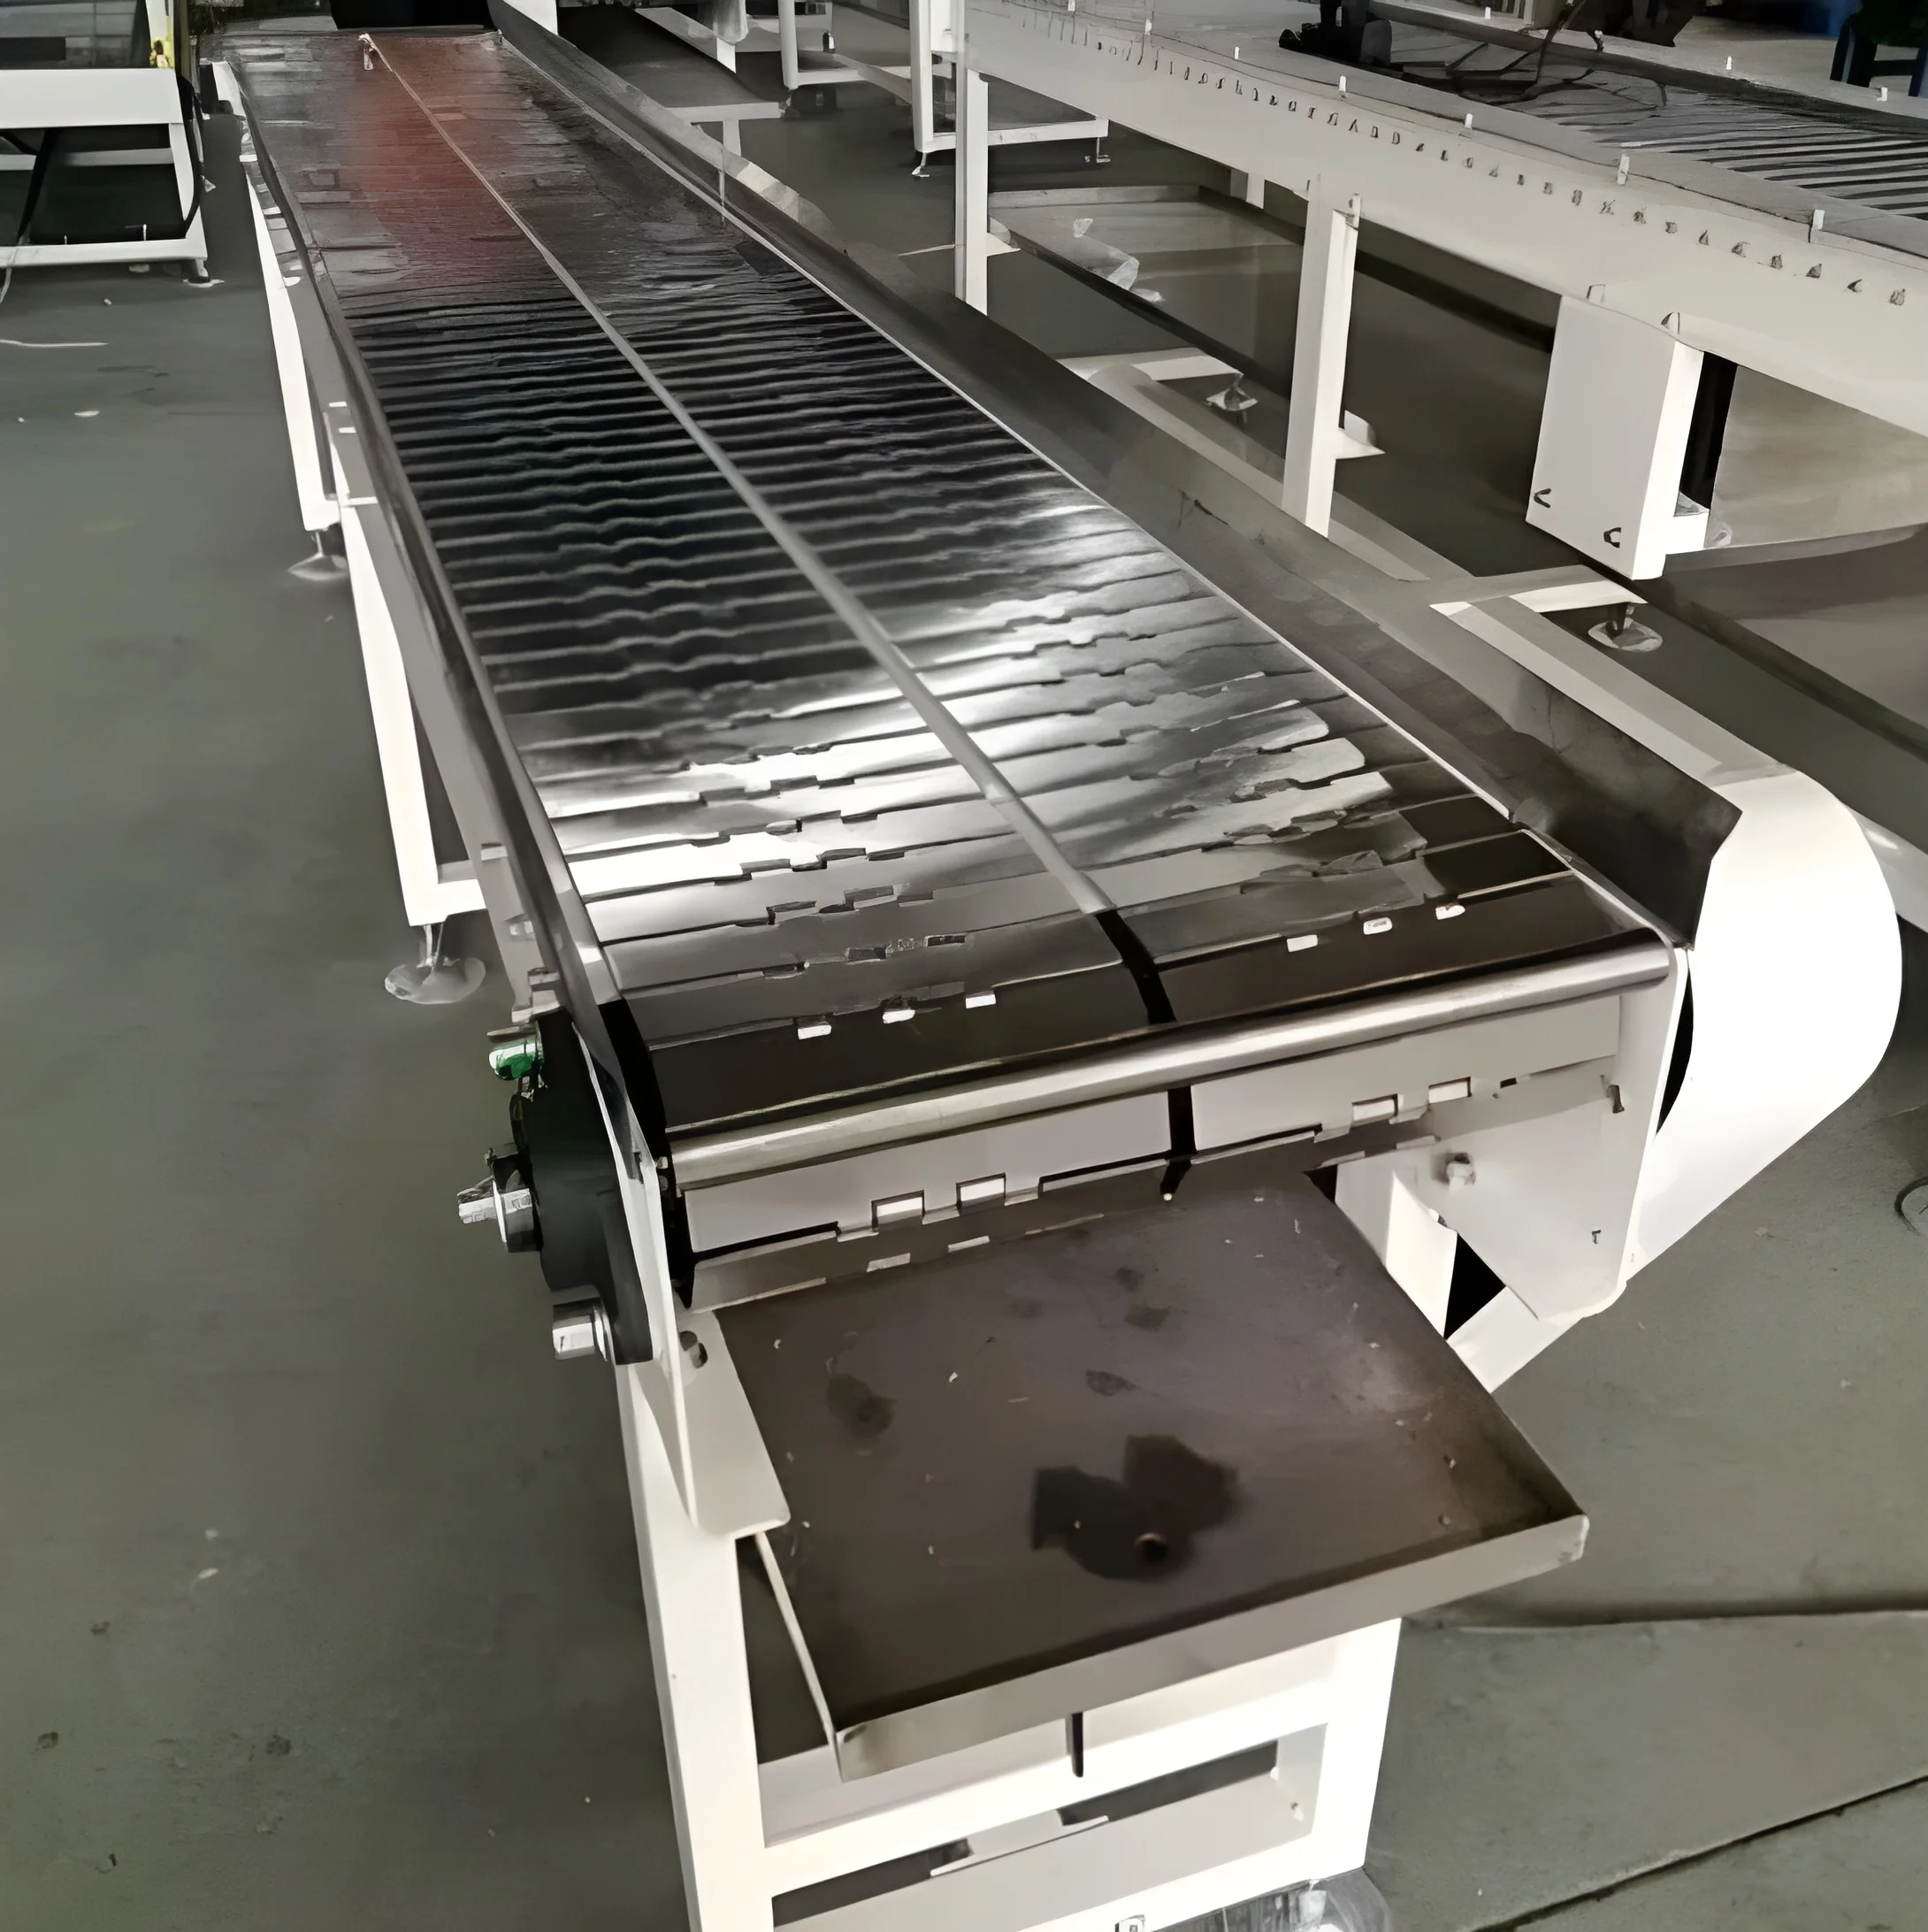
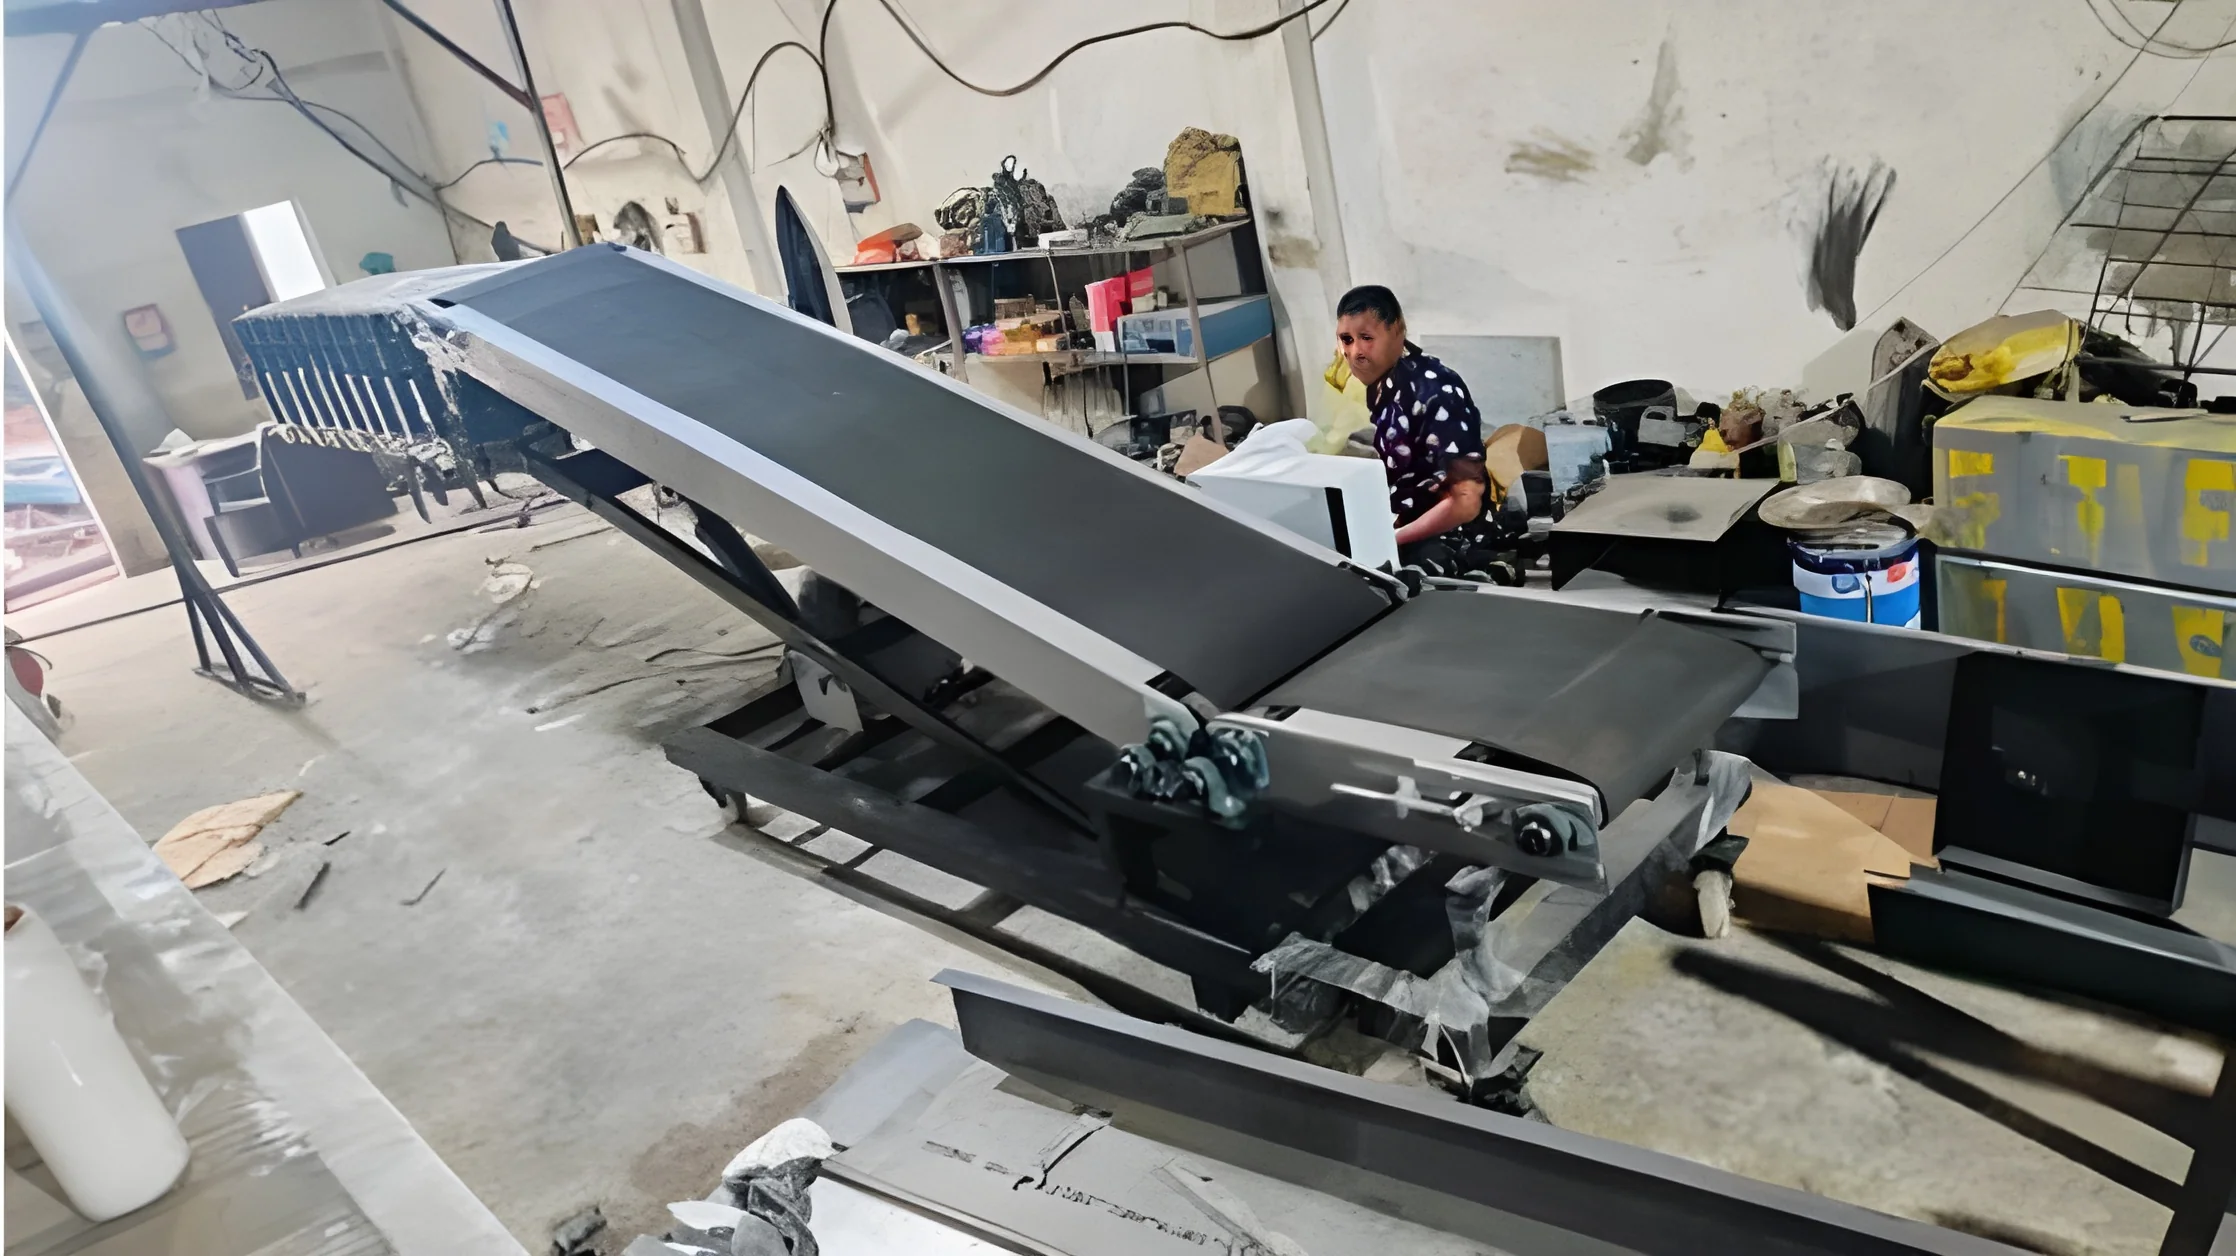
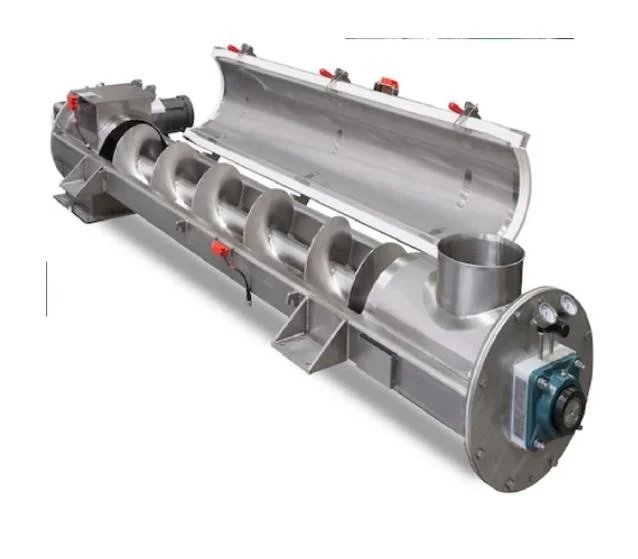
Our Industrial Vertical Screw Conveyor represents advanced bulk material handling technology designed for demanding industrial applications. With a 5-meter vertical reach and 200 kg load capacity, this robust system efficiently transports various materials upward through production facilities. Constructed from high-quality mild steel, the conveyor ensures durability and long-term reliability in challenging environments. The automatic operation eliminates manual handling while maintaining consistent material flow, making it an ideal solution for businesses looking to optimize vertical material movement between different production levels. The design focuses on simplicity and efficiency, ensuring that even complex vertical transport needs are met with minimal operational complexity and maximum reliability.

This vertical screw conveyor serves multiple industries across various sectors, including food processing, pharmaceuticals, chemical manufacturing, construction materials, and agricul...
Our Industrial Vertical Screw Conveyor represents advanced bulk material handling technology designed for demanding industrial applications. With a 5-meter vertical reach and 200 kg load capacity, this robust system efficiently transports various materials upward through production facilities. Constructed from high-quality mild steel, the conveyor ensures durability and long-term reliability in challenging environments. The automatic operation eliminates manual handling while maintaining consistent material flow, making it an ideal solution for businesses looking to optimize vertical material movement between different production levels. The design focuses on simplicity and efficiency, ensuring that even complex vertical transport needs are met with minimal operational complexity and maximum reliability.

This vertical screw conveyor serves multiple industries across various sectors, including food processing, pharmaceuticals, chemical manufacturing, construction materials, and agricultural processing. In food processing plants, it safely moves grains, powders, and ingredients between floors with precision. Pharmaceutical facilities utilize it for controlled substance transfer between production stages while maintaining product integrity. Chemical plants rely on its robust construction to handle various compounds safely, while construction material manufacturers use it for cement, sand, and other building materials. The system's versatility makes it suitable for any industry requiring efficient vertical bulk material transport with limited space availability and consistent performance.

The business value of our Vertical Screw Conveyor lies in its reliability, efficiency, and cost-effectiveness. By automating vertical material transport, businesses significantly reduce labor costs and minimize manual handling errors. The system's durable mild steel construction ensures long service life with minimal maintenance requirements, providing excellent return on investment. The automatic operation ensures consistent performance without constant supervision, enhancing operational efficiency. This conveyor streamlines material flow between different production levels, ultimately contributing to increased productivity and reduced operational costs while maintaining high safety standards and operational consistency.

Key Features:
- 5-meter vertical conveyor length for extensive reach capabilities
- 200 kg load capacity handling substantial material volumes
- Mild steel construction ensuring durability and longevity
- Automatic operation for consistent material flow
- Compact design suitable for space-constrained environments

Benefits:
- Reduces labor costs through automated material handling
- Minimizes manual handling errors and improves safety
- Provides long service life with minimal maintenance requirements
- Enhances operational efficiency and productivity
- Ensures consistent performance in demanding industrial conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | 106 |
Application
Vertical Screw Conveyors provide efficient bulk material handling solutions where floor space is limited. These systems offer reliable vertical transport for powders, granules, and various materials that need movement between different production levels without manual intervention. The compact design and automatic operation make them ideal for modern manufacturing facilities seeking workflow optimization and reduced operational costs.
These conveyors serve multiple industries including food processing, pharmaceuticals, chemicals, construction materials, and agricultural processing. They handle diverse materials from food grains and powders to cement and industrial compounds. The vertical orientation allows flexible installation in tight spaces while maintaining consistent material flow between different levels of production facilities, ensuring smooth operational continuity.
- Transporting flour and grains between production levels in food processing facilities
- Moving pharmaceutical powders between mixing and packaging floors with precision
- Handling cement and construction materials in building material manufacturing plants
- Transferring chemical compounds between processing stages in chemical facilities
- Elevating agricultural products like seeds and grains in processing operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
A R Engineering , Madhya Pradesh
 Madhya Pradesh, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Vertical Screw Conveyor 5m 200kg Capacity Bulk Material Transport
Industrial Vertical Screw Conveyor 5m length 200kg capacity bulk material transport system. Durable mild steel construction ensures reliable performance for industrial material handling applications across various sectors.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
A R Engineering 
 Madhya Pradesh, India
Industrial Equipment & MachineryManufacturer