IN
₹
Apparel & Fashion
Description
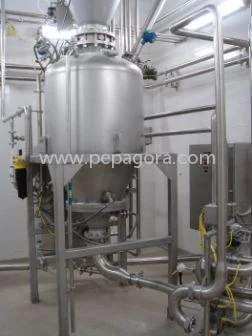
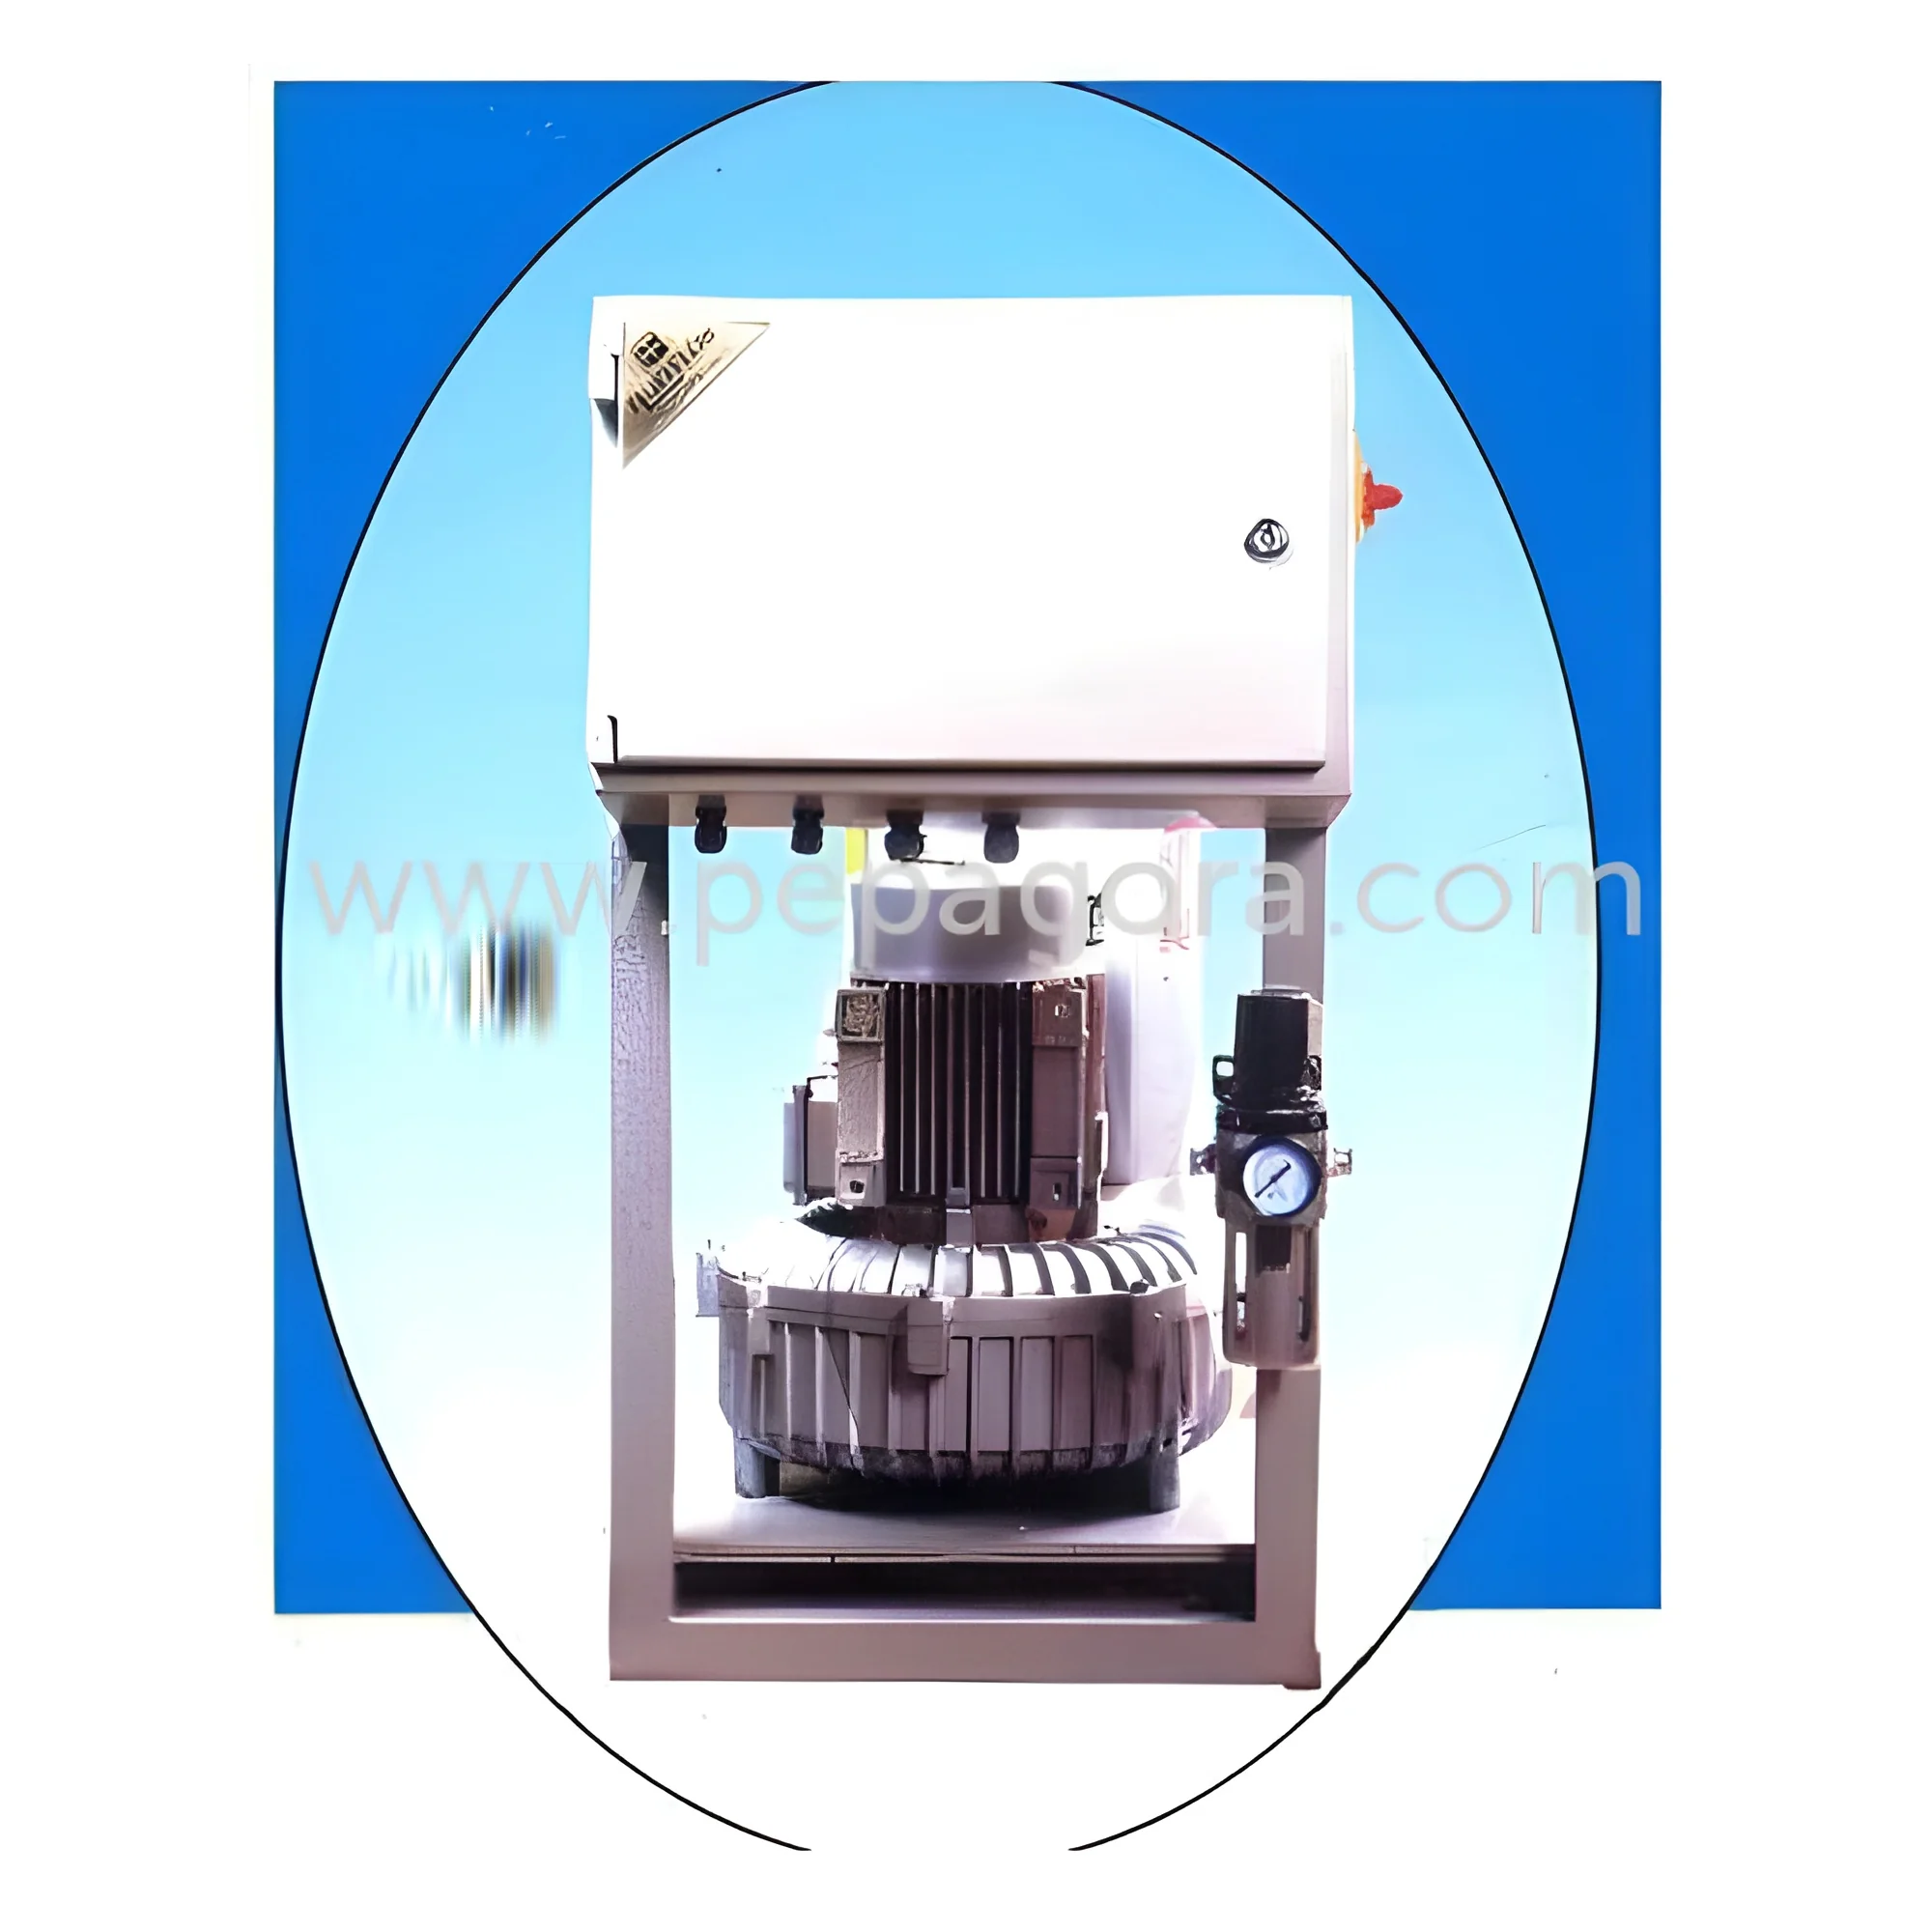
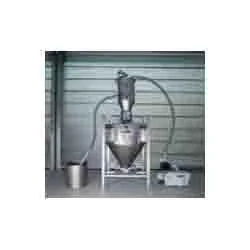
Our industrial vacuum conveying equipment represents advanced material handling technology designed for efficient transfer of powders, granules, and bulk materials in demanding manufacturing environments. Constructed from high-quality stainless steel with heat-resistant properties, these OEM metal conveyors ensure reliable performance and long-lasting durability. The enclosed system provides dust-free operation, maintaining product purity while preventing contamination risks. With precise tolerance control and customizable dimensions, these conveyors integrate seamlessly into existing production lines, offering versatile solutions for various industrial material transfer requirements. The standard design combines robust construction with operational efficiency, delivering consistent performance that meets the rigorous demands of modern manufacturing facilities.

These vacuum conveying systems serve critical functions across multiple industrial sectors including pharmaceuticals, food pr...
Our industrial vacuum conveying equipment represents advanced material handling technology designed for efficient transfer of powders, granules, and bulk materials in demanding manufacturing environments. Constructed from high-quality stainless steel with heat-resistant properties, these OEM metal conveyors ensure reliable performance and long-lasting durability. The enclosed system provides dust-free operation, maintaining product purity while preventing contamination risks. With precise tolerance control and customizable dimensions, these conveyors integrate seamlessly into existing production lines, offering versatile solutions for various industrial material transfer requirements. The standard design combines robust construction with operational efficiency, delivering consistent performance that meets the rigorous demands of modern manufacturing facilities.

These vacuum conveying systems serve critical functions across multiple industrial sectors including pharmaceuticals, food processing, chemicals, plastics manufacturing, and agricultural processing. In pharmaceutical applications, the equipment handles active ingredients and excipients while maintaining sterile conditions essential for product quality. Food manufacturers utilize these systems for hygienic transfer of ingredients such as flour, sugar, and food additives, ensuring compliance with industry standards. Chemical plants benefit from the safe handling of granular compounds and additives, while plastic manufacturers efficiently convey pellets and resins. The equipment's versatility and reliability make it indispensable in operations where material purity, transfer efficiency, and consistent performance are paramount to production success.

The business value of our vacuum conveying equipment lies in its exceptional reliability, durable construction, and operational efficiency that directly impacts bottom-line results. These systems significantly reduce operational costs by minimizing product loss, decreasing maintenance requirements, and improving overall production throughput. The stainless steel construction ensures extended service life even in challenging industrial environments, providing excellent return on investment through reduced replacement frequency and downtime. Custom tolerance control and dimension flexibility allow for perfect integration into existing production infrastructure, while the OEM support ensures compatibility and performance consistency. With reliable on-time delivery and proven performance characteristics, businesses can trust these systems to enhance their material handling processes while maintaining the highest quality standards.

Key Features:
- Stainless steel construction with heat-resistant properties
- Inclining conveyor structure for efficient material flow
- OEM metal design ensuring reliability and durability
- Precise tolerance control as per client specifications
- Enclosed system providing dust-free operation

Benefits:
- Reduced product loss and contamination risks
- Lower maintenance requirements and operational costs
- Extended service life in demanding industrial environments
- Improved production efficiency and throughput
- Seamless integration with existing production systems
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Heat Resistant |
| Structure | Inclining Conveyor |
| Supply Type | OEM |
| Price | Negotiable |
| Type | Conveyor |
| Material Type | Metal |
| Features | Reliable and Durable |
| Standard or Non Standard | Standard |
| Condition | New |
| Tolerance | As per Clients Request |
| Delivery | On Time Delivery |
| Size | As per Customer required |
| Dimension | As per Customer required |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This industrial vacuum conveying system efficiently handles powders, granules, and bulk materials across diverse production environments. The enclosed stainless steel design ensures dust-free operation while maintaining product integrity and preventing contamination. With heat-resistant properties and reliable performance, it delivers consistent material transfer with minimal maintenance requirements, making it ideal for continuous production operations where uptime is critical for success. The robust construction withstands demanding conditions while ensuring long-term durability and operational efficiency.
The inclining conveyor structure facilitates smooth material flow while the OEM construction ensures compatibility with various production systems. These units handle materials with exceptional efficiency while reducing product degradation risks. The precise tolerance control allows for accurate material handling, and the durable design supports continuous operation with minimal downtime. This provides dependable service in challenging industrial environments where material transfer efficiency directly impacts production outcomes and overall operational performance.
- Pharmaceutical manufacturing for handling powders and granules in tablet production lines
- Food processing plants transferring ingredients like flour, sugar, and food additives
- Chemical industry operations moving granular compounds and industrial additives
- Plastic manufacturing facilities conveying pellets, resins, and polymer materials
- Agricultural processing operations handling grains, feed materials, and bulk commodities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Fluid Flow Systems, Tamil Nadu
 Tamil Nadu, India
Raw Materials & Chemicals•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Vacuum Conveying Equipment Stainless Steel Durable OEM
Industrial vacuum conveying equipment features stainless steel construction for efficient material transfer. This OEM metal conveyor offers heat-resistant design, reliable performance, and precise tolerance control for manufacturing applications.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Fluid Flow Systems
 Tamil Nadu, India
Raw Materials & ChemicalsManufacturer