IN
₹
Apparel & Fashion

Description
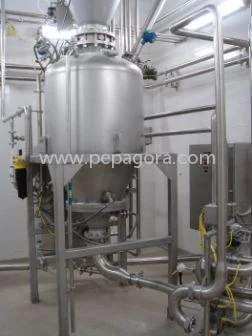
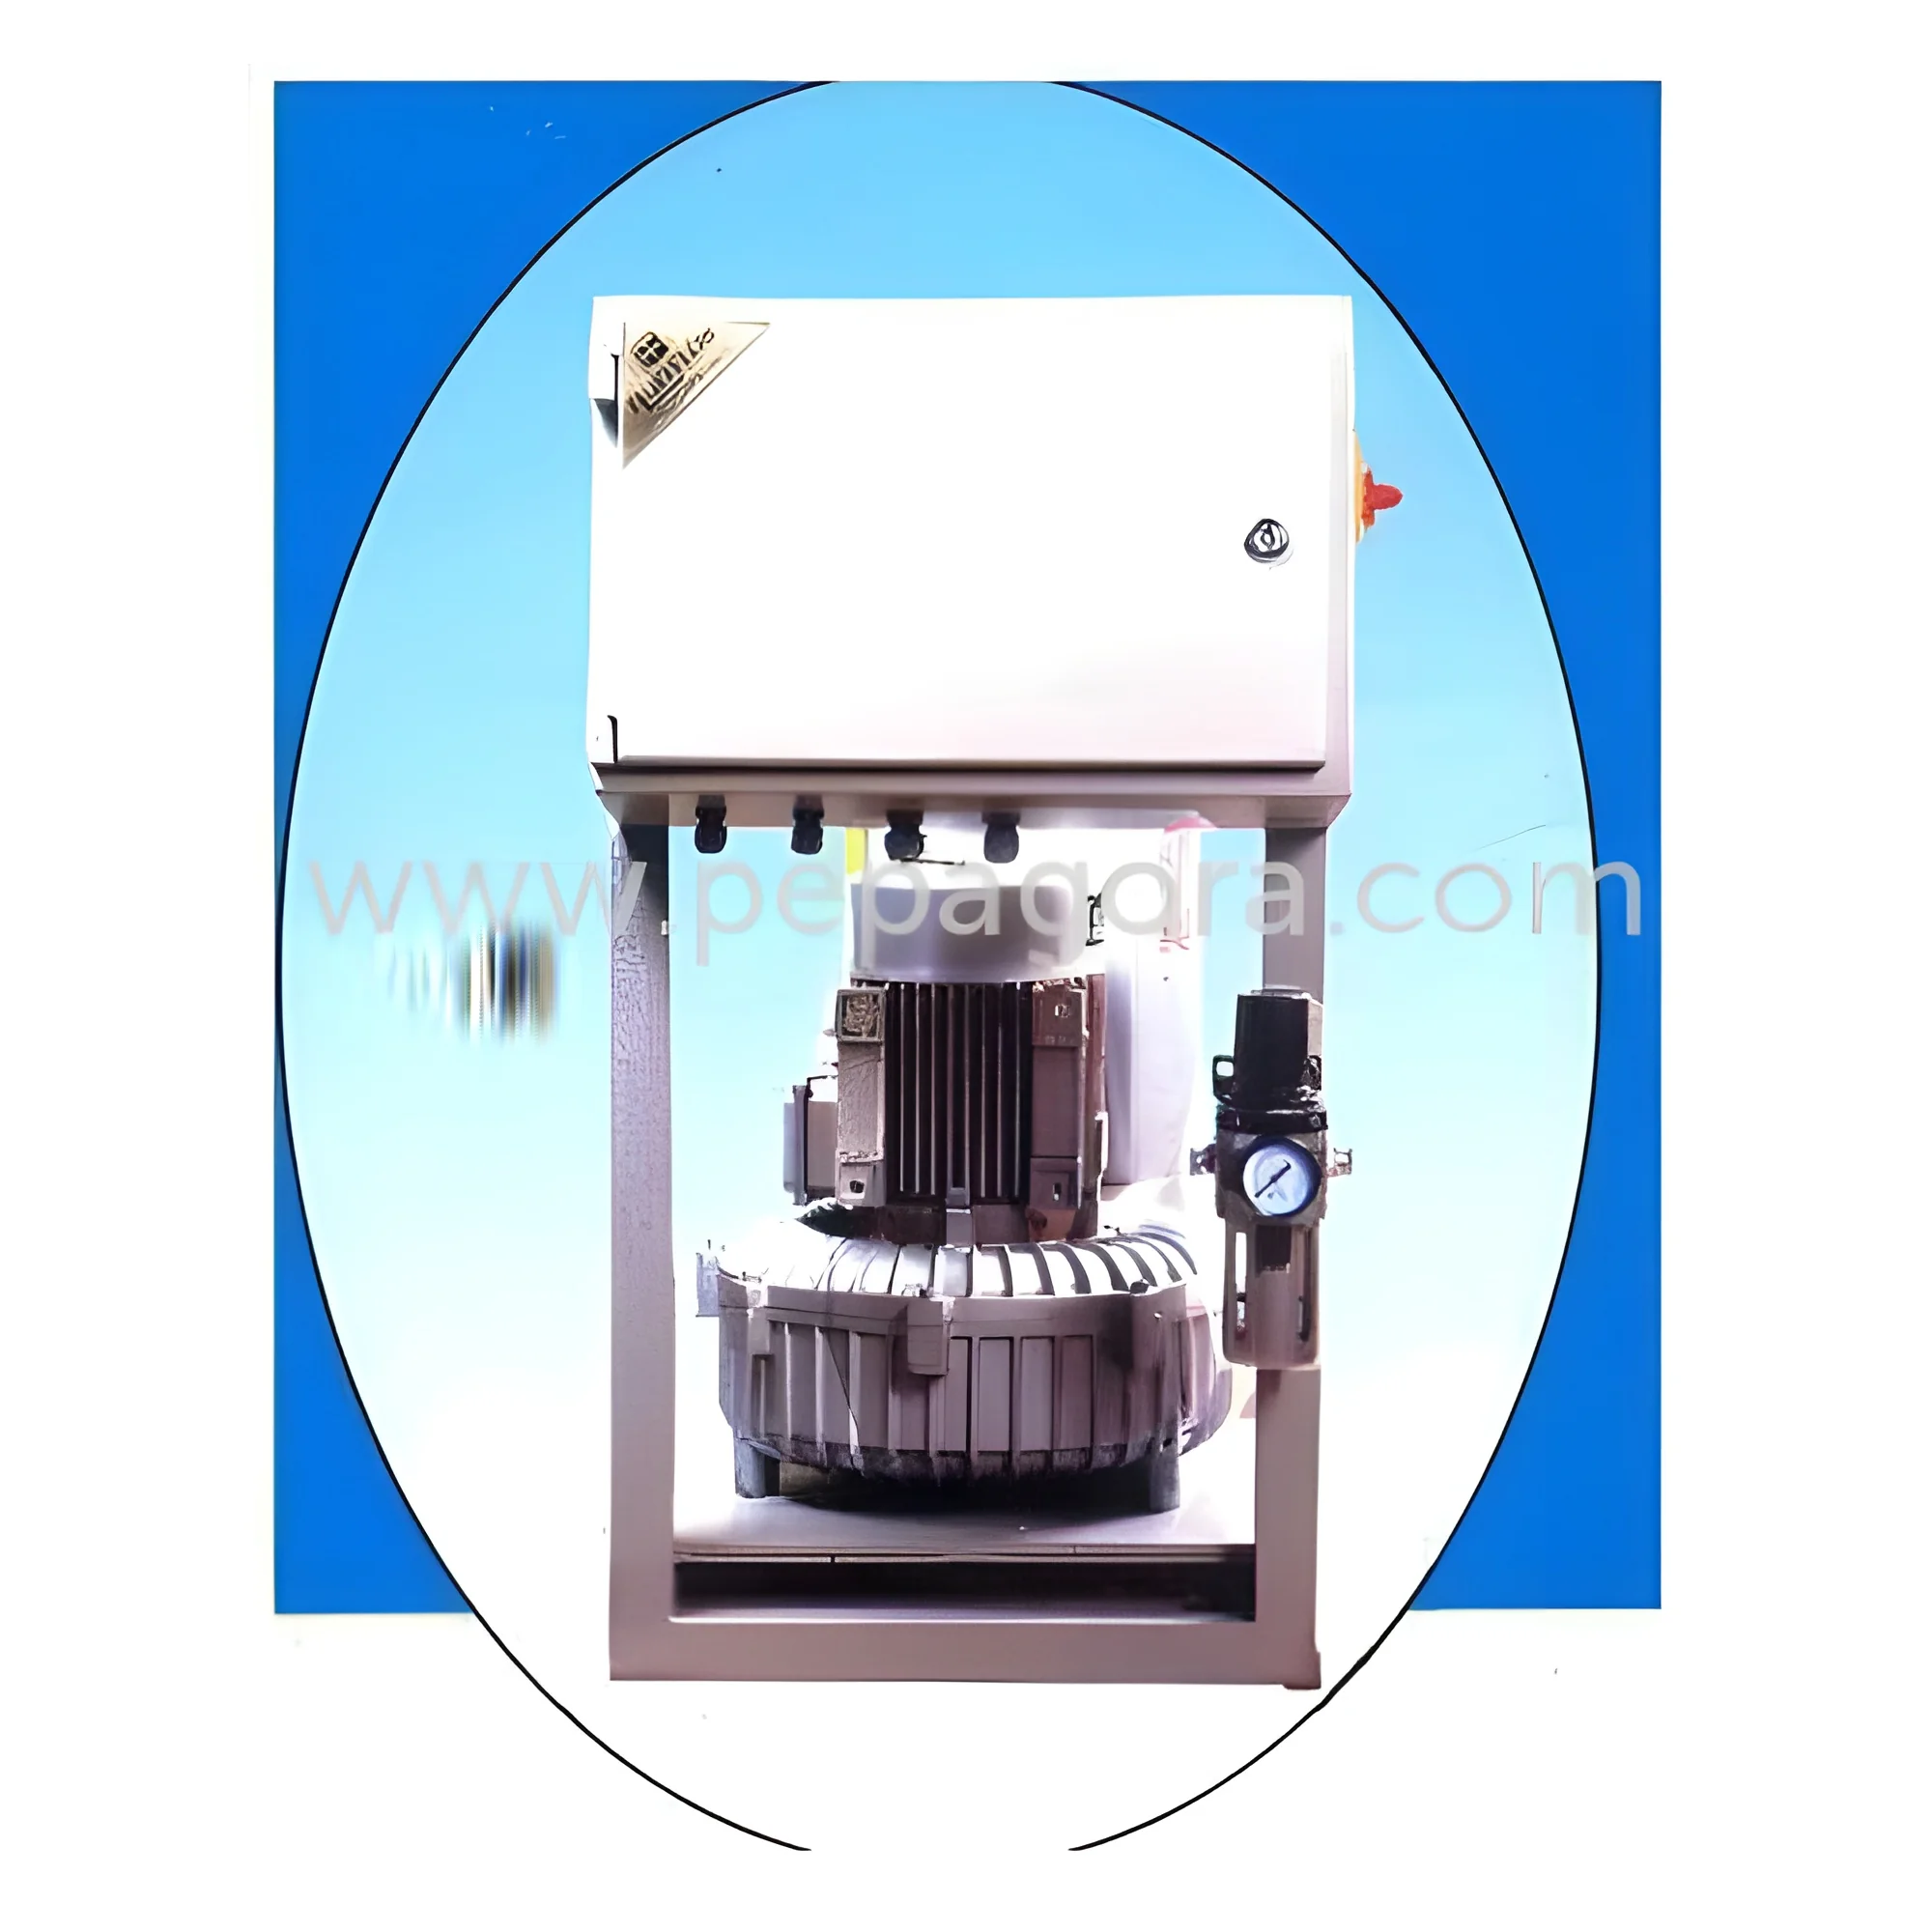
Our industrial vacuum conveying system represents advanced material handling technology designed specifically for transferring powders, granules, and bulk materials within manufacturing environments. Built with premium metal components and engineered for reliability, this system eliminates manual handling while ensuring product integrity throughout the transfer process. The standardized design incorporates dimensions and sizes tailored to individual operational needs. With easy installation capabilities and durable construction, this vacuum conveyor system delivers consistent performance while maintaining the highest standards of operational safety and material purity.

This vacuum conveying system serves critical functions across multiple industries including pharmaceutical manufacturing, food processing, chemical production, and plastics manufacturing. In pharmaceutical applications, it ensures contamination-free transfer of active ingredients and excipients between processing stages...
Our industrial vacuum conveying system represents advanced material handling technology designed specifically for transferring powders, granules, and bulk materials within manufacturing environments. Built with premium metal components and engineered for reliability, this system eliminates manual handling while ensuring product integrity throughout the transfer process. The standardized design incorporates dimensions and sizes tailored to individual operational needs. With easy installation capabilities and durable construction, this vacuum conveyor system delivers consistent performance while maintaining the highest standards of operational safety and material purity.

This vacuum conveying system serves critical functions across multiple industries including pharmaceutical manufacturing, food processing, chemical production, and plastics manufacturing. In pharmaceutical applications, it ensures contamination-free transfer of active ingredients and excipients between processing stages. Food manufacturers utilize these systems for hygienic handling of ingredients like flour, sugar, and additives while maintaining compliance with food safety standards. Chemical plants benefit from the system's ability to handle various powder compositions safely, while plastic manufacturers rely on it for efficient pellet transfer between storage and processing equipment.

The business value of our industrial vacuum conveying system extends beyond material transfer capabilities. It significantly reduces operational costs by minimizing product loss, decreasing labor requirements, and preventing contamination-related waste. The reliable metal construction ensures minimal downtime and reduced maintenance costs, while the easy installation feature allows for quick implementation without major production disruptions. Manufacturers gain competitive advantage through improved production efficiency, consistent product quality, and enhanced workplace safety. The system's durability and standardized components ensure long-term operational reliability, making it a worthwhile investment for businesses looking to optimize their material handling processes.

Key Features:
- Robust metal construction for exceptional durability and longevity
- Standardized design ensuring reliability and consistent performance
- Easy installation process minimizing setup time and complexity
- OEM supply type with comprehensive manufacturing support
- Efficient powder and bulk material transfer capabilities

Benefits:
- Reduced operational costs through minimized product loss
- Decreased labor requirements and improved efficiency
- Prevention of contamination-related waste
- Minimal downtime with reduced maintenance costs
- Enhanced workplace safety and product quality
Specifications
| Key Attributes | |
|---|---|
| Type | Vaccum Conveyors |
| Supply Type | OEM |
| Price | Negotiable |
| Material | Metal |
| Features | Reliable and Durable |
| Size | As per Clients Request |
| Dimension | Customized |
| Condition | New |
| Standard or Non Standard | Standard |
| Advantage | Easy to install |
| Delivery | On Time Delivery |
| Application | Industrial Applications |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial vacuum conveying systems efficiently transfer powders, granules, and bulk materials across production facilities. These systems eliminate manual handling while maintaining product integrity and preventing contamination during transport processes. They are essential for maintaining clean, efficient material flow in demanding industrial environments where precision and hygiene are critical operational requirements.
These conveying solutions serve diverse sectors including pharmaceuticals, food processing, chemicals, and plastics manufacturing. The standardized design allows seamless integration into existing production lines while meeting specific industry compliance standards. Their robust metal construction ensures long-term reliability even in continuous operation scenarios with abrasive or sensitive materials.
- Pharmaceutical powder transfer between mixing and tablet compression machines
- Food grade material handling in baking and confectionery production lines
- Chemical powder conveyance in manufacturing and packaging operations
- Plastic pellet transportation in injection molding and extrusion facilities
- Bulk material transfer in agricultural and construction chemical processing
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Fluid Flow Systems, Tamil Nadu
 Tamil Nadu, India
Raw Materials & Chemicals•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Vacuum Conveyors Metal OEM Reliable Durable Easy Install
Industrial vacuum conveyors for efficient powder and bulk material transfer. Metal construction ensures reliable, durable performance with easy installation. Ideal for pharmaceutical, food, and chemical industries.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Fluid Flow Systems
 Tamil Nadu, India
Raw Materials & ChemicalsManufacturer