IN
₹
Apparel & Fashion
Description
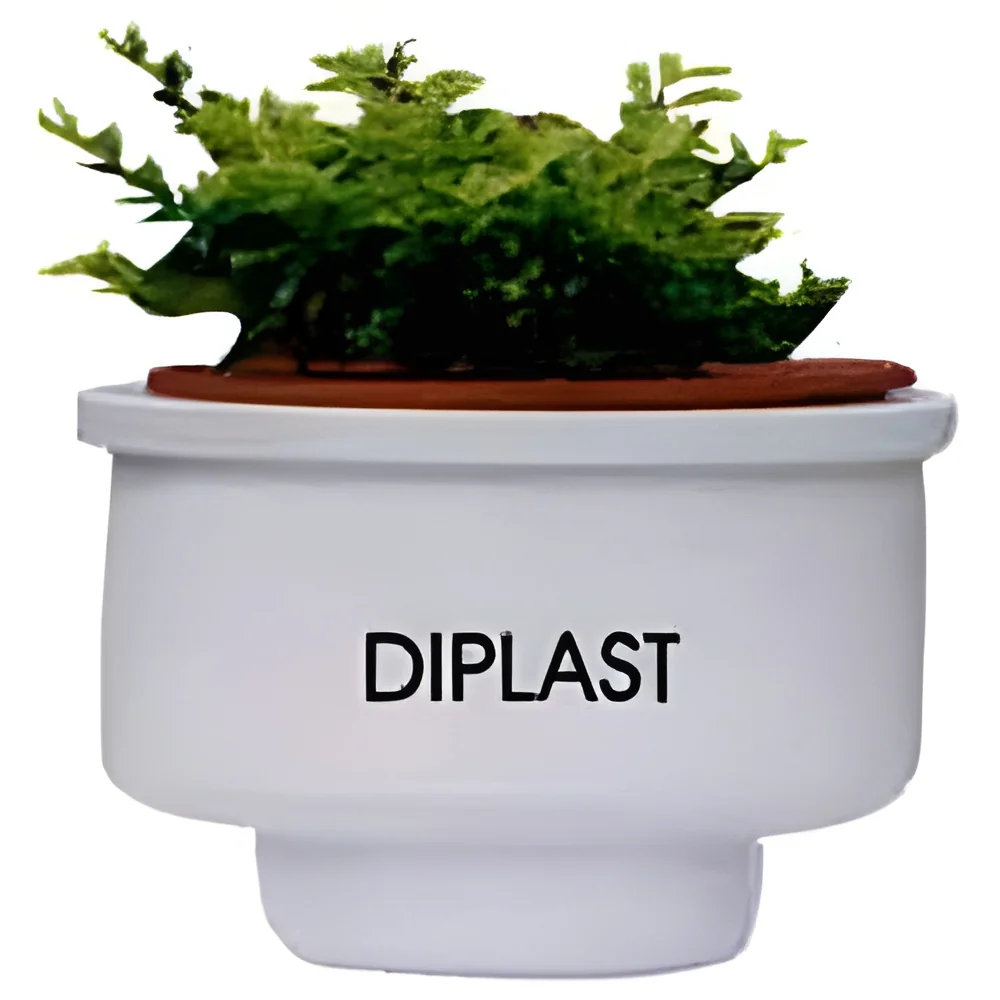
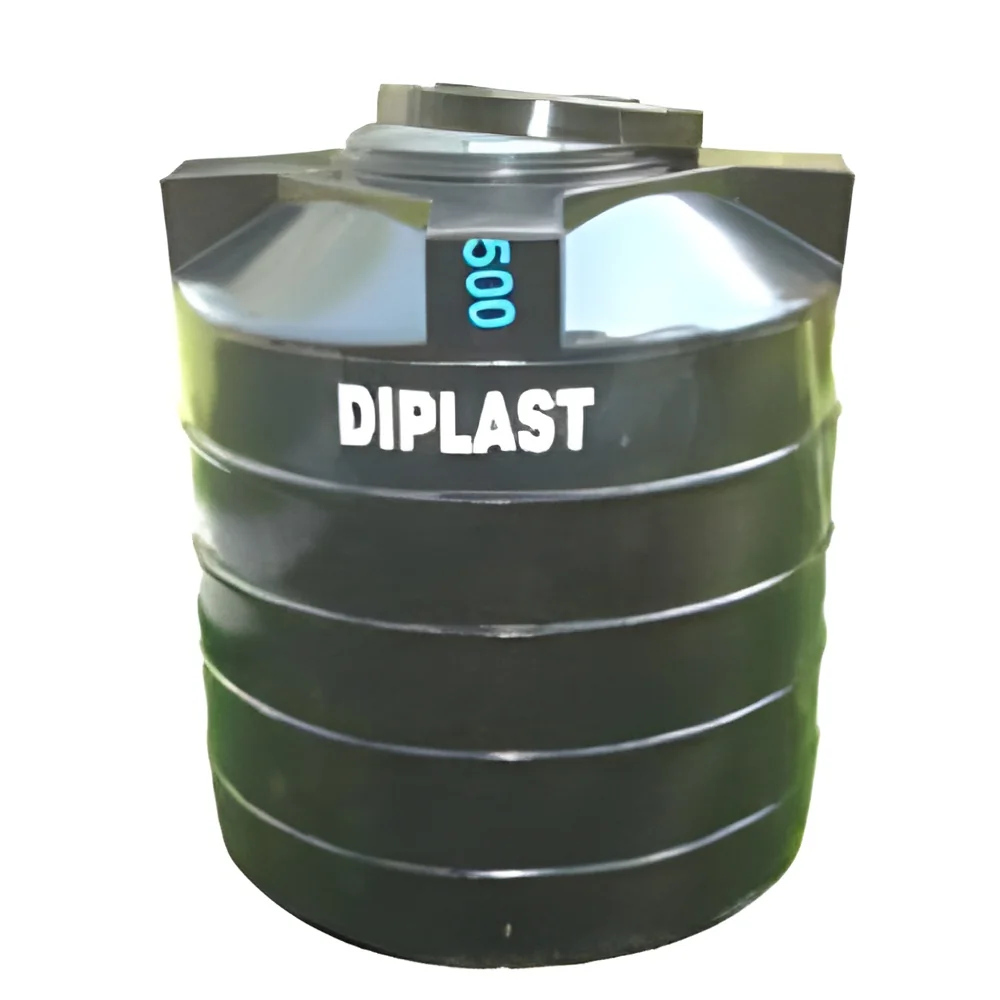
Our industrial transparent tanks are engineered for demanding applications where visibility, durability, and reliability are essential operational requirements. Manufactured from high-grade transparent materials, these tanks provide exceptional clarity while maintaining resistance to impacts, chemicals, and temperature variations. Each unit is designed for seamless integration into existing systems and undergoes rigorous quality testing to ensure compliance with industry standards for performance and safety. The transparent design enables continuous monitoring of contents, reducing the need for manual inspections while enhancing operational efficiency and process control capabilities for various liquid storage and handling applications.

Multiple industries depend on these transparent tanks for their critical operations and processing needs. Chemical processing facilities utilize them for safe storage of corrosive substances while maintaining visual access for level checks and conditio...
Our industrial transparent tanks are engineered for demanding applications where visibility, durability, and reliability are essential operational requirements. Manufactured from high-grade transparent materials, these tanks provide exceptional clarity while maintaining resistance to impacts, chemicals, and temperature variations. Each unit is designed for seamless integration into existing systems and undergoes rigorous quality testing to ensure compliance with industry standards for performance and safety. The transparent design enables continuous monitoring of contents, reducing the need for manual inspections while enhancing operational efficiency and process control capabilities for various liquid storage and handling applications.

Multiple industries depend on these transparent tanks for their critical operations and processing needs. Chemical processing facilities utilize them for safe storage of corrosive substances while maintaining visual access for level checks and condition monitoring. Pharmaceutical manufacturers rely on them for hygienic liquid storage and mixing under controlled environmental conditions. The food processing sector benefits from their non-toxic, easy-to-clean surfaces for ingredient storage and product handling. Water treatment plants incorporate them for chemical dosing and process monitoring, while agricultural operations use them for fertilizer storage and distribution systems requiring visual verification.

Businesses select our transparent tanks for their long-term value, reduced maintenance requirements, and operational reliability. The leak-proof construction ensures minimal downtime and prevents costly spills or contamination incidents. Despite their robust construction, these tanks remain lightweight for easy installation and relocation, saving both time and labor costs. Their resistance to extreme temperatures and environmental factors makes them suitable for diverse operating conditions. The availability of custom sizing options provides tailored solutions for specific operational needs, while the durable materials ensure extended service life and consistent performance, delivering strong return on investment for professional users.

Key Features:
- High transparency material allows clear visual monitoring of liquid levels and conditions
- Leak-proof construction with reinforced seams ensures secure liquid containment
- Chemical-resistant properties withstand exposure to various industrial substances
- Temperature tolerance maintains performance across diverse operating environments
- Custom sizing options available to meet specific space and capacity requirements

Benefits:
- Enhanced process control through continuous visual monitoring of liquid contents
- Reduced maintenance costs with durable, corrosion-resistant construction
- Improved safety with leak-proof design preventing spills and contamination
- Operational flexibility with compatibility across various temperature conditions
- Space optimization through custom sizing that fits specific facility layouts
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These transparent tanks are essential across industries where visual monitoring of liquid processes is critical for quality control and safety. Operators can easily check fluid levels, observe color changes, and detect contamination without opening the system, maintaining process integrity while reducing contamination risks. The durable construction withstands various chemicals and temperature ranges, making these tanks versatile for multiple industrial environments and applications requiring reliable liquid containment solutions.
Manufacturing facilities benefit from these clear tanks for storing acids, solvents, and raw materials while maintaining visual oversight. Water treatment plants utilize them for chemical dosing and process observation, while food processing operations rely on them for ingredient mixing and storage visibility. The corrosion-resistant and non-reactive properties ensure safe handling of diverse substances, supporting both indoor and outdoor applications with consistent performance and reliability across different operational conditions.
- Chemical manufacturing facilities for safe storage and visual monitoring of acids, solvents, and industrial reagents
- Pharmaceutical production for mixing and storing liquid compounds with continuous quality verification
- Food processing plants for ingredient tanks, syrup storage, and fermentation process observation
- Water treatment operations to visually track chemical dosing, sedimentation, and filtration stages
- Laboratory and research settings for experimental setups requiring clear, non-reactive containers
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Diplast Plastics Ltd, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Transparent Tanks Clear Visibility Leak Proof Custom Sizes
Industrial transparent tanks provide clear visibility and leak-proof liquid storage for chemical, pharmaceutical, and food processing industries. These reliable tanks feature durable construction and are available in custom sizes to meet specific operational requirements.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Diplast Plastics Ltd
 Punjab, India
Industrial Equipment & MachineryManufacturer