- Industrial wastewater reduction systems.
- Water conservation projects.
- Sustainable boiler operation.
- Industrial utility management.
- Heat recovery installations.
- Steam energy optimization projects.
- Resource-efficient manufacturing facilities.

 IN
₹
Apparel & Fashion
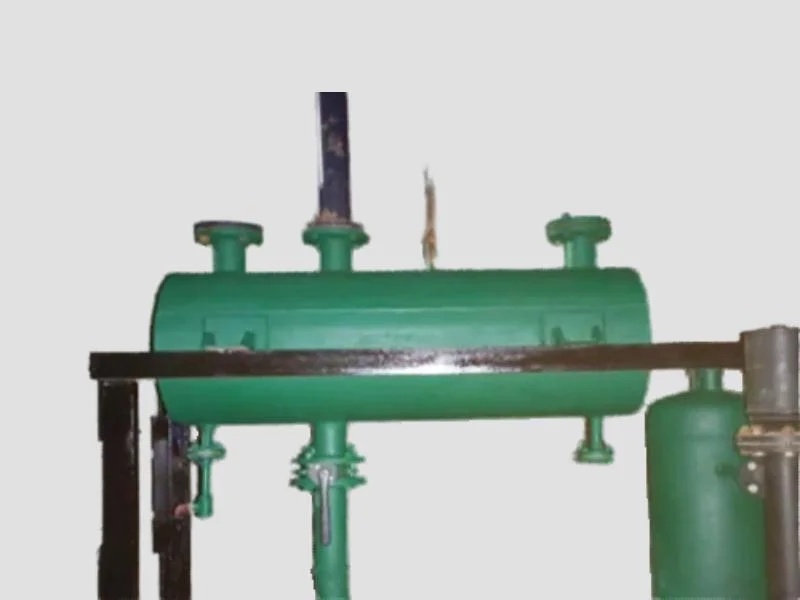
Description
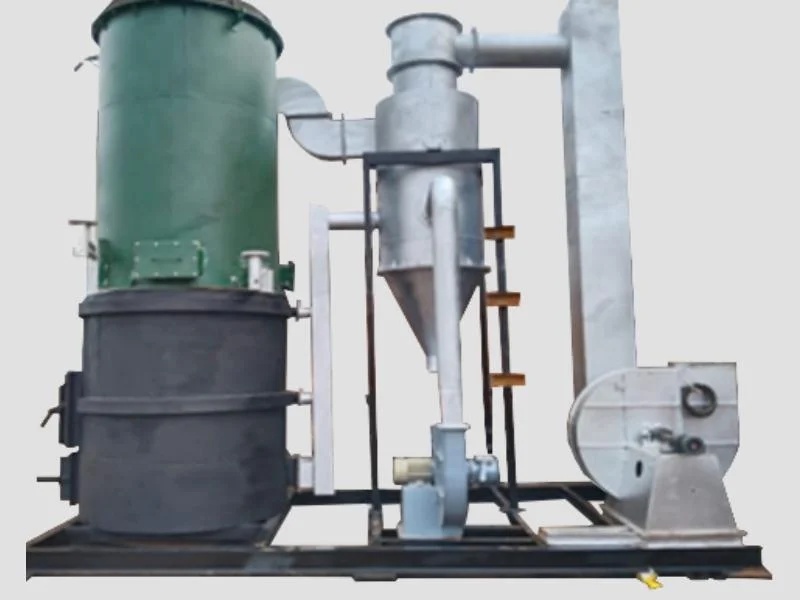
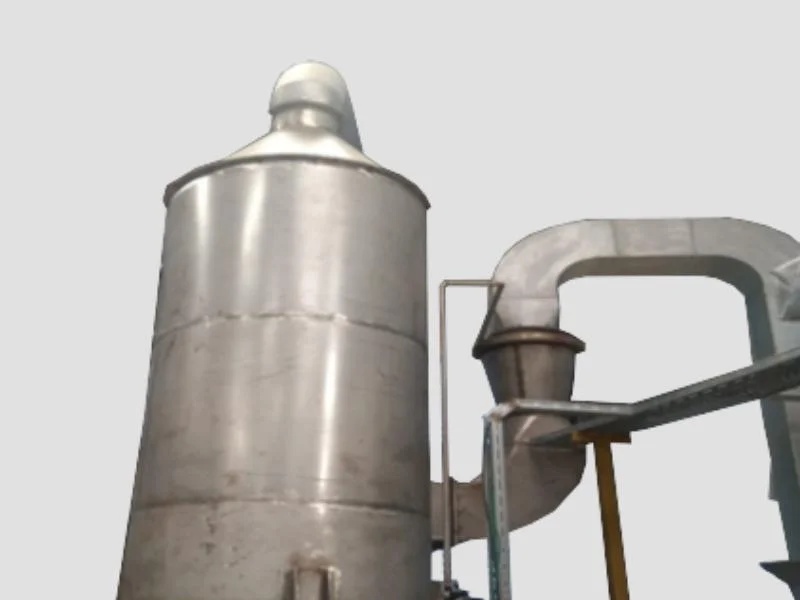
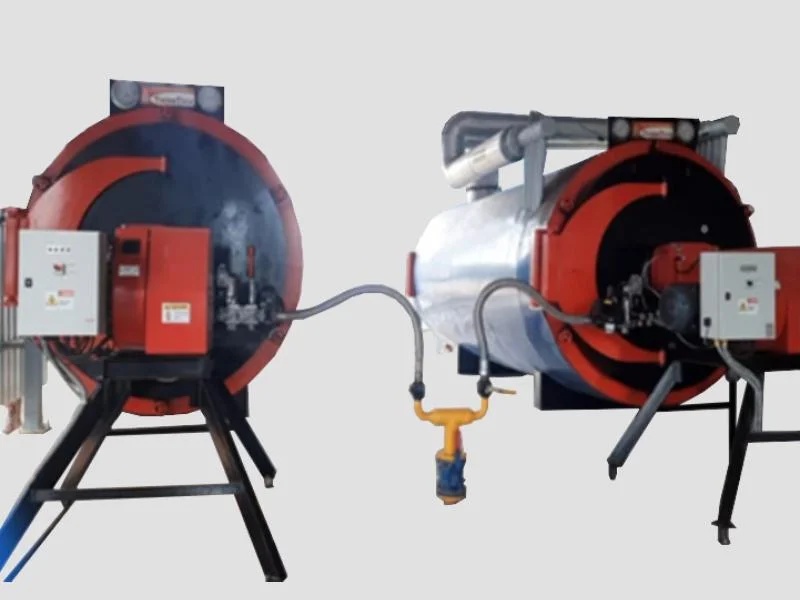
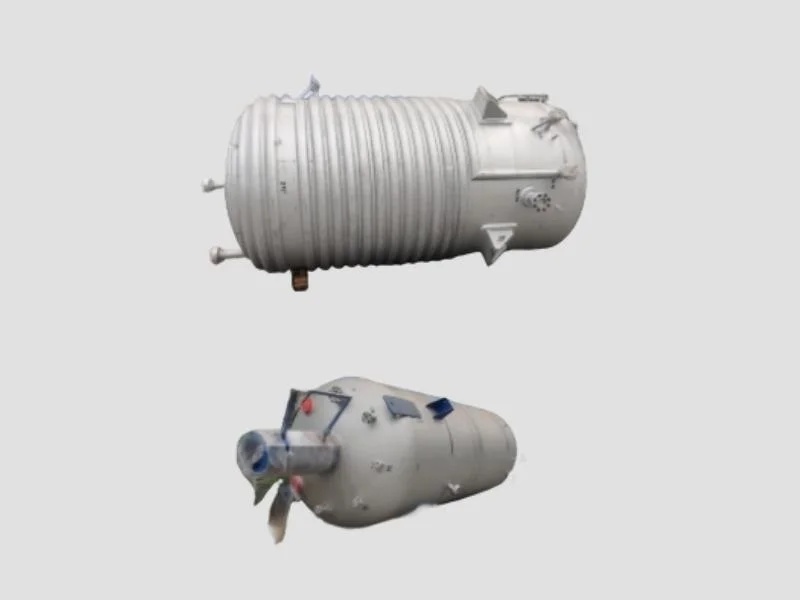
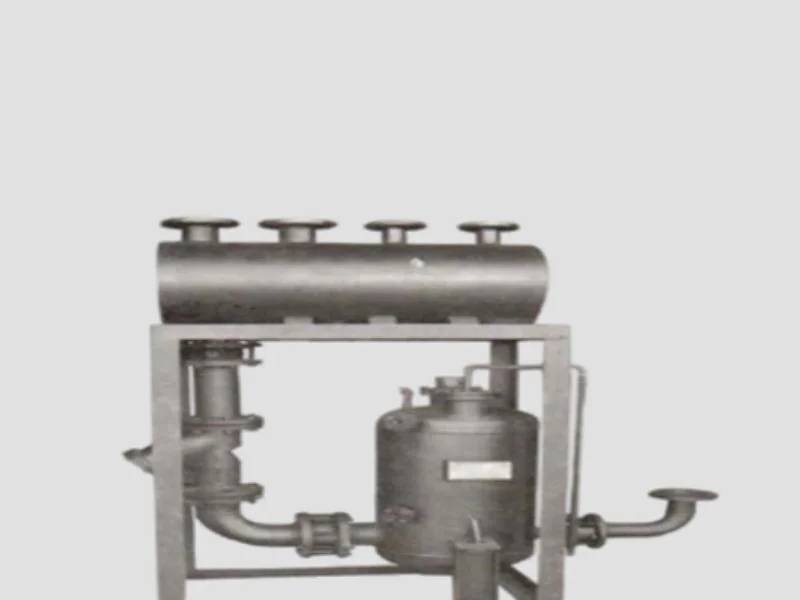
The Industrial Steam Condensate Recovery Unit is a versatile system designed for efficient condensate collection and reuse in various industrial applications. It helps recover hot water produced during steam operations and return it to the boiler system, reducing unnecessary heat and water losses. The equipment can be customized with suitable tank capacities, pumping arrangements, control panels, and piping connections according to plant requirements. Its operation contributes to better thermal efficiency, lower fuel consumption, and reduced wastewater generation. Built for integration into industrial steam networks, it is suitable for textile manufacturing, chemical processing, food production, pharmaceutical plants, paper mills, and power generation facilities.
Specifications
| Key Attributes | |
|---|---|
| Product Type | Industrial Condensate Recovery System |
| Application | Steam Condensate Recovery |
| Usage | Industrial Boiler Systems |
| Operation | Automatic |
| Energy Efficiency | Reduces Fuel And Water Consumption |
| Cost Savings | Lowers Operational Expenses |
| Function | Collection, Storage And Return Of Condensate |
| Pump Type | Condensate Transfer Pump |
| Tank Type | Condensate Collection Tank |
| Additional Information | |
|---|---|
| SKU | 1 |
| Country of Origin | India |
Application
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
| Payment Methods |
|
Shipping & Logistics
| Shipping Internationally | No | |
| Methods |
| |
| IncoTerms |
|
Company Profile
ThermTech Systems, Tamil Nadu
 Tamil Nadu, India
Manufacturer
Factory Details
Factory Size1000-5000 sqm
Annual Production Capacity0
Main Markets
Oceania
Mid East
South Asia
Frequently Asked Questions
1
What is a Condensate Recovery Unit?
A Condensate Recovery Unit is an industrial system designed to capture and reuse condensate water from steam systems, improving efficiency and reducing waste.
2
How does a Condensate Recovery Unit work?
It collects condensate from steam processes, separates it from other fluids, and then pumps it back into the boiler or steam system for reuse.
3
What are the benefits of using a Condensate Recovery Unit?
Benefits include increased energy savings, reduced water costs, lower wastewater disposal fees, and improved overall efficiency of steam systems.
4
Can this unit be customized for specific industrial applications?
Yes, many manufacturers offer customization options to tailor the unit's specifications to meet particular needs in various industrial environments.
5
What payment methods do you accept for purchasing the Condensate Recovery Unit?
We accept payments via credit card, cheque, demand draft, and cash. Choose whichever method is most convenient for you at checkout.
SKU: 1
Condensate Recovery Unit
Optimize your steam generation process with an Industrial Condensate Recovery Unit. Designed for efficient condensate collection and return, it helps maintain boiler water availability, reduce heat losses, and minimize environmental impact. Suitable for manufacturing plants and commercial industrial facilities.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Shipping InternationallyNo
ThermTech Systems
 Tamil Nadu, India
Manufacturer