IN
₹
Apparel & Fashion

Description
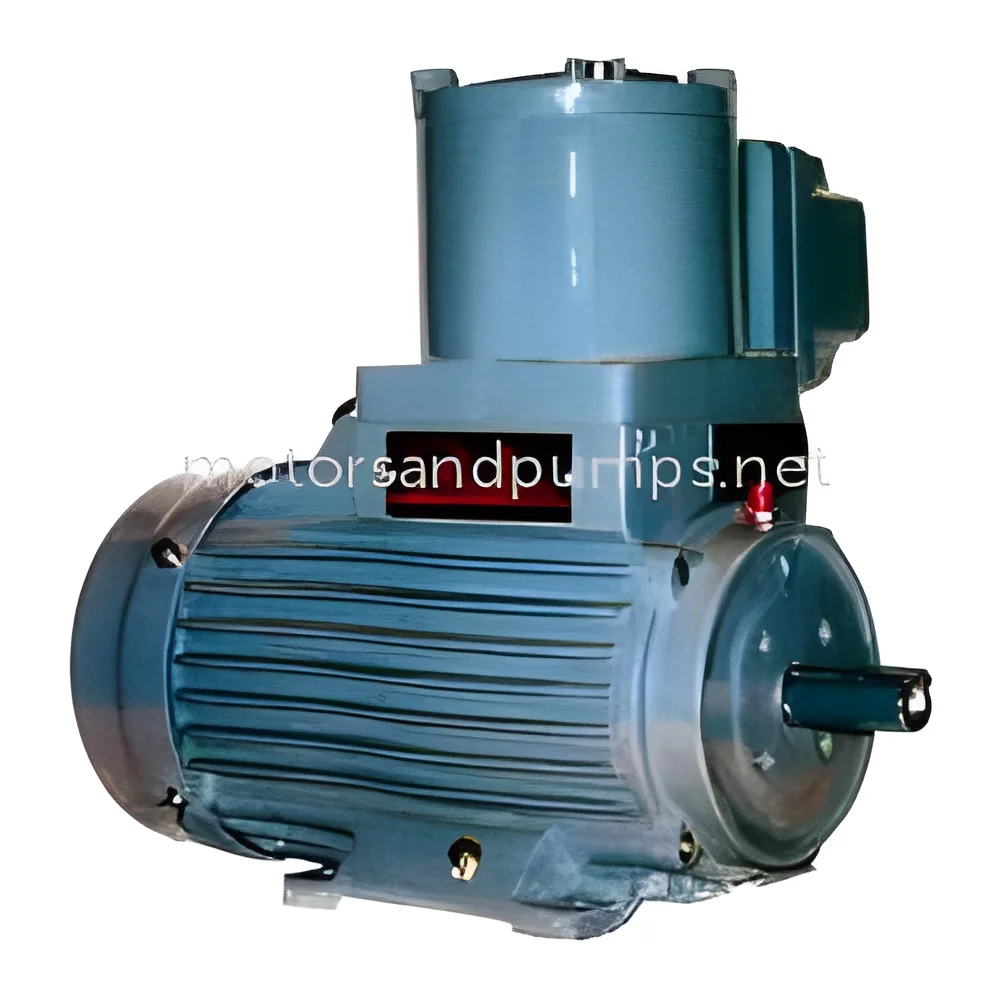
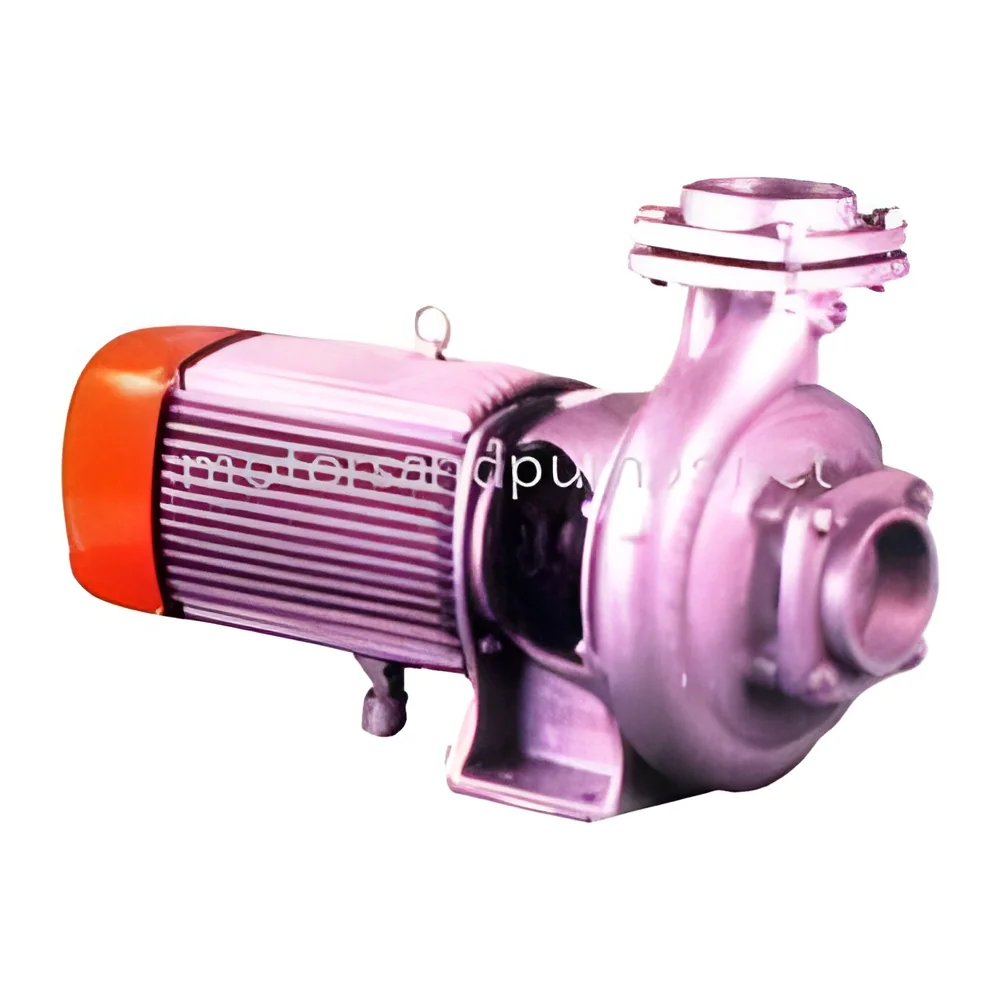
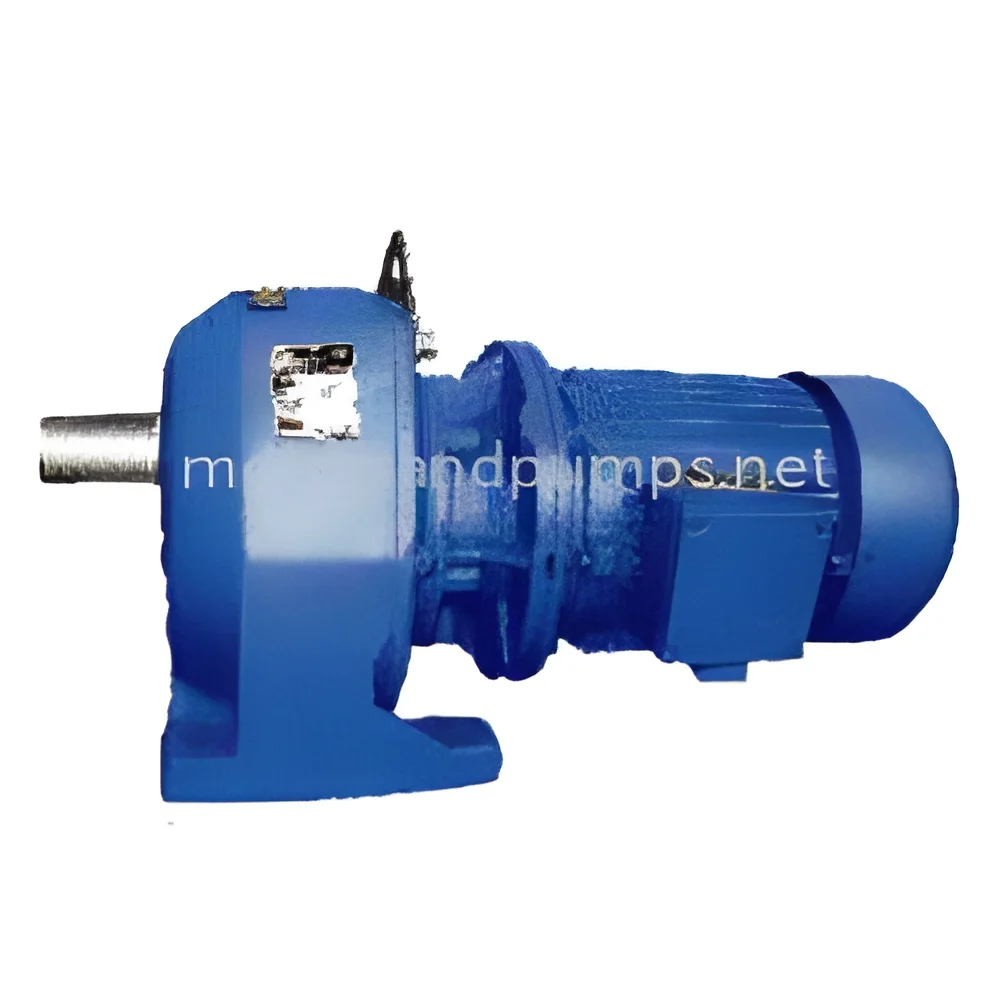
Industrial stainless steel pumps deliver reliable performance for demanding fluid transfer applications across multiple sectors. Constructed from high-grade corrosion-resistant materials, these pumps handle everything from pure water to aggressive chemical solutions with consistent operation. Engineered for continuous use in challenging industrial environments, they reduce downtime and maintenance requirements while ensuring operational safety through superior sealing technology and robust construction design.

These pumps serve critical functions in industries where reliability and material compatibility are essential. Chemical processing facilities utilize them for safe transfer of corrosive liquids and solvents without degradation risks. Food production operations depend on them for ingredient transfer while maintaining strict sanitary standards. Water treatment plants employ these pumps for chemical dosing and fluid transfer operations, while pharmaceutical manufacturers rely on th...
Industrial stainless steel pumps deliver reliable performance for demanding fluid transfer applications across multiple sectors. Constructed from high-grade corrosion-resistant materials, these pumps handle everything from pure water to aggressive chemical solutions with consistent operation. Engineered for continuous use in challenging industrial environments, they reduce downtime and maintenance requirements while ensuring operational safety through superior sealing technology and robust construction design.

These pumps serve critical functions in industries where reliability and material compatibility are essential. Chemical processing facilities utilize them for safe transfer of corrosive liquids and solvents without degradation risks. Food production operations depend on them for ingredient transfer while maintaining strict sanitary standards. Water treatment plants employ these pumps for chemical dosing and fluid transfer operations, while pharmaceutical manufacturers rely on their precision for sensitive production processes requiring contamination-free fluid handling.

The operational value extends beyond initial investment through reduced total cost of ownership and enhanced process reliability. Their durable construction minimizes breakdowns and maintenance needs, directly impacting productivity and operational continuity. Corrosion-resistant properties ensure consistent performance with aggressive media, protecting processes from contamination and equipment failure. These pumps represent long-term investments in operational efficiency, delivering sustained value through reliable performance in demanding industrial applications.

Key Features:
- High-grade corrosion-resistant stainless steel construction for durability
- Engineered for continuous reliable operation in demanding conditions
- Superior sealing technology prevents leaks and ensures operational safety
- Compatible with wide range of fluids including water, chemicals, and food products
- Robust design minimizes maintenance requirements and extends service life

Benefits:
- Reduced downtime through reliable continuous operation capabilities
- Long-term cost savings from minimal maintenance and extended service life
- Enhanced process safety with leak prevention and corrosion resistance
- Versatile application across multiple industrial sectors and fluid types
- Consistent performance protection for critical operational processes
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These stainless steel pumps handle diverse industrial fluids from water to aggressive chemicals with consistent performance. Engineered for durability in challenging environments, they support continuous operation across multiple sectors where reliability is critical for uninterrupted processes and operational efficiency.
Industries including chemical processing, food production, and water treatment rely on these corrosion-resistant pumps for safe fluid transfer. Their robust construction ensures longevity when handling abrasive or corrosive media, making them ideal for businesses requiring dependable pumping solutions that maintain performance across varying operational requirements.
- Chemical plants transferring acids, solvents, and corrosive liquids safely
- Food processing facilities moving ingredients and edible products with hygiene compliance
- Water treatment plants dosing chemicals and transferring treated water efficiently
- Pharmaceutical manufacturers handling precise fluid transfer in production processes
- Industrial cooling systems circulating water and heat transfer fluids reliably
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Industrial Stainless Steel Pumps For Chemical Food Water Transfer
Industrial stainless steel pumps for reliable chemical, food, and water transfer applications. Built for corrosion resistance and continuous operation across demanding industrial environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company