IN
₹
Apparel & Fashion
Description
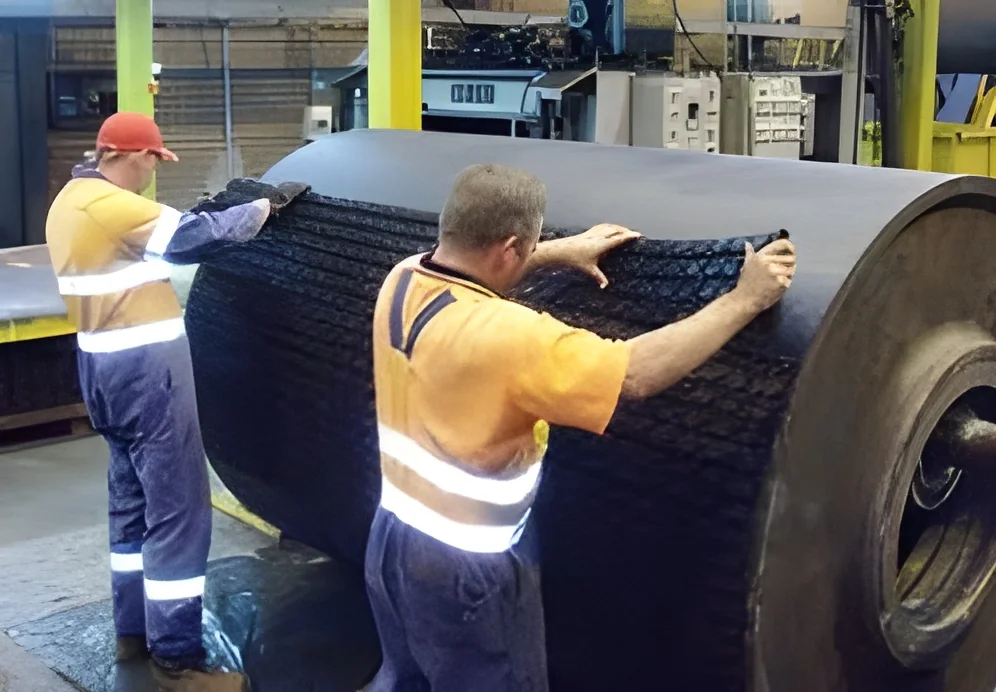
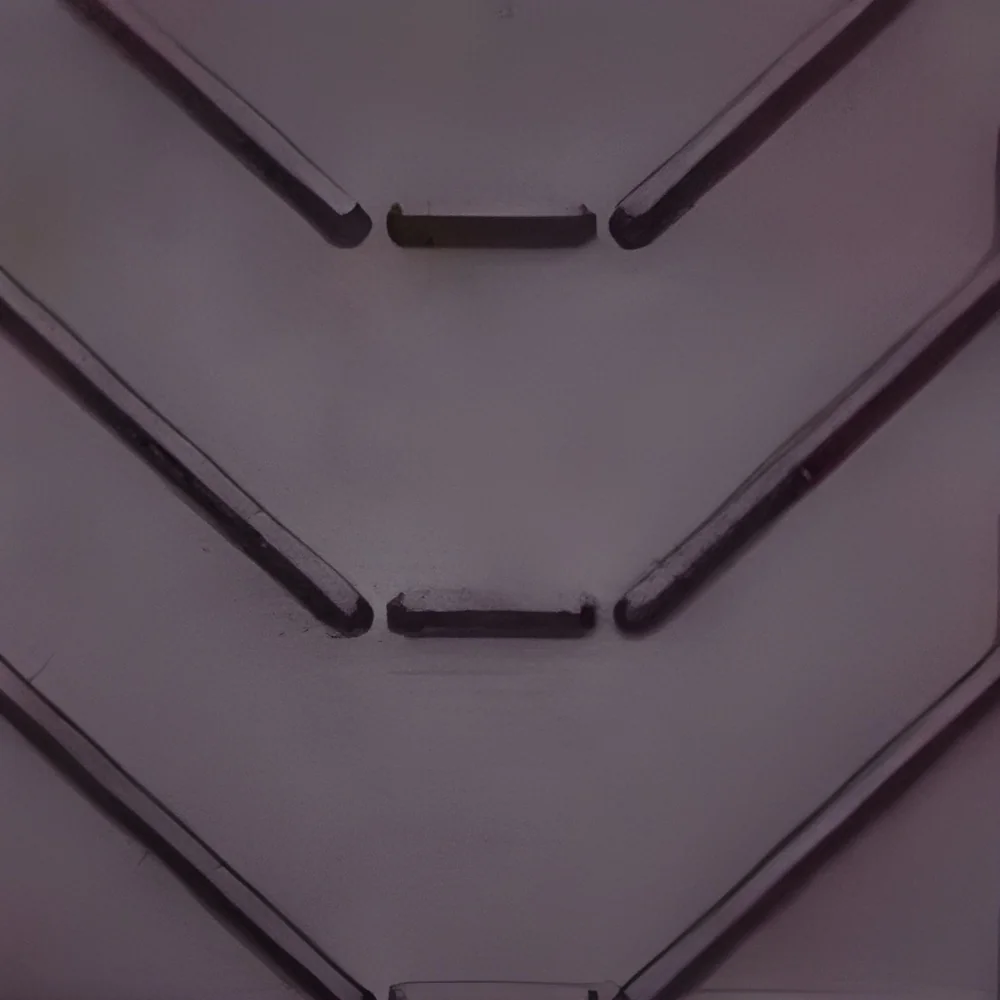
Our premium special purpose conveyor belts represent the pinnacle of material handling technology, engineered for superior performance in demanding industrial environments. Constructed from high-grade materials including industrial rubber, PVC, polyurethane, and steel cord reinforcement, these belts deliver exceptional durability and reliability. They are specifically designed to transport both heavy and lightweight materials across various industrial settings, ensuring smooth operation and minimal downtime. The precision engineering guarantees consistent performance while maintaining exact specifications for seamless integration with existing conveyor systems and operational requirements.

These conveyor belts serve critical functions across multiple industries including mining, manufacturing, logistics, and food processing. In mining operations, they handle heavy ores and aggregates under extreme conditions with unmatched reliability. Manufacturing facilities depend on them for movin...
Our premium special purpose conveyor belts represent the pinnacle of material handling technology, engineered for superior performance in demanding industrial environments. Constructed from high-grade materials including industrial rubber, PVC, polyurethane, and steel cord reinforcement, these belts deliver exceptional durability and reliability. They are specifically designed to transport both heavy and lightweight materials across various industrial settings, ensuring smooth operation and minimal downtime. The precision engineering guarantees consistent performance while maintaining exact specifications for seamless integration with existing conveyor systems and operational requirements.

These conveyor belts serve critical functions across multiple industries including mining, manufacturing, logistics, and food processing. In mining operations, they handle heavy ores and aggregates under extreme conditions with unmatched reliability. Manufacturing facilities depend on them for moving components and assemblies along production lines, while food processing plants utilize specialized versions for safe ingredient handling. Logistics and distribution centers implement these belts in automated sorting systems for efficient package movement, and agricultural operations benefit from their robust construction for transporting harvested crops. Each industry receives belts perfectly suited to their specific environmental and operational challenges.

The business value of our special purpose belts lies in their proven reliability, reduced maintenance requirements, and extended service life, which directly translates to lower operational costs and increased productivity. Their robust construction minimizes unexpected downtime, while the precise engineering ensures perfect system compatibility. The use of premium materials and steel cord reinforcement provides exceptional strength and durability, making them a smart long-term investment for businesses seeking to optimize their material handling processes. These belts represent a commitment to quality that serious industrial buyers can trust for their most demanding applications and challenging operational conditions.

Key Features:
- Constructed from premium materials including rubber, PVC, PU, and steel cord
- Engineered for both heavy and lightweight material transportation
- Designed for compatibility with various conveyor system types
- Built to withstand abrasive materials and high temperatures
- Precision engineering for reliable performance and durability

Benefits:
- Reduced maintenance requirements and extended service life
- Lower operational costs through increased productivity
- Minimal unexpected downtime for continuous operations
- Perfect system compatibility for seamless integration
- Exceptional strength and durability for long-term value
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Special purpose conveyor belts are engineered for demanding material handling applications across diverse industries. These belts transport everything from lightweight packages to heavy bulk materials with consistent reliability. Their robust construction ensures perfect compatibility with existing conveyor systems and specific operational requirements, delivering dependable performance in challenging environments.
Manufactured from premium materials including rubber, PVC, PU, and reinforced steel cord, these belts offer superior strength and longevity. They withstand abrasive materials, high temperatures, and continuous operation without compromising performance. The precise engineering guarantees smooth material flow and reduced maintenance needs, making them ideal for various industrial settings where reliability is paramount.
- Mining operations for transporting heavy ores, coal, and aggregates over extended distances
- Food processing facilities for hygienic movement of ingredients and packaged products
- Airport baggage handling systems for efficient luggage sorting and transfer
- Automotive manufacturing plants for moving components along assembly lines
- Warehouse distribution centers for automated sorting and package transportation
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arushi Engineers, Andhra Pradesh
 Andhra Pradesh, India
Construction•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Premium Special Purpose Conveyor Belts For Heavy And Lightweight Material Handling
Premium special purpose conveyor belts handle heavy and lightweight materials with rubber, PVC, PU, or steel cord construction for reliable performance across industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arushi Engineers
 Andhra Pradesh, India
ConstructionManufacturer